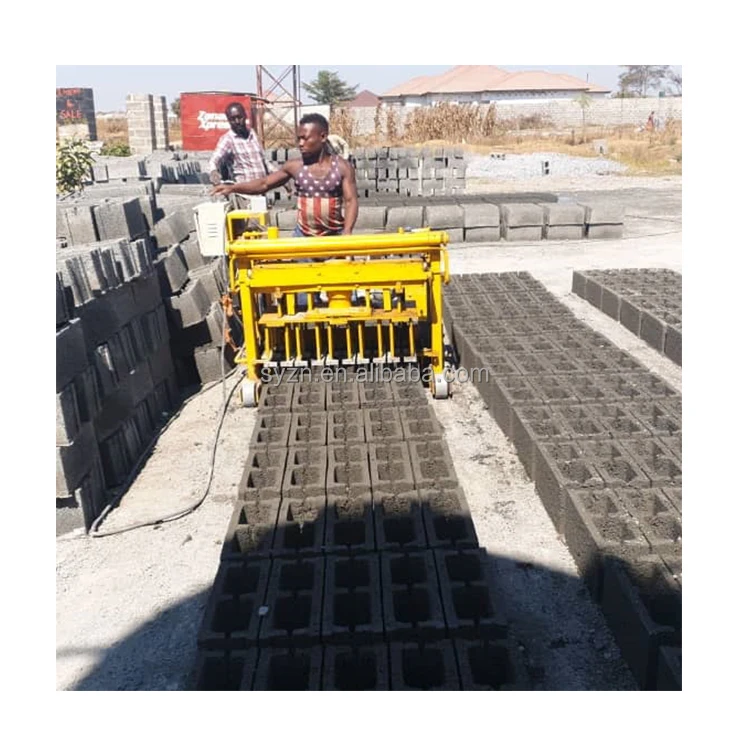
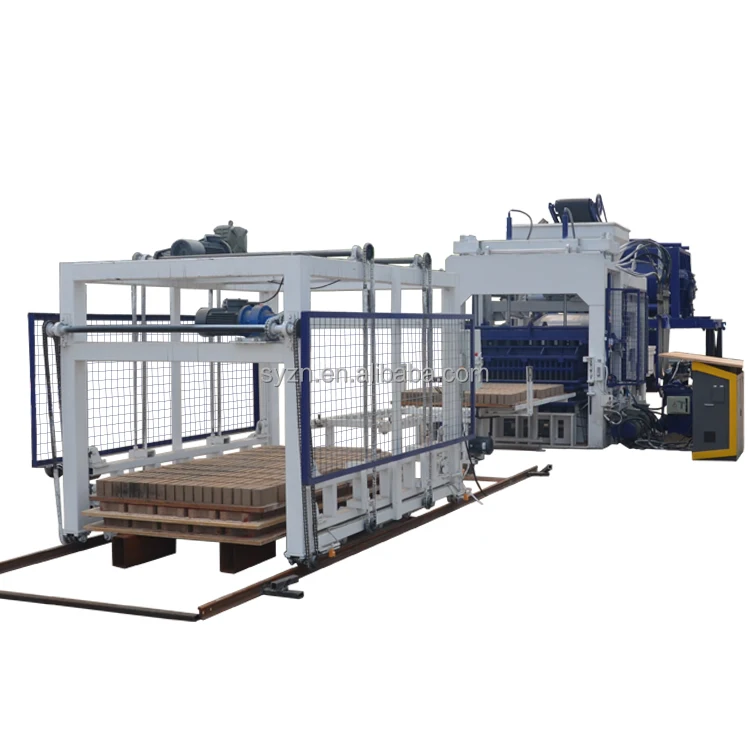
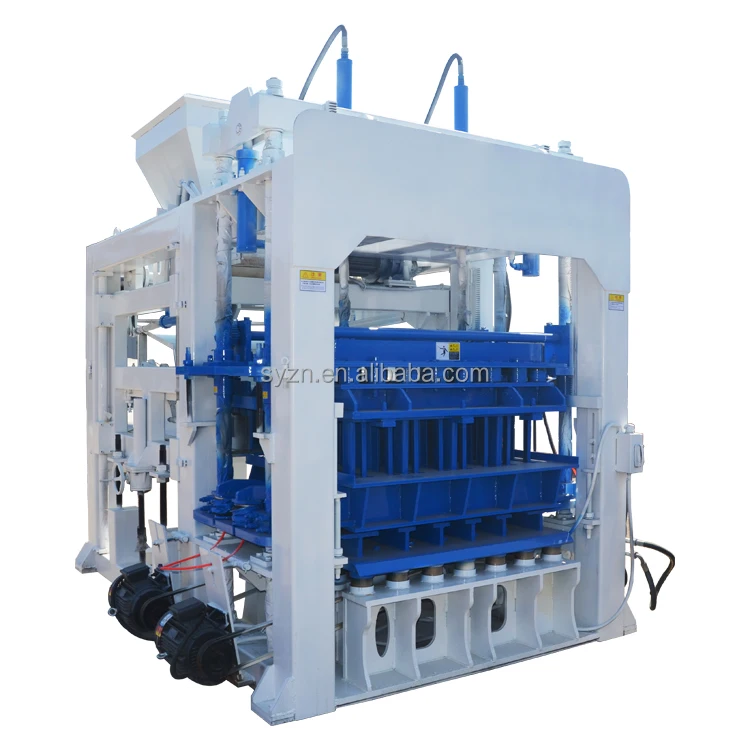
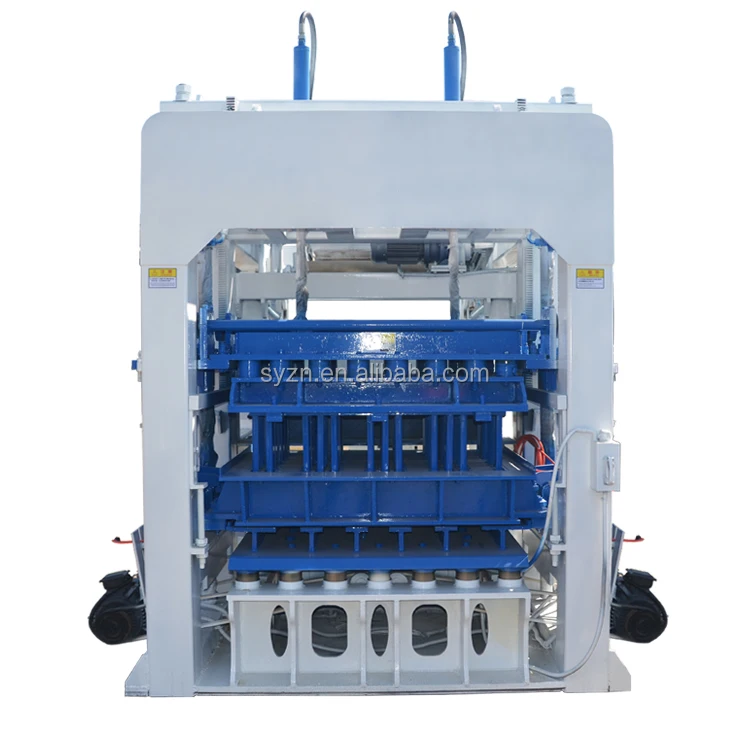

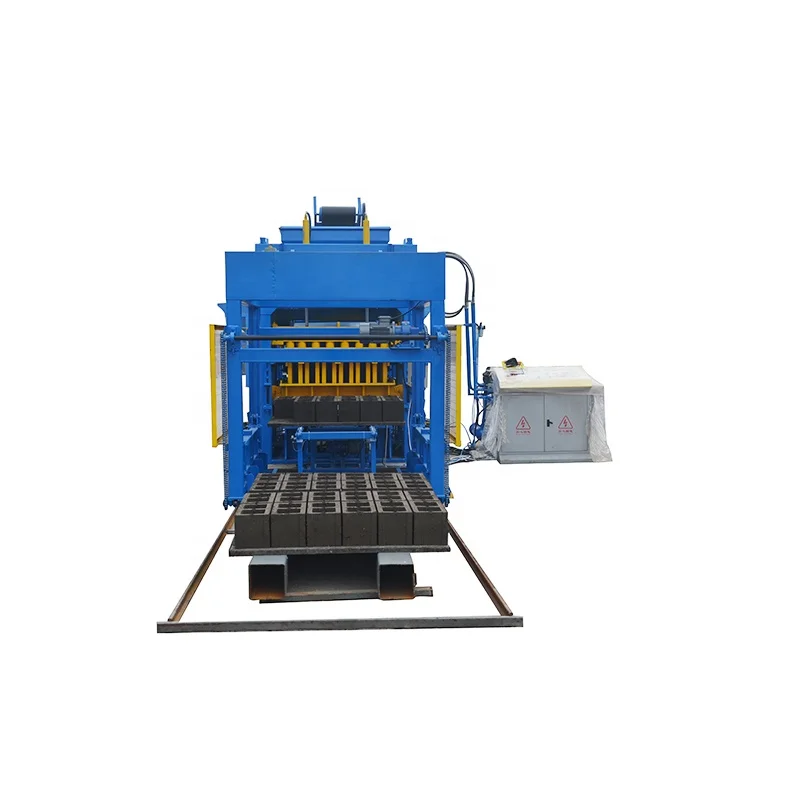
Description
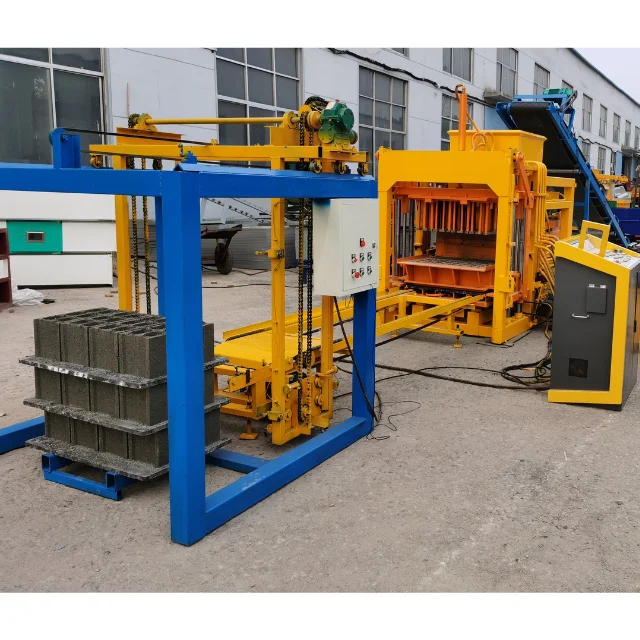
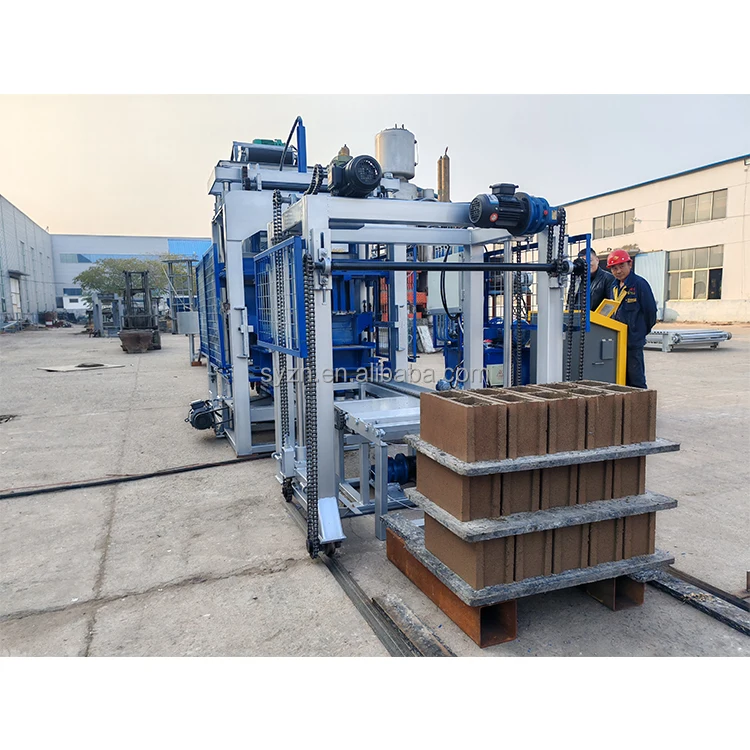
System Matched to Your Product — The QT12-15 is configured around your target block format, local aggregate, and existing curing setup, not pulled from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT12-15 |
| Product Type | Hydraulic Block Making Machine |
| Total Power | 62 kW |
| Pallet Size | 1300 × 900 mm |
| Moulding Cycle | 15–30 seconds (basis not stated in source — confirm block format / material / thickness) |
| Vibration Type | Table vibration |
| Vibration Force | 120 kN |
| Voltage | Customized according to local industrial voltage |
| Moulds | All moulds customized according to buyer block format |
Application Suitability
| Application | Material or Output |
|---|---|
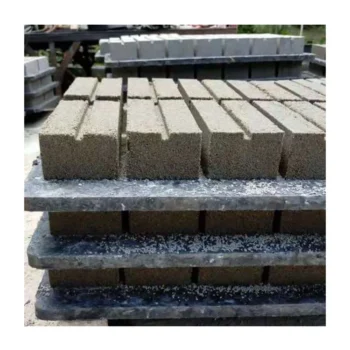
| Hollow block production | Crushed stone, cement, and sand blends for structural masonry |
| Solid block production | Dense aggregate mixes for load-bearing walls |
| Pavement brick production | Fine aggregate and cement for interlocking or rectangular pavers |
| Slope protection brick production | Permeable concrete mixes for erosion control applications |
| Porous brick production | Open-graded aggregate for stormwater management products |
| On-site contractor production | Local quarry materials for project-specific block requirements |
What "15–30 Seconds per Cycle" Actually Means for Your Daily Output
Cycle time only translates to real shift output when the block format, material behaviour, and pallet handling are all defined upfront.
A moulding cycle range of 15 to 30 seconds covers a wide span. A thin paving brick on a clean, well-graded aggregate may sit at the lower end, while a tall hollow block on a mix with high fines content needs longer fill and vibration to reach target density. Quoting a single cycles-per-hour figure without naming the format it assumes sets up a gap between the proposal and the first production run. That gap shows up as pallets piling up at the press exit faster than the curing area can absorb them [NEED_CITE: block plant capacity calculation methods by format].
The QT12-15 block machine specifications should always arrive with a line layout that states which block format was used for the capacity calculation, so the buyer can compare it against the format their market actually buys.
Matching the Press to the Format Your Market Buys
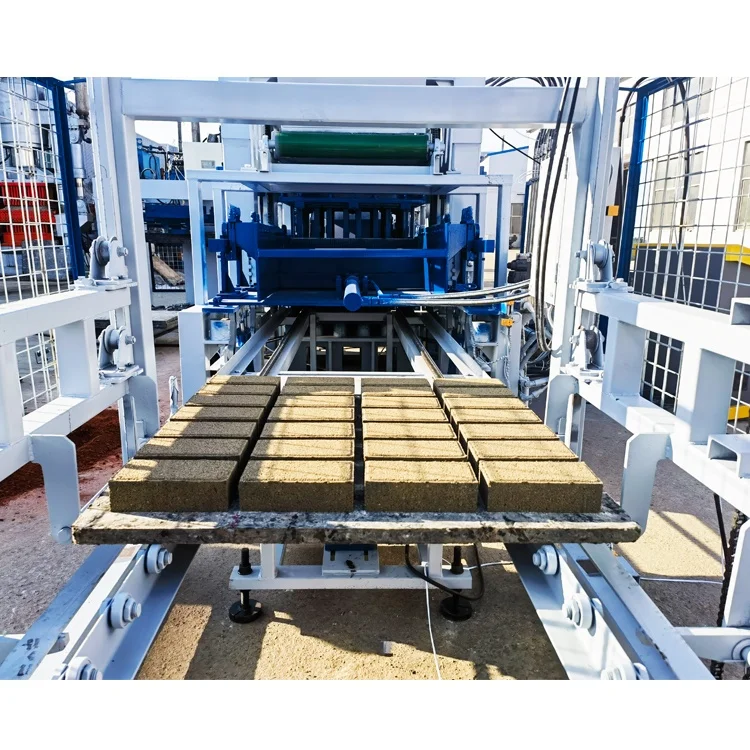
The 1300 × 900 mm pallet defines how many cavities fit per cycle for any given block dimension. A standard 400 × 200 × 200 mm hollow block arranges differently on that pallet than a 200 × 100 × 60 mm interlocking paver, and the mould cavity count changes the pieces-per-cycle figure directly. Before confirming a configuration, the mould drawing and format list need to show the exact cavity count for each product the buyer intends to run, because that number multiplied by cycles per shift is the only honest daily output figure.
Vibration and Pressure Tuned to Local Aggregate
The 120 kN vibration force works against the hydraulic pressure to compact the mix into the mould cavity. When the local aggregate carries more fines or clay than the default mix design assumes, the material flows more slowly into the cavity corners, and the fill phase must be extended. The QT12-15 hydraulic block making machine capacity by format is therefore not a fixed number but a range that shifts depending on how the vibration duration and pressure hold time are set against the specific material on site [NEED_CITE: effect of aggregate grading on concrete block compaction].
Reading the Numbers That Matter
The 62 kW total power covers the hydraulic pump, vibration motors, and conveyor drives together. On a high-capacity press of this pallet size, the hydraulic system must deliver enough pressure to pre-compress the material before vibration completes the densification. The table vibration type means the force is applied through the pallet into the mould base, which suits rigid steel pallets on a flat curing rack system. The moulding cycle range of 15–30 seconds tells a technical buyer that the PLC program must be adjustable per format, and that the quoted output should be recalculated whenever the block format or mix design changes. A buyer comparing the QT12-15 block machine specifications against another press should check whether the cycle time was measured on the same block format and material.
The Cost of Skipping the Format Conversation
When the press arrives and the buyer discovers that the cycle time on their actual block format is longer than the quoted figure assumed, the daily output shortfall cannot be recovered by running extra shifts if the curing area is already at capacity. Pallets wait on the floor, block quality suffers from rushed handling, and the investment payback stretches beyond the original projection. Moulds ordered for a format the local market does not buy become dead inventory, while the format that does sell requires a separate purchase and delivery lead time [NEED_CITE: block plant commissioning delays caused by format mismatch].
Why Source This Press Through a Format-First Process
Every configuration starts from the buyer’s target block format and daily output requirement, not from a standard machine on a list. Mould design is done against the buyer’s own drawings or market samples, and the cavity count per pallet is confirmed before production begins. The pallet size of 1300 × 900 mm is checked against the buyer’s existing curing racks and forklift dimensions to avoid a mismatch on arrival. Voltage and PLC display language are confirmed before the machine enters assembly, so commissioning is not delayed by a control panel the operator cannot read. A factory test record is produced on the buyer’s confirmed block format, not on a convenience product, so the cycle time and block dimensions are documented before the machine leaves the workshop.
Documentation & Verification
- Line layout with capacity calculation stating the block format and cavity count assumed
- Mould drawing and format list showing pieces per pallet for each product
- Pallet specification matched to buyer curing rack and forklift dimensions
- Factory test record on confirmed block format with measured cycle time
- Voltage, frequency, and PLC language confirmation sheet before assembly
- Wear parts and mould maintenance list with first replacement intervals
Installation, Commissioning & Support
- Foundation plan sized to the 62 kW power draw and vibration load of the QT12-15
- Dedicated electrical circuit confirmed for local voltage and frequency before wiring
- Machine dismantled for container loading with reassembly sequence documented
- First production run supervised with cycle time verified on buyer block format
- Operator training covering PLC navigation in confirmed display language
- Wear parts list with hydraulic seal and vibration motor replacement schedule
What to Include in Your Enquiry
To configure the QT12-15 accurately, the technical conversation should cover the exact block formats and dimensions the local market requires, the target daily output per format, and the source and grading of the local aggregate. The curing area layout, existing forklift capacity, and available power supply voltage and frequency all shape the line design. Confirming the PLC display language at enquiry stage prevents a delay that otherwise surfaces only when the machine is powered up on site.
Frequently Asked Questions
Q: How is QT12-15 capacity calculated per block format, and what cycle time applies to hollow vs. paving vs. solid blocks?
A: Capacity is calculated by multiplying the cavity count per pallet by the number of cycles achievable in a shift. The 15–30 second moulding cycle range covers different formats, but the exact cycle time depends on block height, material flow characteristics, and target density. A hollow block typically requires a longer vibration phase than a thin paver, so each format must be quoted with its own cycle time and daily output figure.
Q: Can the mould be designed to my exact block drawing, and what is the expected mould change time?
A: Moulds are designed and manufactured to the buyer’s block drawing or market sample. The cavity count is set to maximise output on the 1300 × 900 mm pallet for that specific format. Mould change time depends on the press configuration and the quick-release system specified, and should be confirmed during the proposal stage so that format flexibility matches the production schedule.
Q: How are vibration force and hydraulic pressure matched to my local aggregate and mix design for consistent block strength?
A: The 120 kN vibration force and hydraulic pressure are adjusted in the PLC program based on the buyer’s aggregate grading report and target block strength. High fines content requires longer fill time and adjusted vibration duration. A factory test on the buyer’s confirmed mix design documents the settings before shipment, so block strength is consistent from the first production run.
Q: Is the 1300 × 900 mm pallet compatible with my existing curing racks and forklift, and what pallet material is recommended?
A: The pallet dimensions must be checked against the curing rack slot width and the forklift tine spacing already in use at the plant. Steel pallets suit high-temperature steam curing, while bamboo or composite pallets work for ambient curing. The pallet material and thickness are confirmed during the proposal to ensure compatibility with existing handling equipment.
Q: What voltage, frequency, and PLC language options are confirmed before shipment?
A: Voltage and frequency are set to match the buyer’s local industrial power supply and confirmed in writing before the electrical panel is assembled. The PLC display language is selected from available options to match the operator’s working language. Both details are documented on the confirmation sheet so that commissioning proceeds without electrical or interface delays.