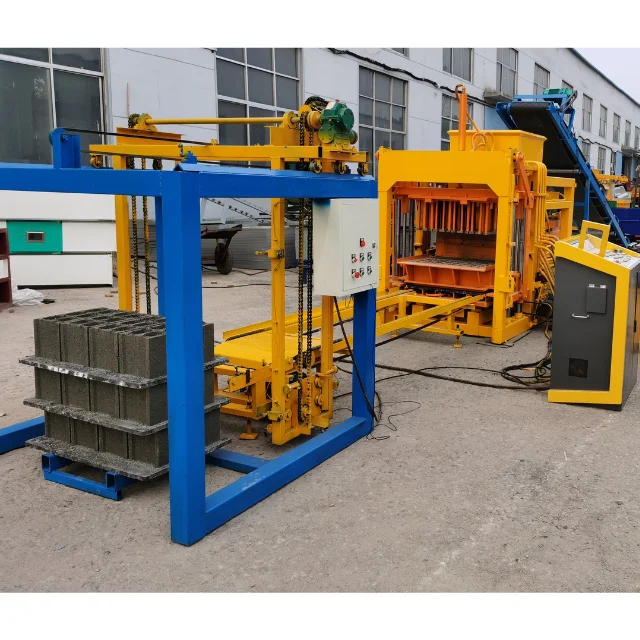

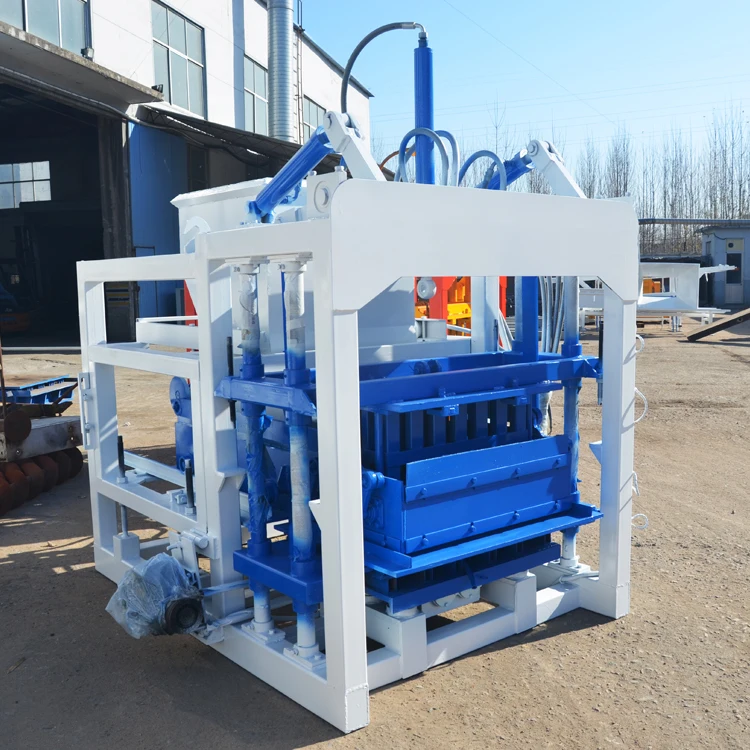
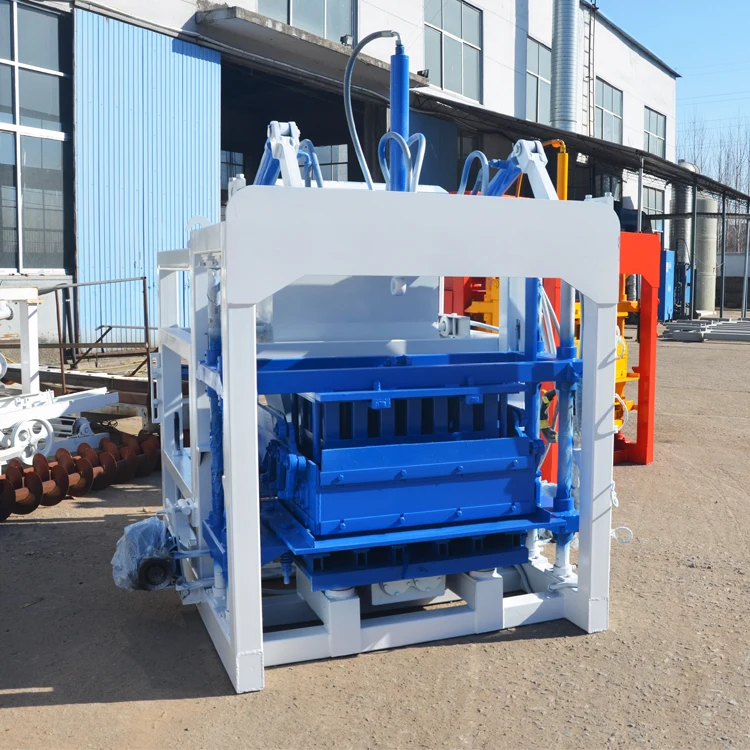
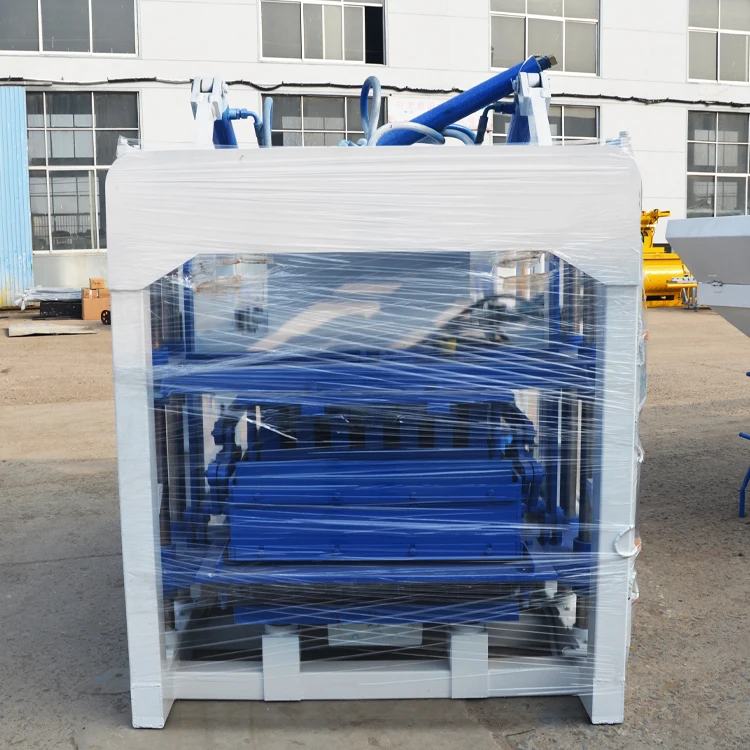

Description
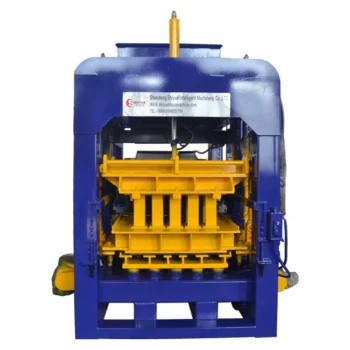
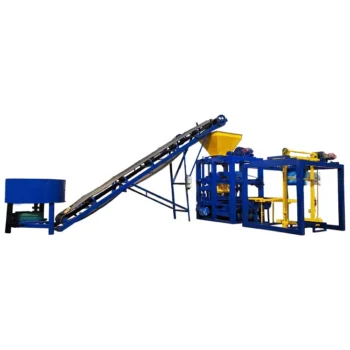
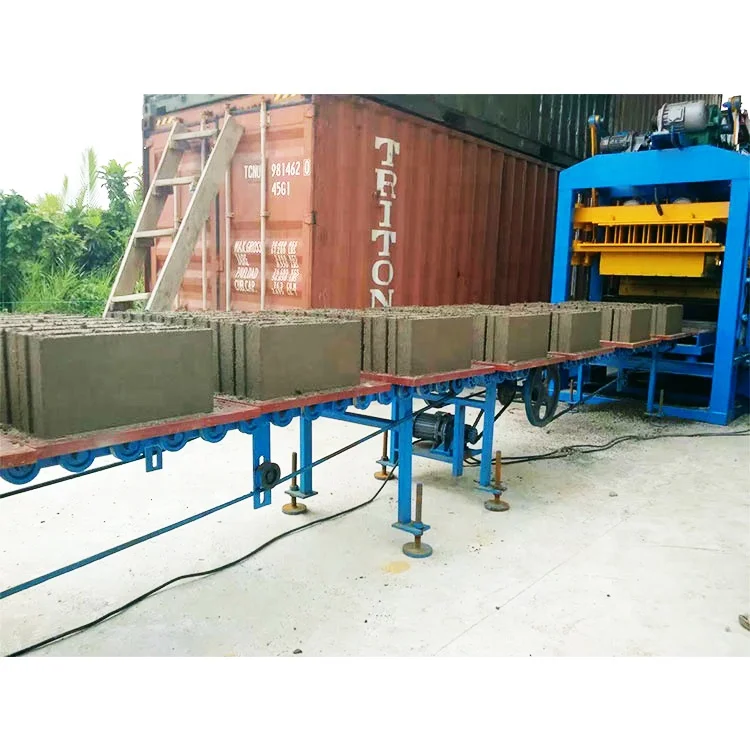
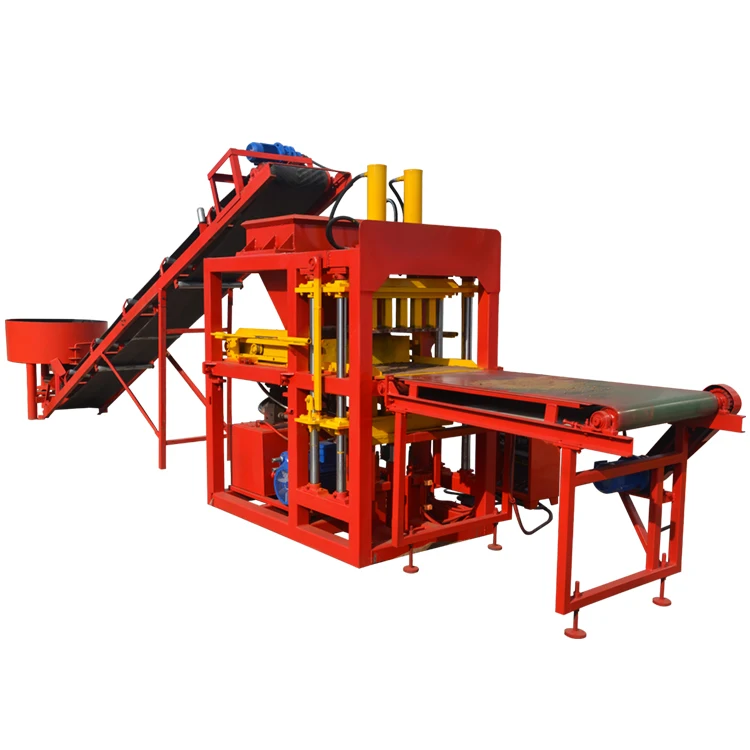
Matched System Engineering — Every QT4-15A block making machine is configured against the buyer’s actual mix design, local aggregate, and target block format before production begins, ensuring vibration force and hydraulic pressure deliver consistent density across every mould.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimension | 4100×1600×2600mm |
| Rated Pressure | 16-21MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 55kN |
| Pallet Size | 880×550mm |
| Molding Cycle | 25-30s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45kW |
| Total Mass | 4T |
| Demolding Method | Hydraulic |
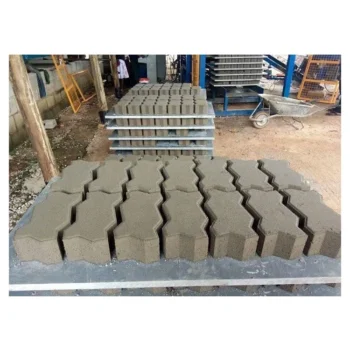
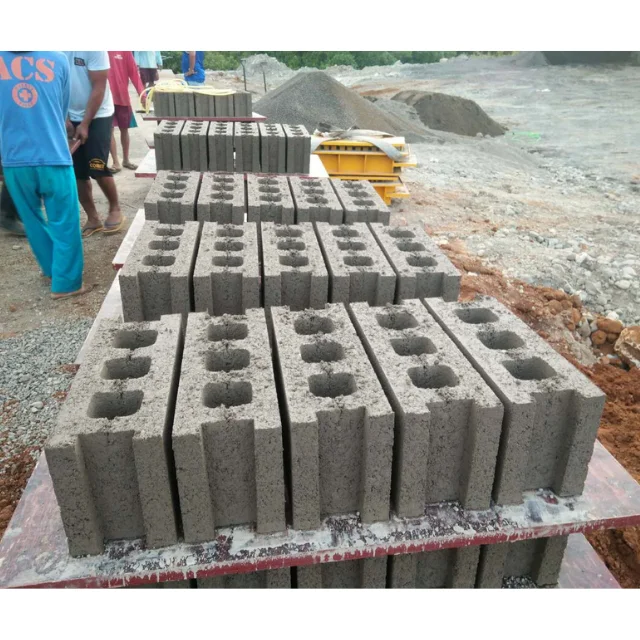
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Loading | 1×40HQ container (basic equipment) |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing for load-bearing structures | Gravel, cement, slag aggregates |
| Paving block and colored paver runs for walkways and plazas | Fine sand, cement, pigment additives |
| Interlocking block and kerbstone production | Coarse aggregate, cement, dust mixes |
Why the QT4-15A Block Machine Specifications Must Be Read Per Format
A single cycle-time number hides the real daily output picture for buyers producing multiple block formats.
I have watched buyers commit to a block machine based on a headline capacity figure, only to discover on site that hollow blocks, pavers, and interlocking bricks each demand a different molding cycle. The vibration settling time for a tall hollow block differs noticeably from the shorter press cycle a thin paver requires. When a quotation lists one cycle time without naming the format it assumes, the buyer is comparing numbers that do not belong to the same product [NEED_CITE: block cycle time variation by format and height]. That mismatch is the reason so many first-year plants fall short of the output they budgeted for.
Pallet Size 880×550mm: The Constraint That Shapes Your Entire Format Range
The 880×550mm pallet on the QT4-15A block machine sets the physical boundary for every mould you will run. This dimension determines how many cavity blocks fit per cycle, how pavers are arrayed across the surface, and whether kerbstones can be produced at all. Buyers who already operate curing racks and forklifts must verify that this pallet footprint matches their existing handling equipment before ordering. A mismatch here forces a change in racking or transport gear that no one priced into the project budget.
Vibration Force and Hydraulic Pressure: Matching Energy to Your Aggregate
The 55kN vibration force at 4200 r/min works together with 16-21MPa hydraulic pressure to compact the mix inside the mould cavity. This energy pairing must align with the density your local aggregate can achieve. High-clay sand absorbs vibration differently from clean crushed stone, and a mix that performs well in one region may produce weak blocks in another without parameter adjustment. I always ask buyers to send a sample of their intended raw material so we can confirm the QT4-15A block machine specifications against their actual conditions rather than relying on a default setting that was calibrated for a different quarry [NEED_CITE: effect of aggregate clay content on block compressive strength].
Reading the Core Parameters Beyond the Brochure Numbers
The platform vibration form means energy enters the mix from below through the pallet, which suits the geometry of hollow blocks where the core voids need uniform wall density. For pavers and interlocking blocks that require a smooth face finish, the hydraulic demolding method protects surface integrity during extraction. The 25-30s molding cycle listed in the QT4-15A block machine specifications carries a basis-to-be-confirmed note because cycle length shifts with block height, wall thickness, and the water content of the mix. The 18.45kW overall power draw covers the main press motor, vibration motor, and hydraulic pump running together, so buyers should verify their site transformer can sustain continuous load at this level plus any upstream mixer and conveyor motors. Total mass at 4T keeps the machine within standard container loading limits, which matters when the buyer is planning foundation depth and floor loading for a 300m² factory area.
What Happens When Configuration Ignores the Buyer’s Real Conditions
When vibration frequency and hydraulic pressure are set to catalogue defaults instead of the buyer’s mix, blocks leave the machine with inconsistent density — some pass strength testing, others crumble at the curing rack. I have seen entire production batches rejected because the mould was designed for a sand grading the buyer could not source locally. The cost is not just wasted cement; it is the weeks spent troubleshooting on site while the plant sits idle and orders go unfilled [NEED_CITE: cost of block rejection due to density inconsistency]. Voltage and PLC display language left unconfirmed before shipment can delay commissioning by days or longer, especially when the local electrician cannot read the control interface.
Why Sourcing the QT4-15A Through This Channel
Block machinery is our single focus, so the QT4-15A arrives as a matched system — press, mould, pallet, and handling equipment specified together rather than assembled from unrelated suppliers. We configure each machine against the buyer’s actual mix design and local aggregate, not a catalogue default that assumes materials from a different region. Mould design covers the formats the buyer’s market actually sells, with custom drawings available when standard options do not fit. The automation level is selectable, letting a buyer start with semi-automatic pallet handling and add stacking or cubing later as volume grows. Installation support includes on-site commissioning and operator training so the crew understands mould change procedure and daily maintenance from the first production run.
Documentation & Verification
- Line layout with capacity calculation stating which block format each output figure assumes
- Mould drawing and format list confirming cavity count per pallet for each product
- Pallet specification sheet matched to buyer’s curing rack and forklift dimensions
- Hydraulic and electrical schematic with voltage, frequency, and PLC language confirmed
- Factory test record run on buyer’s target block format before dispatch
- Operation and maintenance manual with wear parts list and mould inventory
Installation, Commissioning & Support
- Foundation must support 4T static mass plus dynamic vibration load across the 4100×1600mm footprint
- Dedicated electrical circuit sized for 18.45kW continuous draw with confirmed voltage and frequency
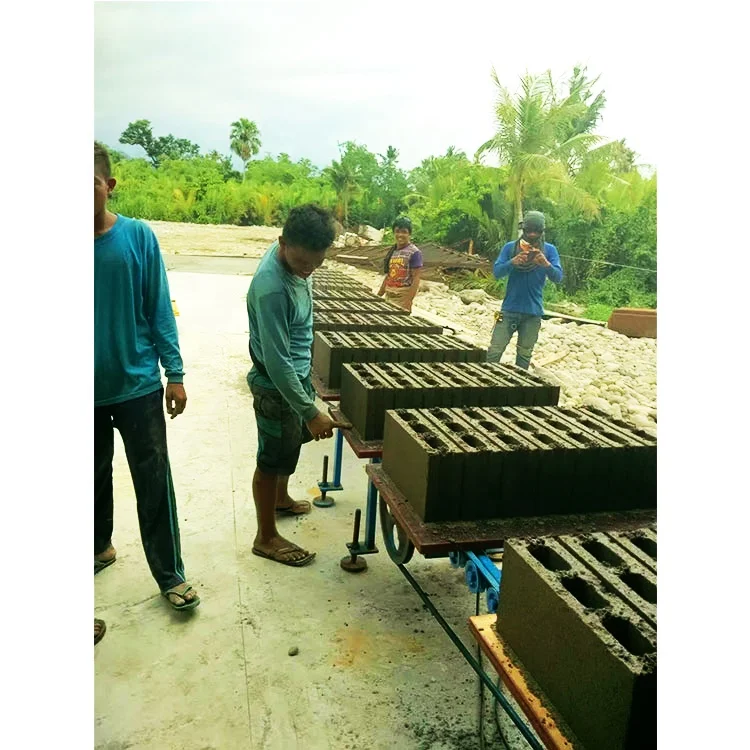
- Machine ships in 1×40HQ container; reassembly includes platform alignment and hydraulic line connection
- First-day commissioning covers vibration frequency tuning and hydraulic pressure calibration per mix sample
- Operator training addresses mould changeover procedure and daily inspection of hydraulic seals and vibration mounts
- Wear parts supply covers mould liners, hydraulic hoses, and vibration motor bearings from first replacement onward
What We Need Before Quoting Your QT4-15A Configuration
Send us the block formats your market buys most — hollow block dimensions, paver thickness, any interlocking profile — so we can calculate cycle time and daily output for each one. Tell us what raw material you have access to locally and whether you can ship a sample for mix testing. Confirm your site voltage, frequency, and the control language your operators will need, along with the curing rack and forklift dimensions you already have on the ground.
Frequently Asked Questions
Q: What is the realistic daily output of the QT4-15A for each block format?
A: Cycle time varies between hollow blocks, solid blocks, pavers, and interlocking bricks because each format requires different vibration settling and hydraulic pressing durations. We provide a per-format capacity table that states the assumed block dimensions, mix type, and cycle length so buyers see the honest output number for their specific product mix before placing an order.
Q: Which mould formats fit the 880×550mm pallet, and can custom moulds be designed?
A: The 880×550mm pallet supports standard hollow block cavity layouts, paver arrays, and interlocking profiles within that footprint. When a buyer’s market requires a non-standard block size or a custom interlocking geometry, we design and manufacture the mould to buyer-supplied drawings, confirming cavity count and demolding clearance before production.
Q: How is vibration force and hydraulic pressure matched to my local aggregate?
A: We request a raw material sample from the buyer’s intended source and run test pressings to observe how the 55kN vibration force and 16-21MPa hydraulic pressure interact with that specific aggregate grading and clay content. Parameters are adjusted so the QT4-15A block machine delivers consistent block density matched to the buyer’s real conditions.
Q: How long does a mould change take on the QT4-15A?
A: Mould changeover time depends on the format being removed and the one being installed, as well as whether the operator has performed the procedure before. We provide a step-by-step changeover guide with the machine and cover the procedure during on-site operator training so the crew can switch formats without losing a full shift [NEED_CITE: mould changeover best practices for hydraulic block presses].
Q: What pallet material does the QT4-15A assume, and will it work with my curing racks?
A: Pallet material and thickness are selected based on the buyer’s block weight per cycle and the curing rack spacing already on site. We confirm pallet specification — size, material, and load rating — against the buyer’s existing racks and forklift capacity before the order is finalized, preventing handling mismatches after the machine arrives.