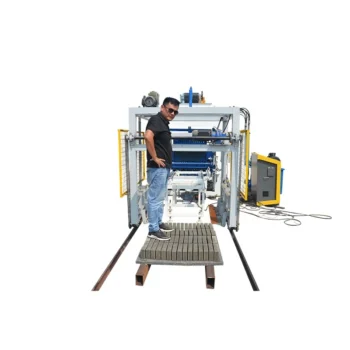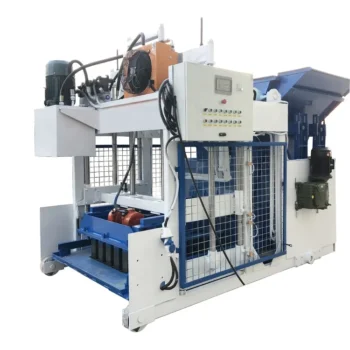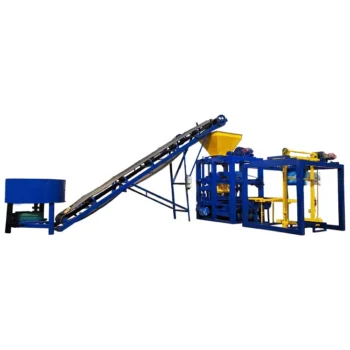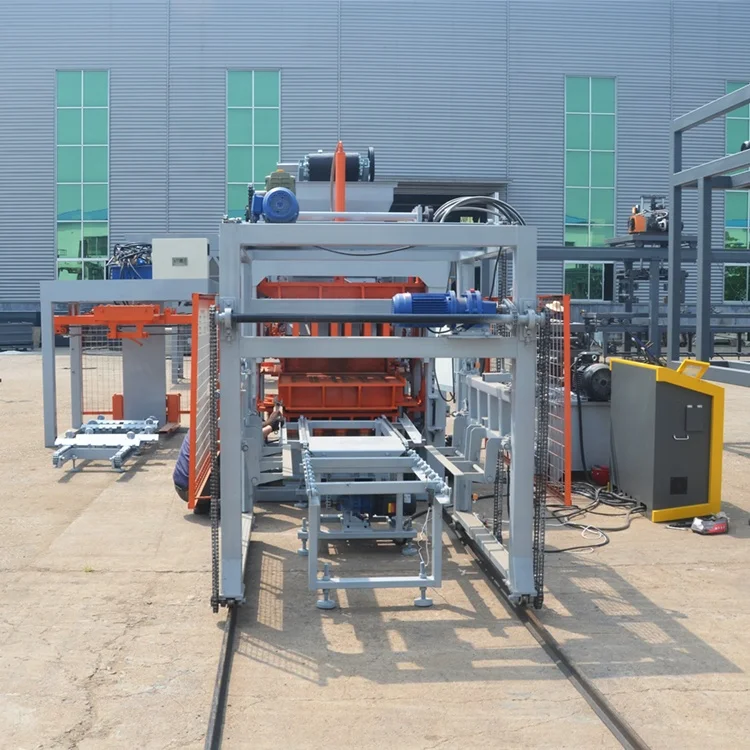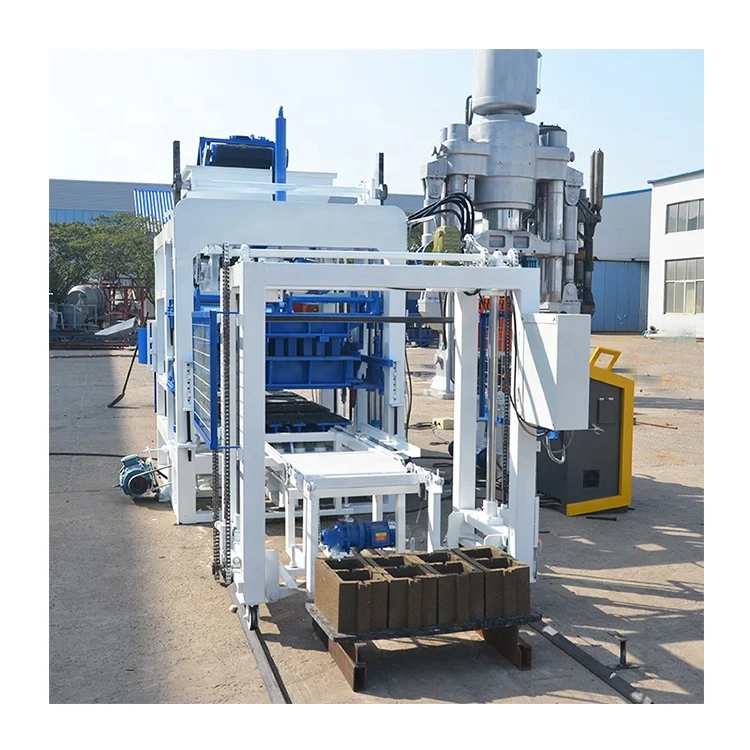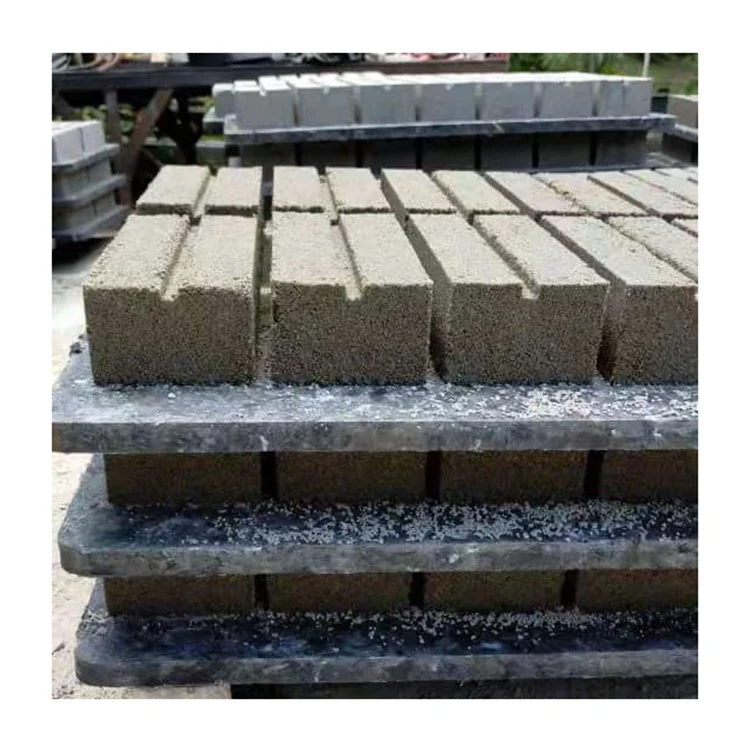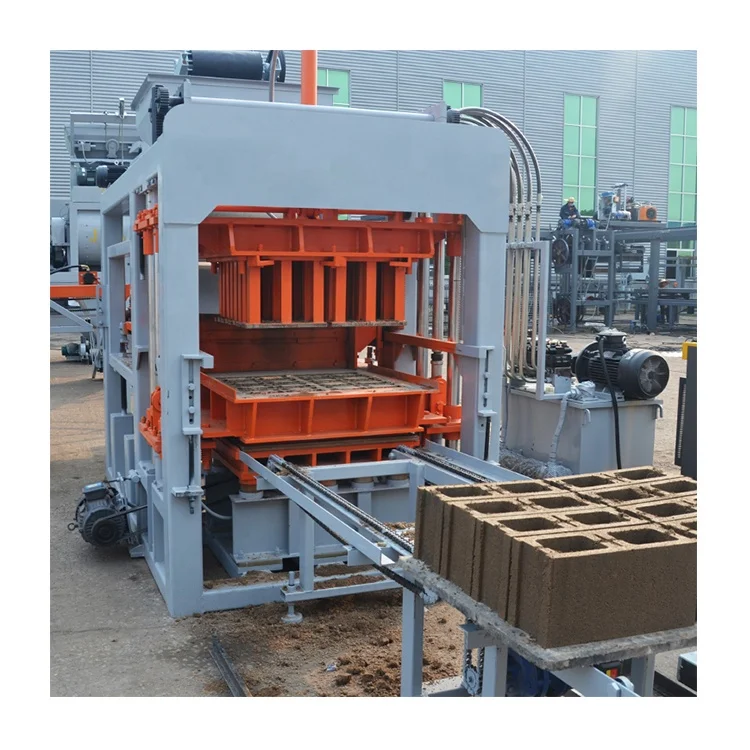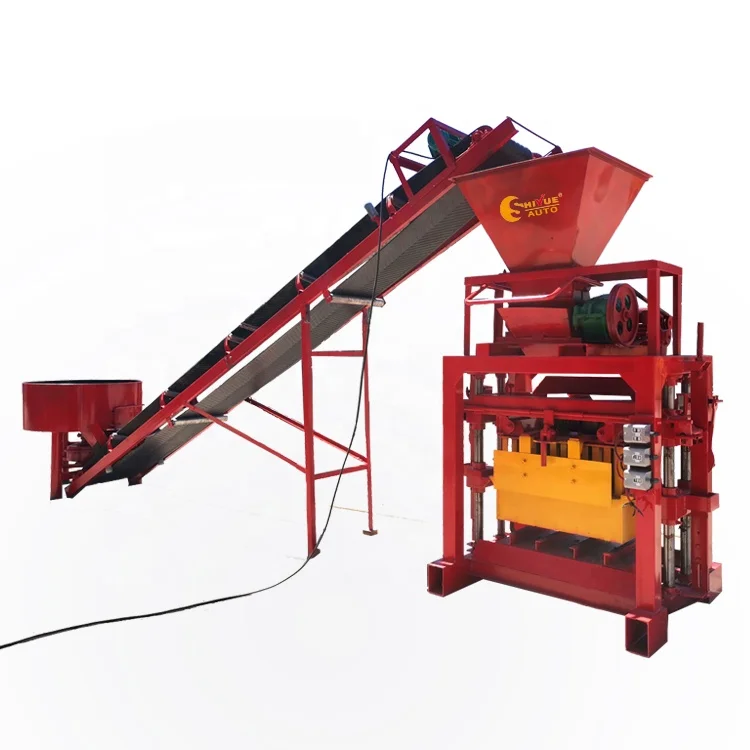

Description
Mould and Format Match — every QTJ4-35 output figure is stated against a named block size, so daily capacity planning starts from what your market actually buys, not a catalogue average.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
| Product Type | Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 1350 × 1460 × 1800 mm |
| Molding Cycle | 35 s |
| Vibration Frequency | 2800 r/min |
| Vibration Force | 30 kN |
| Rated Power | 11.15 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 450 × 20 mm |
| Net Weight | 1500 kg |
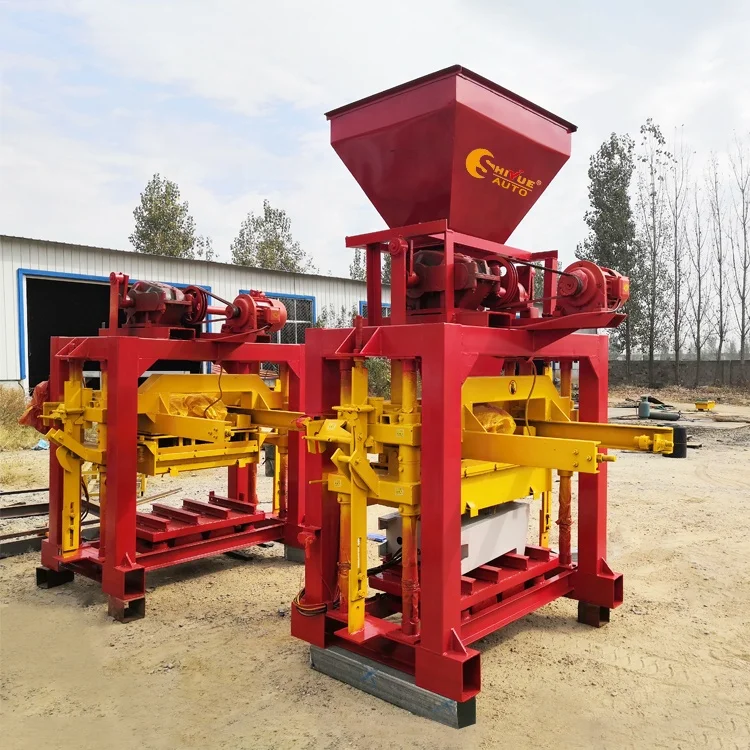
| Frame Structure | Four-lead channel steel stand |
| Mould Compression | Upper and bottom mould compression |
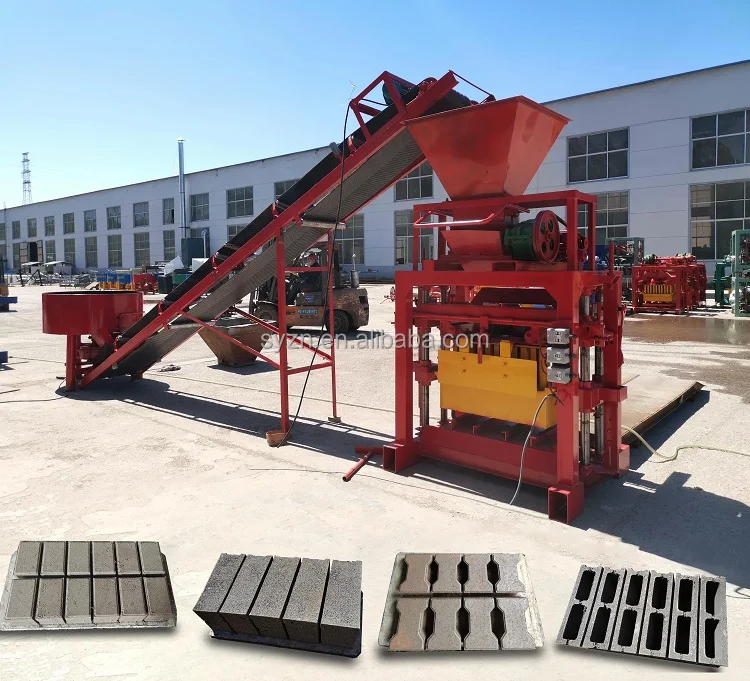
| Applied Products | Concrete blocks, hollow block (8 inch, 6 inch), solid brick |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output — Hollow Block 400×200×200 mm | 4 pcs/mould, 408 pcs/hr, 3264 pcs/8 hr |
| Output — Hollow Block 400×150×200 mm | 5 pcs/mould, 510 pcs/hr, 4080 pcs/8 hr |
| Output — Solid Brick 240×115×53 mm | 18 pcs/mould, 2100 pcs/hr, 17000 pcs/8 hr |
| Automation Level | Semi-automatic / manual pallet handling (basis to be confirmed) |
| Voltage & Frequency | To be confirmed before production |
| Control System | To be confirmed (PLC / manual) |
| Hydraulic Pressure | To be confirmed |
| Mould Change Time | To be confirmed |
| Stacking Method | Manual |
| Certification Scope | CE (verify applicability to this model) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block production | 8 inch and 6 inch blocks from crushed stone, sand and cement |
| Solid brick manufacturing | 240 × 115 × 53 mm bricks from fly ash and cement blends |
| On-site workshop output for housing projects | Mixed hollow and solid formats on a single pallet size |
| First block plant setup | Entry-level capacity with manual pallet handling |
What the Cycle Time Actually Means for Your Shift
The QTJ4-35 block machine specifications list a 35-second molding cycle, but that number only converts into real daily output when tied to a specific block format and operator rhythm. Capacity is format-dependent, not a single headline figure.
I spent years in QC watching machines leave Shandong workshops with a promised hourly rate that assumed the smallest brick in the catalogue. Buyers then ran 8-inch hollow blocks all day and wondered why the tally stopped well short. A 35-second press cycle still needs pallet loading, mould filling, and manual transfer before the next stroke begins [NEED_CITE: realistic shift output versus catalogue cycle time]. When you size the QTJ4-35 to your local market, the honest starting point is the block format you will run most days, not the fastest one on the list.
Matching Vibration to Your Local Aggregate
The 30 kN vibration force at 2800 r/min is the setting this press was tuned against during factory testing. If your local crushed stone runs coarser or your fly ash ratio sits higher than the test mix, the same force may under-compact the core or leave edge spalling. Adjusting the eccentric block angle or re-grading the aggregate brings the QTJ4-35 back into the strength window your market expects. Skipping that step is the shortest route to a pallet of crumbly units that no yard will buy.
Pallet Size Before the Order Goes In
Every stroke of the QTJ4-35 lands on an 850 × 450 × 20 mm pallet, and that dimension decides how your curing racks are spaced and which forklift forks can carry the load. If your yard already runs a different pallet format, the mismatch shows up on day one of commissioning — not as a machine fault, but as a handling problem that slows every subsequent operation. Confirming pallet alignment before the machine enters production is a non-negotiable step in the QTJ4-35 block machine specifications review.
Pressure, Vibration and the Block You Actually Sell
Upper and bottom mould compression works together with the vibration table to drive density through the full height of each cavity. Hollow blocks need enough force to knit the shell walls without collapsing the voids; solid bricks demand steady pressure across the entire face to keep weight variation inside tolerance. The four-lead channel steel frame holds alignment across both mould halves, so the dimensional repeatability buyers check with a caliper at the gate stays inside spec. Mix design, aggregate gradation and moisture sit on the other side of that equation — change any one and the balance shifts [NEED_CITE: relationship between vibration force, hydraulic pressure and block compressive strength].
When the Wrong Configuration Reaches the Site
A machine wired for a voltage your workshop does not supply sits idle until a transformer arrives. A control panel labelled in a language your operators cannot read turns commissioning into a guessing game. A mould set chosen for a block format your neighbours do not buy leaves you with inventory that will not move. Each of these mismatches costs more in lost production days than the hour it takes to confirm the details before the order goes to fabrication [NEED_CITE: common commissioning delays from unconfirmed electrical and control specifications].
Why Buyers Source This Press From Shiyue
Block machinery is our single focus, so the QTJ4-35 is specified as a matched system — press, mould, pallet and handling — rather than assembled from unrelated suppliers. Configuration is set against your actual mix design and target block format, not a catalogue default. Mould design covers the formats your regional market sells, with custom drawings available when the standard list falls short. Automation level is selectable, so a buyer can start with manual pallet handling and add feeding and stacking later as volume justifies it. Installation support, operator training and wear-part supply close the loop after the machine reaches your floor.
Documentation & Verification
- Line layout showing output per block format for the QTJ4-35, not a single blended figure
- Mould drawing and format list confirming which cavity sizes ship with the machine
- Pallet specification matched to your curing rack spacing and forklift capacity
- Voltage, frequency and control language confirmation sheet signed before production
- Factory test record run on a mix ratio close to your local material
- Operation and maintenance manual in the operator language you specify
Installation, Commissioning & Support
- Foundation pad sized to the 1350 × 1460 mm footprint with anchor bolt plan supplied before arrival
- Dedicated circuit for the 11.15 kW rated load, voltage and phase confirmed at order stage
- Machine shipped as a single skid with mixer, reducing on-site assembly to pallet-rack placement
- First-run block test on your aggregate blend to set vibration timing before operator hand-over
- Mould change walkthrough covering alignment pins and compression plate seating
- Wear-part list with part numbers for vibration table springs and mould liner plates
What to Send With Your Enquiry
Tell us which block format your yard moves fastest — hollow, solid, or a mix — and the daily tally you need to sustain. Share a sample of your local crushed stone or fly ash so we can run a test mix against the vibration setting. Confirm your workshop voltage, frequency and the language your operators prefer on the control display. If your curing racks and forklifts are already in place, send the pallet and rack dimensions so the 850 × 450 mm pallet spec can be verified before the QTJ4-35 enters production.
Frequently Asked Questions
Q: How is the 408 pcs/hr figure derived and which block format does it assume?
A: That number applies only to the 400 × 200 × 200 mm hollow block, where the mould produces four cavities per cycle and a 35-second press stroke is assumed. Actual shift output depends on pallet loading speed and operator rhythm, so treat the figure as a benchmark for planning rather than a guaranteed tally.
Q: Can the QTJ4-35 mould be changed on-site, and how long does a format swap take?
A: Moulds are exchanged by releasing the upper and bottom compression plates and lifting the cavity set out of the frame. Swap time is not published in the current specification sheet, so request a recorded changeover before shipment to confirm the minutes required on your floor.
Q: What pallet size does this machine require, and can it use my existing curing racks?
A: The press runs an 850 × 450 × 20 mm pallet. If your current racks are spaced for a different dimension, the pallets will not seat correctly, so share your rack drawings before the order to confirm alignment or adjust the pallet specification.
Q: Which raw materials and aggregate gradations are compatible with this vibration force rating?
A: The 30 kN force at 2800 r/min suits crushed stone, sand, cement and fly ash within standard gradation bands. Coarser aggregate or very high fly ash ratios may need vibration timing adjustment to achieve target compressive strength without surface spalling.
Q: What voltage and control language options are available for my market?
A: Voltage and frequency are confirmed at order stage to match your local supply, and the control panel language is set before the panel is wired. State your site supply and preferred display language when you open the enquiry to avoid commissioning delays.