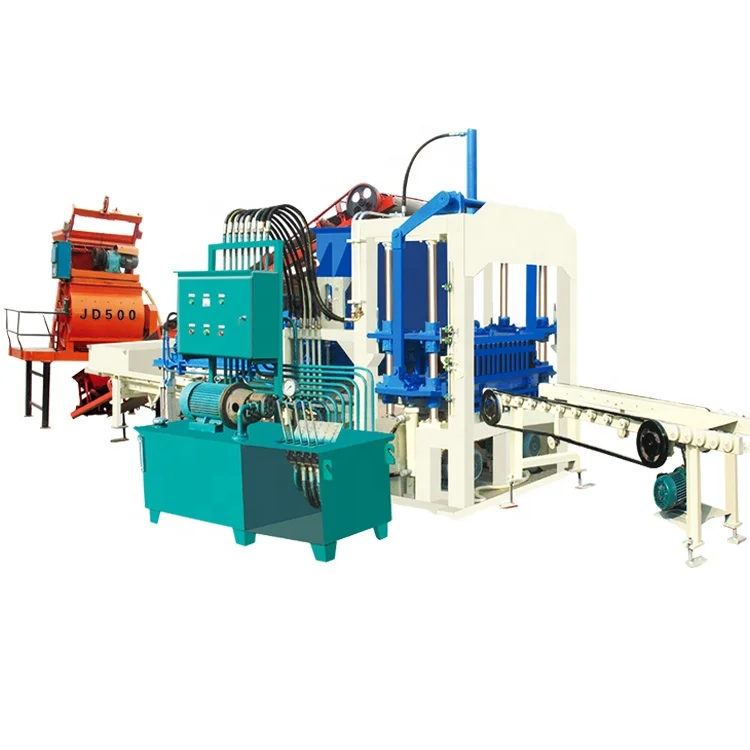
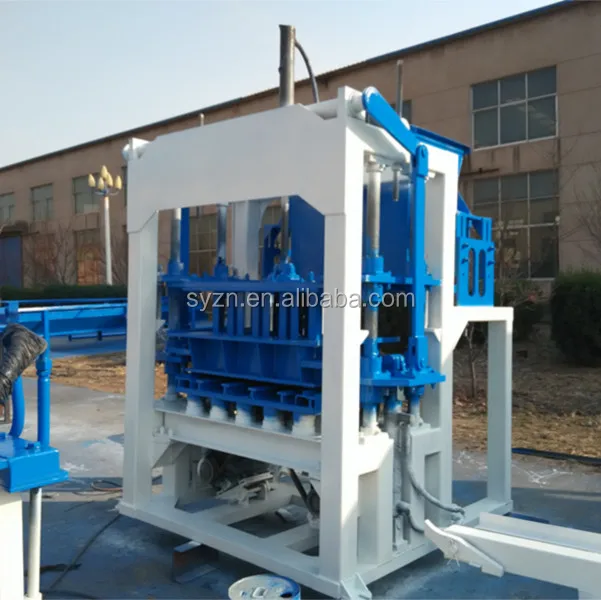
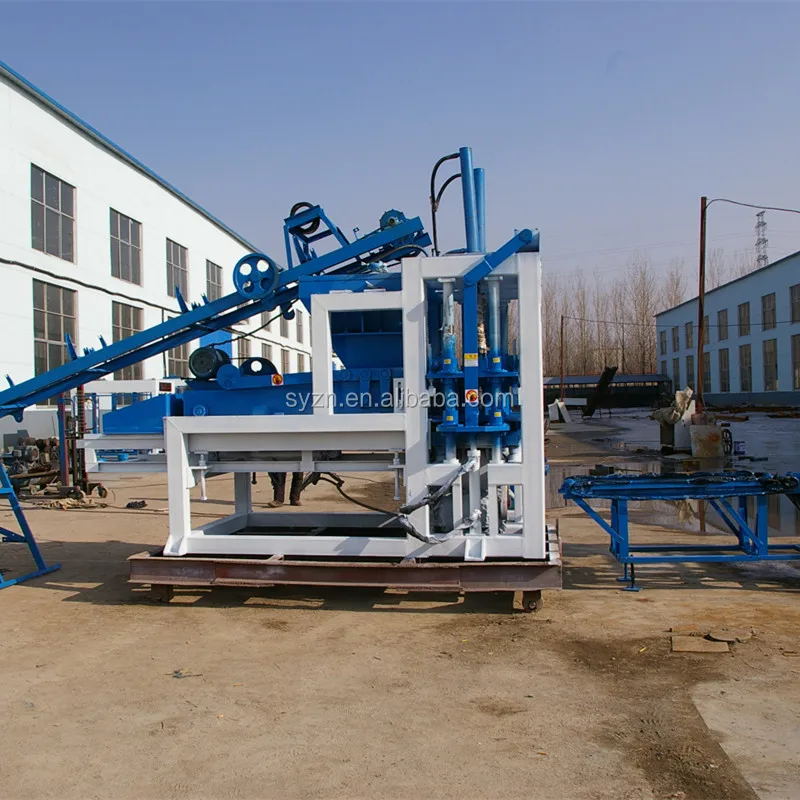
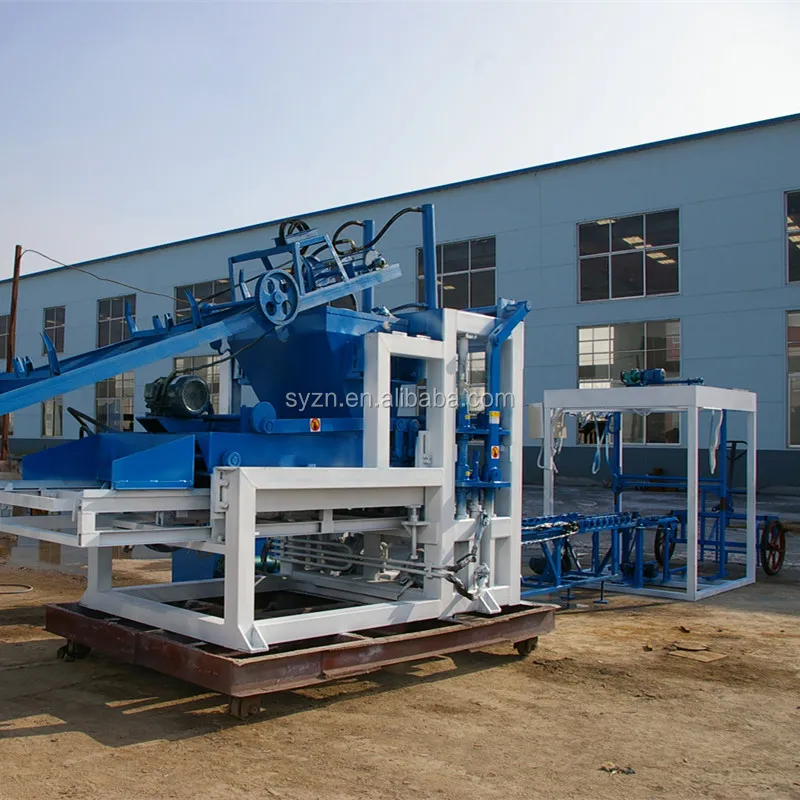
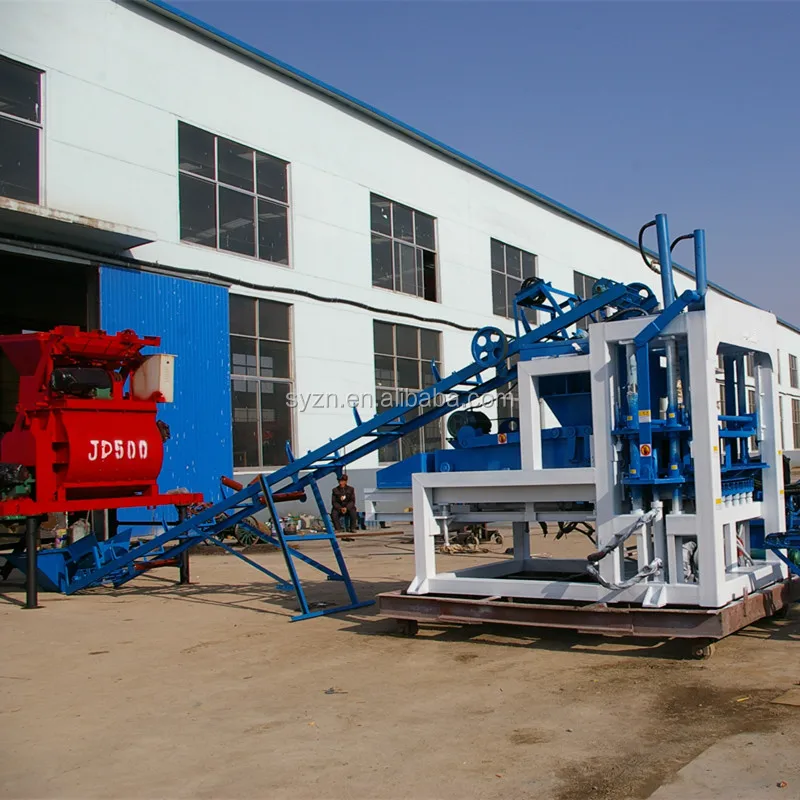
Description
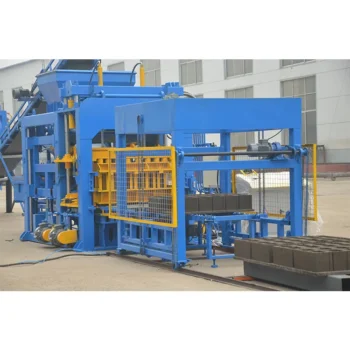
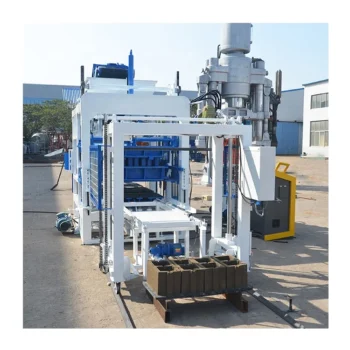
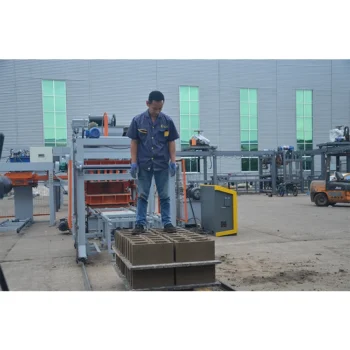
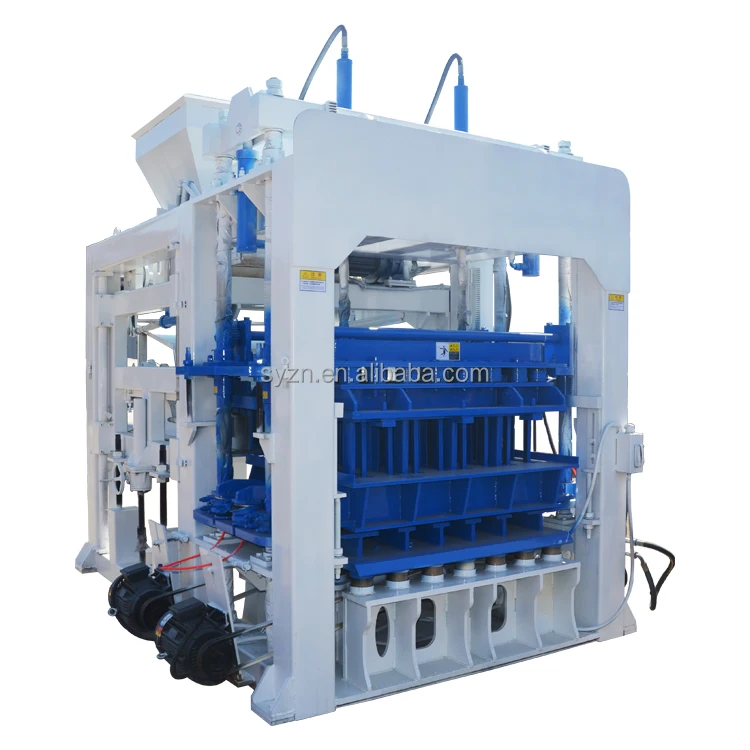
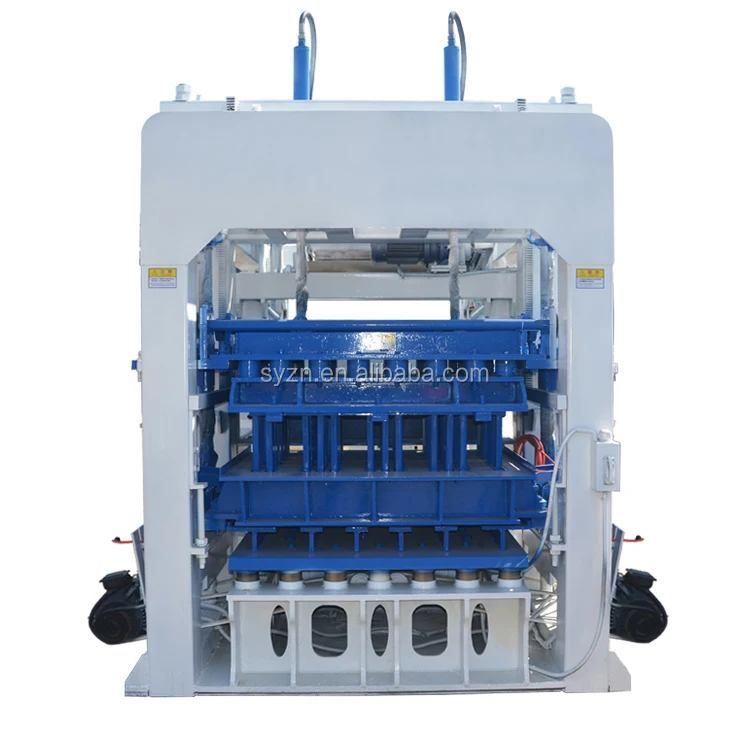
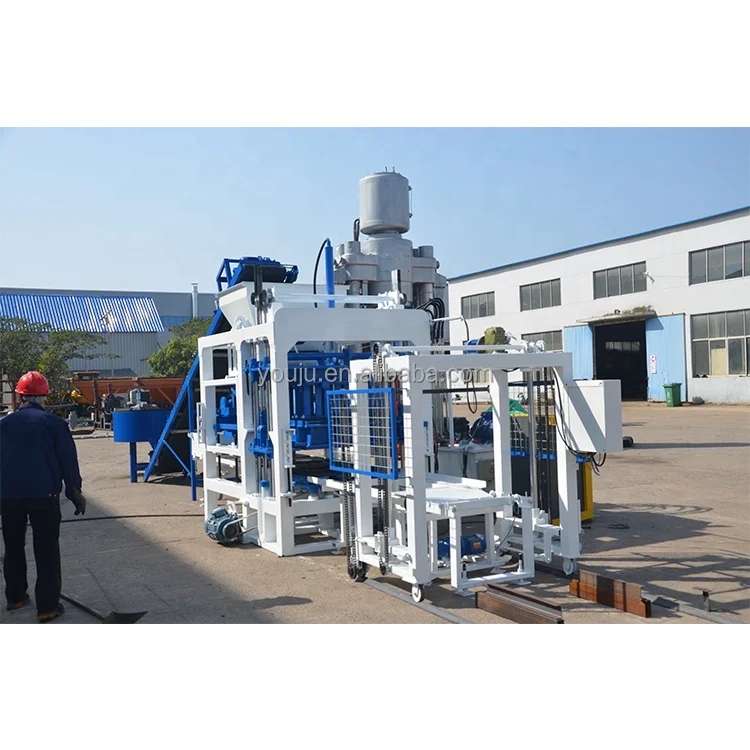
Matched Configuration for Actual Block Formats — the QT4-20 automatic block machine is proposed with cycle time, pallet size and vibration settings confirmed against the buyer’s target product and local aggregate, not pulled from a generic catalogue.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-20 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 60 kN |
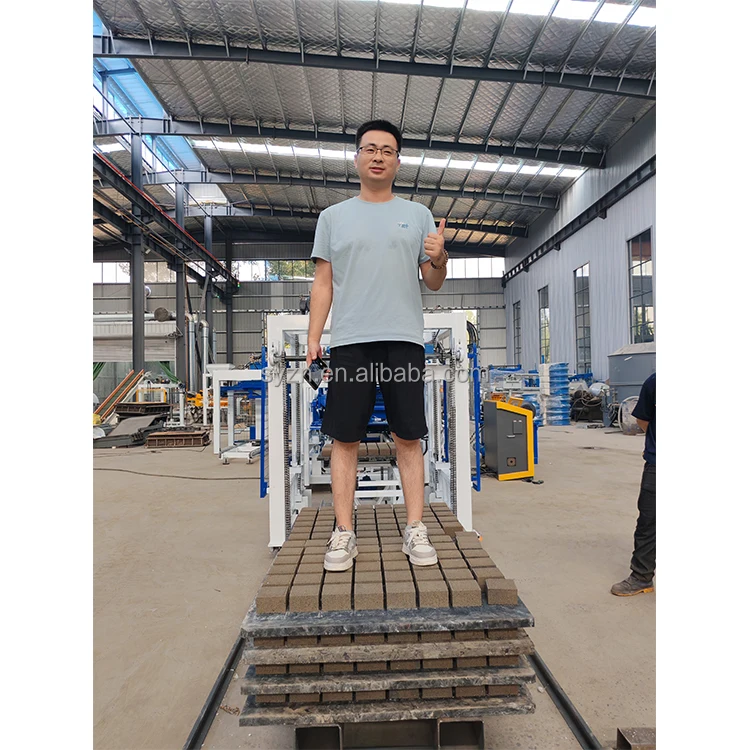
| Pallet Size | 1020×570 mm |
| Molding Cycle | 15–25 s |
| Overall Power | 27.5 kW |
| Total Mass | 5.8 T |
| Demolding Method | Hydraulic |
| General Water Consumption | 8 T/Day |
| Factory Area | 500 m² |
| Control System | PLC with person-machine conversation interface |
| Automation Level | Automatic production line |
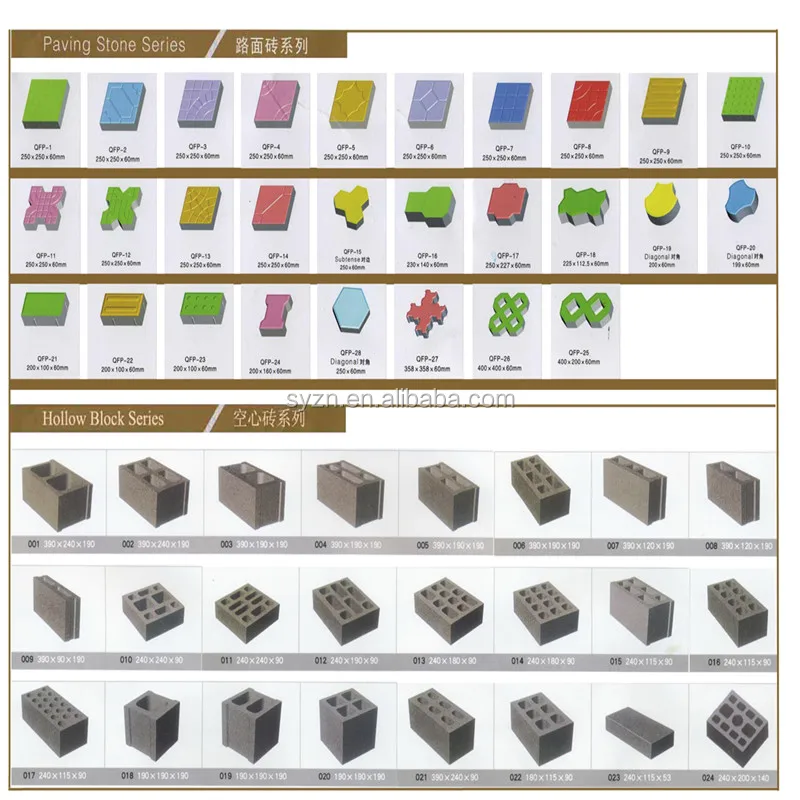
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag, dust |
| Output Capacity | basis to be confirmed per block format and mix design |
| Mould Change Time | basis to be confirmed per block format and thickness |
| Voltage & Frequency | configurable — to be confirmed before production |
| Language Options | configurable — to be confirmed before production |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential walls | Crushed stone, sand, cement with fly ash or slag replacement |
| Solid block manufacturing for load-bearing structures | Gravel, sand and cement at higher compaction pressure |
| Interlocking paver production for driveways and walkways | Fine aggregate, cement and pigment for colored surface layers |
| Kerbstone and curb production for road projects | Coarse aggregate with reinforced mix design |
| Porous and grassed block production for landscaping | Open-graded aggregate with reduced cement content |
| Interlocking block production for retaining walls | Crushed stone and cement with precise dimensional moulds |
What "2800 Cycles Per Hour" Leaves Out About QT4-20 Automatic Block Machine Specifications
Cycle time only matters when tied to the exact block format and the mix you can actually source locally.
I once watched a buyer sign for an automatic block machine based on a brochure figure, only to find his local sand carried high clay content that extended every cycle by several seconds. His daily output dropped to roughly half the quoted number within the first month [NEED_CITE: effect of aggregate clay content on vibration compaction time]. When we review QT4-20 automatic block machine specifications with a new buyer, we always ask for a sample of the intended aggregate before committing to an output figure. The molding cycle of 15–25 seconds covers a wide range of formats, but a hollow block at the shorter end and a dense paver at the longer end produce very different daily totals. Stating capacity per format is the only honest way to plan a production schedule.
Matching Vibration Force to Block Density Requirements
The platform vibration system on the QT4-20 delivers 60 kN of force across a frequency range of 2800–4500 r/min. This adjustability matters because a lightweight hollow block needs rapid, lower-amplitude vibration to settle the mix without cracking thin webs, while a solid paver demands sustained high-force compaction to reach the density required for vehicular traffic. The QT4-20 automatic block machine specifications list both the force and the frequency range so the buyer can verify compatibility with the target block strength before the machine is built.
How Pallet Size Determines Your Curing Layout
The 1020×570 mm pallet size on this machine is not arbitrary. It sets the spacing of curing racks, the reach of the forklift that moves wet blocks to the yard, and the footprint of the entire curing area. A buyer who already operates a block plant needs the new pallets to match existing rack dimensions, otherwise every pallet becomes a manual handling problem [NEED_CITE: pallet standardization in concrete block curing operations]. We confirm pallet material and dimensions against the buyer’s current curing infrastructure before the QT4-20 enters production.
Reading the Pressure and Vibration Numbers Together
The 21 MPa rated hydraulic pressure works in sequence with platform vibration — vibration settles the mix into the mould cavity, then hydraulic pressure compresses it to final density. If either parameter is mismatched to the aggregate gradation, blocks emerge with inconsistent strength from one batch to the next. The QT4-20 automatic block machine specifications pair these two values deliberately: 60 kN vibration at up to 4500 r/min loosens and distributes the material, while 21 MPa hydraulic pressure locks it in place. For a buyer producing structural hollow blocks, this combination must be validated against a trial mix before the machine ships.
The Cost of Skipping Mix-Design Verification
When a machine is configured for a standard mix that the buyer cannot source, the result is either a costly material substitution or a machine that runs below its designed compaction capability. Blocks may pass visual inspection but fail compressive strength tests at the construction site [NEED_CITE: compressive strength testing standards for concrete masonry units]. The vibration frequency and hydraulic pressure on the QT4-20 can be adjusted within their specified ranges, but they cannot compensate for a fundamentally incompatible aggregate. Confirming the local material profile before ordering prevents re-engineering the mix after the machine arrives.
Why Buyers Choose This Configuration Path
Block machinery is the single focus here, which means the QT4-20 is specified as a matched system — press, mould, pallet and handling equipment are selected together rather than sourced from separate vendors. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, with custom drawings available when standard options do not fit. The automation level is selectable, so a buyer can begin with semi-automatic pallet handling and add automatic stacking later. Installation includes on-site commissioning and operator training so the crew understands cycle adjustment and mould change procedures from day one.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Mould drawing and format list confirming included block types and change procedure
- Pallet specification matched to buyer’s curing rack system and forklift capacity
- Voltage, frequency and PLC display language confirmation before production begins
- Factory test record on buyer’s target block format before dispatch
- Hydraulic and electrical schematic for on-site maintenance reference
Installation, Commissioning & Support
- Foundation plan aligned with the 7100×1600 mm footprint and 5.8 T operating mass
- Dedicated power circuit sized for 27.5 kW total load at confirmed voltage and frequency
- Machine arrives dismantled for container loading with reassembly supervised on site
- First-run parameter tuning of vibration frequency and hydraulic pressure for buyer’s mix
- PLC interface language set and verified before operator training begins
- Wear parts and mould maintenance schedule provided with initial spare list
What to Include in Your Inquiry
To size the QT4-20 correctly, share the specific block formats your market demands, the target daily output for each format, and a description of locally available aggregate including gradation and clay content. Confirm your site voltage, frequency and preferred PLC display language. If you already operate curing racks or forklifts, provide their dimensions so the pallet specification can be aligned before the proposal is finalized.
Frequently Asked Questions
Q: How is QT4-20 capacity calculated per block format, and what cycle time applies?
A: Capacity is calculated by dividing available production hours by the molding cycle for each specific format. The 15–25 second cycle range covers hollow blocks at the shorter end and dense pavers at the longer end. We state output per format in the proposal so the buyer sees realistic daily figures, not a single catalogue number that assumes an unstated block type.
Q: Which mould formats are available, and how long does a mould change take?
A: Moulds are available for hollow blocks, solid blocks, pavers, interlocking blocks, kerbstones and colored pavers. Custom moulds can be designed from buyer drawings. Mould change time depends on the format and block thickness, and is confirmed during commissioning so the operator can plan format changeovers within a shift.
Q: How are vibration force and hydraulic pressure matched to local aggregate?
A: The 60 kN vibration force and 21 MPa hydraulic pressure are adjusted within their specified ranges based on the buyer’s aggregate gradation, clay content and cement ratio. A trial mix evaluation determines the optimal frequency and pressure settings before the machine is finalized, ensuring consistent block density and strength across production batches.
Q: What pallet size does the QT4-20 use, and how does it affect the curing area?
A: The machine uses 1020×570 mm pallets. This dimension determines curing rack spacing, forklift handling requirements and overall yard footprint. We confirm pallet material and size against the buyer’s existing curing infrastructure to avoid manual handling bottlenecks after installation.
Q: What documentation confirms voltage, control language and block strength before shipment?
A: Before production, we confirm voltage, frequency and PLC display language in writing. The factory test record documents block output on the buyer’s target format, and the machine specification sheet records all agreed parameters. Hydraulic and electrical schematics are included for on-site maintenance and troubleshooting.