

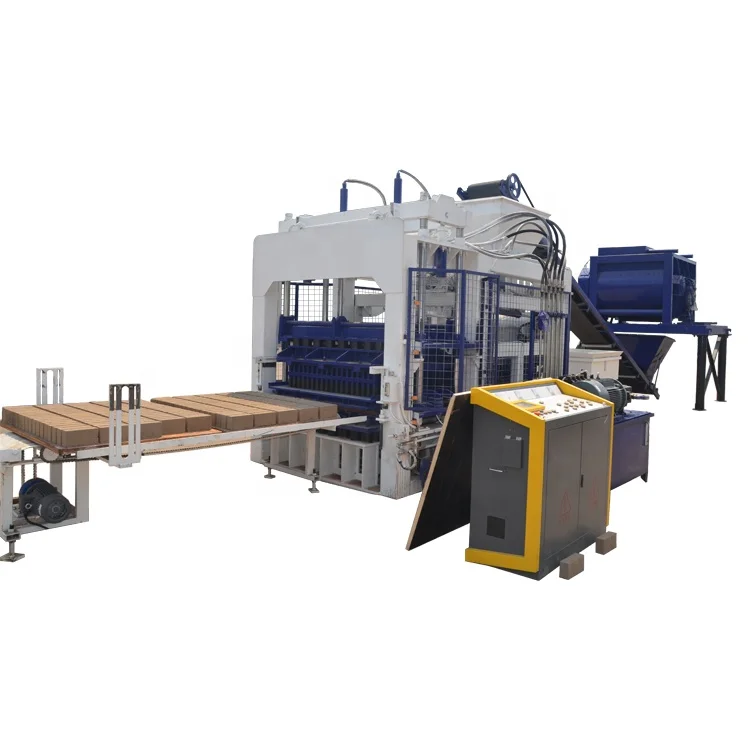

Description
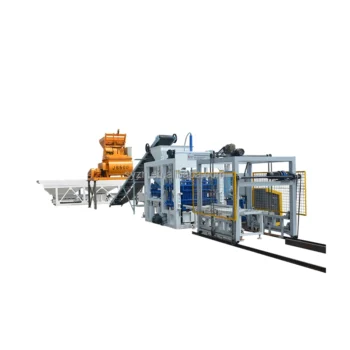
Format-specific configuration — The QT12-15 block machine is sized against the buyer’s actual block format, local aggregate, and target daily output, with mould cycle time stated per format rather than a single optimistic headline figure.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT12-15 |
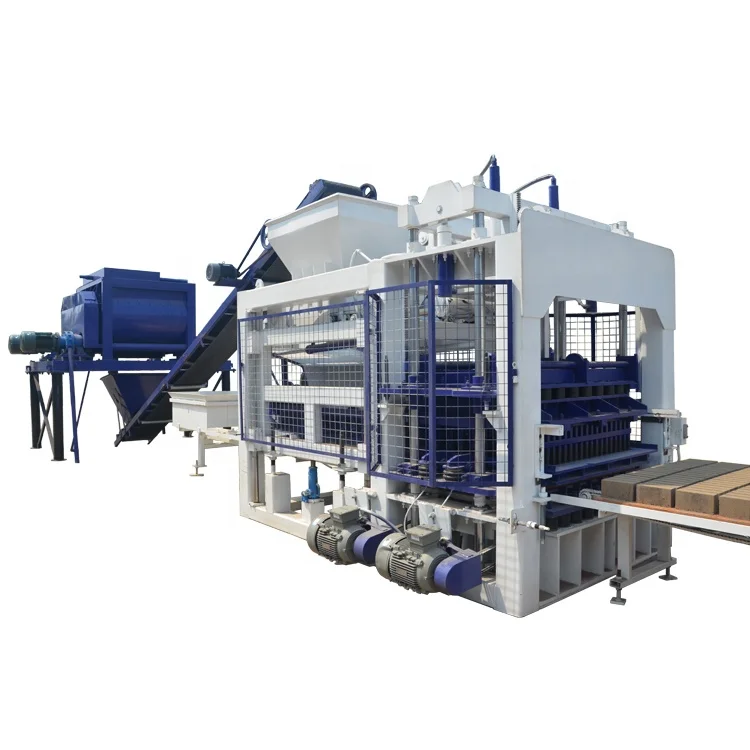
| Product Type | Hydraulic Block Making Machine |
| Total Installed Power | 62 kW |
| Pallet Size | 1300 × 900 mm |
| Vibration System | Dynamic and static table with frequency conversion control |
| Vibration Acceleration | Up to 20g (configuration dependent) |
| Vibration Force | 120 kN (source value — verify against final configuration) |
| Material Feeding | 360° rotating press-in arch breaker |
| Noise Reduction | Flexible head vibration reduction + adjustable air bag on mould box |
| Moulding Cycle | 15–30 seconds (basis not stated in source — confirm block format, material, and thickness) |
| Control Voltage | Customized according to local industrial voltage and frequency |
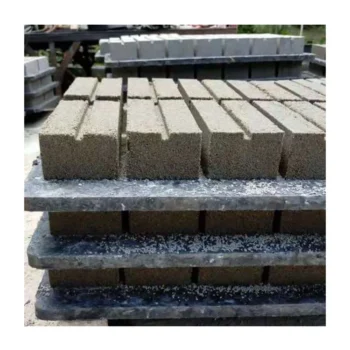
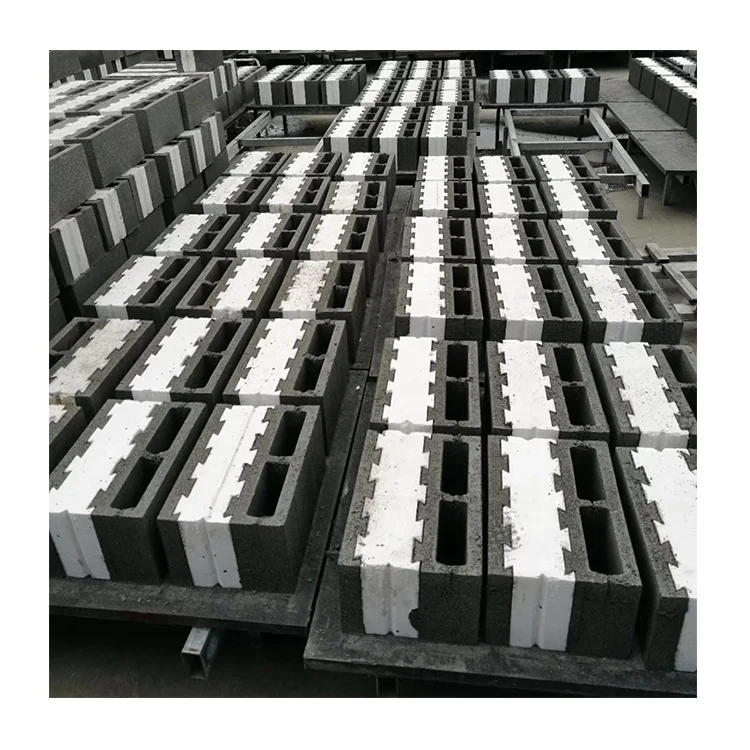
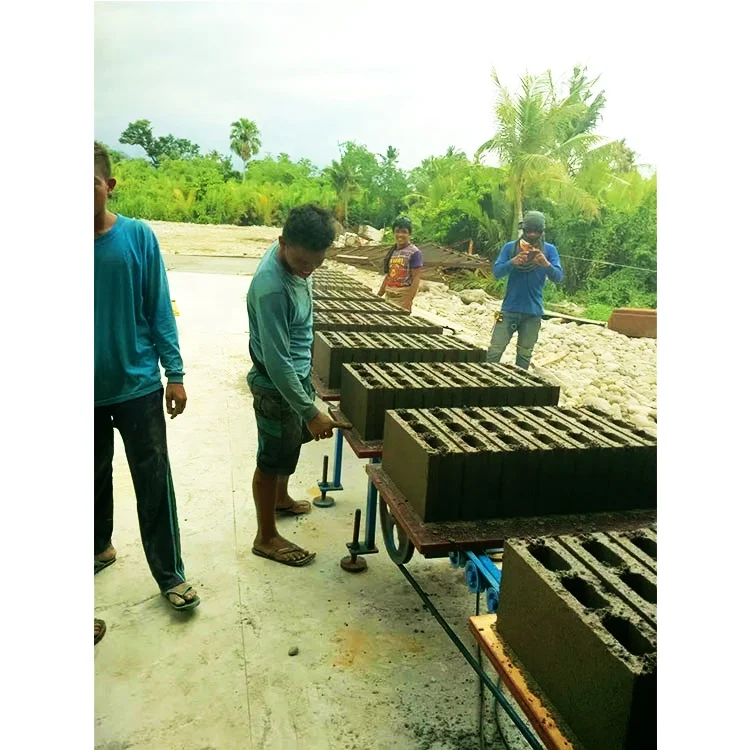
| Mould Compatibility | Hollow, solid, paving, porous, and slope protection formats |
Application Suitability
| Application Scenario | Material or Output Detail |
|---|---|
| Large-scale hollow block production | Crushed stone, river sand, and cement blends for commercial masonry |
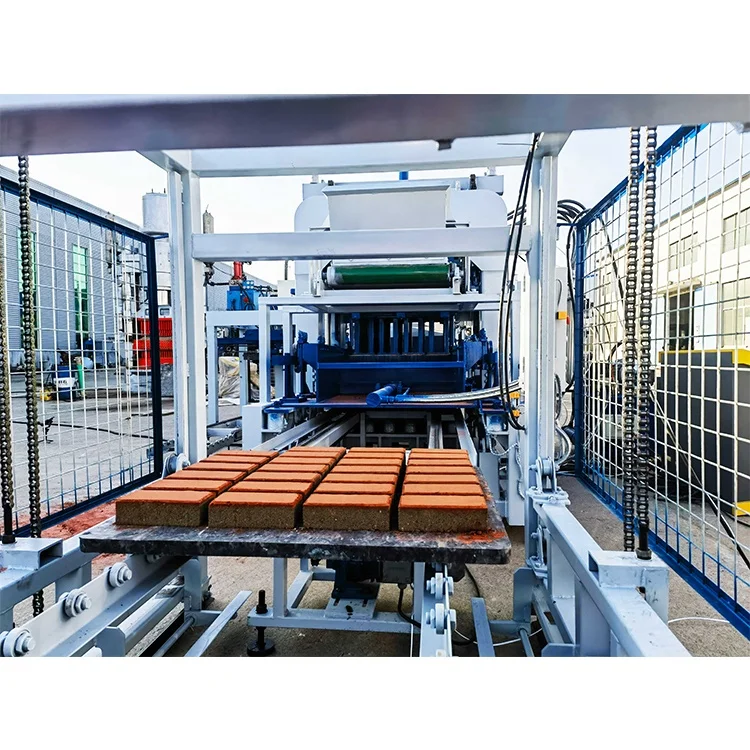
| Interlocking paver manufacturing | Fine aggregate and pigment mixes for landscaping and municipal paving |
| Porous brick production | Permeable concrete mixes for sustainable drainage systems |
| Slope protection block forming | Heavy aggregate blends for civil engineering and retaining structures |
| Solid wall block extrusion | High-density cement and local aggregate for load-bearing walls |
What "15 Seconds Cycle Time" Actually Means for the QT12-15 Block Machine Specifications How to Choose
A cycle time figure is meaningless unless the block format and mix design are stated alongside it.
Many buyers receive quotations that quote a single "blocks per hour" number without revealing that the calculation assumes a thin paving brick rather than the 200mm hollow block the buyer actually sells. When the QT12-15 block machine specifications how to choose are evaluated honestly, the 15–30 second range must be pinned to a specific format, wall thickness, and aggregate blend before any daily output projection is credible. I have watched plants run at a fraction of their quoted output simply because the sales proposal never specified which block the cycle time was based on [NEED_CITE: block machine capacity calculation standards].
Mould Cycle Time by Block Format
The QT12-15 block machine specifications how to choose begin with the format you sell most. A 15-second cycle typically applies to thin paving bricks or solid bricks where the cavity is shallow and the vibration settles the mix quickly. A 200mm hollow block, requiring deeper vibration penetration and longer compression, will push the cycle toward the 30-second end of the range. Every format you plan to produce needs its own cycle time confirmed before the order is placed, not after the machine arrives and the first production run disappoints.
Pallet Sizing Against Your Curing Infrastructure
A 1300 × 900 mm pallet is a substantial working surface that dictates how many blocks are formed per cycle, but it must also fit the curing racks and forklift tines already in your plant. Buyers who overlook this alignment end up either rebuilding curing racks or handling pallets manually because the forklift cannot engage them properly. The pallet material — whether bamboo, PVC, or steel — also interacts with the vibration system and block release characteristics, making this a decision that affects both daily throughput and long-term pallet replacement cost.
Vibration Force, Hydraulic Pressure, and Mix Design Alignment
The 20g acceleration and 120 kN vibration force are not arbitrary targets; they must match the stiffness and moisture content of your local aggregate. High-clay river sand absorbs vibration differently from crushed granite, and a frequency conversion control system allows the operator to dial in the exact amplitude and duration each mix requires. When vibration force and hydraulic pressure are mismatched to the actual material, blocks emerge with inconsistent density — strong in one batch and crumbling in the next [NEED_CITE: concrete block compressive strength testing protocols].
The Hidden Cost of Ignoring Format-Specific Configuration
A plant that runs a single "average" cycle time across all block formats will consistently underperform on the formats that need longer vibration and over-press the formats that need less. Over time this leads to excess cement consumption on simple pavers and structural rejects on hollow blocks. Buyers who skip the format-by-format capacity calculation often discover the mismatch only after the first container of blocks ships to a customer who tests compressive strength independently [NEED_CITE: third-party block strength certification requirements].
Why Procurement Rigor Matters Here
Every QT12-15 is configured against the buyer’s submitted aggregate sample and target block format before production begins, not pulled from a catalogue default. Mould designs are produced to buyer drawings when standard formats do not match local market demand. The pallet specification is cross-checked against the buyer’s curing rack dimensions and forklift capacity to prevent arrival-day surprises. Voltage, frequency, and PLC display language are confirmed in writing before the machine enters assembly. Factory testing runs the actual mould the buyer will use, with cycle times recorded per format and shared in the test documentation.
Documentation & Verification
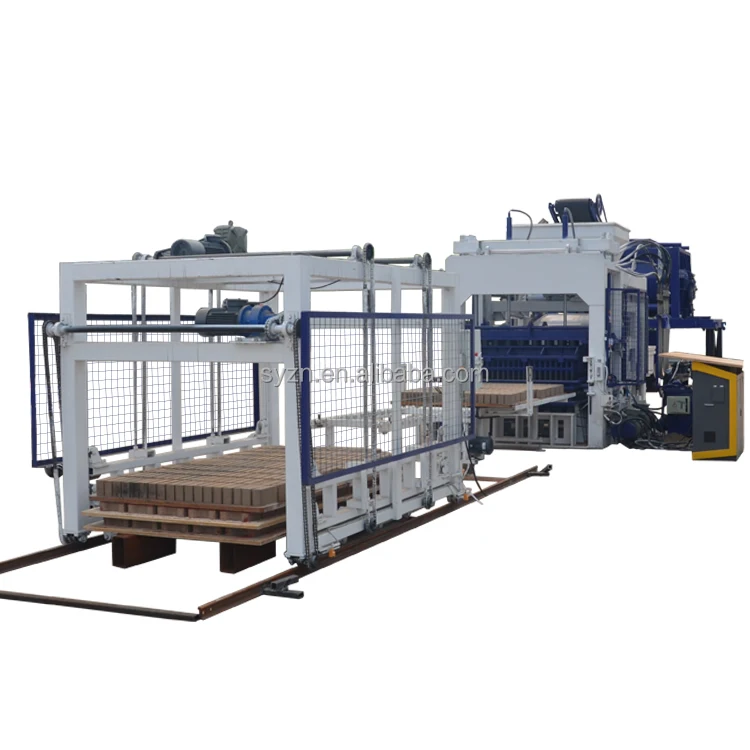
- Line layout drawing with capacity calculation stated per block format
- Mould drawing and format list including custom designs to buyer specifications
- Pallet specification confirming size, material, and load rating
- Voltage and PLC language confirmation signed before production
- Factory test record showing cycle time per format with buyer’s mould installed
Installation, Commissioning & Support
- Foundation plan referencing the QT12-15 footprint and 62 kW power distribution requirements
- Dedicated circuit specification matching confirmed local voltage and frequency
- On-site assembly with vibration frequency calibration to buyer’s aggregate sample
- PLC interface set to confirmed language with operator training on format changeover
- Replaceable wear-resistant plate on cloth platform reviewed during maintenance briefing
Inquiry Preparation
Provide the specific block formats you intend to produce, including dimensions and wall thickness. Share a sample or laboratory analysis of your local aggregate and sand. Confirm your site’s industrial voltage, frequency, and the language required for the control interface so that the QT12-15 block machine specifications how to choose are matched to your production environment before quotation.
Frequently Asked Questions
Q: How is the QT12-15 cycle time verified for my specific block format and mix design?
A: We require a sample of your local aggregate and the exact block dimensions you intend to produce. The machine is factory tested with your mould installed, and cycle times are recorded per format. These recorded figures form the basis of the capacity calculation in your documentation, not a generic catalogue number.
Q: What mould formats are available and how long does a mould change take?
A: Moulds are available for hollow blocks, solid blocks, pavers, porous bricks, and slope protection units. Custom moulds can be designed to buyer drawings. Mould change time depends on the format size and the quick-release system fitted to your configuration, and this duration is confirmed during the proposal stage so it can be factored into your daily production schedule.
Q: How do I confirm the 1300 × 900 mm pallet fits my existing curing racks and forklift?
A: Provide the internal dimensions of your curing racks and the fork tine spacing and load rating of your forklift. The pallet specification is cross-checked against these measurements before order confirmation, and alternative pallet dimensions can be discussed if a mismatch is identified.
Q: What voltage and PLC language options are confirmed before shipment?
A: Your local industrial voltage, frequency, and required PLC display language are confirmed in writing before production begins. This prevents commissioning delays caused by incorrect motor wiring or an interface the operators cannot read upon machine arrival.
Q: How is block strength validated against my local aggregate before the machine is built?
A: The aggregate sample you provide is used during factory testing to run actual production cycles. Blocks produced during this test are checked for density and visual consistency, and the vibration frequency and hydraulic pressure are adjusted until the results match the strength requirements of your market standard.