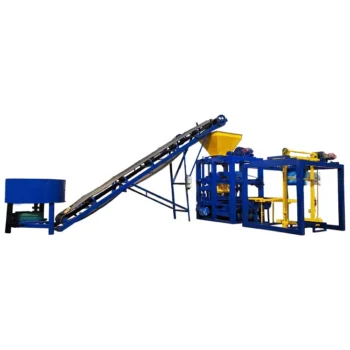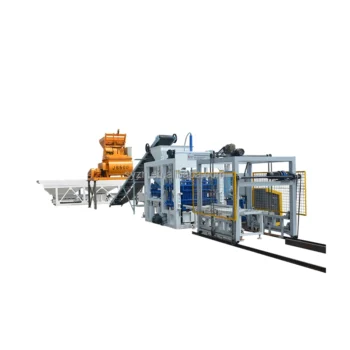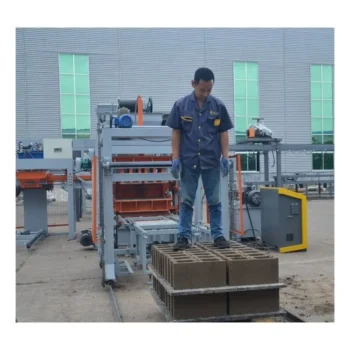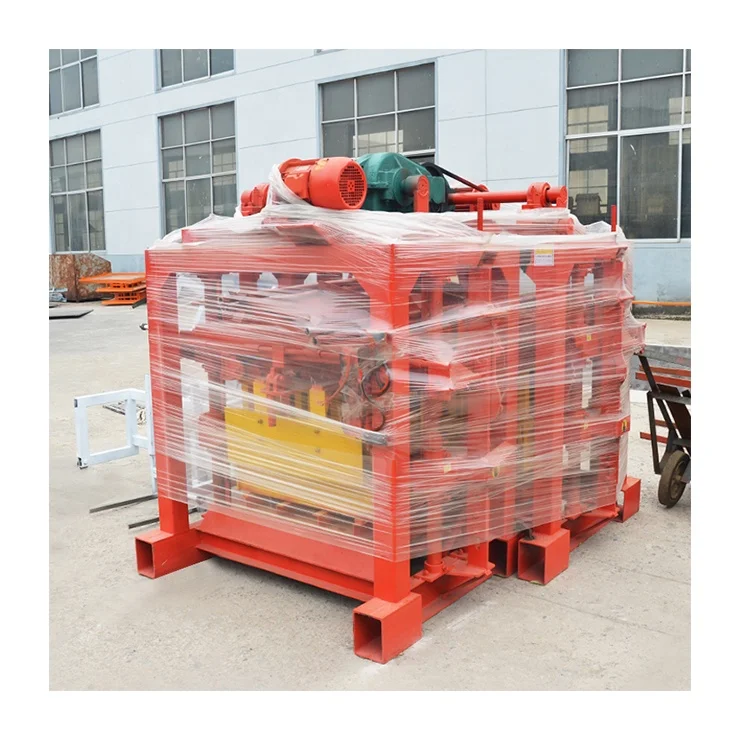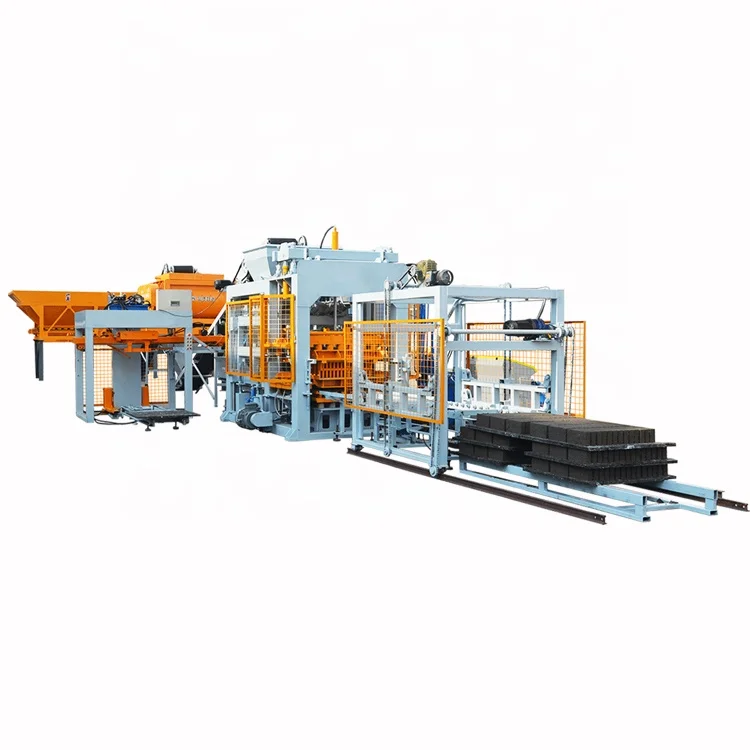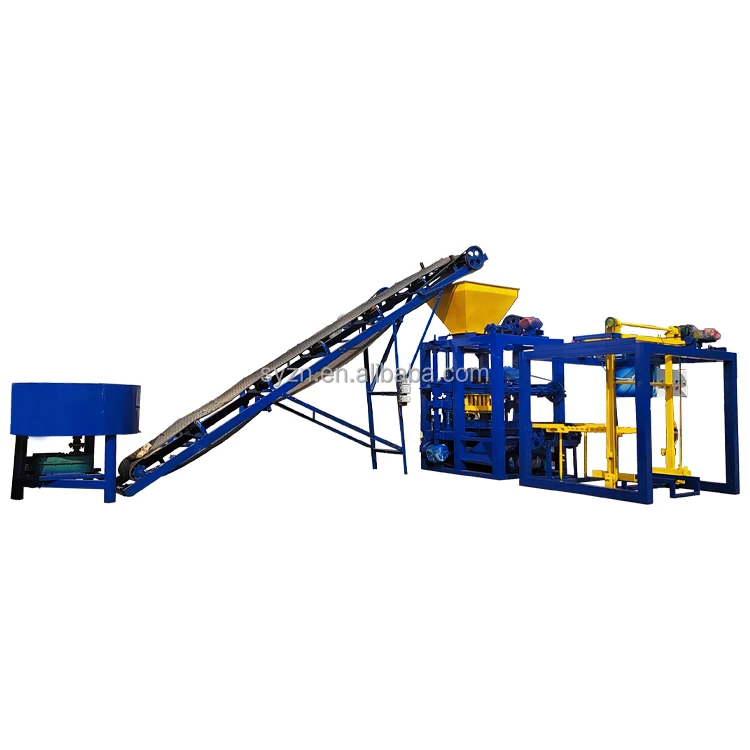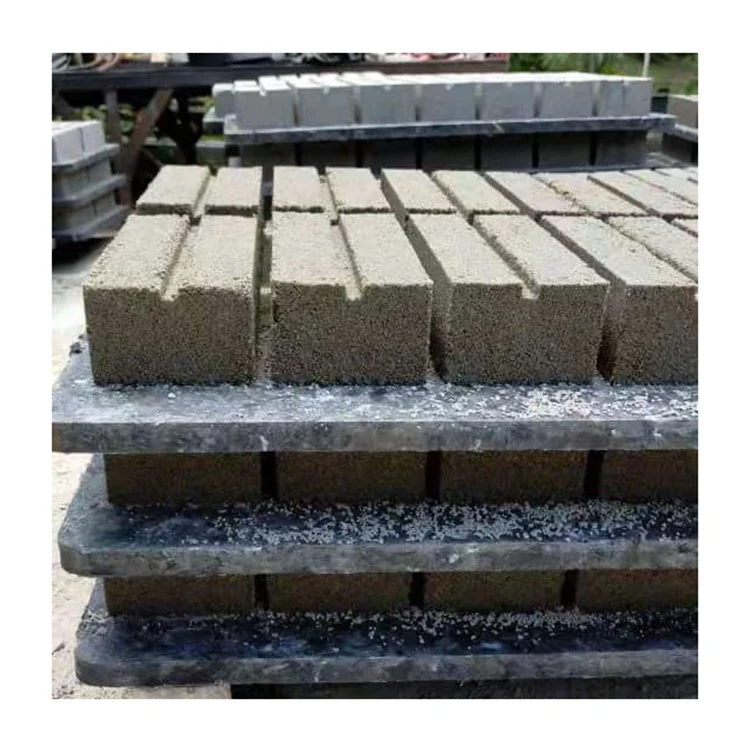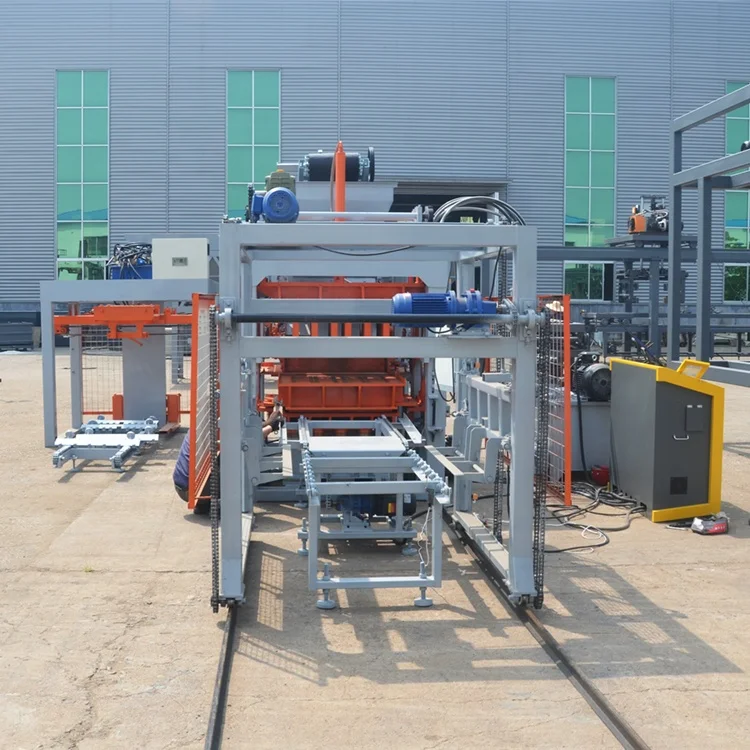
Description
Format-Matched Capacity — every output figure tied to a specific block dimension and mould cavity count rather than a single optimistic headline number.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Hydraulic Cement Block Making Machine |
| Model | QT6-15 |
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Vibration Frequency | 0-60 Hz |
| Vibration Form | Platform Vibration |
| Vibration Force | 45 kN |
| Moulding Mode | Automatic loading with vibration moulding |
| Pallet Size | 880×850 mm |
| Molding Cycle | 15-20 s for standard blocks; 20-25 s for pavers |
| Overall Power | 37 kW |
| Total Mass | 7 T |
| Demolding Method | Hydraulic |
| Control System | PLC with touch screen interface |
| Factory Area Required | 1200 m² |
| Compressive Strength of Blocks | >15 MPa |
| Raw Material Adaptability | Waste ash, slag, cement-based mixes |
| Assembly State | Fully assembled main press with independent hydraulic station |
| Output (Hollow Block 400×200×200 mm) | 1080-1440 pcs/h (basis: stated format and cycle) |
| Output (Hollow Block 400×150×200 mm) | 1440-1920 pcs/h (basis: stated format and cycle) |
| Output (Solid Brick 240×115×53 mm) | 5760-7680 pcs/h (basis: stated format and cycle) |
| Output (Rectangular Paver 200×100×60 mm) | 2160-2880 pcs/h at 20-25 s cycle |
| Output (Zigzag Paver 225×112.5×60 mm) | 2160-2880 pcs/h at 20-25 s cycle |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for masonry walls | Crushed stone, sand, cement-based mixes at 400×200×200 mm and 400×150×200 mm |
| Solid brick manufacturing for load-bearing construction | Local aggregate blended with cement and waste ash at 240×115×53 mm |
| Rectangular paving brick for roads and walkways | High-density mix with fine aggregate at 200×100×60 mm |
| Interlocking zigzag paver for heavy-traffic areas | Cement-bound aggregate at 225×112.5×60 mm |
| On-site block production for housing projects | Locally sourced sand and slag with cement binder |
What a Generic "Cycles per Hour" Figure Leaves Out of Your QT6-15 Block Machine Specifications
A cycle time only becomes meaningful once you state which block format, mould cavity count, and material it assumes.
I have watched buyers sign contracts based on a single hourly output number, only to discover on commissioning day that the figure assumed a small solid brick while their market demands 400×200×200 hollow blocks. The press physically cannot run the larger format at the same cycle, and daily output drops well below the projection. [NEED_CITE: capacity calculation methods in concrete block manufacturing standards] The cement block making machine capacity by format is the only honest way to compare machines, because every format change alters cavity count, fill depth, vibration duration, and demoulding travel. Without that breakdown, you are sizing your plant on a number that does not belong to your product.
Pallet Size Determines Which Formats Actually Fit
The QT6-15 block machine specifications list the pallet at 880×850 mm, and that dimension governs everything downstream. Your block layout on the pallet decides how many cavities each mould can carry. A 400×200×200 hollow block typically arranges in a four-cavity layout on this pallet, while a 240×115×53 solid brick fills the surface with a much higher cavity count. If your existing curing racks and forklift forks are sized for a different pallet, you face a choice between modifying your handling equipment or constraining the block formats you produce.
Mould Change Time and Format Flexibility
Buyers who need multiple formats from one press must ask how long a mould swap actually takes on the shop floor. The QT6-15 uses a hydraulic demolding method and platform vibration, which means the mould sits on a vibrating table clamped by hydraulic bolts. Mould change involves releasing those clamps, lifting the old mould with the overhead crane, lowering the new one, and re-tightening. If the bolt pattern differs between moulds, the operator also repositions the clamp shoes. This is a mechanical task measured in tens of minutes, not a quick-release affair, and it directly affects how many formats you can realistically produce in a single shift. [NEED_CITE: mould change procedures for hydraulic vibration block presses]
How Vibration Force and Hydraulic Pressure Interact
The 45 kN vibration force works together with hydraulic pressure to compact the mix into the mould cavity. Platform vibration transmits energy upward through the pallet into the material, while the hydraulic head presses from above. If your local aggregate is angular crushed stone, the vibration must be strong enough to rearrange particles into a dense pack before the hydraulic pressure locks them in place. If the aggregate is rounded river gravel, less vibration force may suffice but the hydraulic pressure must still reach the threshold needed for >15 MPa compressive strength. The PLC touch screen lets the operator store separate cycle recipes for each format, adjusting vibration duration and pressure hold time independently.
Reading the Specs Against Your Actual Mix
The QT6-15 block machine specifications show an overall power of 37 kW, split across the vibration motors, hydraulic pump, and material feed system. The vibration frequency range of 0-60 Hz is adjustable through the PLC, but the useful window depends on your mix stiffness. A dry, low-slump mix with waste ash may need sustained high-frequency vibration to achieve full compaction, drawing more current from the vibration motors. A wetter mix with slag may compact faster but risks slump after demoulding if the cycle is too aggressive. Matching the QT6-15 cement block making machine capacity by format to your real material requires a factory test with your actual aggregate sample before the machine ships.
The Cost of Skipping the Format Conversation
When the block format is not confirmed before production, the consequences appear one by one after arrival. The mould cavities may not align with the pallet guides, causing misfed material and rejected blocks. The vibration table may be tuned for a different mix stiffness, producing blocks that crack during curing or fail compressive strength tests. The curing area may be too small for the pallet dimensions, forcing manual restacking and creating a bottleneck that has nothing to do with the press itself. [NEED_CITE: common commissioning delays in exported block making equipment] These issues are not machine defects; they are specification gaps that a format-first conversation would have prevented.
Why Sourcing the QT6-15 Here Reduces Format Risk
Every capacity figure in this QT6-15 block machine specifications sheet is tied to a named block dimension and cavity count, so you can size your plant against the product your market actually buys. The pallet size of 880×850 mm is confirmed before quotation, and your existing curing racks and forklift are checked against it. The PLC control language and display are confirmed in writing so operators can read fault codes on day one. Mould drawings are provided for every format, including custom designs if your local standard differs from the off-the-shelf catalogue. The factory test runs your actual mix sample at the target format, and the recorded cycle times form part of the dispatch documentation. Voltage, frequency, and plug configuration are locked in before the electrical panel is wired, eliminating the most common cause of delayed commissioning. [NEED_CITE: export machinery voltage and frequency confirmation practices]
Documentation & Verification
- Capacity calculation sheet stating the assumed block format and cavity count for every output row
- Mould drawing package with dimensional layout matching the 880×850 mm pallet boundary
- Factory test record showing cycle times run with your supplied aggregate sample
- Voltage, frequency, and PLC language confirmation document signed before wiring begins
- Hydraulic and electrical schematic for local maintenance troubleshooting
Installation, Commissioning & Support
- The 1200 m² factory area requirement includes press footprint, pallet return path, and curing rack access lanes
- 37 kW overall power demands a dedicated circuit with soft-start or VFD on the vibration motors to limit inrush current
- The main press ships fully assembled with an independent hydraulic station bolted to the frame for easier container loading
- PLC touch screen calibration and recipe storage for each block format performed during on-site commissioning
- Operator training covers mould change procedure, hydraulic clamp tightening sequence, and vibration frequency adjustment per mix
- Wear parts list identifies hydraulic seals, vibration motor bearings, and mould liner plates by part number for reorder
What to Share When Requesting a Quotation
Send the exact block dimensions your market sells, along with a sample or description of the local aggregate you plan to use. Specify your available voltage and frequency, and confirm the language your operators need on the PLC display. Let us know whether your curing area already has pallet racks and what pallet size they accept, so we can verify the 880×850 mm pallet fits your existing handling flow.
Frequently Asked Questions
Q: How is the QT6-15 cement block making machine capacity by format calculated?
A: Each output row starts from the pallet area of 880×850 mm, divides it by the block footprint including mortar gap, and multiplies by the number of cavities per mould. That figure is then divided by the molding cycle for that format — 15-20 seconds for blocks, 20-25 seconds for pavers — and adjusted for loading and demoulding time.
Q: Can I use a mould for my local block size that is not in the standard catalogue?
A: Yes. We design custom moulds to your drawings and verify cavity count against the 880×850 mm pallet boundary. The mould drawing is submitted for approval before machining, and the first test pressing is included in the factory test record so you can confirm dimensions and block strength before dispatch.
Q: How do I match the 45 kN vibration force to my local aggregate?
A: The PLC allows vibration frequency adjustment from 0-60 Hz and cycle duration tuning per recipe. For angular crushed stone, longer vibration at higher frequency packs particles tightly. For rounded gravel, shorter duration may suffice. A factory test with your aggregate sample confirms the recipe that achieves >15 MPa compressive strength.
Q: What does the 880×850 mm pallet size mean for my curing area layout?
A: Your curing racks must accept pallets of this dimension with clearance for automated handling. Forklift fork width and rack spacing should be verified against this size before the machine arrives. If your existing racks are sized differently, we can discuss pallet adapters or curing rack modification options during the layout planning stage.