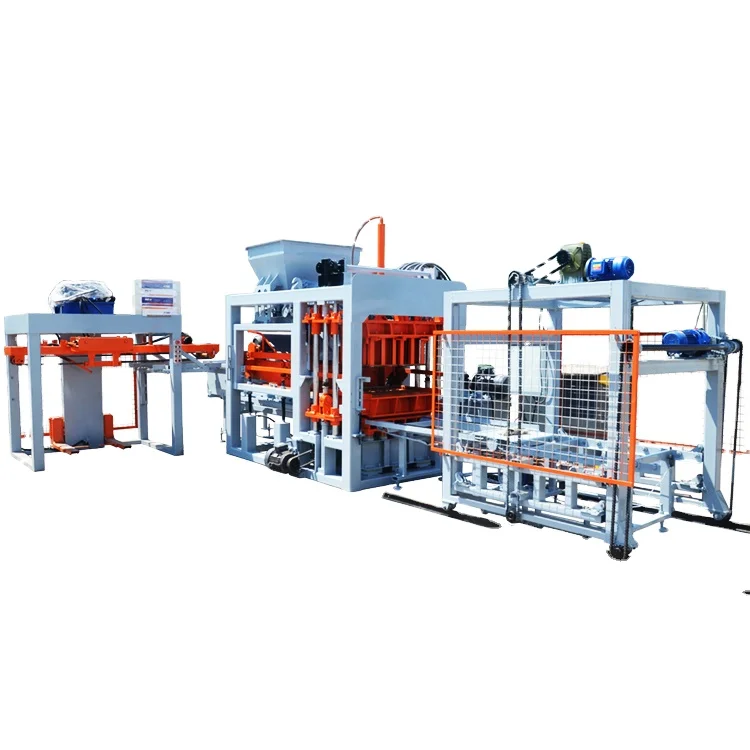
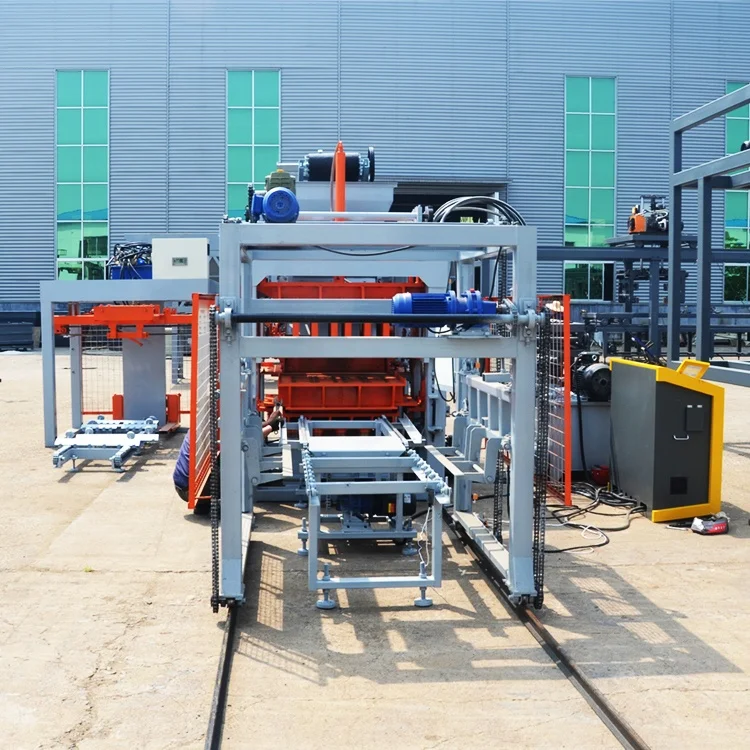


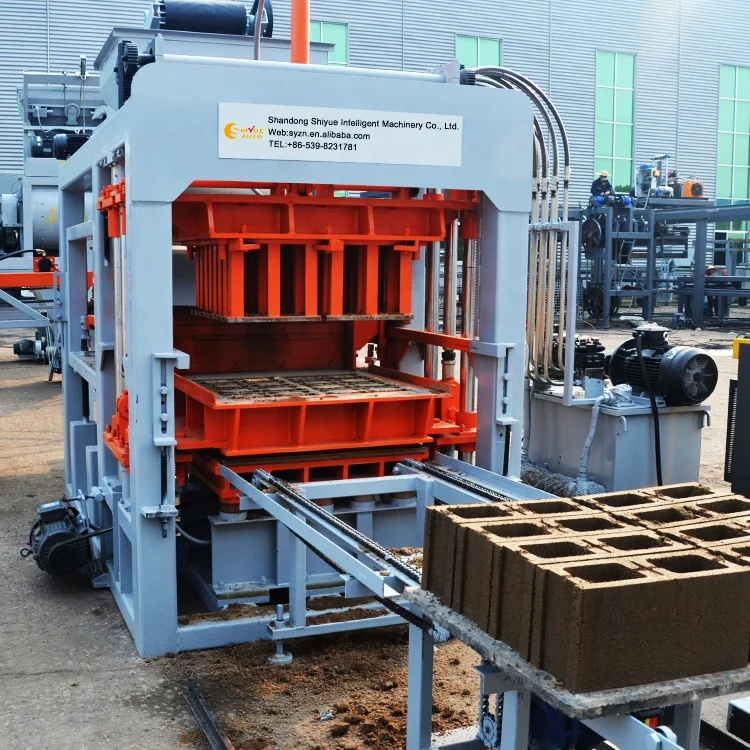

Description
Format-Matched Engineering — Every output figure is tied to a specific block size and cycle time so the QT6-15 delivers what the datasheet promises.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
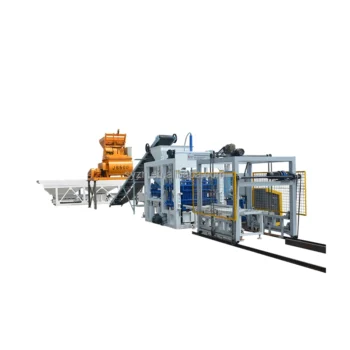
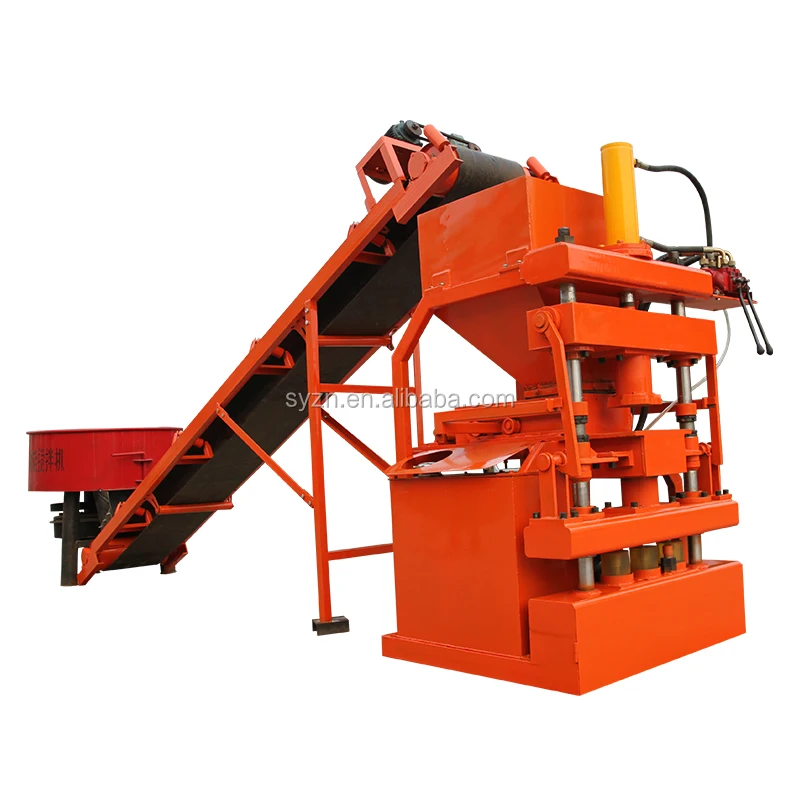
| Product Type | Fully Automatic Hydraulic Vibration Block Making Machine |
| Overall Dimensions (L×W×H) | 7400×1900×2660 mm |
| Total Weight | 7 T |
| Molding Cycle | 15-25 s |
| Vibration Frequency | 4600 r/min |
| Exciting Power (Vibration Force) | 40-50 kN |
| Total Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Control System | PLC control system |
| Hydraulic Station | Included (high pressure, stable operation) |
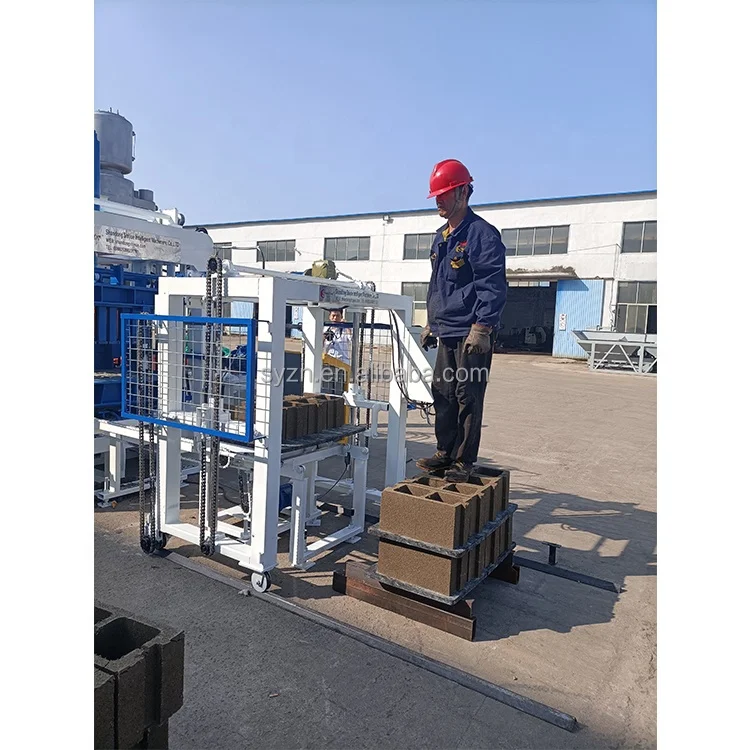
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Output Capacity (Hollow Block 400×200×200 mm) | 1200-1680 pcs/h, 9600-13440 pcs/8hr |
| Output Capacity (Hollow Block 400×150×200 mm) | 1800-2400 pcs/h, 14400-19200 pcs/8hr |
| Output Capacity (Solid Brick 240×115×53 mm) | 3240 pcs/h, 16200-19440 pcs/8hr |
| Cycle Time per Format | 15-20 s (basis: hollow block and solid brick formats listed above) |
| Automation Level | Fully automatic (with pallet feeder, brick conveyor, block sweeper) |
| Voltage & Frequency | To be confirmed with buyer’s local grid |
| PLC Display Language | To be confirmed before production |
| Mould Change Time | To be confirmed with manufacturer |
| Stacking Method | To be confirmed (automatic stacking inclusion unverified) |
| Key Features | PLC controlled, hydraulic pressure and vibration combined, multiple mould compatibility, automatic pallet feeding and block sweeping |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial walls | Crushed stone, sand, cement, fly ash |
| Solid brick manufacturing for load-bearing structures | Sand, cement, dust, crushed stone |
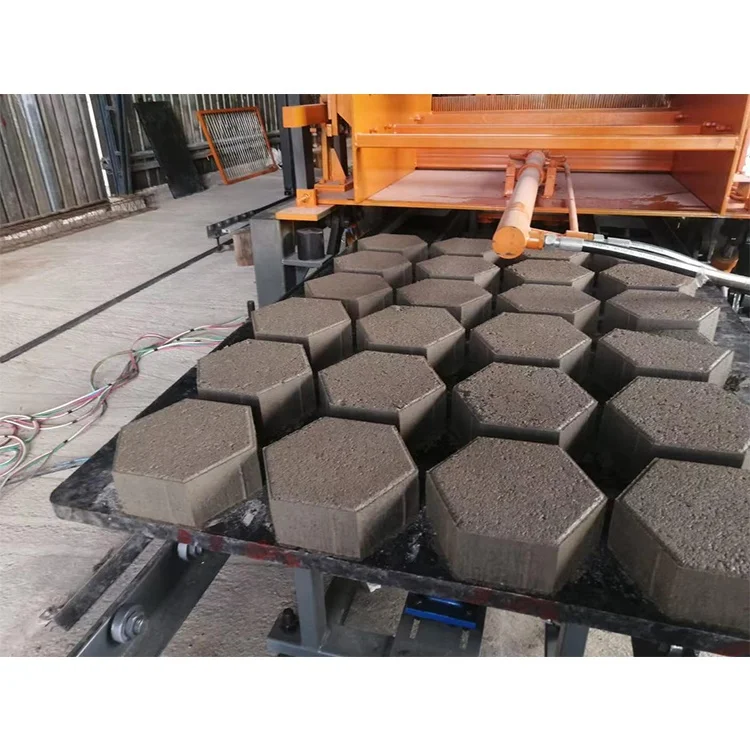
| Paver production for walkways and driveways | Crushed stone, sand, cement |
| Curbstone forming for road and infrastructure projects | Crushed stone, sand, cement |
| On-site block production for housing developments | Local aggregate, cement, fly ash |
| Building material distributor stock expansion | Multiple format moulds for regional demand |
What "15-25 Seconds Cycle Time" Actually Means for Your Daily Output
Cycle time is only meaningful when tied to a specific block format and mould configuration.
I have watched buyers sign contracts based on a single cycle time number, then discover on commissioning day that their primary product runs slower than the brochure suggested. The QT6-15 block making machine specifications list a 15-25 second range, but that range spans fundamentally different products. A 400×200×200 mm hollow block demands a different press rhythm than a 240×115×53 mm solid brick. The vibration profile, hydraulic dwell, and feed cycle all shift. When a supplier quotes one number without naming the format, the buyer ends up with a machine that underperforms against the business plan [NEED_CITE: block format assumptions in capacity quotations].
Matching Block Format to Mould and Cycle
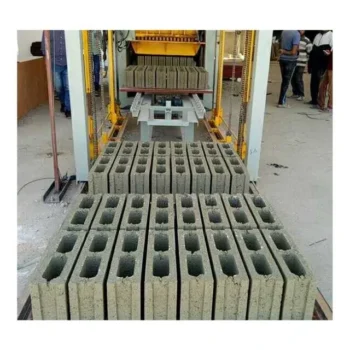
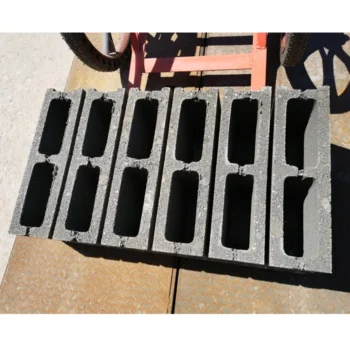
The QT6-15 block making machine supports multiple mould formats, and each one changes the production rhythm. The 400×200×200 mm hollow block yields 1200-1680 pieces per hour based on a 15-20 second cycle. Switch to the 400×150×200 mm hollow block, and the same machine produces 1800-2400 pieces per hour because the smaller cavity fills and compacts faster. The solid brick at 240×115×53 mm runs at 3240 pieces per hour. These numbers only hold when the mould, vibration force, and feed settings are configured for that exact format.
Vibration Force and Local Aggregate Compatibility
The 40-50 kN vibration force at 4600 r/min must be evaluated against the buyer’s actual raw material. Desert sand, common across Middle Eastern sites, requires different vibration tuning than angular crushed stone. I once stood on a site where a machine specified for river gravel could not compact fine desert sand properly, and block strength dropped below the required standard. The mix design and vibration profile have to be developed together. The QT6-15 offers the frequency and force range to work across different aggregates, but only when the configuration starts from the buyer’s material sample rather than a default setting [NEED_CITE: vibration force matching to aggregate particle shape].
Pallet Dimensions and Curing Area Coordination
The 850×550×25 mm pallet size is not a universal standard. It must fit the buyer’s existing curing racks, forklift fork spacing, and storage yard layout. A pallet that is too wide for the curing rack means manual rehandling. A pallet material that warps under local humidity or temperature ruins block flatness. Before the QT6-15 ships, the pallet specification needs to be verified against the site’s handling infrastructure.
Understanding the Core Specifications
The 31.25 kW total power covers the hydraulic pump, vibration motors, mixer, and conveyor drives. This power draw requires a dedicated circuit with appropriate breaker sizing at the installation site. The JQ350 mixer feeds material into the press hopper, and its capacity must keep pace with the fastest cycle the machine can run. The PLC control system coordinates pallet feeding, material dosing, press cycling, and block sweeping in sequence. Without this coordination, the press waits idle between cycles. The hydraulic station delivers the compaction pressure that works together with vibration to achieve target block density. Higher hydraulic pressure compresses the mix more tightly, while vibration settles fine particles into voids. Both must be tuned to the specific mix design to produce consistent block strength across every pallet.
The Cost of Skipping Configuration Verification
When voltage and frequency are not confirmed before production, the machine arrives and cannot start. I have seen entire commissioning schedules collapse because a 380V/50Hz machine was shipped to a 440V/60Hz grid. The PLC display language, if left unspecified, forces operators to navigate menus in a language they cannot read, slowing every mould change and parameter adjustment. Pallet handling equipment that arrives mismatched to the curing area means workers carry blocks by hand, negating the automation the buyer paid for [NEED_CITE: commissioning delays from unconfirmed electrical specifications].
Why Technical Buyers Source Here
Block machinery is the single focus, which means the QT6-15 is specified as a matched system. The machine, mould, pallet, and handling equipment are selected together against the buyer’s target format and local aggregate, not pulled from separate catalogues. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard options do not fit. Configuration starts from the buyer’s mix design and target block strength rather than a default factory setting. Automation level is selectable, so a buyer can begin with the included pallet feeder and conveyor, then add stacking later. Installation and commissioning support includes operator training so the crew can run the machine independently from the first week.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format for each output figure
- Mould drawing and format list confirming all block types and changeover requirements
- Voltage, frequency, and PLC display language confirmation signed before production begins
- Pallet specification sheet covering size, material, and quantity matched to curing infrastructure
- Factory test record on buyer’s specified block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement schedule
Installation, Commissioning & Support
- Foundation pad sized for 7400×1900 mm footprint with vibration isolation requirements
- Dedicated power circuit rated for 31.25 kW total draw at confirmed voltage and frequency
- Machine arrives in dismantled shipment configuration with reassembly guided by technical team
- First-run parameter setting for buyer’s specific mix design and target block format
- Operator training covering PLC navigation, mould changeover, and daily maintenance routines
- Wear parts list with hydraulic seal and vibration motor replacement intervals defined
Preparing Your Technical Inquiry
To size the QT6-15 correctly, provide the specific block formats your market demands along with target daily output for each. Share your local aggregate type and any available mix design data so vibration and hydraulic parameters can be matched. Confirm your site voltage, frequency, and preferred PLC display language to prevent commissioning delays. If you have existing curing racks or forklifts, send their dimensions so the 850×550 mm pallet compatibility can be verified before the order enters production.
Frequently Asked Questions
Q: How is the QT6-15 output capacity verified for each specific block format?
A: Each output figure is calculated from a defined block size and its corresponding cycle time. The 400×200×200 mm hollow block runs at 15-20 seconds per cycle yielding 1200-1680 pieces per hour. Verification requires a factory test on the buyer’s actual mould format, and the capacity calculation document states the exact format assumed so there is no ambiguity between quoted and delivered output.
Q: What mould formats are available and how long does a mould change take?
A: The QT6-15 accepts moulds for hollow blocks, solid bricks, pavers, and curbstones. Custom mould designs are available to buyer drawings. Mould change time depends on the changeover system configuration and must be confirmed with the manufacturer before purchase, as this directly affects how many format switches are practical within a single production shift.
Q: How should the machine be configured for local aggregate and mix design?
A: Configuration starts with the buyer’s material sample and target block strength. Vibration force and frequency are adjusted alongside hydraulic pressure to match the aggregate particle shape and cement content. Desert sand requires different tuning than crushed stone. The mix design and machine parameters must be developed together to ensure consistent density and strength across every production run.
Q: What voltage, frequency, and PLC language options are confirmed before shipment?
A: The buyer’s local grid voltage and frequency must be confirmed before production begins to ensure the motor and hydraulic pump are wound correctly. The PLC display language is set to the buyer’s preference so operators can navigate all menus without translation barriers. Both items are documented and signed off during the order confirmation stage.
Q: Is the 850×550 mm pallet compatible with existing curing racks and forklifts?
A: Compatibility depends on the buyer’s specific equipment. The curing rack slot width must accommodate the 850 mm dimension, and forklift fork spacing must handle the 550 mm width safely. Pallet material must also suit local temperature and humidity conditions. These dimensions should be verified against site infrastructure before the pallet order is finalized.