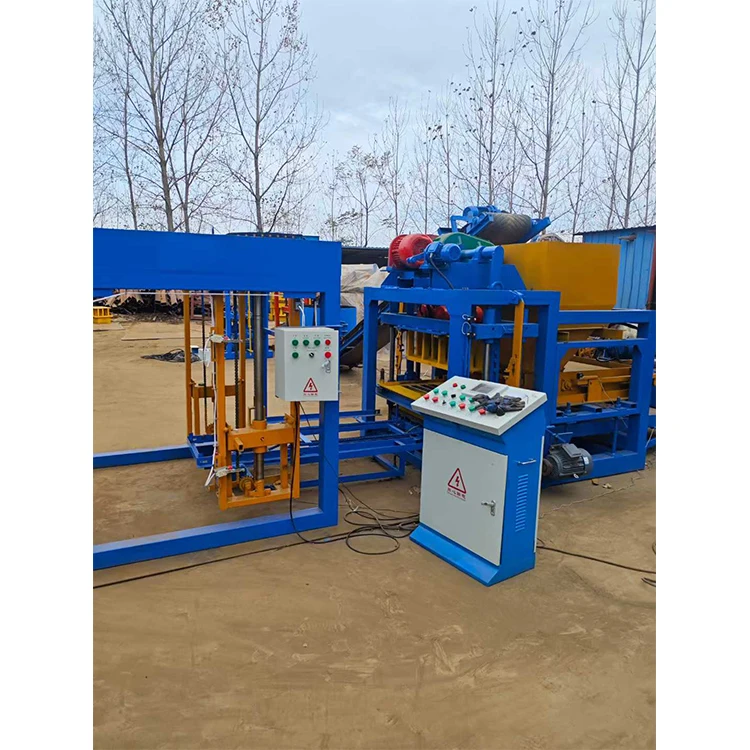
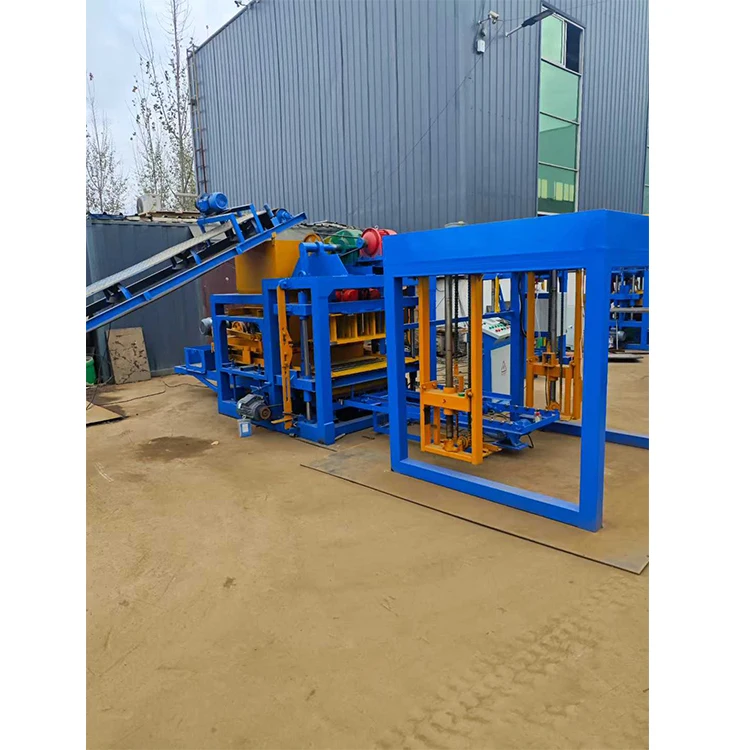
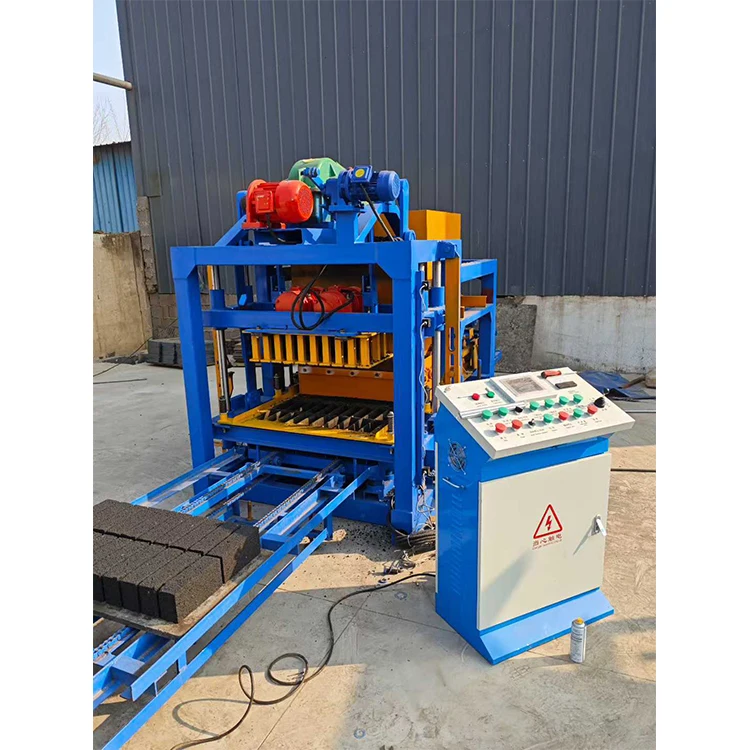
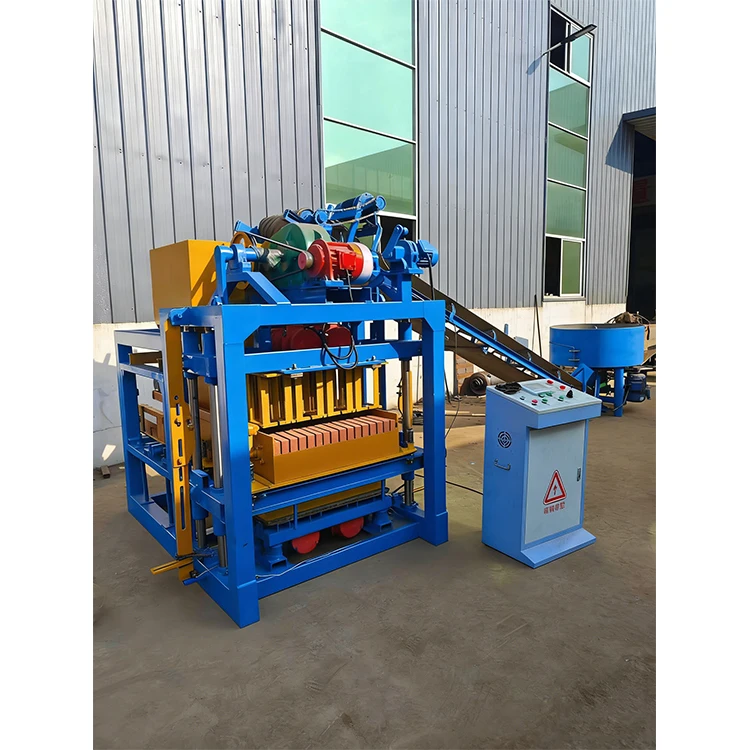
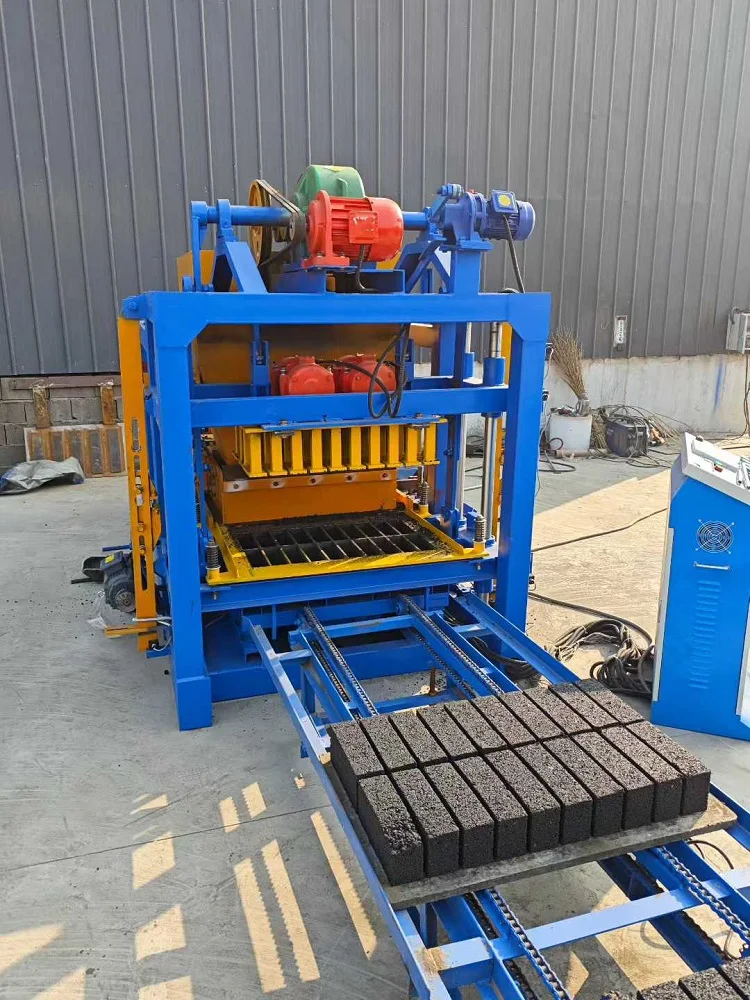
Description
Pallet sizing locked to your curing layout — the 850 × 480 mm pallet on the QTJ4-25D is confirmed against your existing racks and forklift before the machine is built, so freshly pressed blocks move straight into curing without a handling bottleneck.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25D |
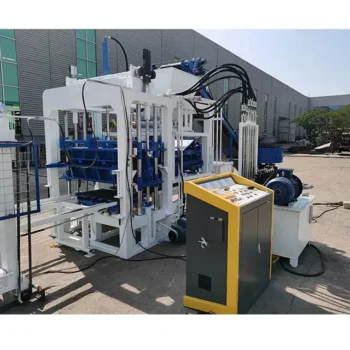
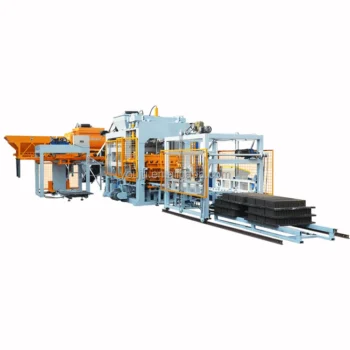
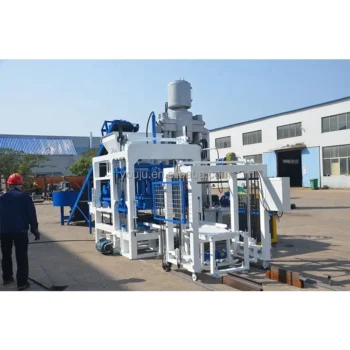
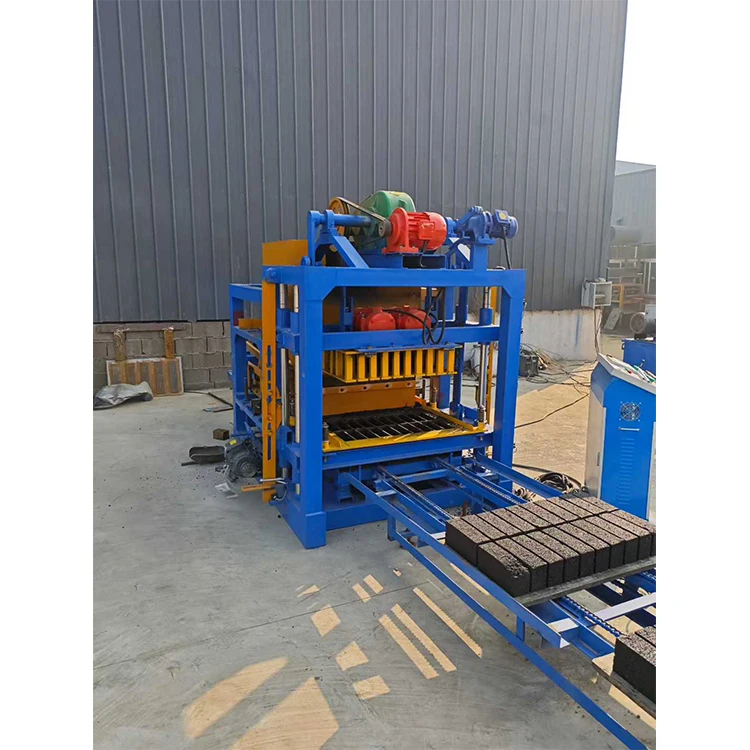
| Product Type | Automatic Concrete Hollow Block Making Machine |
| Control System | PLC controlled, fully automatic |
| Rated Power | 16.58 kW |
| Molding Cycle | 25 seconds |
| Output Capacity | 4600 pcs / 8 hours (basis not stated in source — confirm block format, material, and thickness) |
| Machine Weight | 5000 kgs |
| Overall Dimensions (L×W×H) | 6400 × 1500 × 2700 mm |
| Pallet Size | 850 × 480 mm |
| Voltage | Configurable to buyer’s local voltage and frequency |
| Raw Materials | Concrete, sand, cement, fly ash, crushed stone, lime, water |
| Vibration System | Vibration motor + large vibration box (force rating to be confirmed) |
| Hydraulic Pressure | Not applicable — vibration-only compaction |
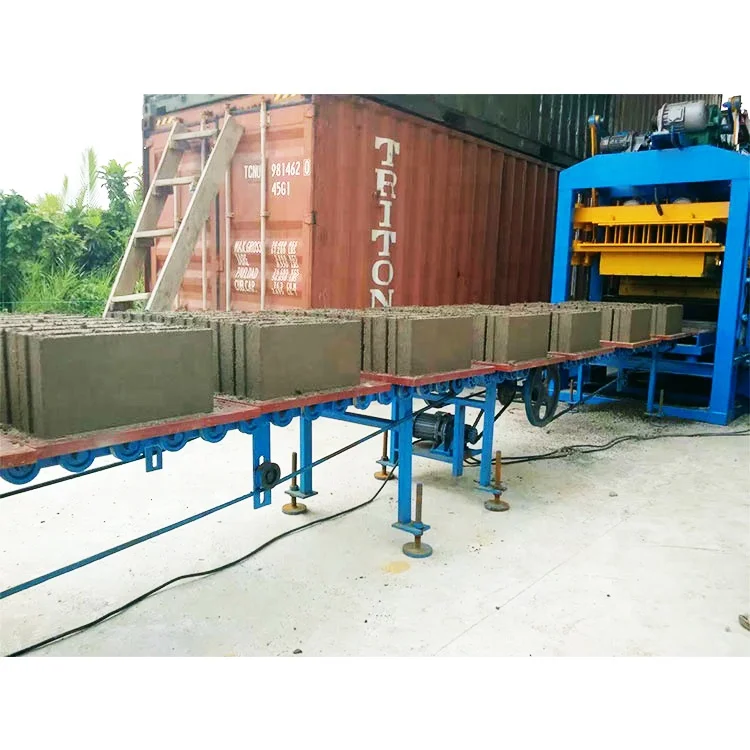
| Key Features | Automatic pallet feeding, automatic material feeding and scraping, automatic block stacker |
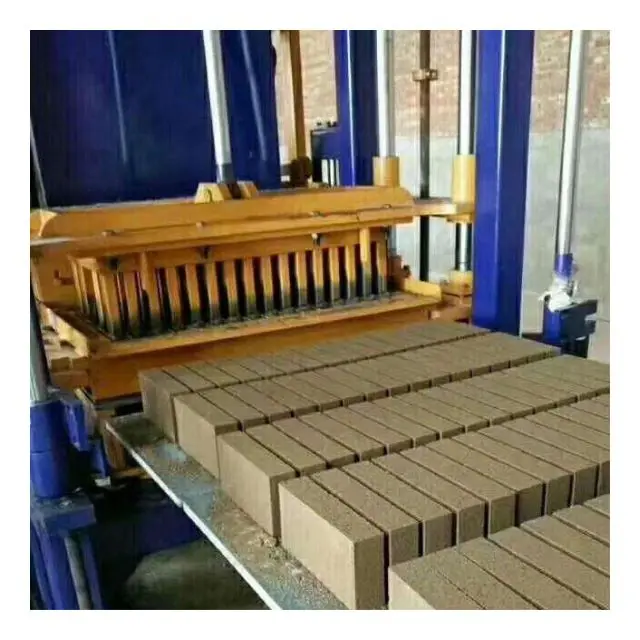
| Block Formats Supported | Hollow blocks, solid blocks/bricks, paver stones (mould list to be confirmed) |
| Motor Brand | Siemens motor (verify against datasheet) |
| Frame Construction | Thickened steel frame |
| Warranty | 1 year with free parts supply |
Application Suitability
| Application | Material or Output |
|---|---|
| Medium-scale hollow block production | Crushed stone, cement, sand, and water |
| Solid brick manufacturing for local housing projects | Fly ash blended with lime and cement |
| Paver stone production for walkways and driveways | Concrete with fine aggregate |
| On-site block production for development contractors | Locally sourced sand and crushed stone |
| Format expansion for existing block manufacturers | Cement-based mixes matching existing plant recipes |
What "4600 Pieces in 8 Hours" Actually Depends On
That figure only holds when the block format, wall thickness, and aggregate blend match the test conditions used to derive it.
I once watched a medium-output machine arrive at a job site in Eastern Europe where the buyer had ordered based on a cycle time proven on standard graded sand. The local river sand ran coarser, the mould cavities filled unevenly, and real output dropped to roughly half the quoted number before anyone understood why. The QTJ4-25D automatic concrete block making machine specifications look capable on paper, but the 25-second cycle assumes a specific material behaviour that must be validated against your own mix [NEED_CITE: effect of aggregate grading on vibration compaction cycle time]. Without that validation step, the pallet stacker and curing area downstream sit idle while the press struggles through incomplete fills.
Mould Cavity Count versus Real Daily Output
Every block format that fits the 850 × 480 mm pallet yields a different number of pieces per cycle. A hollow block with three cavities may produce four pieces per pallet, while a solid brick mould might fit sixteen on the same surface. The QTJ4-25D automatic concrete block making machine delivers one pallet every 25 seconds, so multiplying that cycle by the cavity count for your target format is the only honest way to project daily volume. This is the calculation we run before a quotation goes out, and it is the document you should ask for.
Pallet Size as a Line Design Constraint
The 850 × 480 mm pallet is not a detail you adjust later. It determines how many blocks sit on each board, how many boards fit on a single curing rack tier, and whether your existing forklift tines can lift a fully loaded rack. Choosing a QTJ4-25D automatic concrete block making machine without confirming pallet compatibility against your curing area means either wasting floor space or building new racks [NEED_CITE: pallet and curing rack sizing in concrete block plants]. We confirm pallet material and dimensions in writing before production starts.
Vibration Force and Aggregate Matching
This model uses a vibration motor paired with a large vibration box rather than hydraulic pressure. That design keeps the machine simpler and reduces maintenance points, but it also means compaction energy is fixed by the motor and box geometry. If your local aggregate is angular crushed stone, the vibration must be strong enough to settle it fully into the mould corners. We review your material sample and mix proportions to confirm that the vibration system can achieve consistent block density with your actual raw materials.
When the Quoted Output Breaks Down at the Site
A machine rated for a 25-second cycle on a clean, well-graded mix will behave differently when fed material with inconsistent moisture or oversized particles. Mould cavities fill short, the automatic scraper cannot compensate, and the operator ends up pausing the cycle to clear jams. Output that looked reliable in a factory test becomes unpredictable in daily production, and the stacking and curing stages downstream fall out of rhythm. These issues trace back to specifying the machine without anchoring cycle time to the buyer’s own material [NEED_CITE: common causes of output shortfall in concrete block production].
Why Buy the QTJ4-25D Through This Configuration Process
The QTJ4-25D is specified as a matched system — machine, mould, pallet, and handling equipment sized together rather than sourced separately. Capacity calculations state the exact block format assumed, so you know what you are committing to. Mould drawings and format lists are provided before order confirmation, including custom mould design from your drawings. Voltage, frequency, and PLC display language are confirmed in writing before the machine enters production. Factory test records use your target mix where sample material is available.
Documentation & Verification
- Line layout drawing showing pallet flow from press through curing racks for your block format
- Capacity calculation sheet stating the block format and wall thickness behind each output figure
- Mould drawing and complete format list confirming cavity count per pallet
- Pallet specification sheet noting size, material, and forklift compatibility
- Voltage, frequency, and PLC language confirmation signed before production
- Factory test record on your target mix when sample material is supplied
Installation, Commissioning & Support
- Foundation plan based on the 6400 × 1500 mm footprint and 5000 kg machine weight
- Electrical schematic confirming voltage and dedicated circuit requirements for the 16.58 kW rated power
- Machine arrives partially dismantled for container loading with reassembly guidance on site
- Commissioning includes cycle time verification against your actual raw material blend
- Operator training covers PLC navigation in the confirmed display language
- Wear parts list identifying mould liners, vibration box components, and replacement pallets
Before You Send an Inquiry
To size the QTJ4-25D correctly, we need your target block format and wall thickness, the aggregate and cement you plan to source locally, and the daily output your market requires. Share your curing area dimensions and forklift specification so the 850 × 480 mm pallet can be validated against your existing handling setup. If you have a preferred voltage, frequency, and control language, include those details so the electrical and PLC configuration is locked in before we quote a lead time.
Frequently Asked Questions
Q: What is the realistic daily output of the QTJ4-25D for my specific block format?
A: The 4600-piece figure is a reference point that must be recalculated for your actual block size and cavity count. We multiply the 25-second cycle by the number of pieces each mould produces on the 850 × 480 mm pallet, then factor in material feed behaviour with your local aggregate. A written capacity breakdown per format is provided with every quotation.
Q: Which mould formats are available and how long does a mould change take?
A: The QTJ4-25D supports hollow blocks, solid bricks, and paver stones within the pallet envelope. Specific mould options and changeover procedures depend on the formats your market demands, including custom designs from your drawings. We provide a complete format list before order confirmation so you know exactly which products the machine will produce.
Q: Is the 850 × 480 mm pallet compatible with my curing area and forklift?
A: We confirm pallet size, material, and stacking pattern against your curing rack dimensions and forklift tine width before production. If your existing handling equipment requires an adjustment, we address it at the specification stage rather than discovering a mismatch after the machine arrives on site.
Q: How do I match vibration force to my local aggregate for consistent block strength?
A: The vibration motor and large vibration box deliver a fixed compaction energy suited to medium-output plants. We review your aggregate grading and mix proportions to confirm the system can fully settle your material into mould corners. When a mismatch is identified, we adjust the recommendation before the order is placed.
Q: What voltage, frequency, and PLC language will be confirmed before shipment?
A: These three items are confirmed in writing before the machine enters production. The electrical system is configured to your local supply, and the PLC display is set to your preferred language so commissioning proceeds without delays caused by communication gaps between the operator and the control interface.