


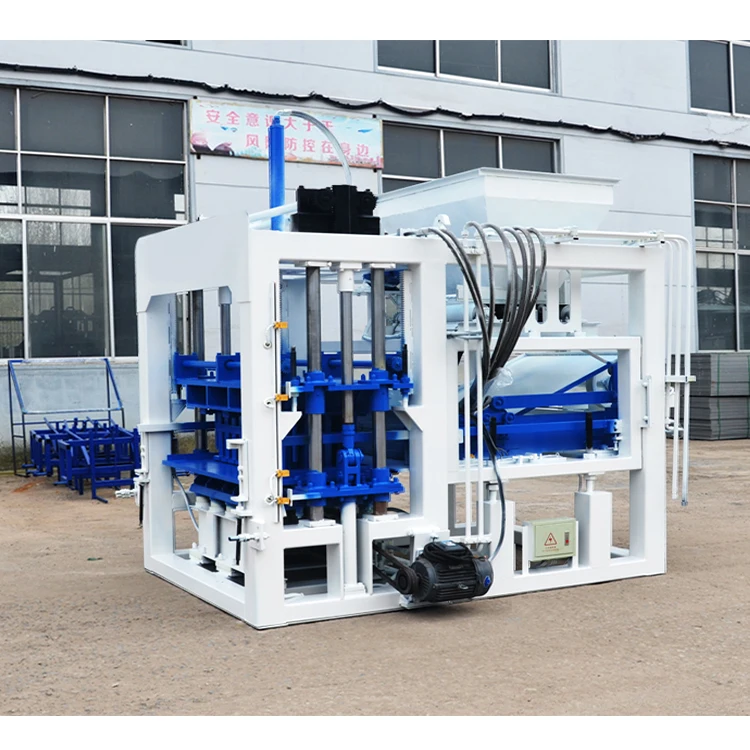
Description
Format-matched output — every QT5-15 capacity figure below is tied to a specific block size, pallet dimension, and cycle time rather than quoted from a generic catalogue sheet.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
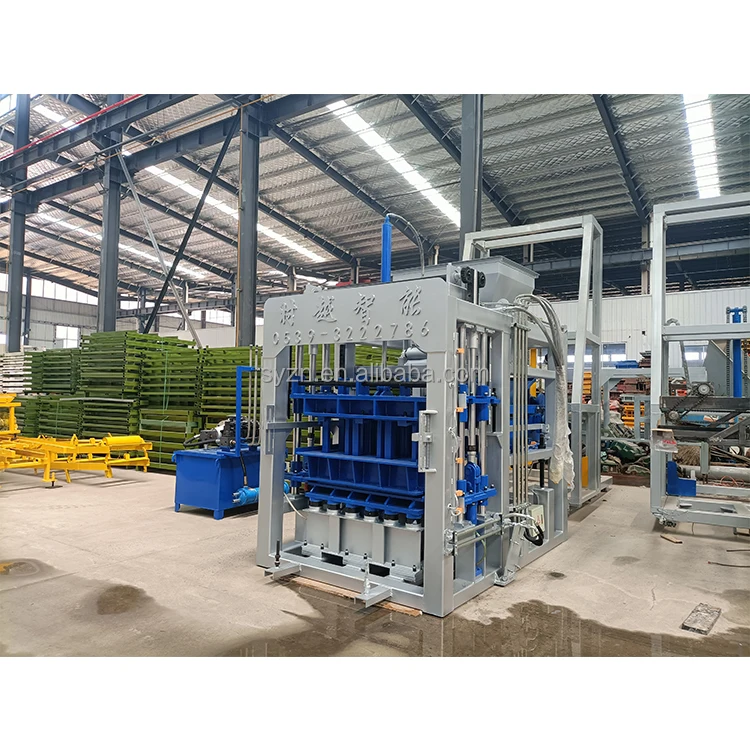
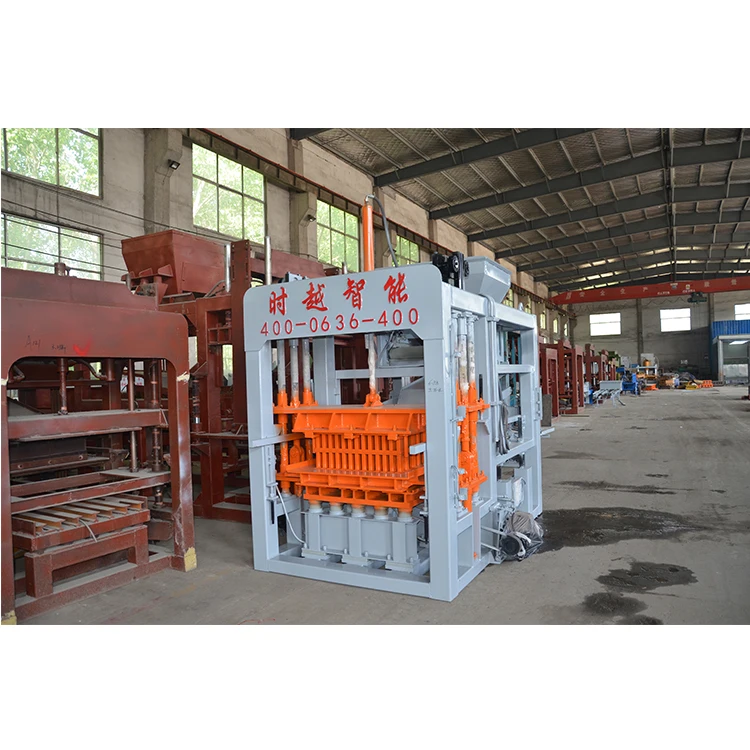
| Product Type | Fully Automatic Concrete Block Making Machine |
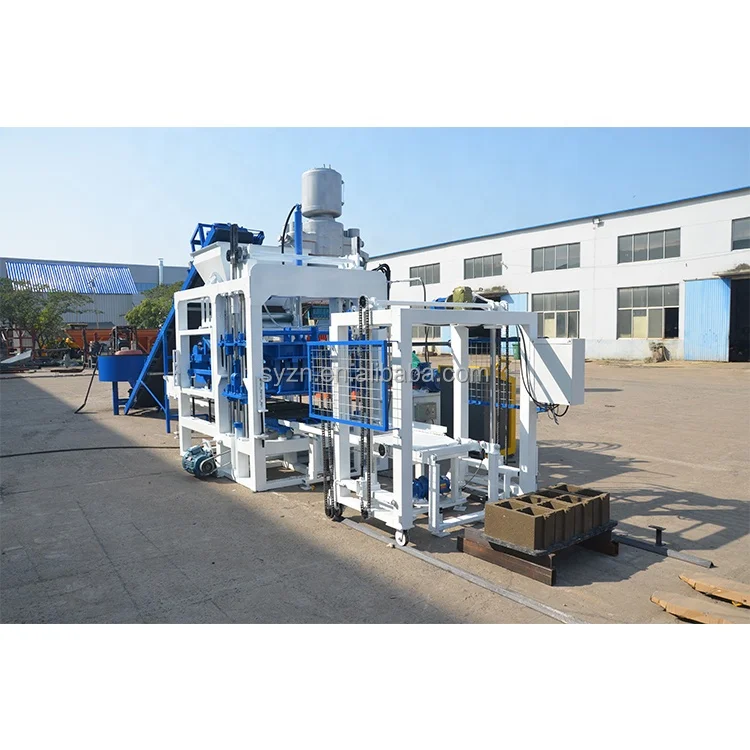
| Overall Dimensions (L×W×H) | 7400×1950×2800 mm |
| Total Mass | 5000 kg |
| Pallet Size | 1100×550 mm |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 0-60 Hz |
| Vibration Force | 80 kN |
| Moulding Mode | Automatic loading with vibration moulding |
| Demolding Method | Hydraulic |
| Molding Cycle | 15-20 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 32 kW |
| Control System | PLC with touch screen interface |
| Hydraulic System | Independent integrated hydraulic station |
| Automation Level | Fully automatic (pallet feeding, material feeding, vibrating, demoulding) |
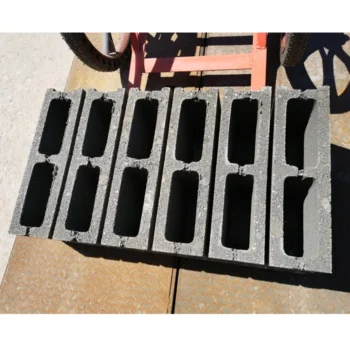
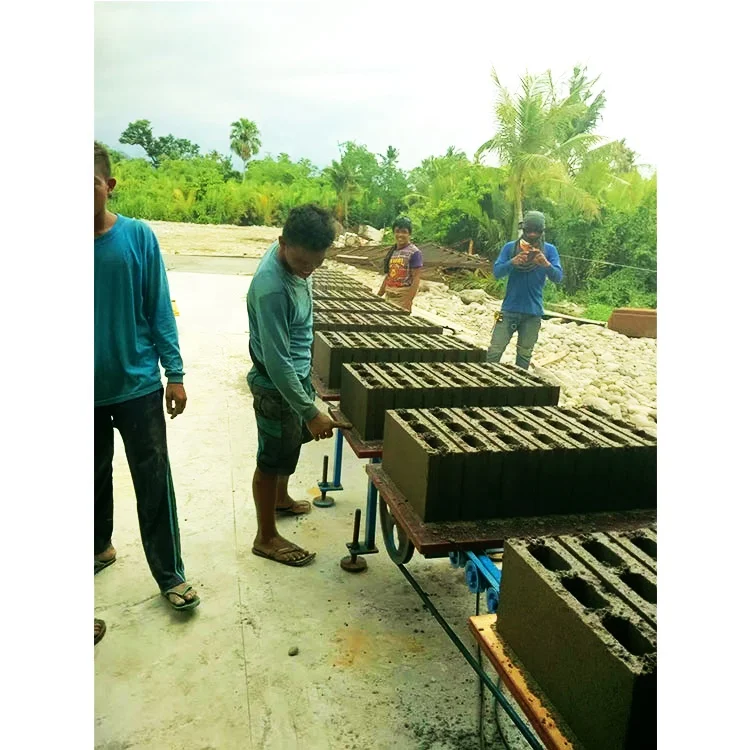
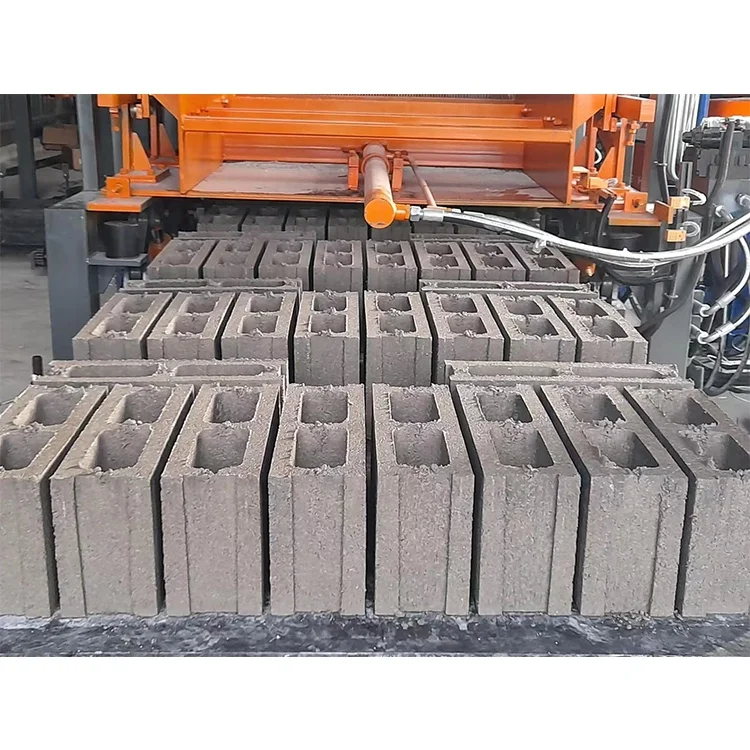
| Output — Hollow Block 400×200×200 mm | 900-1200 pcs/h, 7200-9600 pcs/8hr (5 pcs/mould, 15-20 s cycle) |
| Output — Hollow Block 400×150×200 mm | 1080-1440 pcs/h, 8640-11520 pcs/8hr (6 pcs/mould, 15-20 s cycle) |
| Output — Solid Brick 240×115×53 mm | 5760-7680 pcs/h, 46080-61440 pcs/8hr (32 pcs/mould, 15-20 s cycle) |
| Output — Rectangular Paver 200×100×60 mm | 3600-4500 pcs/h, 28800-36000 pcs/8hr (25 pcs/mould, 20-25 s cycle) |
| Output — Zigzag Paver 225×112.5×60 mm | 2304-2880 pcs/h, 18432-23040 pcs/8hr (16 pcs/mould, 20-25 s cycle) |
| Raw Material Compatibility | Fly ash (up to 70%), slag, gangue, sand, crushed stone, cement, water |
| Recommended Factory Area | 1000 m² |
| Voltage & Frequency | Configurable — confirm before order |
| PLC Display Language | Configurable — confirm before order |
| Warranty | 1 year for whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
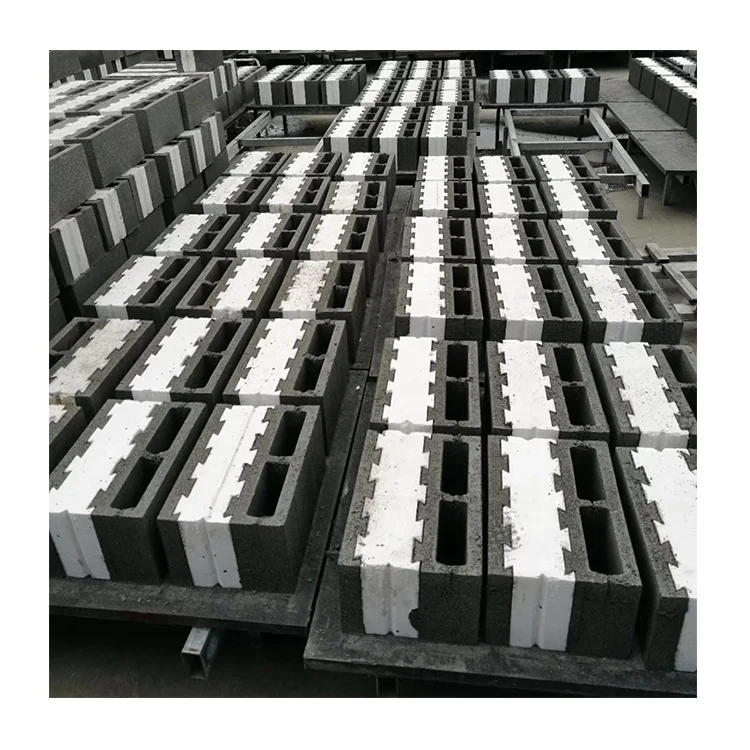
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid brick manufacturing for masonry | Sand, gangue, slag with cement binder |
| Rectangular paving brick for roads and yards | High-density aggregate mix with cement |
| Interlocking zigzag paver for driveways | Graded crushed stone and cement |
| Industrial residue utilisation | Fly ash, slag, gangue as primary aggregate |
What "15-20 Seconds per Cycle" Actually Means for Your Output
A cycle time only matters when you know which block format and mould cavity count it was measured on.
Suppliers often quote the shortest cycle they have ever achieved on the easiest format, then let buyers assume that number applies across every mould they will ever run. I have seen projects where the daily hollow block target was missed by a wide margin because the quoted cycle was taken from a solid brick test with a completely different material profile. The QT5-15 block machine specifications listed above tie each output figure to a specific block dimension, cavity count, and cycle range so you can calculate realistic shift totals for the format your market actually buys. [NEED_CITE: common discrepancies in block machine capacity quoting]
Matching the Press to the Block Your Market Sells
The QT5-15 block machine specifications cover five distinct output tiers, each tied to a different mould configuration. A buyer producing 400×200×200 mm hollow blocks will see five cavities per cycle, while the same press running 240×115×53 mm solid bricks fills thirty-two cavities in the same window. Choosing the right starting format determines not only daily volume but also pallet turnover speed, curing rack occupancy, and the labour required downstream to handle the output.
Pallet Size, Curing Area, and the Forklift You Already Own
The 1100×550 mm pallet dimension was not picked at random. It dictates how many blocks sit on each board, how the boards stack in the curing yard, and whether the forklift tines on site can carry a full rack without modification. When a buyer’s existing curing area was designed around a different pallet standard, the entire handling chain — from press discharge to stacking — has to be rethought. [NEED_CITE: pallet standardisation in concrete block production] Confirming pallet size against the buyer’s yard layout before the order is placed avoids costly rescheduling after the machine arrives.
Reading the Specs That Actually Shape Block Quality
Vibration force and hydraulic pressure work together during compaction. The 80 kN platform vibration compacts the aggregate matrix, while the independent hydraulic station supplies consistent demoulding force without pressure drops caused by shared circuits. If the hydraulic pressure is too low relative to vibration intensity, blocks emerge with weak edges and inconsistent density. The 0-60 Hz vibration frequency range allows fine-tuning for different mix designs — finer sand requires higher frequency, while coarse crushed stone needs lower frequency with longer dwell. The PLC touch screen stores these parameters so an operator can recall a proven recipe instead of re-entering values after every mould change. Overall power draw sits at 32 kW, which determines the dedicated circuit and transformer sizing the buyer must arrange before installation.
The Cost of Skipping the Mix-Design Conversation
When a machine is configured for a standard sand mix that the buyer cannot source locally, the result is weeks of trial-and-error on site. Red clay with high plasticity, for example, sticks to mould walls and slows demoulding far beyond the quoted cycle time. Fly ash from different power stations varies widely in fineness and carbon content, altering water demand and final block strength. I once spent two full weeks adjusting parameters for a client whose local laterite soil behaved nothing like the test aggregate we used at the factory. Every specification sheet for the QT5-15 block machine specifications should be validated against a sample of the buyer’s actual raw material before production begins. [NEED_CITE: impact of local aggregate variability on block machine performance]
Why Buyers Come Back for a Second Line
Capacity calculations are issued per block format, not as a single headline number, so buyers can plan around the products their market actually demands. Mould designs are produced from the buyer’s own drawings when standard formats do not match local building codes. The pallet, handling equipment, and stacking arrangement are specified as one matched system rather than left for the buyer to source separately. Voltage, frequency, and PLC display language are confirmed in writing before production starts, eliminating the most common commissioning delays. Factory test records document actual cycle times on the buyer’s chosen format, not a catalogue benchmark.
Documentation & Verification
- Line layout showing pallet flow and curing rack arrangement for the 1100×550 mm board
- Capacity calculation sheet stating the exact block format behind every output figure
- Mould drawing and format list covering all block types in your product range
- Voltage, frequency, and PLC language confirmation signed off before production
- Factory test record with measured cycle times on your selected block format
- Hydraulic and electrical schematic for on-site troubleshooting
Installation, Commissioning & Support
- Foundation plan sized to the 7400×1950 mm footprint and 5000 kg operating mass
- Dedicated 32 kW power circuit with confirmed voltage and frequency before energising
- PLC touch screen configured in the operator’s language prior to first run
- Vibration frequency and hydraulic pressure tuned to the buyer’s verified mix design
- Mould change procedure demonstrated with realistic changeover time on site
- Wear parts list and recommended reorder intervals for hydraulic seals and mould liners
What We Need from You to Size the Line Correctly
Send us a sample of your local aggregate — sand, crushed stone, fly ash, or slag — along with the block formats your market sells and the daily volume you need to hit. Tell us the voltage and frequency at your site, the PLC language your operators read, and the dimensions of your existing curing yard so we can match pallet handling to your layout. If you already run forklifts or curing racks, share those specifications so the line integrates without rework.
Frequently Asked Questions
Q: How is output capacity verified and which block format does each figure assume?
A: Every output number in the QT5-15 block machine specifications is paired with a specific block dimension, cavity count, and cycle range. A factory test record documents actual measured cycle times on the buyer’s chosen format before dispatch, rather than relying on a catalogue benchmark that may not reflect the buyer’s mix or mould configuration.
Q: How do I match vibration force and hydraulic pressure to my local aggregate?
A: The 80 kN vibration force and 0-60 Hz frequency range are adjusted against the buyer’s submitted mix sample. Coarse aggregate typically needs lower frequency with higher amplitude, while fine sand requires the opposite. Hydraulic pressure is then set to match demoulding resistance, ensuring blocks release cleanly without edge damage or density loss.
Q: What is the mould change procedure and realistic changeover time?
A: The QT5-15 uses a bolt-on mould frame with hydraulic clamping. Changeover involves removing the current mould box, positioning the new one, and re-aligning the vibration table. Actual time depends on operator familiarity and whether the new mould requires pallet guide adjustment. A realistic changeover window is confirmed during on-site commissioning.
Q: How are pallet size and material chosen for my curing area?
A: The standard 1100×550 mm pallet is evaluated against the buyer’s curing rack spacing, yard dimensions, and forklift capacity. If the existing yard was designed for a different board size, an alternative pallet dimension can be specified before production so that downstream handling remains unchanged.
Q: What voltage, frequency, and PLC language options are confirmed before shipment?
A: Voltage and frequency are matched to the buyer’s site supply and written into the production order. The PLC touch screen language is set to the operator’s preference. Both items are confirmed in a signed document before the machine enters assembly, preventing the most common delays during commissioning.