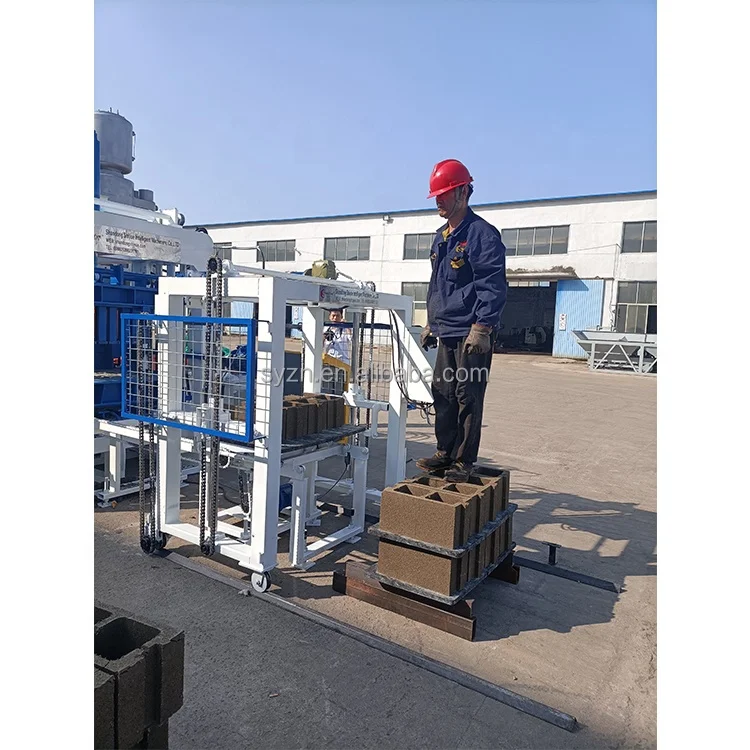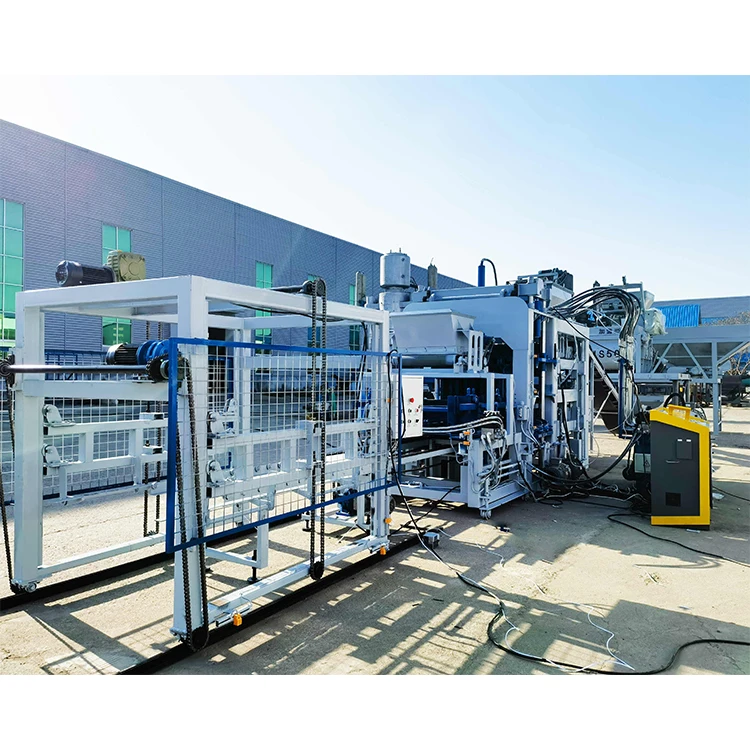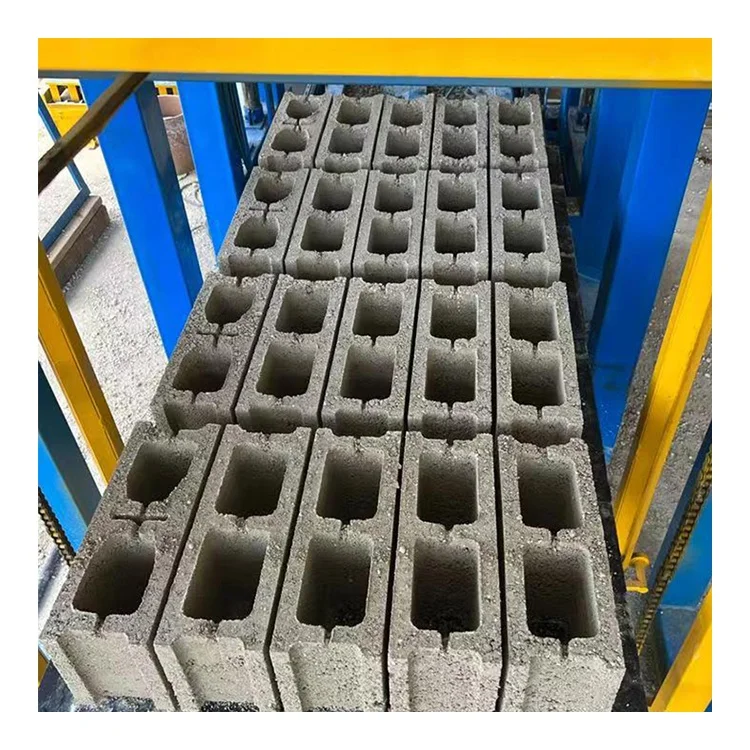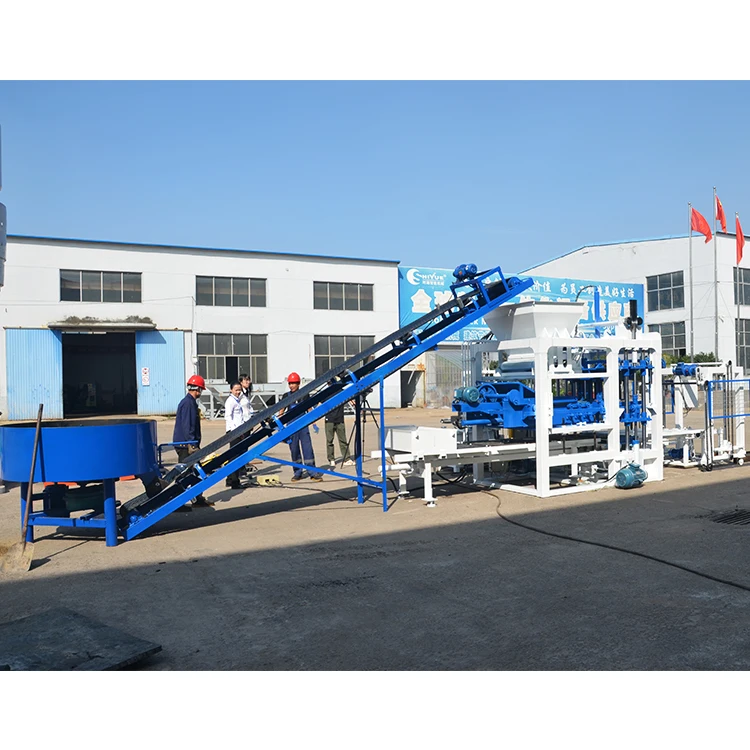
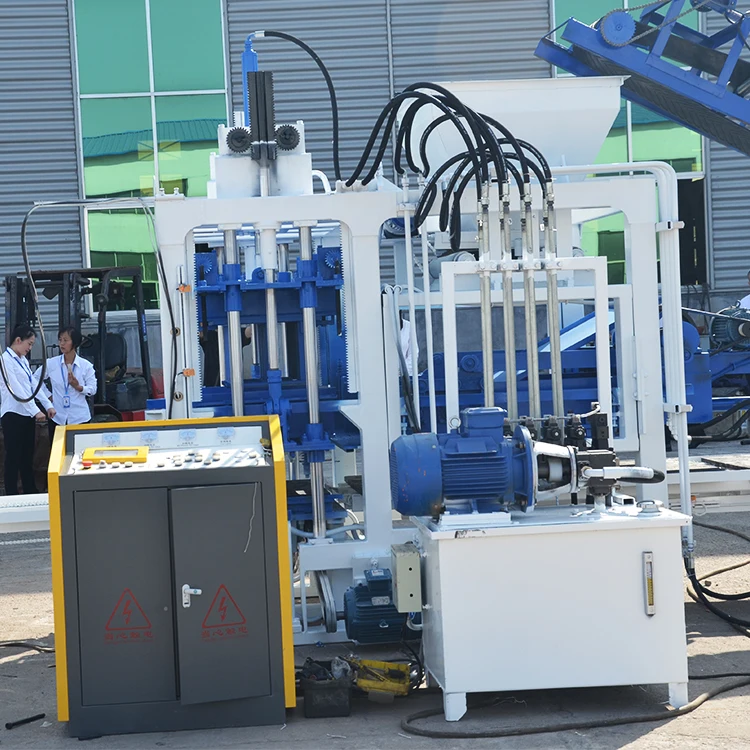
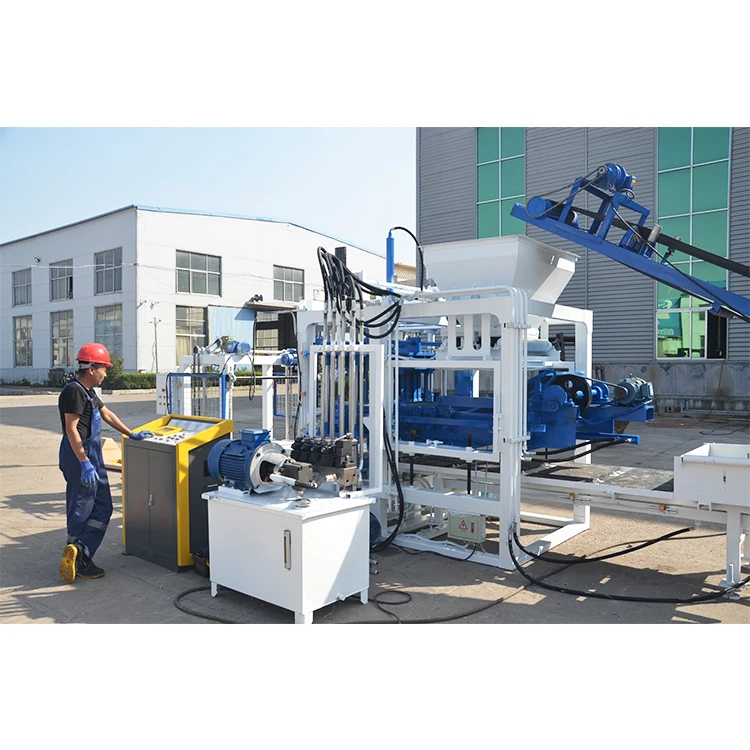
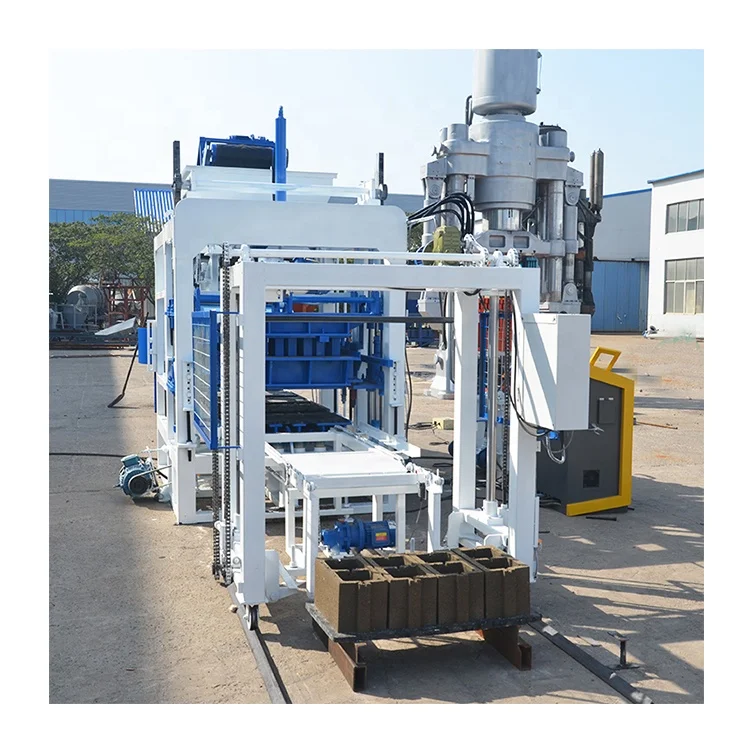
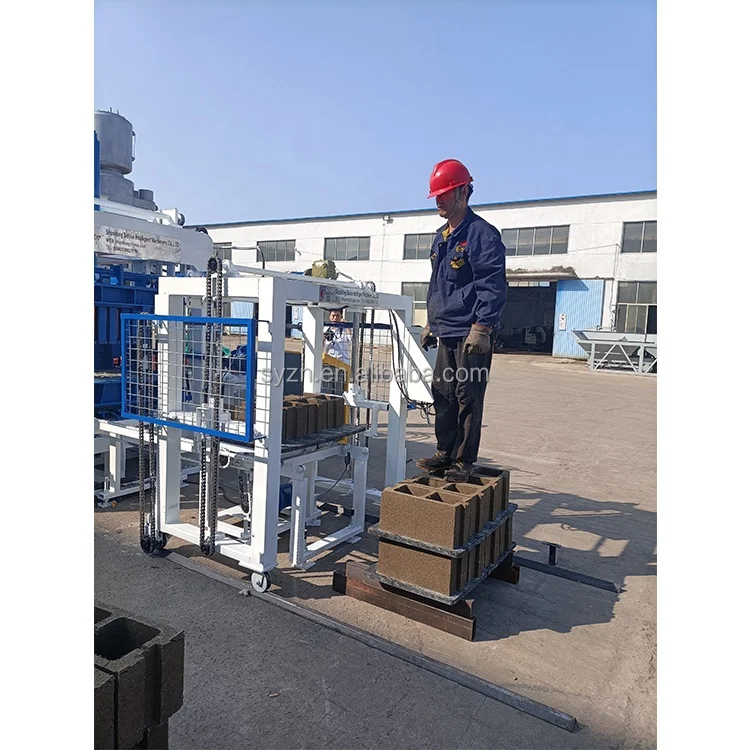
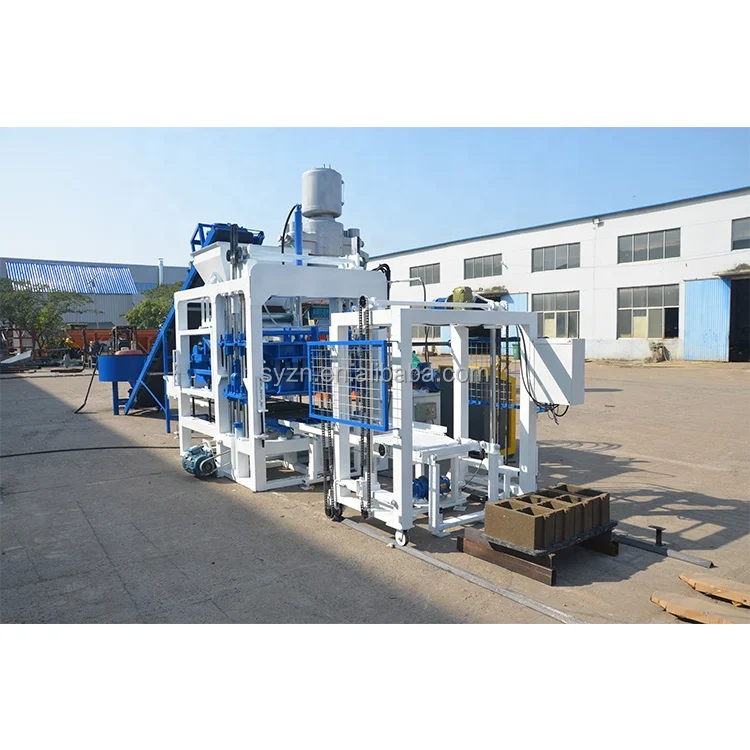
Description
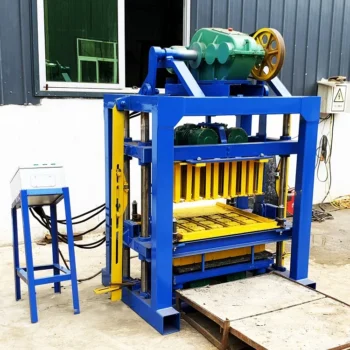
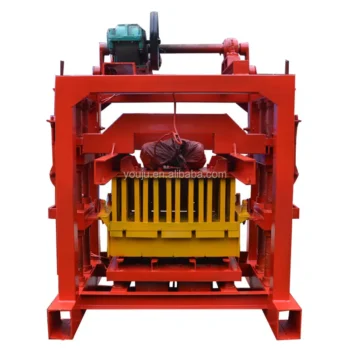
Format-Matched Sizing — Every QT4-18 quotation starts with your local aggregate test report and target block dimensions before we quote a cycle time.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Vibration Frequency | 0-60 HZ |
| Vibration Form | Platform Vibration |
| Pallet Size | 900 x 500 MM |
| Molding Cycle | 18-25 S |
| Vibration Force | 45 KN |
| Demolding Method | Hydraulic |
| Control System | PLC (source value — verify against manufacturer catalog) |
| Output Capacity (Hollow Block 400x200x200mm) | 799 pcs/hour, 6399 pcs/8hr (basis: 4 pcs/mould, 18s cycle) |
| Output Capacity (Hollow Block 400x150x200mm) | 999 pcs/hour, 7999 pcs/8hr (basis: 5 pcs/mould, 18s cycle) |
| Output Capacity (Solid Brick 240x115x52mm) | 5199 pcs/hour, 41599 pcs/8hr (basis: 26 pcs/mould, 18s cycle) |
| Hydraulic Pressure | (basis not stated in source — confirm block format / material / thickness) |
| Mould Change Time | (basis not stated in source — confirm block format / material / thickness) |
| Automation Level | (basis not stated in source — confirm block format / material / thickness) |
| Overall Dimensions | (basis not stated in source — confirm block format / material / thickness) |
| Net Weight | (basis not stated in source — confirm block format / material / thickness) |
| Voltage & Frequency | (basis not stated in source — confirm block format / material / thickness) |
| Standards | CE (source value — verify against manufacturer catalog) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, cement, sand, and fly ash blends for structural masonry |
| Solid brick manufacturing | Dense aggregate mixes for load-bearing walls and paving sub-base |
| Paving brick production | Interlocking and color-face formats for walkways and light-traffic areas |
| Kerb and road curb rocks | Coarse aggregate with high cement content for impact resistance |
| Sod and environmental bricks | Porous mixes with organic additives for landscaping applications |
What "18-25 Seconds Per Cycle" Leaves Out on the QT4-18
Molding cycle is only one variable in your daily throughput equation; material flow and vibration tune-up dictate the real output.
When I was supporting block plants across West Africa, I watched a machine with an 18-second nominal cycle struggle to hold even 25-second intervals because the local sand had a high clay content. The hopper bridged, the mix fed unevenly, and the operator kept pausing the QT4-18 block machine specifications cycle to clear the chute. Buyers saw a 6,400-block daily figure on paper and planned their logistics around it, only to find the forklift sat idle half the day. Honest capacity planning starts with a raw material sieve analysis and a moisture test, not a catalogue number [NEED_CITE: typical aggregate variability in sub-Saharan African block production].
Mould Selection Dictates Real-World Output
The QT4-18 block machine specifications list a pallet size of 900 x 500 mm, which means each mould must fit within that footprint. A 400 x 200 x 200 mm hollow block uses four cavities per mould, yielding 799 pieces per hour at an 18-second cycle. Switch to a 400 x 150 x 200 mm format with five cavities, and the same cycle delivers 999 pieces per hour. Buyers often fixate on the machine’s hydraulic pressure rating without asking whether the cavity count on their chosen format matches the daily volume their dispatch team needs to ship.
Matching Vibration to Your Aggregate Profile
Platform vibration at 0-60 Hz gives the QT4-18 block machine specifications a wide adjustment band. Coarse, angular crushed stone needs higher frequency to settle into the mould corners, while river sand with finer particles compacts better at mid-range settings. I have stood beside lines where the operator never touched the default frequency and wondered why edge corners kept breaking. Five minutes on the VFD dial, watching the block surface change from grainy to dense, is usually enough to find the right window [NEED_CITE: vibration frequency effects on concrete block density].
Reading the Core Parameters for Production Planning
Vibration force at 45 KN works in tandem with hydraulic demolding pressure to set block density. If your target market demands 7 MPa compressive strength for structural hollow blocks, both values must be sufficient to compact a drier mix without cracking the green block during ejection. The 900 x 500 mm pallet size also determines your curing rack spacing and the forklift tine width you already own. A mismatch here means buying new racks or stacking by hand, which quietly erases any cycle-time advantage the press itself provides.
The Hidden Cost of Skipping the Pallet Audit
Buyers sometimes treat pallets as a consumable afterthought. With a 900 x 500 mm pallet, you need curing racks cut to that exact span and a forklift that can slide tines under the pallet overhang. One plant owner in South Asia took delivery only to discover his existing bamboo racks were 850 mm wide; every pallet sagged at the edges during curing, warping the blocks underneath. The solution was a complete rack rebuild and a three-week production gap he had not budgeted for [NEED_CITE: pallet dimension compatibility with curing infrastructure].
Why Sourcing the Press and the Pallet Line Together Matters
Quoting the QT4-18 as a standalone press leaves pallet feeding, stacking, and curing rack handling to be sourced separately. When the stacker cycle is half a second slower than the press, the press waits. When the pallet feeder jams, the press stops. Specifying the entire block line from one supplier means the cycle times at every station are validated against each other before the equipment leaves the factory, so the press is never the bottleneck waiting on a mismatched upstream or downstream station.
Documentation & Verification
- Line layout drawing showing pallet flow from press to curing rack
- Capacity calculation sheet stating the exact block format assumed
- Mould drawing with cavity count for your chosen brick dimensions
- Hydraulic and electrical schematic matching your site voltage
- Factory test record run on a mix design close to your local aggregate
- Packing photographs documenting each crate before container loading
Installation, Commissioning & Support
- Foundation slab must bear the 45 KN vibration force without resonance transfer
- Dedicated three-phase circuit with voltage confirmed before PLC power-up
- Pallet feeder aligned to 900 x 500 mm pallet travel with 2 mm tolerance
- Vibration frequency dialed in on-site using your actual raw material batch
- Mould change drill practiced with your crew until swap time is repeatable
- Wear parts list supplied with first-order spares for hydraulic seals and vibrator mounts
Before You Request a Quote
Send us your target block dimensions, the daily volume your market absorbs, and a sieve analysis of the aggregate you can source locally. Tell us the voltage and frequency at your panel board and the language your operators read. With those data points we can size the QT4-18 mould set, pallet specification, and line automation level to your actual conditions rather than a default catalogue build.
Frequently Asked Questions
Q: How is capacity calculated for different block sizes on the QT4-18?
A: We multiply the number of cavities in the mould by the number of cycles you can sustain per hour, using the 18-second baseline as a starting point. The 400x200x200mm hollow block uses four cavities, so 799 pieces per hour is the reference. Your actual cycle depends on mix flow and pallet handling speed.
Q: Can the vibration force be adjusted to match my local raw material mix?
A: Yes, the platform vibration frequency is adjustable from 0-60 Hz through the VFD. During commissioning we run your actual aggregate blend and watch block surface density, then lock the setting that gives consistent compaction without corner cracking.
Q: What is the realistic mould change time for this model?
A: Mould change time depends on the clamp design and whether you have a quick-release kit installed. We recommend timing a dry-run during commissioning and stocking the correct wrench sizes at the press so your crew can swap formats within a single shift break.
Q: Does the quotation include pallet handling and stacking systems?
A: Not by default. We can quote the QT4-18 as a standalone press or as a full line with pallet feeder, automatic stacker, and curing rack handling. Specifying the line together ensures every station cycle matches the press output.
Q: How do I confirm voltage and PLC display language before shipment?
A: We ask for your site voltage, frequency, and preferred operator language during the quotation stage. Those values are written on the purchase order and confirmed again on the electrical schematic before the control panel is wired.