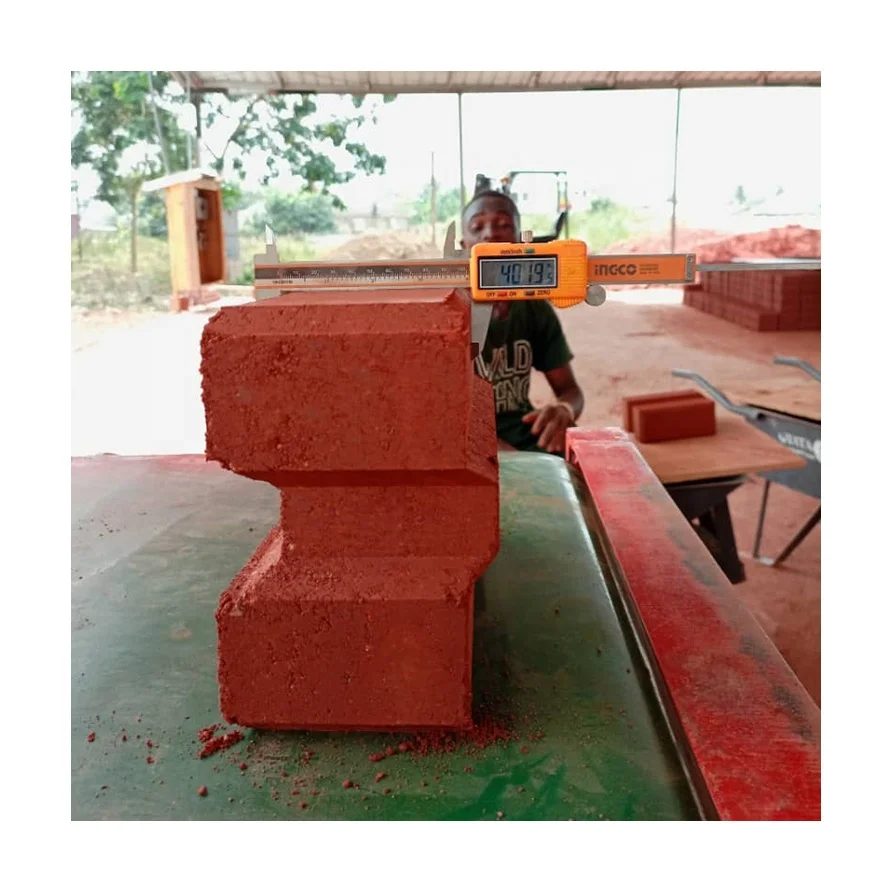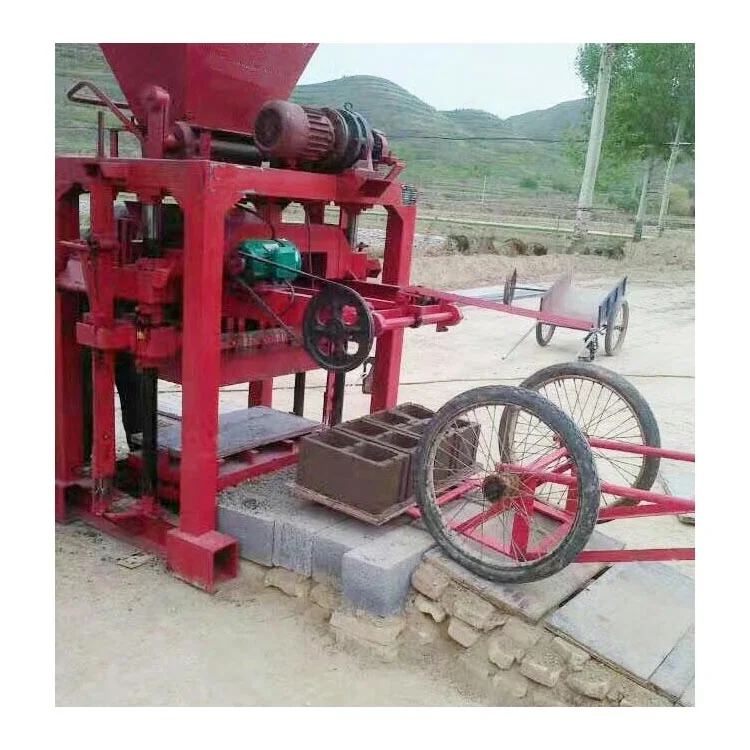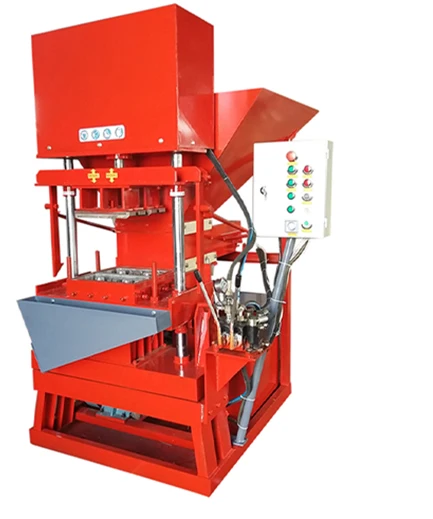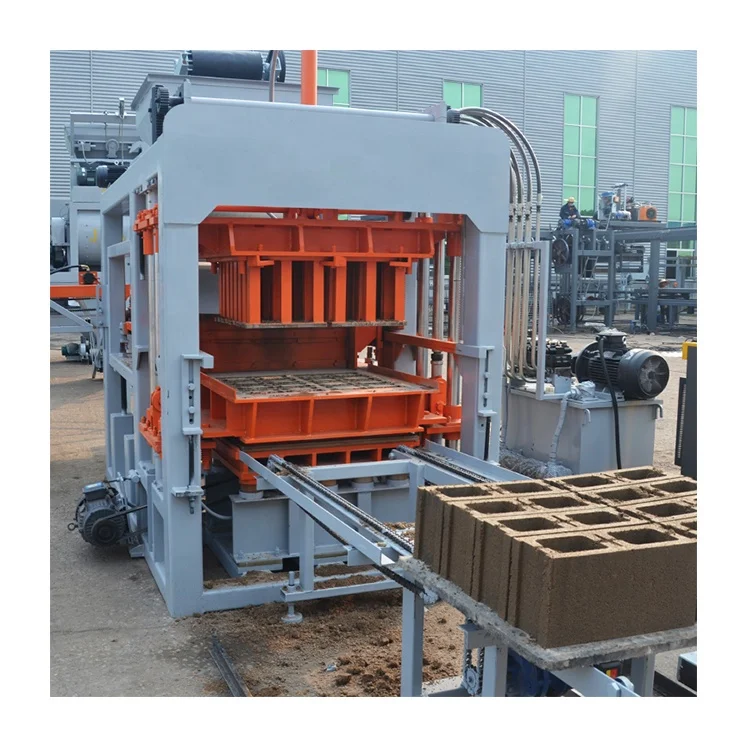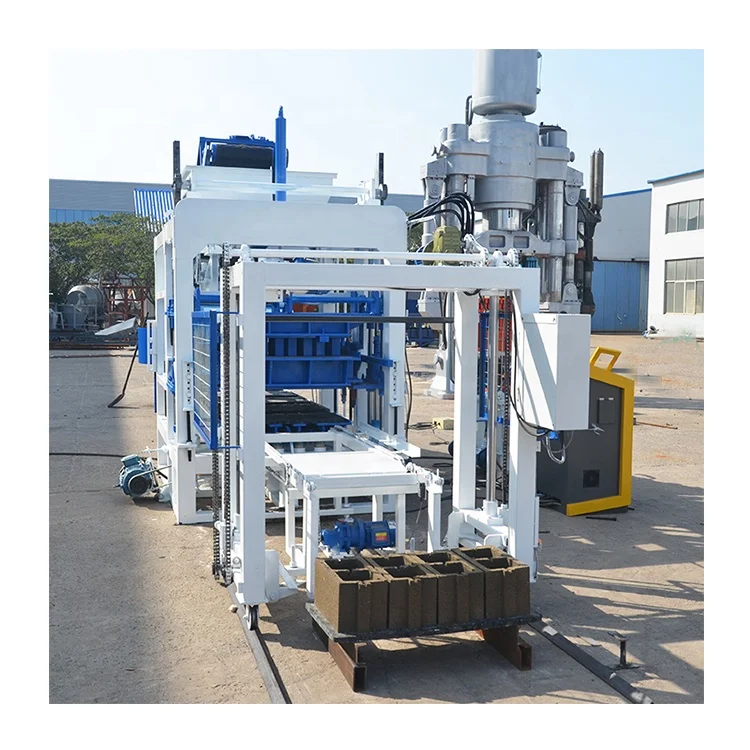
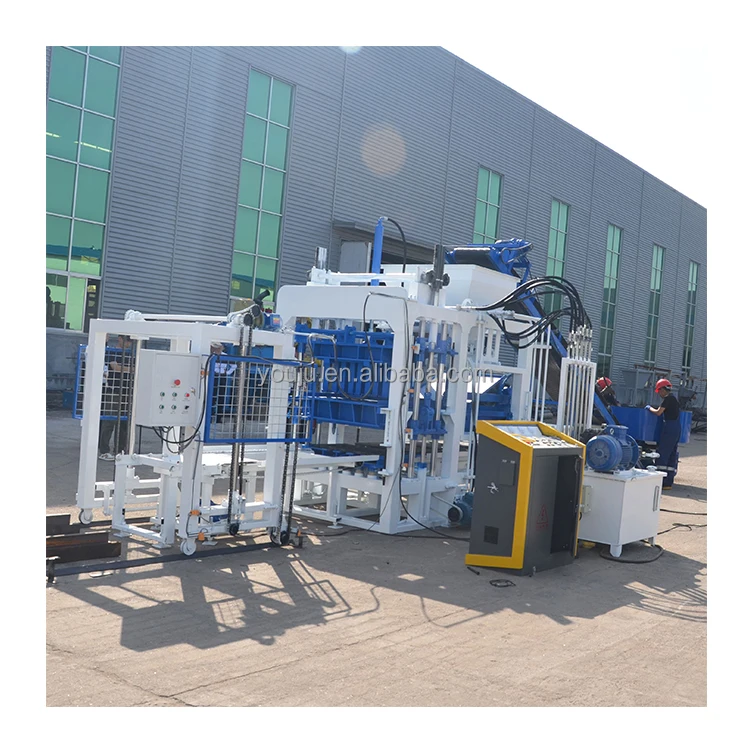
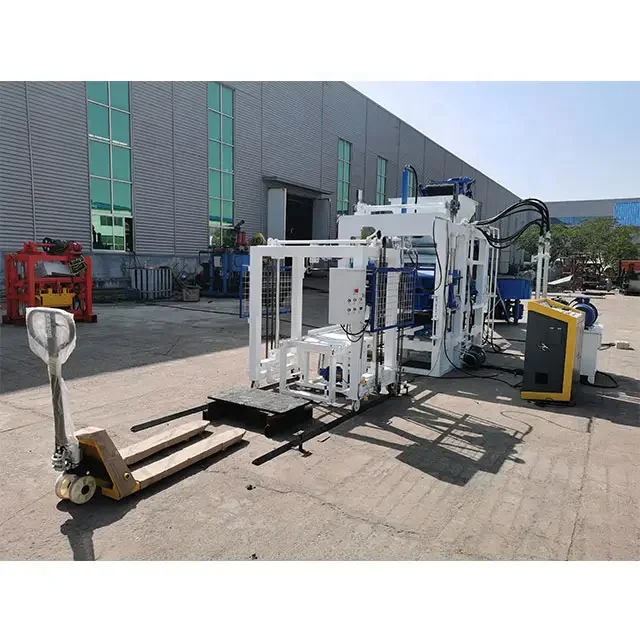
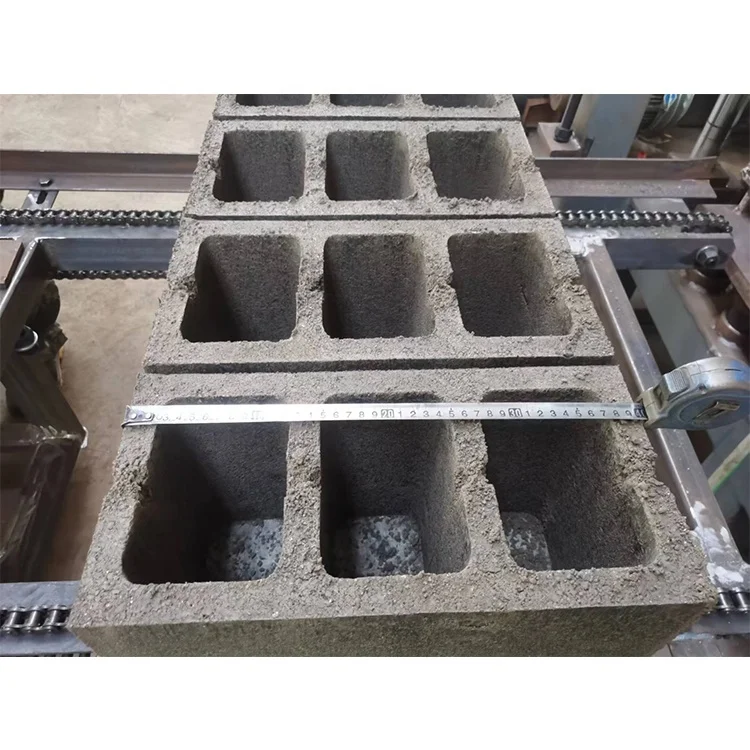
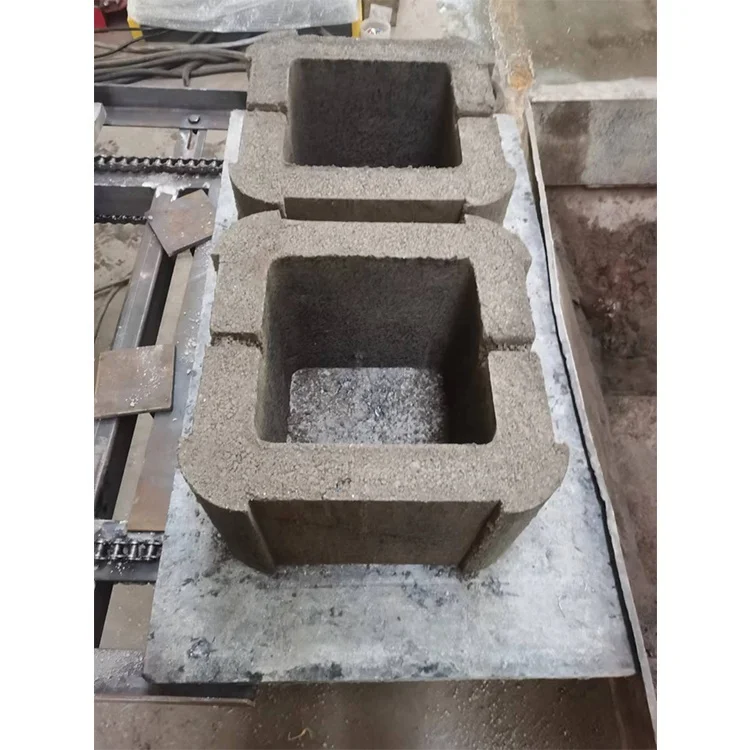
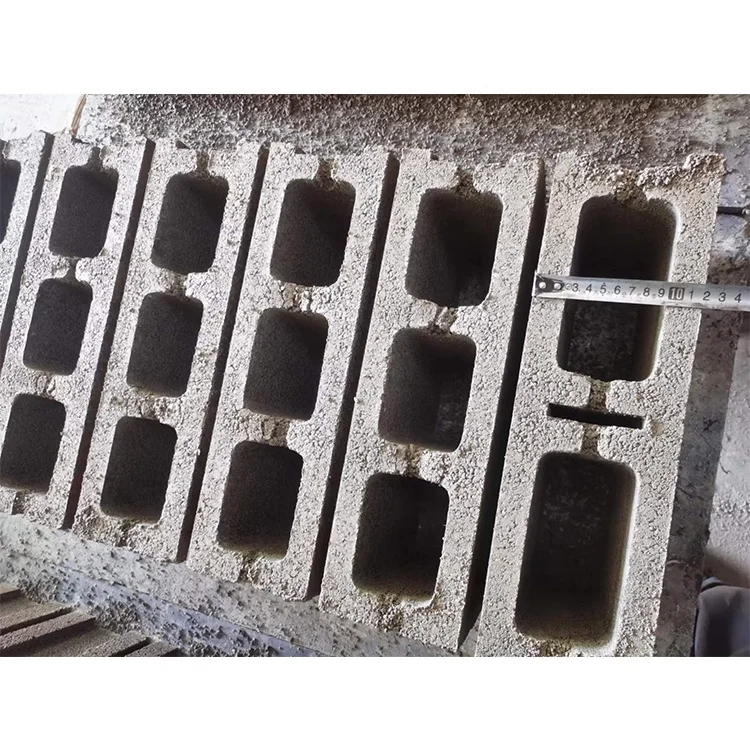
Description
Format-Matched System — QT4-16 specifications set against your actual block dimensions, local aggregate, and daily target rather than a generic catalogue sheet.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-16 |
| Product Type | Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400×1950×2800 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 40 kN |
| Pallet Size | 900×550 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format / material / thickness) |
| Total Mass | 5 T |
| Demolding Method | Hydraulic |
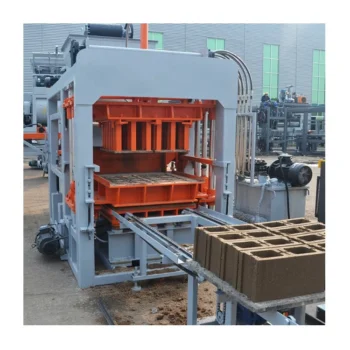
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, kerbstones, colored pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag |
| Control System | PLC with man-machine interface, fault diagnosis, remote diagnostic function |
| Automation Level | Full Automatic (conflicts with Semi automatic block category — verify with supplier) |
| Voltage & Frequency | Not stated (confirm before order) |
| Rated Power | Not stated (confirm before order) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential walls | Crushed stone, sand, cement, fly ash |
| Solid load-bearing block manufacturing | Gravel, cement, slag blends |
| Interlocking paver production for walkways and plazas | Fine aggregate, cement, pigment |
| Kerbstone and curb manufacturing | Coarse aggregate, cement, high-density mix |
| Colored concrete paver runs | Standard mix with oxide pigments |
| On-site block production for housing projects | Locally sourced aggregate and cement |
What "15–20 Second Cycle Time" Actually Means for the QT4-16 Concrete Block Making Machine
A cycle time is only meaningful when tied to a specific block format, wall thickness, and mix density.
Catalogue sheets for the QT4-16 concrete block making machine often quote a 15–20 second molding cycle without naming the block size or mix design that figure assumes. A thin-walled 400×200×200 mm hollow block may press within that window, but a dense interlocking paver or a thick kerbstone demands longer vibration and higher compaction. [NEED_CITE: cycle time variation by block format and aggregate density in hydraulic block presses]. I once spent a week in a Peruvian plant recalibrating vibration parameters because the volcanic ash aggregate the customer used was nothing like the crushed granite the factory tested with. The machine ran fine — but cycle times stretched well past the brochure figure. Sizing a QT4-16 to your output target means testing with your actual raw material before the order is finalized.
Matching Vibration and Pressure to Your Mix
The QT4-16 pairs 21 MPa hydraulic pressure with platform vibration at 2800–4500 r/min and 40 kN force. These two values must work together against your specific mix design. A high-fly-ash blend with low cement content needs different vibration amplitude and duration than a clean-crushed-stone mix. When pressure and vibration are correctly balanced, block density stays consistent across a full production shift. When they are not, you get weak blocks on one end of the pallet and over-compacted waste on the other.
Pallet Sizing and Curing Area Alignment
The 900×550 mm pallet on this QT4-16 concrete block making machine determines how many blocks you press per cycle and how your curing yard must be laid out. If your forklift is rated for a different pallet footprint, or your curing racks were built for a supplier’s previous machine, the mismatch shows up on day one. [NEED_CITE: pallet size compatibility with curing rack systems in block plants]. Confirming pallet material — hardwood, bamboo, or composite — against your climate and handling method prevents warping and replacement costs that eat into the first year of production.
Reading the Specs That Matter
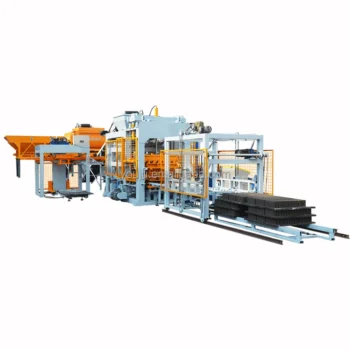
Rated pressure at 21 MPa indicates the hydraulic system can compact dense mixes needed for load-bearing blocks and pavers. Vibration frequency spanning 2800–4500 r/min gives the operator range to adjust between fine paver mixes and coarse hollow block blends. The 7400 mm machine length signals a single-station press footprint that fits within a 600 m² factory area alongside mixer and pallet return systems. PLC control with fault diagnosis and remote diagnostic capability means a technician can walk an operator through alarm codes over a video call rather than waiting for a site visit. [NEED_CITE: PLC remote diagnostic protocols in concrete block press controls]. These four parameters together define what the QT4-16 concrete block making machine can actually produce in your plant.
The Hidden Cost of Unconfirmed Specifications
Buyers who skip the configuration step often discover after delivery that the machine voltage does not match the local grid, or the PLC display language is one the operators cannot read. [NEED_CITE: commissioning delays caused by unconfirmed voltage and control language in exported machinery]. Pallets arrive in a size that does not fit the existing curing racks, forcing a yard rebuild. Moulds are supplied for a block format the local market does not buy, while the format that sells is missing from the quotation. These are not warranty issues — they are specification gaps that no amount of after-sales service can fix quickly.
Why Source This QT4-16 Concrete Block Making Machine Here
Machine, mould, pallet, and handling equipment are specified as one matched system rather than assembled from separate vendors. Configuration is set against your local aggregate test results and the block formats your market actually purchases, not a default catalogue setting. Mould design covers the exact dimensions your buyers order, including custom drawings if your market runs a non-standard kerbstone or interlocking profile. Automation level is selectable, so you can start the QT4-16 at a semi-automatic configuration and add stacking or cubing stations later. Installation support includes operator training on your mix and your mould set, not a generic start-up procedure.
Documentation & Verification
- Line layout showing capacity per block format the QT4-16 will produce
- Mould drawing and format list confirming block dimensions covered by quotation
- Pallet specification matched to your curing rack and forklift dimensions
- Hydraulic and electrical schematic for local maintenance reference
- Voltage, frequency, and PLC language written confirmation before production
- Factory test record run on block format and mix matching your order
Installation, Commissioning & Support
- Foundation plan sized for the 7400×1950 mm footprint and 5 T operating mass
- Dedicated circuit planned once voltage, frequency, and rated power are confirmed
- Machine shipped in dismantled sections for container loading and reassembly on site
- First-run commissioning uses your raw material to set vibration frequency and pressure
- Operator training covers mould change, PLC fault codes, and daily maintenance intervals
- Wear parts list and mould maintenance schedule provided at handover
What We Need to Quote Accurately
To size the QT4-16 to your actual output, send the block format and dimensions your market sells, your target daily production per format, and a sample or analysis of your local aggregate. Include your site voltage, frequency, and preferred PLC display language. If you have existing curing racks or forklifts, share their dimensions so pallet sizing is confirmed before the quotation is issued.
Frequently Asked Questions
Q: What is the realistic daily output of the QT4-16 for different block formats?
A: Daily output depends entirely on the block format, wall thickness, and aggregate density you run. A 15–20 second molding cycle is quoted without a stated format assumption, so we calculate capacity per format after reviewing your target dimensions and mix. The quotation includes a line layout showing output for each block type you plan to produce.
Q: How is the mould matched to the blocks my market actually sells?
A: We review your block format list and dimensions before quoting. Moulds are designed to those exact specifications, including custom profiles if your market requires non-standard interlocking or kerbstone shapes. The quotation includes a mould drawing and format list so you can verify every product the QT4-16 will make before production begins.
Q: How does the 900×550 mm pallet fit my existing curing area?
A: Pallet size determines your curing rack spacing and forklift handling method. We confirm pallet material — hardwood, bamboo, or composite — against your climate and yard setup. If your existing racks or forklifts do not match, we adjust the pallet specification or advise on yard modifications before the machine is built.
Q: How is the QT4-16 configured against my local raw material?
A: We request a sample or technical analysis of your aggregate, sand, and cement blend. Vibration frequency, amplitude, and hydraulic pressure are then set to match that mix design. This prevents the common problem where a machine configured for one aggregate type produces weak or inconsistent blocks with a different local source.
Q: What voltage, frequency, and PLC language options are available?
A: These are confirmed in writing before production starts. We verify your site voltage and frequency, and the PLC display language is set to your operator’s preference. This step is included in the sales process to prevent commissioning delays that occur when electrical or control specifications are assumed rather than confirmed.