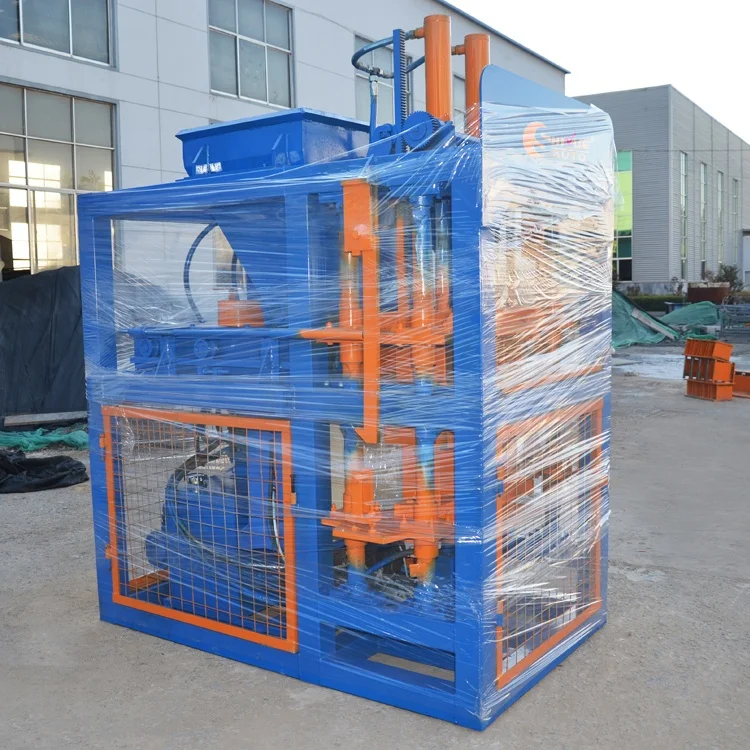
Description
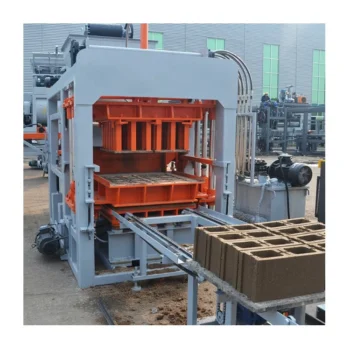
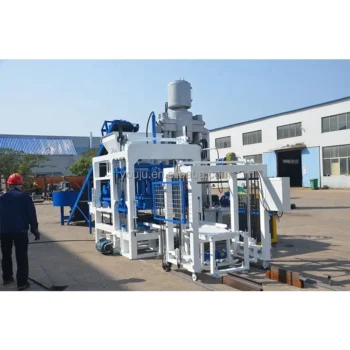
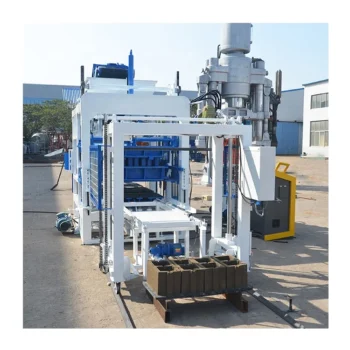
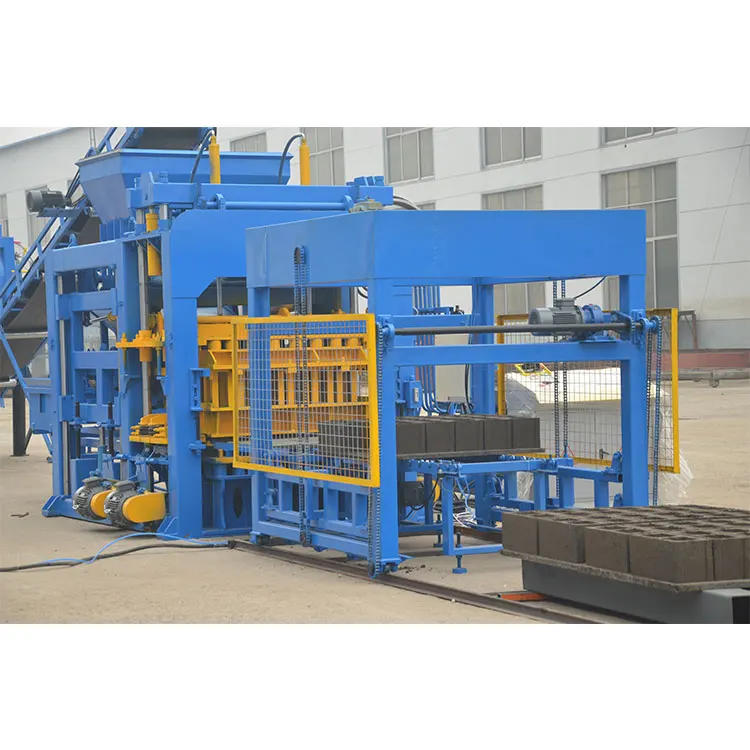
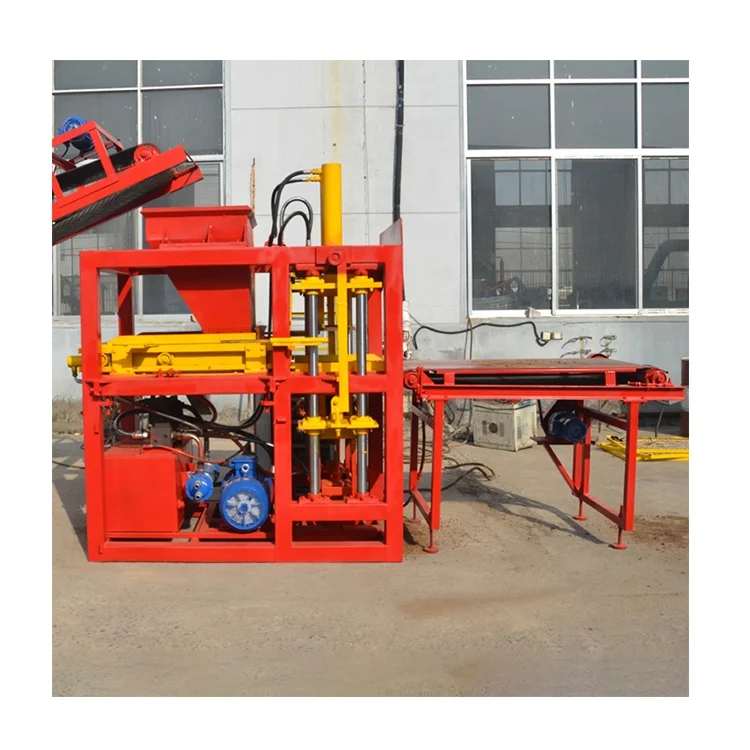
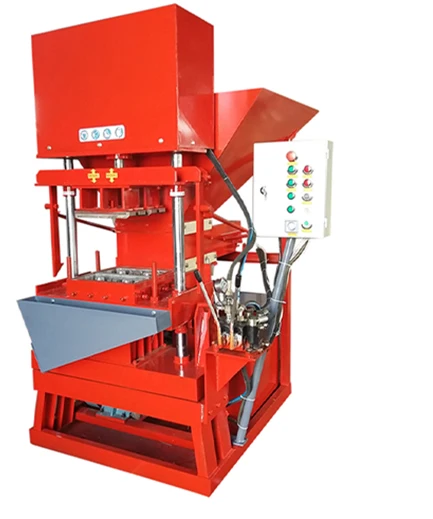
Configuration set against the buyer’s actual mix design, local aggregate and target block format — the LY4-10 interlocking clay brick making machine is evaluated per block dimension rather than a single headline capacity, ensuring your plant output matches what your market actually demands.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY4-10 |
| Product Type | Hydraulic Interlocking Clay Brick Making Machine |
| Machine Power | 11 kW |
| Hydraulic Pressure | 25-32 MPa |
| Molding Cycle | 7-10 seconds (basis not stated in source — confirm block format / material / thickness) |
| Output Capacity | Four pcs per mould cycle (basis not stated in source — confirm block format / dimensions) |
| Machine Weight | 1500 KGS |
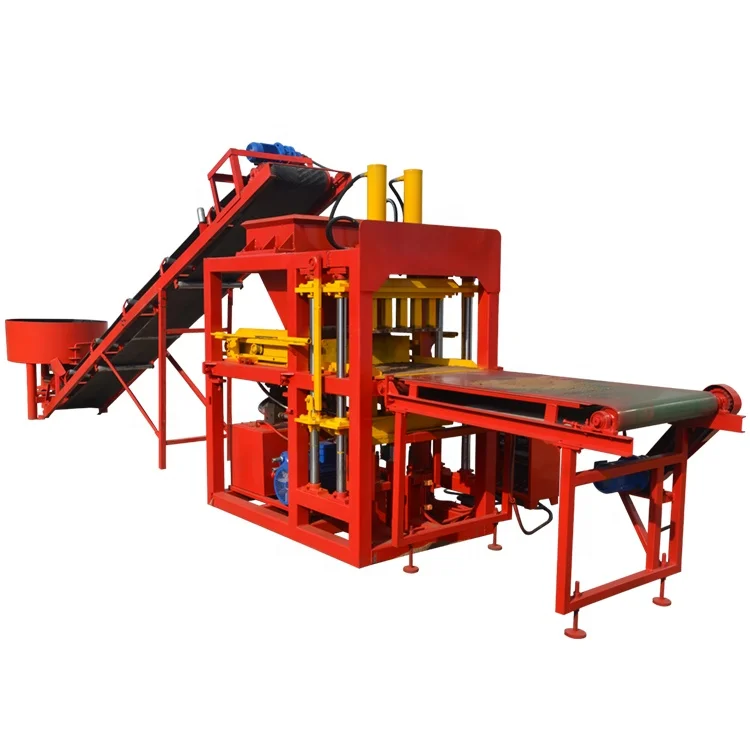
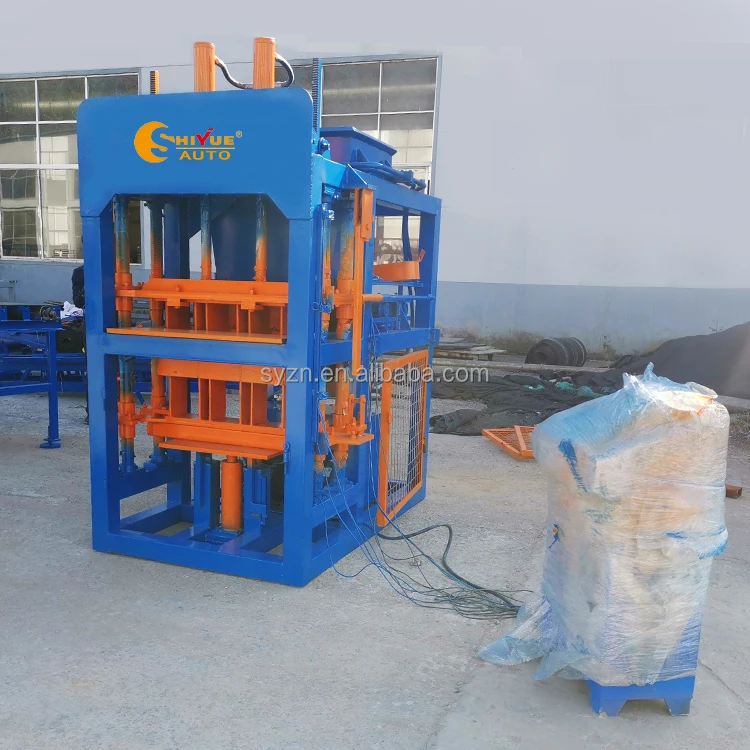
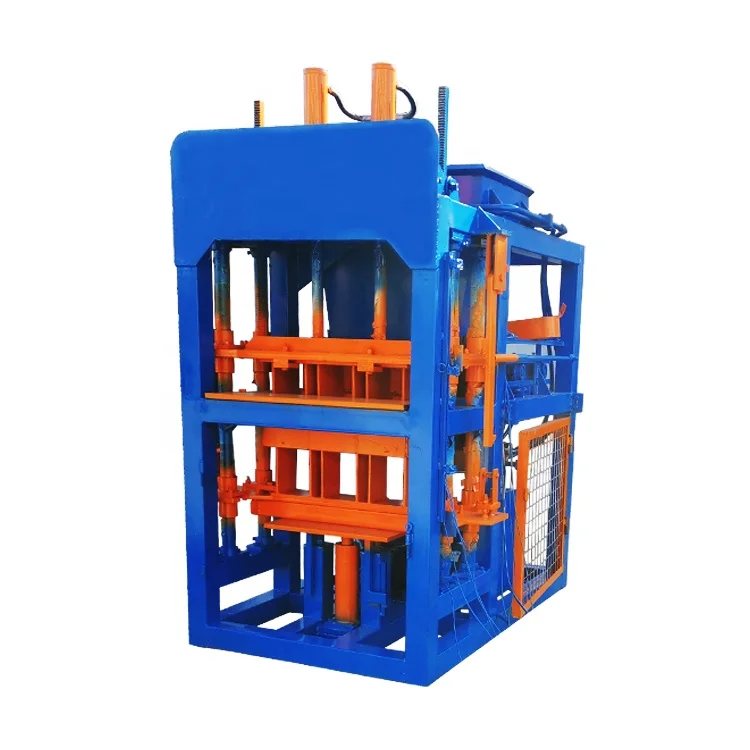
| Overall Dimensions (L×W×H) | 2260×1500×2380 mm |
| Voltage | Customized to local voltage (value not stated in source) |
| Automation Level | Automatic material feeding, mould pressing and mould lifting |
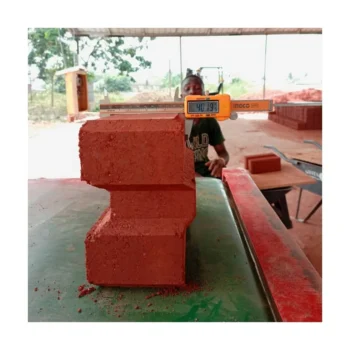
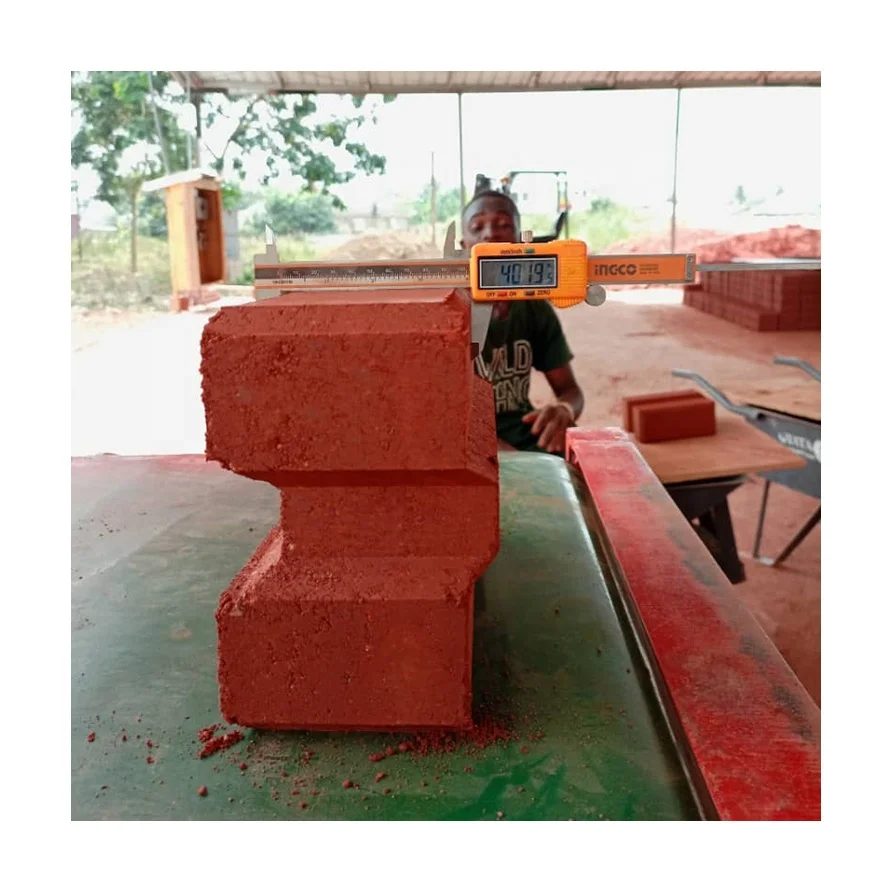
| Mould Format | Interlocking brick (specific dimensions not stated) |
| Warranty | 1 year (excluding wearing parts) |
Application Suitability
| Application | Material or Output |
|---|---|
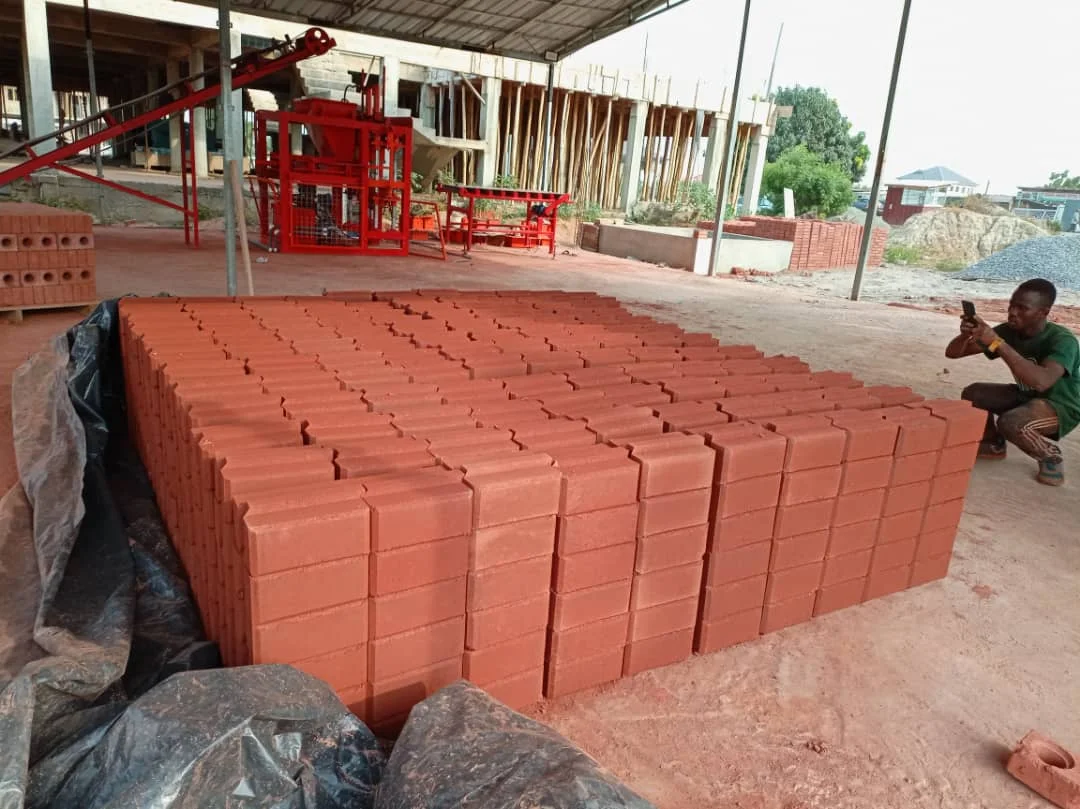
| Interlocking clay brick production | Clay-soil-cement mix designs for load-bearing and non-load-bearing walls |
| Compressed earth block (CEB) manufacturing | Stabilized earth with cement binder, utilizing local soil profiles |
| Ecological brick for construction projects | Low-cement soil blends targeting sustainable building standards |
| Cement and clay brick manufacturing | Standard sand-clay-cement ratios for general masonry units |
What "Four Pieces per Cycle" Leaves Out About LY4-10 Interlocking Clay Brick Making Machine Specifications
Capacity means nothing until you name the brick.
A headline figure of four pieces per mould cycle sounds straightforward until you realize that an interlocking block measuring 300×150×100 mm demands a different compaction time, pressure dwell, and soil-cement ratio than a thinner paver format. I once visited a site in the Levant where the contractor had selected a machine based purely on cycle count. The local red clay was highly cohesive, and the standard sand-soil trial mix used at the factory bore no resemblance to what the machine actually received on arrival. Demoulding dragged, block edges crumbled, and daily output fell well below what the buyer had used to justify the investment. That mismatch is exactly what the LY4-10 interlocking clay brick making machine specifications aim to prevent when evaluated honestly per format [NEED_CITE: soil-cement stabilization ratios by region].
Matching Pressure to Your Soil Profile
The 25-32 MPa hydraulic pressure range on the LY4-10 determines how densely the soil-cement mix is compacted before curing begins. Lower pressure suits sandy soils with higher cement content, where excessive force can actually push the binder out of the matrix. Higher pressure is necessary when clay content is significant, because cohesive soils resist compaction and need greater force to eliminate voids. Without confirming where your local aggregate sits on that spectrum, the machine may produce blocks that either fracture under their own weight or fail compressive strength testing after curing.
Cycle Time and the Workflow Around the Press
A 7-10 second moulding cycle only governs what happens between the moment the mould closes and the finished block is released. The LY4-10 interlocking clay brick making machine specifications list automatic material feeding, pressing, and lifting, which removes three operator interventions from each cycle. However, pallet placement, wet block handling off the press, and transport to the curing area remain manual tasks in a semi-automatic configuration. If those surrounding steps are not paced to match the press cycle, the machine will sit idle between strokes regardless of how fast the hydraulic ram operates [NEED_CITE: semi-automatic block plant workflow bottlenecks].
Reading the Specification Sheet Without Being Misled
Hydraulic pressure, moulding cycle, and output per cycle interact in ways that a single-number summary conceals. A shorter cycle at lower pressure may yield acceptable blocks from a sandy mix but produce under-compacted, fragile units from a clay-heavy soil. The 11 kW machine power must supply both the hydraulic pump and any vibration system simultaneously, so voltage stability at your site directly affects whether the rated pressure is achievable stroke after stroke. Pallet size — not stated in the source data — must align with both the mould footprint and the curing racks or floor space you have available, otherwise finished blocks pile up beside the press waiting for somewhere to go.
The Cost of Ignoring Format-Specific Capacity
When a machine is chosen on headline cycle speed alone, the consequences surface within the first week of production. Blocks crack during demoulding because the pressure was too low for the clay content. Operators slow the cycle manually to compensate, cutting actual daily output well below the projection used for the business plan. Mould wear accelerates when the soil mix includes abrasive aggregate that the original specification did not account for. Each of these problems traces back to a specification sheet that stated one capacity number for all formats rather than breaking output down brick by brick [NEED_CITE: compressed earth block failure modes related to mix design].
Why Sourcing This Machine Through a Format-First Approach Matters
Every LY4-10 configuration is set against the buyer’s actual block format and soil sample, not pulled from a catalogue default. Mould design covers the interlocking profiles your regional market sells, and custom mould drawings are available when standard dimensions do not match local building codes. The machine, pallet, and handling workflow are specified as one matched system so the press is never waiting on upstream or downstream steps. Voltage, frequency, and control language are confirmed before production begins, eliminating commissioning delays when the machine arrives on site. Factory testing uses your specified mix design, and the test record documents actual cycle times and block density achieved under those conditions.
Documentation & Verification
- Line layout showing LY4-10 placement with pallet flow and curing area dimensions
- Per-format capacity table stating block dimensions assumed for each output figure
- Mould drawing confirming interlocking profile dimensions and tolerances
- Factory test record documenting cycle times with the buyer’s soil-cement mix
- Voltage and control language confirmation sheet signed before production release
Installation, Commissioning & Support
- Foundation pad sized to the 2260×1500 mm footprint with anchor bolt template
- Dedicated power circuit rated for the 11 kW motor plus hydraulic pump startup surge
- Hydraulic line pressure verified on site against the 25-32 MPa operating range
- First-run cycle timing validated using local soil sample before full production begins
- Operator training on mould change procedure and semi-automatic pallet handling workflow
- Wear parts list covering hydraulic seals and mould liner replacement intervals
Before You Request a Quotation
Send your target interlocking brick dimensions, the soil-cement ratio you plan to use, and your local voltage and frequency so the LY4-10 interlocking clay brick making machine specifications can be confirmed against your actual production conditions rather than a generic baseline.
Frequently Asked Questions
Q: How is the 7-10 second cycle time verified, and which block format does it assume?
A: The stated range depends on block thickness, soil-cement ratio, and hydraulic pressure setting. Verification requires a factory test using the buyer’s specific mix and target interlocking brick dimensions, which is documented in the test record before shipment.
Q: What interlocking brick dimensions can the LY4-10 mould accommodate?
A: The machine supports interlocking profiles sized to regional building standards. Custom moulds are designed to buyer drawings when standard formats do not match local masonry requirements, with profile dimensions confirmed in the mould drawing before production.
Q: How does the 25-32 MPa hydraulic pressure affect block strength with different soil mixes?
A: Higher pressure increases compaction density in clay-heavy soils, improving compressive strength. Sandy mixes with more cement may require lower pressure to avoid extruding the binder. The correct setting is determined by testing your specific soil-cement ratio.
Q: What pallet size does the LY4-10 require, and how does it affect my curing layout?
A: Pallet dimensions must match both the mould footprint and your existing curing racks or floor space. Confirming pallet size during specification ensures compatibility with your forklift and curing area, preventing handling bottlenecks after installation.
Q: Which voltage configurations are available, and is the control language confirmed?
A: Voltage and frequency are customized to the buyer’s local power supply. Control display language is confirmed before production to ensure operators can read the interface during commissioning and daily operation without translation delays.