
Description
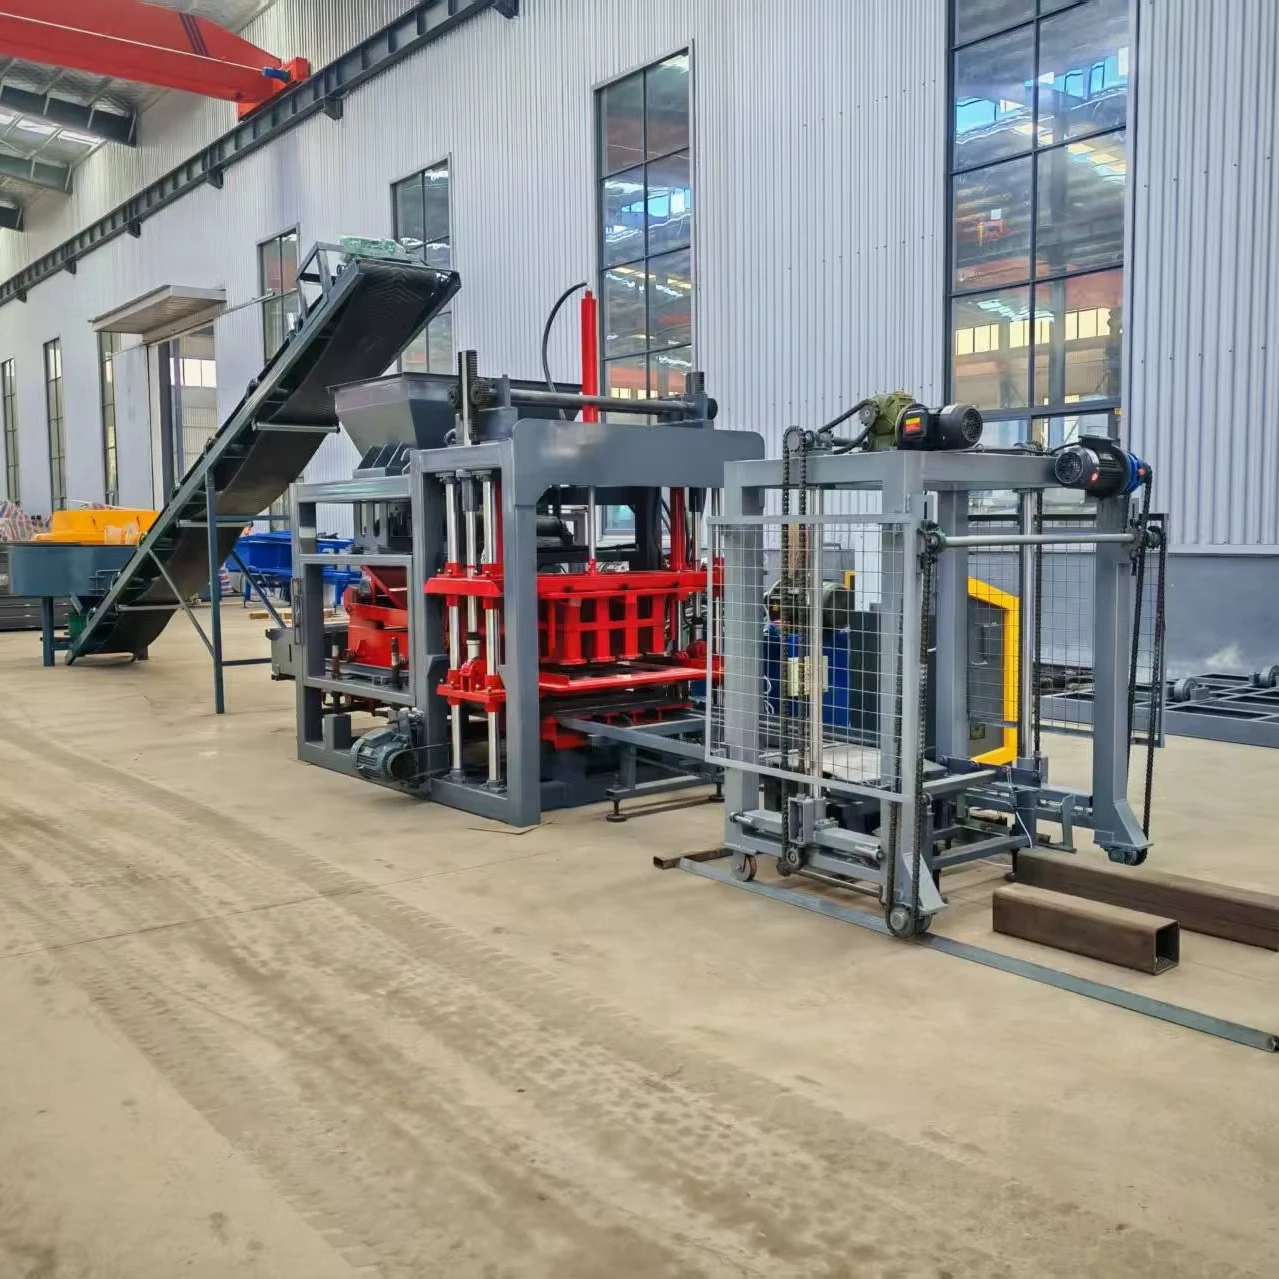
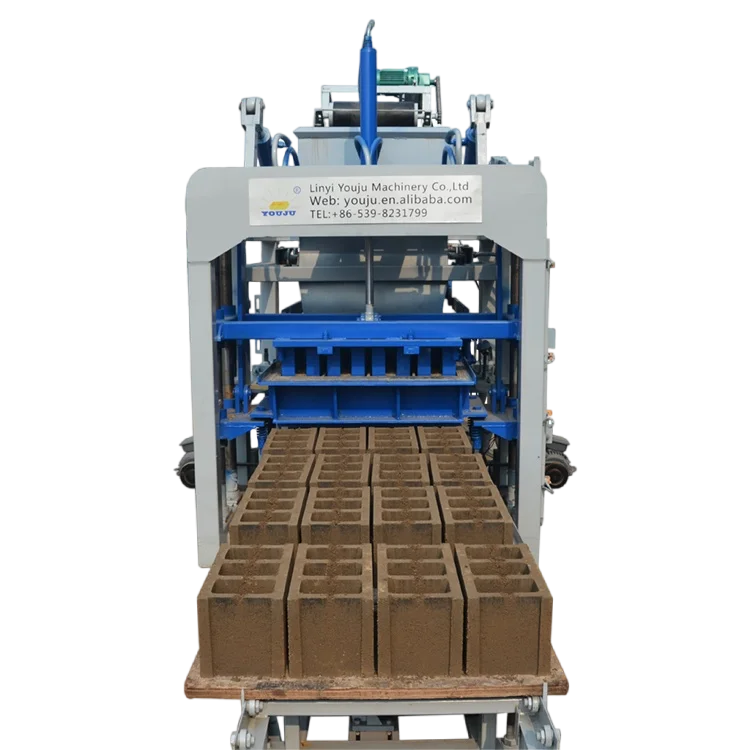
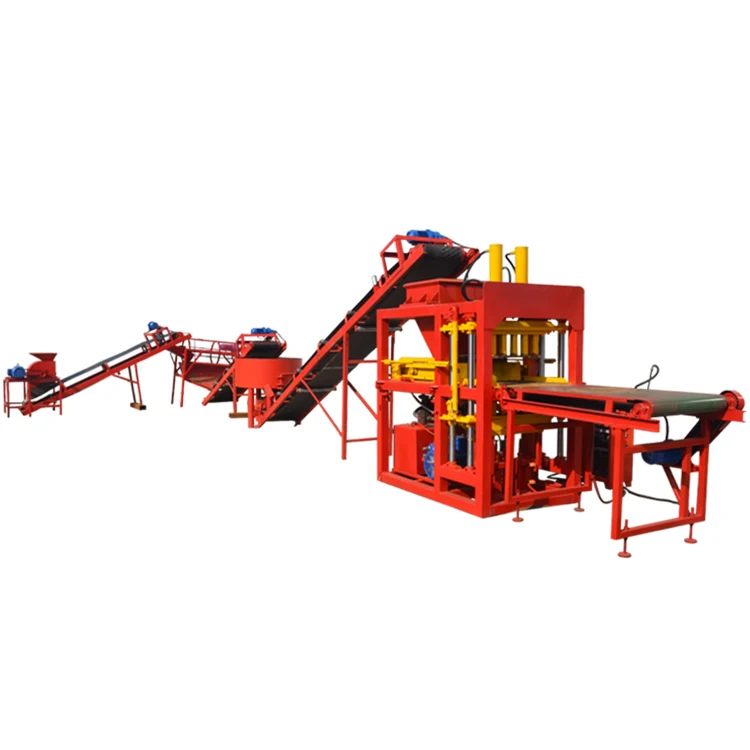
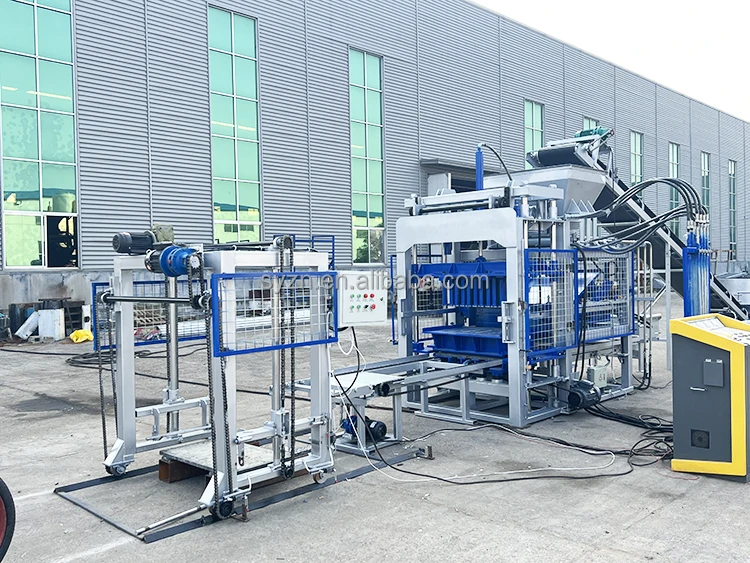
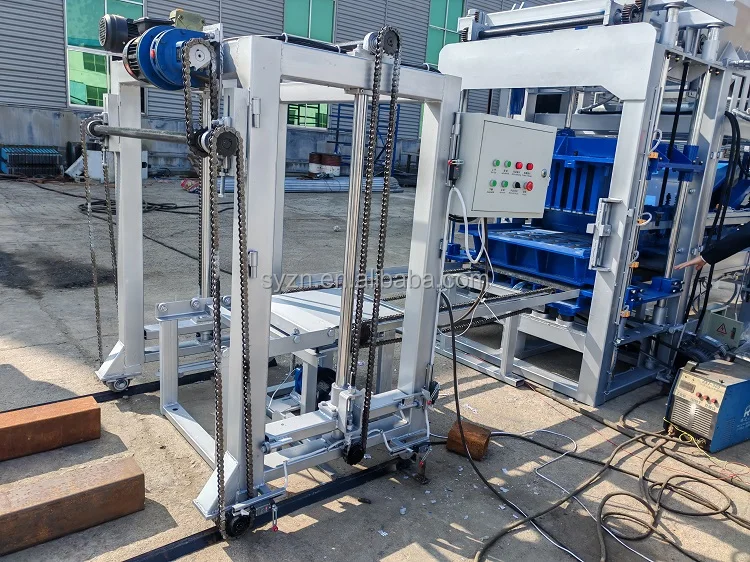
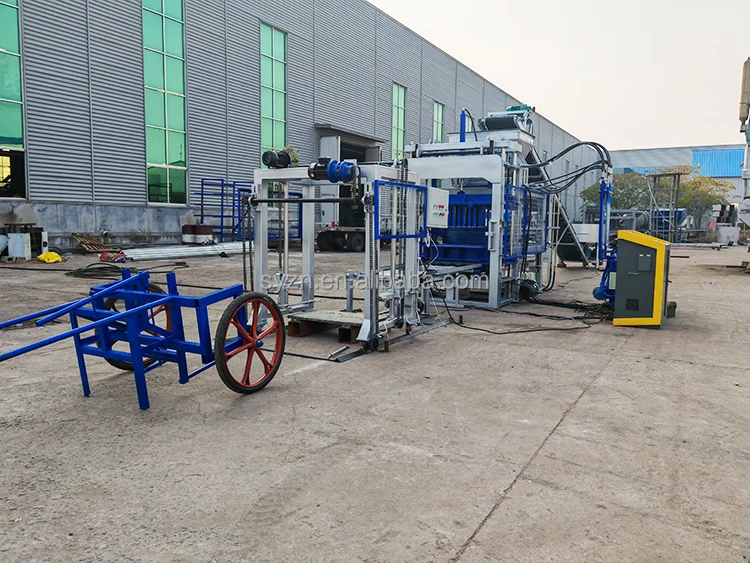
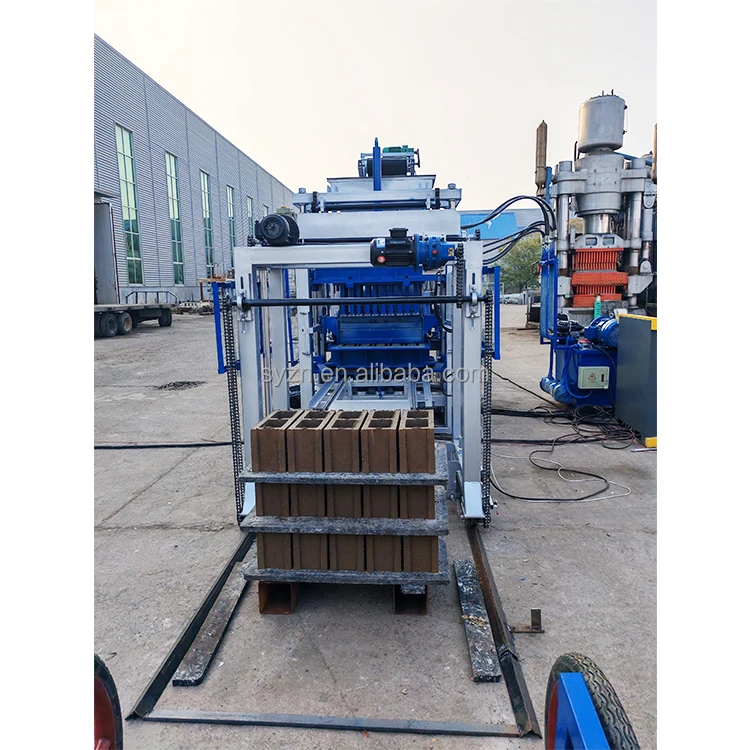
Mould-to-Pallet Matched Engineering — every cycle on the QT4-15A is calculated against the 880×550 mm pallet and the buyer’s confirmed block format, so quoted capacity survives contact with a real production floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
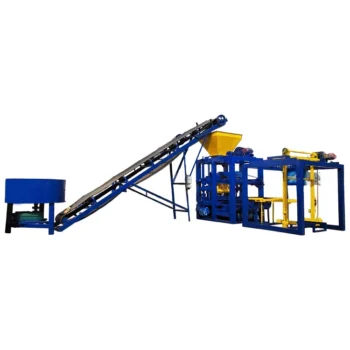
| Product Type | Fully Automatic Concrete Block Making Machine |
| Overall Dimensions | 4100×1600×2600 mm |
| Total Mass | 4 T |
| Rated Pressure | 16–21 MPa |
| Vibration Force | 55 kN |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Pallet Size | 880×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45 kW (source value — verify against manufacturer catalog) |
| Demolding Method | Hydraulic |
| Factory Area Required | 300 m² |
| Automation Level | Fully Automatic |
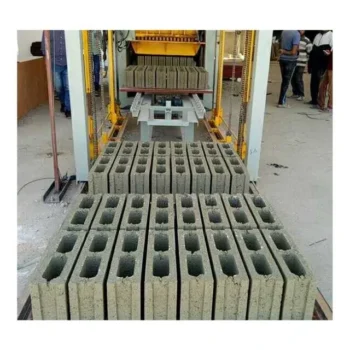
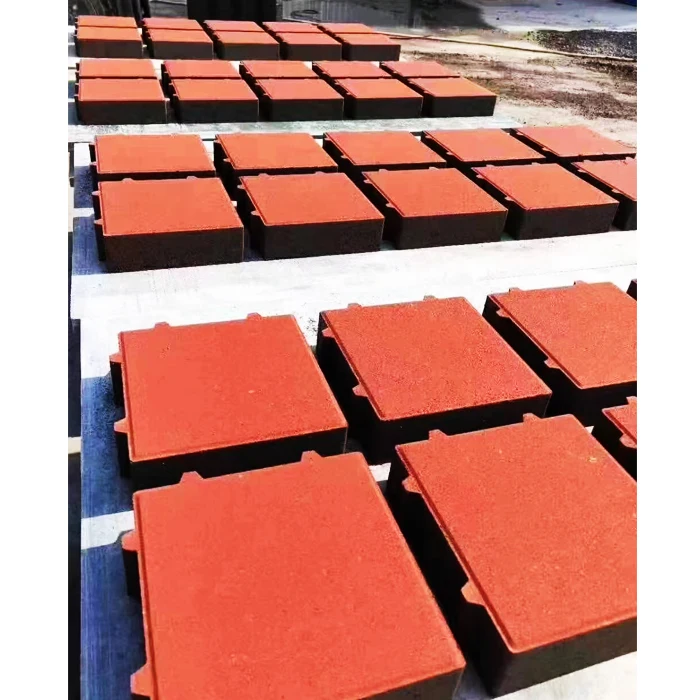
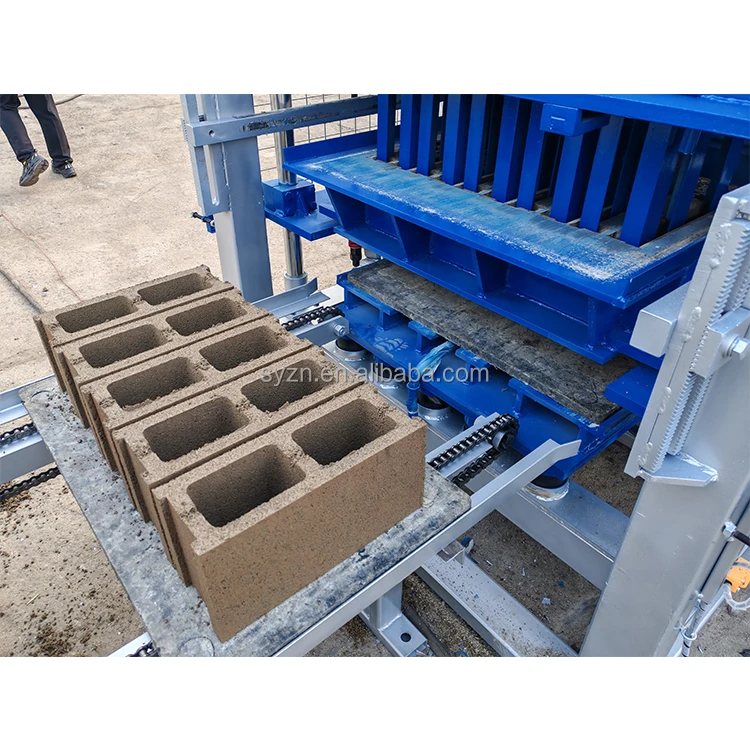
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential walling | Crushed stone, sand, cement blended with fly ash or slag |
| Solid block manufacturing for load-bearing structures | Dense aggregate mixes requiring higher hydraulic pressure |
| Interlocking paver production for driveways and walkways | Colored face mix over a standard concrete base |
| Curbstone forming for road and kerb projects | Coarse gravel and cement with extended vibration cycles |
| Porous block runs for permeable paving | Open-graded aggregate with reduced cement content |
What the "25-Second Cycle" Promise Hides About Real Output
Cycle time only means something when tied to the exact block format, material density, and pallet layout your market actually buys.
Catalogues routinely quote a single molding cycle number as if it applies across every product the machine can run. In practice, a 25-second cycle might hold for a thin paver with a simple face mix, but the same QT4-15A block machine specifications could stretch well past 30 seconds once you switch to a deep hollow block filled with a stiff crushed-basalt mix. [NEED_CITE: relationship between block geometry and compaction time in hydraulic vibration presses] Buyers who plan daily throughput on the fastest cycle figure end up with a production shortfall that only appears after the line is installed and running.
Vibration and Pressure Tuned to Your Aggregate, Not a Default Curve
The 55 kN vibration force and 16–21 MPa hydraulic pressure on the QT4-15A work together to compact the mix inside the mould cavity. When the buyer’s local aggregate is river sand, a lower pressure setting with higher vibration frequency typically produces a clean, dense block. Switch that same setting to crushed basalt or slag-heavy mixes and the block edges start crumbling before demolding.
Getting this balance right means the parameter set has to be rebuilt around a sample of the actual raw material. The QT4-15A block machine specifications provide a starting envelope, but the final pressure curve and vibration duration must be locked in during commissioning — not assumed from a factory default.
Pallet Footprint Dictates What the Rest of Your Plant Can Handle
An 880×550 mm pallet is a mid-range format that fits a wide selection of block layouts per cycle. The issue arises when the buyer’s existing curing racks, forklift tines, and stacking area were built around a different pallet dimension. Mismatched pallets mean manual rehandling between the press and the curing zone.
Before the QT4-15A ships, the pallet size must be checked against the curing yard layout and the forklift fork width on site. This is a five-minute conversation that prevents weeks of pallet re-sorting once production starts. [NEED_CITE: pallet handling standards for concrete block curing operations]
Reading the Specs Beyond the Numbers
The platform vibration at 4200 r/min sets the compaction rhythm. Higher frequency works for finer sands and paver face mixes, but coarse gravel demands longer vibration at slightly lower frequency to settle particles without segregation. The 16–21 MPa pressure range gives the operator room to adjust downward for lightweight hollow blocks and upward for high-density curbstone.
Molding cycle of 25–30 seconds is a range, not a single promise — the lower end applies to thin, simple-format blocks in free-flowing sand, while the upper end covers tall hollow blocks in stiff mixes with fly ash replacement. Total machine mass of 4 T means the foundation must absorb repeated vibration loads; a thin concrete pad will crack within months. The 18.45 kW overall power draw requires a dedicated circuit sized above the nameplate rating to handle startup inrush current without tripping.
The Cost of Skipping Format-by-Format Capacity Checks
When a buyer approves a line based on a single pieces-per-hour figure, the first format change often reveals that the cycle time for the actual best-selling block is considerably longer. The result is a plant that runs overtime shifts to fill orders that the original calculation said would fit in eight hours.
Worse, if the mould was not designed for the buyer’s pallet size, each cycle leaves unused pallet surface or overhangs that damage block edges during demolding. These losses are not dramatic — they are a steady bleed of rejected blocks, extra cement consumption, and operator frustration that erodes margin without ever showing up as a single line item. [NEED_CITE: impact of mould-to-pallet mismatch on block rejection rates]
Why Sourcing the QT4-15A Here Makes Sense
Block machinery is the single product focus, so the QT4-15A arrives with moulds, pallets, and handling equipment specified as a matched system rather than bolted together from separate vendors. Every configuration is set against the buyer’s confirmed mix design and target block format, not pulled from a default catalogue page.
Mould design covers the formats the buyer’s market actually sells, with custom drawings available when a non-standard kerbstone or interlocking profile is needed. Automation level is selectable, allowing a buyer to start with basic pallet handling and add automatic stacking later as volumes grow. Installation support includes on-site commissioning where the vibration and pressure parameters are tuned to the local aggregate before the first production run.
Documentation & Verification
- Line layout with capacity calculation tied to each confirmed block format
- Mould drawing and format list matched to the 880×550 mm pallet
- Hydraulic and electrical schematic for the buyer’s voltage and frequency
- Factory test record showing cycle time achieved with a stated mix design
- Voltage and PLC display language confirmation sheet before dispatch
- Operation and maintenance manual with wear parts and mould replacement schedule
Installation, Commissioning & Support
- Foundation plan sized for 4 T mass and repeated platform vibration loads
- Dedicated power circuit sized above 18.45 kW nameplate for inrush tolerance
- Machine shipped partially assembled to fit standard container dimensions
- On-site parameter tuning of vibration force and hydraulic pressure to local aggregate
- Operator training covering mould change procedure and daily maintenance checkpoints
- Wear parts list with hydraulic seals and vibration motor brushes identified
What We Need From You to Size This Line Correctly
Before a configuration proposal is drafted, the conversation needs to cover the specific block formats your market demands, the daily volume for each format, and the local aggregate available at your site. Voltage, frequency, and PLC display language must be confirmed early so the QT4-15A block machine specifications align with your electrical infrastructure and operator capability.
Frequently Asked Questions
Q: How is output capacity calculated, and which block format is assumed in the cycle time figure?
A: The 25–30 second molding cycle is a range that shifts depending on block format, wall thickness, and mix stiffness. A thin paver may sit at the lower end, while a deep hollow block in a fly-ash mix pushes toward 30 seconds. We calculate daily throughput per format using your confirmed product list, not a single blanket number.
Q: What mould formats fit the 880×550 mm pallet, and can custom moulds be built to buyer drawings?
A: Standard hollow blocks, solid blocks, interlocking pavers, and curbstones all fit within the 880×550 mm pallet envelope. When a buyer’s market requires a non-standard profile or a specific kerbstone dimension, custom moulds can be engineered from buyer-supplied drawings and tested at the factory before shipment.
Q: How do I confirm voltage, frequency, and PLC language match my site before shipment?
A: Voltage and frequency are confirmed during the quotation stage and locked on the order sheet. PLC display language is agreed at the same time so the control panel arrives readable for your operators. Any mismatch caught at this stage avoids commissioning delays on site.
Q: How do vibration force and hydraulic pressure need to be matched to my local aggregate?
A: The 55 kN vibration force and 16–21 MPa pressure range provide an operating envelope. Coarse crushed stone typically needs longer vibration at moderate pressure, while fine river sand compacts faster at higher pressure. Final parameters are tuned during commissioning using your actual raw material.
Q: What documentation is provided with the QT4-15A block machine specifications package?
A: The package includes a line layout with per-format capacity calculation, mould drawings matched to the pallet, hydraulic and electrical schematics, a factory test record, voltage and language confirmation, and an operation manual with a wear parts schedule.