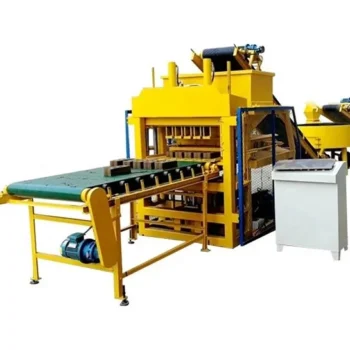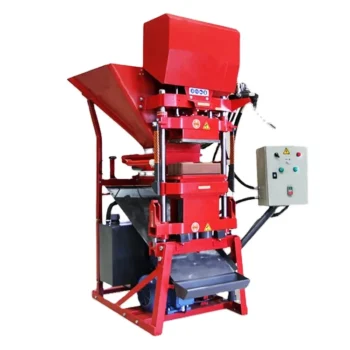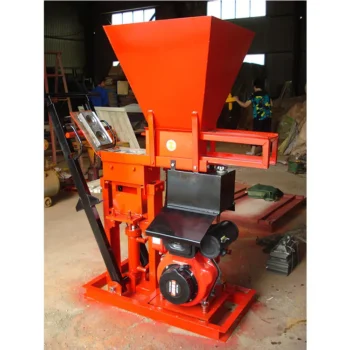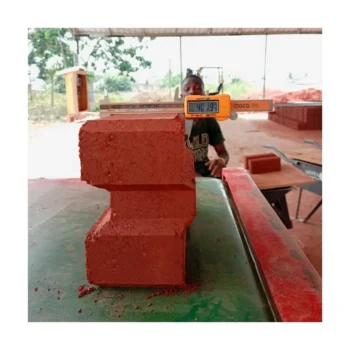
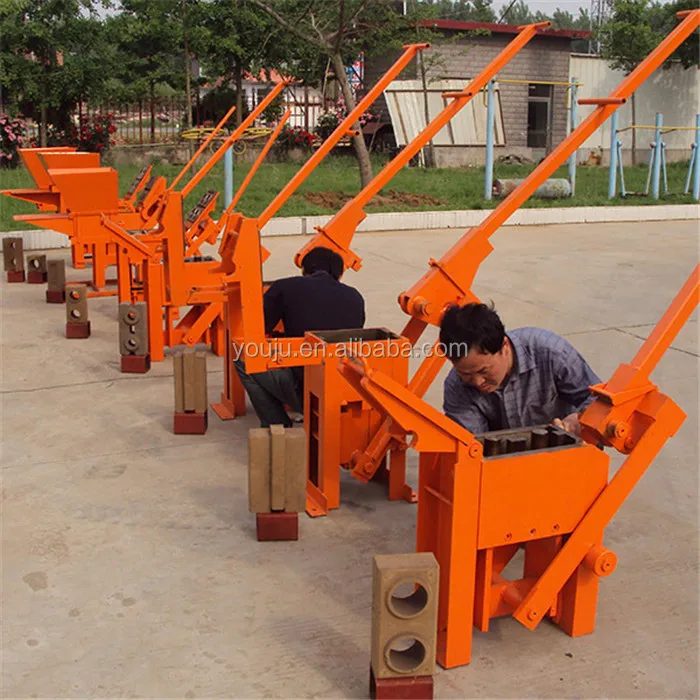
Description
Format-Matched Engineering — every LY2-40 press ships with a mould profile and soil-cement ratio verified against your local clay, not a generic catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY2-40 |
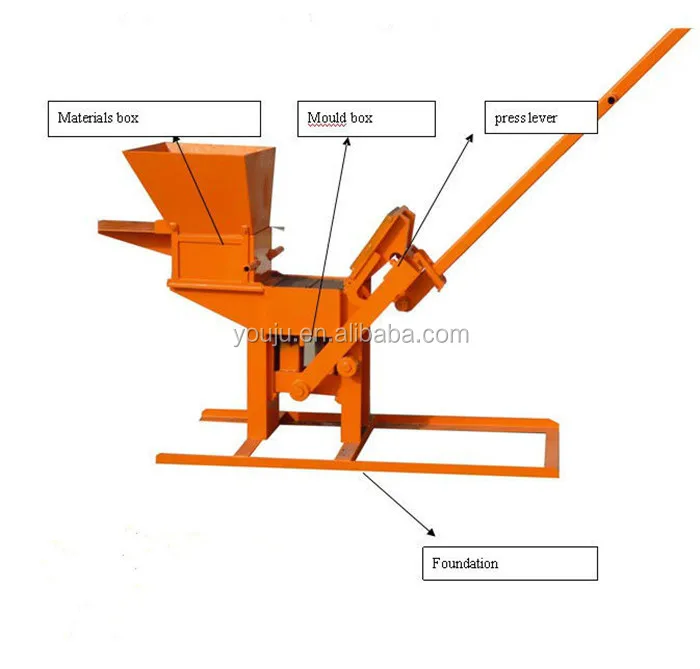
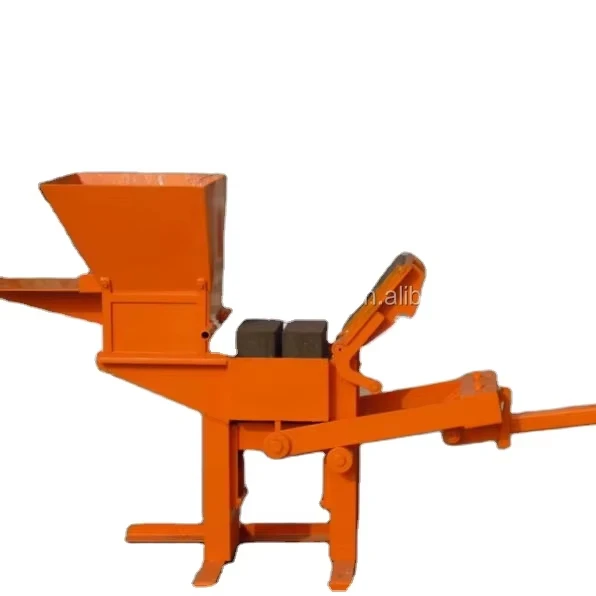
| Product Type | Manual Clay Interlocking Brick Making Machine |
| Power Source | No Power, Completely Manual |
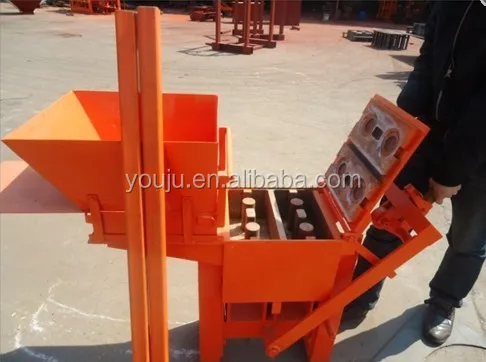
| Lifting System | Manual Lever Press |
| Mobility | Steel Wheels |
| Dimension (L × W × H) | 1600 × 700 × 1200 mm |
| Molding Cycle | 30–40 s per press |
| Capacity | 400–1000 pcs/day (basis not stated in source — confirm block format, material, thickness) |
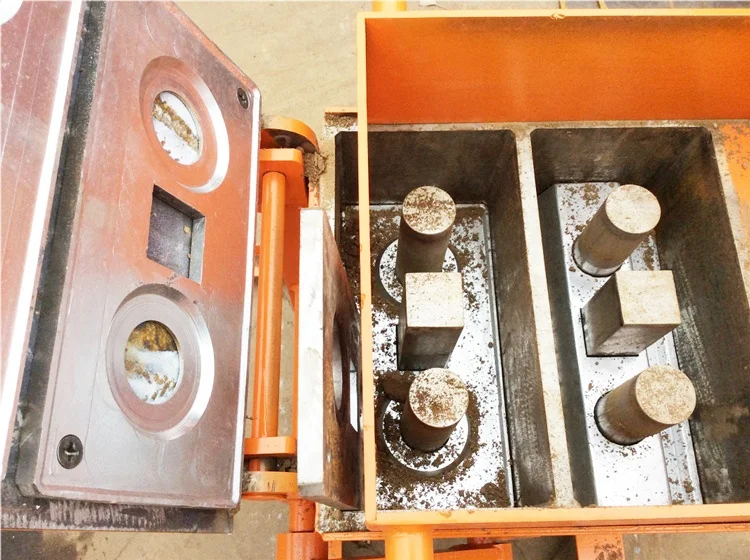
| Mould Options | Changeable Moulds for Various Interlocking Block Formats |
| Included Mixer | JFA-1 or JQ350 Mixer |
| Material Compatibility | Clay and Soil with Cement Mix |
| Warranty | 1 Year |
Application Suitability
| Application | Material or Output |
|---|---|
| Off-grid interlocking brick production | Local clay blended with Portland cement, no grid power required |
| On-site ecological brick manufacturing for housing projects | Soil-cement mix using excavated site soil |
| Small masonry suppliers adding interlocking formats | Clay-cement interlocking blocks for retaining walls and paving |
| Rural construction and development projects | Compressed earth blocks from locally sourced laterite or red clay |
What "400 to 1000 Pieces per Day" Actually Means for Your Shift
Daily output on the LY2-40 depends entirely on the interlocking brick format you press and the cycle rhythm your operators sustain, not a single brochure number.
When a manual clay interlocking brick making machine specifications sheet quotes a broad range like 400–1,000 pieces per day, buyers often plan labour and curing space around the upper figure. In practice, a 30-40 second molding cycle means a two-person team pressing a standard 250 × 125 × 100 mm interlocking block can sustain a realistic rhythm only for part of a shift before fatigue slows the lever stroke [NEED_CITE: operator fatigue impact on manual press cycle consistency]. Moisture content in the clay-cement mix also changes how quickly the compacted brick releases from the mould — a wetter mix sticks, a drier mix crumbles, and both add seconds to every cycle that never appear in the headline capacity figure.
Mould Profiles Determine Your Real Daily Count
The LY2-40 manual clay interlocking brick making machine accommodates changeable moulds for various interlocking brick formats. A larger format such as a 300 × 200 mm paving-style interlock requires a longer fill and a heavier lever stroke, pulling your daily count toward the lower end of the range. A smaller solid interlocking brick presses faster and releases more easily, pushing output upward. Matching the mould to the block your market actually buys is the first configuration decision, and it must happen before the machine leaves the factory.
Soil-Cement Homogenization Sets Block Strength
The included JFA-1 or JQ350 mixer handles the clay-cement blend that feeds the press. Uniform distribution of cement through the clay is what gives the interlocking brick its compressive strength, and a hand-loaded mixer must run long enough to eliminate dry pockets [NEED_CITE: soil-cement mixing time and compressive strength correlation]. Operators who short-cut mixing to chase cycle speed produce bricks that pass visual inspection but fail a simple drop test after curing. We specify mixer run time against your clay sample before shipment so the mixing step never becomes the hidden bottleneck.
Reading the Specs That Matter on the Shop Floor
The 30–40 second molding cycle is a function of the manual lever mechanism: the operator pulls the handle, the press plate descends under mechanical advantage, holds for compaction, and retracts. No hydraulic pump or electric motor is involved, which keeps maintenance minimal but places all consistency responsibility on the operator’s rhythm. The steel wheel mobility means the LY2-40 rolls across a prepared ground slab without a fixed foundation, letting you move the press closer to stockpiles as the clay source shifts across a large site. Total machine mass sits in the 200–240 kg range, heavy enough to resist shifting during the lever stroke but light enough for two workers to reposition on wheels. The changeable mould system uses a bolt-on retention frame; swapping formats requires unbolting the current mould, cleaning the cavity, and bolting in the next profile — a task that takes a portion of a shift if no dedicated tools are staged nearby.
The Cost of Skipping Mix and Format Verification
Buyers who order a manual press without submitting a local clay sample often discover on arrival that their soil requires a higher cement percentage than the default recommendation, driving up material cost per brick beyond what the project budget allows [NEED_CITE: clay mineralogy effect on cement stabilization ratio]. Others find that the mould shipped produces a format their local market does not buy, forcing a custom mould order and weeks of idle capacity. When pallet size and curing area are not confirmed before dispatch, freshly pressed bricks end up stacked directly on uneven ground, warping before the cement hydrates fully.
Why Sourcing This Press Through a Format-First Process Matters
Block machinery is our single focus, so the LY2-40 is specified as a matched system — press, mould, mixer, and pallet handling reviewed together rather than assembled from separate suppliers. We set the configuration against your actual clay sample and target interlocking format, not a catalogue default. Mould design covers the profiles your market sells, and custom drawings are accepted when a standard profile does not match. The automation level is selectable, so a buyer starting with the manual LY2-40 can move to a semi-automatic press later without scrapping the mixer and material handling already on site. Installation support includes operator training on cycle rhythm and mix consistency, reducing the trial-and-error period that typically consumes the first production weeks.
Documentation & Verification
- Capacity calculation stating the exact interlocking format and soil-cement ratio assumed
- Mould drawing and format list confirming included profiles and custom options
- Factory test record with photographs taken on your specified clay mix
- Mixer specification sheet matching the JFA-1 or JQ350 unit shipped
- Operation and maintenance manual covering lever mechanism and mould change procedure
Installation, Commissioning & Support
- Ground slab must be level and cured to support the 200–240 kg mass during lever stroke
- No electrical connection required for the press; mixer needs local voltage confirmation before dispatch
- Machine arrives assembled on steel wheels; roll to position and chock before first press
- First-day commissioning includes test pressing with your local clay to verify mould release
- Operator training covers lever rhythm, mix loading sequence, and mould swap procedure
- Wear parts list identifies lever pivot bushings and mould liner plates for first reorder
What We Need to Size Your Configuration
Send us the interlocking brick format your market buys, including length, width, and height, along with a photo or lab report of the local clay you plan to use. Tell us the daily output you need to sustain and the curing space available on your site. If grid power exists at your location for the mixer, confirm the voltage and frequency so the JFA-1 or JQ350 ships with the correct motor winding.
Frequently Asked Questions
Q: How is the 400–1,000 pieces per day capacity range calculated, and which interlocking block format is assumed at each end?
A: The range reflects different interlocking block sizes and operator shift lengths. A smaller solid interlocking format pressed at a sustained 30-second cycle pushes output toward the upper figure, while a larger 300 mm paving-style block at a 40-second cycle sits near the lower end. We issue a capacity calculation document naming the exact format and mix ratio before order confirmation.
Q: What clay-to-cement ratio and moisture content does the LY2-40 require for adequate block strength?
A: Typical soil-cement stabilisation runs between six and twelve percent cement by dry soil weight, depending on clay mineralogy. Moisture content at pressing should be near the optimum value determined by a simple Proctor-style test on your sample. We recommend a ratio after reviewing your local clay report and target compressive strength.
Q: How long does a mould change take, and are custom interlocking profiles available to buyer drawings?
A: Swapping a standard bolt-on mould takes a portion of a working shift when the correct tools are staged. Custom interlocking profiles are manufactured to buyer-supplied drawings, and we confirm cavity dimensions and release taper before machining begins. Mould lead time depends on profile complexity.
Q: What pallet size and curing area footprint are needed to sustain the stated daily output?
A: Pallet dimensions must match the mould cavity plus handling clearance. For sustained daily output, the curing area should hold at least two days of production to allow cement hydration before stacking. We confirm pallet size against your existing forklift and curing rack layout before shipment.
Q: Can the machine be upgraded later to a semi-automatic press if production volume increases?
A: The mixer and material handling equipment supplied with the LY2-40 remain compatible with our semi-automatic presses, so an upgrade replaces the manual press unit without scrapping the rest of the line. Pallet systems and curing racks can also be carried forward.