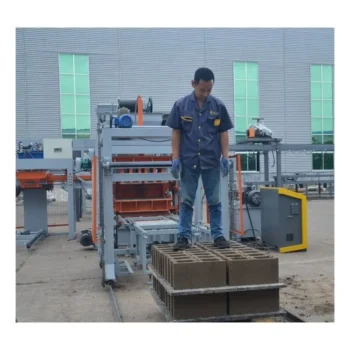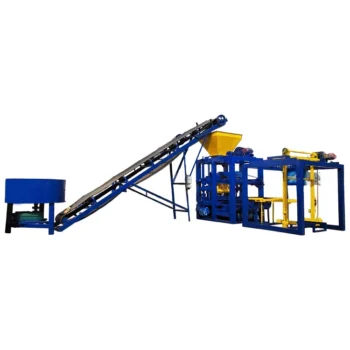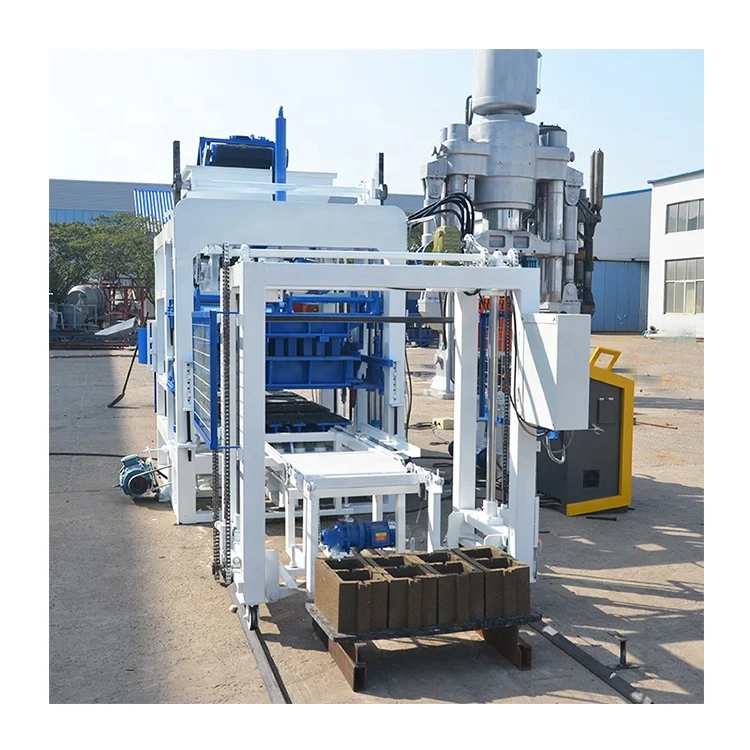
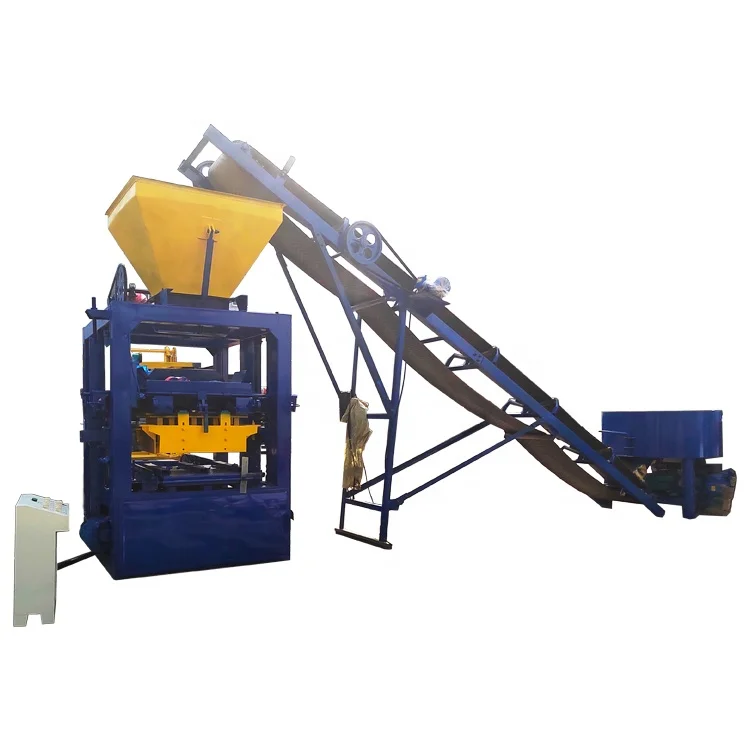

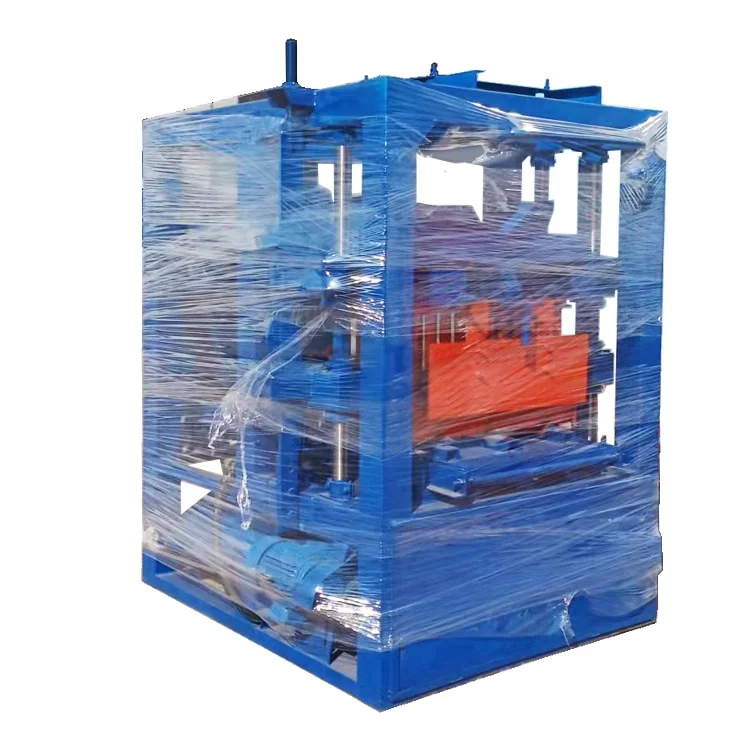

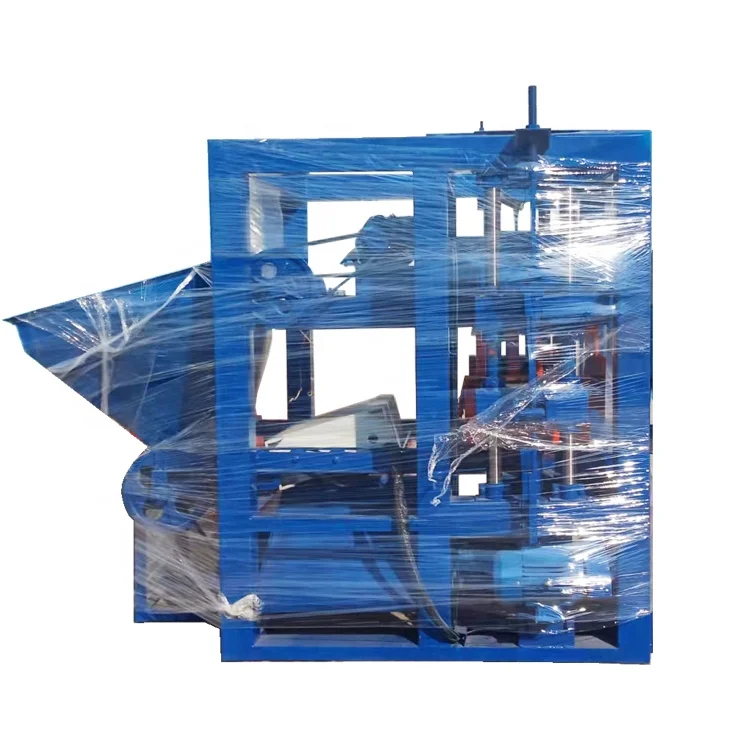
Description
Format-Matched Capacity Sizing — the QTJ4-24 concrete block making machine is configured against your actual block format, local aggregate source, and daily volume target rather than quoted as a generic cycles-per-hour figure detached from real production conditions.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
| Product Type | Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 2060×1700×2650 mm |
| Rated Exiting Force | 35.5 kN |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Pallet Size | 900×450 mm |
| Molding Cycle | 24 s per press cycle (basis not stated in source — confirm block format, material, and thickness) |
| Overall Power | 11.95 kW |
| Total Mass | 2000 kg |
| Demolding Method | Vibration |
| Factory Area Required | 260 m² |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag |
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstones, colored pavers |
| Voltage & Frequency | Configurable — confirm before production |
| Control System | Confirm PLC / relay / manual before shipment |
| Hydraulic Pressure | Confirm MPa rating before production |
| Automation Level | Semi-automatic (inferred from model tier — verify against manufacturer catalog) |
| Stacking Method | Manual (confirm pallet handling arrangement) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential wall construction | Crushed stone, sand, cement mixtures |
| Solid block manufacturing for load-bearing structures | Gravel, cement, fly ash blends |
| Paving block production for driveways and walkways | Fine aggregate, cement, pigment for colored pavers |
| Interlocking block production for retaining walls | Crushed stone, sand, cement at higher compaction |
| Curbstone manufacturing for road and landscaping projects | Coarse aggregate, cement with extended vibration cycles |
| On-site block production for housing development contractors | Locally sourced sand, gravel, and cement |
What "24 Seconds per Cycle" Actually Means for Your Daily Output
The QTJ4-24 concrete block making machine specifications list a 24-second molding cycle, but that number only matters once you tie it to the specific block format you intend to produce.
Too many quotations quote a cycle time without naming the block it was measured on. A 24-second cycle producing a standard 400×200×200 mm hollow block yields a very different daily figure than the same cycle producing a 60 mm thick paving block with a face-mix layer. I once reviewed a quote where the supplier promised a buyer thousands of blocks per shift, but the cycle time they cited was based on a thin paver the buyer never planned to sell [NEED_CITE: capacity calculation standards for concrete block machines]. The real output on the buyer’s actual hollow block format was less than half. That mismatch is the single most common reason block plant investors miss their revenue projections in the first year.
Matching Vibration Force to Your Local Aggregate
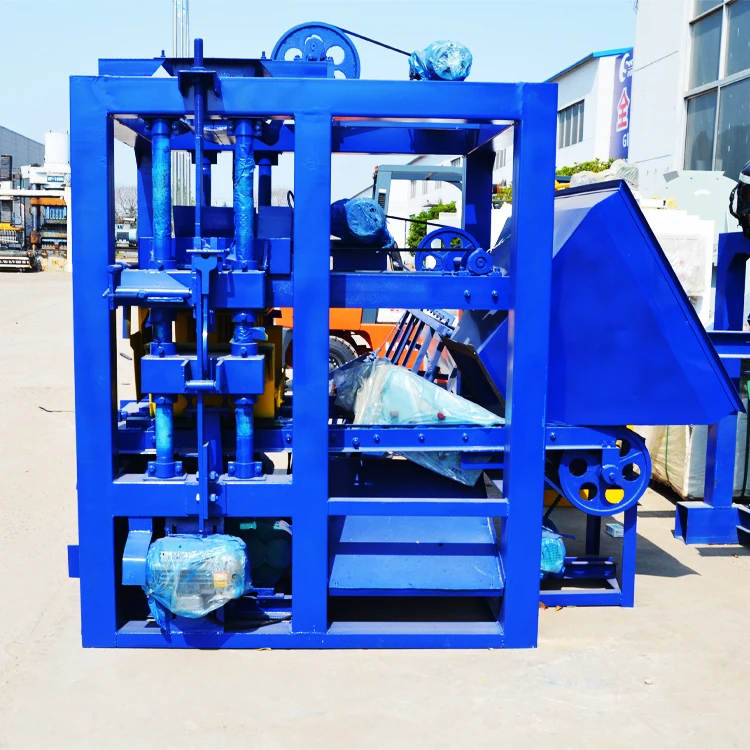
Platform vibration at 4200 r/min with a rated exiting force of 35.5 kN sits in a range that works well for medium-density mixes using standard crushed stone and river sand. The QTJ4-24 concrete block making machine delivers this force through the platform rather than the mould box, which means the energy transfers upward through the pallet into the mix column. When your local aggregate is angular crushed stone with good particle interlock, this vibration profile compacts effectively. But if your sand source carries high clay content or your fly ash has elevated carbon residue, the same force can leave blocks under-consolidated at the core. We always ask for a sieve analysis and aggregate photos before confirming the vibration settings on this model.
Pallet Size and What It Dictates Beyond the Press
The 900×450 mm pallet size is not just a press parameter — it governs your curing rack dimensions, the aisle width in your drying yard, and the fork tine spacing on the forklift that moves wet blocks to the curing area. A buyer in Southeast Asia once ordered a machine with a pallet size that did not match his existing bamboo curing racks, forcing him to rebuild the entire curing infrastructure before the machine even arrived [NEED_CITE: pallet handling compatibility in block plant layout]. The QTJ4-24 uses this pallet format across all its mould configurations, so confirming material — timber, composite, or steel — and verifying that your handling equipment aligns with it should happen during the quotation stage, not after the container is loaded.
Reading the Core Specifications for Production Impact
The 35.5 kN exiting force combined with platform vibration determines the maximum compaction density the press can achieve. For hollow blocks, this force level produces wall densities suitable for non-load-bearing and lightly loaded structural applications, provided the mix design is proportioned correctly. The 11.95 kW overall power draw matters when you are sizing a generator for a site without stable grid supply — undersizing the generator causes voltage sag during the vibration motor startup, which directly weakens block strength in the first seconds of compaction. The 2000 kg total mass keeps the machine within the range where standard container loading is straightforward, and the 2060×1700×2650 mm footprint fits within the stated 260 m² factory area allocation including space for pallet circulation and raw material staging. Voltage and frequency remain configurable and must be confirmed against your local supply before the QTJ4-24 concrete block making machine enters production.
The Cost of Skipping Format-Specific Capacity Confirmation
When buyers accept a quotation that lists only a blanket daily output figure, they inherit every assumption the supplier embedded in that number — assumptions about shift length, mould change frequency, pallet turnaround speed, and mix consistency. A buyer who planned to run three block formats across a single shift discovers that manual mould changes on a semi-automatic platform consume time that was never accounted for in the capacity quote [NEED_CITE: mould change time impact on shift output]. The result is not a machine failure; it is a planning failure that surfaces only after the buyer has committed to delivery schedules with construction contractors. The QTJ4-24 does not eliminate this risk — it demands that the capacity conversation happen format by format before the order is placed.
Why Sourcing This Model Through a Format-Focused Supplier Matters
Block machinery is the only product category we configure, which means the machine, mould, pallet, and handling equipment are specified as one matched system rather than assembled from separate vendors. Every QTJ4-24 configuration is set against the buyer’s actual mix design and target block format, not pulled from a catalogue default. Mould design covers the specific formats the buyer’s market demands, including custom drawings when standard options do not match local building codes. The automation level on this semi-automatic platform allows a buyer to start with manual pallet handling and upgrade stacking and feeding later without replacing the press. Installation support includes operator training on mould change procedures, vibration tuning for the local aggregate, and daily maintenance routines specific to this model’s drive and hydraulic layout.
Documentation & Verification
- Line layout drawing with capacity calculated per block format for the QTJ4-24
- Machine specification sheet confirming voltage, frequency, and control language before production
- Mould drawing and format list covering every block type in your market range
- Pallet specification matching size and material to your curing racks and forklift
- Factory test record run on your target block format before dispatch
- Operation and maintenance manual with wear parts list for the platform vibration system
Installation, Commissioning & Support
- Foundation pad sized to the 2060×1700 mm footprint with vibration isolation mounts
- Dedicated electrical circuit rated for the 11.95 kW overall power draw with correct voltage and frequency
- Machine shipped partially assembled with platform and vibration motor pre-mounted
- First-run commissioning includes vibration frequency tuning against your local aggregate sample
- Operator training covers mould change sequence, pallet loading rhythm, and daily greasing points
- Wear parts list provided with recommended reorder intervals for vibration springs and pallet guide rails
What We Need to Configure Your Machine Correctly
Send us the block formats your market actually buys, including dimensions and wall thickness requirements. Tell us what aggregate you can source locally — sand type, maximum stone size, and whether fly ash or slag is available. Share your site voltage and frequency, the control language your operators read, and the pallet material and curing rack layout you already have in place or plan to build.
Frequently Asked Questions
Q: How is daily output calculated for each block format on the QTJ4-24?
A: Daily output depends on the specific block format, its molding cycle, shift length, and pallet turnaround time. The 24-second cycle listed in the QTJ4-24 concrete block making machine specifications is a per-press-cycle figure, and the actual block format determines how many pieces each cycle produces. We provide a capacity calculation document that states the output for each format you plan to run.
Q: Which mould formats are available and how long does a change take?
A: Standard mould options cover hollow blocks, solid blocks, pavers, interlocking blocks, and curbstones, all matched to the 900×450 mm pallet. Custom moulds can be designed from buyer drawings. Mould change time on this semi-automatic platform depends on the format size and operator familiarity — we cover the change procedure during commissioning training so your crew can manage it within a shift.
Q: How do I confirm voltage, frequency, and control language before production?
A: These parameters are confirmed during the quotation stage before the QTJ4-24 concrete block making machine enters production. We document your site voltage, frequency, and the PLC or relay display language in the specification sheet so the electrical panel and operator interface match your local requirements upon arrival.
Q: What pallet size does the QTJ4-24 use and will it fit my curing setup?
A: The machine uses 900×450 mm pallets. Pallet material — timber, composite, or steel — is selected based on your curing environment and handling equipment. We verify that the pallet specification aligns with your curing rack dimensions and forklift tine spacing before confirming the order.
Q: How is vibration force matched to my local aggregate?
A: The 35.5 kN exiting force at 4200 r/min is evaluated against your sieve analysis, aggregate photos, and mix proportions. If your sand carries high fines or your stone shape limits interlock, we adjust the vibration profile or recommend a mix correction so the QTJ4-24 produces consistent block density across your production run.