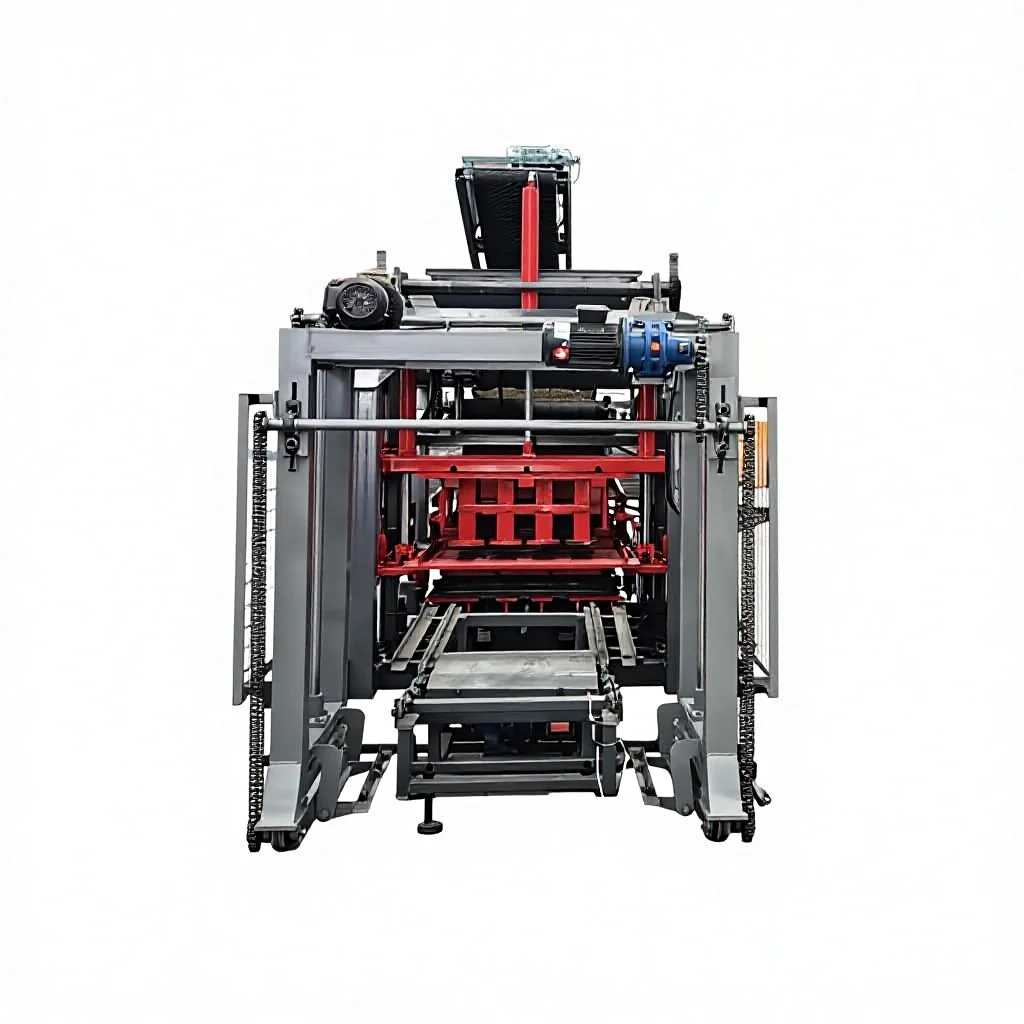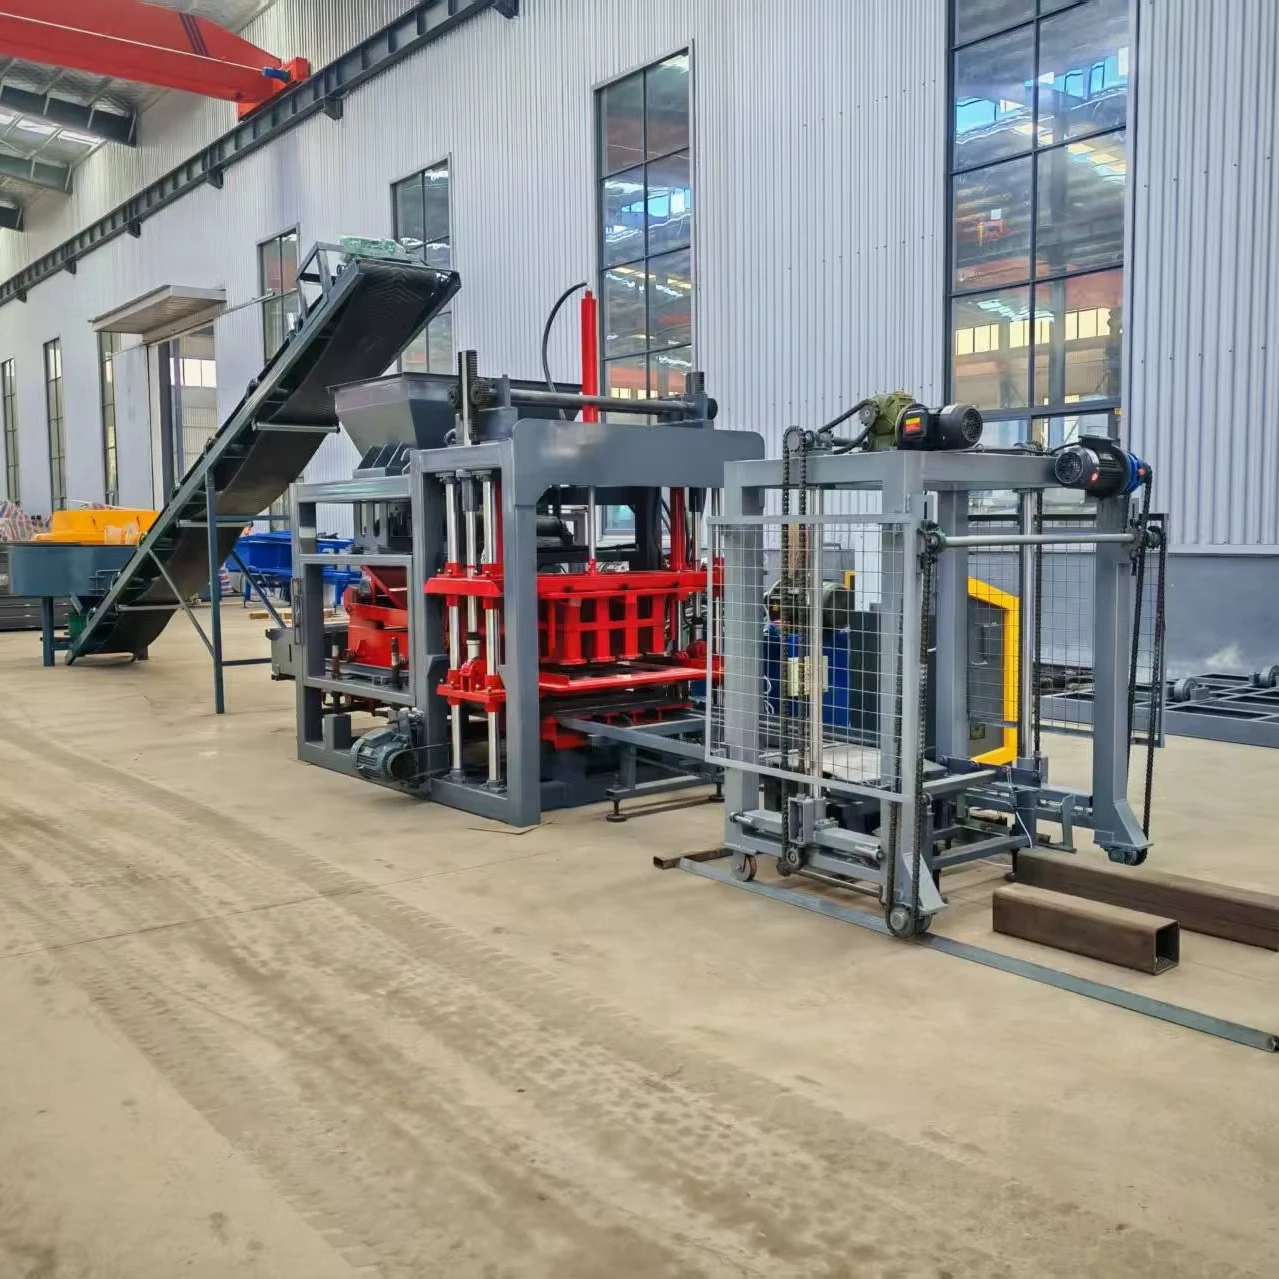
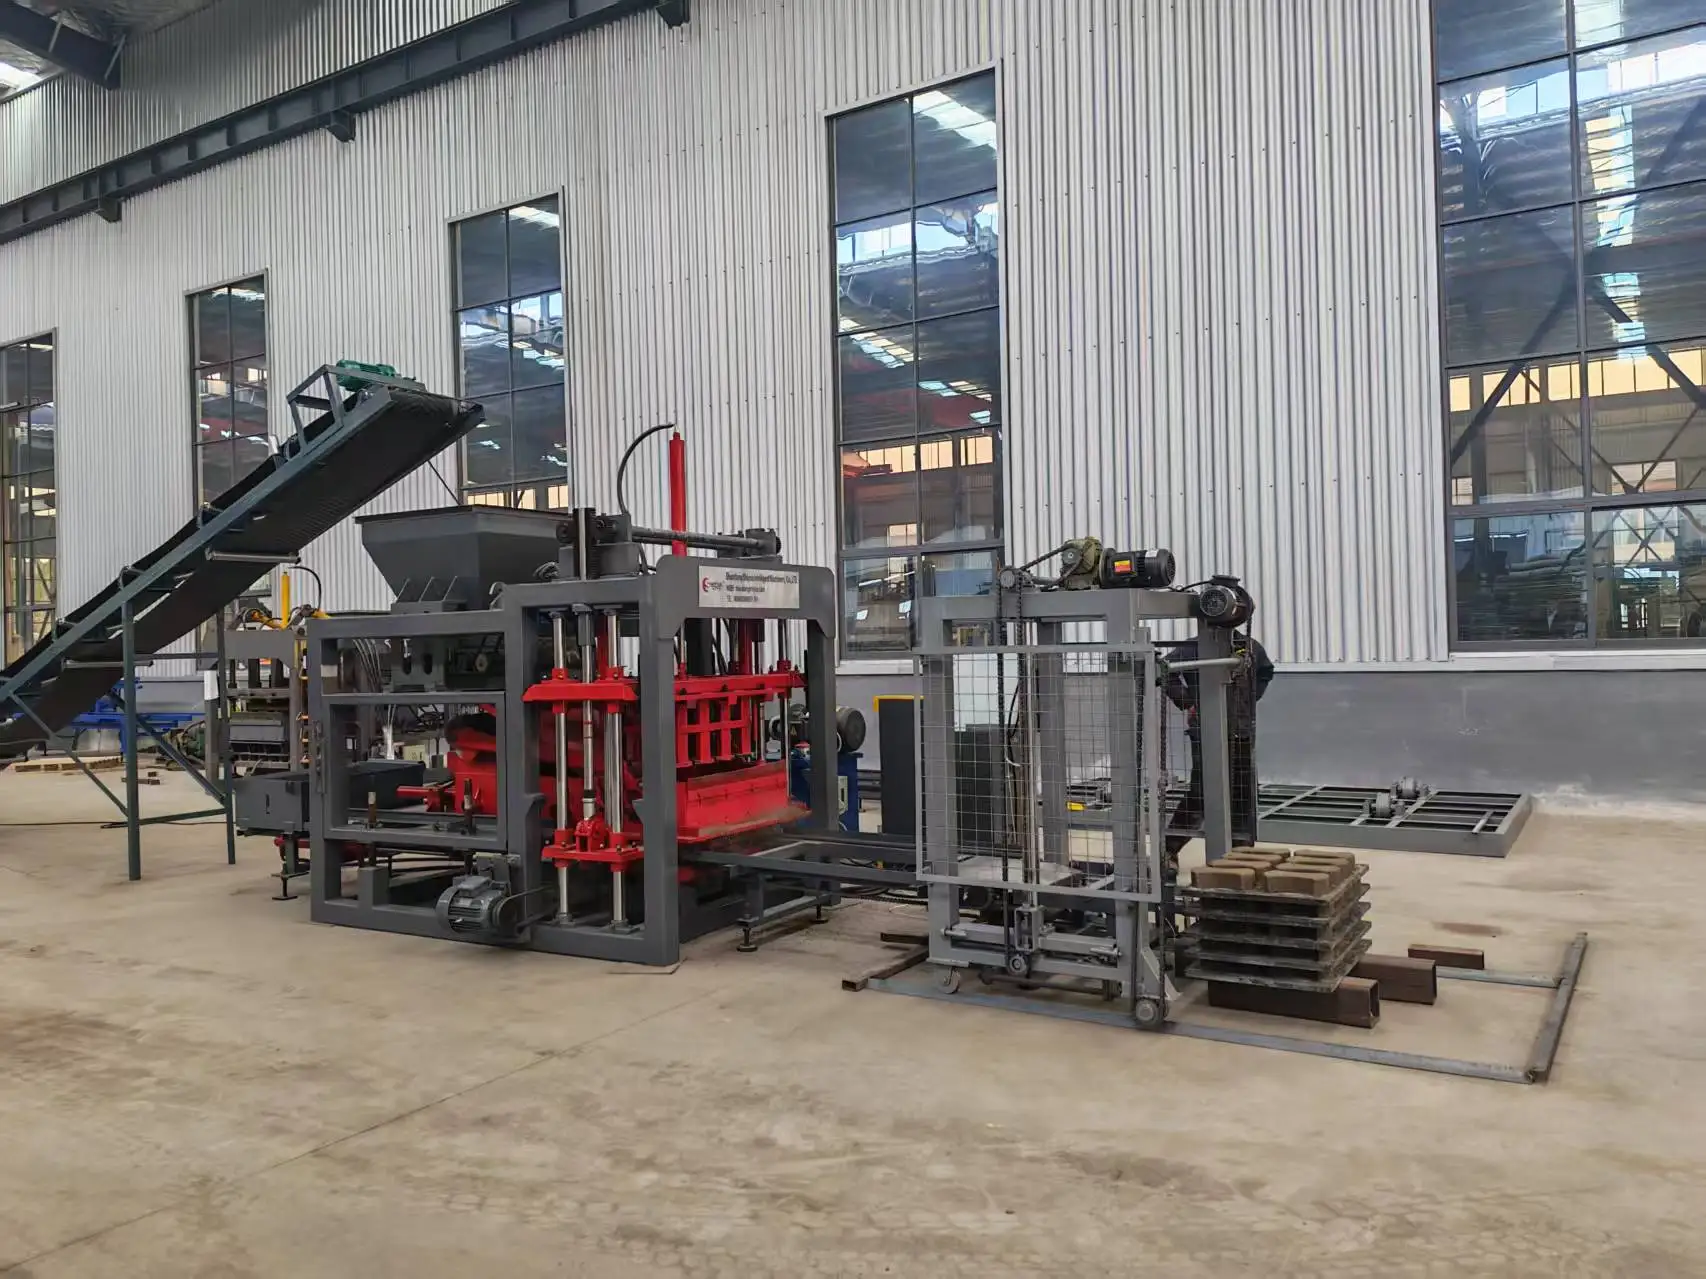
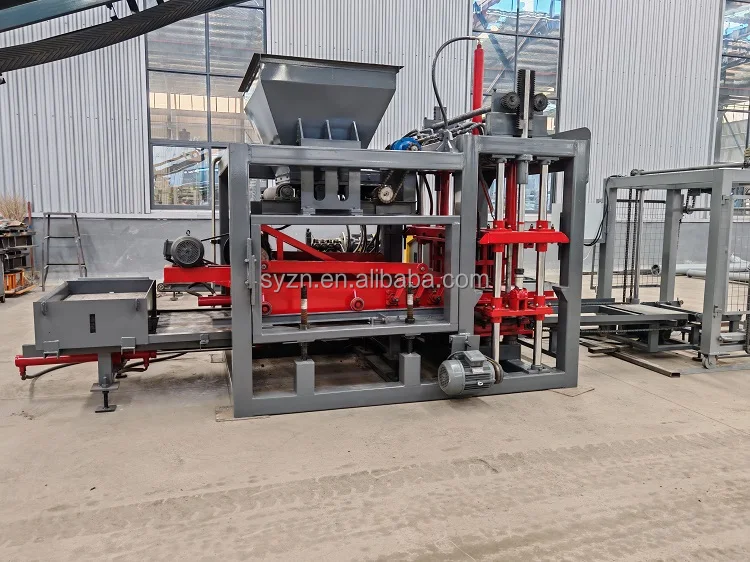
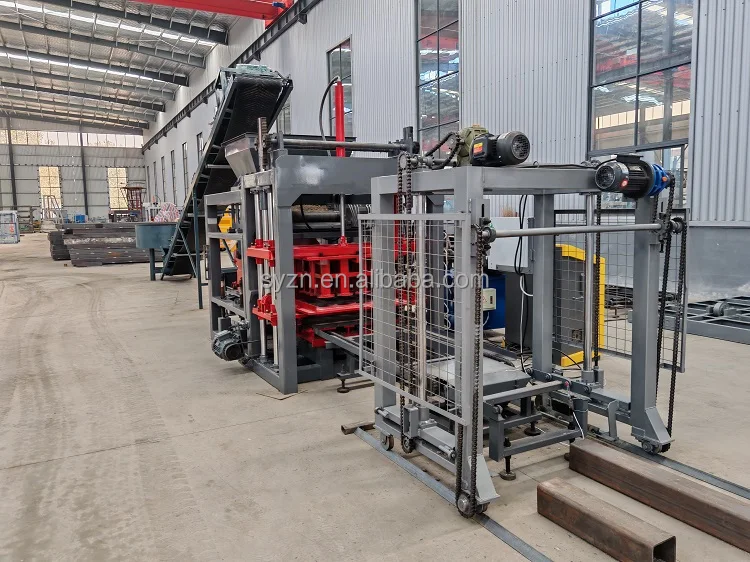
Description
Format-Specific Capacity Alignment — Every output figure for the QT4-18 is calculated against the exact block format and mould cavity count the buyer plans to run, eliminating the guesswork that causes new plants to miss daily targets from day one.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Hydraulic Concrete Block Making Machine |
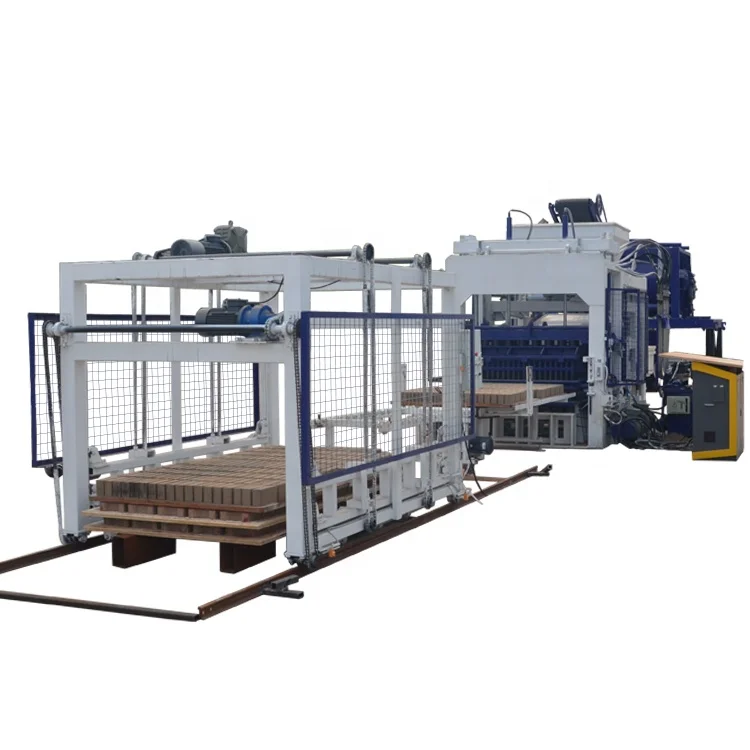
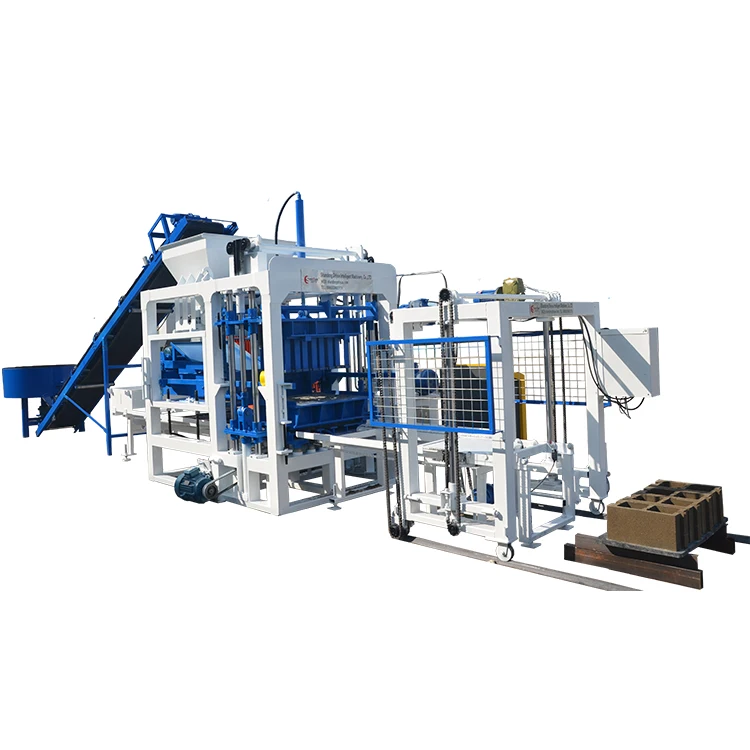
| Overall Dimensions (L×W×H) | 3900×1600×2300 mm |
| Total Weight | 3T |
| Rated Power | 24KW |
| Molding Cycle | 15-25s |
| Exciting Power (Vibration Force) | 40-50KN |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
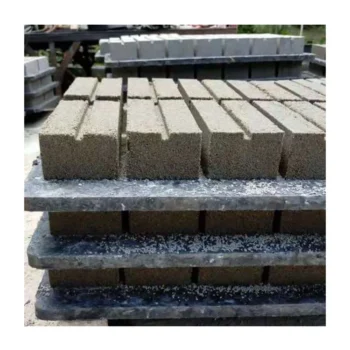
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output Capacity | 1200-1680 pcs/hr (basis: 400×200×200mm hollow block, 15-20s cycle) |
| Output Capacity | 1800-2400 pcs/hr (basis: 400×150×200mm hollow block, 15-20s cycle) |
| Output Capacity | 3240 pcs/hr (basis: 240×115×53mm solid brick, 15-20s cycle) |
| Daily Output (8hr) | 9600-13440 pcs (basis: 400×200×200mm hollow block) |
| Daily Output (8hr) | 14400-19200 pcs (basis: 400×150×200mm hollow block) |
| Daily Output (8hr) | 16200-19440 pcs (basis: 240×115×53mm solid brick) |
| Automation Level | Semi-automatic |
| Hydraulic System | Hydraulic station for high pressure and stable operation |
| Vibration Method | Bed mould vertical vibration and upper mould compression vibration |
| Mould Change | Mould and squeeze head interchangeable for different block formats |
| Voltage & Frequency | Configurable to site supply (basis to be confirmed) |
| Control System | PLC or MCC configuration (basis to be confirmed) |
| Certification | CE or other applicable standard (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow Block Production | 400×200×200mm and 400×150×200mm standard sizes using crushed stone, sand, and cement |
| Solid Brick Production | 240×115×53mm formats utilizing fly ash, dust, and cement blends |
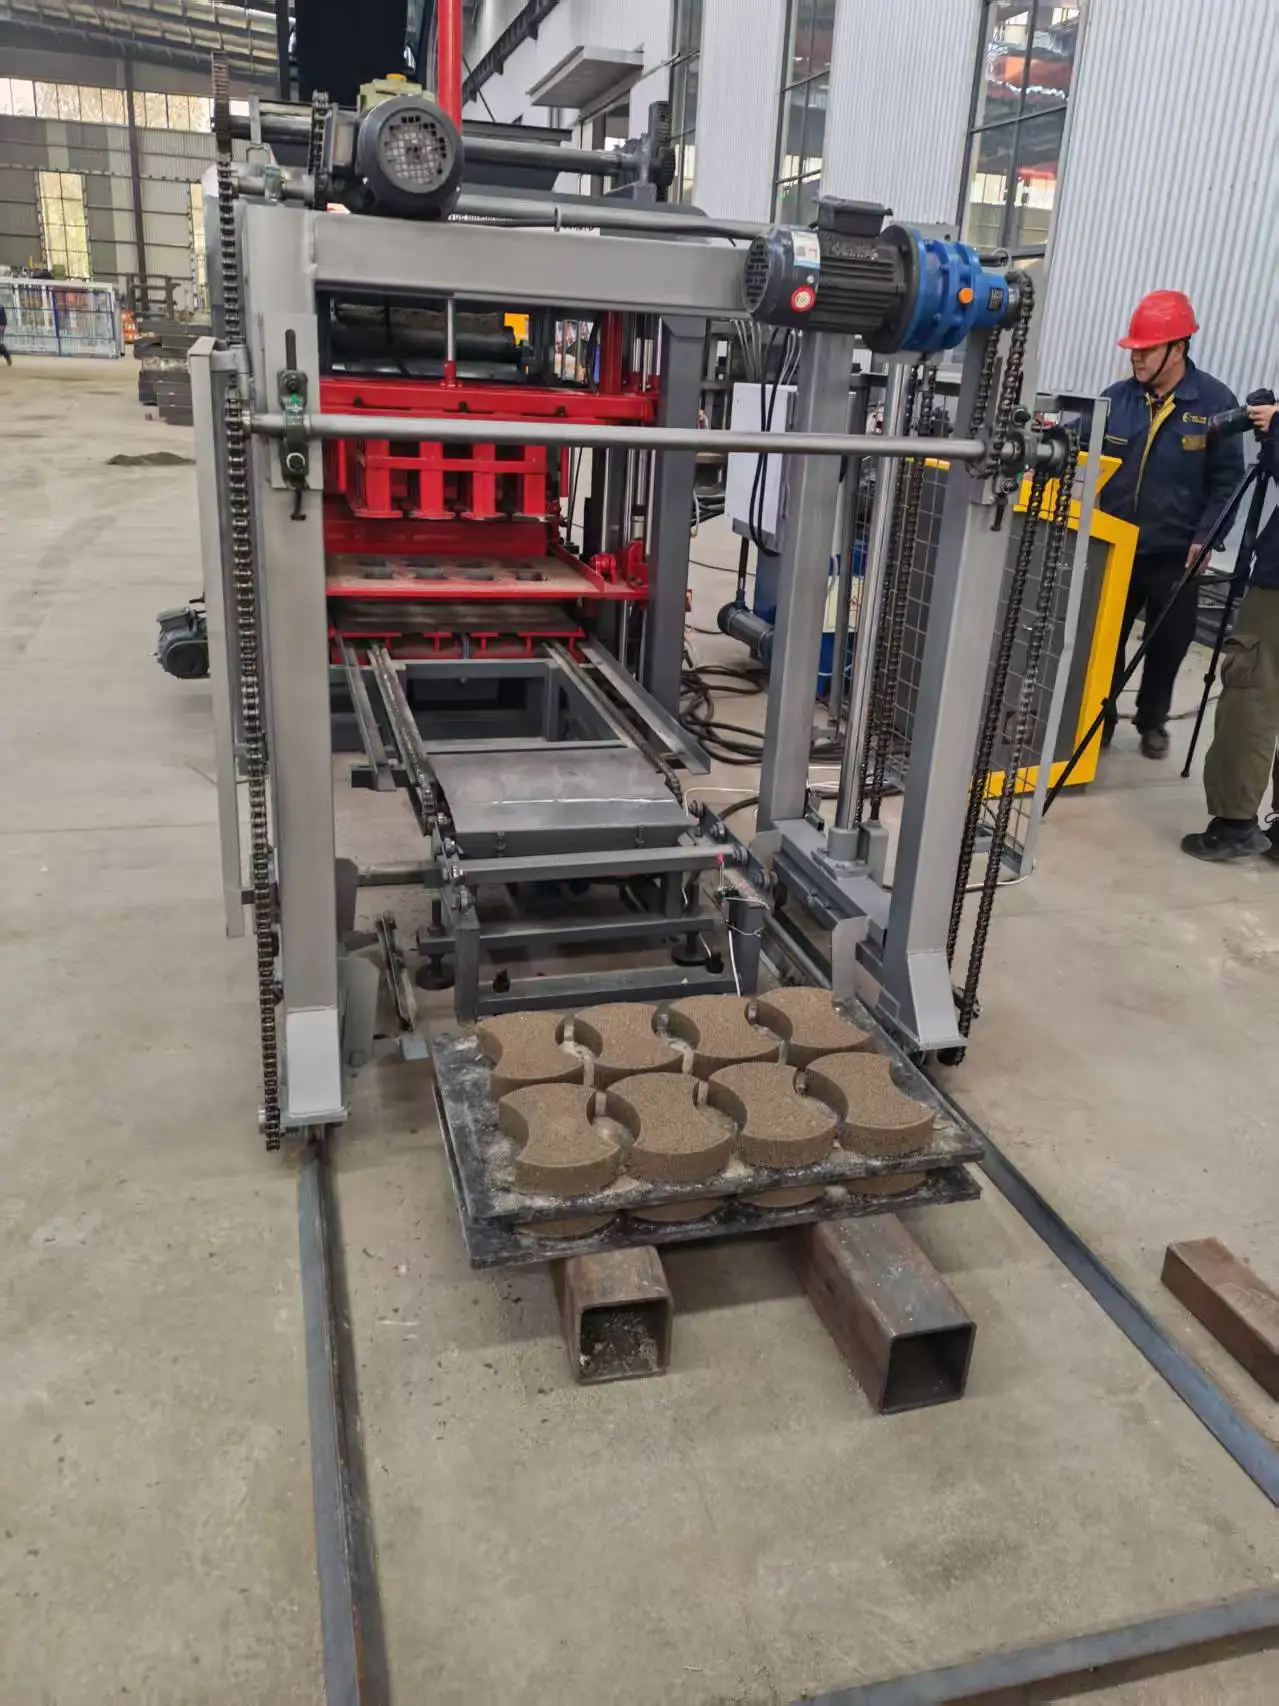
| Paver Block Production | Interlocking and standard pavers from high-density aggregate mixes |
| Kerbstone / Curbstone Production | Heavy-duty curbstone formats requiring maximum hydraulic pressure and vibration force |
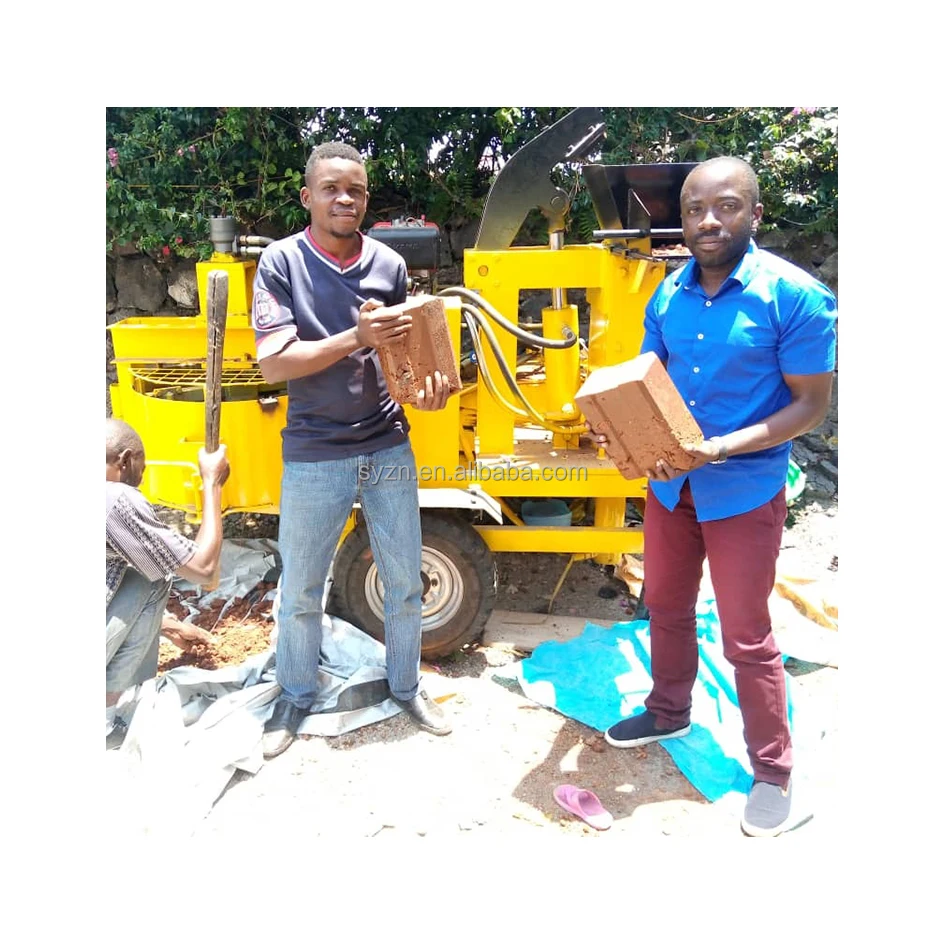
| On-Site Construction Production | Medium-scale output for housing projects using locally sourced raw materials |
Why "Maximum Output" Means Nothing Without a Block Format Attached
The QT4-18 hydraulic block making machine specifications only matter when tied to the exact block size your market buys.
I have seen plant owners in West Africa disappointed because a quoted capacity assumed a small solid brick, while their entire business plan relied on 200mm hollow blocks. The difference in daily volume between these two formats is massive. When we quote a capacity, we state the block dimensions, the mould cavity count, and the cycle time used for the calculation. This prevents the situation where a machine arrives, the operator runs the primary product, and the daily tally falls short of the business plan. The QT4-18 hydraulic block making machine specifications must be read alongside the specific format you intend to produce [NEED_CITE: block format standard dimensions and market preferences by region].
Matching the Vibration Profile to Your Local Aggregate
The vibration system on this press combines bed mould vertical vibration with upper mould compression vibration. This dual action is necessary when working with varied aggregates. In regions where builders use lightweight volcanic scoria or highly angular crushed dust, the vibration frequency and amplitude must be tuned differently than for smooth river sand. The 40-50KN exciting power provides the force, but the hydraulic pressure must be balanced against it to achieve consistent density. If the pressure is too high for the vibration, the mix segregates; if the vibration dominates, the block edges crumble.
Pallet Dimensions and the Curing Area Bottleneck
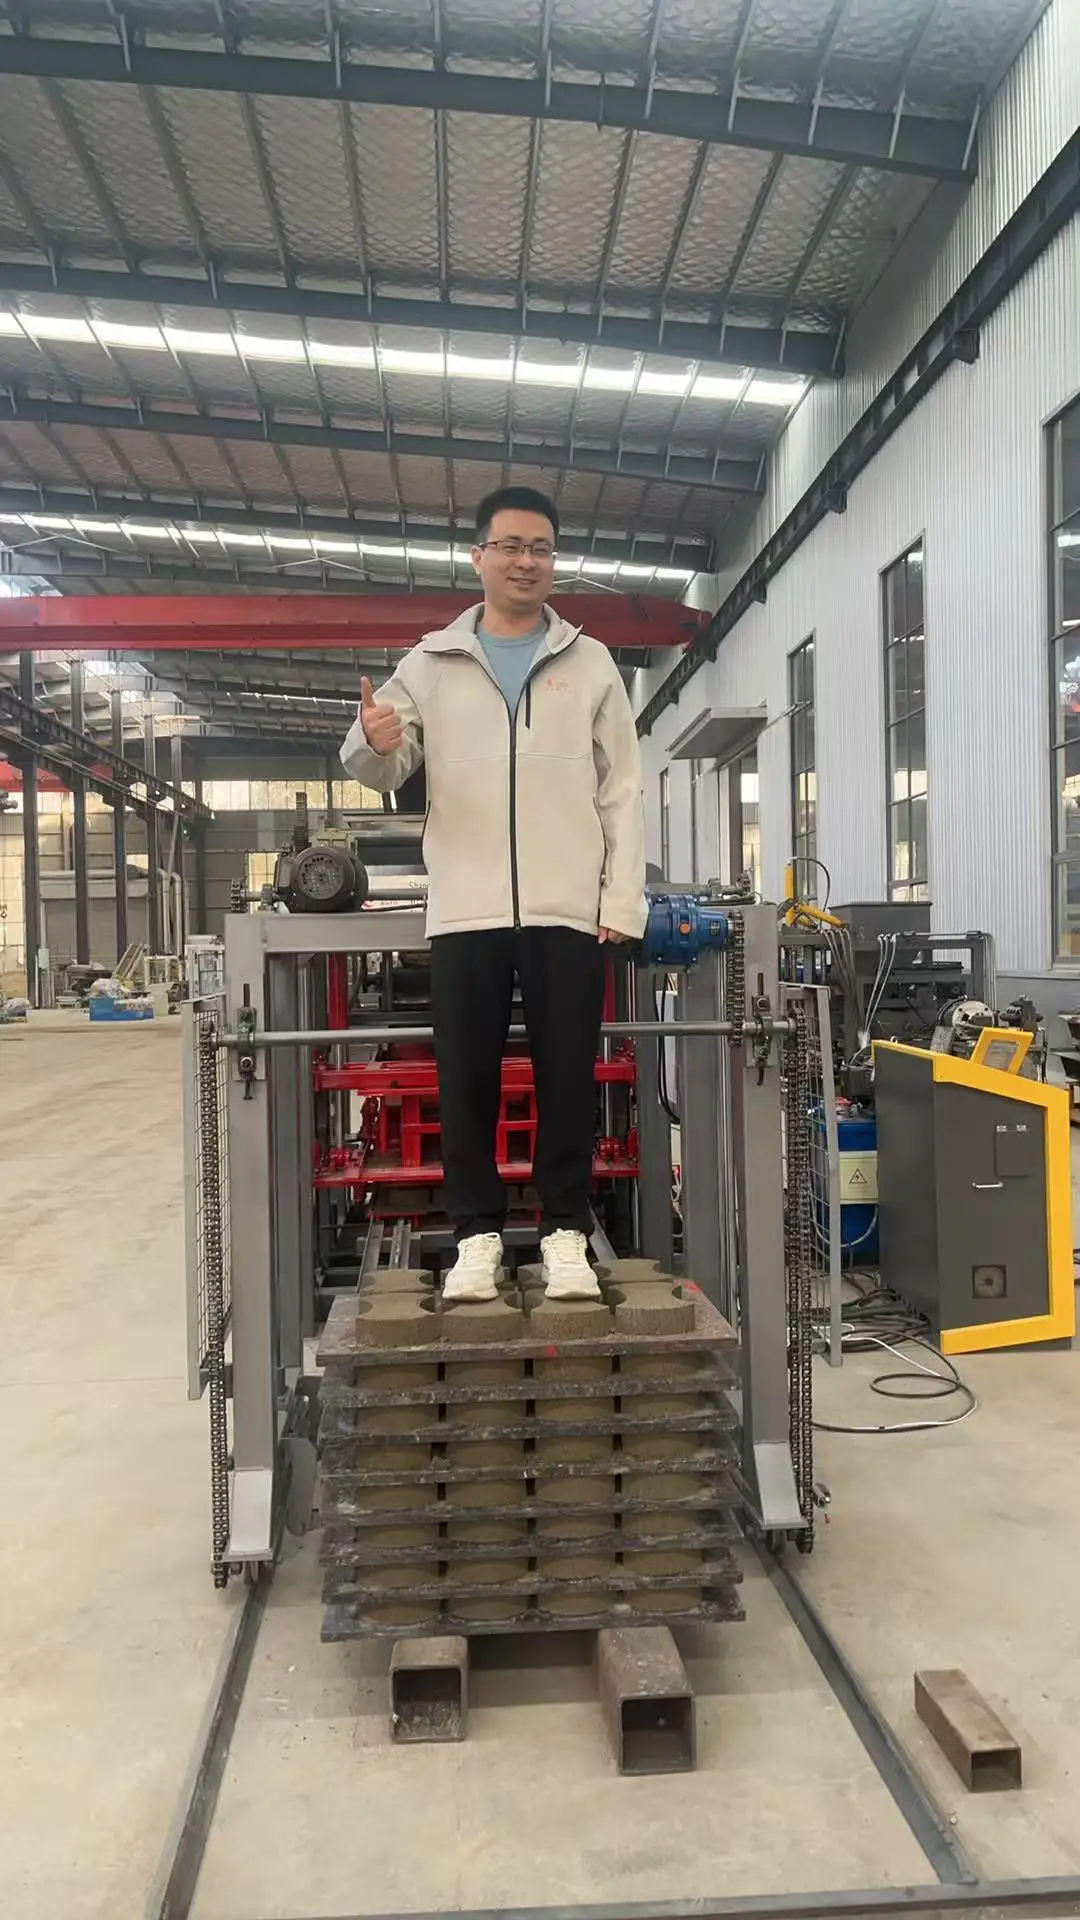
The fixed pallet size of 850×550×25 mm dictates the entire downstream handling process. Before confirming an order, the buyer must measure their existing curing racks and forklift tines. I once visited a site where the pallets were too wide for the curing chamber doors, forcing the crew to stack manually in the yard. The QT4-18 hydraulic block making machine specifications include this pallet dimension, and it is non-negotiable without changing the entire machine chassis. Verifying this measurement against your site layout prevents a costly bottleneck on the first day of production [NEED_CITE: pallet handling and curing area logistics in block manufacturing].
The Reality of Mould Changeover and Format Flexibility
The QT4-18 produces hollow, solid, paver, and kerbstone formats by changing the mould and squeeze head. The host machine remains the same, but the changeover requires mechanical tools and operator familiarity. A buyer planning to run three different formats in a single shift must account for the time spent unbolted, realigning, and recalibrating the squeeze head. This machine is best suited for plants that dedicate several days to a single format before switching, rather than those attempting hourly product rotation. The interchangeability is a genuine advantage, but it demands a disciplined production schedule to realize the capacity figures stated in the specification sheet.
The Hidden Cost of Unconfirmed Electrical and Control Parameters
Voltage, frequency, and PLC display language are often left until the machine is crated. When a 380V/50Hz machine arrives at a site running 440V/60Hz, the hydraulic pump motor overheats within the first week, and the PLC logic timers run at the wrong speed, ruining cycle accuracy. The cost of replacing a burnt motor and rewinding the control circuit far exceeds the time spent confirming these parameters before production begins. The QT4-18 hydraulic block making machine specifications list these as configurable, meaning the buyer must provide the exact site supply data and preferred operator language before the electrical panel is assembled [NEED_CITE: industrial voltage and frequency standards by country].
Why Sizing Against the Buyer’s Actual Product Mix Matters
The configuration of the QT4-18 is set against the buyer’s actual mix design and local aggregate, not a catalogue default. This means the hydraulic pressure and vibration force are matched to the specific density and strength requirements of the block the buyer sells.
The mould design and supply cover the formats the buyer’s market actually demands, including custom drawings for non-standard pavers or interlocking bricks.
The automation level is selectable, allowing a buyer to start with the semi-automatic configuration of the QT4-18 and plan for future handling upgrades without replacing the core press.
Installation and commissioning support includes operator training focused on the specific block formats and mould change procedures the plant will use daily.
Documentation & Verification
- Line layout and capacity calculation document stating the block format assumed for each output tier of the QT4-18.
- Mould drawing and format list showing every block size the machine can produce with the 850×550 mm pallet.
- Voltage, frequency, and PLC display language confirmation sheet signed before electrical panel assembly.
- Hydraulic and electrical schematic, factory test record, and wear parts list for first replacement planning.
Installation, Commissioning & Support
- Foundation pad must support the 3T total weight and 24KW power draw with a dedicated circuit breaker.
- Pallet feeding system requires manual loading at the semi-automatic level; operator training covers feed rate consistency.
- Hydraulic station filled with specified fluid grade; initial pressure set against the buyer’s confirmed mix design.
- Mould and squeeze head alignment verified on-site using the factory test record as the baseline.
- Wear parts list identifies the specific vibration springs and hydraulic seals for the first scheduled replacement.
- Daily maintenance checklist covers pallet surface inspection and vibration motor mounting bolt torque checks.
Preparing the Technical Inquiry
To move from a general inquiry to a confirmed configuration, provide the exact block format dimensions your market requires and the daily volume target for that specific size. Include a sample or description of your local aggregate (sand type, crushed stone size, fly ash source) so the vibration and pressure settings can be matched. Finally, confirm your site’s voltage, frequency, and the language your operators will need on the control display. This information allows us to generate an accurate capacity calculation and pallet handling recommendation before any commitment is made.
Frequently Asked Questions
Q: How is output capacity calculated per block format, and which format does the headline figure assume?
A: Every output figure for the QT4-18 is tied to a specific block size, mould cavity count, and cycle time. For example, 1200-1680 pieces per hour assumes a 400×200×200mm hollow block on a 15-20 second cycle. We do not use a single headline number that ignores the format you actually produce.
Q: How does the QT4-18 vibration force and hydraulic pressure match my local aggregate and mix design?
A: The 40-50KN vibration force and hydraulic pressure are balanced during commissioning based on your specific raw materials. If you use volcanic scoria or high-dust fly ash, the parameters are adjusted to maintain block density and edge integrity without causing mix segregation.
Q: What is the realistic mould change time, and what tools are needed on site?
A: Changing the mould and squeeze head on the QT4-18 requires standard mechanical hand tools and takes a portion of a shift. This machine is configured for plants that run a single format for several days rather than those attempting multiple format changes within a single production day.
Q: How do I confirm pallet size compatibility with my existing curing racks and forklift?
A: The QT4-18 uses a fixed pallet size of 850×550×25 mm. Before ordering, measure the internal width of your curing racks and the spacing of your forklift tines. If your existing infrastructure does not match this dimension, the pallet handling and curing layout must be redesigned before the machine arrives.