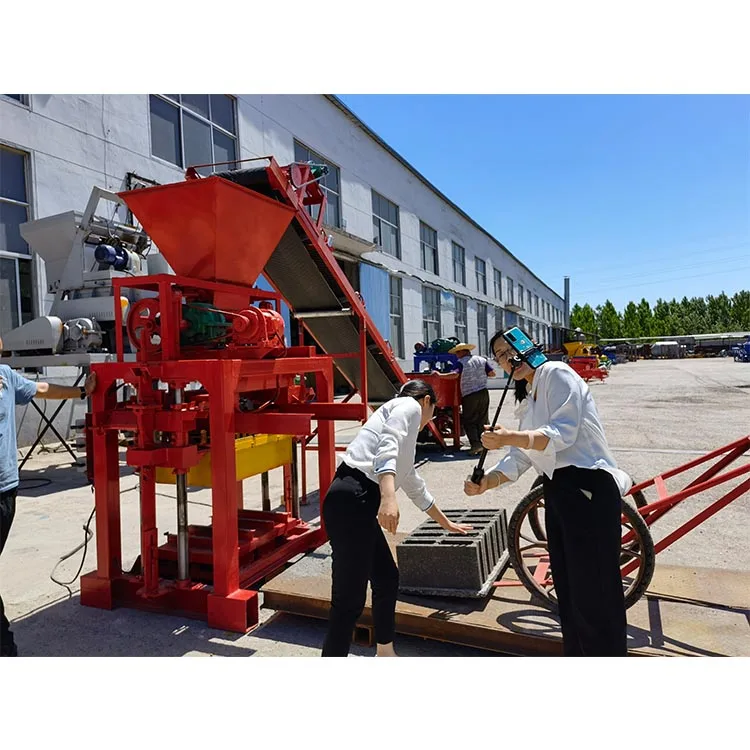
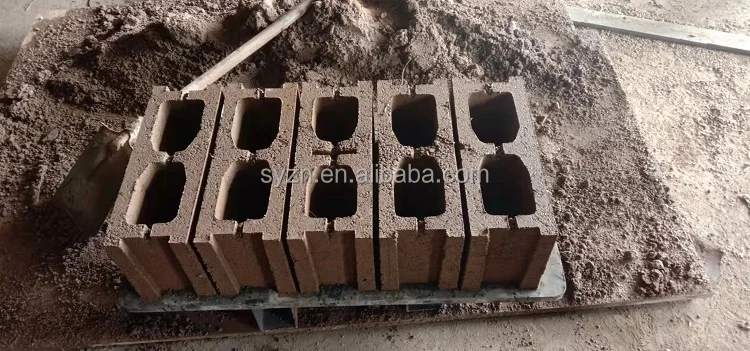
Description
Format-Matched Capacity — The QTJ4-35 is configured around the specific block dimensions your market actually sells, with every output figure tied to a named format rather than a single catalogue headline.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
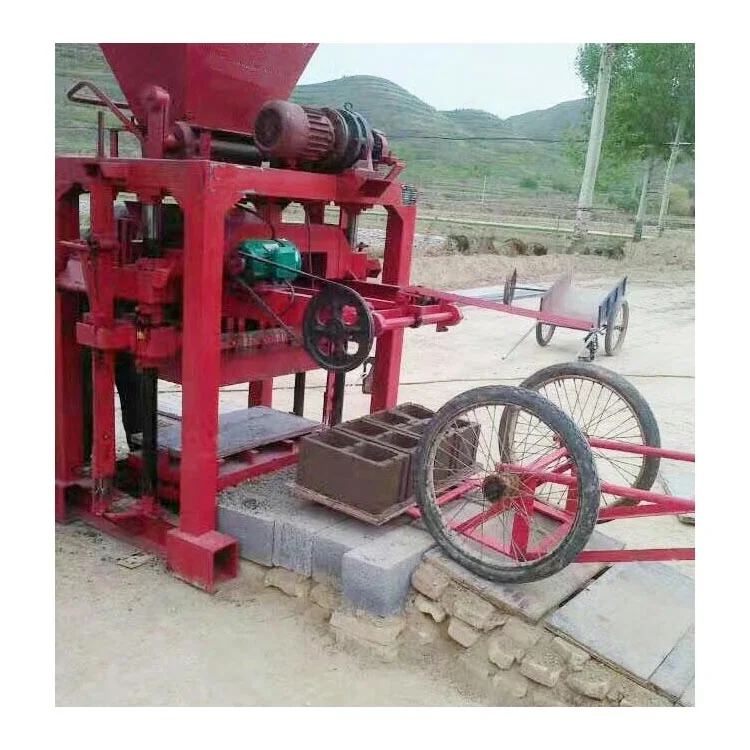
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Automation Level | Semi-automatic |
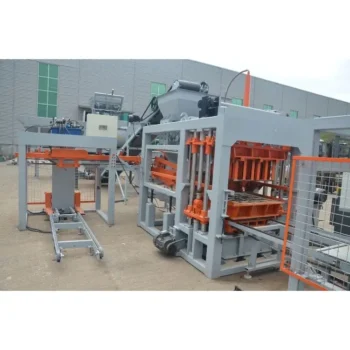
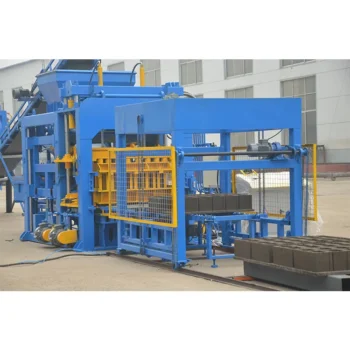
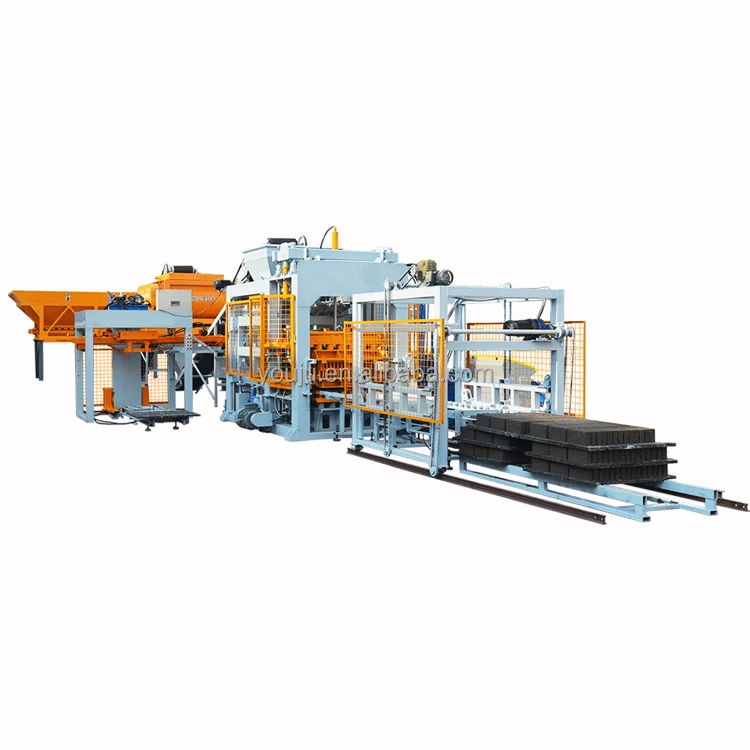
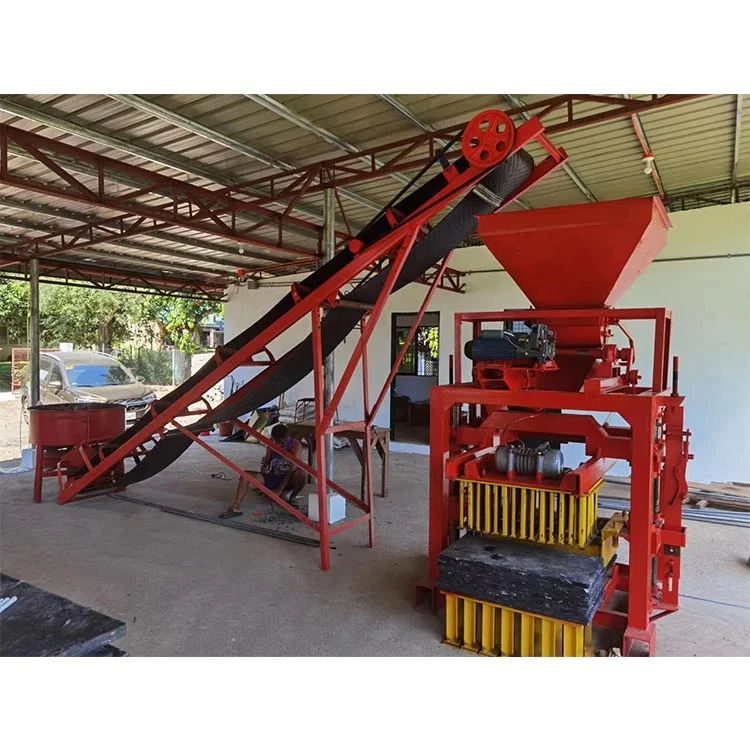
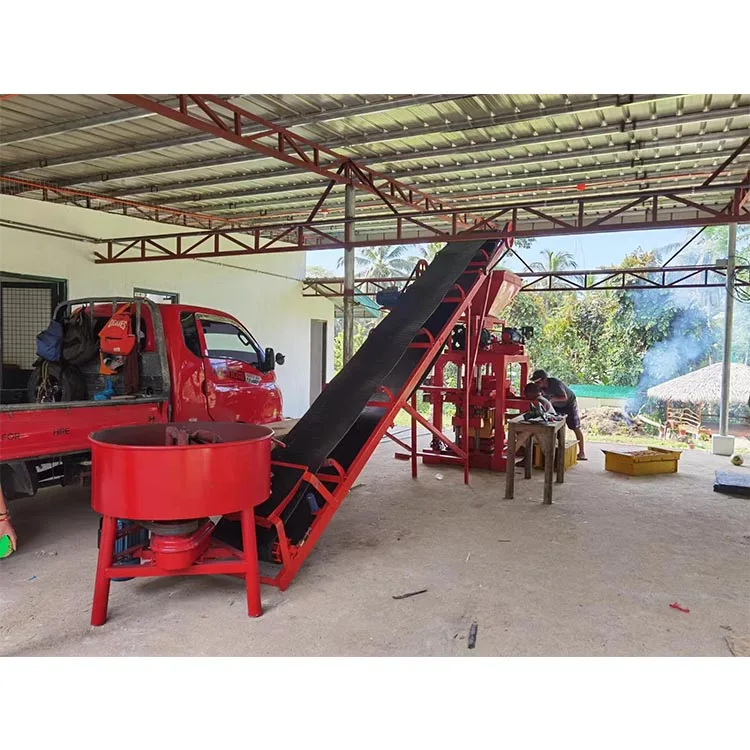
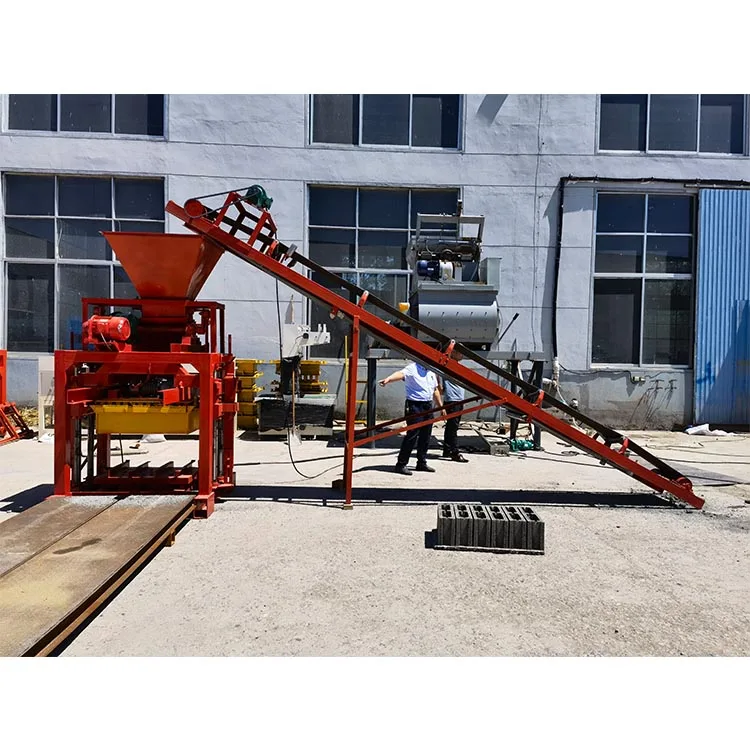
| Production Line Components | JQ350 mixer, belt conveyor, host machine |
| Mould Format Capability | Hollow blocks, solid blocks, pavers (via mould change) |
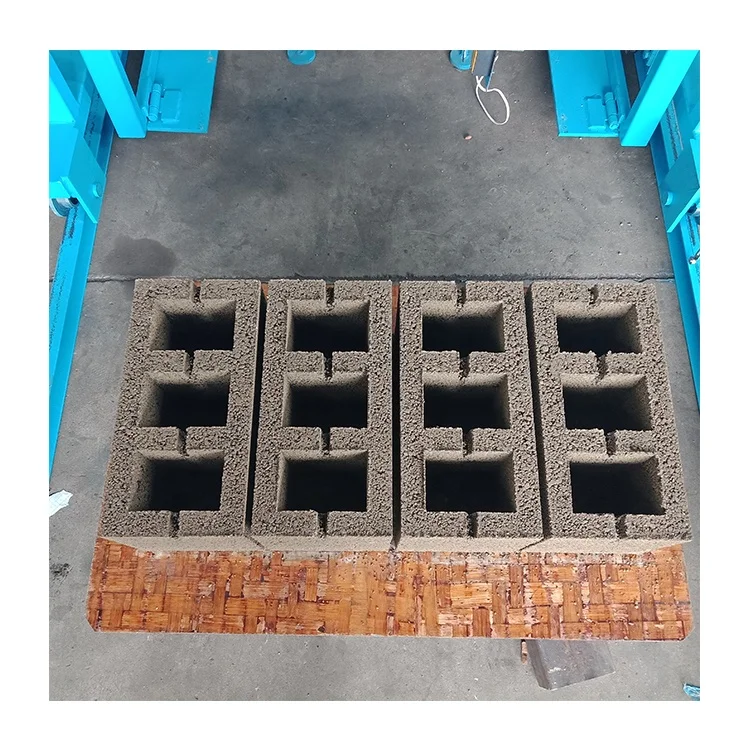
| Capacity at 400×200×200mm | 4 pcs/mould, 400 pcs/hour, 3,200 pcs/8 hours |
| Capacity at 400×150×200mm | 5 pcs/mould, 500 pcs/hour, 4,000 pcs/8 hours |
| Capacity at 225×112.5×60mm | 9 pcs/mould, 900 pcs/hour, 7,200 pcs/8 hours |
| Cycle Time | ~35 seconds (source value — verify against manufacturer catalog) |
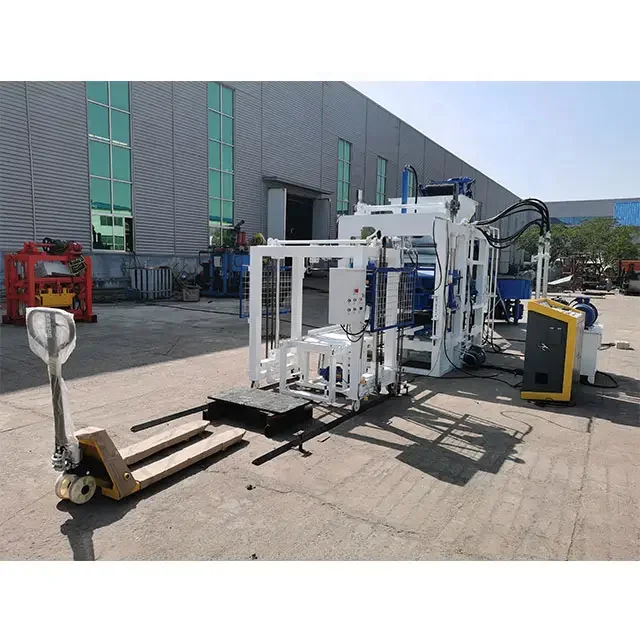
| Stacking Method | Manual pallet handling |
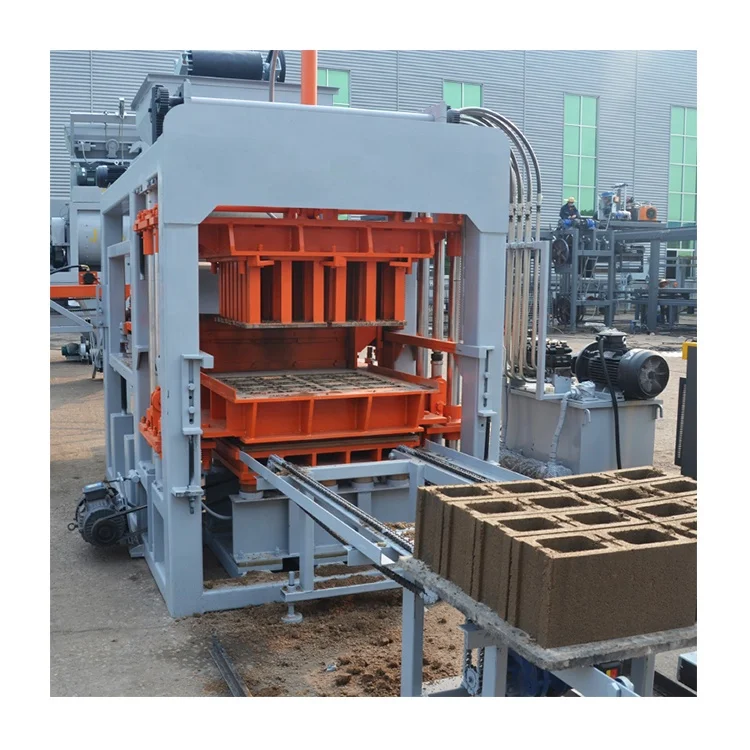
| Key Features | Vibration-based compaction, interchangeable moulds, manual/button control |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block production | Crushed stone, sand, cement and water mix for 400×200×200mm and 400×150×200mm wall blocks |
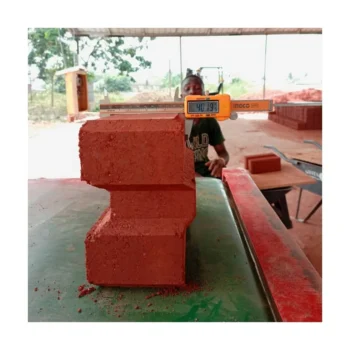
| Solid block manufacturing for load-bearing walls | Dense aggregate-cement mix producing 400×200×200mm solid blocks |
| Interlocking paver and slab production | Fine aggregate-cement mix for 225×112.5×60mm paving formats |
| On-site block production for construction projects | Locally sourced sand and gravel for hollow and solid blocks at the building site |
| Start-up block plant with limited capital | Entry-level production of multiple block formats on a single host machine |
Why "Pieces per Hour" Without a Format Name Is Useless to You
A capacity number means nothing until you know which block size it was measured on.
Sellers often quote a peak cycle count and let you assume it applies to whatever you plan to make. The reality is that a mould producing four large hollow blocks per cycle and a mould producing nine small pavers per cycle sit on the same host machine but deliver completely different daily totals. When the format assumption is buried or missing entirely, buyers end up planning a plant around a number that never materialises on the shop floor. The semi-automatic block machine specifications on this page tie every output figure to a specific block dimension so you can plan honestly [NEED_CITE: common misrepresentation of block machine capacity in export quotations].
Matching the Mixer and Conveyor to the Press Cycle
The QTJ4-35 ships as a matched line: a JQ350 pan mixer feeds a belt conveyor that delivers to the host machine hopper. This matters because a semi-automatic block machine runs in roughly 35-second cycles, and if the mixer cannot discharge a fresh batch before the next cycle begins, the press sits idle and your real output drops. The JQ350 capacity is sized to keep pace with the press at its standard cycle rate, so the bottleneck stays where it should — at the vibration table, not upstream.
Mould Change as a Real Production Variable
A single host machine handles hollow blocks, solid blocks, and pavers through mould swaps, which gives a small plant the ability to follow market demand without a second capital outlay. The semi-automatic block machine specifications list above shows how output shifts across formats — from 3,200 pieces per eight-hour shift at 400×200×200mm hollow block size up to 7,200 pieces at 225×112.5×60mm paver size. Buyers who intend to run two or three formats in a single week need to confirm the actual mould change procedure and tooling required, because a swap that takes most of a morning effectively cancels out the flexibility you paid for [NEED_CITE: mould change time impact on daily production scheduling].
How Vibration, Mix Design and Pallet Choice Intersect
Vibration-based compaction on the QTJ4-35 relies on a consistent feed material to produce uniform block density. The local aggregate gradation, cement ratio and moisture content all affect how the vibration energy transfers through the mix and into the mould cavity. If the mix is too dry, the block crumbles at de-moulding; too wet, and it slumps before curing begins. Pallet size must also match the curing yard dimensions and the forklift or hand cart you already have on site, because every wet block leaves the press on a pallet and stays there through the initial cure.
The Hidden Cost of Skipping Voltage Confirmation
I spent years assembling machines of this class on the workshop floor, and one mistake that still haunts me involved a shipment to Turkey. The customer’s facility ran on 440V three-phase, and the machine left the factory wired for 380V. It arrived, the electrician threw the breaker, and nothing happened. A temporary transformer took three weeks to source locally, and the customer’s project timeline collapsed. Voltage and frequency are not a footnote on the quotation — they are the first conversation, before any other specification is discussed, because correcting a mismatch after the machine is bolted to the floor is expensive, slow and entirely avoidable [NEED_CITE: industrial voltage and frequency standards by export market].
Why Procurement Through This Configuration Works
Block machinery is the single focus here, which means the host machine, mould, pallet and mixer are specified together rather than pulled from unrelated suppliers and forced to communicate on site. The configuration is set against your actual mix design and local aggregate, not a catalogue default that assumes materials you cannot source. Mould design covers the formats your market sells, and custom mould drawings are available when a standard format does not match. The semi-automatic tier keeps initial investment contained while leaving a defined path to add automatic pallet feeding, stacking and cubing later. Installation support includes operator training so the crew running the line on day one understands cycle timing, mould change procedure and daily maintenance checkpoints.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for every output figure
- Mould drawing and format list confirming each block size with pallet dimensions
- Voltage, frequency and control language confirmed in writing before production begins
- Factory test record on the buyer’s specified block format before dispatch
- Wear parts and mould list shipped with the machine for the first replacement cycle
- Operation and maintenance manual covering daily checkpoints and lubrication intervals
Installation, Commissioning & Support
- Foundation slab must be level and cured before the host machine and JQ350 mixer are positioned
- Dedicated three-phase circuit required; voltage and frequency locked before wiring begins
- Machine ships in assembled sections; belt conveyor and mixer are bolted on site to the host frame
- First production run supervised to confirm cycle timing, vibration intensity and block density
- Operator training covers mould change procedure, mixer loading sequence and manual pallet handling
- Wear parts list and mould inventory provided for planning the first replacement order
What We Need to Configure Your Line
To build a quotation that reflects your actual production plan, share the block formats and dimensions your market demands, your target daily output per format, the raw materials available locally with typical aggregate sizes, your site’s voltage and frequency, and the curing yard dimensions so pallet size can be matched. If you are replacing an existing machine, tell us what you are currently running and where the bottlenecks are.
Frequently Asked Questions
Q: How is daily output calculated, and which block format is each capacity figure based on?
A: Every output number on this page is tied to a specific block dimension. The 3,200 pieces per eight-hour shift figure assumes 400×200×200mm hollow blocks at four per mould. The 4,000 and 7,200 figures assume 400×150×200mm and 225×112.5×60mm formats respectively. Always ask for a written capacity calculation that names the format, because a single headline number without a block size is meaningless for production planning.
Q: What pallet size does the QTJ4-35 require, and how do I match it to my curing area?
A: Pallet size is determined by the mould format and the number of cavities. Before ordering, confirm your curing yard dimensions, stacking method and forklift or hand cart capacity so the pallet specification fits your existing workflow. Mismatched pallets create bottlenecks in curing and handling that reduce real daily output regardless of press speed.
Q: How long does a mould change actually take, and what tools are needed?
A: Mould change time depends on the format pair being swapped and the condition of the guide pins and clamps. Confirm the exact procedure and required tools before ordering if you plan to run multiple formats in a single week. A mould change that consumes most of a shift effectively eliminates the format flexibility you invested in.
Q: Can the JQ350 mixer keep up if I switch from hollow blocks to a denser solid block mix?
A: The JQ350 is sized to match the host machine cycle at standard mix designs. Denser mixes with higher cement content or finer aggregate may alter discharge time from the pan mixer. Confirm your intended mix design and material proportions so the mixer-to-press feed rate can be verified before the line is built.
Q: What voltage and control language will the machine ship with, and how is this confirmed?
A: Voltage, frequency and any control panel language must be confirmed in writing before production begins. This is the first item we lock down, because a mismatch discovered on site delays commissioning by weeks and costs significantly more to correct than a conversation at the quotation stage would have.