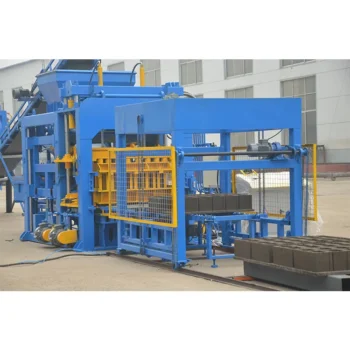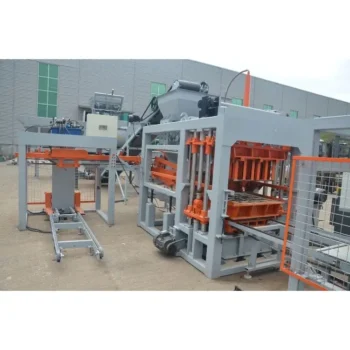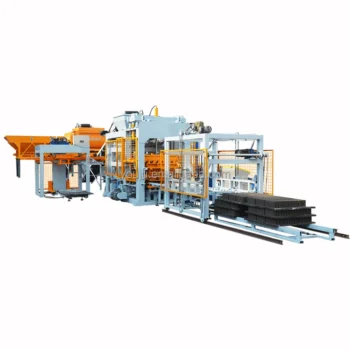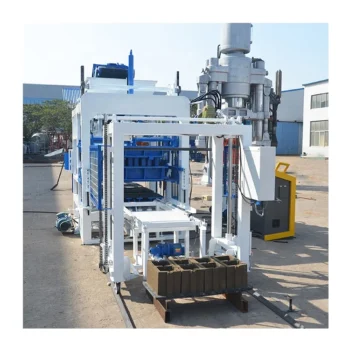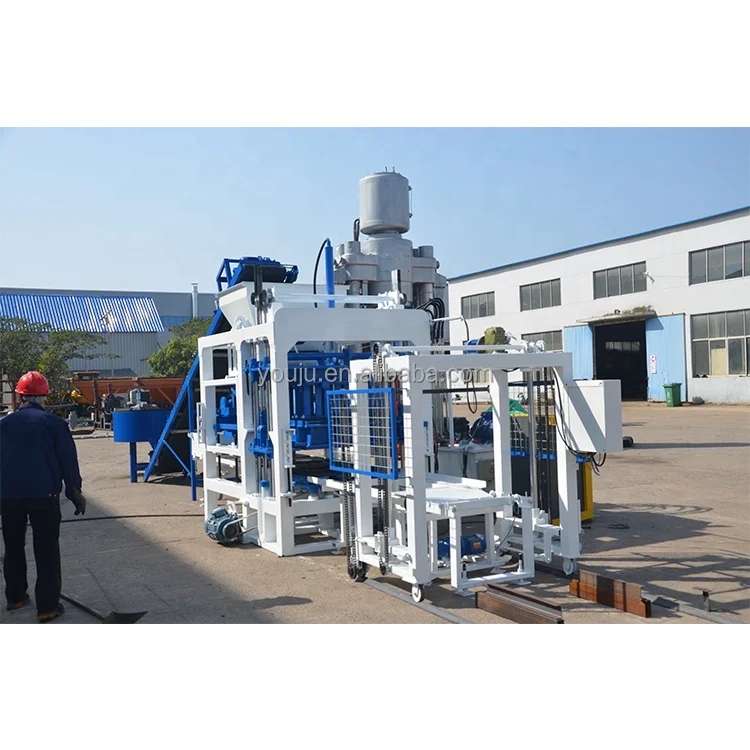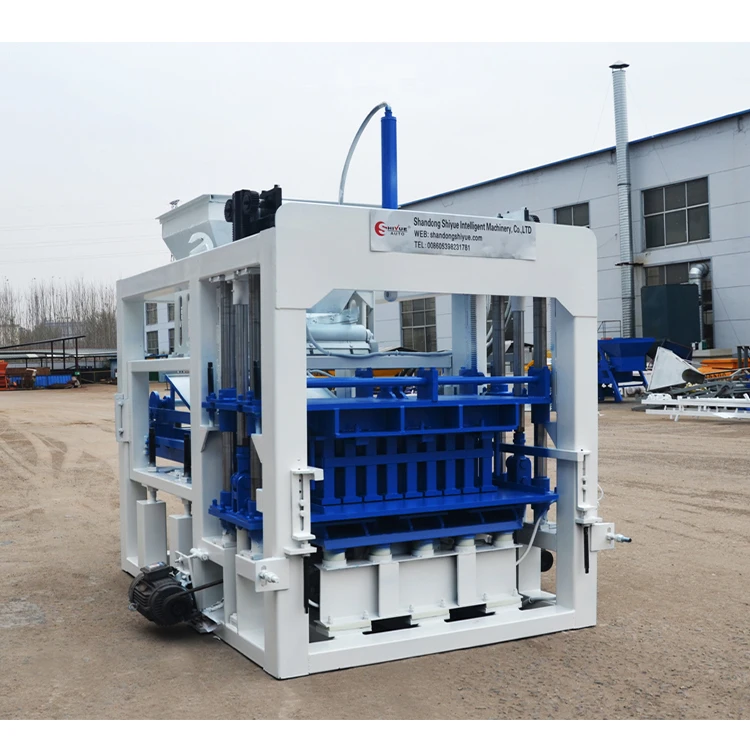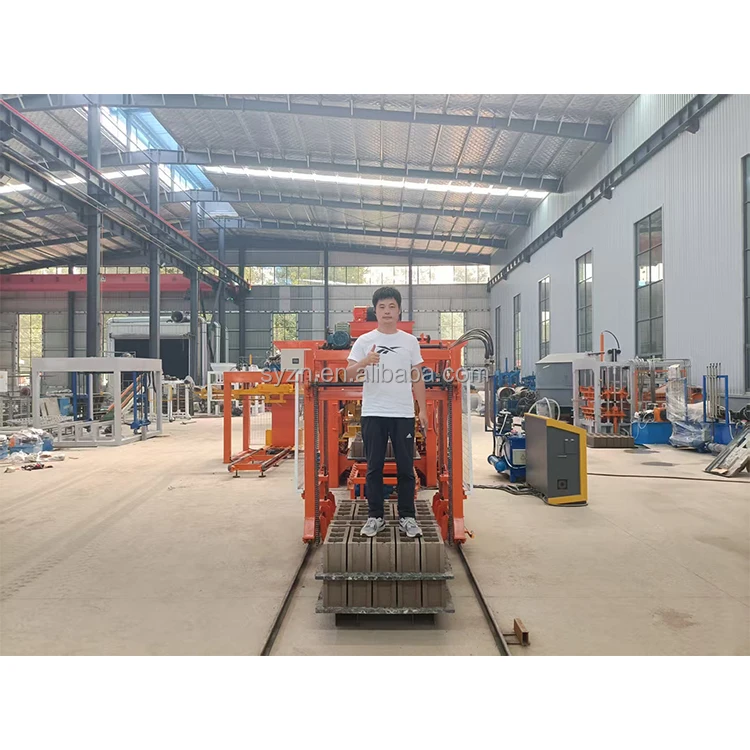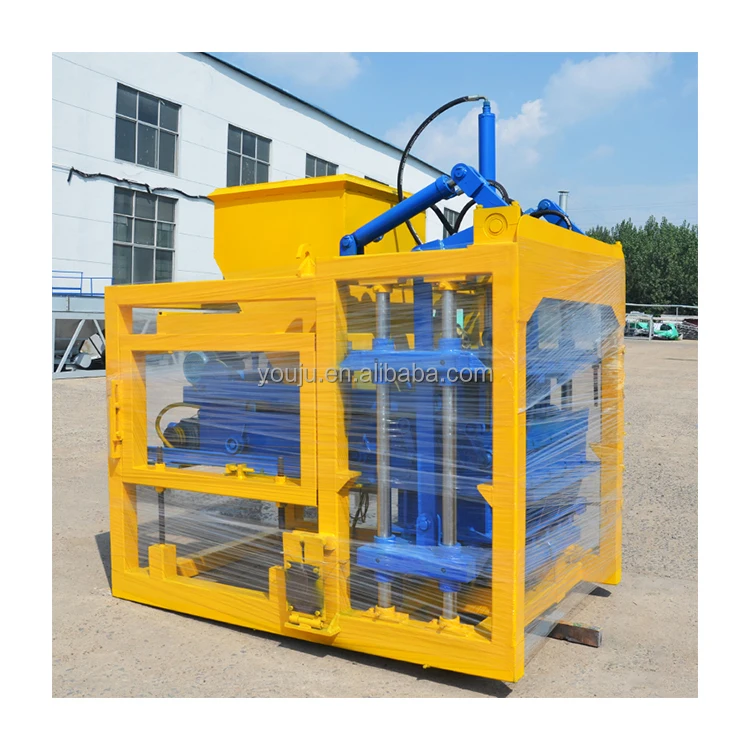
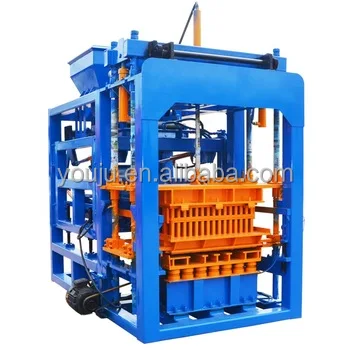
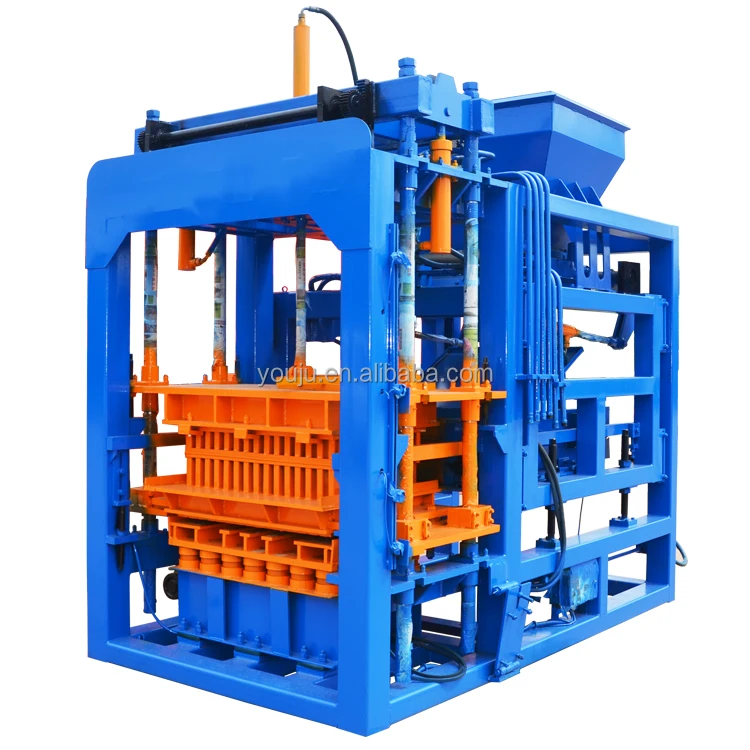
Description
Single-Format Honesty — capacity calculations tied to your exact block dimensions, not a generic catalogue figure that hides which product it assumes.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
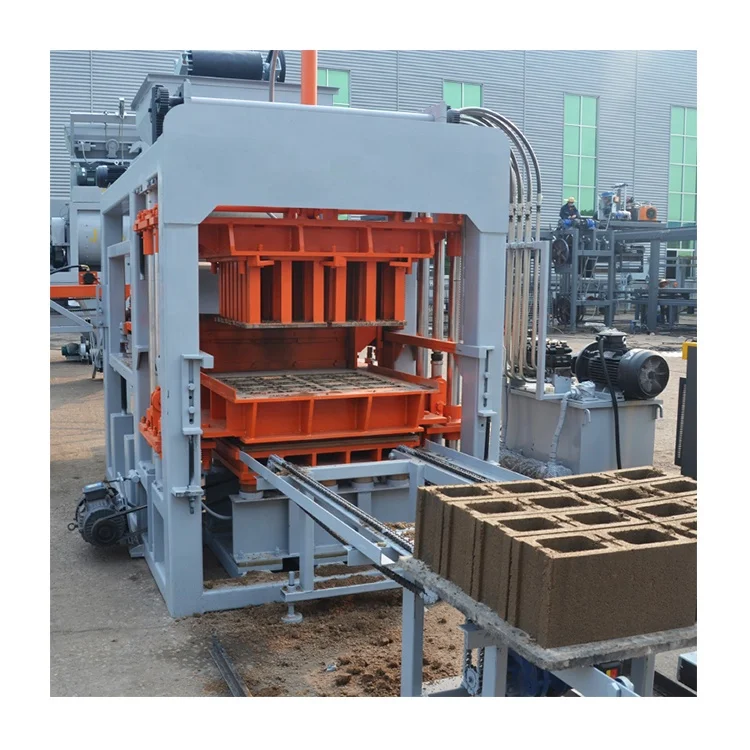
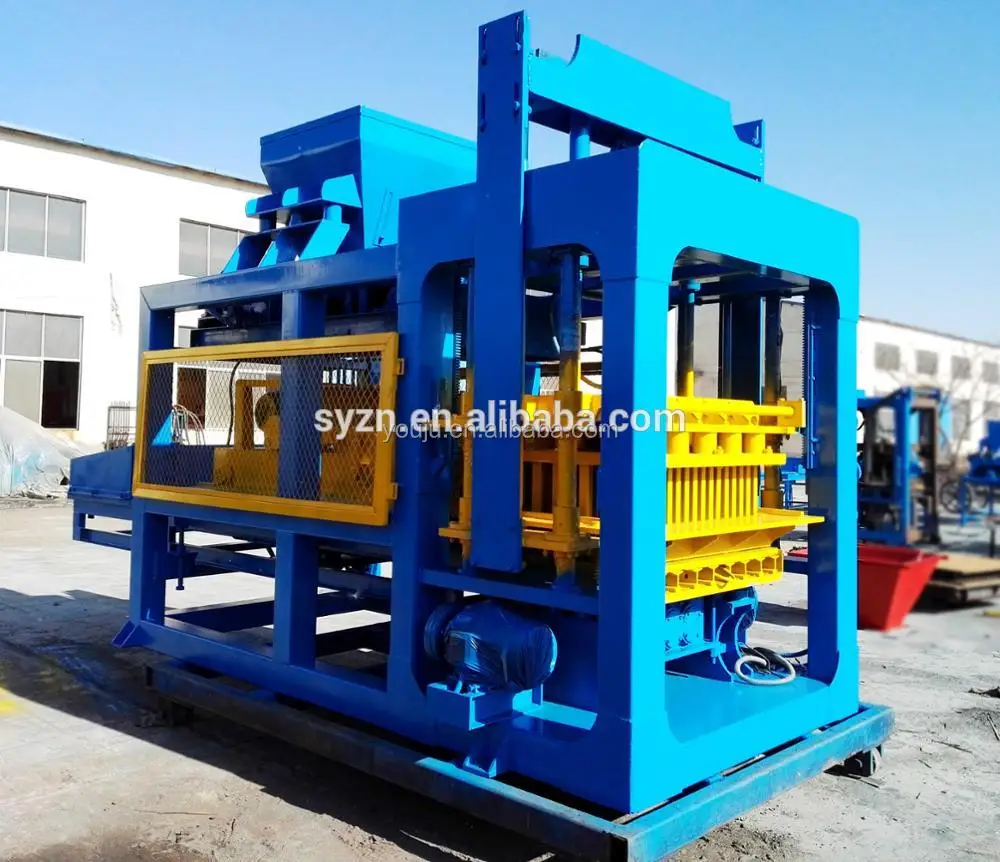
| Product Type | Automatic Concrete Block Making Machine |
| Molding Method | Vibration and hydraulic pressing |
| Rated Pressure | 21 MPa |
| Molding Cycle | 15 s – 20 s (basis not stated in source — confirm block format, material, and thickness before quoting) |
| Pallet Size | 900 × 700 mm |
| Main Machine Weight | 6000 kg |
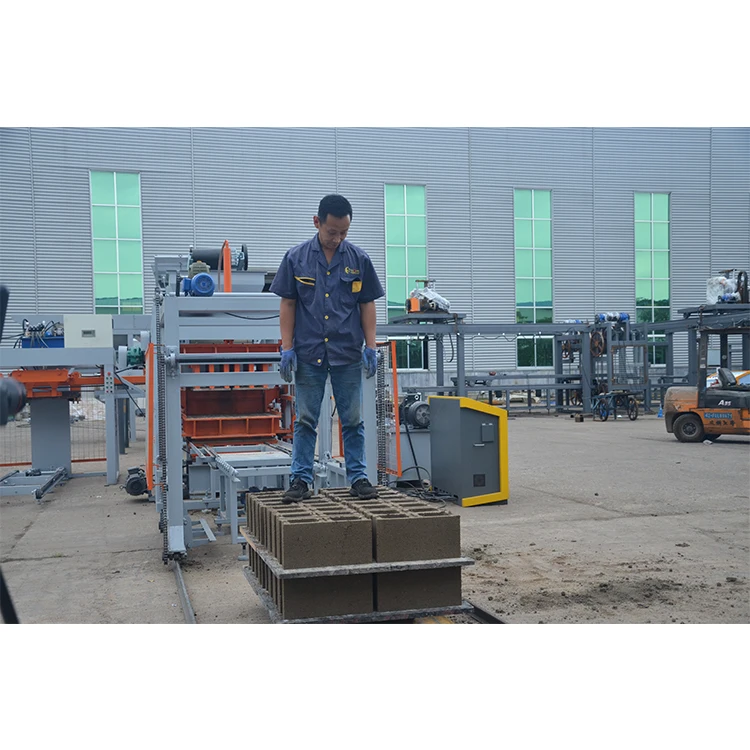
| Output – Hollow Block 400×200×200 mm | 6 pcs / pallet, 1440 pcs / h, 11 520 pcs per 8 h shift |
| Output – Paving Brick 200×100×60 mm | 21 pcs / pallet, 5040 pcs / h, 40 320 pcs per 8 h shift |
| Output – Solid Brick 240×115×53 mm | 32 pcs / pallet, 7680 pcs / h, 61 440 pcs per 8 h shift |
| Compatible Raw Materials | Cement, sand, fly ash, stone powder, slag |
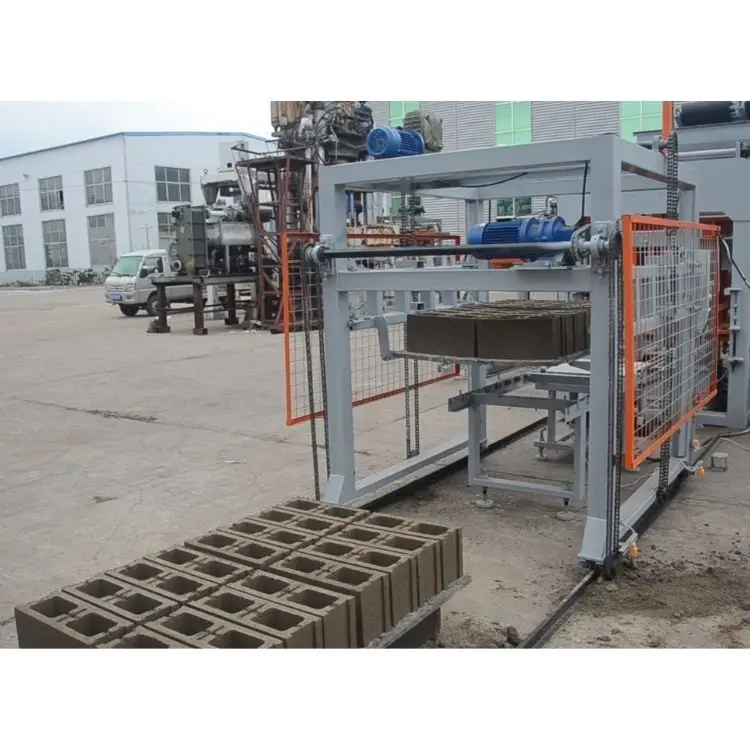
| Standard Line Configuration | JS500 mixer, 8 m conveyor belt, automatic stacker, cement silo, screw conveyor, cement scale, batching machine, pallet loader, block-and-pallet separator (optional) |
| Voltage | Customizable to local supply |
| Warranty | 1 year (excluding wearing parts) |
| Assembly for Shipment | Top cylinder removed for container loading |
| Included Accessories | One hollow block mould, two hydraulic trolleys |
| Machine Mobility | Factory-fitted wheels for on-site relocation |
Application Suitability
| Application | Typical Material or Output |
|---|---|
| Load-bearing hollow block production | Crushed stone, cement, and sand blends for structural walls |
| Interlocking brick for housing projects | Laterite or volcanic ash aggregate common in tropical markets |
| Paving brick for walkways and yards | Dense sand-cement mixes requiring high vibration force |
| Solid brick for partition walls | Fly ash and stone powder blends where clay is restricted |
| Kerbstone and color pavement brick | Pigmented face-mix layers over standard base concrete |
What "Blocks per Hour" Really Means for Your Plant
Every output figure on this page names the exact block format and dimension it was calculated on.
I still remember an Indonesian buyer who ordered an interlocking brick press rated at a certain hourly cycle count, only to discover on arrival that the number was based on a standard sand mix his region does not use. His local volcanic ash aggregate shifted the whole density curve, and the first production run had to be scrapped. Sizing an automatic block machine without locking the format, pallet size, and mix design to your market is how projects lose weeks before the first saleable brick leaves the yard. That lesson is the reason we now insist on seeing a material test report before any automatic block machine specifications and mould selection are finalized [NEED_CITE: local aggregate variability and compressive strength outcomes in concrete block production].
Cycle Time, Vibration, and the Density Target
The QT6-15 pairs 21 MPa hydraulic pressure with controlled vibration to compact each pallet. For hollow blocks the press must deliver enough force to close the void walls without crushing them, while paving bricks demand higher peak pressure to reach the density required for vehicular traffic. Matching automatic block machine specifications and mould selection to the buyer’s target strength grade starts here — pressure alone is not the whole story.
Pallet Dimensions Decide Your Curing Layout
A 900 × 700 mm pallet governs how many blocks sit on each curing rack, which forklift capacity you need, and how much floor space the wet-block zone occupies. Before the order is placed, we cross-check the pallet size against the buyer’s existing rack spacing and handling equipment so that blocks are never stacked by hand after the press releases them [NEED_CITE: pallet and curing rack compatibility in block plant logistics].
Reading the Pressure and Vibration Numbers
Hydraulic pressure of 21 MPa determines the static compaction force applied through the upper mould head, while the vibration motor fluidizes the concrete mix so particles settle into the cavity. If vibration is too weak for a given aggregate size, voids remain inside the block and compressive strength drops. If vibration is too aggressive for a fine fly-ash mix, the surface slumps before the mould lifts. The QT6-15 allows the vibration amplitude and duration to be tuned per mould format, so a paving brick cycle and a hollow block cycle each receive a different energy profile. Pallet size of 900 × 700 mm sets the upper bound on mould footprint; any custom interlocking or kerbstone mould must fit within that envelope while still leaving clearance for the hydraulic trolley guide rails. Moulding cycle of 15 s to 20 s is achievable on thinner solid bricks, whereas deeper hollow blocks and color face-mix paving bricks typically sit at the longer end of that range, which is why output per hour must always be stated alongside the format.
The Cost of Skipping the Mix-Design Check
When a machine is configured for a standard silica-sand recipe and the buyer’s site only has access to crushed coral or volcanic tuff, the water-to-cement ratio shifts and the block emerges either too brittle or too soft. Moulds machined for one aggregate gradation will wear unevenly against a harder local stone, cutting mould life in ways that only appear after several production runs. These mismatches rarely show up in a factory acceptance test because the test uses the supplier’s stock material, not the buyer’s [NEED_CITE: premature mould wear from abrasive aggregate in concrete block production].
Why Sourcing Through This Range Makes Sense
Block machinery is our only product line, so the QT6-15 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate vendors. Each proposal sets the configuration against the buyer’s actual mix design and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings for interlocking profiles that do not exist in our standard library. Automation level is selectable — a buyer can start with the JS500 mixer, conveyor, and automatic stacker, then add batching and pallet separation later. Installation support includes operator training on the specific mould formats delivered, so the crew knows the changeover procedure before the first production day.
Documentation & Verification
- Line layout drawing stating capacity per block format and pallet count
- Mould drawing package listing every included and optional format
- Pallet specification sheet with size, material, and load rating
- Voltage, frequency, and PLC display language confirmation record
- Factory test video run on the agreed mix proportion before dispatch
- Operation and maintenance manual with wear parts and mould list
Installation, Commissioning & Support
- Foundation plan sized for the 6000 kg main frame and vibration isolation pads
- Electrical cabinet wired to confirmed local voltage before the machine leaves the factory
- Top cylinder re-mounted on site after container unloading, guided by assembly marks
- First-run parameter tuning against the buyer’s local aggregate and target block strength
- Operator training covering mould changeover, pallet loading, and daily lubrication points
- Wear parts list with hydraulic seals and vibration motor bearings identified by part number
What to Include in Your First Inquiry
To size the QT6-15 line correctly, send us the block formats you sell today along with their target dimensions and minimum compressive strength. Share a recent sieve analysis of your local aggregate and the cement type available in your region. Let us know the daily output you need, the curing area dimensions you have or plan to build, and the voltage and frequency at the site so we can confirm motor and control ratings before production begins.
Frequently Asked Questions
Q: How is output capacity calculated per block format on the QT6-15?
A: Each capacity figure pairs a specific block dimension with a pallet count and cycle time. For example, 400×200×200 mm hollow blocks run six per pallet at the stated molding cycle, yielding 11 520 pieces in an eight-hour shift. Different formats have different pallet counts and cycle lengths, so the hourly number changes with the product.
Q: Which mould formats are included and how are custom moulds handled?
A: One hollow block mould and two hydraulic trolleys ship with the standard package. Additional formats — paving brick, solid brick, interlocking, or kerbstone — are quoted separately. Custom moulds are built from the buyer’s drawings or designed in-house against a sample block and local market requirement.
Q: How is the machine configured against local aggregate and mix design?
A: We request a sieve analysis and material test report before finalizing vibration amplitude, pressure dwell time, and mould cavity tolerances. This ensures block strength meets the buyer’s standard when using locally available sand, stone powder, or fly ash rather than the supplier’s test material.
Q: What pallet size is recommended and how does it affect curing layout?
A: The standard pallet is 900 × 700 mm. We cross-check this size against the buyer’s existing curing racks and forklift capacity. If rack spacing or handling equipment differs, pallet dimensions can be adjusted before production to avoid manual restacking after the press releases each board.
Q: What documentation confirms voltage and control language before shipment?
A: A written confirmation record locks voltage, frequency, and PLC display language before the machine enters production. A factory test record showing the agreed mix proportion and block format is shared with the buyer before container loading to verify cycle time and output.