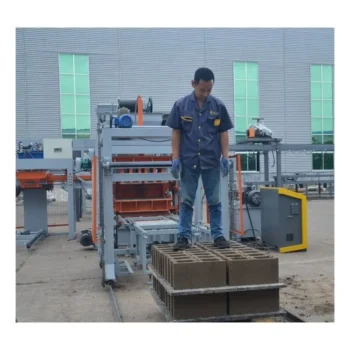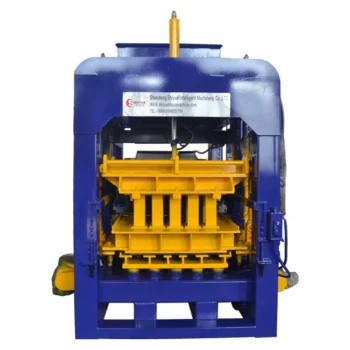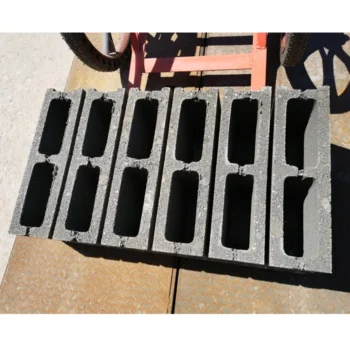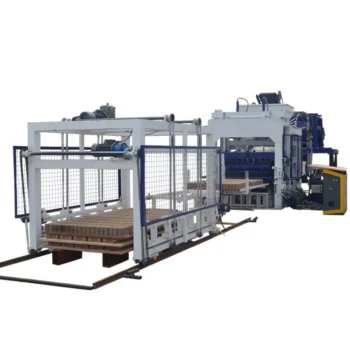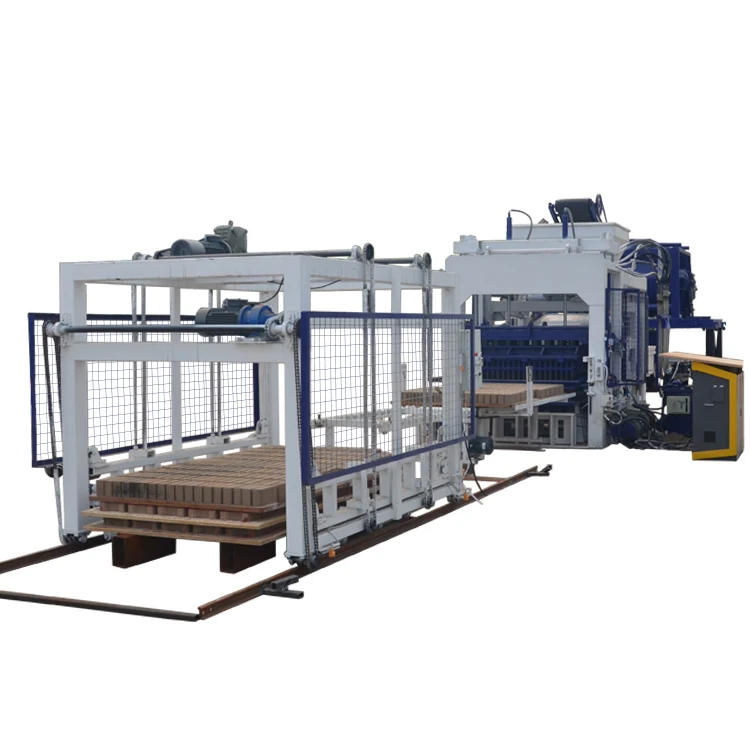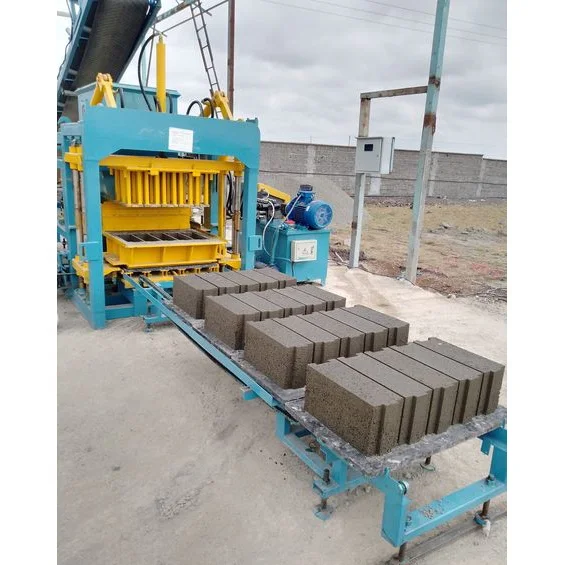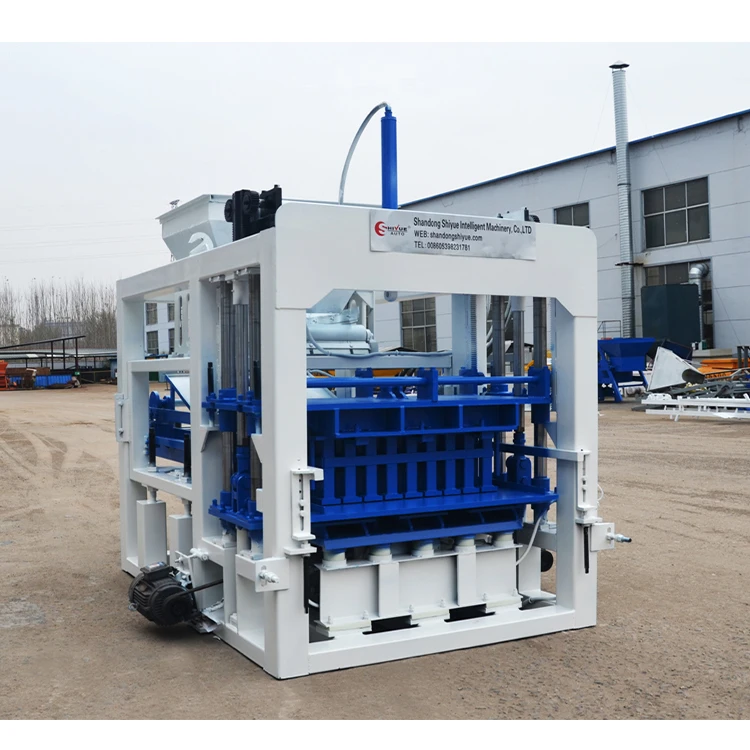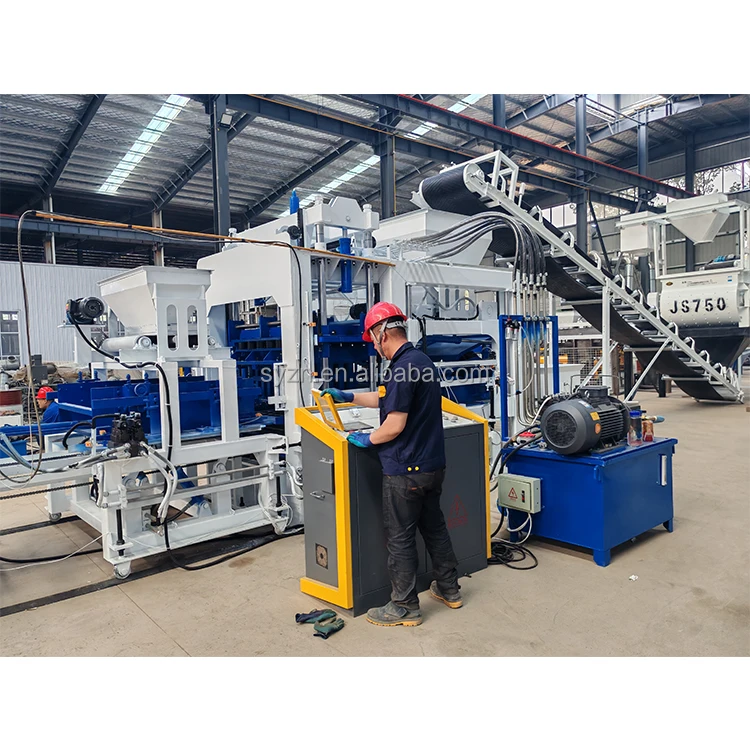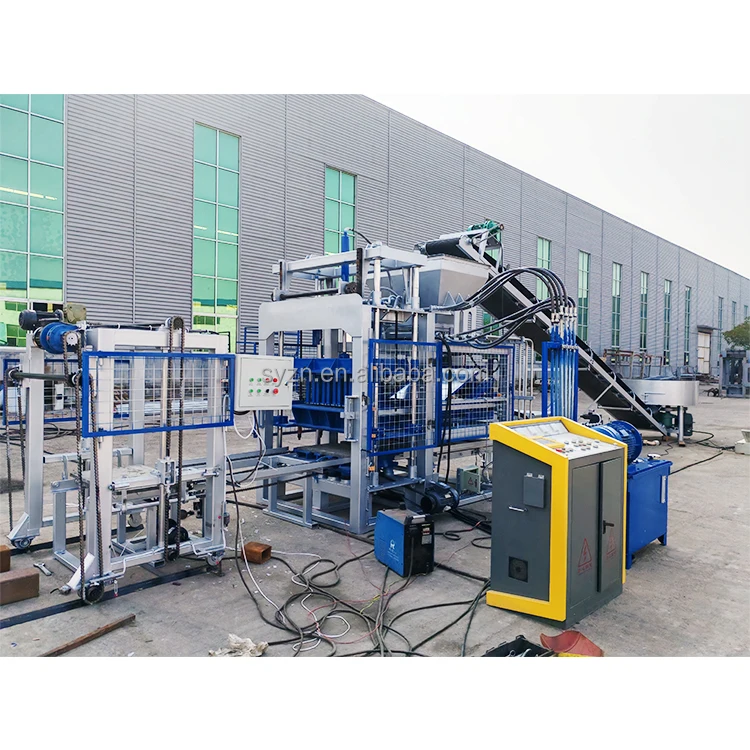
Description
Realistic output by format — Every capacity figure for the QT4-15 Automatic Concrete Block Making Machine is tied to a named block format and pallet size, never quoted as a bare hourly cycle count.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions | 4100×1600×2600 mm |
| Total Mass | 4 T |
| Rated Hydraulic Pressure | 16–21 MPa |
| Vibration Force | 55 kN |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format, material, and thickness) |
| Pallet Size | 880×550 mm |
| Overall Power | 18.45 kW |
| Demolding Method | Hydraulic |
| Factory Area Required | 300 m² |
| Raw Material Compatibility | Crushed stone, sand, cement, fly ash, gravel, slag, dust |
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Automation Level | Fully automatic |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential walls | Crushed stone, sand, and cement blends |
| Solid block manufacturing for load-bearing structures | Gravel and cement with fly ash additions |
| Interlocking paver production for driveways and walkways | Fine sand, cement, and colored pigments |
| Curbstone forming for road and pavement edges | Coarse aggregate and high-strength cement mixes |
| Porous brick output for permeable landscaping | Slag, dust, and cement combinations |
What "3000 Blocks a Day" Actually Means for the QT4-15
Cycle time only translates to real daily output when the block format, mix design, and pallet handling are all stated.
The QT4-15 block machine specifications often appear in brochures as a single throughput number, leaving out which block size and wall thickness that figure assumes [NEED_CITE: block machine capacity measurement standards]. When a technical buyer sizes a QT4-15 Automatic Concrete Block Making Machine for 400×200×200 mm hollow blocks but the quoted cycle was measured on a smaller solid paver, the molding cycle stretches and daily volume falls noticeably short of the printed claim. Matching vibration force and hydraulic pressure to local aggregate ensures the QT4-15 block machine specifications hold up in actual production rather than only on paper.
Pallet Size and Curing Area Alignment
The 880×550 mm pallet specified for this machine dictates how cured blocks move from the press to the yard. If the buyer’s existing forklift tines or curing racks were dimensioned for a different pallet footprint, every loaded pallet requires manual re-stacking before it enters the curing zone. Confirming pallet material — timber, composite, or steel — against local humidity and handling intensity prevents premature pallet warping that causes uneven block bottoms.
Mould Change-Over and Format Flexibility
A plant producing both hollow blocks and interlocking pavers on the same press needs a mould change procedure that fits within a single shift break. The QT4-15 block machine specifications should be accompanied by a documented mould change sequence listing the bolts, hydraulic lines, and PLC parameter swaps involved [NEED_CITE: mould change procedures in block making equipment]. Without that detail, a machine bought for format flexibility spends more time idle during changeovers than running the secondary product.
Vibration Force, Hydraulic Pressure, and Block Density
The 55 kN vibration force and 16–21 MPa rated hydraulic pressure work together to compact the mix into the mould cavity. Higher vibration frequency at 4200 r/min liquefies the concrete momentarily, while hydraulic pressure from above squeezes out air voids. If the local aggregate is angular crushed stone rather than rounded river gravel, the vibration amplitude and pressure dwell time must be adjusted to achieve the same block density and compressive strength. The QT4-15 Automatic Concrete Block Making Machine delivers consistent compaction only when these parameters are set against the actual mix design, not a generic default.
The Hidden Cost of Misconfigured Voltage and PLC Language
When voltage and frequency are not confirmed before production, a machine wired for 380 V / 50 Hz arrives at a site running 440 V / 60 Hz, burning out motors on the first test run [NEED_CITE: voltage and frequency standards by export market]. Similarly, a PLC display in a language the local operators cannot read turns every parameter adjustment into a guessing game. Both issues delay commissioning by weeks and shift the cost burden onto the buyer. The QT4-15 block machine specifications must include a written voltage, frequency, and control language confirmation before the machine leaves the factory.
Why Sourcing Through a Format-Focused Supplier Matters
Block machinery is the single focus here, so the QT4-15 Automatic Concrete Block Making Machine is specified as a matched system of press, mould, pallet, and handling rather than assembled from unrelated vendors. Machine configuration is set against the buyer’s actual mix design and target block format, replacing catalogue defaults with verified parameters. Custom mould design is available to buyer drawings for formats the local market demands. Automation level is selectable, allowing a semi-automatic start with a clear upgrade path to full stacking and cubing. Installation and commissioning support includes operator training on the specific formats loaded onto the machine.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format assumed for each output figure
- Mould drawing and format list covering every cavity profile supplied with the press
- Pallet specification sheet detailing size, material, and load rating per pallet
- Hydraulic and electrical schematic matching the confirmed voltage and frequency
- Factory test record filmed on the buyer’s target block format before dispatch
Installation, Commissioning & Support
- 300 m² factory area requirement verified against the buyer’s site plan before shipment
- 18.45 kW total power load confirmed against available supply and dedicated circuit capacity
- Platform vibration isolation pads sized for the 4 T machine mass and local floor slab rating
- First-run mould alignment and hydraulic pressure calibration on the buyer’s raw material blend
- Operator training covering PLC navigation, mould change procedure, and daily lubrication points
- Wear parts list with recommended reorder intervals for hydraulic seals and vibration springs
What to Include in a Technical Inquiry
Provide the target block format with exact dimensions, required compressive strength, and daily volume expectation. Include the locally available aggregate type and cement grade so the mix design can be matched to the 55 kN vibration force and 16–21 MPa hydraulic pressure. State the site voltage, frequency, and preferred PLC display language to ensure the QT4-15 block machine specifications align with the installation environment.
Frequently Asked Questions
Q: Which block format is assumed when a cycle time is quoted for the QT4-15?
A: Cycle time varies with block height, wall thickness, and mix stiffness. A quoted 25–30 second molding cycle must specify whether it was measured on a 400×200×200 mm hollow block, a thinner solid paver, or another format. Without that declaration, daily output calculations will not match real production.
Q: How should vibration force and hydraulic pressure match my local aggregate?
A: Angular crushed stone requires longer vibration dwell and higher hydraulic pressure than rounded river gravel to achieve the same density. The 55 kN vibration force and 16–21 MPa pressure range on the QT4-15 are adjusted against the buyer’s specific aggregate and cement ratio before the machine is finalized.
Q: What is the realistic mould change time between formats?
A: Mould change involves releasing hydraulic clamps, swapping the mould box, reconnecting vibration contacts, and updating PLC parameters. Actual changeover time depends on operator training and tool availability. A documented procedure should be requested so changeovers fit within a planned shift break.
Q: Does the 880×550 mm pallet fit my existing curing racks and forklift?
A: Pallet dimensions must be cross-checked against curing rack spacing and forklift tine width before order confirmation. If the buyer’s yard equipment was built for a different pallet footprint, every loaded pallet will need manual re-stacking, adding labour and slowing the curing cycle.
Q: Are voltage, frequency, and PLC language confirmed before production?
A: These three items must be agreed in writing before the machine enters assembly. A mismatch in voltage or frequency damages motors at first startup, and an unreadable PLC display prevents operators from adjusting cycle parameters. Written confirmation eliminates commissioning delays.