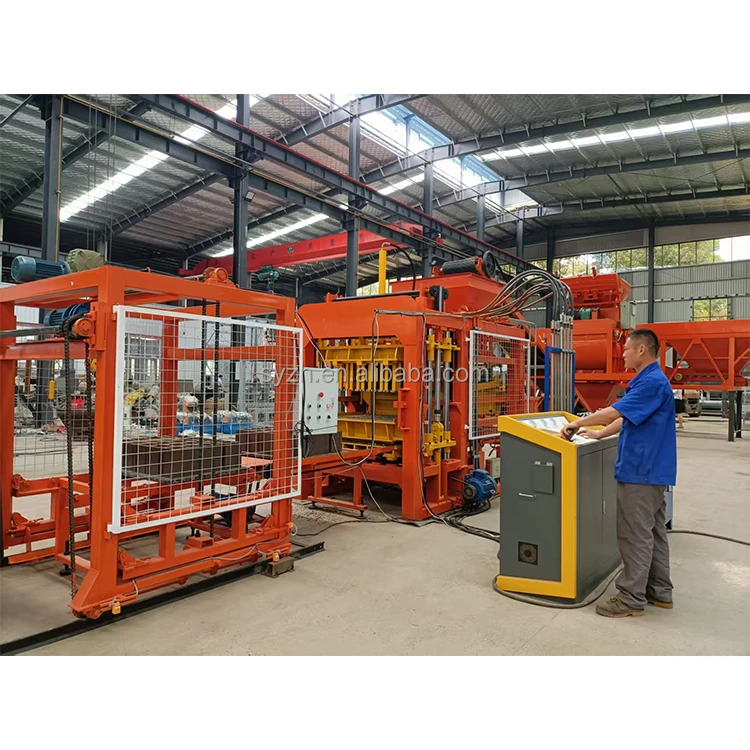
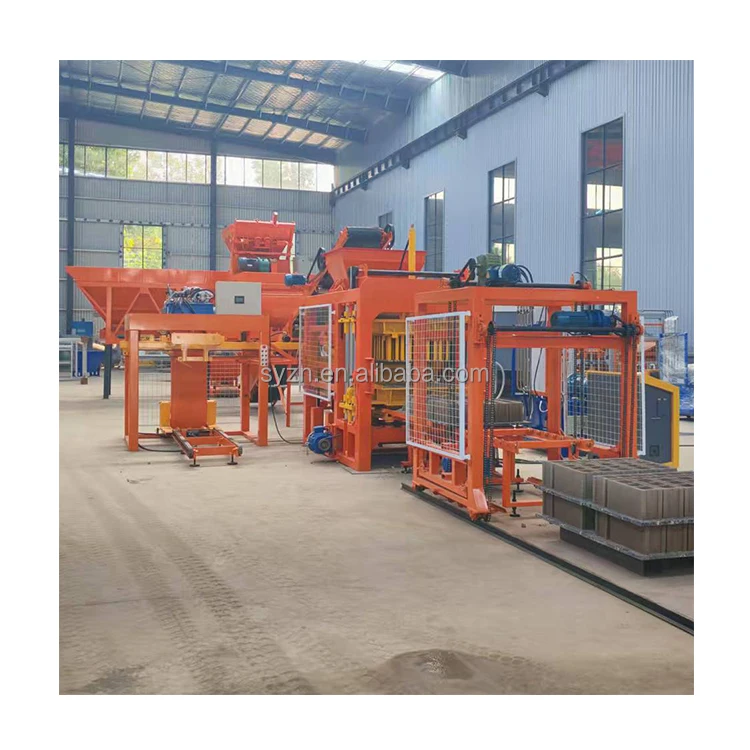
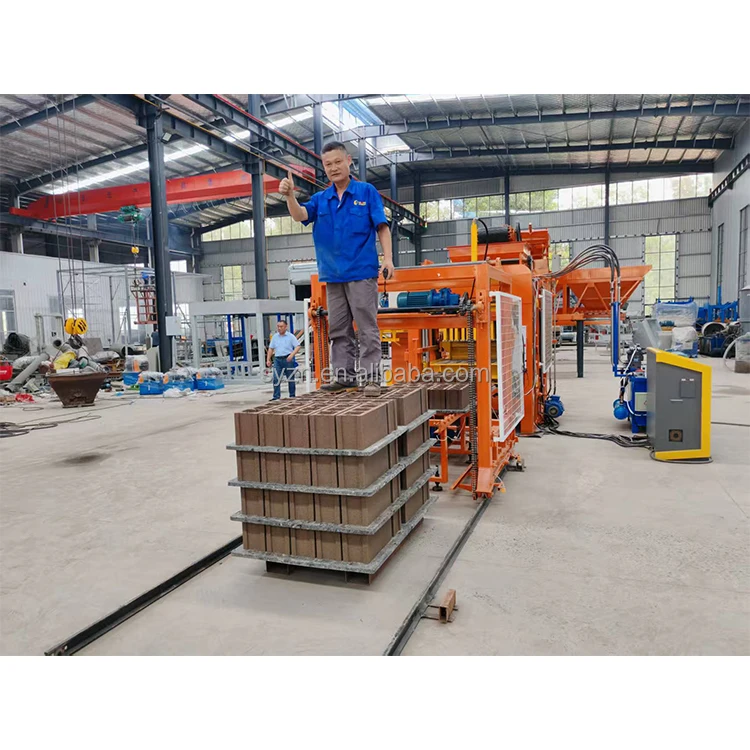
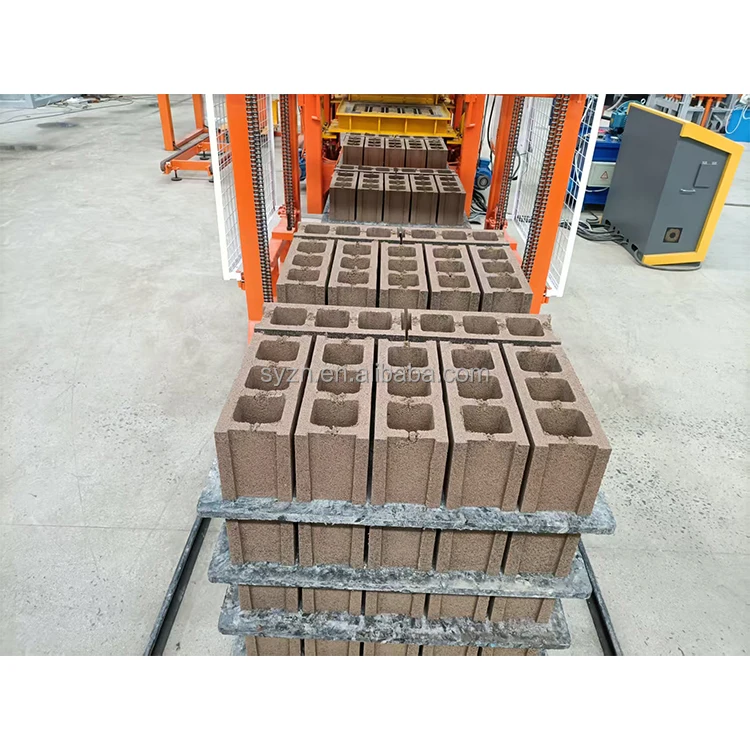


Description
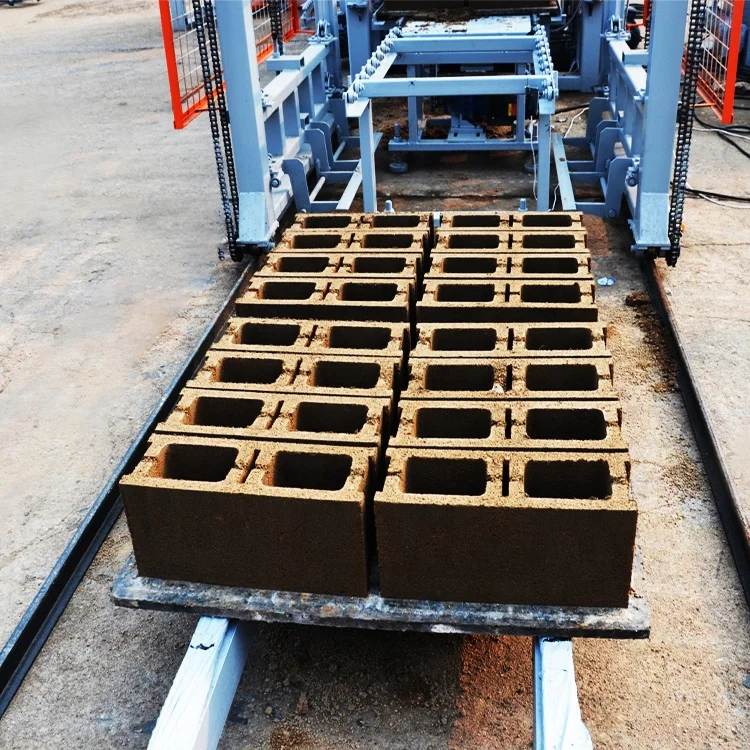
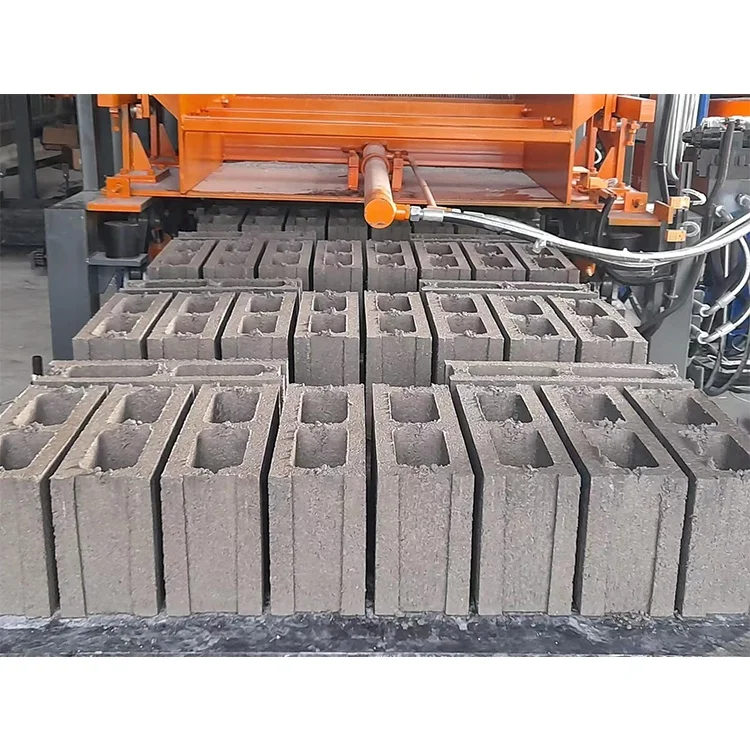
Format-Matched Capacity — Every QT6-15 proposal we issue ties cycle time and daily output to the buyer’s confirmed block format, local aggregate sample, and pallet handling layout, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Concrete Block Making Machine |
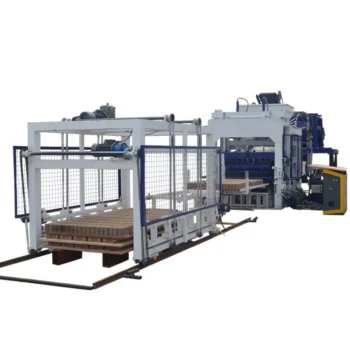
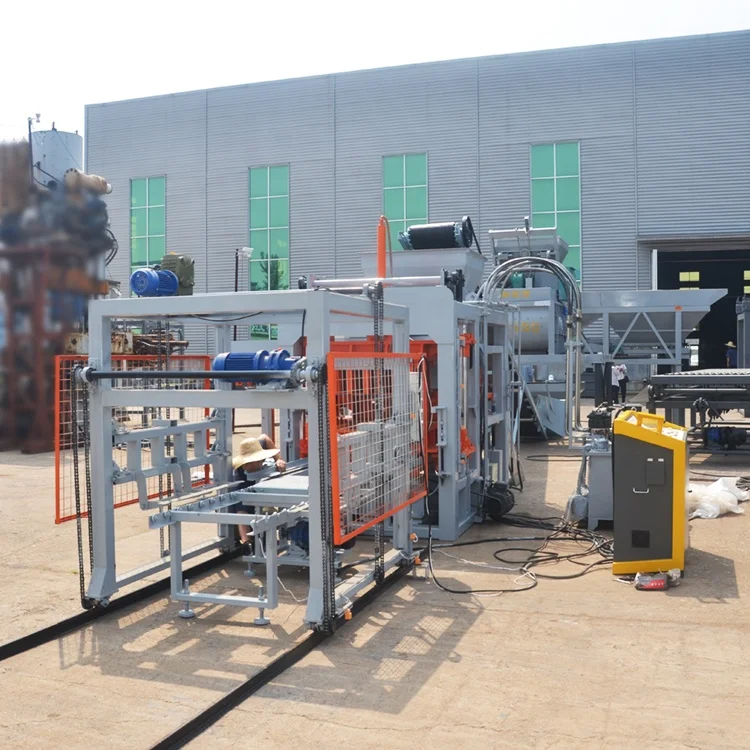
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Total Mass | 7 T |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 0–60 Hz |
| Vibration Force | 45 kN |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Hydraulic System | Independent integrated hydraulic station |
| Pallet Size | 880×850 mm |
| Molding Cycle | 15–20 s |
| Overall Power | 37 kW |
| Control System | PLC (Programmable Controller) with touch screen interface |
| Block Compressive Strength | >15 MPa |
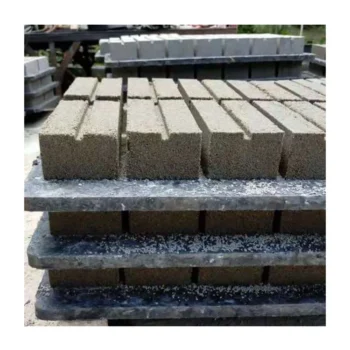
| Output — Hollow Block 400×200×200 mm | 1080–1440 pcs/h, 8640–11520 pcs/8 hr (basis: stated format) |
| Output — Hollow Block 400×150×200 mm | 1440–1920 pcs/h, 11520–15360 pcs/8 hr (basis: stated format) |
| Output — Solid Brick 240×115×53 mm | 5760–7680 pcs/h, 46080–61440 pcs/8 hr (basis: stated format) |
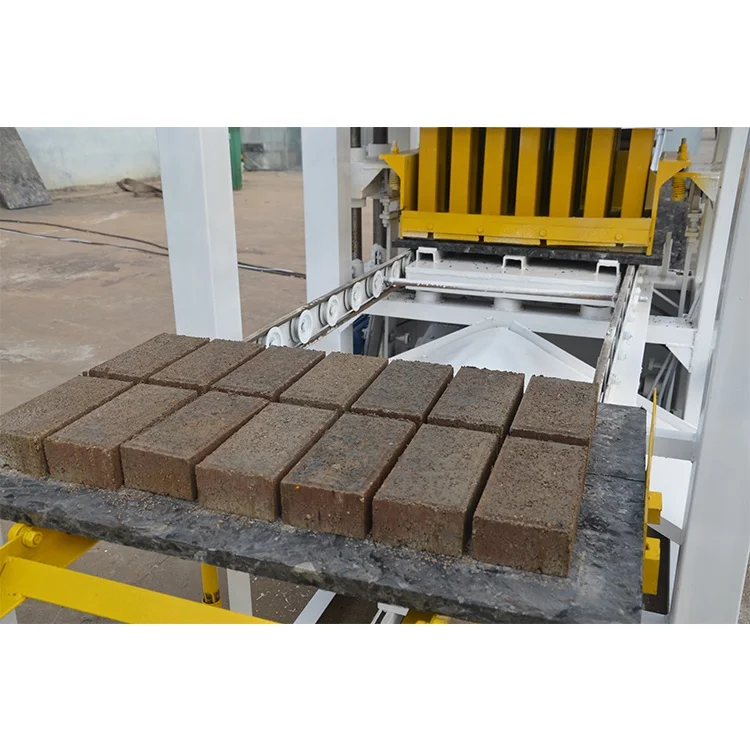
| Output — Rectangular Paver 200×100×60 mm | 2160–2880 pcs/h, 17280–23040 pcs/8 hr (cycle 20–25 s, basis: stated format) |
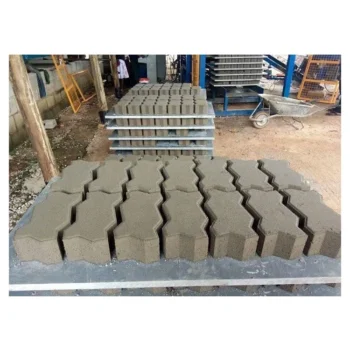
| Output — Zigzag Paver 225×112.5×60 mm | 2160–2880 pcs/h, 17280–23040 pcs/8 hr (cycle 20–25 s, basis: stated format) |
| Raw Material Adaptability | Waste ash, slag, conventional aggregates |
| Recommended Factory Area | 1200 m² |
| Voltage & Frequency | To be confirmed per site |
| PLC Display Language | To be confirmed per buyer |
| Mould Change Time | To be confirmed per mould set |
| Hydraulic Pressure | To be confirmed per configuration |
| Certification | CE (specific certificate to confirm) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production — load-bearing and non-load-bearing | Conventional concrete, ash-based or slag-based mixes |
| Solid brick production | Standard concrete or blended aggregate mixes |
| Rectangular paving block production | Concrete with fine aggregate, pigmented or plain |
| Interlocking / zigzag paver production | Concrete with fine aggregate, colour-compatible mixes |
| Waste material recycling into blocks | Fly ash, slag, crushed construction waste blended with cement |
Why a Single Headline Capacity Figure Misleads QT6-15 Buyers
The only honest QT6-15 block machine specifications sheet is one that lists capacity separately for every block format the buyer intends to run.
I learned this on a job in Central America where a contractor had ordered a block machine based on a brochure figure quoted in "cycles per hour" — with no mention of which block size that assumed. When the machine arrived and ran 400×150×200 hollow blocks instead of the smaller format the brochure had silently assumed, daily output dropped to roughly sixty percent of what the project schedule required. The contractor was left paying overtime and renting extra curing space to catch up [NEED_CITE: common discrepancies between brochure capacity and site output in block making equipment]. That experience shaped how I now approach every QT6-15 configuration: the capacity table must show a separate row for each format, with its own cycle time, so the buyer sees exactly what the machine will produce in their actual product mix.
Matching Mould Format to the Market the Buyer Actually Serves
The QT6-15 block machine specifications cover a range of block formats, but not every format will be relevant to every market. A buyer whose primary revenue comes from 400×150×200 hollow blocks needs to see that format’s cycle time — 15–20 seconds per mould cycle — and the corresponding output of 1440–1920 pieces per hour calculated on that basis. If the same buyer plans to add rectangular pavers later, the cycle shifts to 20–25 seconds and the pallet coverage changes entirely, which affects downstream curing rack density.
How Pallet Size Determines Everything Downstream
The 880×850 mm pallet is not an arbitrary number. It dictates the curing rack dimensions, the forklift tine spacing, and the stacking pattern in the yard. A buyer who already operates a curing system designed for a different pallet size will face costly retrofitting or double-handling. Before finalising any QT6-15 configuration, we confirm the buyer’s existing pallet infrastructure and yard layout so the machine integrates without creating a bottleneck at the stacking station [NEED_CITE: pallet handling integration in concrete block production lines].
Vibration Force, Hydraulic Pressure, and the Density Equation
Block compressive strength above 15 MPa does not come from the hydraulic system or the vibration system alone — it requires both working in concert. The QT6-15 delivers 45 kN of vibration force at a frequency range of 0–60 Hz through platform vibration, while an independent integrated hydraulic station handles demolding and pressure application. When processing heavier mixes such as slag-based or high-ash blends, the vibration frequency and hydraulic pressure must be tuned together; setting one without adjusting the other produces blocks with inconsistent density across the pallet. The PLC touch-screen control allows operators to store parameter sets for different mix designs, reducing batch-to-batch variation when switching between conventional aggregate and waste-material blends.
What Happens When Configuration Is Skipped
Ordering a QT6-15 based on price and headline capacity alone creates downstream costs that appear only after installation. If the voltage and frequency are not confirmed against the site supply before production, the motor and PLC may not communicate correctly on arrival, delaying commissioning by days or weeks. If the mould set does not match the buyer’s primary market format, the machine sits idle while a replacement mould is manufactured and shipped. And if the pallet specification — material, thickness, and size — is chosen without checking the buyer’s curing racks and forklift, every pallet must be manually repositioned before it enters the yard, adding labour the buyer never budgeted for [NEED_CITE: equipment specification mismatches and commissioning delays in industrial machinery exports].
Why Technical Buyers Source the QT6-15 Here
Every QT6-15 proposal starts with the buyer’s target block format, daily output requirement, and a sample of the local raw material. The capacity calculation we return states output per format, not a single blended figure.
Mould design covers the formats the buyer’s market actually demands, including custom drawings when standard moulds do not match the required dimensions or interlocking profile.
The automation level is selectable, allowing a buyer to begin with semi-automatic pallet handling and add automatic stacking and cubing as volume justifies the investment.
Configuration accounts for the buyer’s actual mix design and aggregate source rather than defaulting to a catalogue recipe, which protects block strength consistency from the first production run.
Installation, commissioning, and operator training are included so the machine reaches stable production with the buyer’s own crew running it.
Documentation & Verification
- Line layout with capacity calculation tied to the buyer’s confirmed block format and cycle time
- Mould drawing and format list showing every included mould with changeover procedure
- Pallet specification covering size, material, and thickness matched to the buyer’s curing system
- Hydraulic and electrical schematic for the independent integrated station and PLC wiring
- Voltage, frequency, and PLC display language confirmation sheet signed before production
- Factory test record run on the buyer’s specified format before container loading
Installation, Commissioning & Support
- Foundation plan sized for the QT6-15 footprint of 8200×1700 mm with vibration isolation requirements
- Dedicated power circuit rated for the 37 kW overall power draw, voltage and frequency confirmed pre-production
- Machine dismantled into container-load sections with reassembly sequence documented per unit
- First-run parameter tuning on the buyer’s mix design, adjusting vibration frequency and hydraulic pressure together
- Operator training on the PLC touch-screen interface including fault diagnosis logic and action interlocks
- Wear parts and mould maintenance schedule with replacement intervals for the buyer’s production volume
What We Need to Configure Your QT6-15
To prepare an accurate QT6-15 block machine specifications proposal, share the primary block format your market demands along with the target daily output for that format. Provide a sample or analysis of your local aggregate — whether conventional crushed stone, fly ash, or slag — so vibration and hydraulic parameters can be set correctly. Confirm your site voltage, frequency, and preferred PLC display language so commissioning proceeds without delay upon arrival.
Frequently Asked Questions
Q: How is QT6-15 capacity calculated per block format, and why does the same machine produce different hourly outputs for hollow block versus paver?
A: Each format occupies a different area on the 880×850 mm pallet and requires a different moulding cycle. The 400×200×200 hollow block runs at 15–20 seconds per cycle yielding 1080–1440 pcs/h, while rectangular pavers need 20–25 seconds per cycle at 2160–2880 pcs/h because more units fit per pallet. Honest capacity reporting states each format separately.
Q: Which mould formats come with the QT6-15, and how does a mould change work on site?
A: The standard scope is configured around the buyer’s confirmed primary format, with additional moulds quoted based on the buyer’s product range. Mould change involves releasing the clamping system, lifting the old mould, positioning the new one, and recalibrating vibration and hydraulic parameters through the PLC. Exact changeover time depends on the mould set and must be confirmed per configuration.
Q: How should the 880×850 mm pallet be matched to existing curing racks and forklifts?
A: The pallet dimensions must align with curing rack slot width and forklift tine spacing. If a buyer’s existing racks were built for a different pallet size, either the racks need modification or pallets need to be double-handled. We confirm pallet material, thickness, and size against the buyer’s yard layout before finalising the QT6-15 order.
Q: What mix designs has the QT6-15 been configured for, and how does vibration force need adjusting?
A: The machine handles conventional concrete, fly ash blends, and slag-based mixes. Heavier or more abrasive blends like slag require adjustments to both the 0–60 Hz vibration frequency and hydraulic pressure in tandem. The PLC allows operators to store separate parameter sets for each mix, maintaining block compressive strength above 15 MPa across different recipes.
Q: What documentation ships with the QT6-15 to support commissioning and maintenance?
A: Every unit ships with a line layout and capacity calculation by format, machine specification sheet, mould drawings, pallet specification, hydraulic and electrical schematics, voltage and PLC language confirmation, factory test record, operation and maintenance manual, and a wear parts and mould list with replacement references.