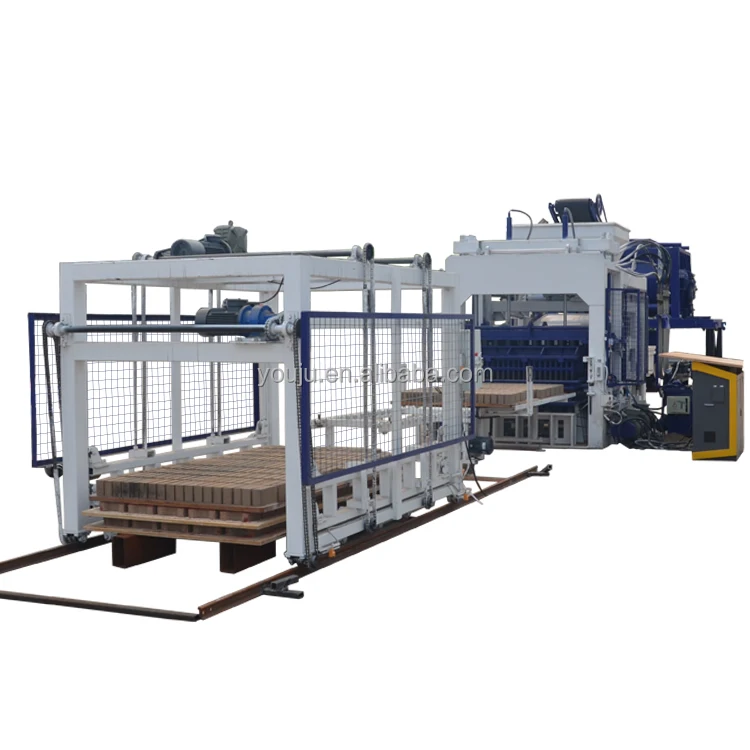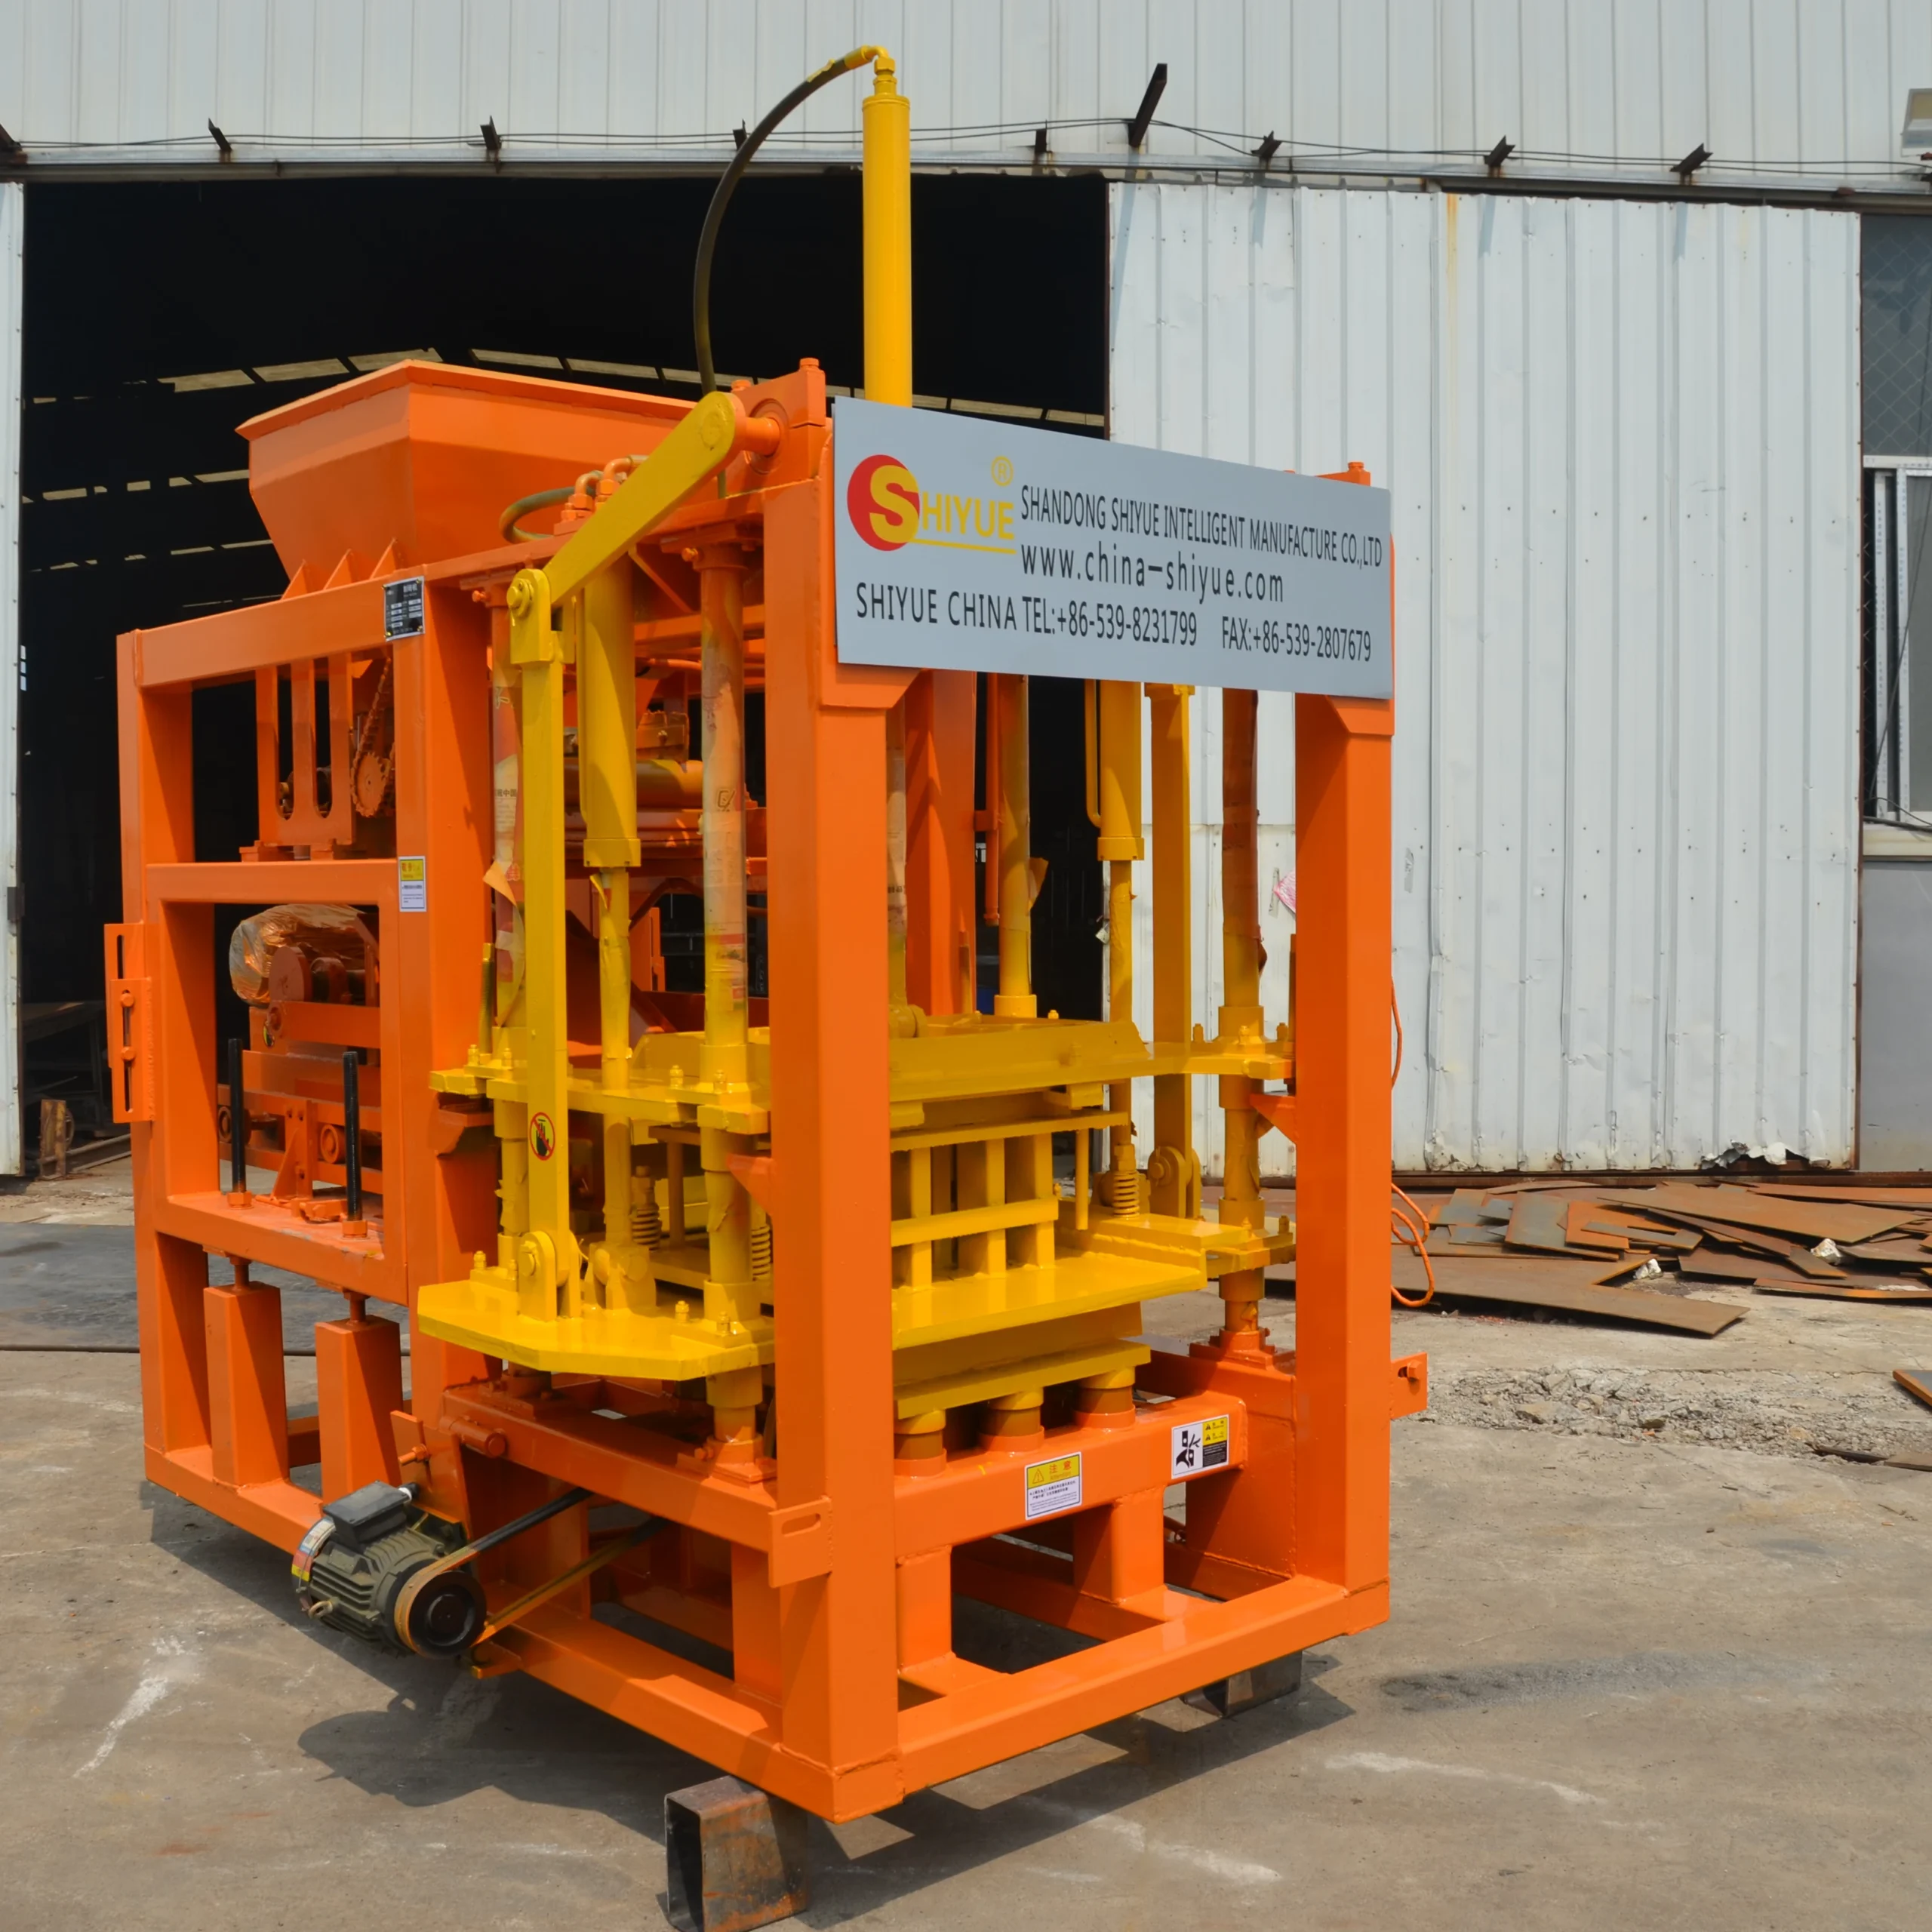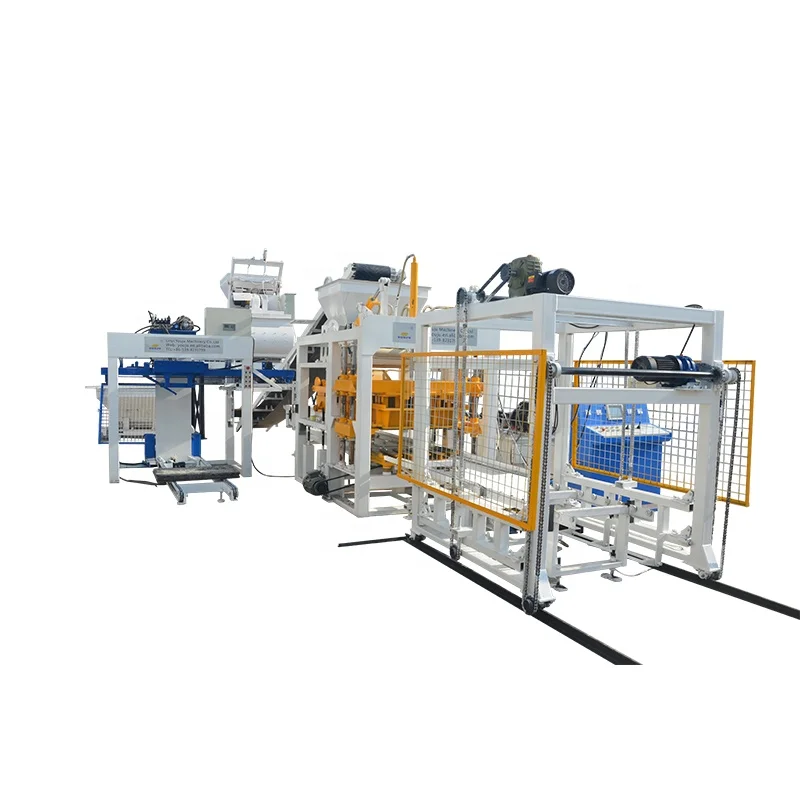
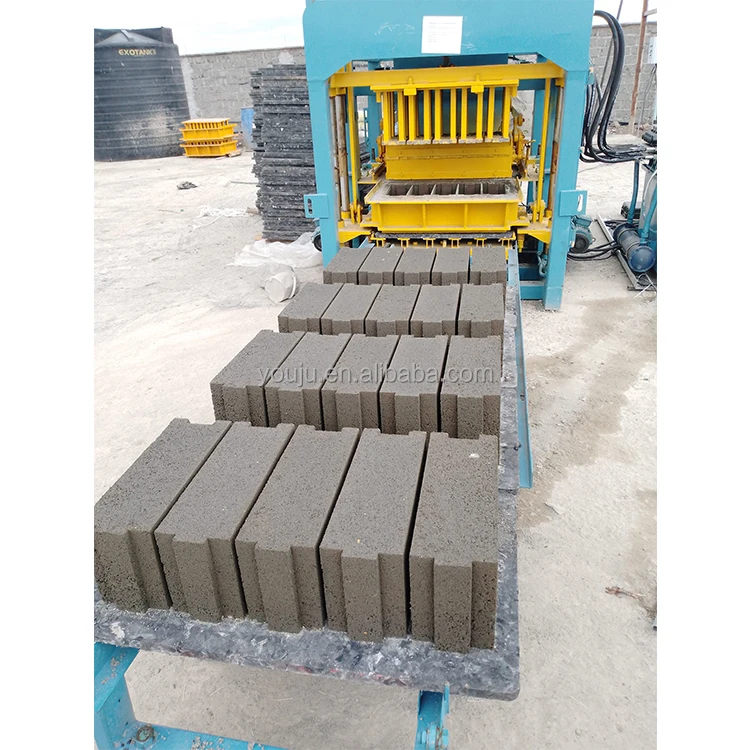

Description
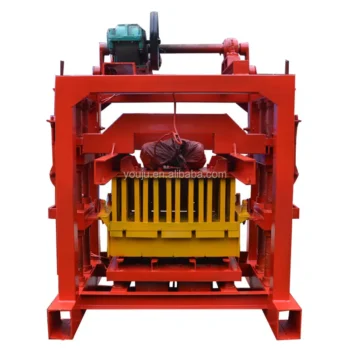
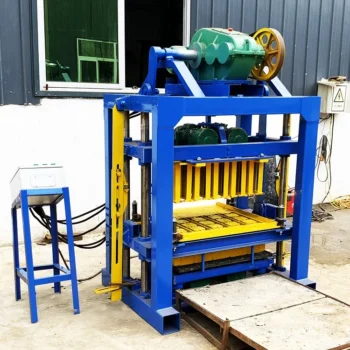
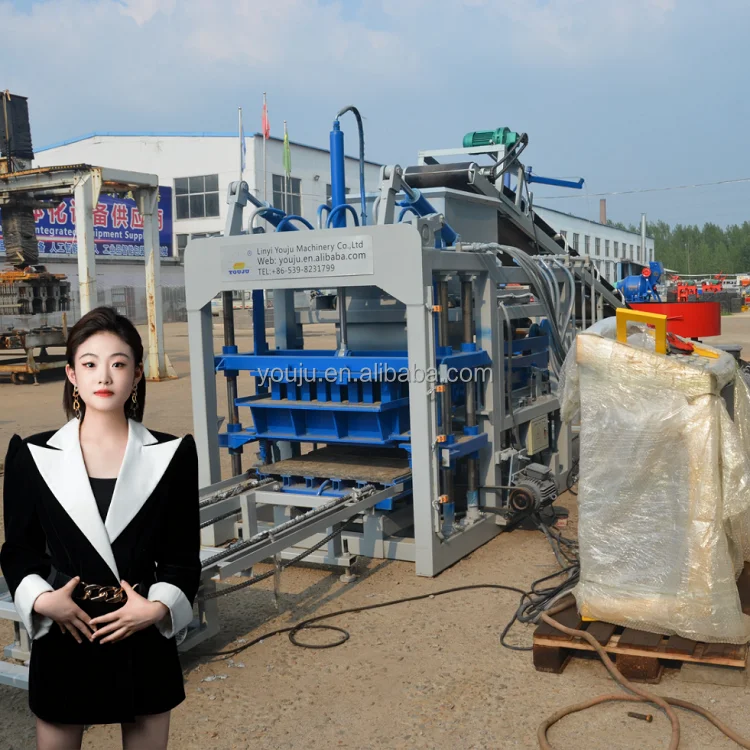
Matched Mould Configuration — Every QT4-15 block machine ships with pallet size, vibration force and hydraulic pressure aligned to the buyer’s local aggregate and target block format, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Stationary block machine |
| Vibration Force | Hydraulic and vibration combined system |
| Mould Compatibility | Hollow, solid, paving, interlocking, kerbstone formats |
| Pallet Size | Configurable to curing area and existing forklift dimensions |
| Control System | PLC control with selectable display language |
| Voltage & Frequency | Configurable to buyer’s local grid standard |
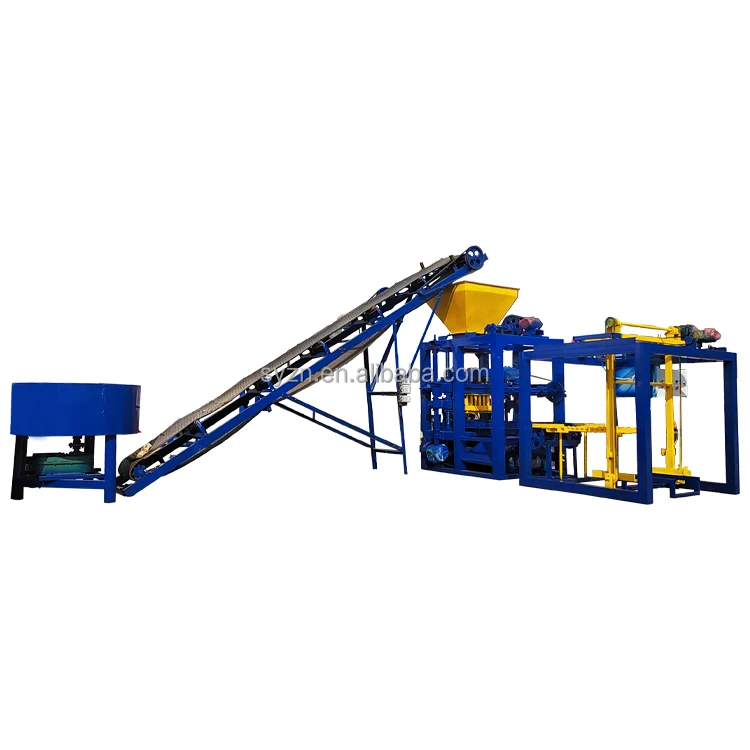
| Degree of Automation | Semi-automatic to fully automatic stacking and cubing |
| Cycle Time | Varies by block format and mix design (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement and water mix |
| Solid block production | Local aggregate with cement binder |
| Paving block and kerbstone | High-density mix with fine aggregate |
| Interlocking brick | Coloured or standard concrete mix |
| Porous brick | Permeable aggregate blend for drainage applications |
What "Cycles Per Hour" Leaves Out About Block Output
Capacity figures only mean something when tied to a specific block format and mix design.
Many quotations quote a peak cycle rate without stating whether that assumes a small solid block or a large hollow format. A machine running 400×200×200mm hollow blocks completes far fewer pieces per shift than the same press running 200×100×60mm paving bricks. I have watched buyers invest based on a headline number, then discover the real daily output of a Cement QT4-15 Block Making Machine falls well short once the actual product format enters the calculation. The mix design, vibration duration and hydraulic dwell all shift when you change formats. [NEED_CITE: block format impact on realistic cycle time]
Matching the Machine to Your Market Format
The block your market actually buys dictates everything downstream of the press. If hollow blocks dominate local construction, the mould portfolio and pallet size must reflect that volume. Switching to paving blocks later means new moulds, possibly different pallets, and a revised vibration profile. A buyer planning to run multiple formats needs to know upfront how long a mould change takes and whether the hydraulic system can adjust between formats within a single shift.
Honest Capacity Calculation per Format
Every capacity statement on a Cement QT4-15 Block Making Machine should name the block format, the mix design and the curing assumption behind it. Without those three variables pinned down, the number is a guess. Buyers comparing quotations from different suppliers should ask each one to state which format their quoted output assumes. A realistic daily output table, listing each block type the buyer intends to produce, prevents surprises after installation. [NEED_CITE: importance of format-specific capacity disclosure]
Reading the Spec Sheet for Production Impact
Vibration force and hydraulic pressure work together to compact the concrete mix into the mould. Higher vibration reduces air voids, but without adequate hydraulic hold the block can relax and lose density before ejection. Pallet size determines how many blocks form per cycle and must match the curing rack spacing and the forklift tines already in the yard. The PLC control language affects how quickly a local operator can troubleshoot a fault without calling the supplier. Voltage and frequency confirmation before production avoids a machine that sits idle while transformers are sourced locally.
The Cost of Ignoring Configuration Details
When pallet size is chosen without checking the buyer’s existing curing racks, blocks end up stacked by hand until new racks arrive. An unconfirmed voltage specification can delay commissioning by weeks if the local grid does not match the motor rating. Moulds ordered in a format the local market does not buy sit unused while the buyer waits for replacements. These are not theoretical problems; they appear regularly in post-delivery support conversations. [NEED_CITE: common commissioning delays from unconfirmed electrical specs]
Why Buyers Specify Here Before Ordering
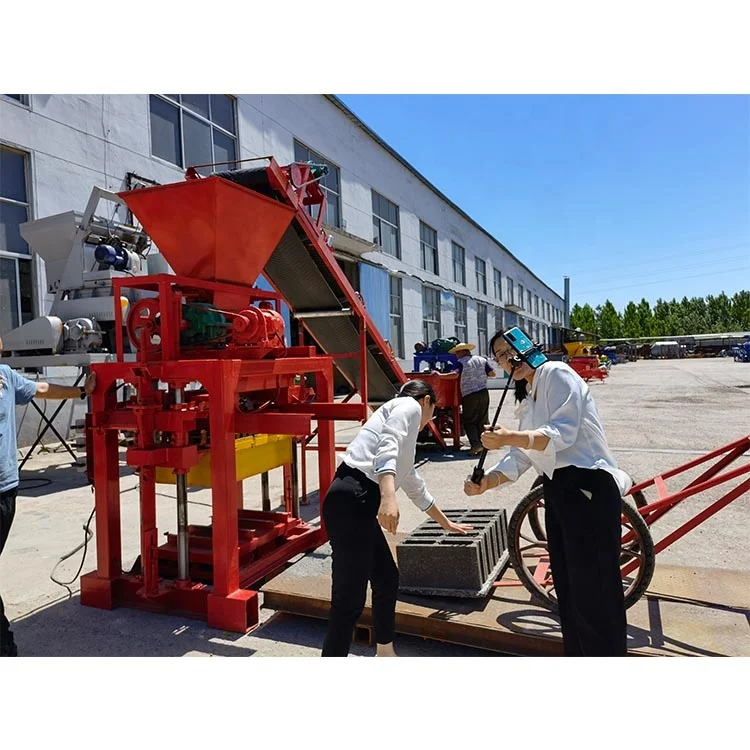
Block machinery is the single focus of this operation, so the press, moulds, pallets and handling equipment are specified as one matched system rather than assembled from separate suppliers. The Cement QT4-15 Block Making Machine configuration is set against the buyer’s actual mix design and local aggregate, not a generic catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings when standard formats do not fit. Automation level is selectable, allowing a buyer to start semi-automatic and add stacking or cubing later. Installation includes operator training so the team can run the line independently from day one.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed
- Machine specification sheet with hydraulic and vibration ratings
- Mould drawing and format list for every included mould
- Pallet specification matched to curing area dimensions
- Voltage, frequency and PLC display language confirmation record
- Factory test record on buyer’s target block format before dispatch
Installation, Commissioning & Support
- Foundation drawing provided based on machine footprint and vibration load
- Dedicated power circuit sized to the confirmed motor rating and starting current
- Machine shipped in dismantled state with reassembly guide and labelled connections
- First-run parameter setting on the buyer’s local aggregate and target format
- Operator training covering mould change, PLC fault reading and daily maintenance
- Wear parts and mould list supplied with recommended replacement intervals
What to Include in Your Inquiry
To size the line accurately, share the block formats your market demands and the daily volume for each. Confirm the local aggregate types available and the cement source. State the site voltage, frequency and any existing handling equipment such as forklifts or curing racks that the new line must integrate with.
Frequently Asked Questions
Q: How long does a mould change take on this machine?
A: Mould change time depends on the format size and the clamping system fitted. The quotation includes a stated changeover duration for each mould supplied, so you can plan shift schedules around the formats you run most often.
Q: Can the pallet size be changed after delivery?
A: Pallet size is set during configuration to match your curing racks and forklift. Changing pallet size later requires new pallets and may need mould adjustments, so it is better to confirm the size before production.
Q: What happens if my local voltage differs from the standard?
A: Voltage and frequency are confirmed before production begins. The motor, control panel and PLC are built to your local grid specification, avoiding the need for external transformers after arrival.
Q: Is it possible to add automatic stacking later?
A: The automation level is selectable at order and can be upgraded. A semi-automatic line can receive a stacker and cubing unit later if the foundation space and pallet return system were planned for that expansion path.