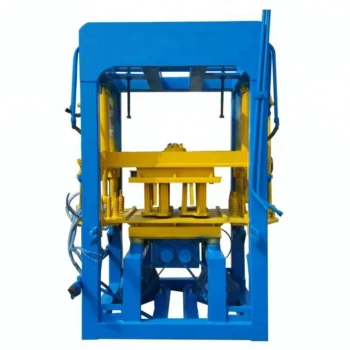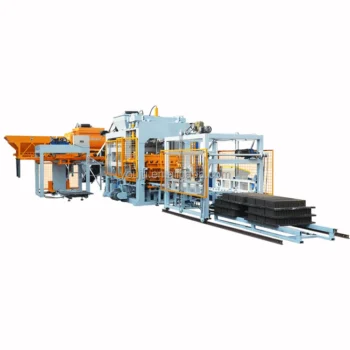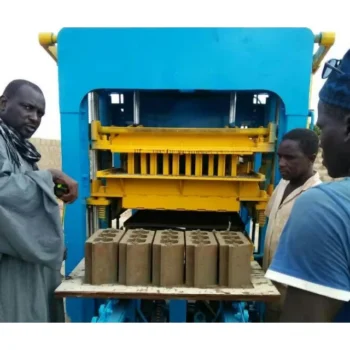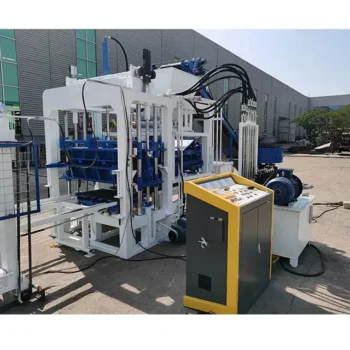
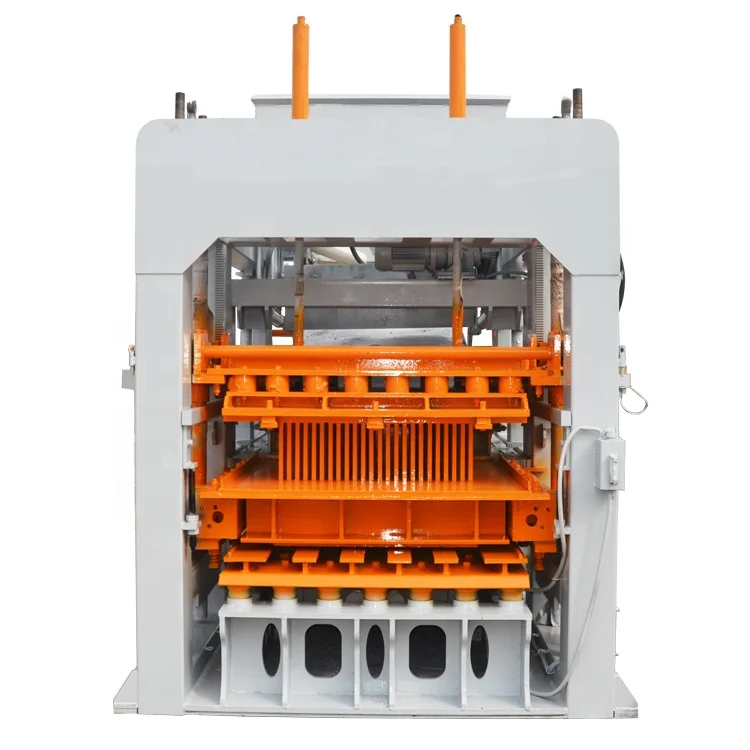
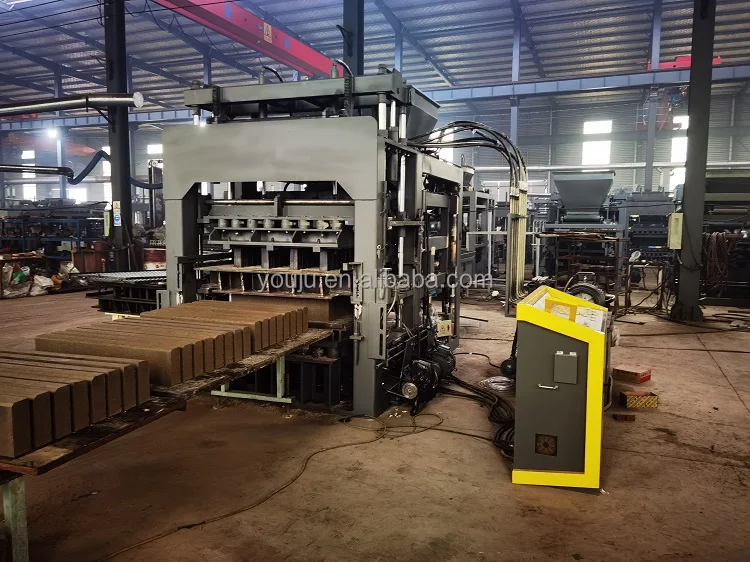
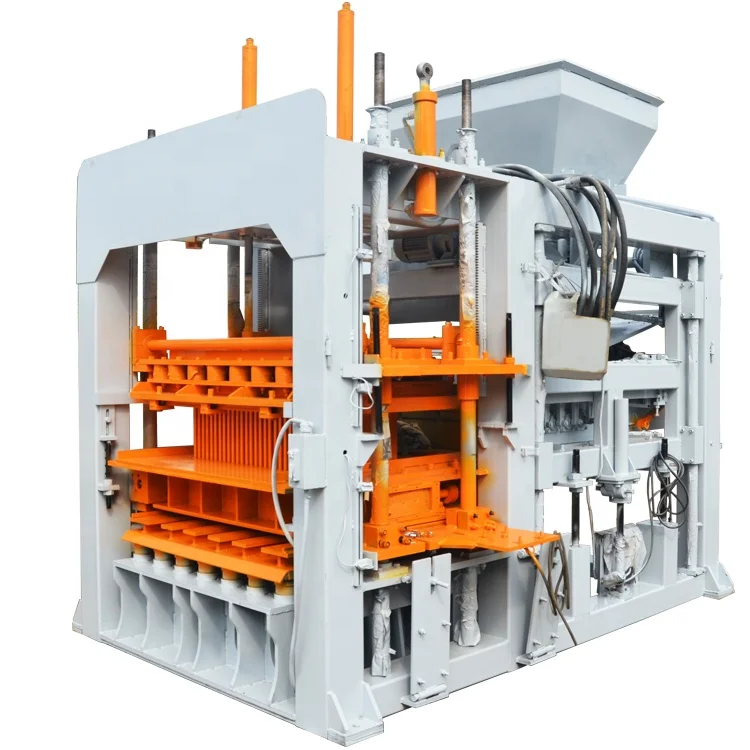
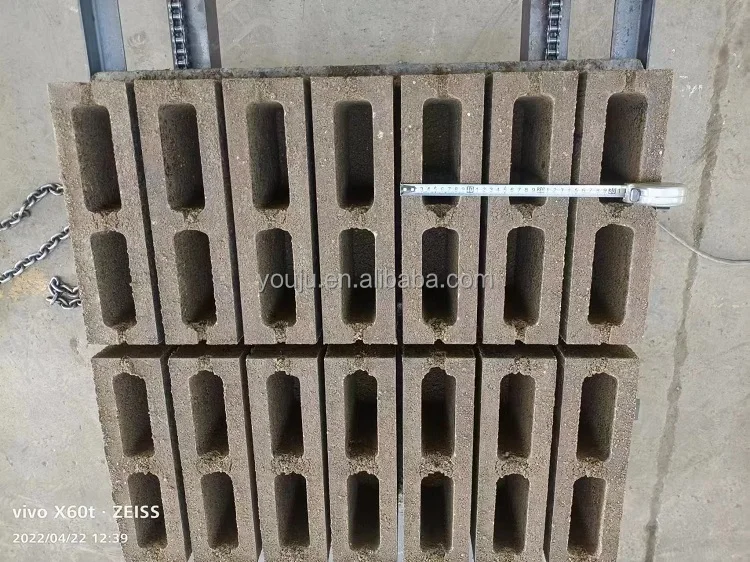
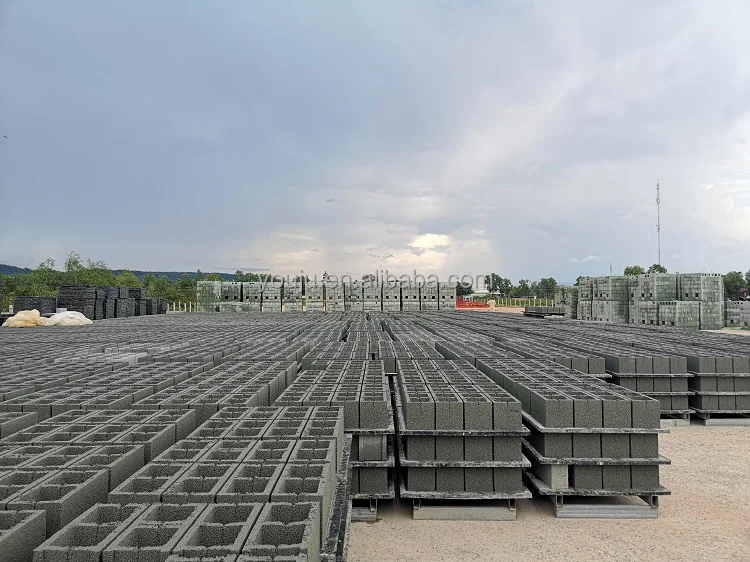
Description
Matched to Your Mix — every QT8-15 configuration starts with the buyer’s actual aggregate sample and target block format, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Forming Method | Hydraulic pressure with vibration system |
| Forming Cycle | 15-20 s (basis not stated in source — confirm block format, material and thickness) |
| Output — Hollow Block 400×200×200 mm | 1 600-1 900 pcs / h, 12 800-15 000 pcs / 8 h (8 pcs per mould) |
| Output — Solid Brick 240×115×53 mm | 8 000-10 000 pcs / h, 64 000-80 000 pcs / 8 h (45 pcs per mould) |
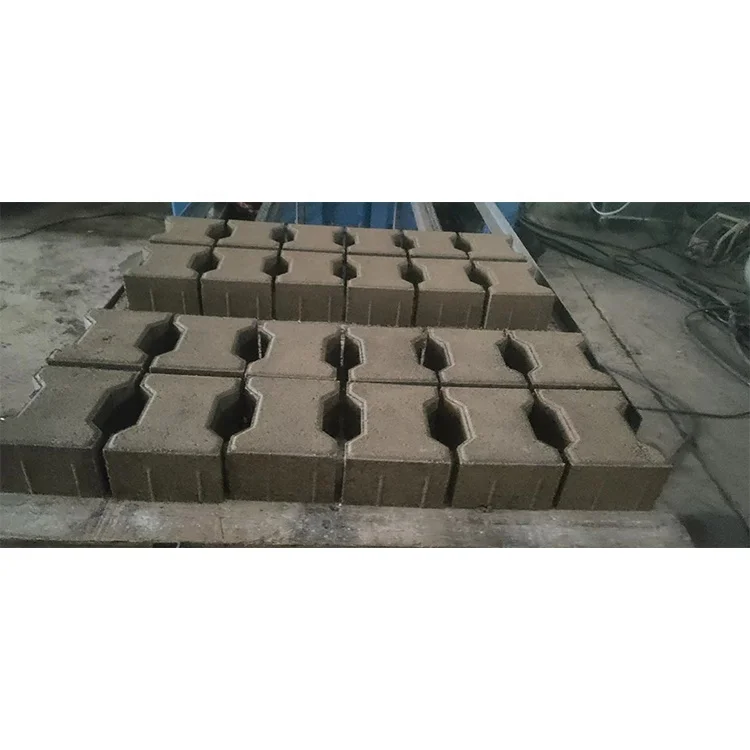
| Output — Paver Brick 200×160×60 mm | 3 000-3 600 pcs / h, 24 000-28 800 pcs / 8 h (15 pcs per mould) |
| Output — Interlocking Brick 225×112.5×60 mm | 4 000-5 000 pcs / h, 32 000-40 000 pcs / 8 h (24 pcs per mould) |
| Mould Compatibility | Hollow block, solid brick, paver brick, kerbstone (mould change required) |
| Mould Treatment | Heat treatment for extended working life |
| Automation Level | Automatic (source value — verify against manufacturer catalog) |
| Rated Power | To be confirmed at quotation stage |
| Voltage & Frequency | Configurable to buyer’s site supply |
| Control System | PLC (brand and display language to be confirmed) |
| Pallet Size | To be matched to curing area and forklift |
| Warranty | 1 year |
| After-sales Support | 24-hour online technical support; on-site installation and operator training available |
Application Suitability
| Application | Typical Output Scope |
|---|---|
| Hollow block production from crushed stone, sand and cement | Wall blocks 400×200×200 mm for residential and commercial construction |
| Solid brick runs from local aggregate blends | 240×115×53 mm bricks for load-bearing and infill masonry |
| Paver and kerbstone manufacturing | 200×160×60 mm pavers and kerbstones for roads, walkways and parking areas |
| Interlocking brick production for slope and channel lining | 225×112.5×60 mm interlocking units for erosion control and retaining walls |
| On-site block production by housing project contractors | Format switching between hollow block and solid brick within a single project phase |
Why "Pieces per Hour" Without a Block Format Misleads Buyers
A cycle time only becomes meaningful once the block format, mould cavity count and mix design are pinned down.
I learned this the hard way when I specified a high-output block press for a West African project using standard river sand test data. The customer’s site ran volcanic ash aggregate with completely different particle geometry. Vibration parameters had to be re-tuned on-site for over two weeks before block strength met specification [NEED_CITE: aggregate particle shape influence on vibration compaction]. The QT8-15 block machine specifications table above lists four distinct formats, each with its own cavity count and resulting hourly output. A buyer who only sees a headline cycle figure without checking which format it assumes will plan curing space, pallet inventory and labour around a number that never materialises in daily production.
Capacity Breakdown That Respects Your Product Mix
When a technical buyer evaluates the QT8-15 concrete block making machine how to choose between output tiers, the first step is listing the exact formats the local market actually purchases. A hollow block line running eight cavities per cycle delivers a different daily volume than a paver run with fifteen cavities, even on the same press. Stating cycle time per format removes the guesswork from shift planning.
Matching Vibration and Pressure to Local Aggregate
Hydraulic pressure and vibration force must work together against the specific friction and moisture characteristics of the buyer’s raw materials. A mix that flows easily under vibration in one region may resist compaction in another due to angular aggregate or high fines content [NEED_CITE: hydraulic vibration compaction principles for concrete masonry]. Sending a representative aggregate sample before final machine configuration allows the vibration amplitude and pressure dwell to be set on the factory floor rather than adjusted through trial and error after arrival.
Reading the Specs That Matter Most
Forming cycle of 15-20 seconds is a range, not a fixed value, because thickness, aggregate gradation and target block density all shift the time needed for full compaction. Mould heat treatment extends service life across repeated format changes, but the actual mould change time on-site depends on the clamping system and operator familiarity — a detail worth confirming before purchase. Pallet size must align with the curing rack spacing and the lift capacity of the forklift already in the yard; a mismatch here forces manual re-stacking and erases any throughput gain from the press itself. The PLC control language should be locked in before production so operators can read alarms and adjust parameters from day one [NEED_CITE: PLC interface language requirements in export machinery contracts].
The Cost of Skipping Configuration Details
When voltage and frequency are assumed rather than confirmed, the machine arrives with motors wound for the wrong supply, and commissioning stalls until replacement components ship. When pallet dimensions are chosen without checking the curing rack pitch, half the rack slots go unused and output piles on the floor. When the mould change procedure is not reviewed in advance, a format switch that should take minutes stretches across an entire shift, negating the flexibility the buyer paid for [NEED_CITE: mould change best practices in multi-format block plants].
Why Sourcing the QT8-15 Here Reduces Configuration Risk
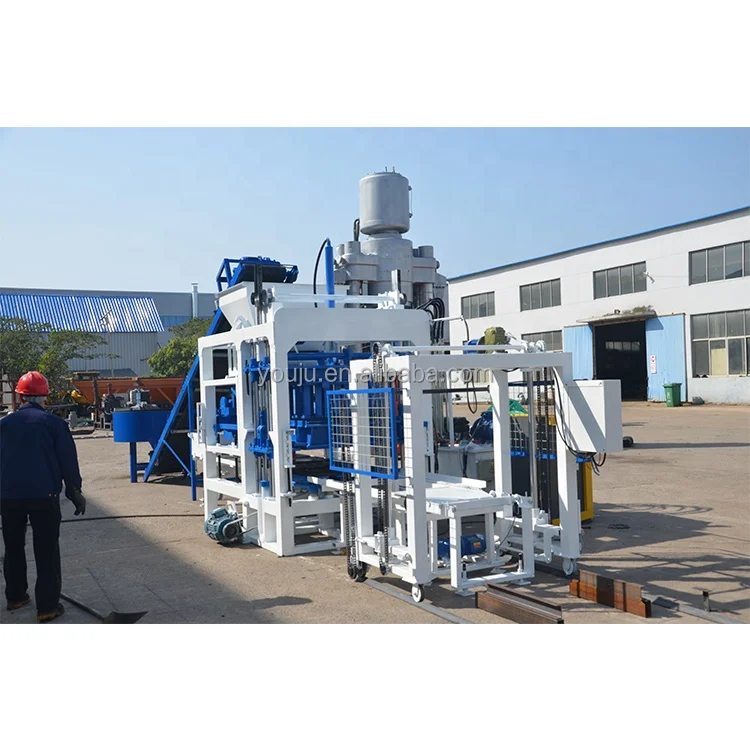
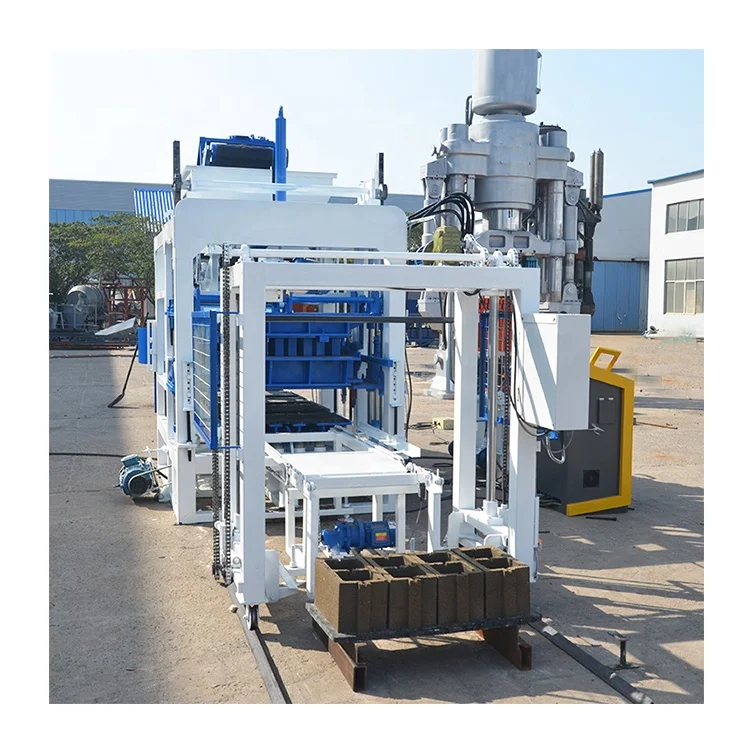
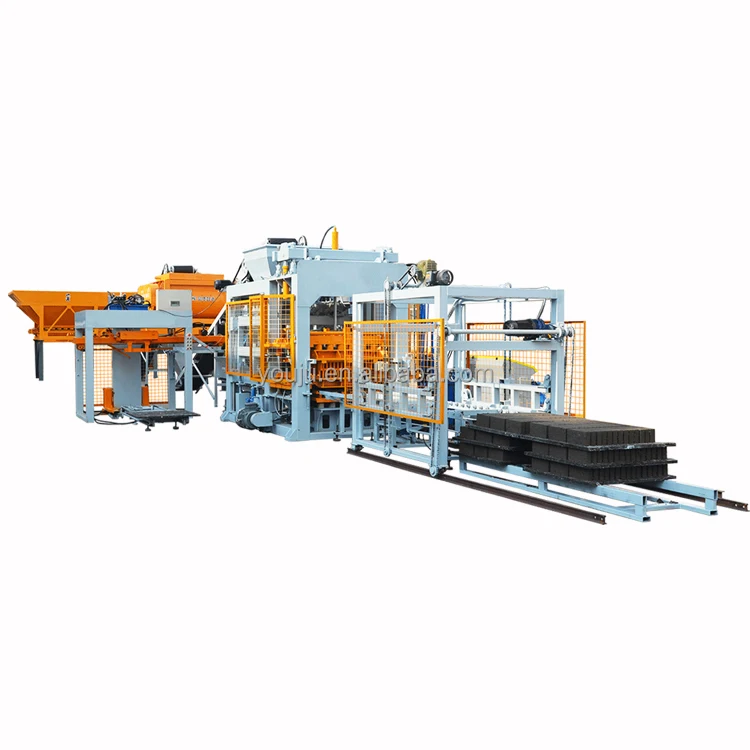
Block machinery is the sole product focus, so the press, mould, pallet and handling equipment are specified as one matched system rather than sourced separately. Machine settings are calibrated against the buyer’s submitted mix design and target block format instead of a generic factory default. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard cavities do not fit. Automation level is selectable, allowing a semi-automatic start with a defined upgrade path to full stacking and cubing. Installation includes on-site commissioning and operator training so the crew can run independent shifts before the technician leaves.
Documentation & Verification
- Line layout drawing showing each station and the block format assumed for capacity calculation
- Machine specification sheet with confirmed voltage, frequency and PLC display language
- Mould drawing and format list covering every cavity the buyer will run
- Pallet specification matched to curing rack pitch and forklift load rating
- Factory test record run on the buyer’s submitted aggregate sample before crating
Installation, Commissioning & Support
- Foundation plan sized to the QT8-15 footprint and dynamic vibration load
- Dedicated circuit requirement confirmed against the rated power at quotation
- Machine dismantled into container-load sections with re-assembly sequence documented
- First-run parameter setting using the buyer’s actual mix design and aggregate
- Operator training covering mould change procedure and daily maintenance checkpoints
- Wear parts and mould reorder list provided before the first replacement cycle is due
What We Need to Configure Your QT8-15 Accurately
To move from general specifications to a firm quotation, share the block formats your market demands along with the daily output target for each. Provide a sample of the coarse and fine aggregate you will use, plus the cement type and any admixtures. Confirm the site voltage, frequency and the language your operators will need on the PLC screen. If you already have curing racks or forklifts in place, send the rack pitch and fork dimensions so pallet size can be matched before the machine is built.
Frequently Asked Questions
Q: How is QT8-15 capacity calculated per block format, and what cycle time applies?
A: Each format has its own cavity count and compaction time. The hollow block at 400×200×200 mm uses eight cavities and a 15-20 second cycle, yielding 1 600-1 900 pieces per hour. Paver and interlocking formats carry different cavity counts, so their hourly outputs differ even on the same press. Always tie capacity to the specific format you intend to run.
Q: How should vibration force and hydraulic pressure be matched to my local aggregate?
A: Angular aggregate with high fines content needs different vibration amplitude and pressure dwell than rounded river sand. The reliable approach is sending a kilogram of your actual coarse and fine aggregate to the factory so test cycles can be run and parameters locked before the machine ships, avoiding weeks of on-site re-tuning.
Q: What is the actual mould change time, and what tools are required?
A: Mould change time depends on the clamping mechanism and operator practice. Ask for a step-by-step procedure and tool list during the quotation stage so you can verify whether the changeover fits within your planned shift schedule and format rotation.
Q: Which pallet size and material should I choose for my curing setup?
A: Pallet dimensions must match the curing rack pitch and the load rating of your existing forklift. Confirm rack slot width and fork length before the pallet order is placed; a mismatch forces manual re-handling and cuts real daily output.
Q: Can I start semi-automatic and add full stacking later?
A: Yes. The QT8-15 automation level is configurable, allowing buyers to begin with manual pallet handling and add automatic stacking and cubing as production volume grows. The upgrade path and interface readiness should be confirmed in the initial specification sheet.