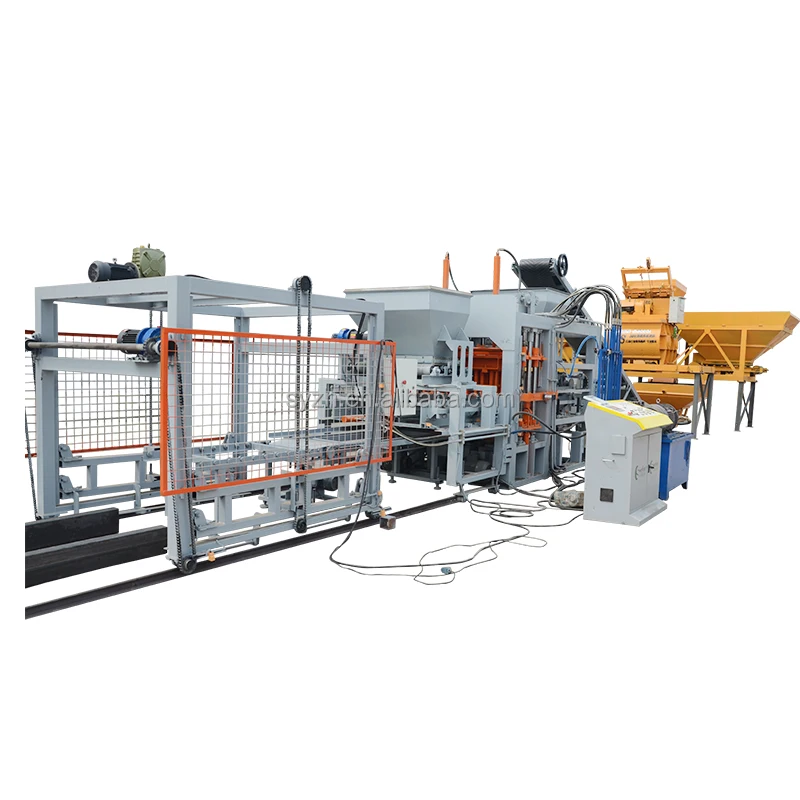
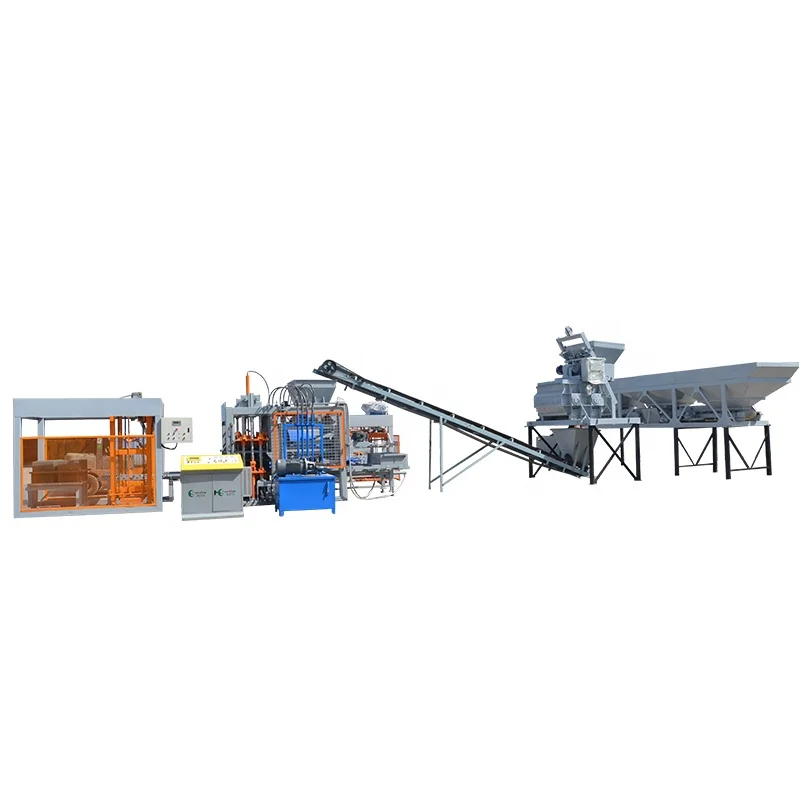
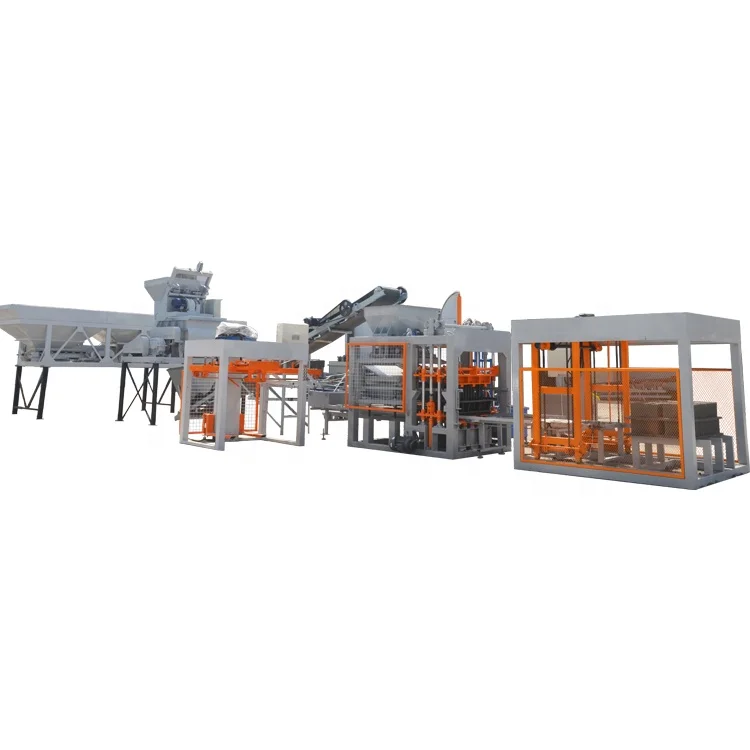
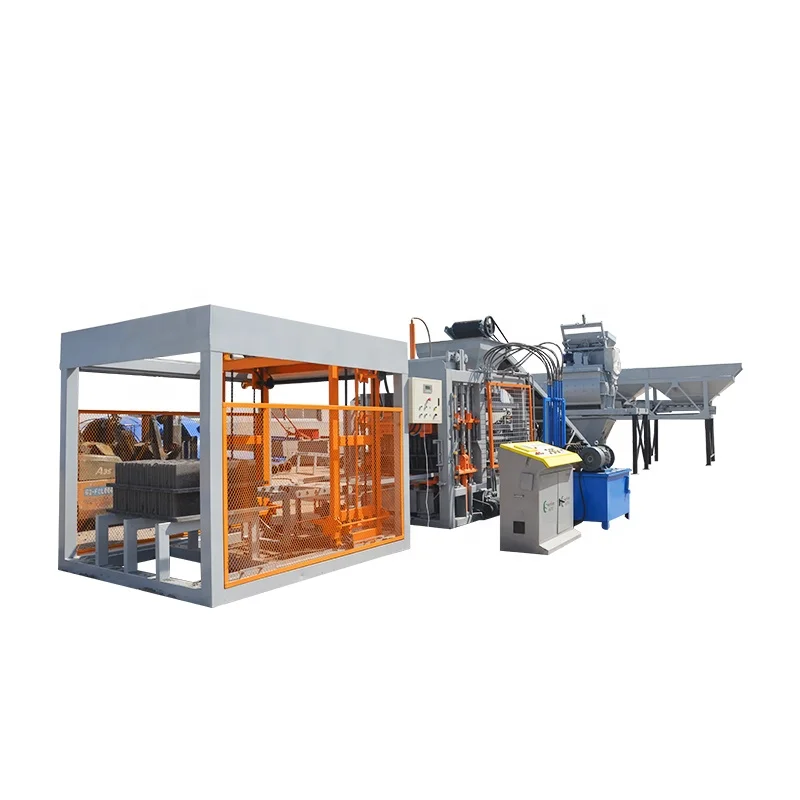
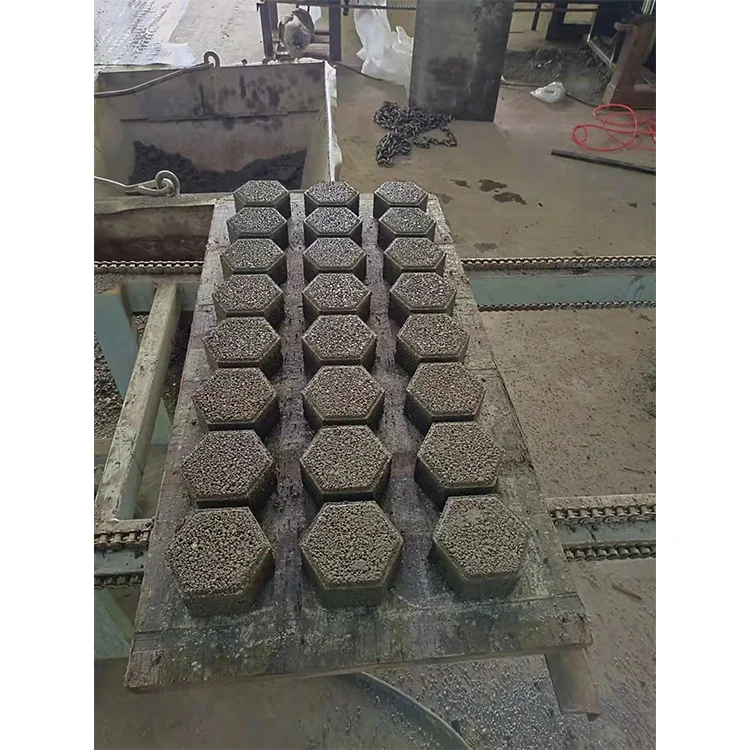
Description
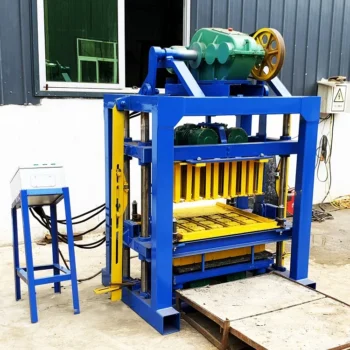
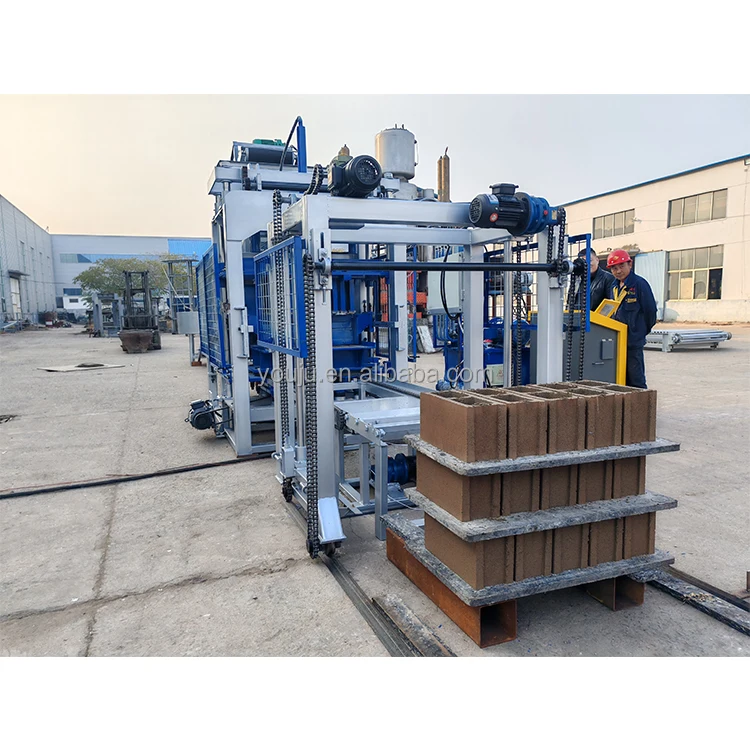
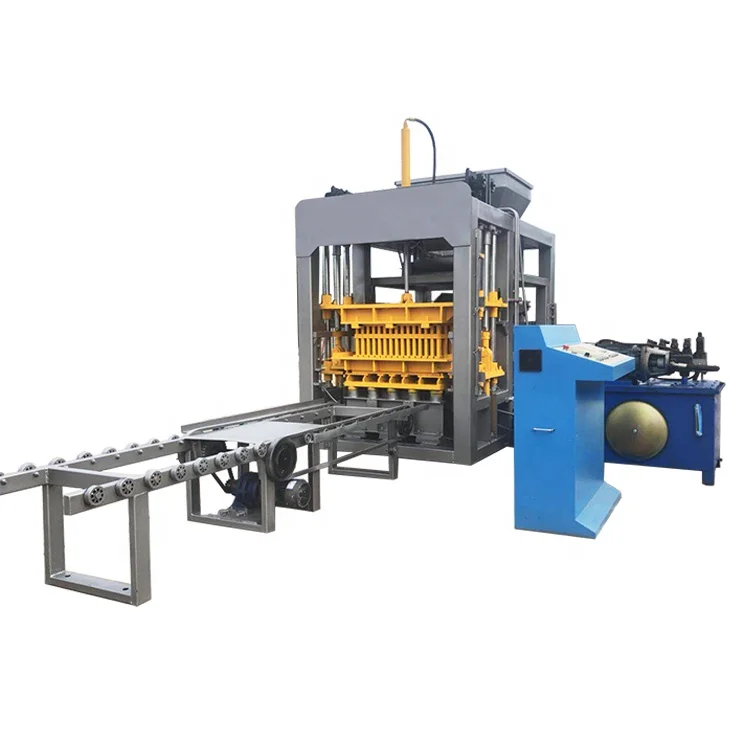
Honest Capacity by Format — The QT5-15 is a stationary block machine where every output figure ties to a named block format, pallet dimension, and cycle time, removing the guesswork from your plant sizing decision.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
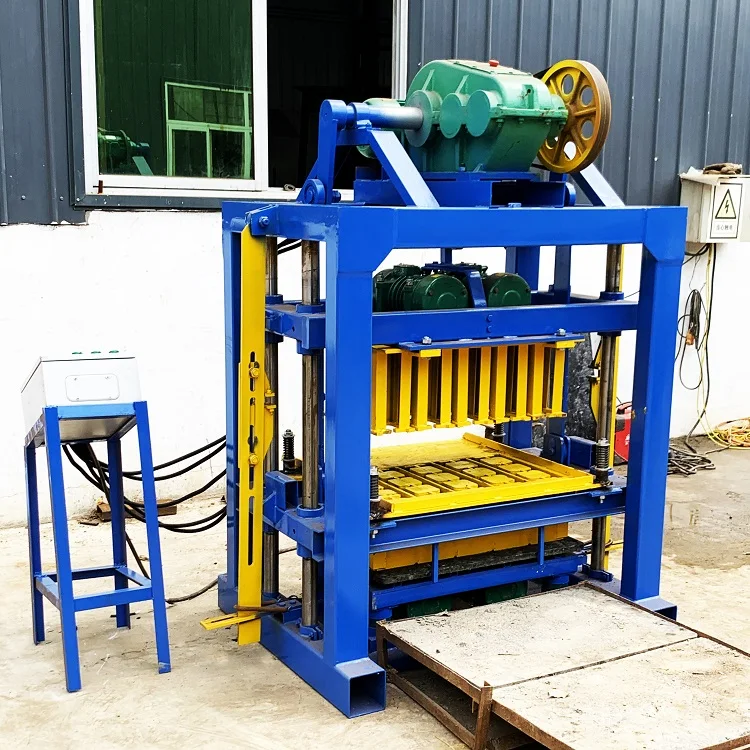
| Product Type | Stationary Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400×1950×2800 mm |
| Rated Power | 26.5 kW |
| Hydraulic Pressure | 21 MPa |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Pallet Size | 1100×550 mm |
| Cycle Time | 15–25 s (basis not stated in source — confirm block format) |
| Demolding Method | Hydraulic |
| Control System | PLC |
| Automation Level | Fully Automatic |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Capacity — 400×200×200 mm hollow brick | 1800 pcs/h (5 pcs/mould, 16–20 s cycle) |
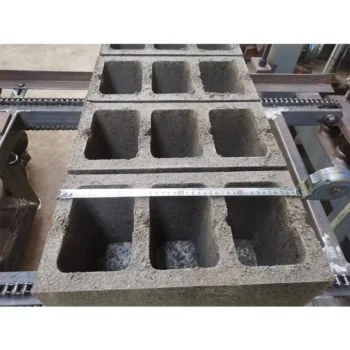
| Capacity — 400×150×200 mm hollow block | 1300 pcs/h (6 pcs/mould, 15–20 s cycle) |
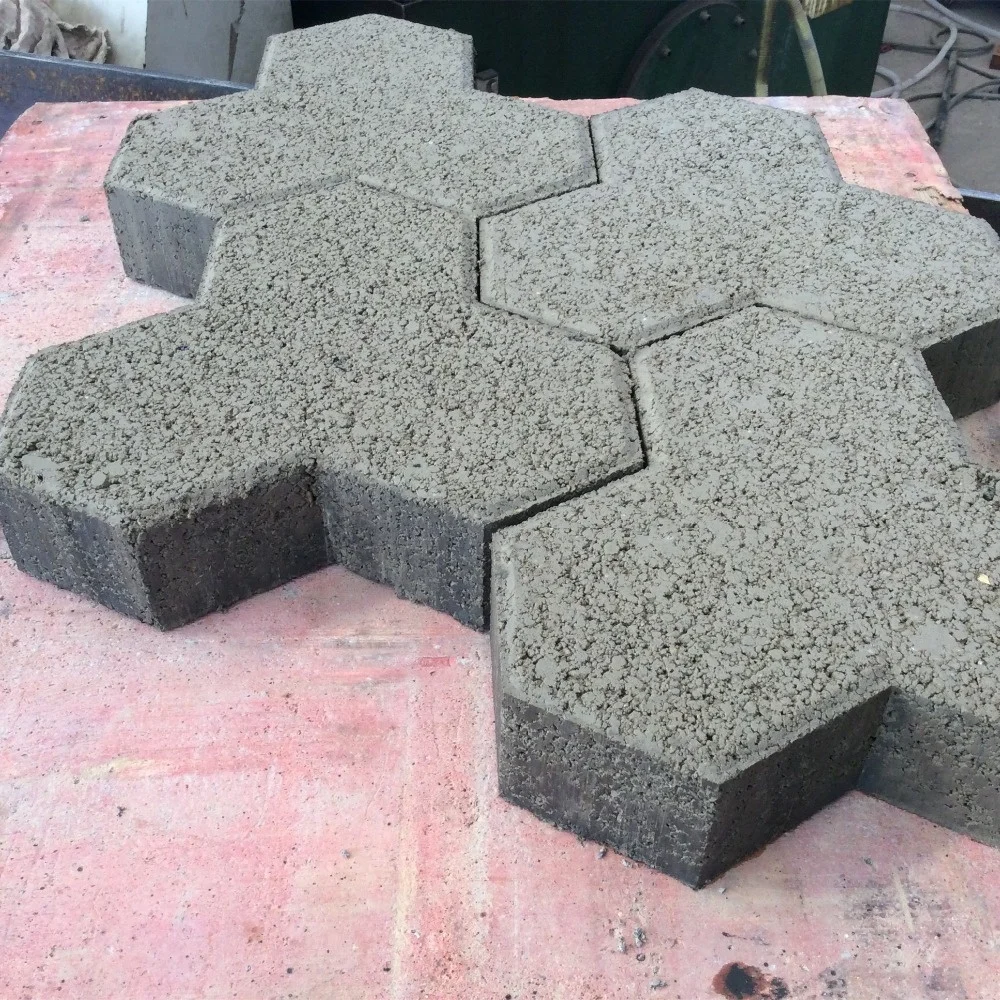
| Capacity — 225×112.5×60 mm S paver | 3700 pcs/h (16 pcs/mould, 15–17 s cycle) |
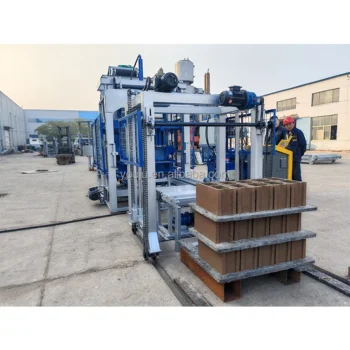
| Applicable Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for load-bearing walls | Crushed stone and cement with fly ash blend |
| Solid block manufacturing for partition walls | Sand, gravel, and cement mix |
| Interlocking paver runs for driveways and walkways | Fine aggregate with pigment additive |
| Curbstone and kerb production for roadworks | Coarse aggregate and high-cement ratio |
| Colored paver batches for landscape projects | Sand, cement, and oxide pigment |
Why Cycle Time by Format Decides Your Real Output
A headline capacity number means nothing without the block format that produced it.
I once flew to a Middle East site where a buyer had ordered a mid-tier stationary machine based on a single hourly figure. The local aggregate had high clay content, the vibration frequency was wrong for that mix, and the real cycle stretched well beyond the quoted range. Daily output fell far below expectation, and five days of on-site mix adjustment and pressure curve tuning were needed to recover the line. That is the exact reason the QT5-15 block machine specifications capacity by format exist — so you can match the machine to the product your market actually buys, not a catalogue default. [NEED_CITE: effect of aggregate clay content on block compaction cycle time]
When a supplier quotes cycles per hour without naming the format, the pallet footprint, or the mould cavity count, the gap between brochure and reality widens fast. Buyers end up short on the products that move volume in their region while over-equipped for formats they rarely run.
Matching the Press to Your Best-Selling Block
Every technical buyer knows the difference between a hollow block and a paver goes far beyond shape. The QT5-15 block machine specifications capacity by format list three reference products with their mould cavity counts and cycle ranges, letting you calculate realistic daily output for the format your plant will run most shifts. Platform vibration frequency adjusts across the 2800–4500 r/min band to suit everything from lightweight hollow blocks that need gentler compaction to dense pavers requiring sustained high-frequency vibration.
Pallet Size Downstream Determines the Line Layout
The 1100×550 mm pallet is not just a press parameter — it sets the geometry of your curing racks, the aisle width for your forklift, and the stacking pattern in your yard. A buyer who already runs a curing area designed for a different pallet dimension will face either a costly rack rebuild or a daily handling bottleneck. Confirming pallet compatibility before the machine ships avoids discovering the mismatch when the first rack of fresh blocks has nowhere to go. [NEED_CITE: pallet dimension standards in stationary block production lines]
Reading the Specs That Shape Block Strength
Hydraulic pressure at 21 MPa and platform vibration together determine the density and compressive strength of every block the QT5-15 produces. If your local aggregate is angular crushed stone, higher vibration frequency combined with moderate hydraulic pressure generally yields better interlock than brute-force pressure alone. Conversely, a sandy mix with fly ash benefits from sustained pressure at a lower frequency to push fines into the void network. The PLC control system stores these parameter sets so operators can recall them per mould format, reducing the trial-and-error that wastes a full shift after each changeover. Demolding is fully hydraulic, which keeps block edges intact even on deeper cavity formats like curbstone where mechanical ejection would crack the green product.
The Cost of Skipping Format-Level Sizing
Choosing a machine on a single output figure and discovering mid-installation that your primary format runs slower than expected turns a planned expansion into a cash-flow problem. Pallets pile up faster than the curing area can absorb them, forklift drivers idle waiting for rack space, and the press sits blocked. Buyers who did not confirm mould change time before ordering also report losing a significant portion of a shift each time they rotate formats, cancelling out the flexibility they paid for in the first place. [NEED_CITE: mould change downtime impact on multi-format block plants]
Why Technical Buyers Source This Machine Here
Block machinery is the single focus of this operation, which means the press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. Configuration is set against your actual mix design and local aggregate, not a catalogue default — I have seen the alternative, and it ends with a technician on a plane. Mould design covers the formats your market sells, including custom drawings when standard cavities do not fit. Automation level is selectable, so a buyer can start semi-automatic and add stacking or cubing modules later without replacing the press. Every machine goes through a factory test using the buyer’s own material sample before dispatch, because data that does not match should hold up shipment, not the other way around.
Documentation & Verification
- Capacity calculation sheet stating block format, cavity count, and cycle time for each reference product
- Mould drawing and format list confirming included and optional moulds
- Pallet specification covering material, thickness, and weight matched to your curing racks
- Voltage, frequency, and PLC display language confirmed in writing before production
- Factory test record run on your submitted raw material sample
- Hydraulic and electrical schematic for local maintenance teams
Installation, Commissioning & Support
- Foundation pad sized to the 7400×1950 mm footprint with vibration isolation provisions
- Dedicated power circuit rated for the 26.5 kW total draw at confirmed voltage and frequency
- PLC display language and control parameters loaded and verified before the crate leaves the factory
- On-site commissioning includes first-run parameter tuning against your live mix and aggregate
- Operator training covers mould change procedure, vibration frequency adjustment, and daily inspection points
- Wear parts list with hydraulic seal and vibration motor intervals specific to this model
What We Need to Size the Line Correctly
Share the block formats your market moves in volume, the daily output you need per format, and the raw materials you can source locally — including aggregate gradation and any fly ash or slag proportion. Confirm your existing curing rack dimensions and forklift capacity so pallet specs align before production starts. Let us know the local voltage and frequency standard and the preferred PLC display language so commissioning begins the day the machine powers up.
Frequently Asked Questions
Q: How is the QT5-15 hourly capacity calculated, and which block format does each figure assume?
A: Each capacity figure is tied to a specific block format, mould cavity count, and cycle time range. For example, 1800 pieces per hour is based on a 400×200×200 mm hollow brick running five cavities per mould at a 16–20 second cycle. Without the format stated, a single headline number is meaningless for plant planning.
Q: What mould formats are available, and how long does a mould change take?
A: Standard formats include hollow blocks, solid blocks, interlocking pavers, and curbstones, with custom moulds available to buyer drawings. Mould change time depends on the specific format pair and operator familiarity — confirm this during commissioning so your daily rotation schedule reflects actual downtime.
Q: How do I confirm the pallet size is compatible with my curing area and forklift?
A: The standard pallet measures 1100×550 mm. Cross-check this against your existing curing rack slot width, rack spacing, and forklift tine length. If your current system uses a different dimension, rack modification or pallet re-specification should happen before the machine ships.
Q: What block strength can I expect given my local aggregate and mix design?
A: Block strength depends on the combination of hydraulic pressure at 21 MPa, vibration frequency, and your specific aggregate gradation and cement ratio. Submitting a material sample for factory testing before shipment lets us tune the pressure and vibration curve to your mix rather than relying on generic defaults.
Q: What documentation verifies capacity and electrical compatibility before shipment?
A: You receive a capacity calculation per format, mould drawings, pallet specification, voltage and frequency confirmation, PLC language record, and a factory test report run on your submitted raw material — all issued before the machine is crated.