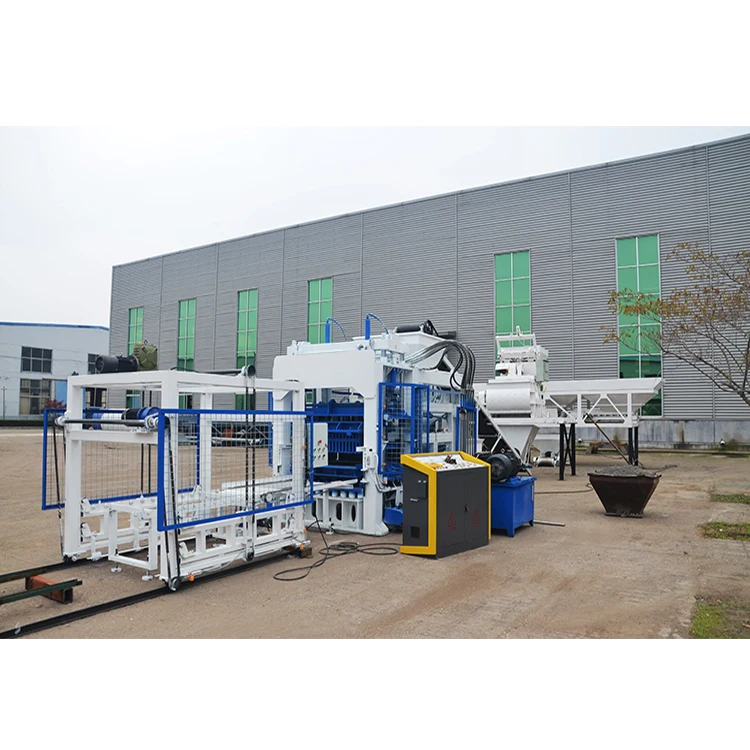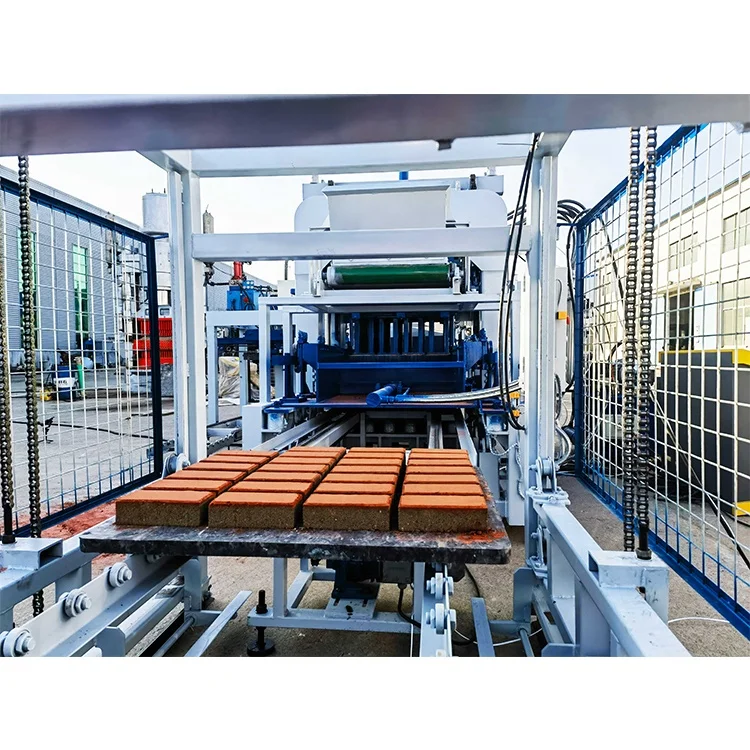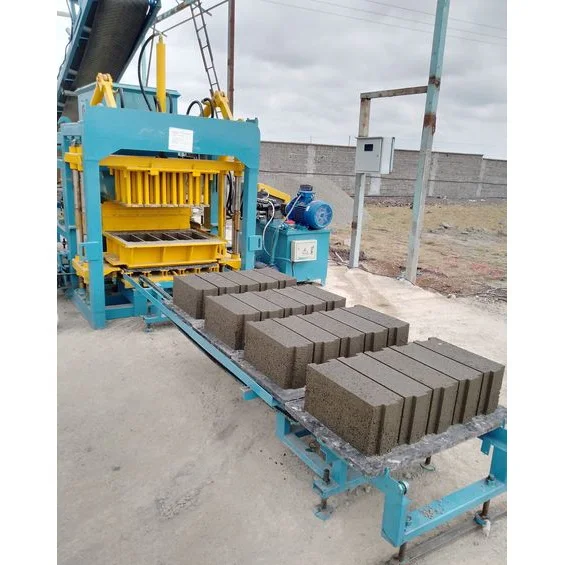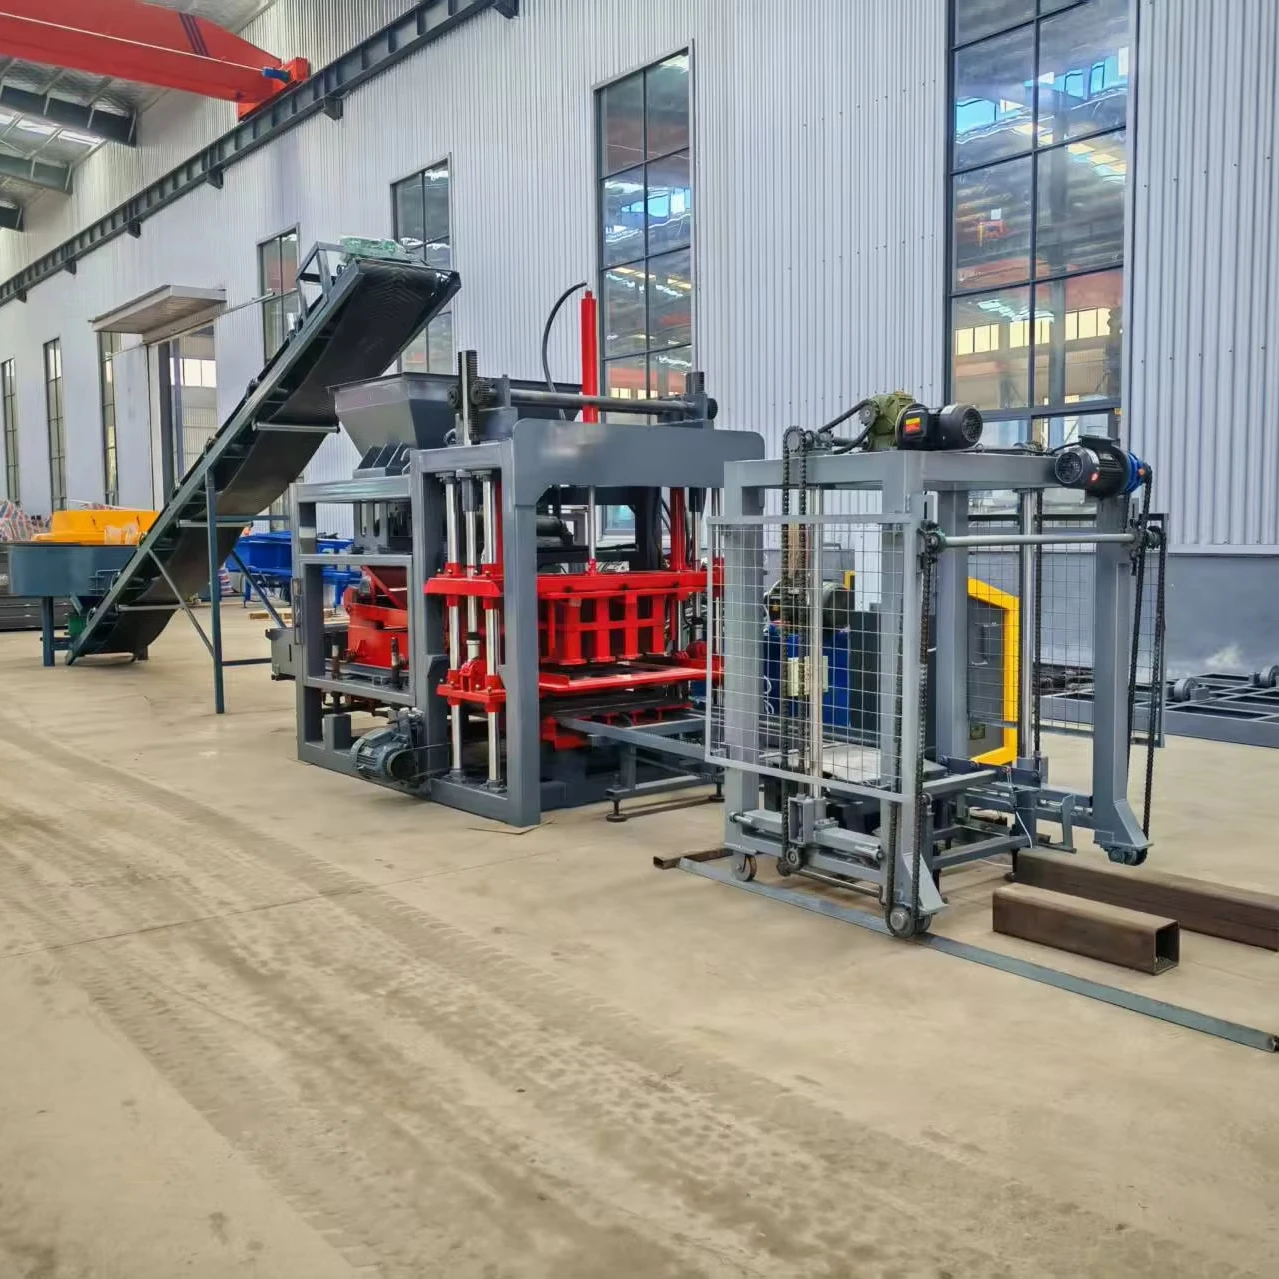


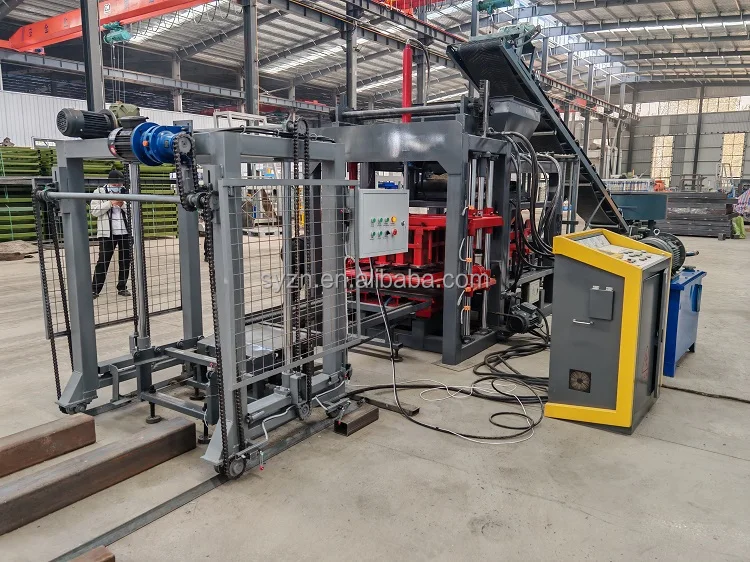
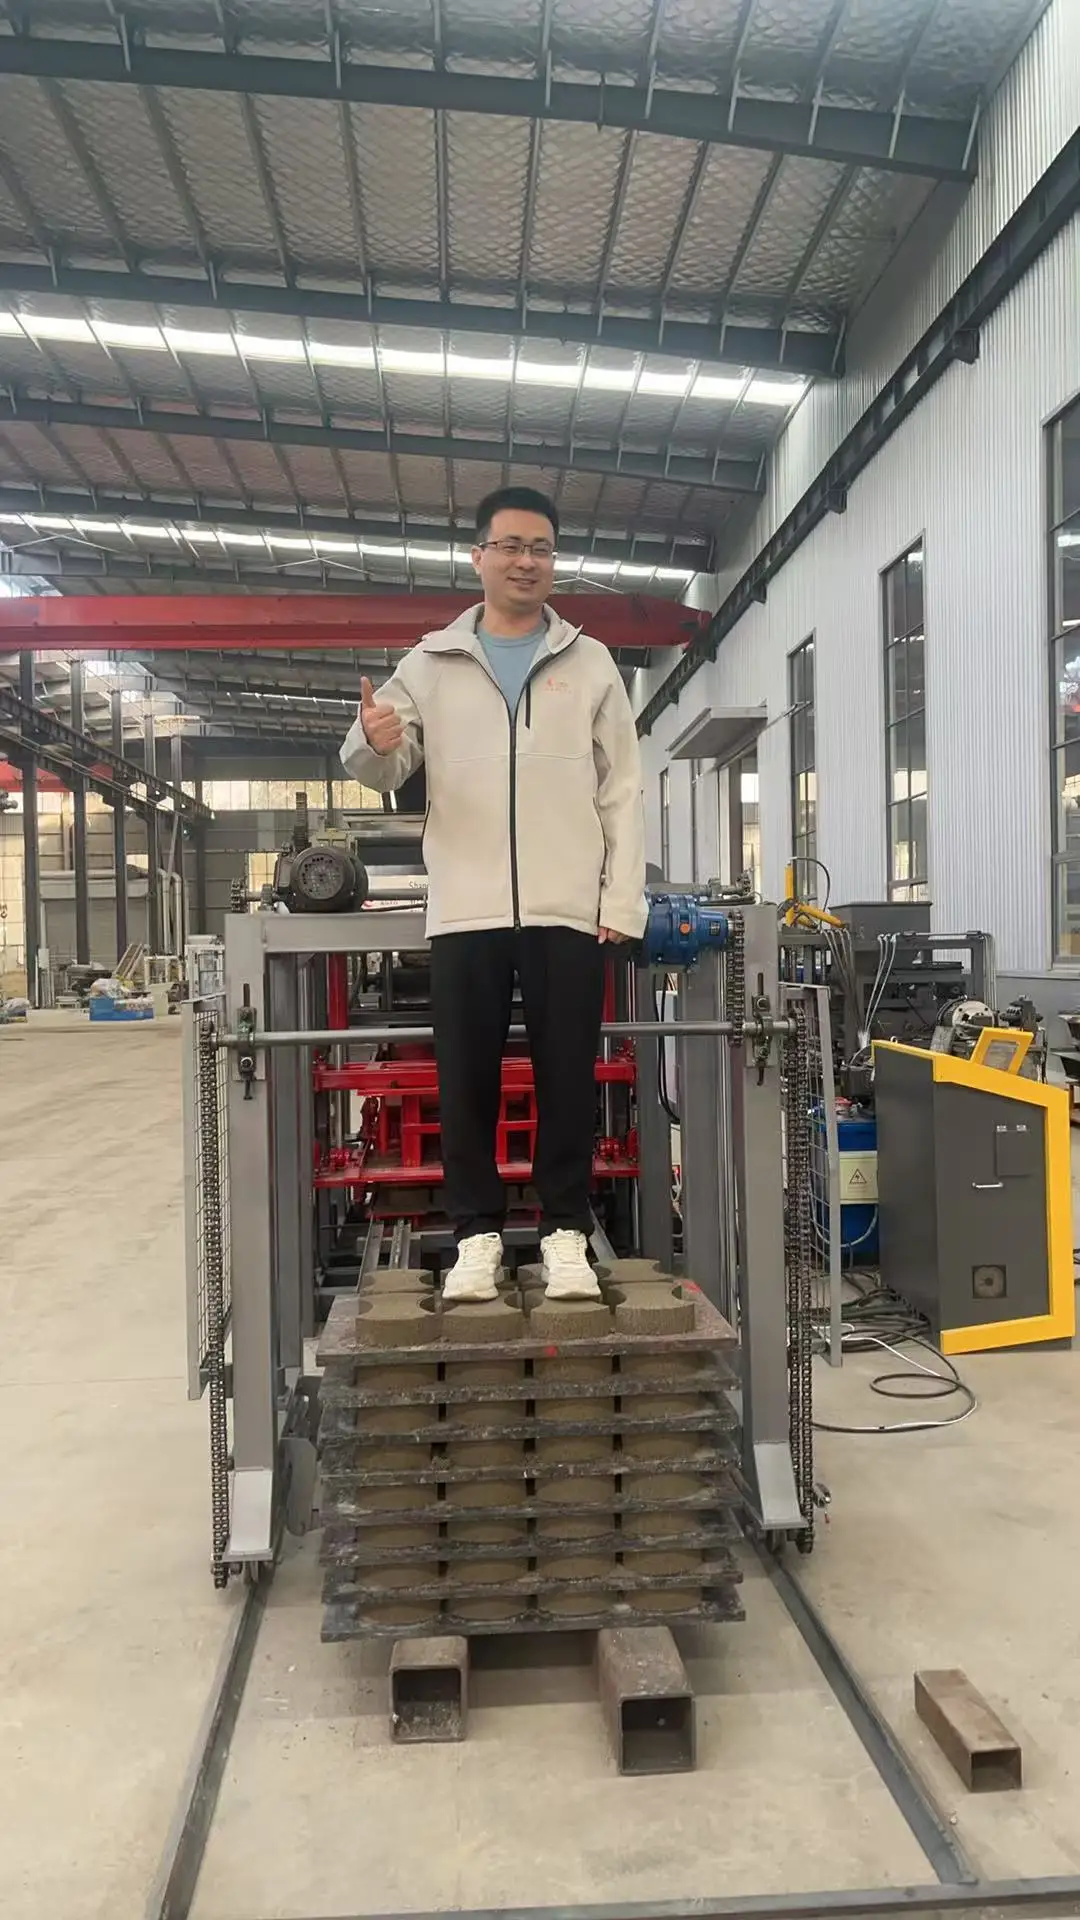
Description
Mould-First Configuration — capacity calculations for this machine are stated per block format with pallet sizing matched to your curing area, not pulled from a generic catalogue.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
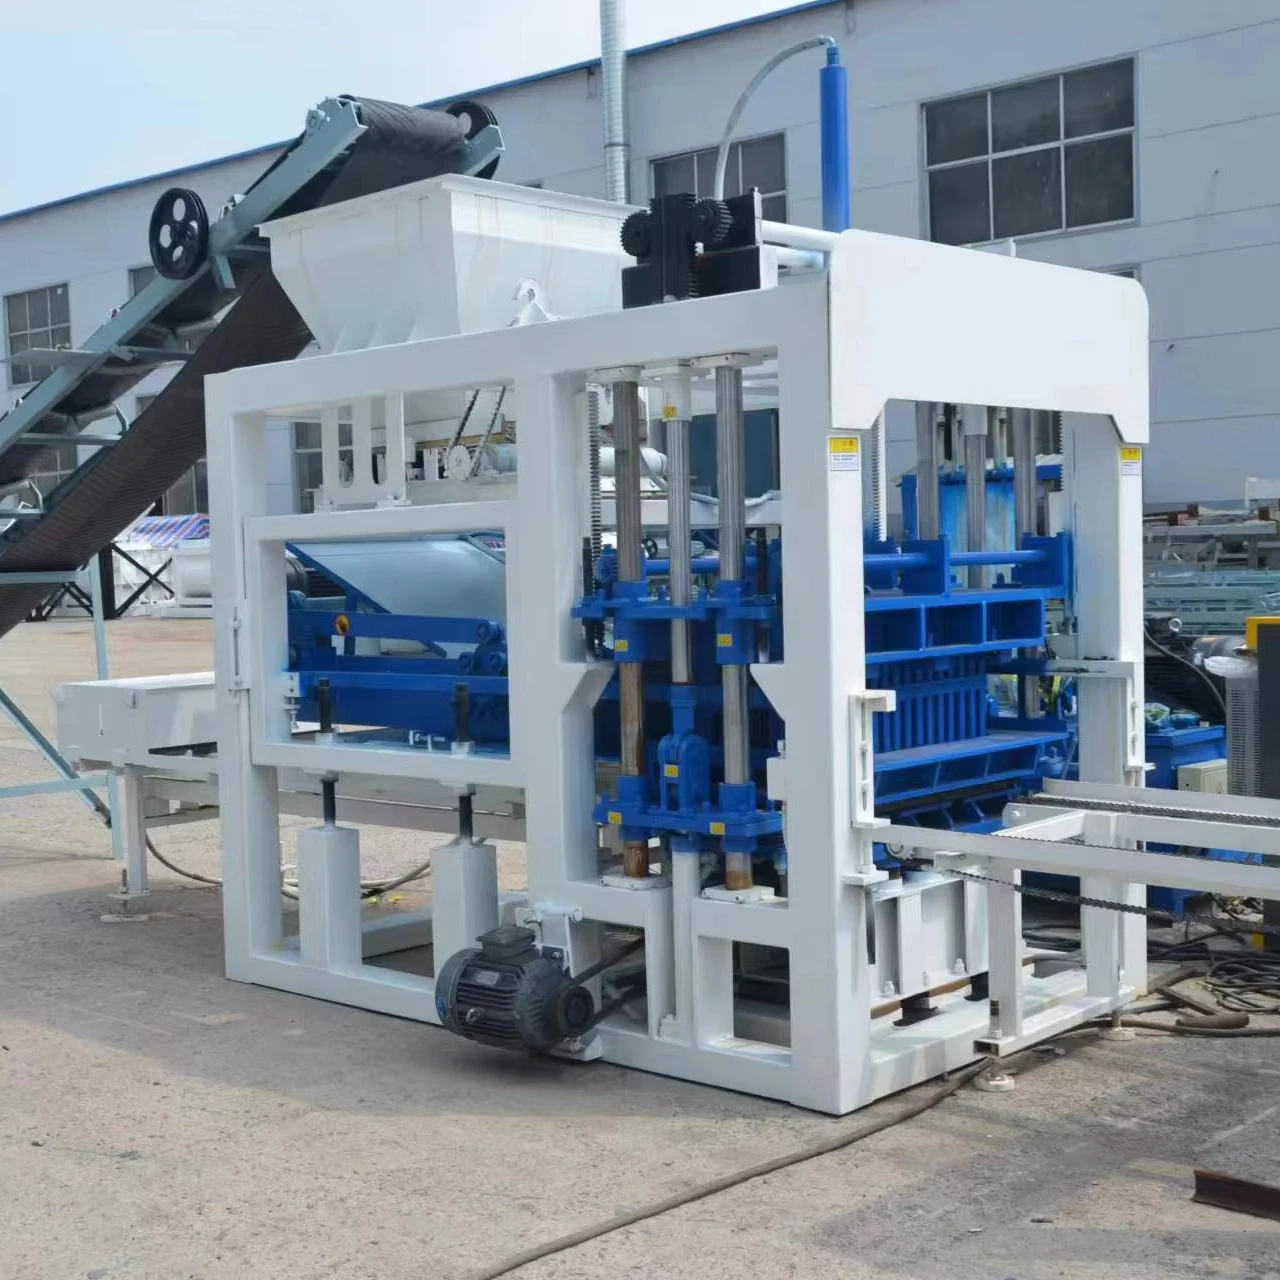
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 3900×1600×2300 mm |
| Total Weight | 3 T |
| Rated Power | 24 kW |
| Vibration Force (Exciting Power) | 40-50 kN |
| Moulding Cycle | 15-25 s |
| Pallet Size | 850×550×25 mm |
| Mixer Model | JQ350 |
| Automation Level | Semi-automatic |
| Stacking Method | Automatic stacker included |
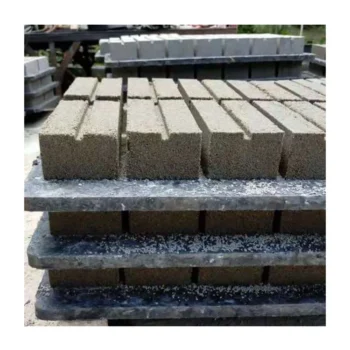
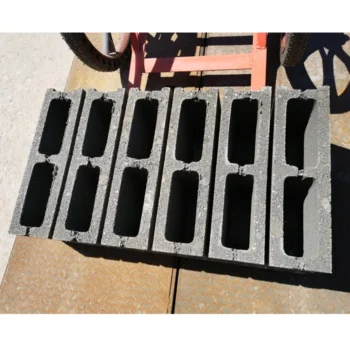
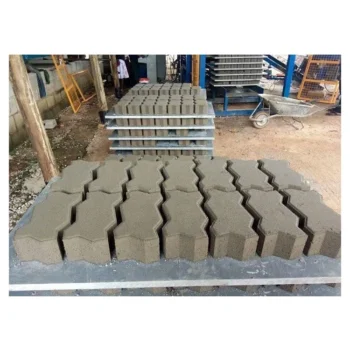
| Mould Format Compatibility | Hollow, solid, paver, curbstone (mould change required) |
| Output: Hollow Block 400×200×200 mm | 1200-1680 pcs/hr, 9600-13440 pcs/8hr |
| Output: Hollow Block 400×150×200 mm | 1800-2400 pcs/hr, 14400-19200 pcs/8hr |
| Output: Solid Brick 240×115×53 mm | 3240 pcs/hr, 16200-19440 pcs/8hr |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Voltage & Frequency | To be confirmed with buyer’s site supply |
| Control System | To be confirmed (PLC or relay logic) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid brick manufacturing for load-bearing structures | Cement and fine aggregate mixes |
| Paving block production for walkways and yards | High-density crushed stone and cement |
| Curbstone forming for road and infrastructure projects | Coarse aggregate with cement binder |
What the QT4-18 Block Making Machine Specifications Actually Mean for Your Output
A cycle time only matters when tied to a specific block format and your local mix design.
Too many quotations list a single "pieces per hour" figure without naming the block size behind it. When the machine arrives and you start running the format your market actually buys, daily output can fall far short of what you planned. The QT4-18 block making machine specifications here are broken down per format — 400×200×200 mm hollow, 400×150×200 mm hollow, and 240×115×53 mm solid — so you can match the number to your real production target [NEED_CITE: honest capacity disclosure standards in block machinery trade].
I have watched buyers commit to a machine based on a headline capacity, only to discover that figure assumed a small solid brick while they needed large hollow blocks. The moulding area stays the same, but fewer cavities fit, and the cycle stretches. That gap between quoted and actual output is where project timelines break.
Mould Selection and Format Flexibility on the QT4-18
The host machine accepts moulds for hollow blocks, solid bricks, pavers, and curbstones, but each format change requires a physical mould swap on the press. When you size your QT4-18 block making machine order, confirm which moulds are included in the quotation and which are optional extras. A buyer producing mainly 400×200×200 hollow blocks with occasional paver runs needs a different mould package than one running three formats daily.
Pallet Sizing Against Your Curing Area and Forklift
The standard pallet for this machine measures 850×550×25 mm. Before confirming the order, check that dimension against your curing racks and the fork spacing on your forklift. Pallets that do not fit existing racks force you to rebuild the curing area or handle blocks manually — a cost that never appears on the machine quotation [NEED_CITE: pallet handling compatibility in block plant layout].
How Vibration Force and Hydraulic Pressure Shape Block Density
The 40-50 kN vibration force works together with hydraulic pressure to compact the mix inside the mould cavity. Higher vibration alone does not guarantee stronger blocks; the hydraulic station must apply enough pressure to hold the mould box steady while vibration consolidates the material. If your local aggregate is sticky — like laterite or high-clay sand — the balance between vibration amplitude and pressure must shift, or blocks will stick to the mould walls and crack on ejection. The JQ350 mixer feeds material at a consistency that matches this vibration range, but the actual water-to-cement ratio still depends on your aggregate moisture on the day of production.
The Cost of Skipping Format-Specific Capacity Checks
When a buyer selects a machine without confirming capacity per format, the consequences cascade. The curing area is built for a pallet count that never materialises. Labour is hired for an output level the line cannot sustain. Contracts with construction sites carry penalty clauses for late delivery. These are not machine faults — they are specification gaps that surface only after commissioning [NEED_CITE: common causes of block plant underperformance].
Why Sourcing the QT4-18 Through a Format-Matched Approach Matters
Every quotation for this machine leaves our workshop with a line layout that names the exact block format behind each capacity figure. Mould drawings are reviewed against the block dimensions your market sells, not a default catalogue page. The pallet specification is cross-checked with your curing rack dimensions and forklift capacity before steel is cut. Voltage, frequency, and control language are confirmed in writing so the electrician on your site is not guessing when the container arrives. We focus on block machinery as a single product line, which means the press, mould, pallet, and handling equipment are specified as one system rather than assembled from separate suppliers after the fact.
Documentation & Verification
- Line layout with capacity stated per block format for the QT4-18
- Mould drawing and format list showing included cavity sizes
- Pallet specification matched to your curing rack and forklift
- Hydraulic and electrical schematic for on-site troubleshooting
- Factory test record run on your target block format before dispatch
- Voltage, frequency, and PLC display language confirmation sheet
Installation, Commissioning & Support
- Foundation plan based on the 3900×1600 mm machine footprint and 3 T weight
- Power supply check for 24 kW rated draw with dedicated circuit breaker
- Semi-automatic operation training covering mould change procedure on site
- Mixer JQ350 feed rate calibration matched to your local aggregate moisture
- Vibration force tuning between 40-50 kN for your specific mix design
- Wear parts list covering hydraulic seals and mould liner plates
What to Share Before Requesting a Quotation
Send the block format your market sells most — dimensions, wall thickness, and target compressive strength. Include a sample or description of your local aggregate so the mix can be evaluated before the mould is built. Confirm your site voltage, frequency, and preferred control display language so the QT4-18 block making machine leaves the factory configured for your electrical supply.
Frequently Asked Questions
Q: How is the output capacity calculated, and which block format does each figure assume?
A: Each capacity figure on this page is tied to a specific block size. The 1200-1680 pieces per hour assumes a 400×200×200 mm hollow block, the 1800-2400 figure assumes a 400×150×200 mm hollow block, and the 3240 figure assumes a 240×115×53 mm solid brick. Your actual output depends on mix design, operator pace, and curing logistics.
Q: What mould formats are included, and what is the mould change time on site?
A: The host machine supports hollow, solid, paver, and curbstone moulds, but the quotation must state which are included. Mould change time depends on the quick-lock system fitted and operator practice. Confirm the exact change time with your supplier before committing to a multi-format production schedule.
Q: How should pallet size and material be chosen to match my curing area?
A: The standard 850×550×25 mm pallet must align with your curing rack spacing and forklift fork width. If your racks are built for a different pallet, you face rebuilding costs or manual handling. Share your rack dimensions and forklift model before the order is finalised.
Q: How is vibration force matched to local aggregate and mix design?
A: The 40-50 kN vibration range is adjusted during commissioning based on your aggregate type. Sticky materials like laterite need lower amplitude with higher hydraulic pressure to prevent mould sticking. A trial run with your actual material is the only way to confirm the right balance.