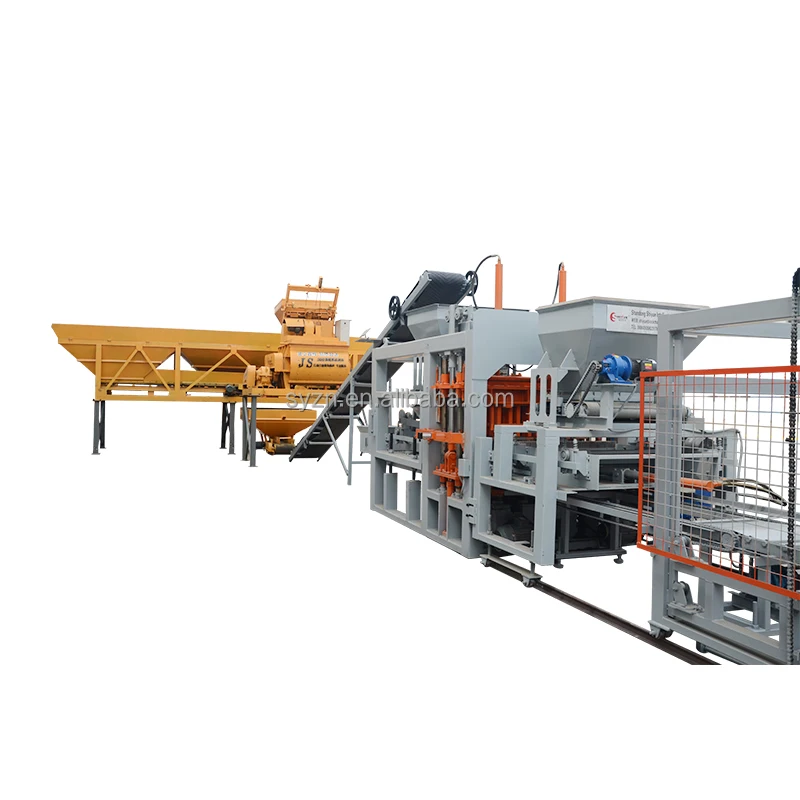
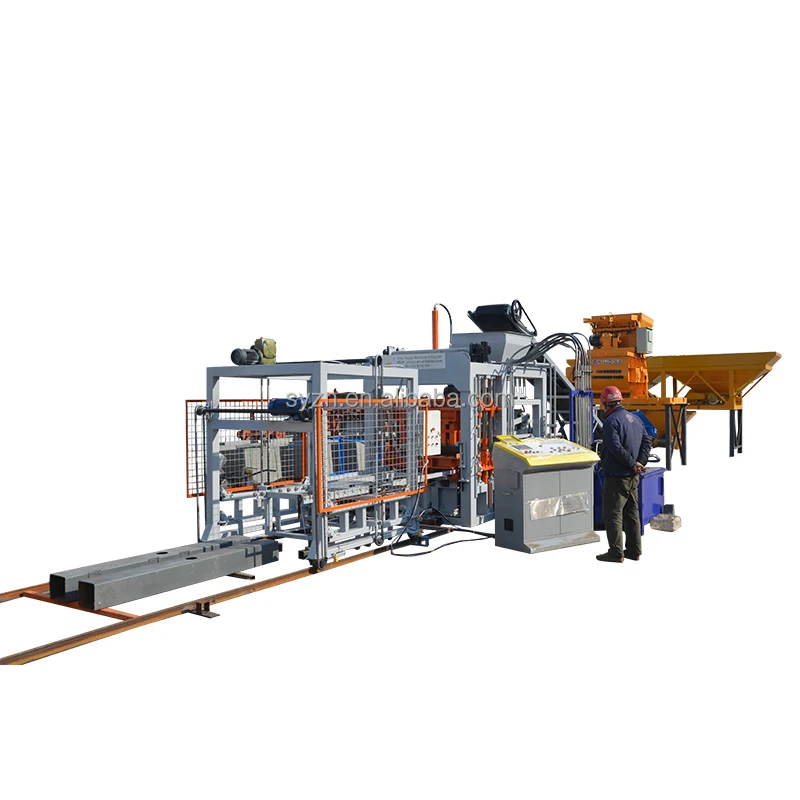


Description
Matched System Sizing — the QT7-15 block machine format and mould capacity is specified against your actual product mix, not a generic catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT7-15 |
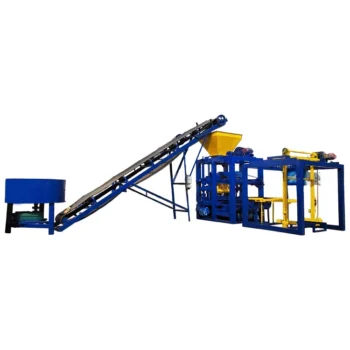
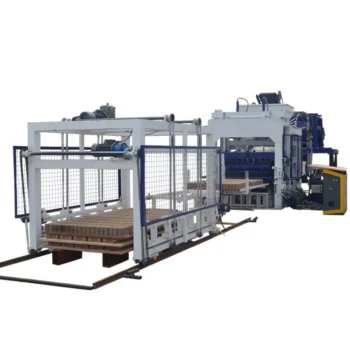
| Product Type | Hydraulic Concrete Block Making Machine |
| Pallet Size | 1150×700 mm |
| Molding Cycle | 15–20 s |
| Overall Power | 45 kW |
| Vibration Force | 100 kN |
| Vibration Frequency | 0–60 Hz |
| Vibration Form | Platform Vibration |
| Total Mass | 8 T |
| Demolding Method | Hydraulic |
| Control System | PLC (Programmable Logic Controller) |
| Interactive Interface | Touch Screen |
| Remote Diagnostics | Supported |
| Automation Level | Automatic with PLC Intelligent Control |
| Mould Change | Simple Mould Replacement Supported |
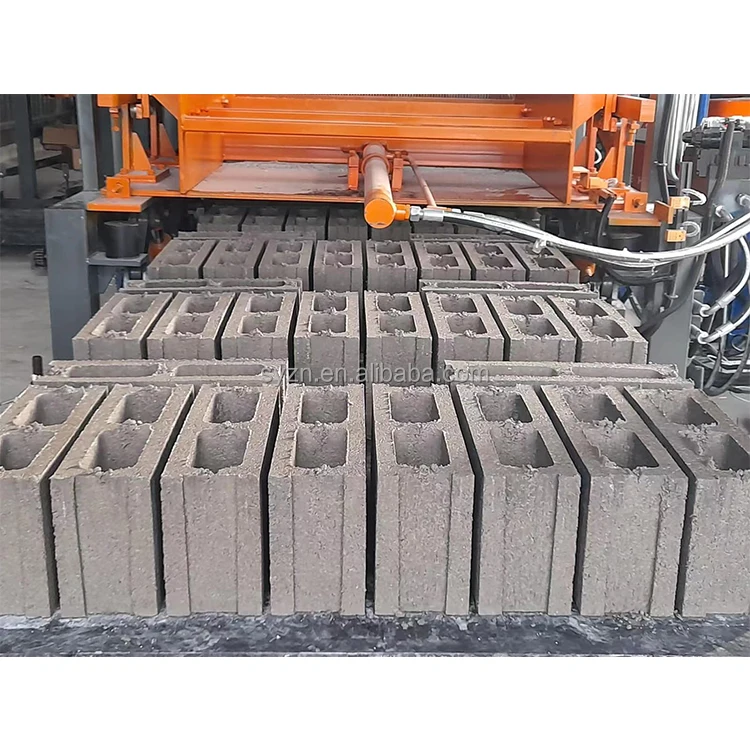
| Output Capacity (Hollow Block 400×200×200 mm) | 1260–1680 pcs/hour (based on 7 pcs/mould, 15–20 s cycle) |
| Output Capacity (Hollow Block 400×150×200 mm) | 1440–1920 pcs/hour (based on 8 pcs/mould, 15–20 s cycle) |
| Output Capacity (Rectangular Paver 200×100×60 mm) | 3888–4860 pcs/hour (based on 27 pcs/mould, 20–25 s cycle) |
| Standards | CE Declaration (where applicable) |
| Voltage & Frequency | Configurable to Buyer Market |
Application Suitability
| Application | Material or Output |
|---|---|
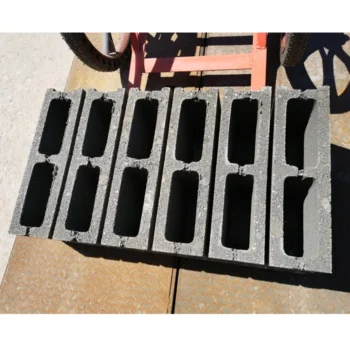
| Hollow Block Production | Cement, crushed stone, sand, water — standard masonry units for wall construction |
| Solid Block Production | Dense aggregate mixes for load-bearing structural blocks |
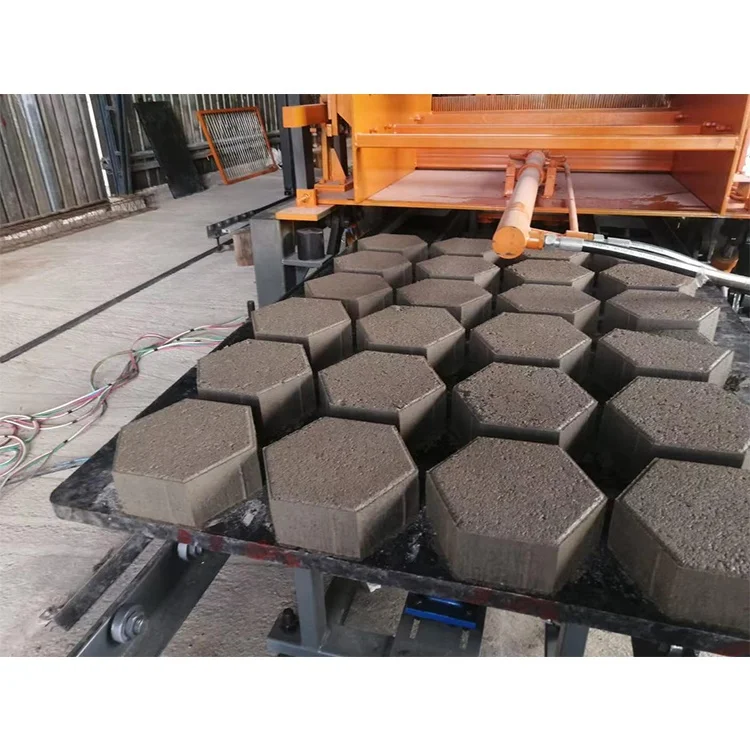
| Paving Block Production | Fine aggregate and cement blends for pedestrian and light-traffic surfaces |
| Interlocking Brick Production | Soil-cement or concrete mixes for dry-stack wall systems |
| Kerbstone Production | High-strength concrete mixes for road and pavement edging |
Why "Cycles per Hour" Tells You Nothing About Real Daily Output
The QT7-15 block machine specifications mean very little if you do not know which block format the capacity figure assumes. Many quotations list a single hourly number — often based on the smallest, fastest paver — and leave the buyer to discover on commissioning day that their main product, a 200 mm hollow block, runs at nearly half that rate. We quote output per format, per mould, per cycle, so your daily tonnage matches your business plan, not a brochure.
I have watched plant owners in East Africa recalibrate entire production schedules after arrival because nobody told them the quoted throughput assumed a paver format they never intended to sell. When the local red soil carries higher clay content than the test mix, vibration settings need adjustment or block strength drops below market acceptance. These are the conversations that must happen before the machine ships [NEED_CITE: aggregate variability and its effect on concrete block compressive strength].
Mould Format Matching and Cycle Time Reality
The QT7-15 block machine format and mould capacity table above separates each product type with its own cycle range. A 400×200×200 mm hollow block at seven per mould runs a 15–20 second cycle, while a 200×100×60 mm rectangular paver at twenty-seven per mould shifts to a 20–25 second cycle due to the higher fill volume and compaction demand. This granularity lets you size downstream curing racks and pallet return conveyors to the format you will actually run eight hours a day.
Vibration and Hydraulic Pressure Tuned to Your Aggregate
Platform vibration at 0–60 Hz adjustable frequency paired with 100 kN force is not a fixed setting; it is a range that must be narrowed against your specific sand, stone dust and cement blend. Coarse crushed granite demands higher amplitude at lower frequency to consolidate without fracturing aggregate, while fine river sand responds to higher frequency at moderate amplitude. The hydraulic demolding pressure must release the block cleanly without scuffing edges — too high and the green block cracks, too low and it sticks to the core [NEED_CITE: vibration frequency selection for different aggregate gradations in block production].
Reading the Specs That Actually Matter on Site
The 1150×700 mm pallet size determines how many blocks travel per cycle, but it also dictates the curing rack spacing and forklift tine width you need in the yard. If your existing racks were built for a smaller pallet, retrofitting them costs time and steel. The 45 kW overall power draw requires a dedicated supply circuit — sharing a feeder with the mixer motor risks voltage sag that trips the PLC mid-cycle. The touch screen interface stores process parameters per mould, so when you switch from hollow block to paver, the operator recalls the saved profile rather than re-entering vibration frequency, feed time and press dwell from memory.
The Cost of Skipping Format Confirmation
Ordering a block press without locking the pallet size to your curing yard means pallets may not stack on existing racks, forcing a manual double-handling step that erases any automation advantage. Unconfirmed voltage and frequency delay commissioning by weeks while transformers are sourced locally. A PLC display in a language the operator cannot read turns intelligent control into an expensive guesswork panel. These are not theoretical risks — they appear repeatedly in post-delivery service calls [NEED_CITE: common commissioning delays caused by unconfirmed electrical specifications].
What This Purchase Process Looks Like
Every machine is configured against the buyer’s actual mix design and target block format before production starts, so the vibration and hydraulic settings arrive close to optimal rather than at catalogue defaults. Moulds are designed for the formats your market buys, with custom drawings reviewed and approved before machining. Pallet size, material and thickness are confirmed against your existing curing racks and forklift capacity. Automation level is selectable — a buyer can begin with semi-automatic pallet handling and add automatic stacking later. Factory test records document performance on your specified block format before the machine is crated.
Documentation & Verification
- Line layout showing pallet flow from press through curing rack to cubing station
- Capacity calculation sheet stating block format, mould count and cycle time for each output row
- Mould drawing pack with dimensional tolerances before machining begins
- Hydraulic and electrical schematic matching the as-built machine configuration
- Factory test record on buyer-specified block format before dispatch
- CE declaration included where destination market requires it
Installation, Commissioning & Support
- Foundation pad must support 8 T static mass plus dynamic vibration load from the platform
- Dedicated 45 kW circuit with confirmed voltage and frequency before energising the control panel
- PLC display language set to operator preference during commissioning, not left at factory default
- Vibration frequency and hydraulic pressure fine-tuned on site using buyer’s actual raw material batch
- Mould change procedure demonstrated with operator hands-on practice until changeover meets target time
- Wear parts list supplied with recommended replacement intervals for hydraulic seals and vibration springs
What We Need From You to Size This Correctly
Tell us the block formats your market actually buys, the daily volume you need per format, and the local aggregate and cement type available at your site. Share your existing curing rack dimensions and forklift specifications so pallet sizing aligns from day one. Confirm your site voltage, frequency and preferred PLC display language to eliminate commissioning delays.
Frequently Asked Questions
Q: How is capacity calculated per block format and what cycle time does each format assume?
A: Each output figure in the specification table ties a specific block dimension to its mould cavity count and cycle range. The 400×200×200 mm hollow block at seven cavities assumes a 15–20 second cycle, while the paver at twenty-seven cavities uses 20–25 seconds. No single number represents all formats.
Q: How long does mould change take on the QT7-15 and what formats are available?
A: The simple mould replacement system allows trained operators to swap moulds within a single shift without special tools. Available formats include hollow blocks, solid blocks, rectangular pavers, interlocking bricks and kerbstones, with custom moulds produced to buyer drawings.
Q: How is vibration force and hydraulic pressure matched to my local aggregate and mix design?
A: Before production, we request a sample of your local aggregate and cement to run trial batches. Vibration frequency and amplitude are adjusted against that mix, and hydraulic demolding pressure is set to release the block cleanly without edge damage.
Q: What pallet size does the QT7-15 require and how does it relate to my curing rack and forklift?
A: The machine uses a 1150×700 mm pallet. Before order confirmation we verify this dimension against your existing curing rack slot width and forklift tine spacing so no yard modifications are needed after arrival.
Q: What voltage, frequency and PLC language options are confirmed before shipment?
A: We confirm your site voltage, frequency and preferred PLC display language in writing before the control panel is wired. This prevents transformer sourcing delays and ensures the operator can read all process parameters on commissioning day.