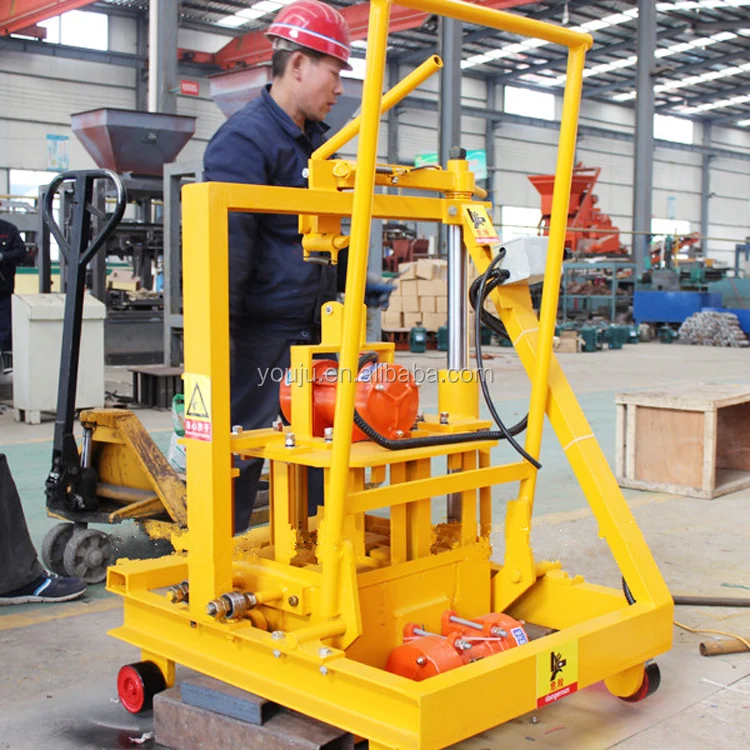
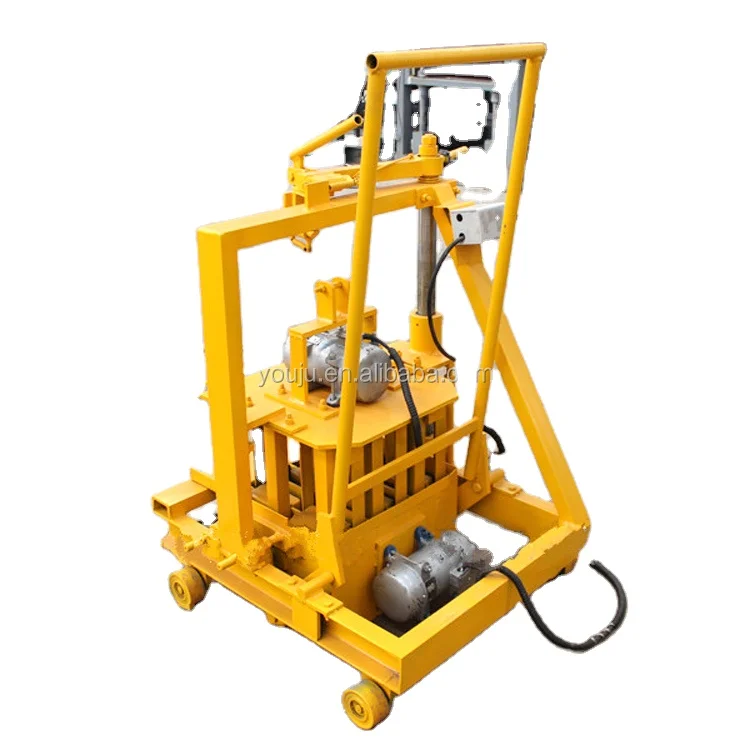
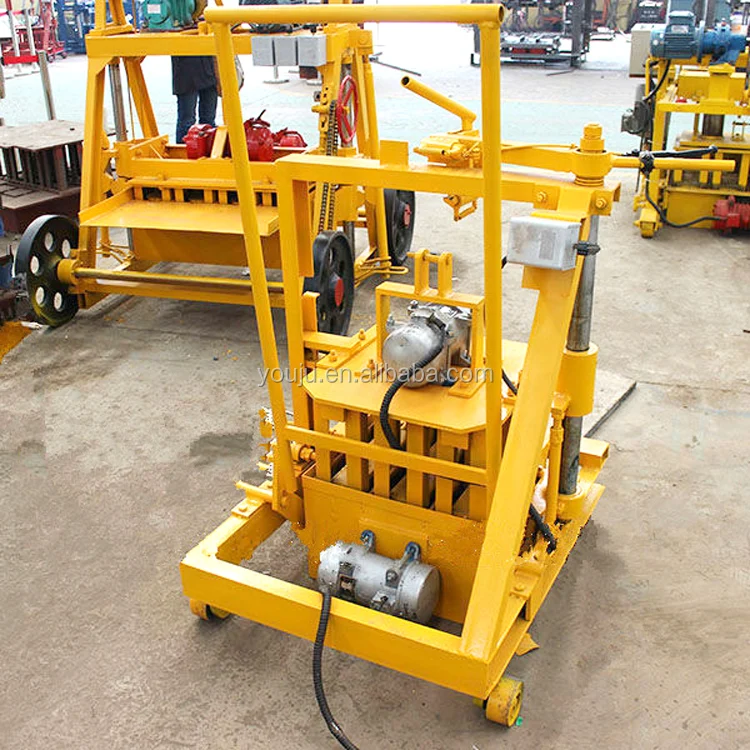


Description
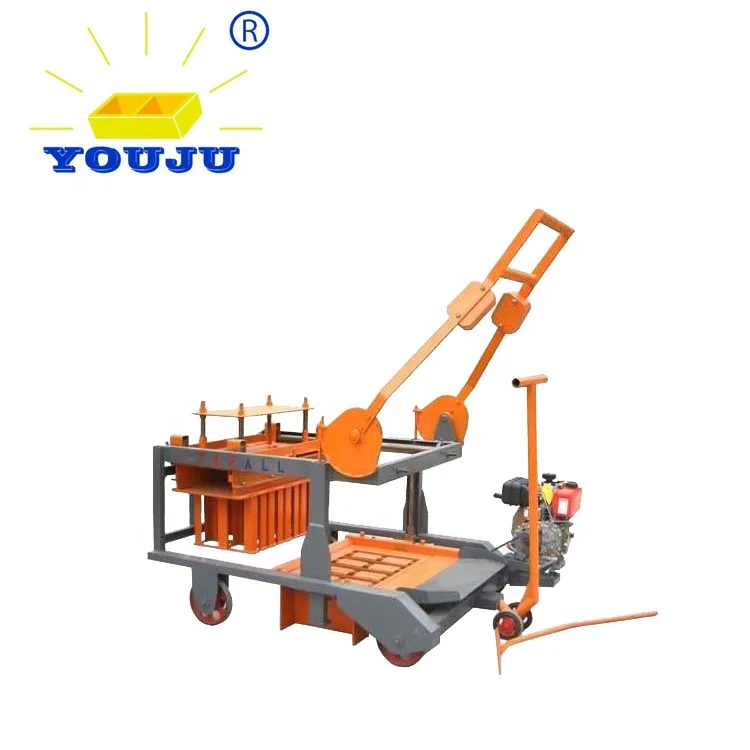
Format-matched capacity — every output figure for the QMJ2-45 ties directly to a named hollow block size and cavity count, so the daily total you plan against is the total you actually produce on site.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Concrete Block Making Machine |
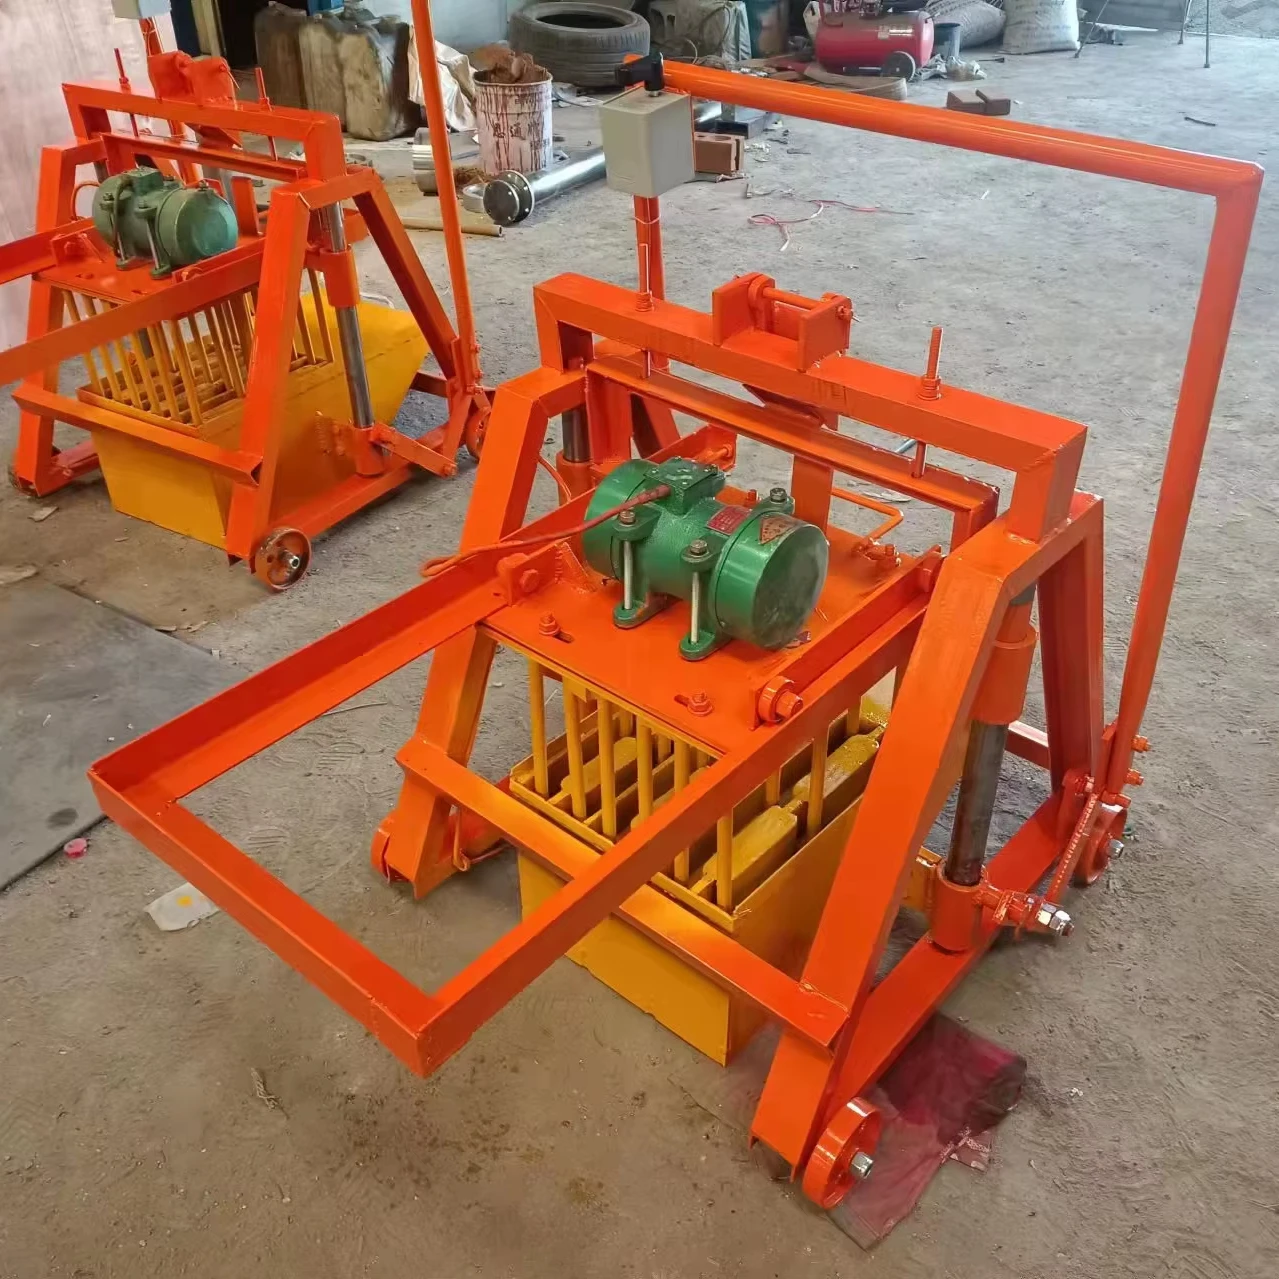
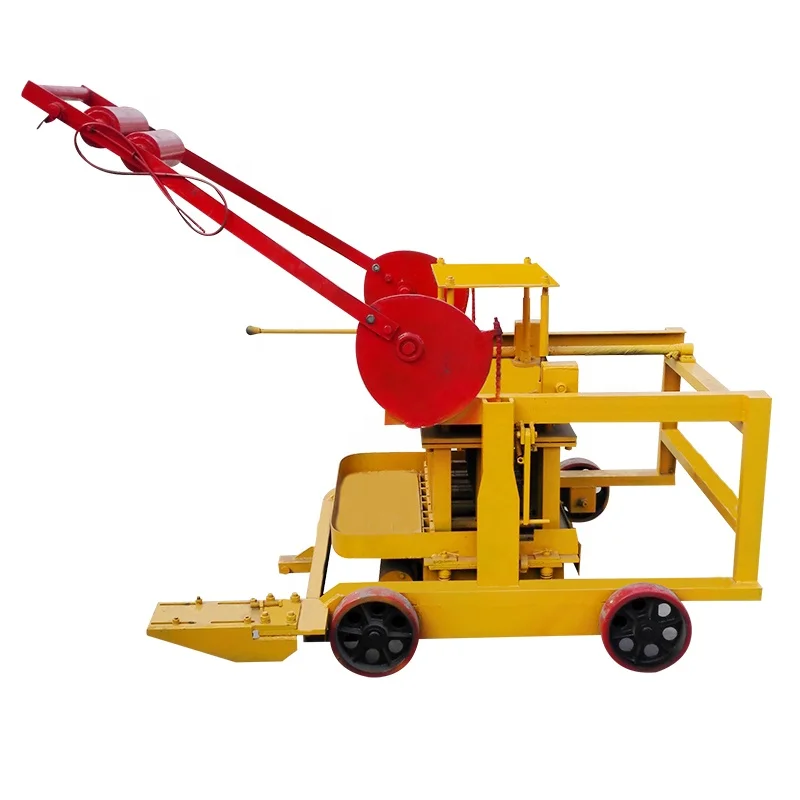
| Machine Type | Mobile / egg-laying |
| Automation Level | Manual |
| Pallet Requirement | No pallet required |
| Power Source | Electric |
| Labor Requirement | 1 to 3 workers |
| Mould Formats Available | 400×200×200mm / 400×150×200mm / 400×100×200mm hollow brick |
| Cycle Time (all listed formats) | 25–30 seconds |
| Output — 400×200×200mm | 160 pcs/h, 1280 pcs/8hr (2 pcs/mould) |
| Output — 400×150×200mm | 240 pcs/h (basis not stated in source) |
| Output — 400×100×200mm | 320 pcs/h, 2560 pcs/8hr (4 pcs/mould) |
| Spatial Footprint | Small space operation |
| Mobility | Free movement on site, no fixed plant |
| Vibration Force | Not stated in source |
| Hydraulic Pressure | Not applicable (manual mobile type) |
| Voltage & Frequency | Configurable to site supply |
| Standards | ISO 9001:2000, CE |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production | Crushed stone, sand and cement mixes laid directly on prepared ground |
| Small-scale block plant start-up | 400×200×200mm to 400×100×200mm hollow brick in confined yards |
| Contractor self-supply on building sites | Hollow concrete masonry units produced beside the structure being built |
| Distributor adding mobile capability | Hollow block formats serving scattered project demand without a fixed yard |
What "320 Blocks per Hour" Actually Means on a Real Site
The number only holds when you run the 400×100×200mm mould at four cavities per cycle.
I have stood on project sites in the Gulf where the foreman pointed at a nameplate rating and then pointed at a pallet stack that told a different story. A mobile block making machine specification sheet that quotes a single hourly figure without naming the block format sets the buyer up for a shortfall the moment the first shift ends. With the QMJ2-45, the output table is split across three hollow brick widths, each tied to its cavity count and a 25–30 second cycle, so the daily plan starts from a number that already knows which mould is bolted on [NEED_CITE: capacity calculation methodology for manual egg-laying block machines].
Where the Format Table Meets the Ground
Choosing a mobile block making machine is really choosing the block your market buys. The QMJ2-45 runs three hollow brick widths from one base frame. Switching from the 200mm width to the 100mm width doubles the cavity count per cycle, which is why the hourly figure moves from 160 to 320 pieces while the cycle time stays in the same 25–30 second band. That relationship is the one number buyers need to internalise before they compare quotes from different suppliers.
Pallet Elimination and What It Removes from the Site
Egg-laying machines leave each block where it is formed, so the curing yard does not need pallet racks, pallet return conveyors, or a forklift dedicated to pallet shuffling. On tight urban sites in the Middle East, that absence often decides whether the machine fits between the cement bags and the rebar stack at all. The QMJ2-45 needs only a level, compacted strip of ground and one worker guiding the next lay-down position while two others feed the mixer and the hopper [NEED_CITE: site preparation requirements for mobile egg-laying block production].
Reading the Specs That Actually Govern Block Quality
Vibration force and hydraulic pressure are the two numbers that decide whether a hollow block survives the journey from the mould to the wall. The QMJ2-45 is a manual mobile type with no hydraulic press stage, so consolidation relies on the vibration motor and the weight of the concrete column in the mould box. That makes the local aggregate grading and moisture content the variables you can adjust on site when a test block crumbles at the edges. Cycle time matters less than mix consistency; a 25-second cycle with poorly graded sand produces a weaker block than a 30-second cycle with a well-proportioned mix. Voltage and frequency, meanwhile, determine whether the vibration motor reaches its rated speed at all — a 50 Hz motor fed at 60 Hz will cycle faster but may overheat within the first production day.
When the Wrong Mould Stays Bolted On Too Long
A buyer who orders only the 200mm mould because it is the largest format will produce the fewest pieces per shift and may never reach the volume the business plan assumed. Equally, a buyer who plans around the 320-piece-per-hour figure but whose local market only specifies 200mm hollow blocks will find the machine sitting idle every time a customer asks for the larger format. The hidden cost is not a broken part; it is the shift that produced nothing sellable because the format list was never checked against the order book [NEED_CITE: common causes of low utilisation in small-scale block plants].
Why Buyers Come Back for the Second Machine
Block machinery is the single focus here, so the machine, mould, pallet strategy and handling are specified as one system rather than assembled from separate catalogues. The configuration conversation starts with the buyer’s actual mix design and local aggregate, not a default recipe. Mould drawings are supplied for the formats the buyer’s market actually orders, and custom mould design from buyer drawings is available when the standard range does not cover a local specification. Automation is selectable, meaning a buyer can begin with the manual QMJ2-45 and move to a semi-automatic or fully automatic line later without changing suppliers. Installation support and operator training are included so the first production day is not a learning curve paid for in broken blocks.
Documentation & Verification
- Line layout drawing naming the block format used for every capacity figure
- Machine specification sheet matched to your confirmed voltage and frequency
- Mould drawing and format list for each hollow brick width before production
- Factory test record run on your specified aggregate mix before dispatch
- Packing photographs showing dismantling and container loading arrangement
- Customs documentation package supporting your import clearance process
Installation, Commissioning & Support
- Level compacted ground strip prepared to the machine footprint before arrival
- Electric supply circuit confirmed to the agreed voltage and frequency rating
- Machine arrives partially dismantled; reassembly completed with basic hand tools
- First-run parameter setting adjusted to your local sand and cement proportions
- Operator training covers mould change procedure and daily vibration motor inspection
- Wear parts and mould replacement list provided before the first production week ends
Before You Request a Quote
Send the hollow block dimensions your market orders most often, the daily piece count you need from a single shift, and the voltage and frequency of the site supply. A sample or description of the local sand and aggregate lets the configuration start from your actual material rather than a generic assumption [NEED_CITE: raw material assessment for concrete block production].
Frequently Asked Questions
Q: How is the output capacity calculated for each hollow block format, and what cycle time is assumed?
A: Each capacity row ties a specific hollow brick dimension to its mould cavity count and a 25–30 second cycle. The 400×200×200mm figure uses two cavities per cycle, while the 400×100×200mm figure uses four. No single headline number is quoted without the format it belongs to, so the daily total you plan against already reflects the mould you will actually run.
Q: What block formats can the QMJ2-45 produce, and can custom mould sizes be supplied to my drawings?
A: The standard range covers 400×200×200mm, 400×150×200mm and 400×100×200mm hollow brick. When a local specification falls outside these dimensions, custom mould design is available from buyer-supplied drawings, provided the mould footprint stays within the machine’s mould box envelope and the cavity count remains practical for manual operation.
Q: What mix design and local aggregate work with this mobile machine, and how does that affect block strength?
A: Because the QMJ2-45 has no hydraulic press stage, block strength depends on vibration consolidation, aggregate grading and cement content. A sample of your local sand and stone lets the mix be adjusted before the first production run. Poorly graded or high-salt sand will produce weak blocks regardless of cycle time, so testing the local material is a necessary step.
Q: How long does a mould change take on the QMJ2-45, and what tools are required on site?
A: Mould change is a manual procedure using standard hand tools. The mould box is unbolted, lifted off with the site crane or block clamp, and the replacement mould is bolted in its place. Plan for the better part of a shift when changing formats for the first time; subsequent changes become faster once the crew knows the bolt pattern and alignment marks.