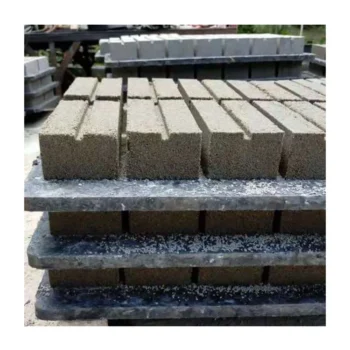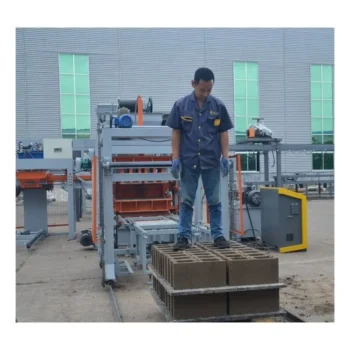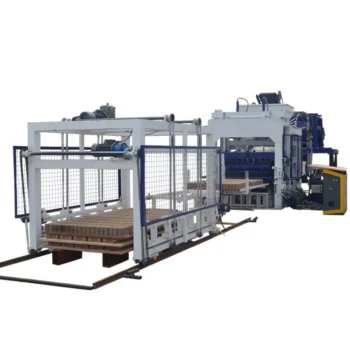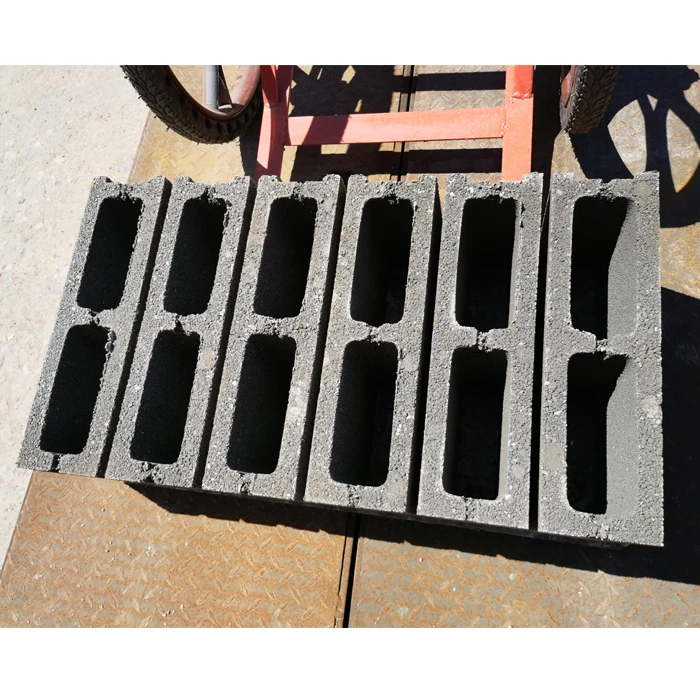

Description
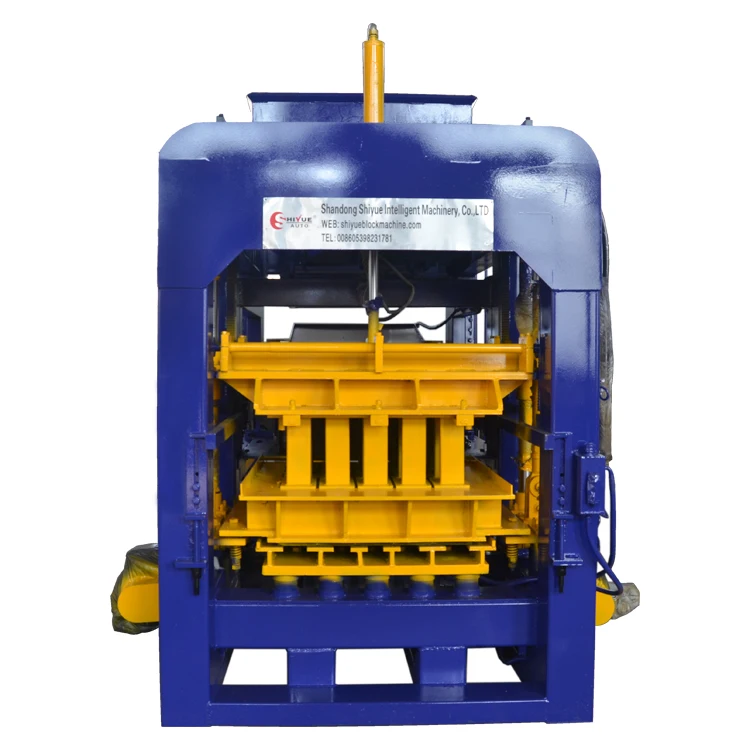
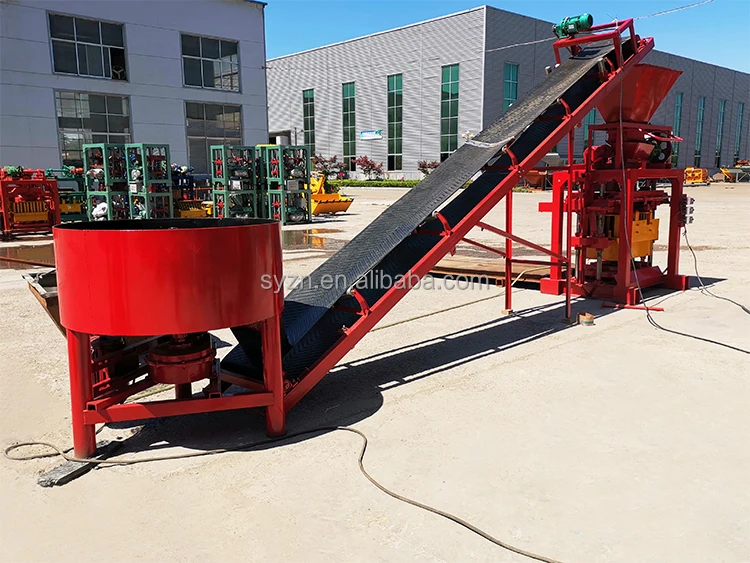
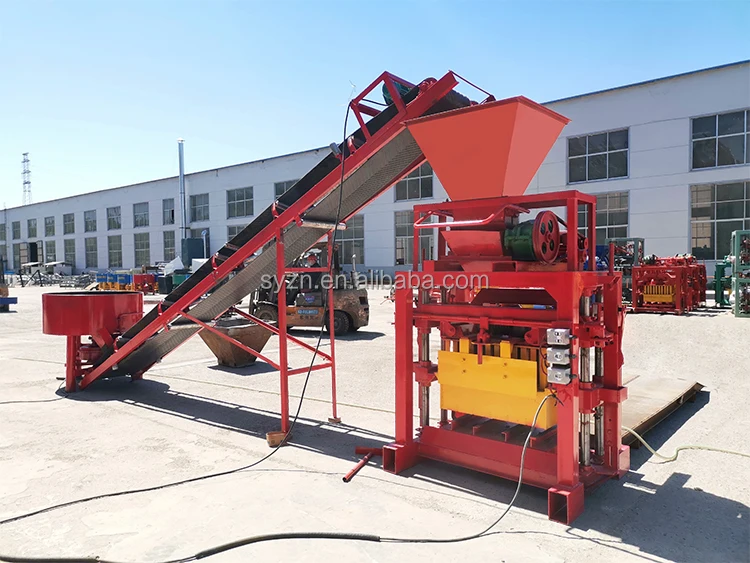
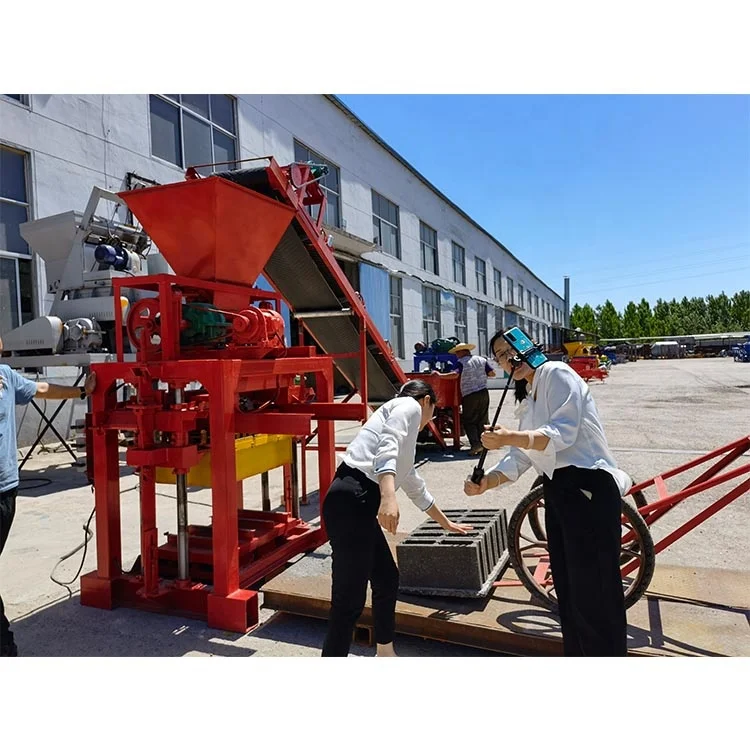
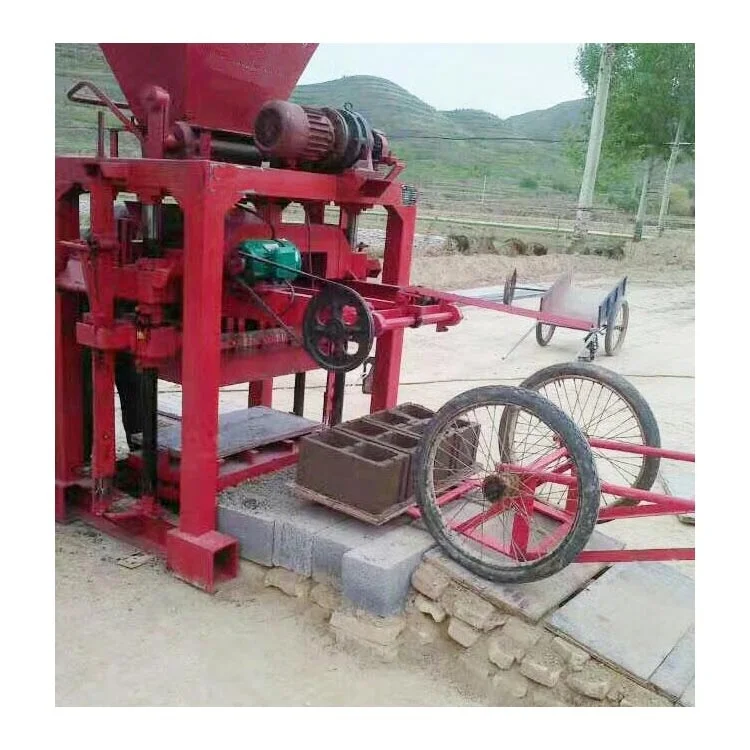
Mould and Format Matched — the QTJ4-35 block making machine configuration starts with the exact hollow block and paver dimensions your market sells, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
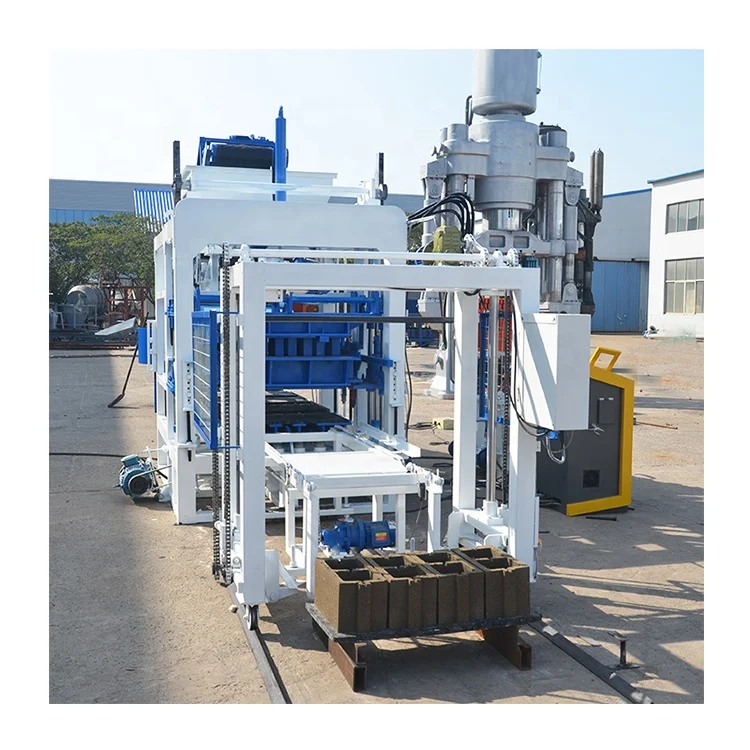
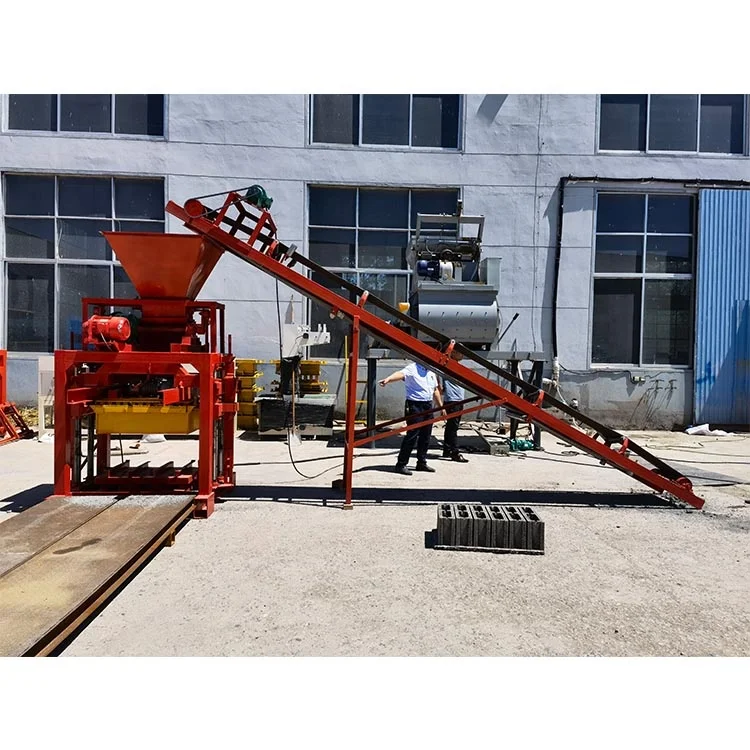
| Product Type | Semi-Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 1350×1460×1800 mm |
| Molding Cycle | 35 s (basis not stated in source — confirm block format and material) |
| Vibration Frequency | 2800 r/min |
| Exciting Force | 30 kN |
| Total Power | 11.15 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×450×20 mm |
| Net Weight | 1500 kg |
| Automation Level | Semi-automatic |
| Hydraulic System | High-pressure hydraulic station equipped |
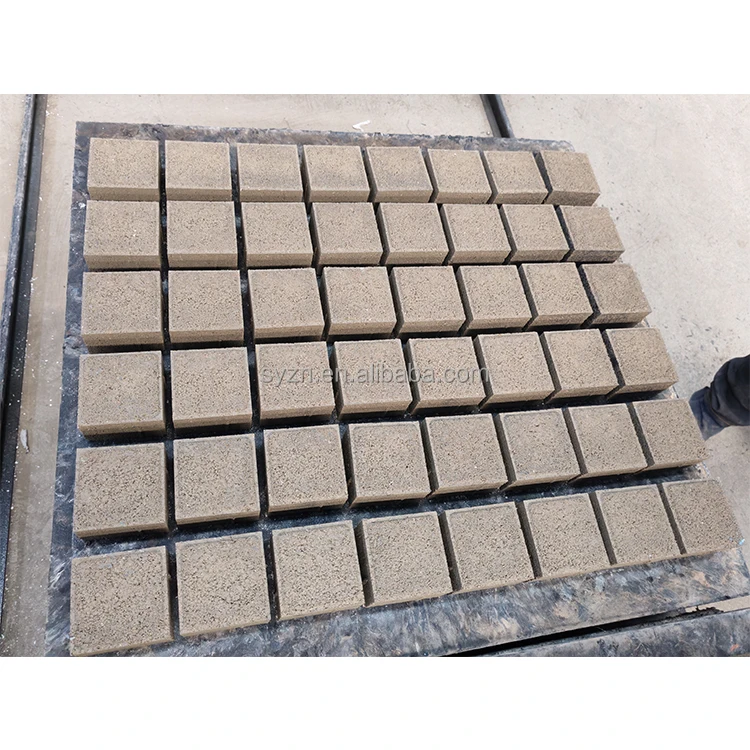
| Applied Products | Concrete hollow blocks (8 inch, 6 inch), solid bricks, pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, dust |
| Output Capacity (400×200×200 mm hollow block) | 408 pcs/h, 3264 pcs/8hr |
| Output Capacity (400×150×200 mm hollow block) | 510 pcs/h, 4080 pcs/8hr |
| Output Capacity (240×115×53 mm solid brick) | 2100 pcs/h, 17000 pcs/8hr |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block production | Crushed stone, sand, cement mix — 8 inch and 6 inch formats |
| Solid brick manufacturing for local housing | Cement and fly ash blends, standard 240×115×53 mm format |
| Paving block production for driveways and walkways | Dense aggregate mix with fine sand grading |
| On-site block production for construction contractors | Locally sourced aggregate with portable semi-automatic line |
| First block plant for entrepreneurs | Low investment entry with format flexibility to test market demand |
What "3264 Blocks per Day" Actually Means on Your Site
Capacity numbers only matter when tied to the exact block format you produce.
I once watched a contractor in West Africa unpack a machine rated for a certain daily output, only to discover the figure assumed a clean quartz sand mix his yard could not source. His local laterite aggregate carried high clay content, which absorbed vibration energy and left blocks crumbling at the edges. The crew spent half each shift scraping failed pieces off the pallets. The QTJ4-35 block making machine specifications in the table above list output per format — 408 pieces per hour based on a 400×200×200 mm hollow block, and 510 pieces per hour based on a 400×150×200 mm hollow block. If your market primarily buys 6 inch blocks, your real throughput sits at the second figure, not the first. [NEED_CITE: aggregate clay content impact on vibration compaction efficiency]
Cycle Time by Format, Not a Single Catalogue Number
The 35-second molding cycle applies differently depending on the mould installed. A 400×200×200 mm hollow block requires the full vibration window to push aggregate into deep cavities, while a flat paver may compact faster but demands higher surface finish. When we quote the QTJ4-35 block making machine, we state capacity per format so your daily plan matches what the operator actually stacks.
Pallet Size Determines Your Curing Layout Before Shipment
The 850×450×20 mm pallet is not arbitrary. It sets the spacing on your curing racks, the fork pocket width on your trolley, and the aisle gap between drying rows. We confirm pallet material — bamboo, steel, or PVC — against your climate and handling method before the machine enters production. If your forklift tines are spaced for a different width, blocks will be hand-carried off the line, and the semi-automatic advantage disappears.
Vibration Force and Hydraulic Pressure Working Together
The 30 kN exciting force at 2800 r/min drives aggregate particles into tight contact, while the high-pressure hydraulic station clamps the mould head down during compaction. Neither works alone: vibration without clamping pressure leaves blocks with porous top faces, and pressure without sufficient vibration traps air voids in the lower section. For the QTJ4-35, these two systems are balanced at the factory against a standard mix. When your local stone dust or fly ash differs from that baseline, we adjust vibration amplitude and mould clearance before dispatch. [NEED_CITE: hydraulic clamping force requirements for hollow block density standards]
When the Mix Design Does Not Match the Machine
A buyer once sent us photos of hollow blocks splitting along the web — the thin wall between cavities. The machine was running correctly, but his quarry sand contained fines below 75 microns that acted like a lubricant under vibration, pushing the mix out of the mould cavity before it set. On the QTJ4-35, we solved this by tightening the mould gap and reducing vibration duration for his specific material. Without that adjustment, any semi-automatic hydraulic block making machine would have produced the same cracked output. The lesson was clear: always send an aggregate sieve report before configuration is locked in. [NEED_CITE: fine aggregate particle size distribution and block web cracking]
Why Configuration Matters More Than the Sticker Price
Buying the cheapest unit and then discovering that voltage, PLC language, and pallet dimensions were never confirmed means weeks of idle time after arrival. A 1500 kg machine sitting in a container with the wrong frequency rating cannot be switched on until a transformer is sourced locally. The QTJ4-35 block making machine ships only after voltage, control display language, and pallet specification are documented and signed off.
Why Source This Machine Through Shiyue
- Block machinery is our single focus, so the press, mould, pallet, and JQ350 mixer are specified as one matched system.
- Configuration is set against your actual aggregate sieve report and target block format, not a generic default.
- Mould design covers the hollow block and paver dimensions your local market sells, with custom drawings available.
- Semi-automatic operation on the QTJ4-35 allows you to add automatic stacking or pallet handling later as volume grows.
- Factory testing runs your specific mix on the actual pallet size before crating, so output consistency is verified before shipment.
Documentation & Verification
- Line layout showing pallet flow from press through curing rack to stacking area
- Capacity calculation sheet stating block format for each output figure
- Mould drawing confirming exact cavity dimensions for your market
- Pallet specification matched to your curing area and forklift
- Voltage and control language confirmation sheet signed before production
- Factory test record on your aggregate blend before dispatch
Installation, Commissioning & Support
- Foundation pad must support 1500 kg static load plus dynamic vibration across 1350×1460 mm footprint
- Dedicated 11.15 kW circuit with correct voltage and frequency confirmed before wiring
- Machine ships partially assembled; hydraulic station and vibration motor connected on site
- First production run adjusts mould clearance and vibration timing to your aggregate
- Operator training covers mould change procedure and pallet feeding rhythm
- Wear parts list identifies hydraulic seals and vibration springs for reorder planning
What to Send With Your Inquiry
Provide the block formats your customers actually buy — dimensions, wall thickness, and daily volume target. Share a sieve analysis or photo of your local crushed stone and sand so we can match vibration settings and mould gap to your material. Confirm your site voltage, frequency, and the language your operators read on a control panel.
Frequently Asked Questions
Q: How is the output capacity verified and which block format does each figure assume?
A: Each capacity figure in the QTJ4-35 specifications is tied to a specific mould — 408 pieces per hour assumes a 400×200×200 mm hollow block, while 510 pieces per hour assumes a 400×150×200 mm hollow block. We provide a capacity calculation sheet listing every format you plan to produce so daily expectations are grounded in your actual product mix, not a single generic number.
Q: What mould formats are available and how long does a change take?
A: The QTJ4-35 supports hollow blocks in 8 inch and 6 inch sizes, standard solid bricks at 240×115×53 mm, and paver moulds. Mould change involves unbolting the current mould box, lifting it clear, and seating the replacement — typically handled by two operators within a shift break. We supply mould drawings for every format so dimensions are confirmed before the mould enters production.
Q: How should pallet size and material be chosen for my curing area?
A: The standard 850×450×20 mm pallet sets your curing rack spacing, forklift tine width, and aisle layout. We confirm whether bamboo, steel, or PVC pallets suit your humidity and handling method before shipment, so blocks move smoothly from press to drying area without manual re-stacking or pallet damage.
Q: What raw material mix does this configuration support?
A: The QTJ4-35 handles crushed stone, sand, cement, fly ash, and stone dust. We ask for your local aggregate sieve report to set vibration force and mould gap accordingly, because high clay or fine dust content changes how the 30 kN exciting force compacts the mix. Configuration is locked only after your material profile is reviewed.
Q: Are voltage, frequency, and control language confirmed before shipment?
A: Yes. Before the QTJ4-35 enters production we document your site voltage, frequency, and the display language your operators need. This avoids commissioning delays caused by mismatched electrical supply or unreadable control prompts after the machine arrives on site.