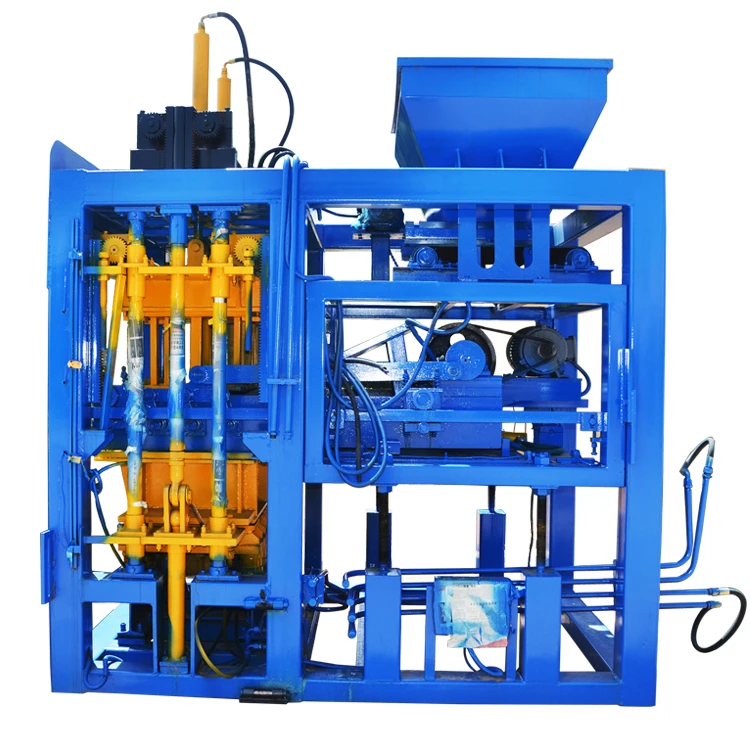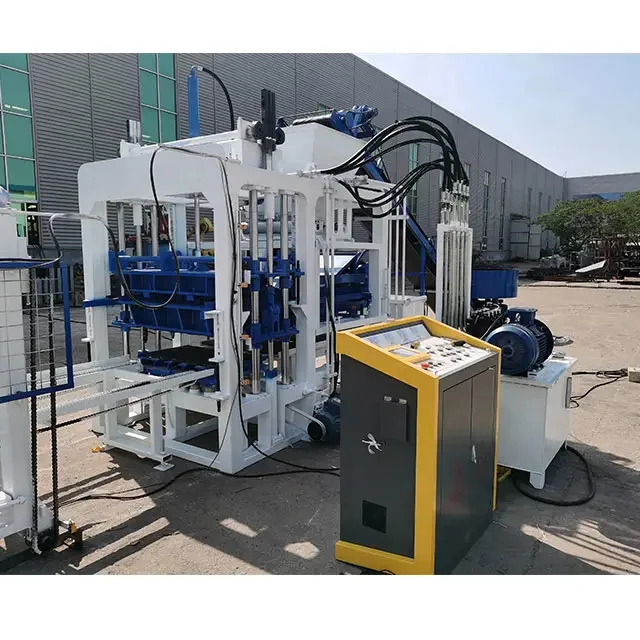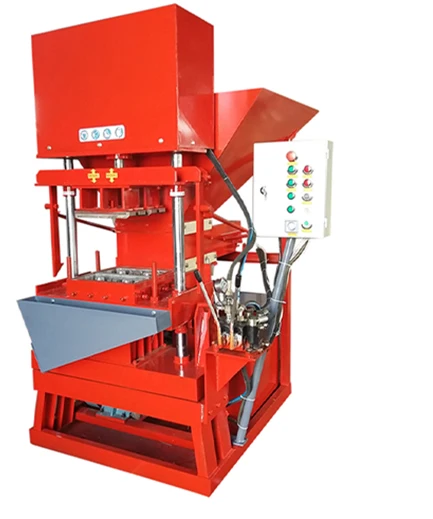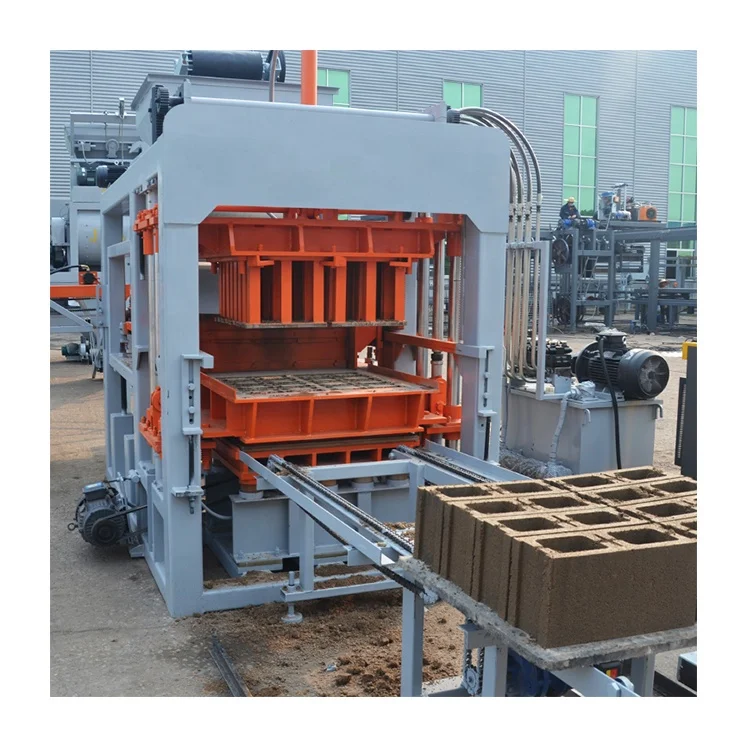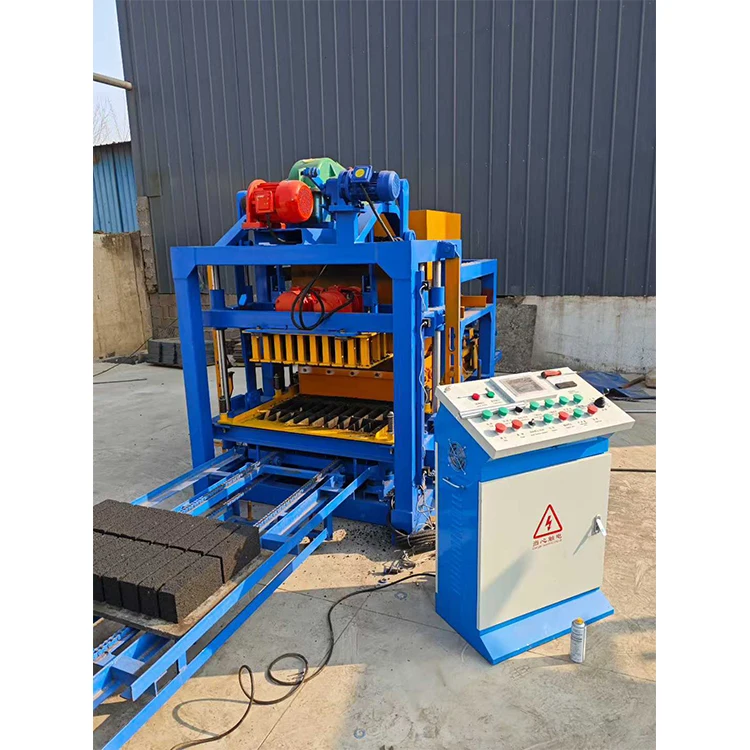
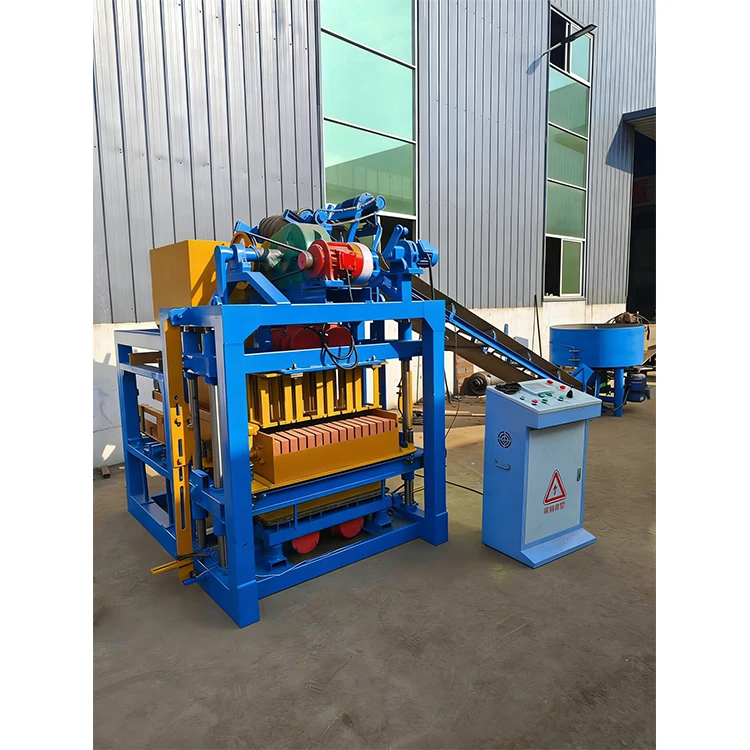
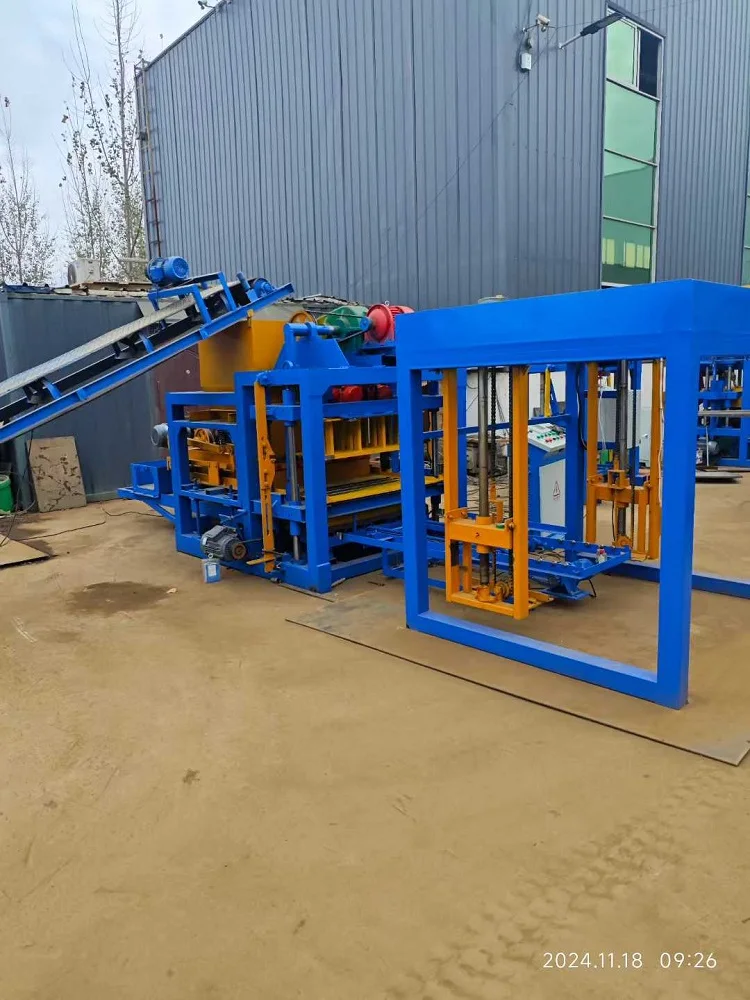
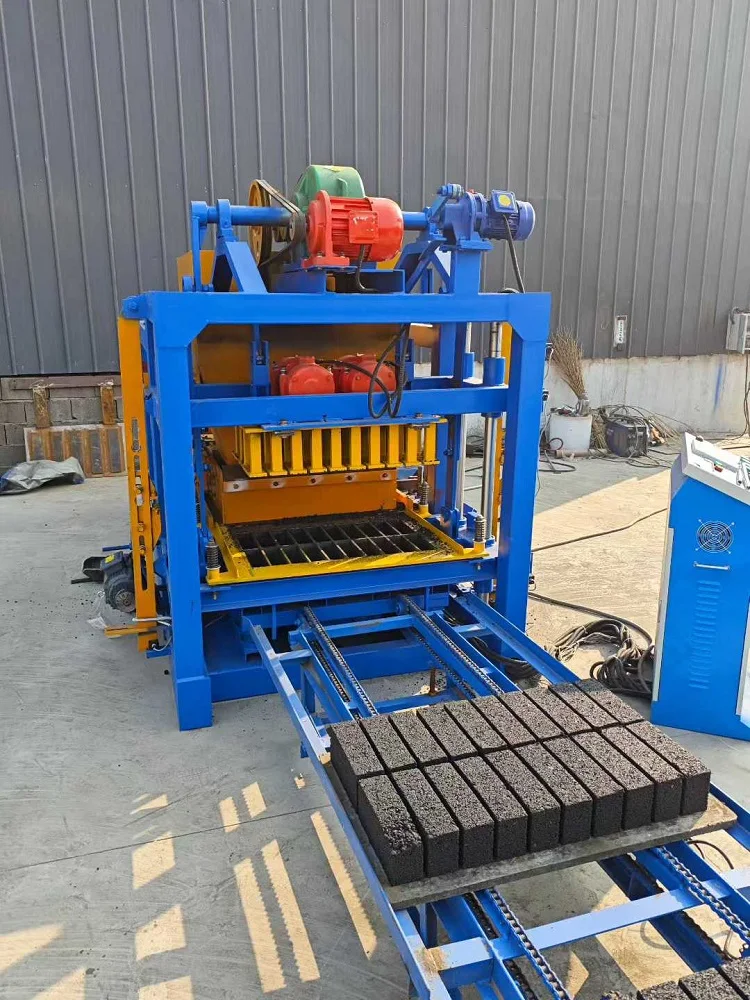

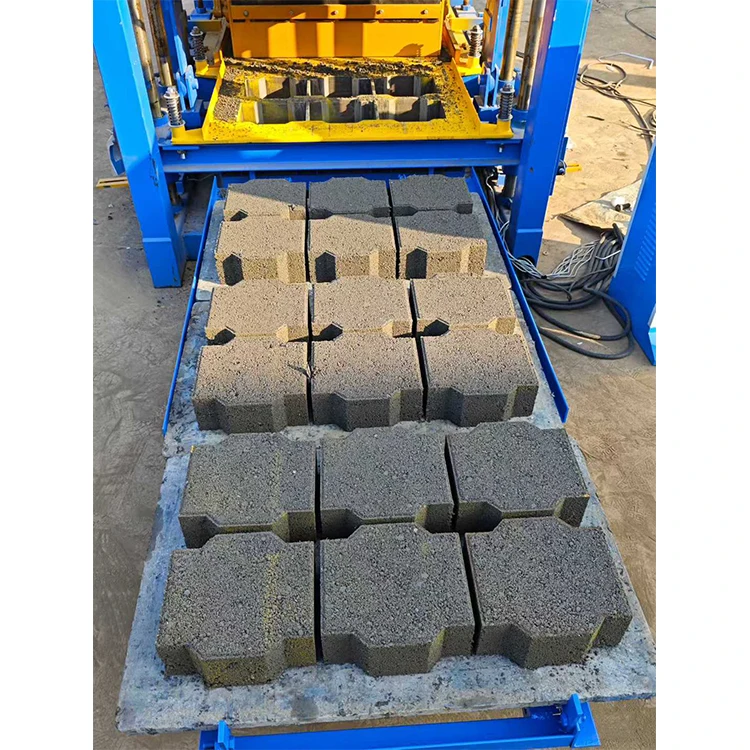
Description
Mould Matched to Format — every QTJ4-25 configuration is set against the buyer’s target block type, pallet size, and local aggregate before production begins.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
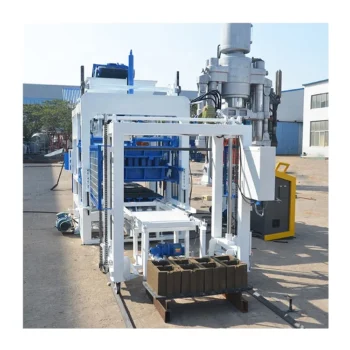
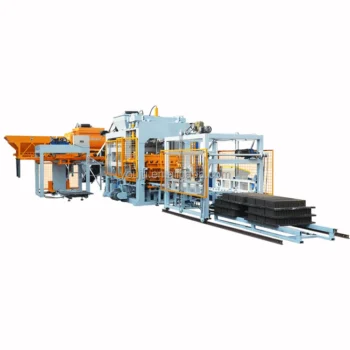
| Product Type | Automatic Concrete Block Making Machine |
| Rated Power | 16.58 kW |
| Voltage & Frequency | Configured to buyer’s local supply (basis to be confirmed) |
| Control System | PLC controlled, fully automatic |
| Overall Dimensions (L×W×H) | 6400 × 1500 × 2700 mm |
| Net Weight | 5000 kg |
| Cycle Time | 25 seconds |
| Pallet Size | 850 × 480 mm |
| Vibration System | Vibration motor with large vibration box (non-hydraulic) |
| Motor Brand | Siemens motor |
| Frame Construction | Thickened steel frame |
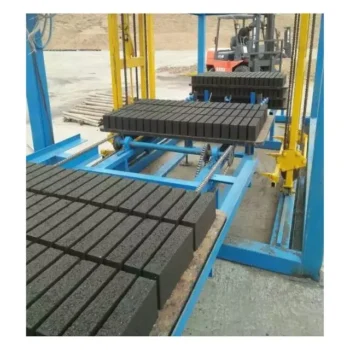
| Automation Level | Fully automatic — pallet feeding, material feeding, scraping, block stacking |
| Raw Materials | Concrete, sand, cement, fly ash, crushed stone, lime, water |
| Output Capacity | 4600 pcs / 8 hours (basis not stated in source — confirm block format) |
| Standards | CE (verify against manufacturer catalog) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, water |
| Solid brick manufacturing for load-bearing structures | Fly ash, cement, lime, sand |
| Paver stone production for walkways and driveways | Concrete mix with fine aggregate |
| Interlocking block production for retaining walls | Cement, crushed stone, sand blend |
| Porous brick manufacturing for permeable surfaces | Coarse aggregate, cement, controlled water ratio |
What "4,600 Pieces per 8 Hours" Actually Means on the QTJ4-25
The number only holds when the block format, mix density, and pallet cycle are all specified upfront.
I have watched buyers sign off on a capacity figure, then discover on commissioning day that the 4,600-piece rating assumed a small solid brick while their market needs 200 mm hollow blocks — cutting realistic daily output in half. The QTJ4-25 automatic block machine specifications change significantly across formats because each mould fills a different number of cavities per cycle. Without a per-format capacity sheet, you are guessing at your plant’s real throughput [NEED_CITE: block format and cavity count impact on cycle output].
Mould Selection Determines Your Real Daily Output
The 25-second cycle stays constant, but the pieces per cycle vary with every mould. A hollow block mould may produce four pieces per cycle while a solid brick mould produces twelve or more. When evaluating the QTJ4-25 automatic block machine specifications, request a capacity table that lists each format you intend to sell alongside its corresponding output. This is the only way to compare machines honestly.
Matching Pallet Size to Your Curing Yard
The 850 × 480 mm pallet is fixed on the QTJ4-25. Before ordering, measure your curing racks and forklift fork spread. A mismatch means pallets will not stack on your existing racks, or your forklift cannot carry them efficiently — bottlenecking the entire line downstream of the press [NEED_CITE: pallet and curing area compatibility in block plants].
How Vibration Without Hydraulic Pressure Shapes Block Density
The QTJ4-25 uses a vibration motor and large vibration box rather than a hydraulic press system. This design compacts the mix through sustained high-frequency vibration, which works well for standard hollow blocks and solid bricks in medium-density ranges. For high-strength paver stones requiring maximum compaction, buyers should discuss whether a hydraulic-assisted machine in the range would better serve their format. The non-hydraulic configuration keeps maintenance simpler and power consumption lower, but block strength is directly tied to how well the vibration parameters match your specific aggregate gradation and cement ratio [NEED_CITE: vibration compaction versus hydraulic press in block forming].
The Cost of Skipping Format-Level Capacity Confirmation
When a buyer orders based on a single headline number, the wrong mould often arrives first. A mould swap that should take minutes can consume a full shift if the change system was not specified correctly, and the formats you paid for sit unused while you run only the one mould that happens to work. I have seen plants operate at half their machine’s potential for months before anyone revisited the original quotation [NEED_CITE: mould change downtime in block production].
Why Procurement Here Is Different
Block machinery is the single focus, so the QTJ4-25 is specified as one matched system — machine, mould, pallet, and handling — rather than assembled from separate suppliers. Configuration starts with your actual mix design, local aggregate, and target block format, not a catalogue default. Mould design covers the formats your market sells, with custom drawings available when standard options fall short. Automation level is selectable, so you can begin with the fully automatic setup or plan an upgrade path later. Installation includes operator training so your team understands cycle settings, mould change procedure, and daily maintenance from day one.
Documentation & Verification
- Line layout showing QTJ4-25 footprint with each station and pallet flow path
- Capacity calculation sheet listing output per block format you intend to produce
- Mould drawing and format list confirming cavity count and changeover procedure
- Pallet specification with size, material grade, and curing rack compatibility note
- Voltage and PLC display language confirmation signed off before production
Installation, Commissioning & Support
- Foundation plan sized for the 6400 × 1500 mm footprint and 5000 kg operating weight
- Dedicated circuit rated for the 16.58 kW total load with correct voltage and frequency
- Machine arrives with pallet feeder and stacking unit disconnected for container loading
- PLC parameters tuned to your confirmed block format and local mix during commissioning
- Operator training on mould change, vibration adjustment, and Siemens motor maintenance
- Wear parts list covering vibration box components and scraper blades for first reorder
What We Need to Quote Accurately
Provide the exact block formats your market sells, including dimensions and required strength class. Share your local raw material source — river sand, crushed stone, fly ash — with a sample if possible. Confirm your site voltage, frequency, and preferred PLC language. If you have existing curing racks or forklifts, send their dimensions so the 850 × 480 mm pallet is verified against your setup before production begins.
Frequently Asked Questions
Q: How is the 4,600 pcs/8h capacity calculated for the QTJ4-25?
A: That figure is based on a specific block format that must be confirmed per order. Different moulds produce different piece counts per 25-second cycle. We provide a per-format capacity table so you know exactly what to expect for each block type you plan to manufacture before committing.
Q: What mould formats are available, and how long does a mould change take?
A: Standard options cover hollow blocks, solid bricks, pavers, and interlocking formats. Mould change time depends on the changeover system specified. Request the format list and changeover procedure in your quotation so you can plan production shifts around realistic swap durations.
Q: How do I match the 850 × 480 mm pallet to my curing setup?
A: Measure your curing rack spacing and forklift fork width before ordering. If your existing racks accept a different pallet size, discuss alternatives early — pallet dimensions affect every station downstream, from stacking to curing to dispatch.
Q: What voltage and PLC language are confirmed before shipment?
A: Voltage, frequency, and PLC display language are confirmed during the quotation stage and written into the production order. This prevents commissioning delays caused by mismatched electrical supply or an interface your operators cannot read on arrival.
Q: How does the non-hydraulic vibration system affect block strength?
A: The vibration motor and large vibration box compact the mix through high-frequency vibration alone. Block strength depends on matching vibration duration and amplitude to your specific mix design and aggregate. For formats requiring higher density, discuss whether hydraulic assistance is needed.