Description
Per-format capacity honesty — The QT10-15 block moulding machine capacity is stated per block format with cycle time and mould cavity count, so daily output matches your actual selling format rather than a misleading headline number.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT10-15 |
| Product Type | Hydraulic Block Making Machine |
| Control System | PLC control cabinet |
| Hydraulic System | Independent integrated hydraulic station |
| Vibration Mode | Vertical station mode resonance with automatic FM-AM |
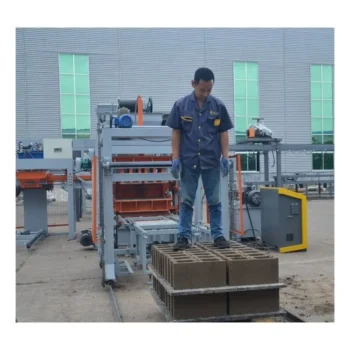
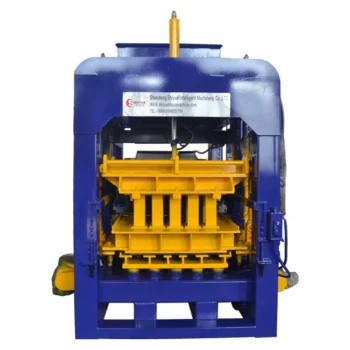
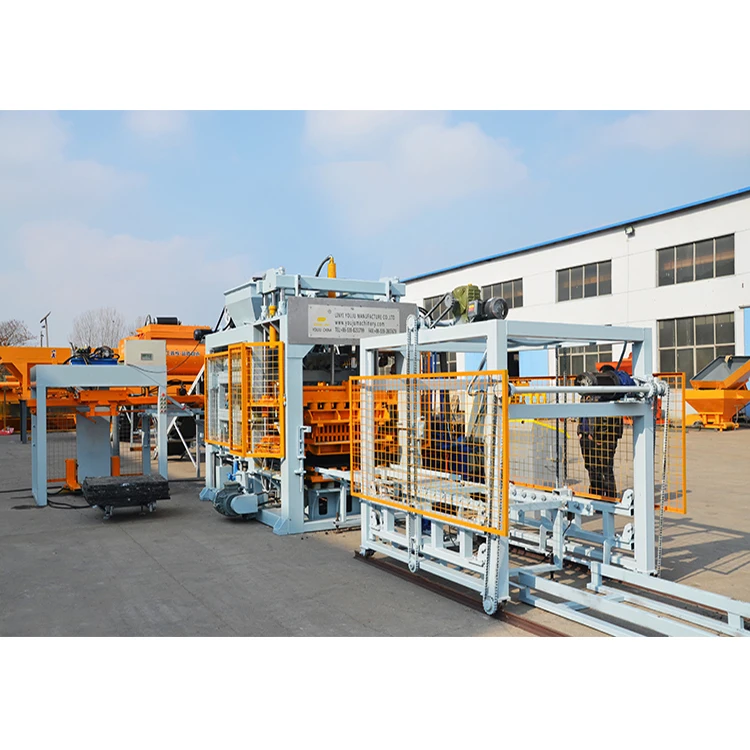
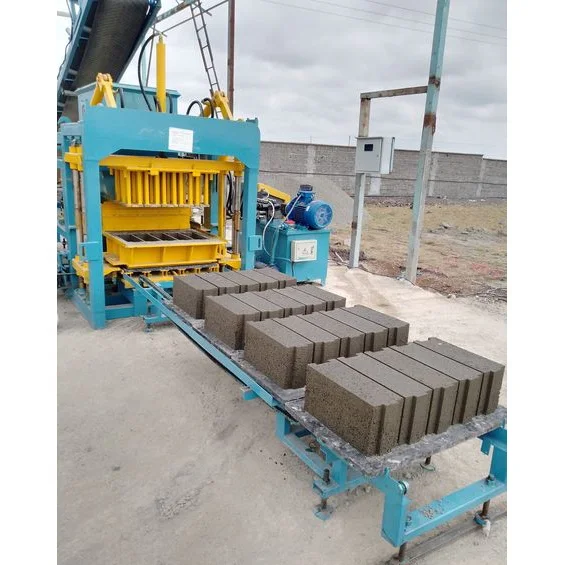
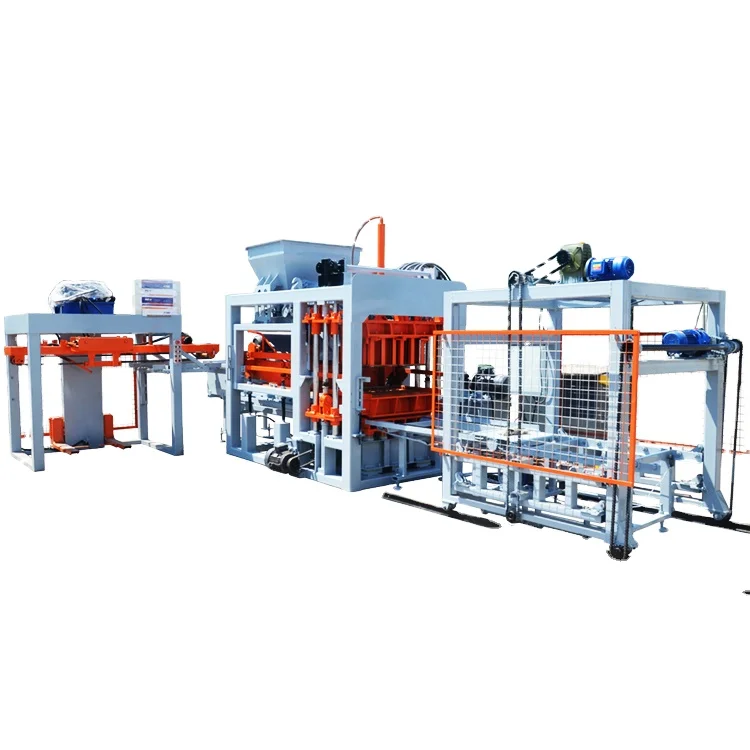
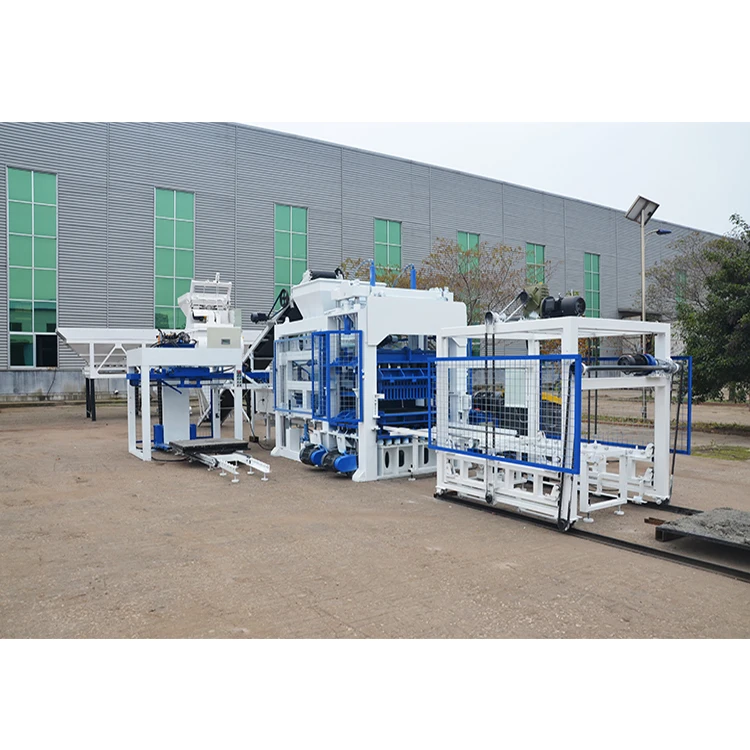
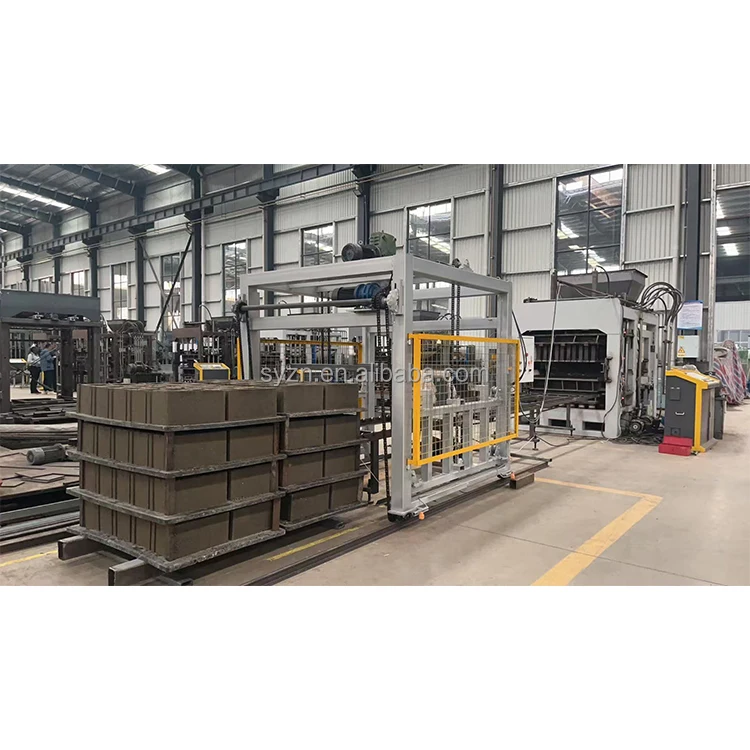
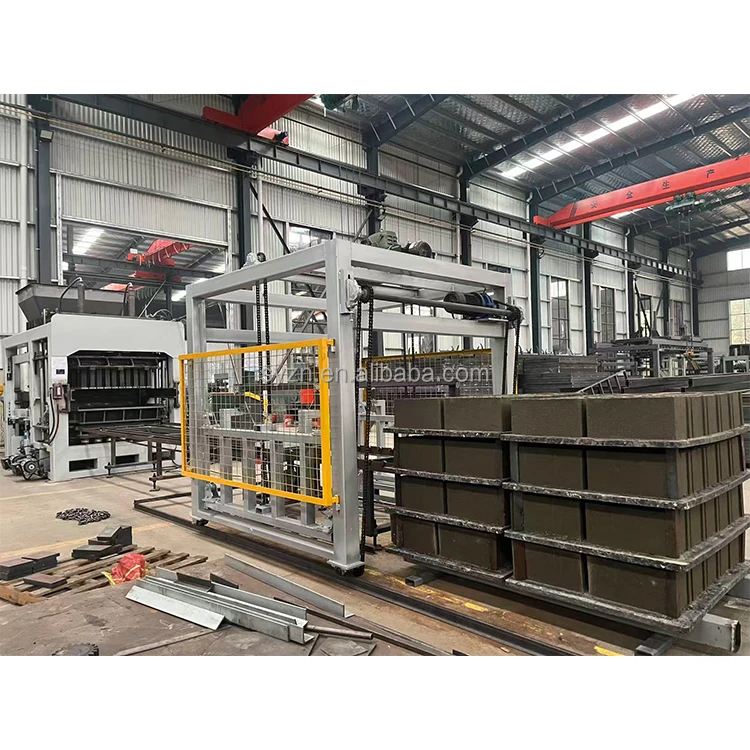
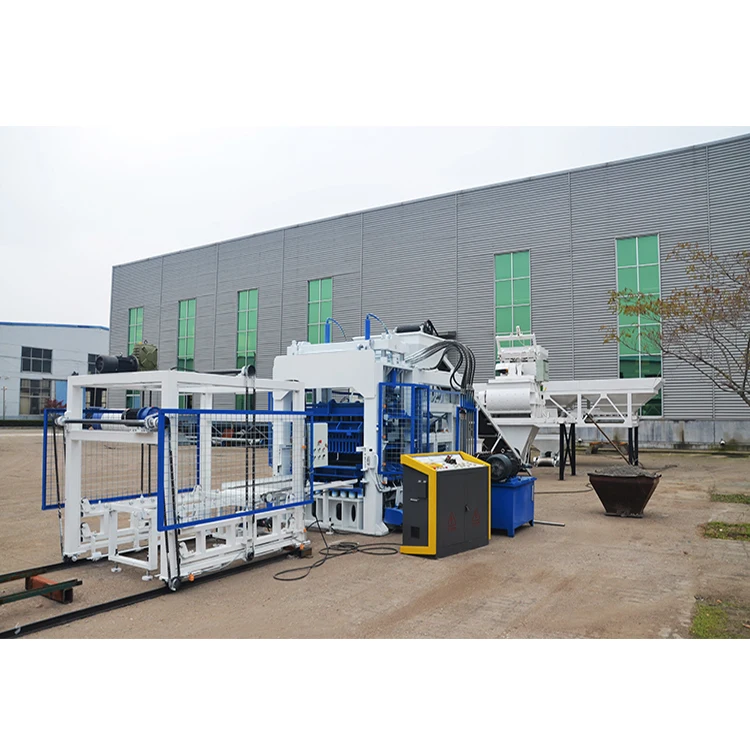
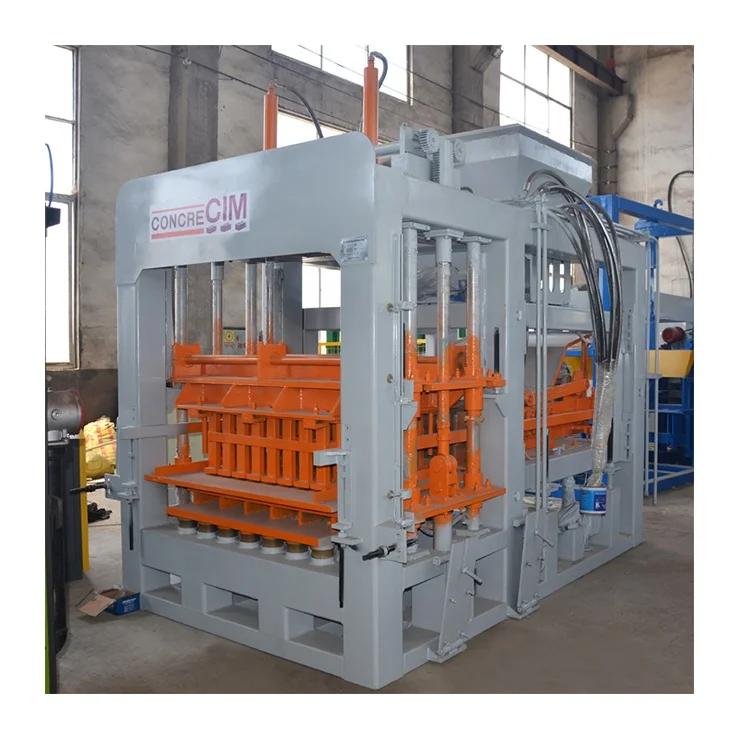
| Components Included | Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
| Mould Change | Simple replacement of mold for multi-format production |
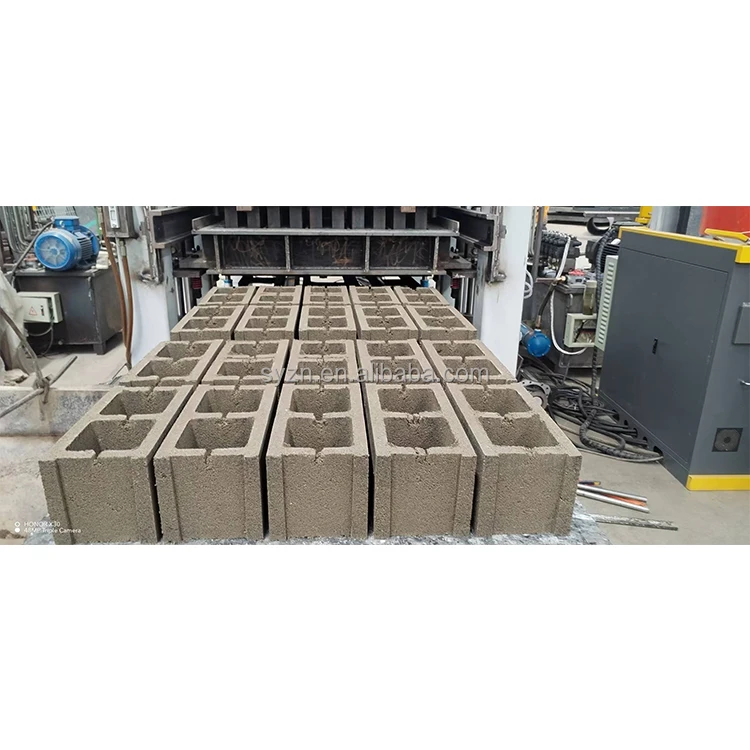
| Output Capacity (400x200x200mm hollow block) | 1800-2400 pcs/hour, 14400-19200 pcs/8hr (basis: 10 pcs/mould, 15-20s cycle) |
| Output Capacity (400x150x200mm hollow block) | 2160-2880 pcs/hour, 17280-23040 pcs/8hr (basis: 12 pcs/mould, 15-20s cycle) |
| Output Capacity (240x115x53mm solid brick) | 8928-11160 pcs/hour, 71424-89280 pcs/8hr (basis: 62 pcs/mould, 15-20s cycle) |
| Output Capacity (200x100x60mm paving block) | 5184-6480 pcs/hour, 41472-51840 pcs/8hr (basis: 27 pcs/mould, 20-25s cycle) |
| Output Capacity (225×112.5x60mm interlocking block) | 4032-5040 pcs/hour, 32256-40320 pcs/8hr (basis: 24 pcs/mould, 20-25s cycle) |
| Cycle Time (hollow block) | 15-20s |
| Cycle Time (paving block) | 20-25s |
| Warranty | 1 year for whole machine (excluding spare parts) |
| Hydraulic Pressure | (source value not stated — confirm with manufacturer) |
| Vibration Force | (source value not stated — confirm with manufacturer) |
| Pallet Size | (source value not stated — confirm with manufacturer) |
| Rated Power | (source value not stated — confirm with manufacturer) |
| Voltage & Frequency | (source value not stated — confirm with manufacturer) |
| Overall Dimensions | (source value not stated — confirm with manufacturer) |
| Net Weight | (source value not stated — confirm with manufacturer) |
Application Suitability
| Application | Material or Output |
|---|---|
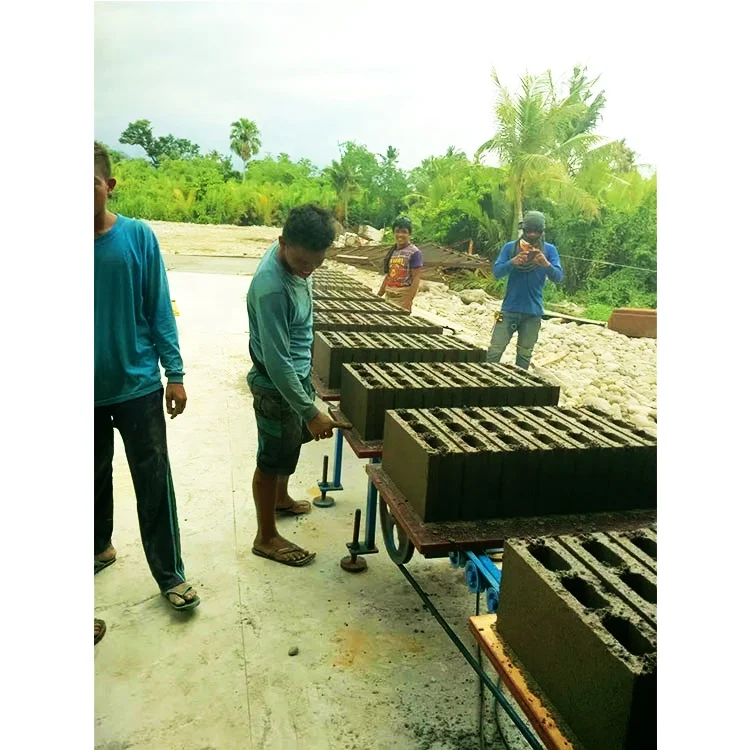
| Hollow block production | Crushed stone, river sand, cement, and fly ash blends for load-bearing and partition walls |
| Paving block production | High-density aggregate mixes for driveways, walkways, and municipal paving |
| Standard solid brick production | Fine aggregate and cement for masonry and infill applications |
| Interlocking brick production | Graded aggregate with cement for retaining walls and landscape edging |
What "1800 Blocks per Hour" Leaves Out About the QT10-15 Block Moulding Machine
The QT10-15 block moulding machine capacity only means something when tied to a specific block format, mould cavity count, and cycle time.
I have watched buyers sign contracts based on a single headline output number, then discover on commissioning day that their primary selling format runs at less than half that rate. One buyer in East Africa ordered based on a hollow block capacity figure, but his daily production was dominated by paving blocks with a longer cycle time and fewer cavities per mould [NEED_CITE: common mismatch between quoted capacity and actual product mix in block plants]. The machine itself was fine; the expectation was wrong from the start. That is why every capacity figure on this page states the exact block dimensions, pieces per mould, and cycle time it is based on.
Cycle Time Differences Across Block Formats
The QT10-15 block moulding machine runs hollow blocks on a 15-20 second cycle but shifts to a 20-25 second cycle for paving blocks and interlocking pavers. That five-second difference compounds across an eight-hour shift. A buyer producing primarily 200x100x60mm paving blocks will see a noticeably different daily total than one running 400x200x200mm hollow blocks all day. Matching the machine to your market’s dominant format is the first step in sizing a plant correctly.
Mould Cavity Count and Its Effect on Hourly Totals
Cavity count varies sharply by format. The solid brick mould carries 62 pieces per press, while the hollow block mould holds 10. This means hourly throughput in pieces is far higher for solid bricks even at the same cycle speed. When you plan production around the QT10-15 block moulding machine, confirm which format drives your revenue and calculate daily output from that row of the table, not the highest number in the list.
Reading the Capacity Table Without Optimism Bias
The ranges shown reflect ideal feeding conditions, consistent mix moisture, and uninterrupted pallet supply. In a working plant, pallet return delays, mix variations, and mould change intervals all eat into the shift [NEED_CITE: real-world block plant utilization rates versus nameplate capacity]. Treat the upper end of each range as a benchmark to approach, not a guaranteed daily figure to promise your customers.
How Vibration and Hydraulic Pressure Shape Block Density
Vertical station mode resonance with automatic FM-AM allows the vibration force to be tuned across formats. Hollow blocks with thin webs need high-frequency, lower-amplitude vibration to consolidate the face mix without cracking the shells. Paving blocks demand sustained high pressure and lower-frequency vibration to achieve the density required for vehicular traffic. The independent integrated hydraulic station sits isolated from the vibration table, which keeps hydraulic oil cleaner and valve response consistent over long production runs. Together, these systems determine whether your blocks meet the compressive strength your local standard requires — or whether they crumble at the curing rack.
Selecting the Wrong Pallet Size for Your Curing Yard
Pallet dimensions on the QT10-15 must match the racking system in your curing area and the fork spacing on your existing forklift. If the pallet is too wide for your rack bays, you will be rebuilding the curing zone before the first production run. If it is too narrow, you waste capacity on every cycle. Confirm pallet size against your site layout before the machine enters production [NEED_CITE: pallet dimension compatibility with curing infrastructure in block plants]. This single check prevents costly rework that has nothing to do with the press itself.
The Hidden Cost of Unconfirmed Voltage and PLC Language
A machine wired for a voltage that does not match the local grid will trip breakers or burn out motors on startup. A PLC display in a language the operator cannot read turns a minor sensor fault into a half-day shutdown while someone translates the error code. These issues surface only after the QT10-15 arrives on site, when the cost to fix them includes idle labour and delayed project timelines [NEED_CITE: commissioning delays caused by unconfirmed electrical specifications]. Confirming voltage, frequency, and control display language before production begins is a small step that protects your entire commissioning schedule.
Why Sourcing the QT10-15 Through a Format-Focused Supplier Matters
Every mould we supply is designed around the block format your market actually buys, including custom drawings when your region uses a non-standard dimension. The machine, mould, pallet, and handling equipment are specified as one matched system so cycle times align from the mixer through to the stacking station. We configure vibration and hydraulic settings against your actual mix design and local aggregate — not a catalogue default — so block strength meets your standard from the first run. Automation level is selectable, letting you start with semi-automatic pallet handling and add automatic stacking later as volume grows. Factory test records document performance on your specified format before the machine ships.
Documentation & Verification
- Line layout drawing showing each station and pallet flow path for the QT10-15
- Capacity calculation sheet stating the exact block format and cycle basis used
- Mould drawing and format list confirming cavity count and changeover procedure
- Hydraulic and electrical schematic with valve and sensor reference numbers
- Factory test record run on your specified block format before dispatch
- CE declaration of conformity where applicable to the destination market
Installation, Commissioning & Support
- Foundation plan showing load points and anchor bolt positions for the QT10-15 frame
- Electrical supply specification confirming voltage, frequency, and dedicated circuit rating
- PLC parameter setting and cycle tuning on your local mix during commissioning
- Operator training covering mould change procedure and daily maintenance checks
- Wear parts and mould list with part numbers for reorder planning
- Ongoing technical support for parameter adjustment as your mix design evolves
What We Need to Configure the QT10-15 for Your Plant
To match the QT10-15 block moulding machine to your production target, share your primary block format and the secondary formats you plan to add. Tell us what aggregate and cement are available locally so we can run a mix trial and set vibration parameters accordingly. Confirm your site voltage and frequency, the language your operators need on the PLC display, and the pallet dimensions your existing curing racks accept. With those details we can return a line layout with honest capacity per format.
Frequently Asked Questions
Q: How is output capacity calculated for each block format on the QT10-15?
A: Each capacity figure is based on the number of pieces per mould multiplied by the cycle time for that specific format, then projected to an hour and an eight-hour shift. Hollow blocks at 15-20 seconds per cycle and paving blocks at 20-25 seconds per cycle produce different totals even on the same machine. Always reference the row that matches your primary selling format.
Q: What block formats can the QT10-15 produce, and how does mould change work?
A: The machine covers hollow blocks, solid bricks, paving blocks, and interlocking pavers through mould replacement. The mould change procedure involves removing the securing bolts, lifting the current mould, and seating the new one. Mould drawings are provided for each format so you can verify dimensions and cavity count before ordering.
Q: How should vibration force and hydraulic pressure be matched to my raw material?
A: Different aggregates and mix moisture levels require different vibration frequencies and pressure settings. We ask for a sample of your local aggregate and cement to run a trial, then set the automatic FM-AM vibration parameters and hydraulic pressure accordingly. This ensures block strength meets your local standard without over-compacting or under-consolidating the mix.
Q: What pallet size does the QT10-15 require, and how do I check compatibility?
A: Pallet size must match both the machine feed mechanism and your existing curing racks and forklift. Confirm your rack bay width and fork tine spacing before we finalise the pallet specification. We provide a pallet drawing in the documentation package so your site team can verify fit before the machine arrives.
Q: What documentation comes with the QT10-15 block moulding machine?
A: The package includes a line layout, capacity calculation per format, mould drawings, hydraulic and electrical schematics, a factory test record on your specified format, operation and maintenance manual, wear parts list, and CE declaration where applicable. Packing photographs and customs documentation support are provided before shipment.