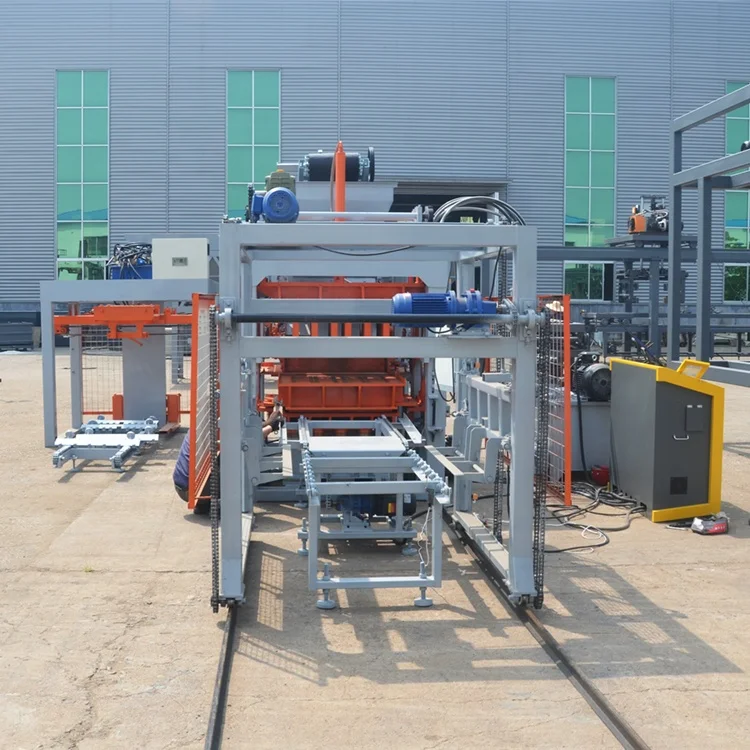
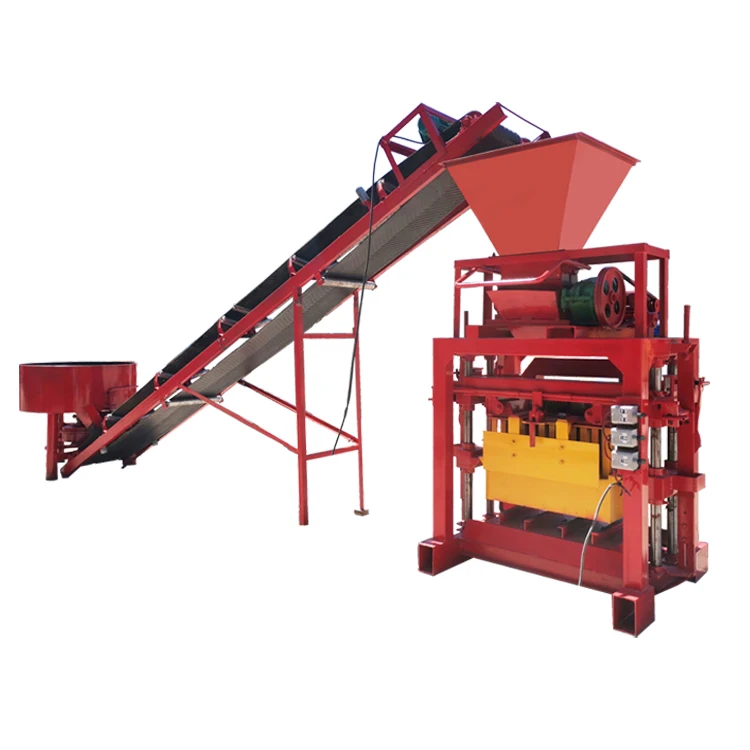


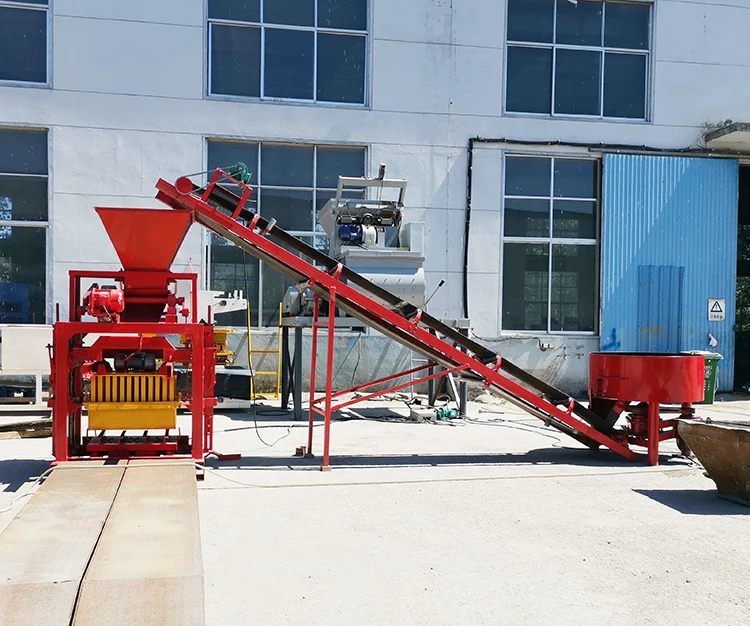

Description
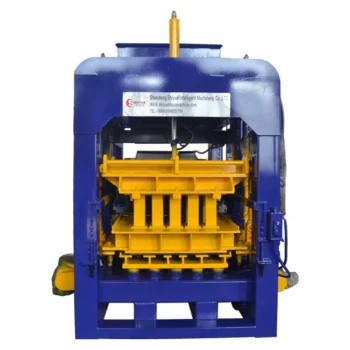
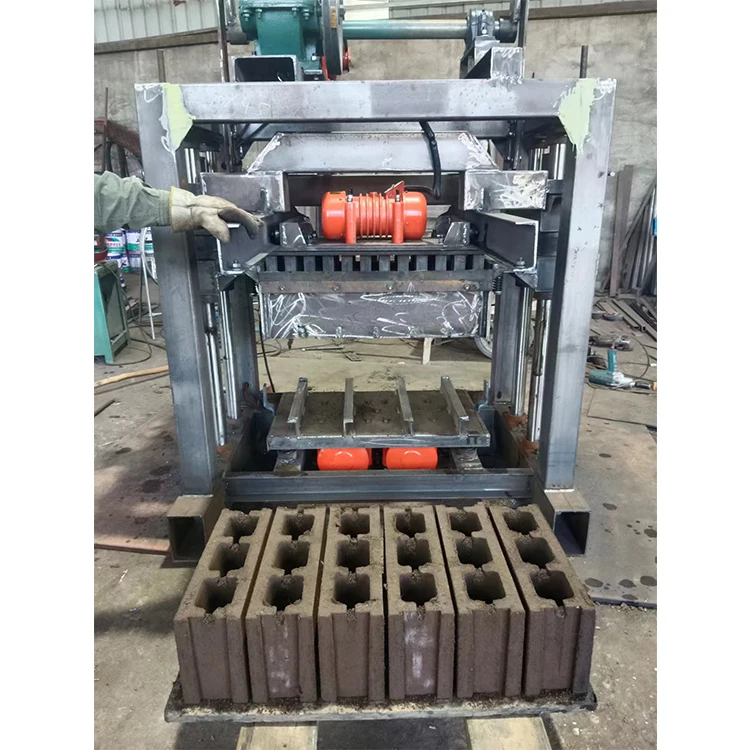
Four-lead structure — motor vibration calibrated to your specific block format and mix design, not a catalogue default
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
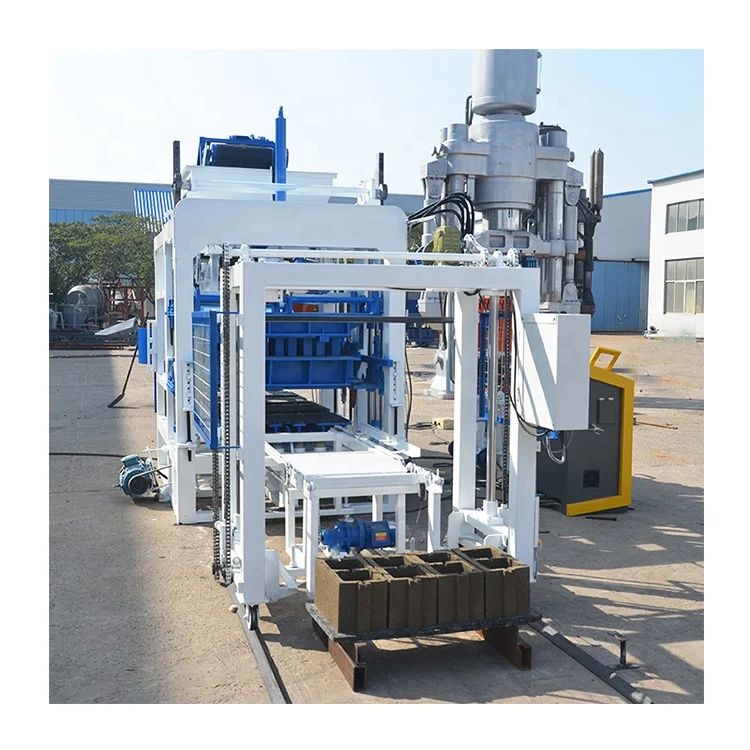
| Product Type | Mechanical Manual Block Making Machine |
| Overall Dimensions (L×W×H) | 2050 × 1660 × 1900 mm |
| Main Vibration Form | Motor Vibration |
| Vibration Force | 35 kN |
| Overall Power | 9.8 kW |
| Pallet Size | 850 × 450 × 20 mm |
| Molding Cycle | 35 s (basis not stated in source) |
| Lead Configuration | Four-lead |
| Mould Change System | Manual (upper and bottom mould compression) |
| Automation Level | Mechanical manual |
| Voltage & Frequency | Configurable (basis to be confirmed before order) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow concrete block production (400×200×200 mm, 400×150×200 mm) | Cement, crushed stone, sand mix |
| Solid brick production (240×115×53 mm) | Cement and fine aggregate |
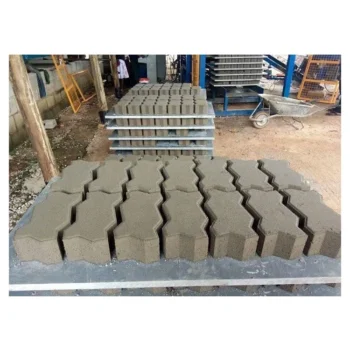
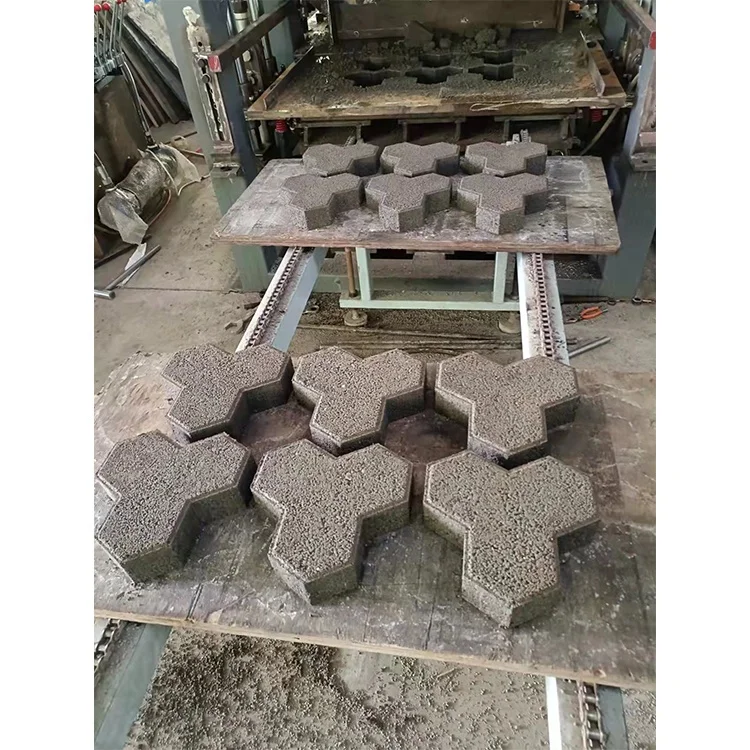
| Paving block production (200×100×60 mm) | Cement with graded aggregate |
| Interlocking block production (225×112.5×60 mm) | Cement and local aggregate blends |
| Small-scale on-site construction production | Site-sourced materials with manual batching |
What the Moulding Cycle Figure Hides from You
A 35-second cycle only means something when tied to the exact block format you intend to sell.
I’ve seen this exact confusion shut down a job site in Amman. The buyer ordered a machine quoting a headline cycle time, but when the local aggregate proved sticky and slow to feed, the actual output for interlocking blocks dropped sharply. The line sat idle while workers waited for material. Real daily output on the QTJ4-35 block machine depends entirely on whether you’re pressing 400×200×200 mm hollow blocks or 240×115×53 mm solid bricks — and whether your local sand, gravel, or volcanic ash behaves in the hopper the way standard test sand does [NEED_CITE: material flow properties of regional aggregates in block production].
How Format Determines Real Cycle Time
The QTJ4-35 block machine compresses each pallet differently depending on the mould mounted. Hollow blocks require longer vibration dwell to consolidate the thin walls, while solid bricks compact quickly but demand higher consistency in the feed mix. A buyer running paving blocks all week will see a different rhythm than one switching between hollow blocks and interlocking pavers each morning.
Why Pallet Size Dictates Your Curing Workflow
The 850 × 450 × 20 mm pallet size is not arbitrary — it must match the forklift tine spacing and the curing rack dimensions already in your yard. I’ve watched crews in Jeddah manually re-stack fresh blocks because the pallets from a new machine didn’t fit their existing racks. Confirming pallet material (bamboo, PVC, or steel) against your local humidity and handling method prevents that waste from day one [NEED_CITE: pallet material selection for block curing environments].
Vibration Force and Block Density
The 35 kN motor vibration, combined with the four-lead mechanical guide, delivers consistent compaction across the mould cavity. For hollow blocks, this vibration force must be balanced against the hydraulic or manual compression to avoid cracking thin webs. For interlocking blocks, uneven vibration creates dimensional drift that makes on-site assembly impossible. The upper and bottom mould compression system on the QTJ4-35 keeps block density uniform when the correct mould and mix are paired.
The Hidden Cost of Skipping Mix Verification
A machine configured for standard silica sand will struggle with the high-clay soils common in parts of Iraq or the lightweight volcanic aggregate used in East Africa. When the mix design doesn’t match the vibration force and cycle settings, blocks crack during curing or fail compressive strength tests. Fixing this after installation means sourcing new materials or paying for re-commissioning — costs that dwarf the extra week a pre-shipment trial would have taken [NEED_CITE: block compressive strength variation with local aggregate substitution].
Why Buyers Choose This Configuration
Every QTJ4-35 is specified against the buyer’s actual target block format, not a generic brochure number. The mould list, pallet specification, and capacity calculation arrive together so nothing is left to assumption. Voltage and control language are confirmed before production starts, preventing the commissioning delays I’ve seen stall projects across the Levant. The mechanical manual design means operators can maintain the machine with basic tools, and mould changes remain possible without specialised equipment.
Documentation & Verification
- Capacity calculation sheet stating output per block format and assumed mix
- Mould drawing and format list confirming included and optional moulds
- Pallet specification with material, thickness, and forklift compatibility notes
- Voltage, frequency, and control language confirmation record before production
- Factory test record on your specified block format before dispatch
Installation, Commissioning & Support
- Foundation pad leveled to 2050 × 1660 mm footprint with drainage provision
- Dedicated 9.8 kW circuit with correct voltage and frequency for your site
- Machine arrives assembled; manual pallet handling verified on your pallet stock
- First-run parameter setting matched to your local aggregate and mix proportions
- Operator training covers mould change procedure and vibration force adjustment
- Wear parts list includes mould liners and vibration motor brushes for local sourcing
What We Need to Configure Your Machine
To size the QTJ4-35 to your production reality, share the block formats your market actually buys, the daily volume you need to sustain, and the raw materials available within hauling distance of your site. Include your existing pallet size and forklift type if you plan to integrate with current curing infrastructure. State your local voltage and frequency so the electrical system is built correctly before shipment.
Frequently Asked Questions
Q: How is cycle time verified for each block format on the QTJ4-35?
A: Each format — hollow block, solid brick, paver, interlocking — has a different compaction requirement. We run a factory test on your specified format and record the actual cycle, noting how your local aggregate’s flow behaviour affects feed time. The capacity calculation you receive states the format assumed, so daily planning is realistic.
Q: Can the QTJ4-35 work with my local aggregate and mix design?
A: Yes, but only if we verify the mix before building the machine. I’ve seen volcanic ash and high-clay soils cut output dramatically because the hopper couldn’t feed fast enough. We request a sample or detailed aggregate description, then adjust the vibration force and mould compression settings to match your material, not a standard test sand.
Q: What pallet size does the machine require, and will it fit my curing area?
A: The QTJ4-35 uses 850 × 450 × 20 mm pallets. Before confirming your order, we need to know your existing curing rack dimensions and forklift tine spacing. Choosing the wrong pallet material — bamboo, PVC, or steel — for your humidity level also causes warping and block rejection, so we specify this together.
Q: How long does a mould change take, and can I run multiple formats per shift?
A: The manual mould change system uses upper and bottom compression, which requires the operator to unbolt and reseat the mould set. In practice this takes a meaningful portion of a shift, so we advise buyers to plan one primary format per day and batch secondary formats across the week rather than switching mid-shift.