Description
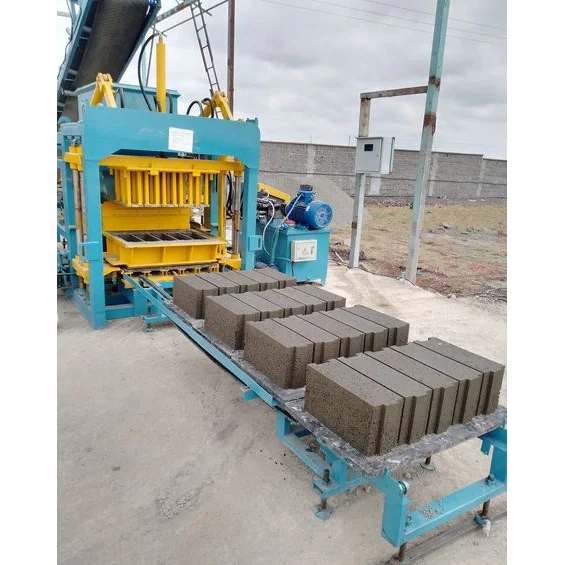
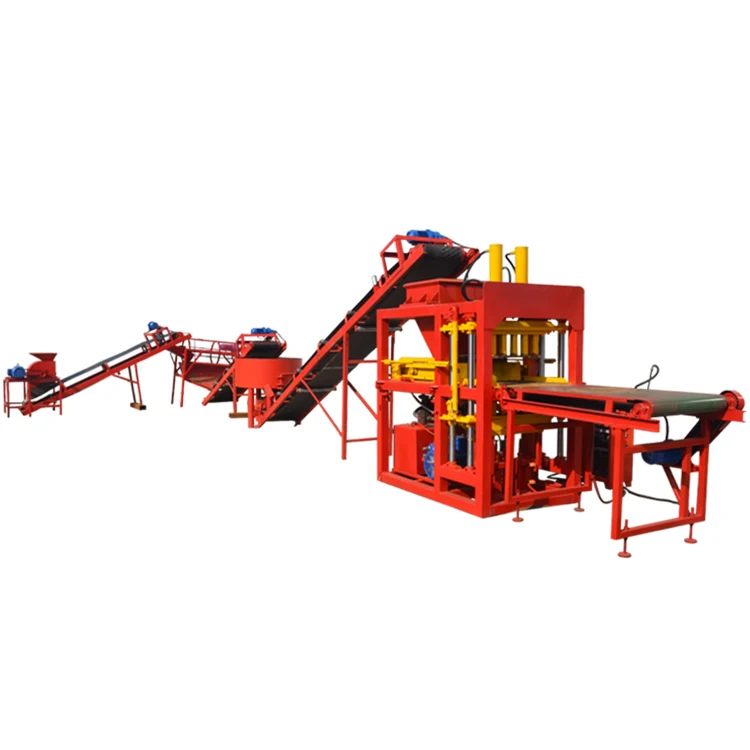
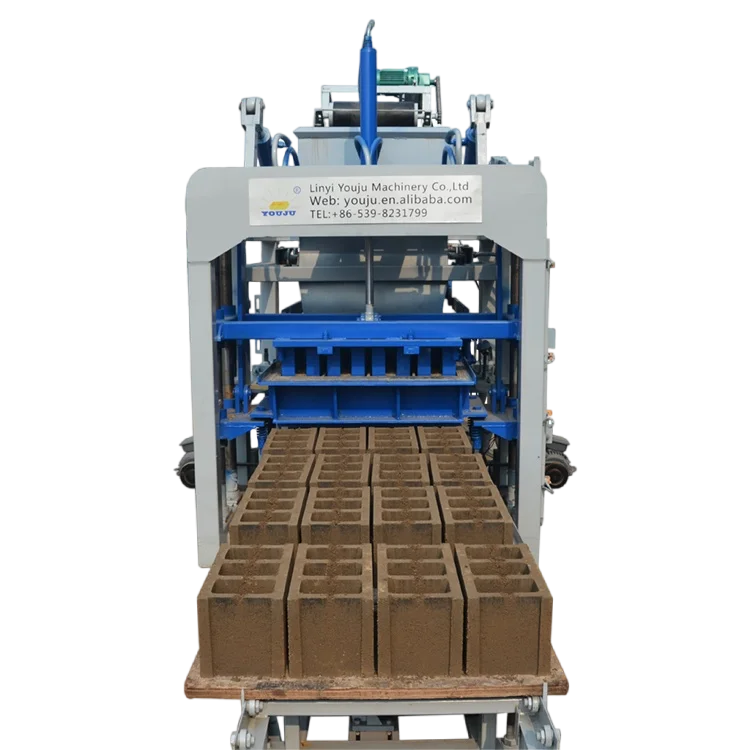
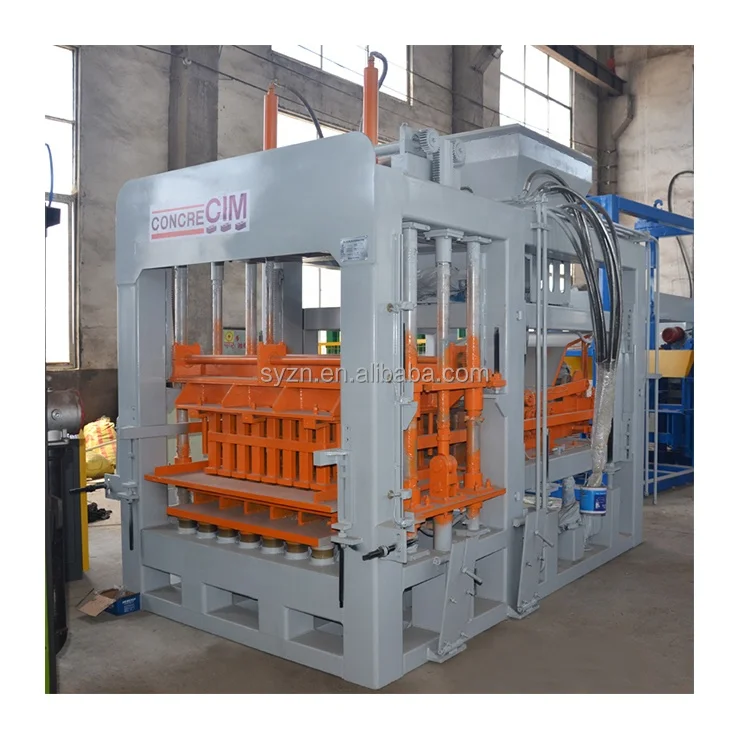
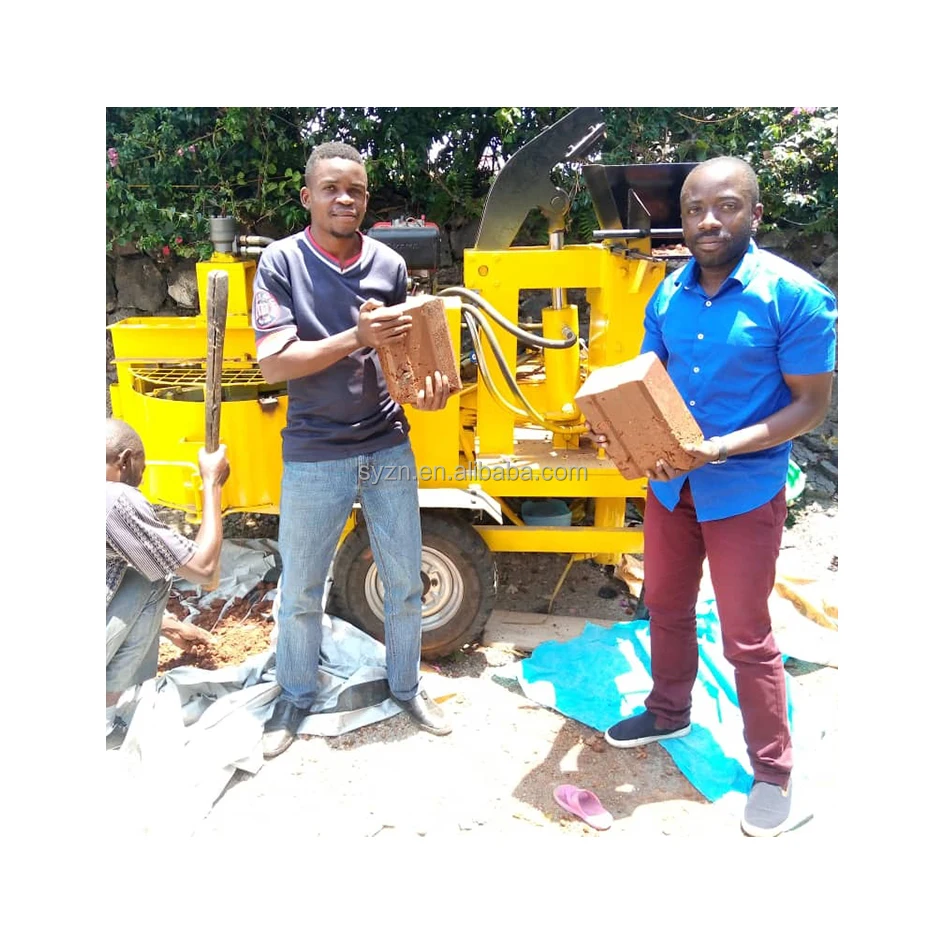
Matched Mould and Mix Design — Every M7MI configuration starts with your local clay or soil sample, ensuring the hydraulic pressure and mould profile produce interlocking blocks that meet your market’s strength and format requirements.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | M7MI |
| Product Type | Hydraulic Interlocking Clay Brick Making Machine |
| Engine Type | Diesel Engine |
| Rated Power | 7.5 kW |
| Hydraulic Pressure | 16 MPa |
| Molding Cycle | 15–20 s |
| Production Rate | 200 pcs/h (based on 300×150×100 mm interlocking block, 20 s cycle, 1 pc/mould) |
| Daily Output | 1600 pcs/8 hr (based on 300×150×100 mm interlocking block) |
| Overall Dimensions (L×W×H) | 3200×1100×1500 mm |
| Total Mass | 1100 kg |
| Raw Materials | Clay, soil, concrete |
| Block Locking Method | Interlocking (mortar-free assembly) |
| Mould Change Capability | Yes, multiple interlocking block formats |
| Automation Level | Semi-automatic / mobile |
| Power Source | Diesel (off-grid capable) |
| Certification | CE (confirm per shipment) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site housing project production | Local clay or soil mixed with cement, interlocking format |
| Off-grid construction sites with no electricity | Diesel-powered operation using available earth materials |
| Small-to-medium contractor block yards | Soil-cement interlocking blocks for mortar-free wall systems |
| Rural development and infrastructure projects | Clay bricks produced directly at the building location |
| Entrepreneur-started brick operations | Locally sourced soil with minimal processing infrastructure |
What "2200 Pieces per Day" Actually Means for Your Block Format
Output figures only matter when the block format behind them is stated.
The M7MI interlocking clay brick machine specifications you see quoted online often carry a single daily number with no format attached. In practice, a 300×150×100 mm interlocking block cycles differently from a thinner paving profile or a wider wall block, and the hydraulic stroke must complete fully before the next press. When I first started sending machines to West Africa, buyers would reference a headline capacity and then wonder why actual site output looked different once their specific mould was installed. The honest approach is to tie every throughput number to the exact block dimensions, cycle time, and material mix [NEED_CITE: block format and cycle time relationship in mobile brick presses].
Mould Selection Determines Your Real Throughput
The M7MI supports multiple interlocking block formats through mould swaps, but each format carries its own cycle time and demoulding behaviour. A taller block with deeper interlock channels requires longer hydraulic dwell and careful extraction, while a simpler profile presses faster. The M7MI interlocking clay brick machine specifications should always be read alongside the mould drawing for the format your market actually buys, because the machine’s physical stroke and vibration sequence are tuned to the cavity depth and soil-cement ratio of that specific profile.
Diesel Power and Off-Grid Production Realities
Many interlocking block projects are located where grid electricity is unreliable or absent entirely. The M7MI’s diesel engine eliminates the dependency on a stable power supply, but it introduces a different set of considerations: fuel availability on site, engine maintenance intervals, and noise levels in residential construction zones. Buyers who have operated both diesel and electric mobile presses report that the diesel option removes the single largest cause of commissioning delays — waiting for an electrical connection that the site was supposed to have ready [NEED_CITE: off-grid construction equipment power source selection].
Reading the Specs That Actually Affect Block Quality
The 16 MPa hydraulic pressure is the figure that most directly governs block density and compressive strength, but pressure alone does not guarantee a good interlocking block. The soil-cement mix must have the right moisture content and particle distribution to consolidate under that pressure without cracking at the interlock edges. The 15–20 second molding cycle range reflects the adjustment needed when switching between a drier clay mix and a wetter soil blend. Machine mass at 1100 kg provides the reaction force necessary to keep the press stable during the hydraulic stroke, which matters particularly on uneven ground at a construction site. The 3200×1100×1500 mm footprint means the M7MI can be positioned close to the building area, reducing the distance workers carry each block [NEED_CITE: hydraulic pressure and soil-cement mix interaction in block forming].
The Hidden Cost of Skipping the Soil Sample
When a mobile clay brick machine arrives on site and the local soil has higher clay content or different grain size than what the mould was designed for, the blocks may release with fractured interlock tongues or insufficient density at the locking channels. I recall a shipment where the test run used standard loam, but the buyer’s actual red laterite soil required significant adjustment to hydraulic dwell time and moisture addition. Two weeks passed before production stabilised. Sending a raw material sample before the machine is configured avoids this entirely and lets the mould clearance and press parameters be set to your specific earth material from the first day.
Why This Configuration Approach Works
Every M7MI is configured against the buyer’s actual soil sample and target block format rather than shipped at a catalogue default setting. Mould design covers the interlocking profiles that sell in your specific market, including custom drawings if your buyers demand a profile we do not already tool. The machine, mould, and any supporting pallet handling are specified as one matched system, so nothing arrives incompatible. Automation level starts at semi-automatic with a clear upgrade path if your operation grows. Commissioning includes operator training on your specific material, and wear parts lists are provided so the first replacement order can be placed before the original parts are exhausted.
Documentation & Verification
- Line layout with capacity calculation tied to your chosen interlocking block format and cycle time
- Mould drawing and format list confirming every interlocking profile included in the delivery
- Diesel engine specification sheet and hydraulic schematic for on-site maintenance reference
- Factory test record run on your soil-cement sample before the machine is crated
- Operation and maintenance manual with mould change procedure and wear parts schedule
- CE declaration where applicable to your import market requirements
Installation, Commissioning & Support
- Level compacted ground required; the 3200×1100 mm footprint fits standard site clearances
- Diesel fuel supply and basic tool kit needed for first-day operation on arrival
- Hydraulic system pre-filled at factory; connections verified during on-site commissioning
- Mould fitted and tested with your soil sample; cycle time adjusted to your mix behaviour
- Operator training covers mould change sequence, daily greasing points, and block stacking method
- Wear parts list with hydraulic seal kit and mould liner replacement intervals documented
What We Need to Configure Your Machine
To move from a general enquiry to a firm configuration, the most useful information you can share includes the interlocking block format your market demands, a sample or description of your local soil or clay type, and whether your site has any electricity available at all. Knowing your target daily output lets us calculate the shift length and crew size needed around the M7MI. If you have an existing curing area or block storage practice, tell us so the delivery sequence can match your site layout.
Frequently Asked Questions
Q: How is daily output calculated, and which interlocking block format does each figure assume?
A: The stated 1600 pieces per 8-hour shift assumes a 300×150×100 mm interlocking block at a 20-second cycle with one block per mould stroke. Different formats change the cycle time and blocks per stroke, so your actual output must be recalculated once the specific mould profile and your soil-cement mix behaviour are confirmed during the factory test.
Q: Which clay or soil types are suitable, and how is the machine configured to the buyer’s local material?
A: The M7MI processes clay, soil, and concrete mixes, but each material behaves differently under 16 MPa hydraulic pressure. We ask buyers to send a raw material sample so the mould clearance, moisture target, and cycle dwell can be adjusted before shipment. This prevents the on-site re-tuning that delays production when the machine arrives set to a generic default.
Q: What mould formats are available, and how long does a mould change take on site?
A: Multiple interlocking profiles are available, and custom moulds can be produced from buyer drawings. Mould change on the M7MI involves unbolting the current cavity plate and fitting the replacement, a task that trained operators complete within a standard shift break. The exact changeover time depends on the profile complexity and whether the new mould requires hydraulic limit adjustment.
Q: What block strength can be expected from the 16 MPa hydraulic pressure with a given soil-cement mix?
A: Compressive strength depends on the soil-cement ratio, moisture content, and curing practice as much as the press pressure itself. At 16 MPa with a properly graded soil-cement mix, interlocking blocks typically meet the requirements for single and double-storey load-bearing walls. A sample test run on your material provides the actual strength data for your specific mix before the machine ships.