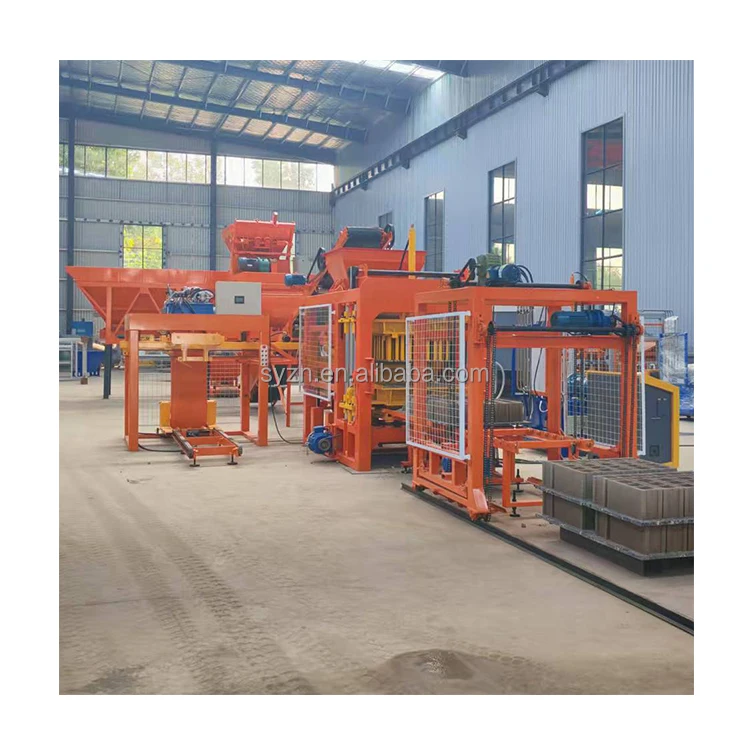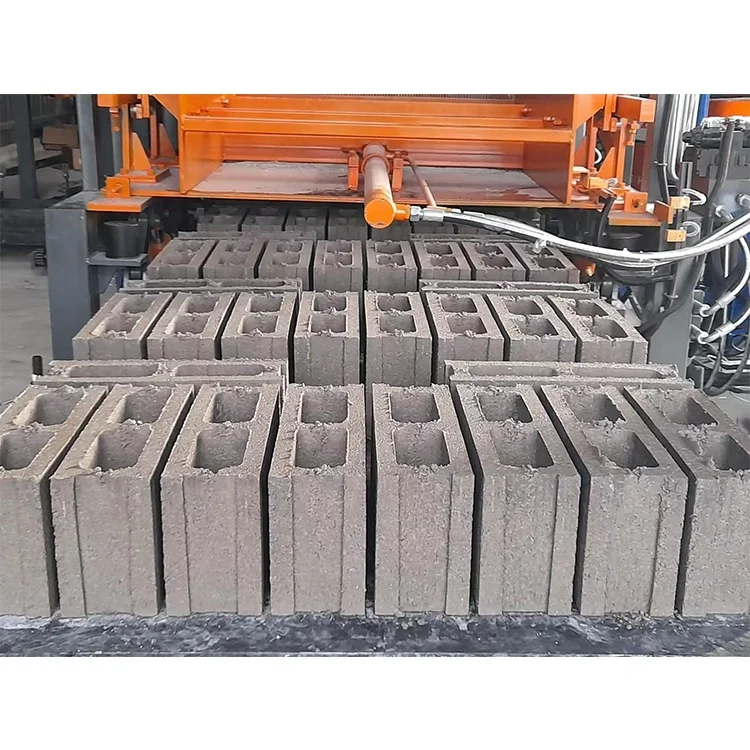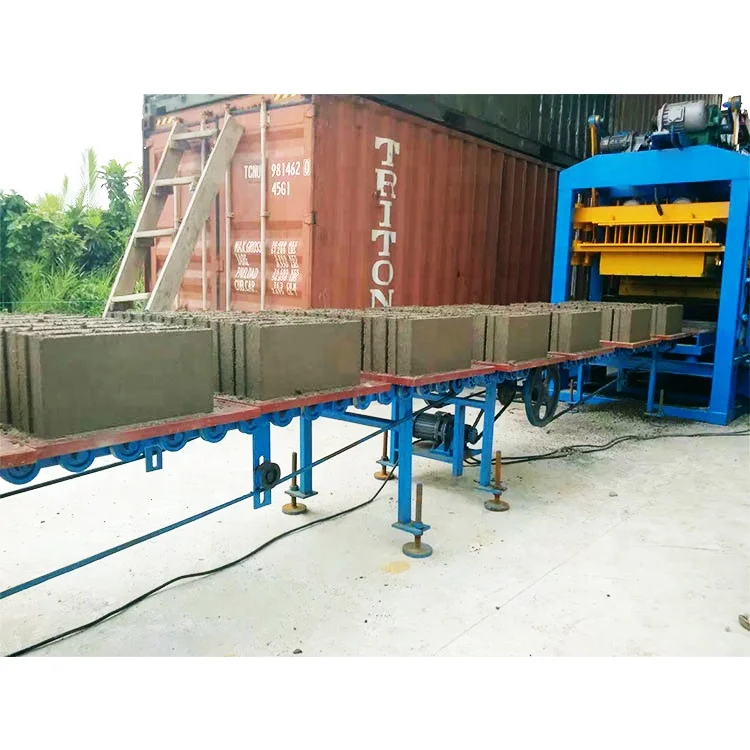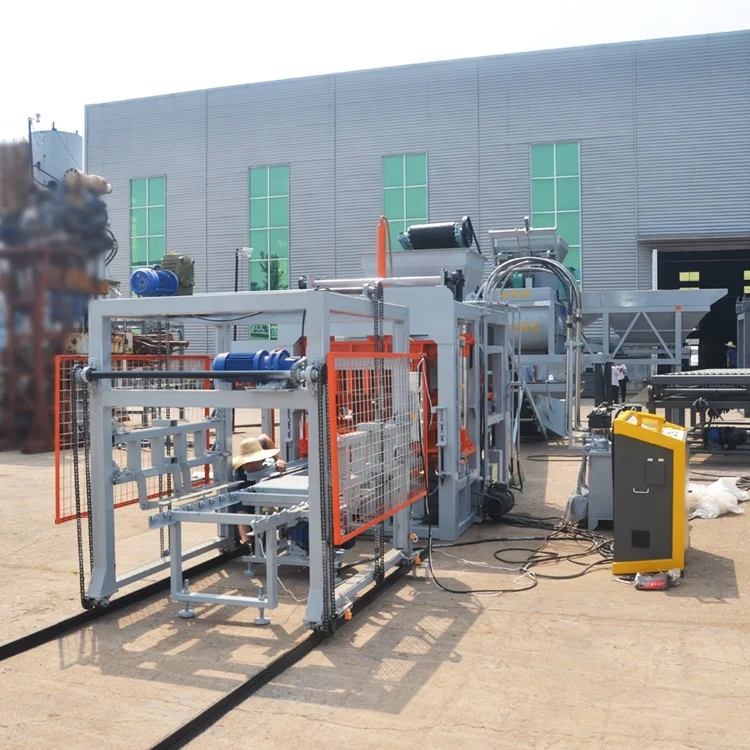
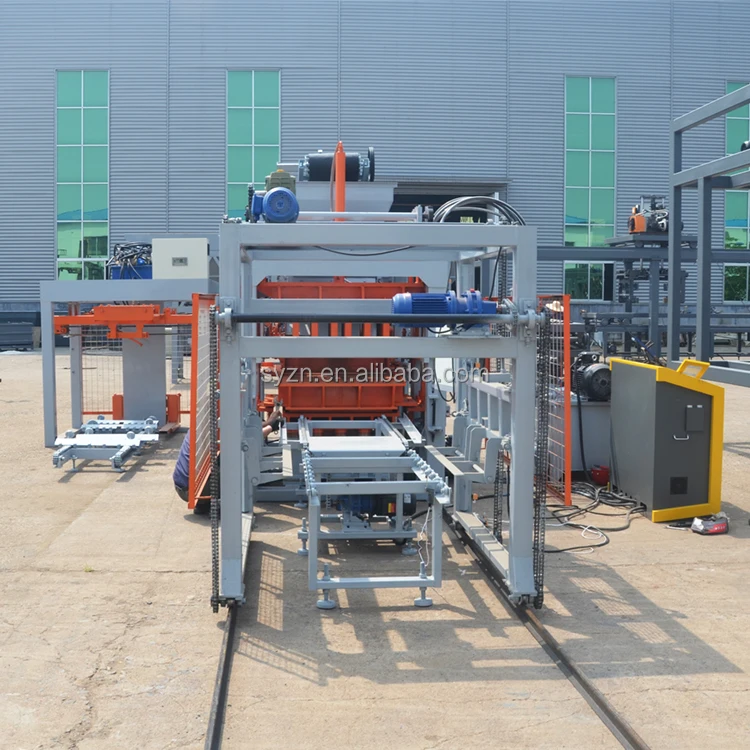


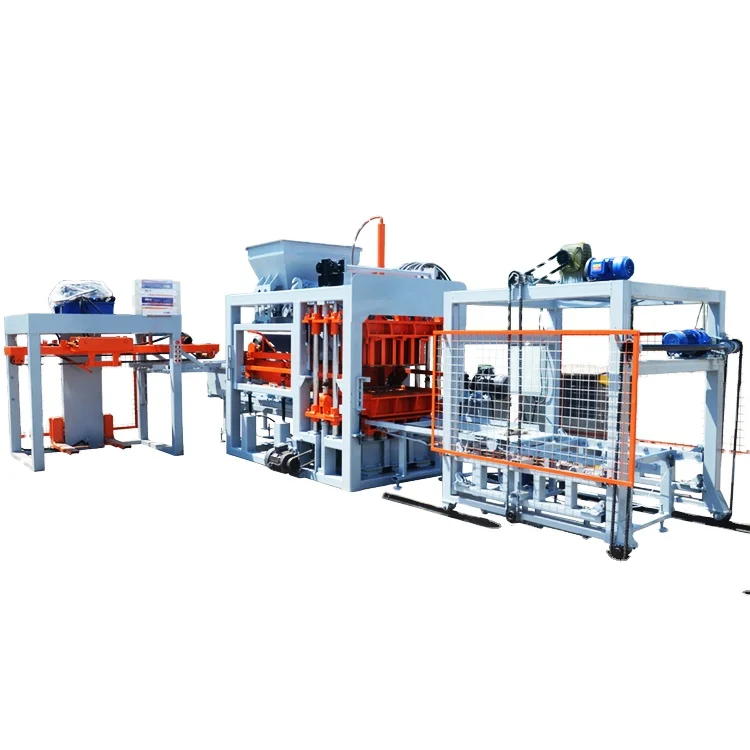

Description
Format-Matched Capacity — Every QT6-15 output figure is tied to a specific block size and cycle time, so your daily production plan matches what the machine actually delivers on your shop floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Hydraulic Block Making Machine |
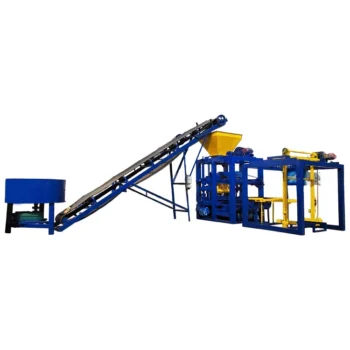
| Overall Dimensions | 8200 × 1700 × 2950 mm |
| Total Mass | 7 T |
| Overall Power | 37 kW |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 0–60 Hz |
| Vibration Force | 45 kN |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Molding Cycle | 15–20 s (hollow block); 20–25 s (paver) |
| Pallet Size | 880 × 850 mm |
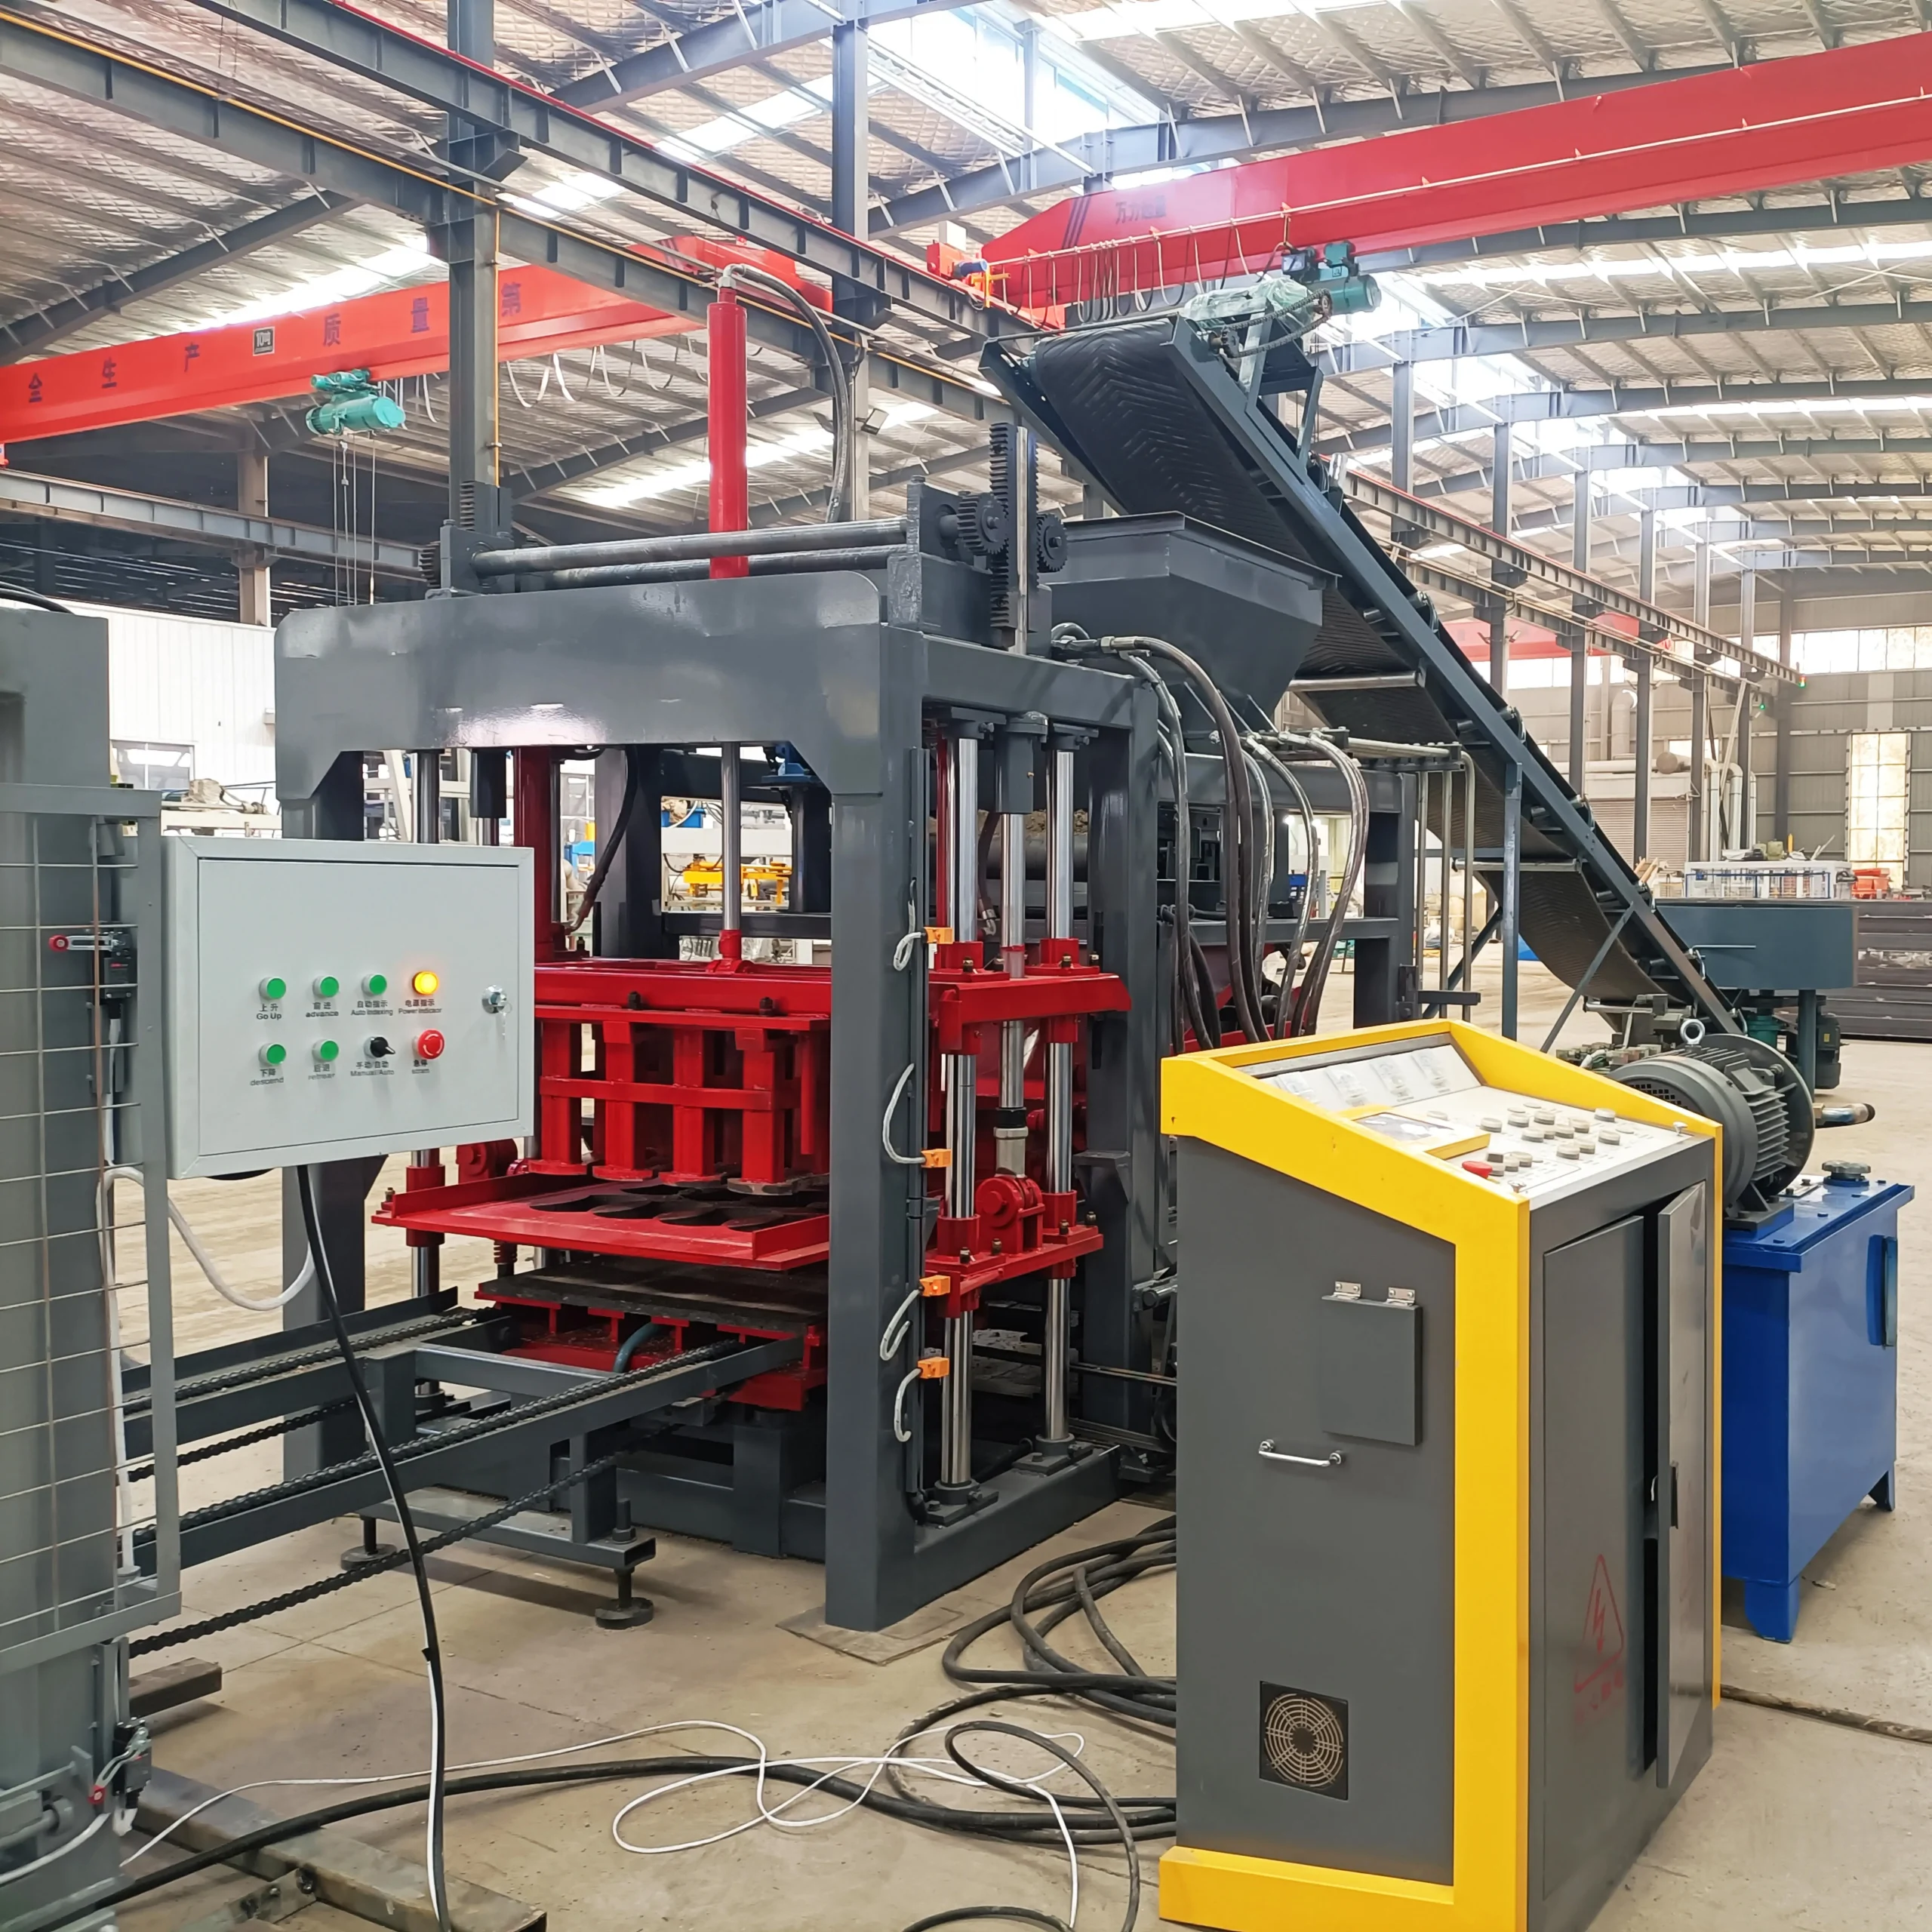
| Control System | PLC with touch screen interface |
| Fault Diagnosis | Built-in fault diagnosis with safe logic interlock circuit |
| Hydraulic System | Independent integrated station, isolated from dust and vibration |
| Block Compressive Strength | > 15 MPa |
| Output — Hollow Block 400×200×200 mm | 1080–1440 pcs/hour, 8640–11520 pcs/8 hr |
| Output — Hollow Block 400×150×200 mm | 1440–1920 pcs/hour, 11520–15360 pcs/8 hr |
| Output — Solid Brick 240×115×53 mm | 5760–7680 pcs/hour, 46080–61440 pcs/8 hr |
| Output — Rectangular Paver 200×100×60 mm | 2160–2880 pcs/hour (20–25 s cycle), 17280–23040 pcs/8 hr |
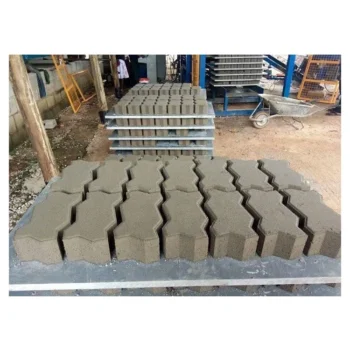
| Output — Zigzag Paver 225×112.5×60 mm | 2160–2880 pcs/hour (20–25 s cycle), 17280–23040 pcs/8 hr |
| Raw Material Compatibility | Waste ash, slag, and various aggregates |
| Factory Area Required | 1200 m² |
| Assembly State | Factory assembled, requires on-site installation |
| Certification | CE (where applicable) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, river sand, cement, and ash blends for 400×200×200 mm and 400×150×200 mm formats |
| Solid brick manufacturing | Fine aggregate and cement mixes for standard 240×115×53 mm bricks |
| Rectangular paving brick | High-density aggregate and cement for 200×100×60 mm interlocking pavers |
| Zigzag paving brick | Graded aggregate with cement for 225×112.5×60 mm zigzag format |
| Multi-cellular block production | Lightweight aggregate blends for partition and insulation blocks |
| On-site construction block making | Contractor-grade mixes for housing and development projects |
| Building material plant expansion | Existing producers adding hollow block or paver formats to current range |
What "8640 Blocks per Shift" Really Means for Your Plant
The QT6-15 block machine specifications only hold when the block format, cycle time, and raw material match what was tested — shift everything by one variable and the number changes.
A buyer once told me their previous machine was rated at over 1000 pieces per hour, but after arrival it never passed 500. The catalogue figure assumed a 400×200×200 mm hollow block on a clean-graded aggregate. His local river sand carried high clay content, which slowed the mix flow and extended every cycle. When we look at the hydraulic block making machine capacity by format, the 8640–11520 pieces per 8-hour shift applies specifically to the 400×200×200 mm hollow block at a 15–20 second cycle. Switch to a rectangular paver at a 20–25 second cycle and the shift output sits in a different range entirely. Quoting one number for all formats is how expectations break down on the first production day [NEED_CITE: common causes of block machine output shortfalls in field conditions].
Matching Block Format to Mould and Cycle Time
Every output number on the QT6-15 block machine specifications sheet is tied to a defined block size and its corresponding mould. The hollow block 400×200×200 mm runs at six pieces per mould within a 15–20 second cycle, while the solid brick 240×115×53 mm fits thirty-two pieces per mould in a similar window. Rectangular and zigzag pavers shift to a 20–25 second cycle because the denser aggregate mix and higher vibration requirement extend the pressing phase. Buyers who plan a product mix across two or three formats need to weight each cycle time by its share of the shift to arrive at a realistic daily total.
Vibration Force and Hydraulic Pressure as a Paired System
Platform vibration at 0–60 Hz delivers up to 45 kN of force across the 880×850 mm pallet, while the independent hydraulic station handles demolding through a separate circuit. This separation matters because dust and press vibration are the two main causes of hydraulic seal wear in block production. When the hydraulic station sits isolated from the vibration table, seal life extends and pressure stays consistent from the first block to the last [NEED_CITE: hydraulic system isolation practices in concrete block machinery]. Compressive strength above 15 MPa depends on both vibration energy compacting the mix and hydraulic pressure holding the mould steady during the cycle — neither parameter works alone.
How Pallet Size, Power, and Footprint Connect to Your Site
The 880×850 mm pallet is the physical link between the press, the curing area, and the forklift that moves finished blocks. If your curing racks were built for a different pallet dimension, every pallet must be transferred by hand before stacking. The 37 kW overall power draw requires a dedicated circuit with stable voltage and frequency; undersized supply lines cause the PLC to register faults mid-cycle. A 1200 m² factory area covers the press, mixer, pallet return, and curing rack space — confirming your site dimensions against this footprint prevents layout conflicts during installation.
The Hidden Cost of Skipping the Mix-Design Conversation
When a machine is configured for a clean-graded aggregate that the buyer cannot source locally, the first week of production reveals weak blocks, extended cycles, and jammed moulds. The vibration force and hydraulic pressure were set for a different material entirely. Correcting this after delivery means either changing the raw material supply at higher cost or requesting new machine parameters — both paths waste weeks of production [NEED_CITE: impact of aggregate gradation on concrete block compressive strength]. Confirming your local sand, stone, and cement proportions before the QT6-15 leaves the factory is the single step that prevents this mismatch.
Why Sourcing Through a Block-Machinery Specialist Matters
Shandong Shiyue Intelligent Machinery focuses exclusively on block machines, moulds, pallets, and handling equipment, which means the press, pallet, and curing system are specified as one matched set rather than assembled from separate suppliers. The QT6-15 block machine specifications are confirmed against your target block format, local aggregate, and site voltage before production begins. Mould designs are available for the formats your market sells, including custom drawings when standard options do not cover your requirement. The automation level is selectable, so a plant can start with semi-automatic pallet handling and add automatic stacking later. Installation support includes on-site commissioning and operator training so the first production shift runs under supervision.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format assumed for each QT6-15 output figure
- Mould drawing and format list confirming every block size included in your quotation
- Pallet specification cross-referenced with your curing rack dimensions and forklift capacity
- Voltage, frequency, and PLC display language confirmation document signed before production
- Factory test record on your specified block format before machine dispatch
- Operation and maintenance manual with hydraulic and electrical schematics
Installation, Commissioning & Support
- Foundation pad sized for the 8200 × 1700 mm machine footprint and 7 T operating weight
- Dedicated 37 kW power circuit with confirmed voltage and frequency matching the PLC and hydraulic station
- Machine arrives factory assembled and requires on-site positioning, pallet conveyor alignment, and utility connection
- PLC touch screen commissioned with your selected display language and block-cycle parameters loaded
- Operator training covers mould change procedure, fault diagnosis navigation, and daily vibration table inspection
- Wear parts list identifies hydraulic seals, vibration springs, and mould liners with reorder intervals
What to Include in Your Inquiry
To size the QT6-15 accurately, share the block formats your market sells along with the daily output target for each format. Confirm the local raw materials available — sand type, stone grading, cement brand — and the voltage and frequency standard at your site. If you already operate curing racks and forklifts, provide the pallet dimensions currently in use so the 880×850 mm pallet can be verified or adjusted before production begins.
Frequently Asked Questions
Q: How is QT6-15 capacity calculated per block format, and why does cycle time differ between hollow blocks and pavers?
A: Each capacity figure on the QT6-15 block machine specifications is tied to a specific block size. Hollow blocks at 400×200×200 mm run a 15–20 second cycle because the larger voids require less compaction time. Pavers at 200×100×60 mm need a 20–25 second cycle to reach the higher density required for traffic-bearing surfaces. Multiply the per-cycle output by achievable cycles in your shift length for a realistic daily figure.
Q: How do you match vibration force and hydraulic pressure to our local aggregate and mix design?
A: Before production, we review your local sand, stone, and cement proportions. The 45 kN vibration force and hydraulic demolding pressure are then set to match the gradation and moisture range of your mix. This step prevents the common problem where blocks leave the mould too soft or too brittle because the machine was calibrated for a different aggregate.
Q: What is the realistic mould change time, and how many formats can one machine run in a single shift?
A: Mould change time depends on the changeover system selected in your configuration. For plants running two formats per shift, the hydraulic block making machine capacity by format must account for the downtime between runs. We confirm the changeover procedure and realistic time during commissioning so your production schedule reflects actual conditions, not best-case assumptions.
Q: How is pallet size selected relative to our curing area and existing forklift equipment?
A: The 880×850 mm pallet must fit your curing rack spacing and match the fork dimensions of your existing handling equipment. If your racks were built for a different size, we discuss pallet options before the machine is built. Confirming this detail upfront avoids costly manual transfer of blocks between pallets during daily production.
Q: What voltage, frequency, and PLC language options are confirmed before shipment?
A: Voltage and frequency are confirmed to match your site electrical supply before the QT6-15 enters production. The PLC touch screen display language is selected at the same stage. A written confirmation document covers both items, preventing the common delay where a machine arrives on site but cannot be commissioned until electrical or language issues are resolved [NEED_CITE: voltage and frequency standards by export market].