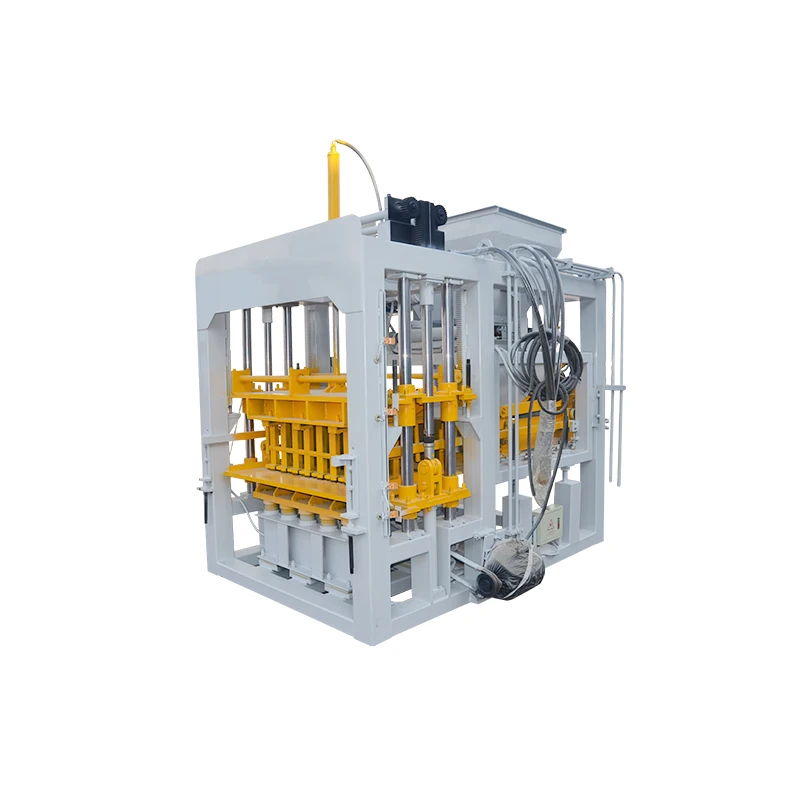
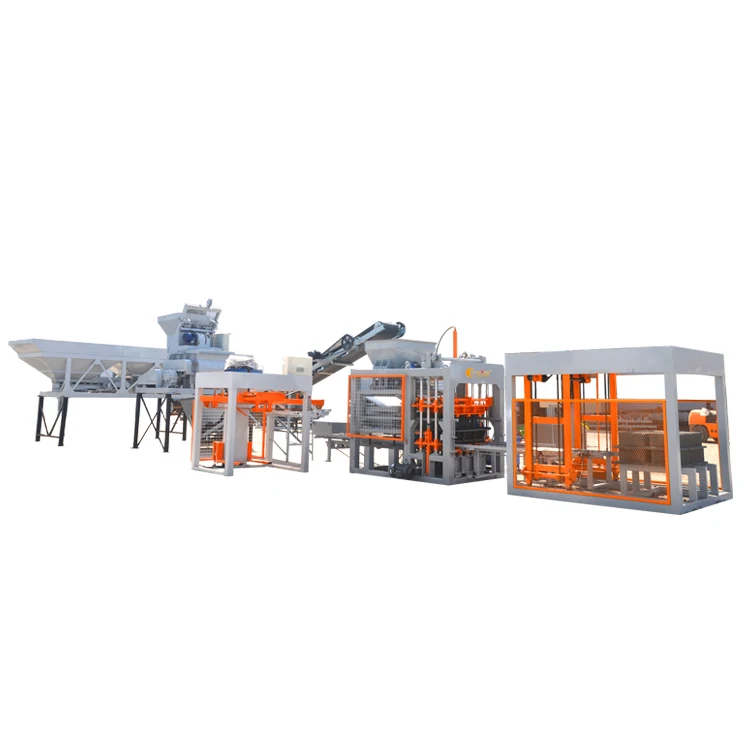
Description
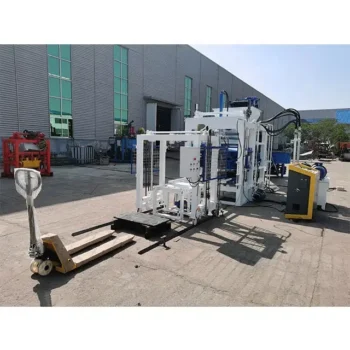
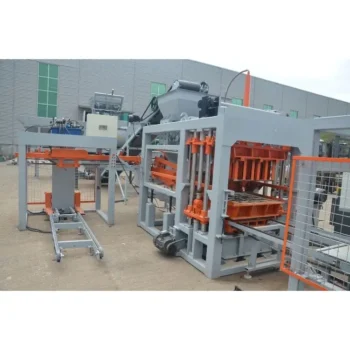
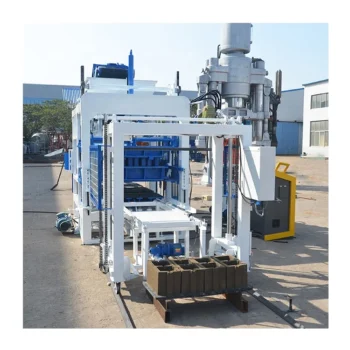
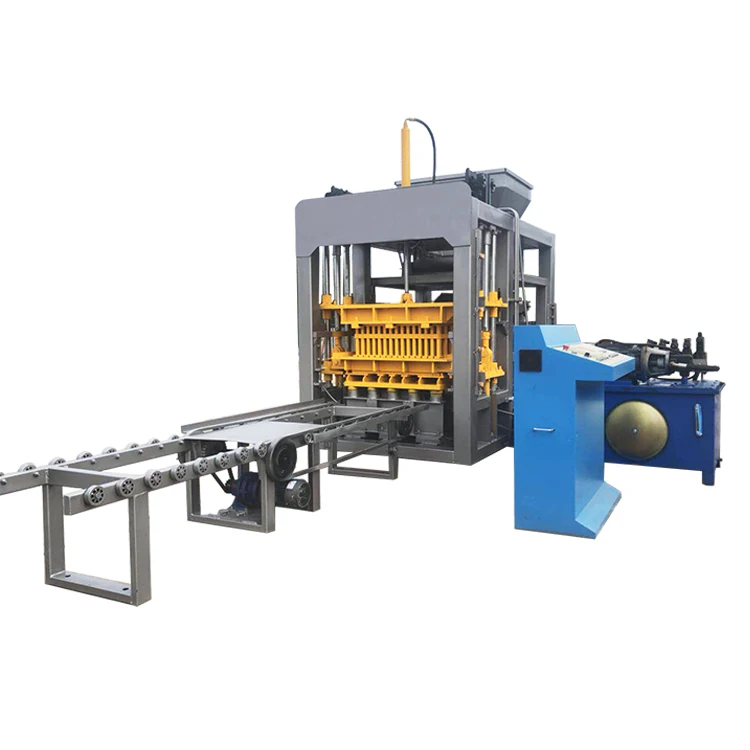
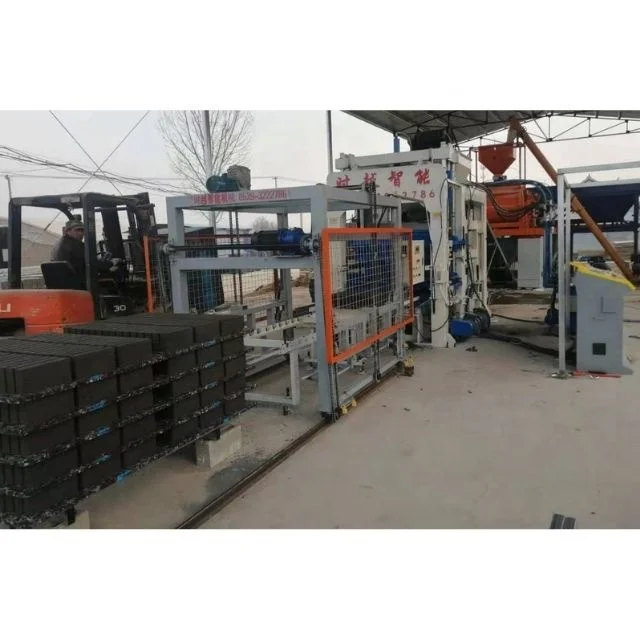
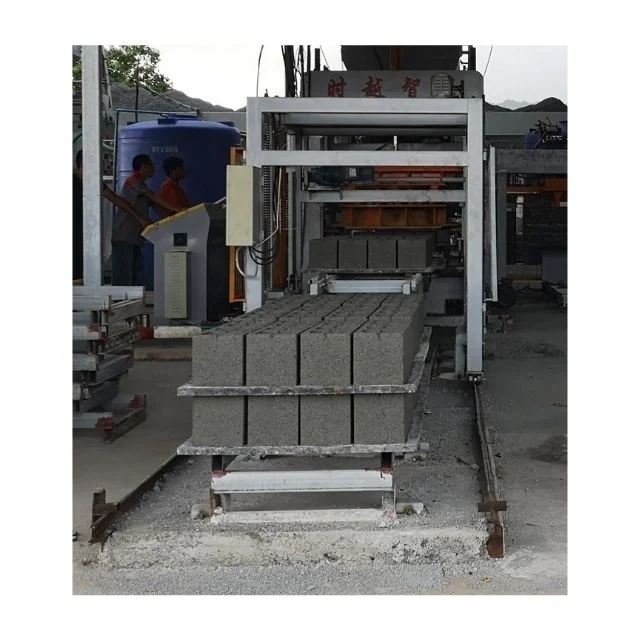
Format-Specific Capacity Matching — every output figure for the QT5-15 hydraulic block machine is tied to a named block format, mould cavity count, and verified cycle range, not a single catalogue headline.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400×1950×2800 mm |
| Total Mass | 5000 kg |
| Overall Power | 32 kW |
| Vibration Force | 80 kN |
| Vibration Frequency | 0–60 Hz |
| Vibration Form | Platform Vibration |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Pallet Size | 1100×550 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format, material, and thickness before ordering) |
| Control System | PLC with touch screen interface |
| Hydraulic System | Independent integrated hydraulic station |
| Recommended Factory Area | 1000 m² |
| Output — Hollow Block 400×200×200 mm | 900–1200 pcs/h (5 pcs/mould, 15–20 s cycle) |
| Output — Hollow Block 400×150×200 mm | 1080–1440 pcs/h (6 pcs/mould, 15–20 s cycle) |
| Output — Solid Brick 240×115×53 mm | 5760–7680 pcs/h (32 pcs/mould, 15–20 s cycle) |
| Output — Rectangular Paver 200×100×60 mm | 3600–4500 pcs/h (25 pcs/mould, 20–25 s cycle) |
| Output — Zigzag Paver 225×112.5×60 mm | 2304–2880 pcs/h (16 pcs/mould, 20–25 s cycle) |
| Block Compressive Strength | >15 MPa (verify against final mix design) |
| Raw Material Compatibility | Fly ash (up to 70%), slag, gangue, sand, crushed stone, cement, water |
| Mould Change | Simple replacement, multi-format capability |
| Automation Level | Automatic (pallet feeding, material feeding, vibrating, demoulding) |
| Warranty | 1 year for whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement; fly ash blends up to 70% content |
| Solid brick production for masonry | Sand, crushed stone, and cement with standard aggregate grading |
| Interlocking and rectangular paving block for roads and walkways | Fine aggregate, cement, and pigment for colour-face pavers |
| Zigzag (I-shaped) paver for heavy-duty pavement | High-strength mix with crushed stone base and cement binder |
| Industrial residue utilization | Fly ash, slag, and gangue incorporated at up to 70% content |
Why QT5-15 Hydraulic Block Machine Specifications Must Start with Block Format
Capacity means nothing until you name the product you intend to sell.
Too many quotations list a single hourly output figure and leave the buyer to assume it applies to whatever format they plan to run. On a job site in East Africa, I watched a machine rated at an impressive cycle count produce barely half that volume because the local red soil carried a clay content that the vibration force could not fully compact. The machine was not at fault — the configuration had never been matched to the material. The QT5-15 hydraulic block machine specifications in the table above tie every output number to a specific block format, cavity count, and cycle range so there is no guesswork at the production stage [NEED_CITE: common causes of block machine underperformance in tropical aggregate conditions].
Pallet Size, Curing Area, and the Forklift You Already Own
The QT5-15 runs on 1100×550 mm pallets, and that dimension dictates everything downstream. Your curing racks must accept that width, your forklift tines must span it, and your stacking pattern must account for the weight of a loaded pallet. Buyers who overlook this detail often discover after delivery that their existing curing infrastructure needs modification, adding unplanned cost before the first production run. Confirming pallet compatibility is one of the first steps in our sales process for this block format capacity tier.
Mould Options and What a Format Change Actually Takes
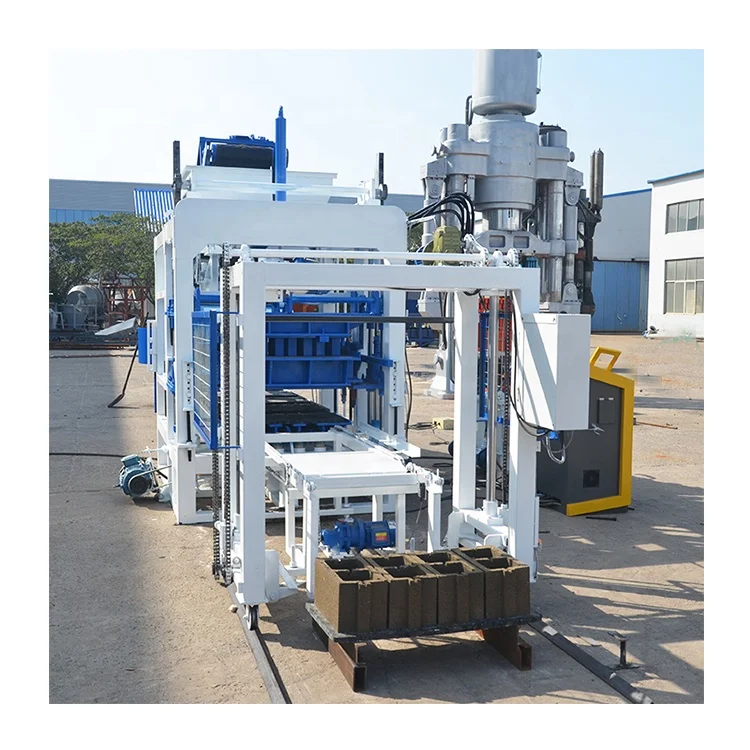
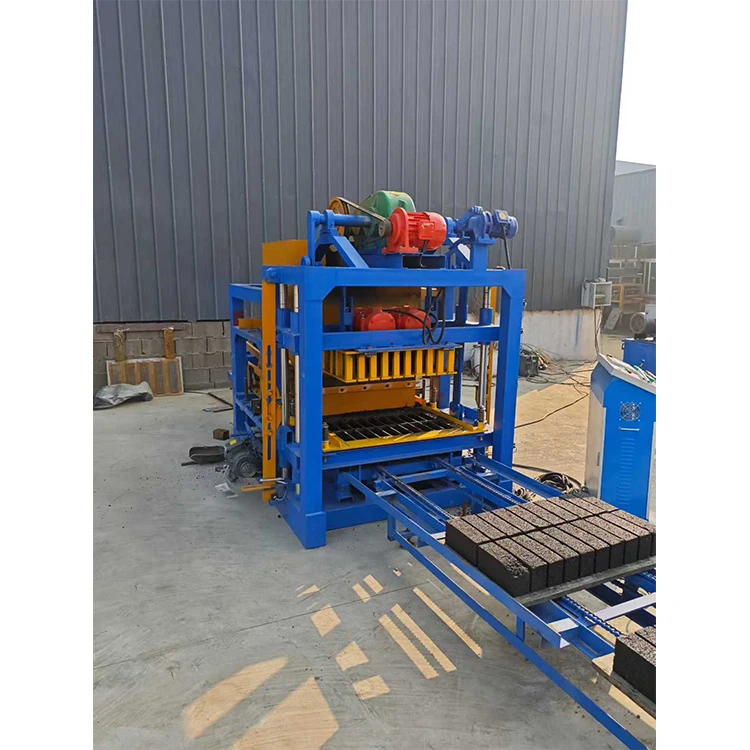
The mould system on the QT5-15 hydraulic block machine supports hollow blocks, solid bricks, rectangular pavers, and zigzag pavers through straightforward mould replacement. Each format listed in the specification table uses a dedicated mould with its own cavity count — five for the large hollow block, thirty-two for the solid brick, and so on. The real question is how long a changeover takes on your shop floor with your crew, because a machine advertised as multi-format only delivers flexibility if the swap happens within a practical window [NEED_CITE: typical mould changeover times on mid-tier hydraulic block machines].
Reading the Numbers That Actually Matter for Production
Vibration force at 80 kN combined with hydraulic demoulding determines how densely the mix is compacted inside the mould cavity. Higher compaction yields greater compressive strength, and the >15 MPa rating assumes a mix design and aggregate profile that must be validated with your local materials before the machine ships. The 32 kW overall power rating covers the full multi-station line including the hydraulic unit, PLC cabinet, conveyor, and pallet feed — not just the press itself. Platform vibration at a frequency range of 0–60 Hz allows the operator to tune the cycle to different mix consistencies, which matters when switching between a fly-ash-heavy blend and a standard crushed-stone mix. The 1000 m² recommended factory area accounts for raw material storage, the press line, and a minimum curing zone.
The Hidden Cost of Skipping the Material Trial
When a block machine is configured for a mix the buyer cannot source locally, the result is either a costly material substitution or a machine that runs below its designed capacity from day one. I have seen projects stall for weeks while the buyer searched for an alternative aggregate that matched the original specification. The vibration force and hydraulic pressure must be matched to the specific density and moisture response of the raw materials available at the site, not to a laboratory ideal [NEED_CITE: impact of local aggregate variability on block compressive strength].
Why Sourcing the QT5-15 Through a Format-Focused Process Works
Block machinery is our single focus, so the QT5-15 is specified as a matched system of press, mould, pallet, and handling equipment rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design, local aggregate, and target block format — not a catalogue default. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard cavities do not match. Automation level is selectable, meaning a buyer can begin with the standard automatic cycle and plan an upgrade path later. Installation support includes on-site commissioning and operator training tied to the specific formats the plant will produce.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Mould drawing and format list confirming cavity count and dimensions for every product in the quotation
- Pallet specification sheet — size, material, and weight — cross-checked against buyer’s curing racks
- Voltage, frequency, and PLC display language confirmed in writing before production begins
- Factory test record on buyer’s specified block format and mix before dispatch
Installation, Commissioning & Support
- Foundation must support 5000 kg total mass across the 7400 mm line length with level tolerance for platform vibration accuracy
- Dedicated 32 kW power circuit required, with voltage and frequency confirmed to local grid before wiring begins
- Multi-station line arrives in dismantled form and requires reassembly of hydraulic unit, PLC cabinet, conveyor, and pallet feed
- First production run validates molding cycle against buyer’s actual mix and target compressive strength
- Operator training covers PLC touch screen navigation, mould change procedure, and daily hydraulic station checks
- Wear parts and mould list provided at handover with recommended reorder intervals for vibration components
What to Prepare Before Requesting a Quotation
Send your target block format with dimensions, the daily volume your market requires, and the raw materials you can source locally — including any fly ash or slag you intend to use and their typical proportions. Confirm your local voltage, frequency, and the language you need on the PLC display. If you have existing curing racks or forklifts, share their specifications so the 1100×550 mm pallet can be cross-checked before the order is placed.
Frequently Asked Questions
Q: How is the output capacity verified, and which block format does each figure assume?
A: Every capacity figure in the specification table is tied to a named block format, a specific mould cavity count, and a cycle time range. For example, the hollow block 400×200×200 mm output is calculated on a 5-cavity mould running a 15–20 second cycle. We provide a written capacity calculation document with your quotation that states the exact format and assumptions used.
Q: What mould formats are available, and how long does a change take?
A: The QT5-15 supports hollow blocks, solid bricks, rectangular pavers, and zigzag pavers through dedicated moulds. Each format requires its own mould unit. Changeover involves removing the current mould and securing the replacement on the vibration platform. We recommend discussing your planned format rotation during the quotation stage so we can include the right mould set and provide changeover guidance.
Q: How do I confirm the pallet size works with my existing curing area?
A: The QT5-15 uses 1100×550 mm pallets. Before ordering, measure your curing rack width and forklift tine spread to confirm compatibility. We provide a pallet specification sheet detailing dimensions, material, and loaded weight so you can verify fit against your existing infrastructure without surprises at commissioning.
Q: How is vibration force matched to my local aggregate and mix design?
A: The 80 kN vibration force and adjustable 0–60 Hz frequency must be tuned to the density, moisture content, and particle size of your raw materials. We request a sample or detailed description of your local aggregate and proposed mix proportions before finalizing machine settings. This trial step ensures the blocks meet compressive strength targets with the materials you can actually source.