Description
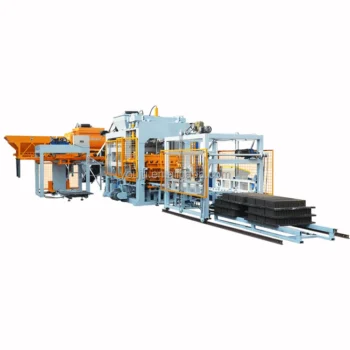
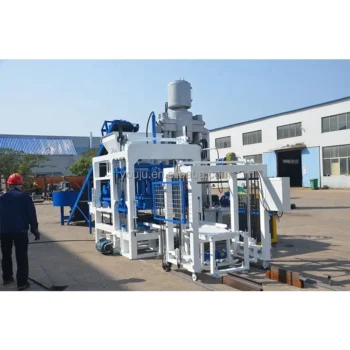
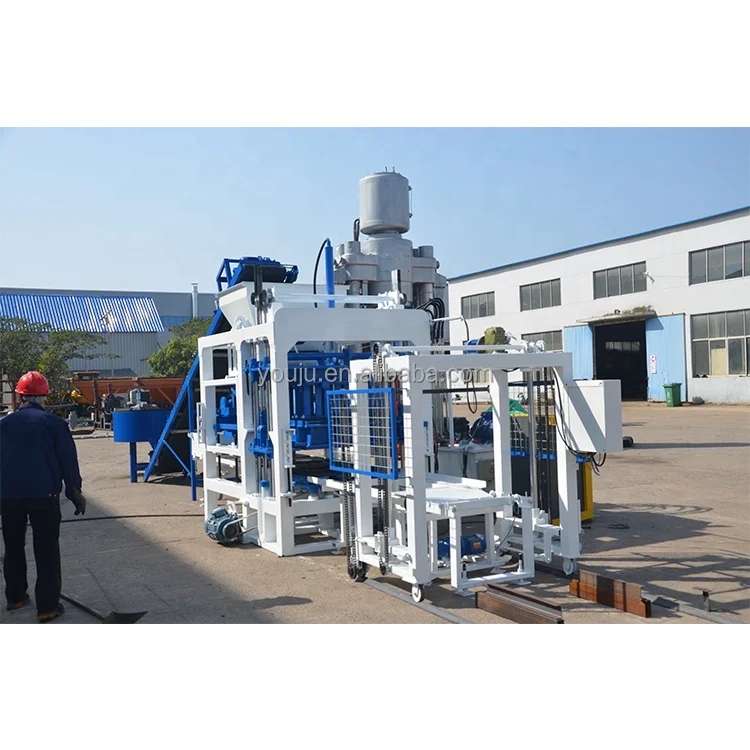
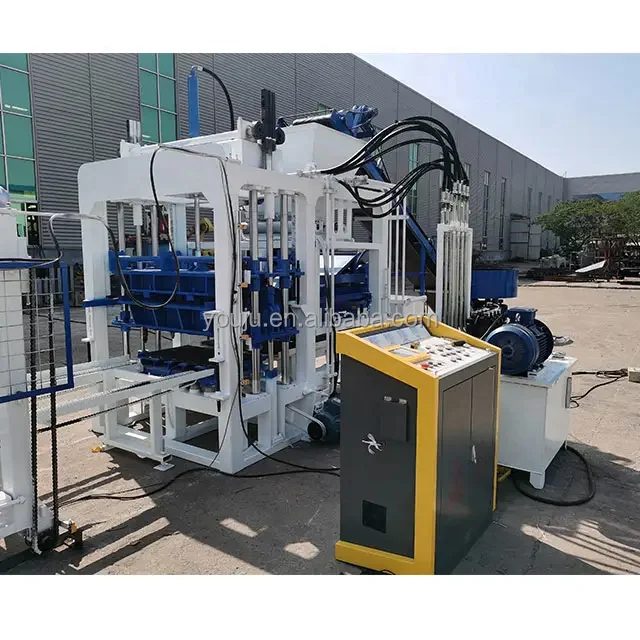
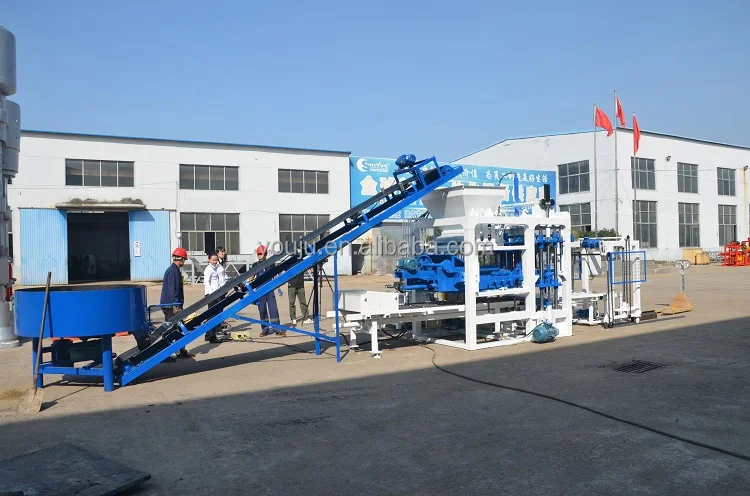
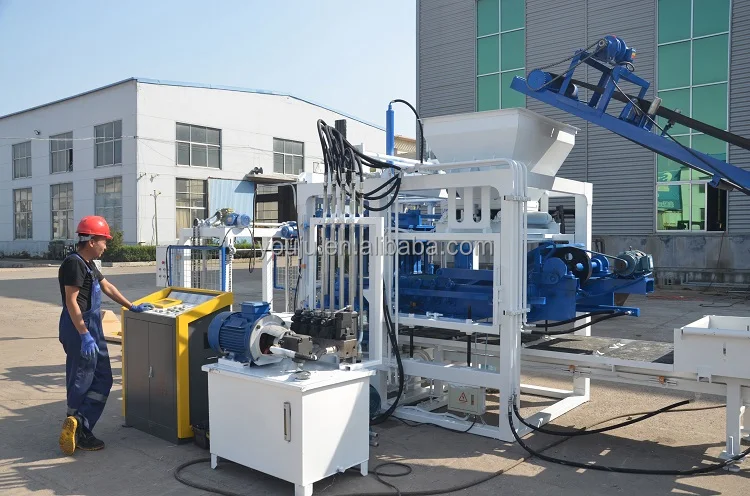
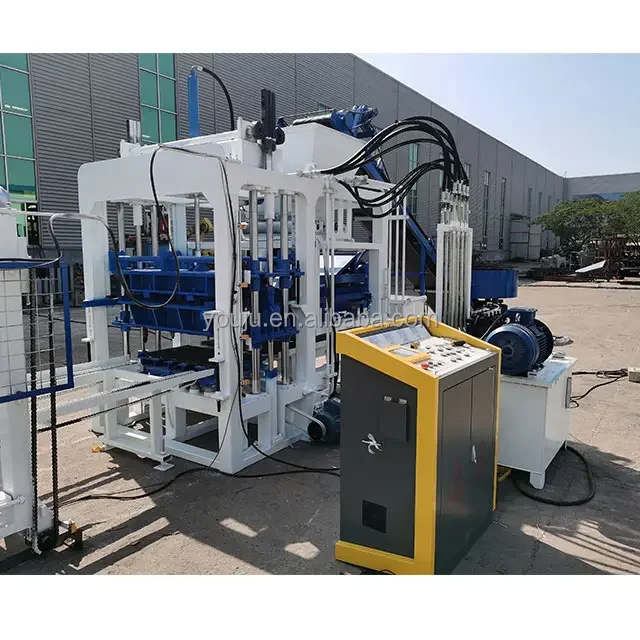
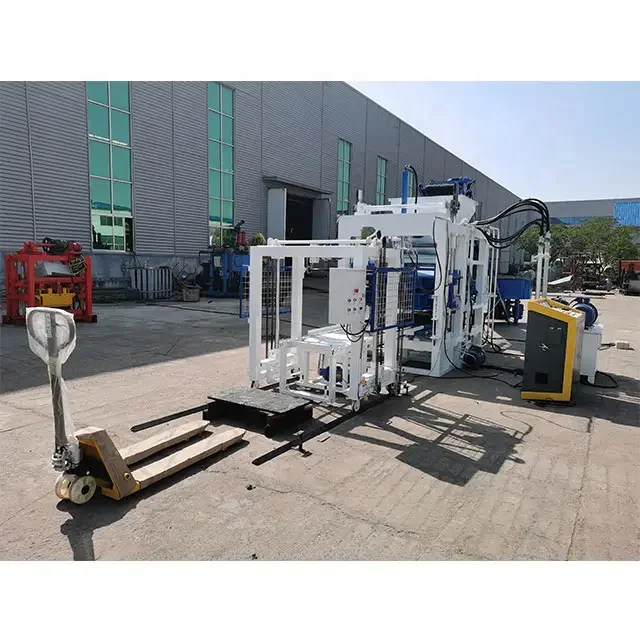
Matched System — machine, mould and pallet configured together against the buyer’s target block format, so the QT4-18 block machine specifications reflect actual production conditions rather than catalogue defaults.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions | 2500 × 1750 × 2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950 × 550 mm |
| Molding Cycle | 18–25 s (varies by block format) |
| Overall Power | 27.5 kW |
| Control System | PLC control with frequency converter |
| Electrical Components | Schneider brand |
| Mould Lifting Mechanism | Double-sided sync gears |
| Material Feeding System | Distribution belt hopper |
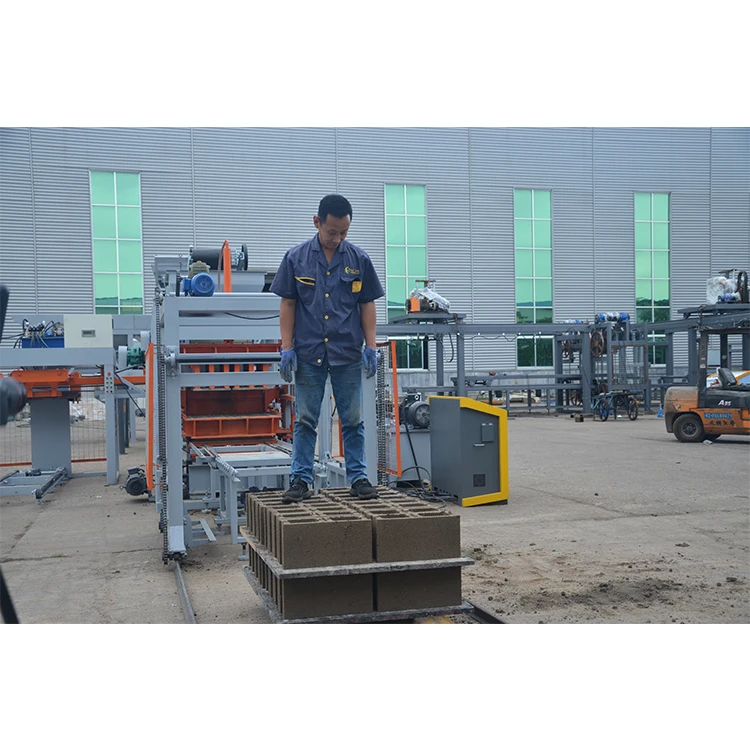
| Automation Level | One-person PLC operation |
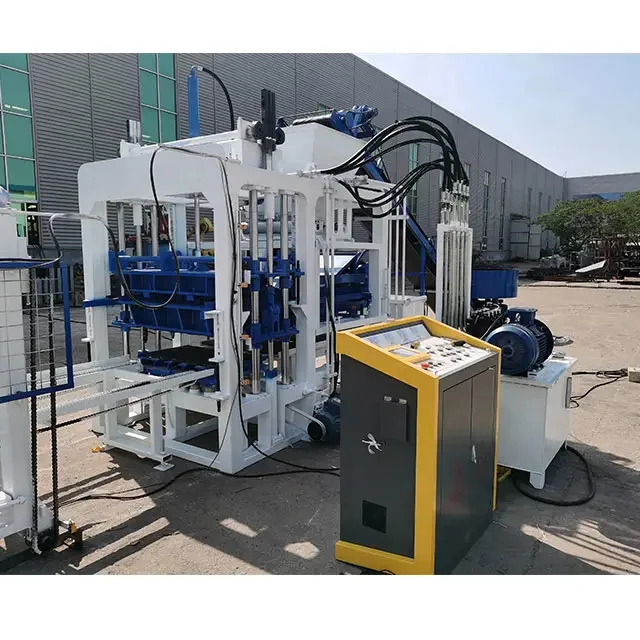
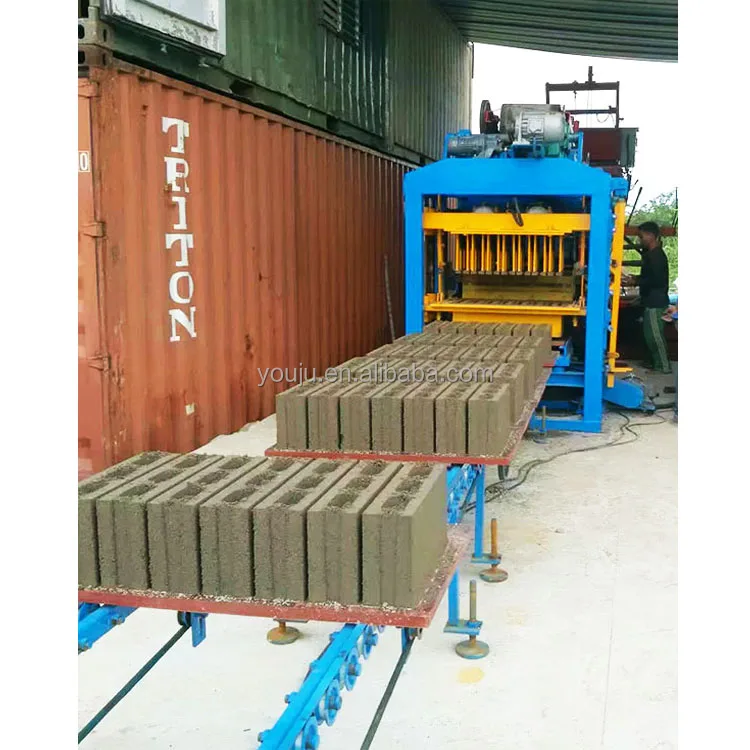
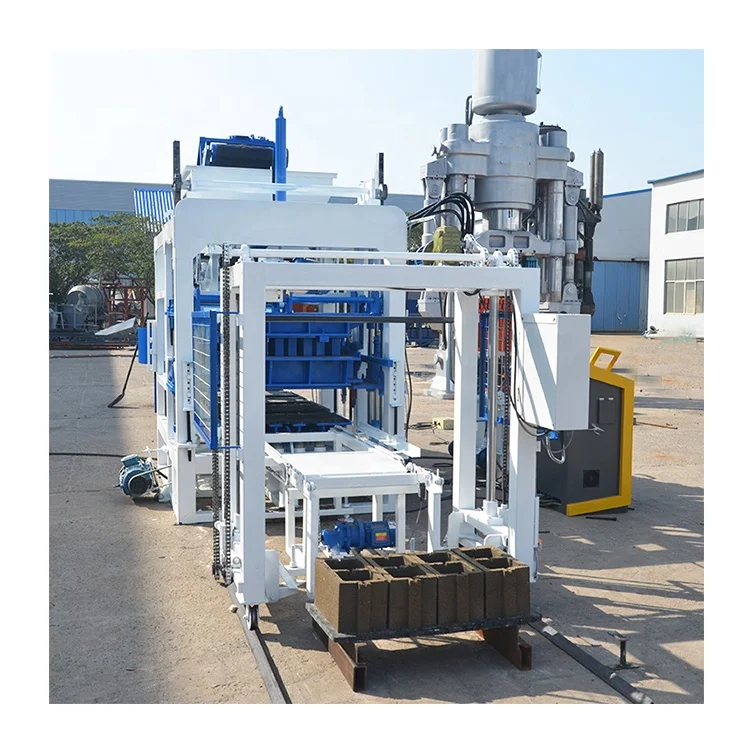
| Assembly State | Mixer, pallet conveyor, molding machine, block conveyor, hydraulic station, electronic console |
| Support Equipment Options | JQ500 concrete mixer, 8 m / 6 m belt conveyor, stacker, block gripper, trolley, concrete batching plant |
| Mould Configuration | One free hollow mould included; extra moulds customizable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial walls | Crushed stone, sand, cement, fly ash aggregates |
| Solid block manufacturing for load-bearing structures | Dense aggregate mixes with standard cement ratios |
| Paving block production for driveways and walkways | High-strength concrete with fine aggregate surface layer |
| Insulated brick production for thermal-efficient buildings | Lightweight aggregate blends such as expanded clay or pumice |
| On-site block production by construction contractors | Locally sourced sand and gravel with portable batching |
| Format expansion for existing concrete product plants | Multiple moulds on a single 950 × 550 mm pallet footprint |
What "One Molding Cycle" Actually Means for Your Daily Output
Cycle time only becomes meaningful when tied to the specific block format you intend to produce.
Manufacturers often quote a single molding cycle figure that sounds impressive until the machine arrives and the buyer discovers it applies to a small solid block, not the hollow block format the local market demands. With the QT4-18, the QT4-18 block machine specifications list a molding cycle of 18–25 seconds, but where your project falls within that range depends entirely on block geometry, wall thickness and the compaction time your aggregate requires [NEED_CITE: how aggregate grading affects vibration compaction time in block molding]. A lightweight volcanic aggregate needs longer vibration and different hydraulic dwell than standard crushed limestone, and the frequency converter in the PLC allows these parameters to be adjusted per mould rather than locked to a single factory preset.
Matching Pallet Size to Your Curing Layout and Handling Equipment
The 950 × 550 mm pallet determines every block format this machine can produce and must align with the curing racks, floor space and forklift dimensions already on site. A pallet that does not fit the buyer’s existing curing area forces a costly reconfiguration of the entire post-press workflow. Before confirming the QT4-18 block machine specifications, we verify that the pallet dimensions work with the buyer’s stacking method and transport equipment so that fresh blocks move from press to curing without manual rehandling.
Why Vibration Force and Hydraulic Pressure Must Be Read Together
Platform vibration alone does not guarantee block density — it works in combination with the 16 MPa rated hydraulic pressure to compact the mix from below and above simultaneously. The balance between these two forces determines whether the finished block meets the strength class the local building code requires. A mix that is too dry will resist compaction under platform vibration alone, while a mix with excessive moisture will collapse under full hydraulic pressure before the vibration cycle completes [NEED_CITE: relationship between vibration amplitude and hydraulic pressure in concrete block forming]. The PLC frequency converter allows the operator to tune vibration intensity per mould, giving the QT4-18 flexibility across different formats without mechanical adjustment.
Reading the QT4-18 Block Machine Specifications Against Your Actual Production Conditions
The 27.5 kW overall power rating covers the molding press, hydraulic station, distribution belt hopper and pallet conveyor running together, which means the electrical supply must support continuous draw at that level, not just peak startup current. The double-sided sync gear mould lifting mechanism keeps the mould box level during extraction, reducing edge damage on hollow blocks with thin shell walls. Schneider electrical components are specified throughout the control cabinet, which matters when replacement contactors or relays need sourcing in markets where industrial electrical supply chains are limited. The distribution belt hopper feeds material evenly across the mould cavity, a detail that becomes critical when producing pavers with a face-mix layer requiring uniform fill depth.
The Hidden Cost of Confirming Voltage After the Machine Ships
Voltage, frequency and PLC display language are details that sometimes get finalized after the order is placed, which delays commissioning by weeks when the machine arrives and the local electrician discovers the control cabinet was built for a different supply standard. The QT4-18 block machine specifications include PLC control with frequency converter, but the incoming power supply must still match the motor windings and hydraulic pump motor rating [NEED_CITE: industrial voltage and frequency standards by region for exported machinery]. Confirming these three items before production begins avoids a scenario where the machine sits idle on the factory floor waiting for a transformer or a replacement control board.
Why Configuration Matters More Than Catalogue Selection
Block machinery is our single focus, which means the press, mould, pallet and handling equipment are specified as one matched system rather than assembled from separate supplier quotations. Each QT4-18 configuration is set against the buyer’s actual mix design and local aggregate, not pulled from a default catalogue page. Mould design covers the formats the buyer’s market actually sells, with custom drawings available when standard moulds do not match local block dimensions. The automation level is selectable, so a buyer can begin with semi-automatic pallet handling and add a stacker or block gripper later as production volume grows. Installation support includes on-site commissioning and operator training so the crew understands PLC parameter adjustment before the first production shift begins.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Mould drawing and format list confirming which block sizes the 950 × 550 mm pallet can produce
- Voltage, frequency and PLC display language confirmation recorded before production starts
- Factory test record showing actual cycle time per requested block format
- Hydraulic and electrical schematic for local maintenance reference
Installation, Commissioning & Support
- Foundation must support 2500 × 1750 mm footprint with level tolerance for the platform vibration assembly
- Dedicated electrical circuit sized for 27.5 kW continuous draw with correct voltage and frequency confirmed pre-shipment
- Machine arrives as matched assembly: press, hydraulic station, pallet conveyor and electronic console bolted separately for container loading
- First-run commissioning includes PLC parameter tuning to match buyer’s specific aggregate and block format
- Operator training covers mould change procedure using the double-sided sync gear lifting mechanism
- Wear parts list and mould maintenance schedule provided for planning first replacement orders
What We Need to Prepare an Accurate Configuration
To size the QT4-18 correctly for your production targets, share the specific block formats you intend to sell, including dimensions and wall thickness for hollow blocks. Provide a sample or description of your local aggregate — whether crushed limestone, volcanic pumice, river sand or industrial by-product — along with your intended cement ratio. Confirm your site voltage, frequency and the language you need on the PLC display so the control cabinet is built correctly from the start.
Frequently Asked Questions
Q: What is the realistic daily output of the QT4-18 for my specific block format?
A: Daily output depends on the block format, wall thickness and aggregate type you use. The molding cycle of 18–25 seconds varies by format, and we calculate realistic output per block size in the capacity proposal. This ensures the figure you plan against matches what the machine actually produces on your mix, not a catalogue number based on a small solid block.
Q: How does the 950 × 550 mm pallet size affect which block formats I can produce?
A: The pallet size sets the maximum mould cavity area, which determines how many blocks fit per cycle and what dimensions are possible. We provide a mould drawing and format list showing every block size the pallet can accommodate. The pallet must also match your existing curing racks and forklift to avoid rehandling after the press.
Q: What is the mould change time and how many formats can one machine run per shift?
A: Mould change involves lifting the mould box with the double-sided sync gear mechanism, swapping the mould and resetting PLC parameters for the new format. The practical number of format changes per shift depends on production volume per format and operator experience. We specify the change procedure during commissioning so your crew can plan shift layouts realistically.
Q: How do I confirm the hydraulic pressure and vibration force match my local aggregate?
A: We request a sample or detailed description of your aggregate and mix design before finalizing the machine configuration. The 16 MPa rated pressure and platform vibration are adjustable through the PLC frequency converter. During the factory test, we run your actual block format and record cycle times so you can verify the match before the machine ships.