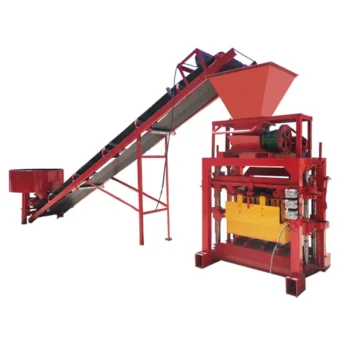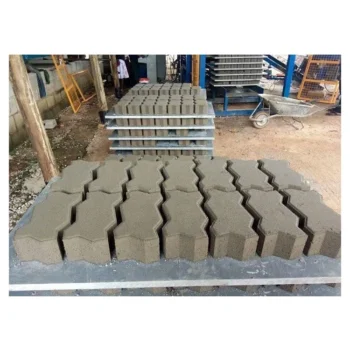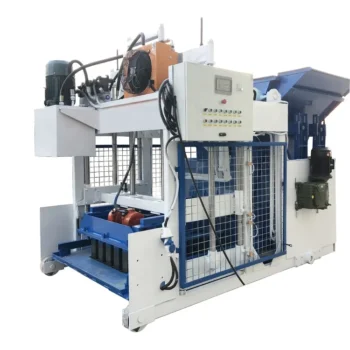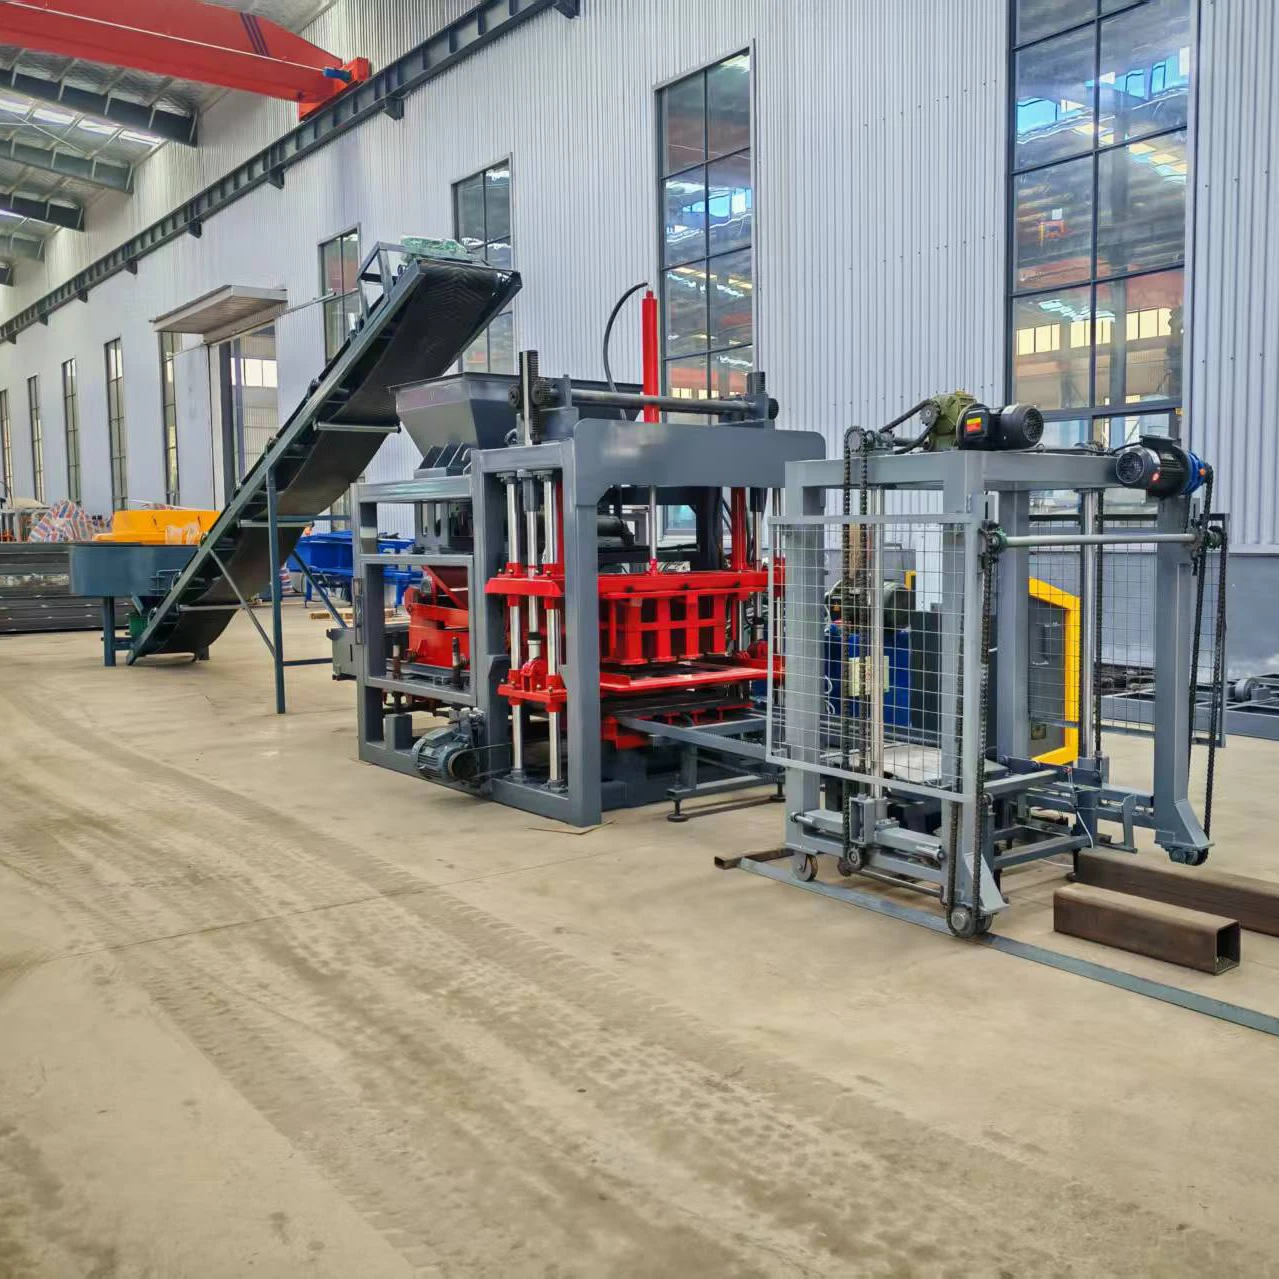
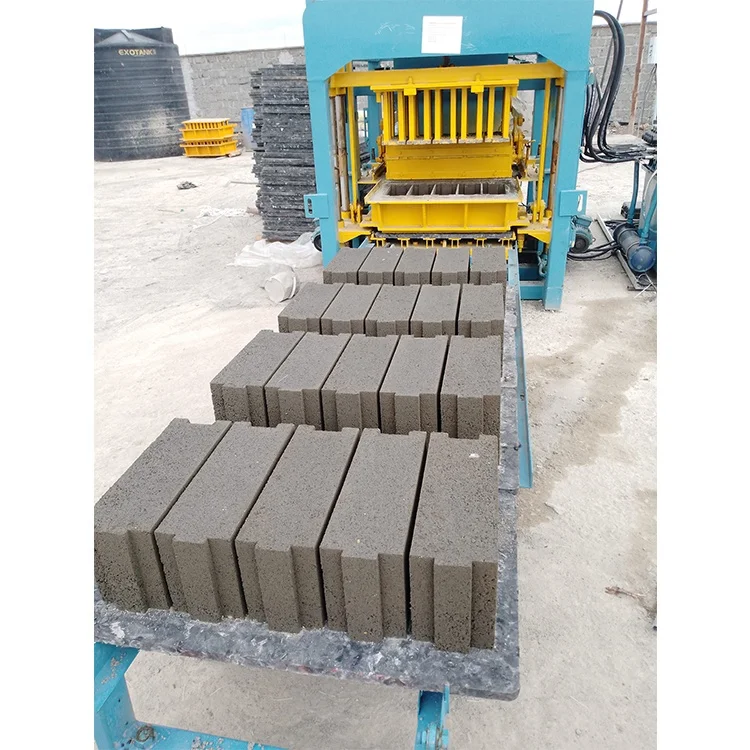
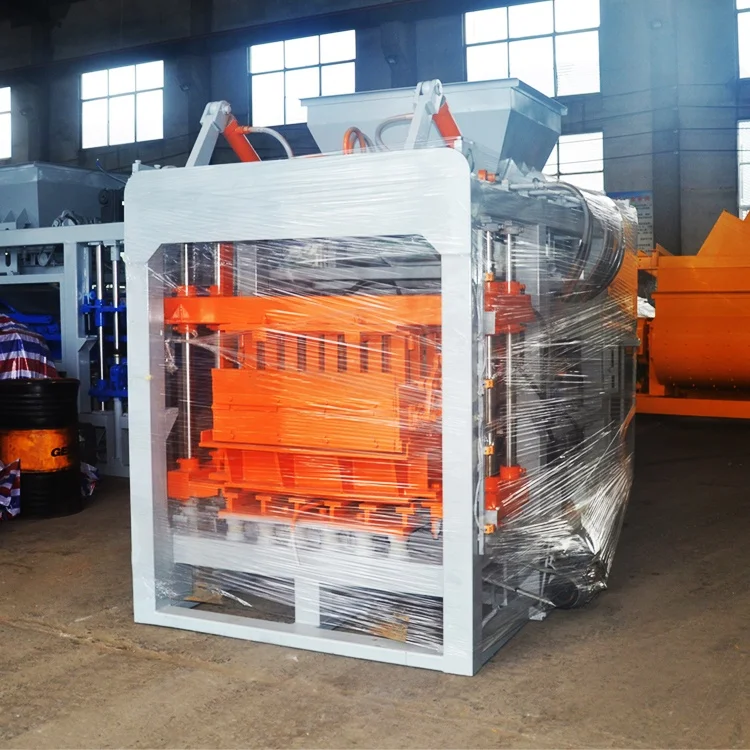
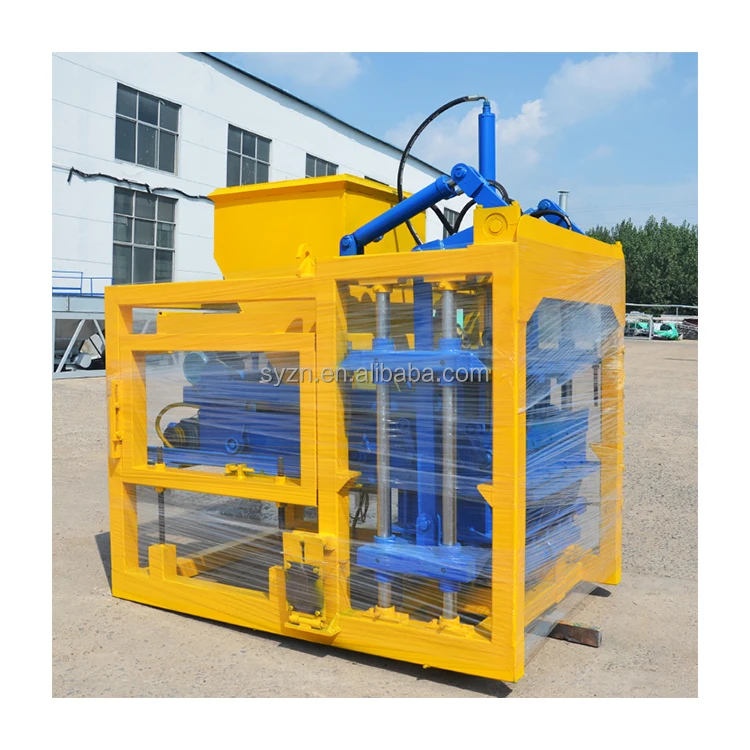
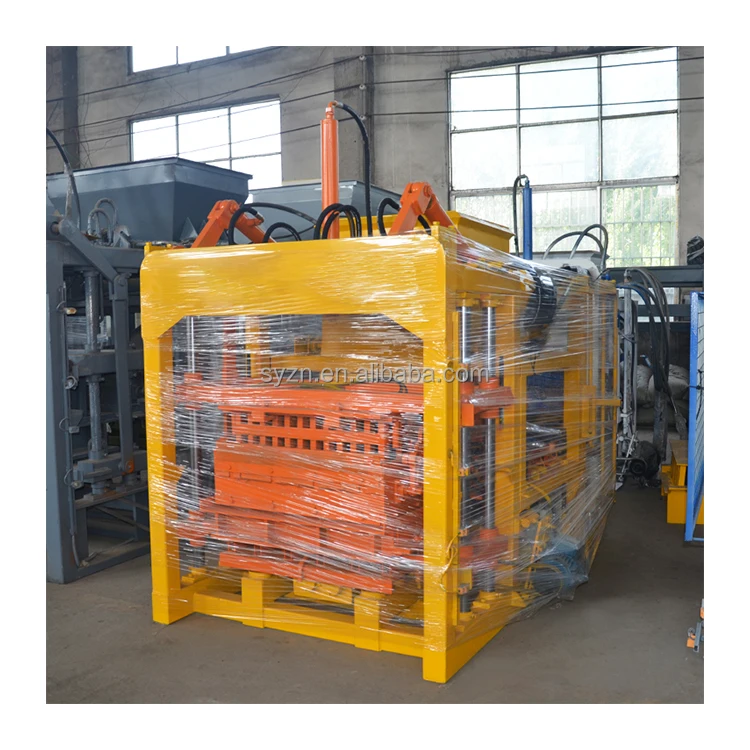

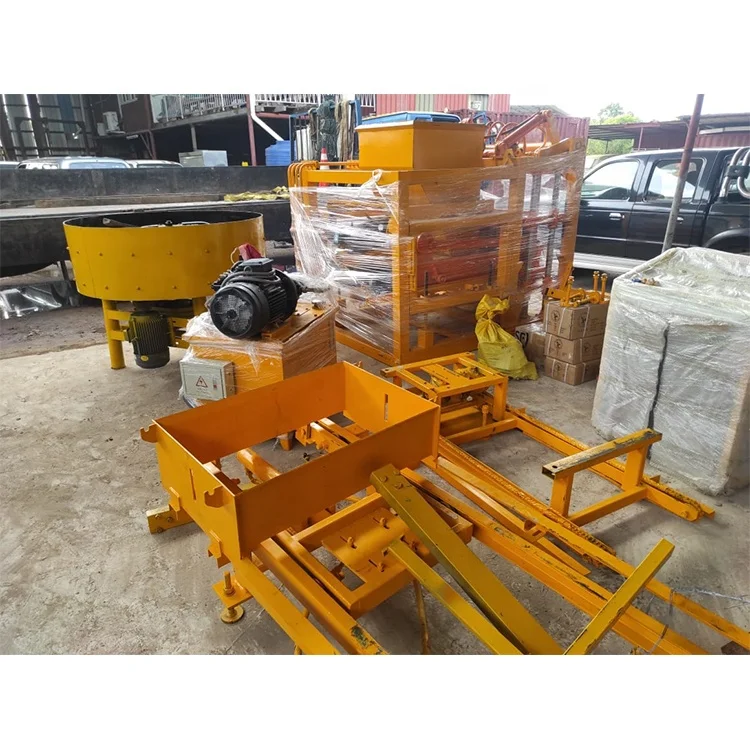
Description
Mould and format first — every output figure on this sheet assumes a specific block dimension, cavity count, and cycle time, because a machine is only as fast as its slowest format change.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Vibration Force (Exciting Power) | 40–50 kN |
| Total Power | 18.45 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Total Weight | 3 T |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Control System | PLC control system |
| Hydraulic Station | Included |
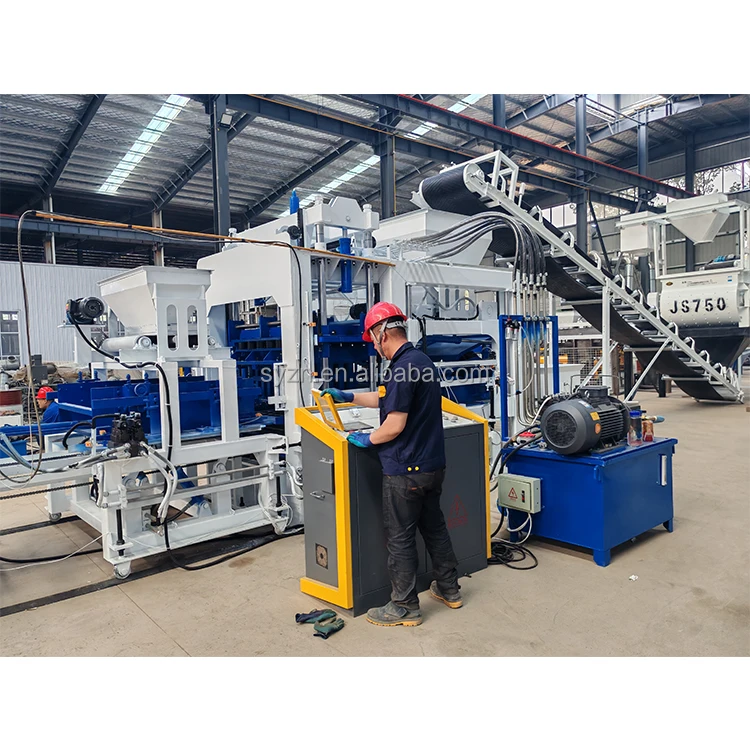
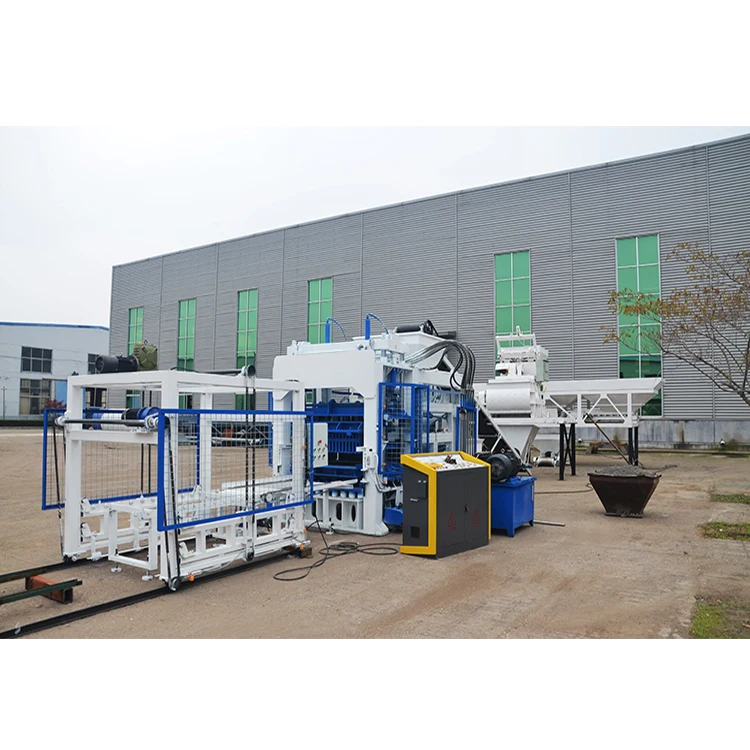
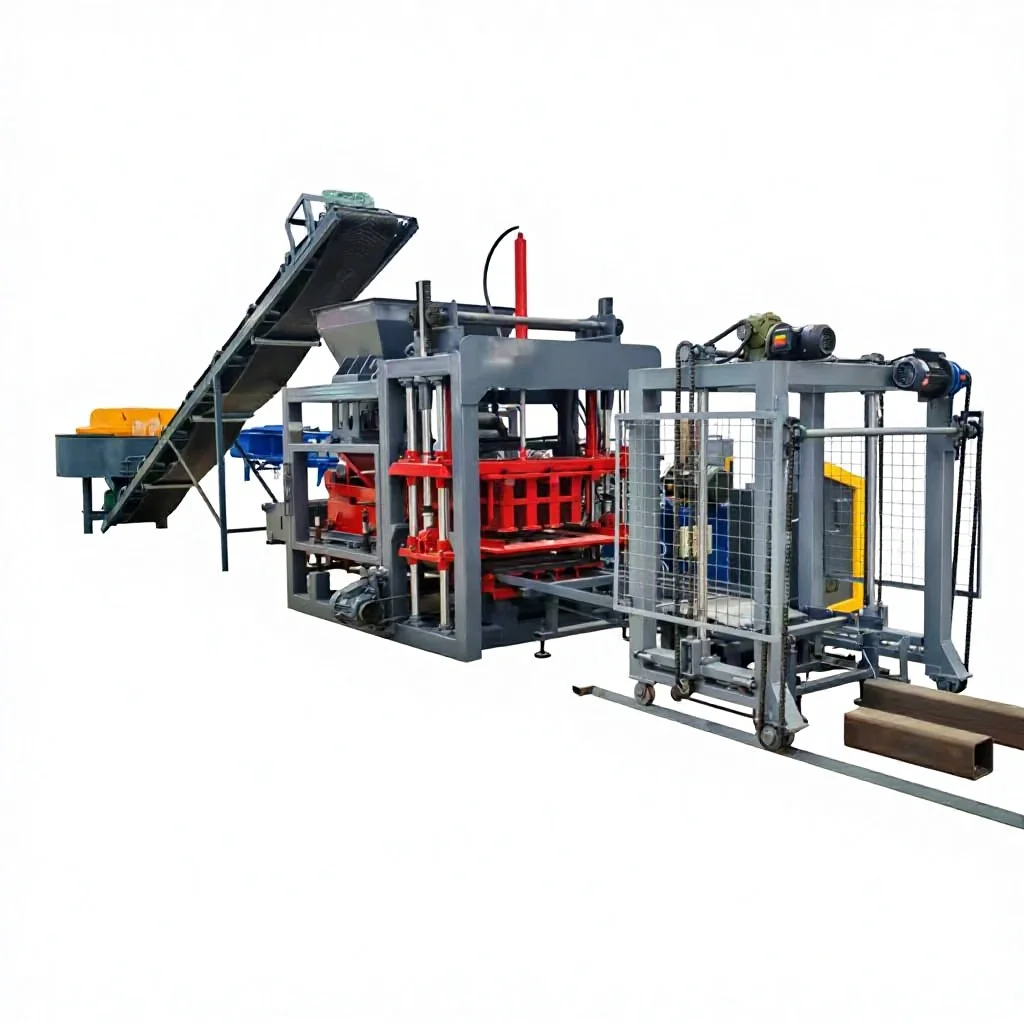
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Free Accessories | Manual hydraulic trolley, spare parts and tools |
| Output: Hollow Block 400×200×200 mm | 4 pcs/mould, 408 pcs/hr, 3264 pcs/8hr |
| Output: Hollow Block 400×150×200 mm | 5 pcs/mould, 510 pcs/hr, 4080 pcs/8hr |
| Output: Solid Brick 240×115×53 mm | 18 pcs/mould, 2100 pcs/hr, 17000 pcs/8hr |
| Voltage & Frequency | Basis not stated in source — confirm with buyer’s site requirement |
| Hydraulic Pressure | Basis not stated in source — confirm block format / material / thickness |
| Mould Change Time | Basis not stated in source — confirm block format / material / thickness |
| Automation Level | Semi-automatic (PLC controlled) |
| Stacking Method | Basis not stated in source — confirm block format / material / thickness |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial walls | Crushed stone, sand, cement, fly ash blends |
| Solid brick manufacturing for load-bearing structures | Cement, sand, and stone dust mixes |
| Paver and interlocking tile production for driveways and walkways | Fine aggregate and cement with pigments |
| Curbstone and kerb production for road and landscape edging | Coarse aggregate with high cement content |
| On-site block manufacturing for housing and development projects | Locally sourced sand, gravel, and cement |
Why "Pieces per Hour" Is the Wrong Question for a Hydraulic Block Making Machine
The only capacity number that matters is the one tied to your exact block format, mix design, and pallet cycle.
I spent my early years running QT4-15A units through factory acceptance tests, and the hardest lesson came later in the field. A Middle East buyer ordered a soil block configuration; we ran trials on standard sand, but his local red clay had high plasticity. On site, the mould stuck constantly, daily output dropped to half the quoted figure, and operators spent more time scraping cavities than running the press. That is why I now ask every buyer to send a soil sample before a single drawing is released. A hydraulic block making machine specifications sheet that quotes one headline capacity across all formats is hiding the bottleneck [NEED_CITE: block format impact on daily output in small-to-medium plants].
Cycle Time Is Format-Dependent, Not a Single Number
The QT4-15A lists a molding cycle of 15–25 seconds, which reflects the range from a thin solid brick to a deep hollow block that requires longer vibration to consolidate. When you evaluate a hydraulic block making machine, always ask for the cycle time broken down by your target format. A 15-second cycle on a solid brick mould may stretch to 25 seconds on a 400×200×200 mm hollow block because the hydraulic pressure and vibration must work through a taller, heavier column of material. The PLC control system stores individual cycle parameters per mould, so format changes do not require manual re-tuning each time.
Pallet Size Locks Your Curing Layout Before You Ship
The 850×550×25 mm pallet is a fixed dimension on this press, and it dictates your curing rack spacing, forklift tine width, and yard layout. I have seen buyers receive machines only to discover their existing racks were built for a competitor’s pallet footprint, forcing them to rebuild the curing area or hand-stack output on the floor. Before production starts, we confirm pallet compatibility against the buyer’s current handling equipment. The pallet feeder integrated in the QT4-15A line feeds boards from a magazine, so the pallet thickness must stay within tolerance to prevent jams during continuous runs.
Vibration Force and Hydraulic Pressure Must Match Your Aggregate
With 40–50 kN of exciting power at 4600 r/min, the vibration system is sized to consolidate standard crushed stone and sand mixes. But if your local aggregate is predominantly fine dust or fly ash with low coarse fraction, the standard hydraulic pressure setting may produce blocks that are too dense on the surface and weak in the core. We adjust the pressure curve during factory testing with your actual mix sample so that density stays uniform through the full block height [NEED_CITE: vibration and hydraulic pressure matching for varying aggregate gradations].
What Happens When the Mould Change Takes a Full Shift
The mould change time on this machine is not published as a fixed figure because it depends on the cavity count, block height, and whether the buyer opts for quick-release clamps or bolt-on retention. A buyer who selected six mould formats to cover every product in his catalogue ended up changing the mould so often that the press sat idle more than it ran. A hydraulic block making machine with honest capacity data means nothing if the format changeover cancels the flexibility you paid for. We recommend starting with the two or three formats that represent the bulk of your market, then adding moulds as demand justifies the changeover time.
The Hidden Cost of Skipping the Voltage Confirmation
Voltage, frequency, and PLC display language are confirmed late or not at all when buyers are rushing to ship. A 380V/50Hz machine sent to a 440V/60Hz market will run the hydraulic pump faster, altering the pressure curve and vibration frequency, which shifts block density out of spec. The PLC screen displaying Chinese characters in a Spanish-speaking plant means the operator cannot interpret fault codes, and a minor sensor alarm becomes a full line stoppage while someone translates the manual. We treat the voltage and language sign-off as a production gate, not an afterthought [NEED_CITE: voltage and frequency standards by export market].
Why Procurement Teams Stay on This Platform
Block machinery is our single focus, so the QT4-15A press, mould, pallet, and handling equipment are specified as one matched system rather than sourced from separate vendors. Configuration is set against the buyer’s actual mix design, local aggregate, and target block format — not a catalogue default that assumes standard sand. Mould design covers the formats the buyer’s market actually sells, including custom drawings when the standard catalogue does not match. The automation level is selectable: a buyer can start with semi-automatic pallet handling and upgrade to automatic stacking later without replacing the press. Installation includes operator training on the specific PLC parameters stored for each mould format.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Mould drawing and format list confirming every block type the buyer’s market requires
- Pallet specification sheet for curing rack and forklift compatibility check
- Voltage, frequency, and PLC display language confirmation signed before production
- Factory test record run on the buyer’s submitted mix sample
- Hydraulic and electrical schematic for local maintenance teams
Installation, Commissioning & Support
- Foundation slab must support the 3 T machine weight and dynamic vibration load across the 7100 mm frame length
- Dedicated power circuit required for the 18.45 kW total draw, with voltage confirmed pre-shipment
- Hydraulic station arrives integrated; field connection limited to hoses, power, and PLC I/O
- First-run commissioning includes cycle time verification per mould format stored in the PLC
- Operator training covers mould change procedure, pallet feeder loading, and fault code interpretation
- Wear parts list provided with cavity liners, vibration springs, and hydraulic seal kits identified by part number
What to Include in Your Inquiry
Send your target block format with dimensions, the daily output you need for that specific format, and a sample or lab analysis of your local aggregate. Tell us your site voltage, frequency, and preferred PLC display language. If you already have curing racks or a forklift, share the pallet dimensions and rack spacing so we can confirm the 850×550 mm board will fit.
Frequently Asked Questions
Q: How is daily output calculated for each block format on this press?
A: Output is based on the moulding cycle for that specific format multiplied by the cavity count and the number of working hours. For the 400×200×200 mm hollow block, the cycle yields 408 pieces per hour, or 3,264 in an 8-hour shift. Each format on the specification sheet carries its own figure.
Q: What mould formats are available and how long does a change take?
A: Standard moulds cover hollow block, solid brick, paver, and curbstone. Change time varies with cavity count and retention method. We confirm the exact procedure and expected duration during factory testing so you can plan shift schedules around your production mix.
Q: How do I confirm the pallet size fits my curing area and forklift?
A: The pallet is fixed at 850×550×25 mm. We ask for your existing rack dimensions and forklift tine width before production. If they do not align, we adjust the curing layout proposal or discuss alternative handling options before the machine ships.
Q: What raw material mix does this machine require?
A: The press runs crushed stone, sand, cement, dust, and fly ash. The exact ratio depends on your local aggregate and target block strength. We request a material sample to set the hydraulic pressure and vibration parameters during factory testing.
Q: How do I specify voltage, frequency, and PLC language before shipment?
A: These are confirmed in a signed document before production starts. We need your site voltage, frequency, and preferred display language. The PLC stores all parameters in that language, so operators can read fault codes and cycle settings without translation.