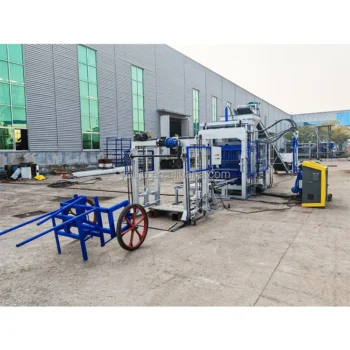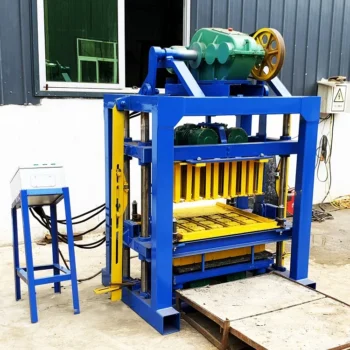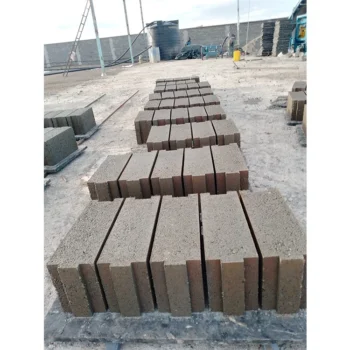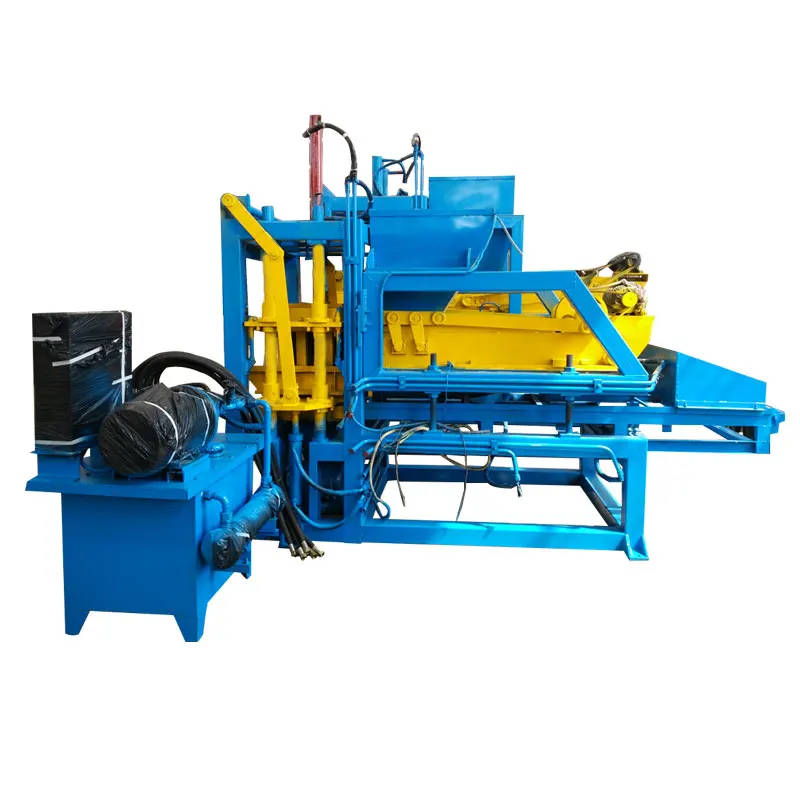
Description
Capacity matched to your block format — the LY7-10 configuration is set against the buyer’s actual clay soil properties and target interlocking profile, not a generic catalogue figure.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY7-10 |
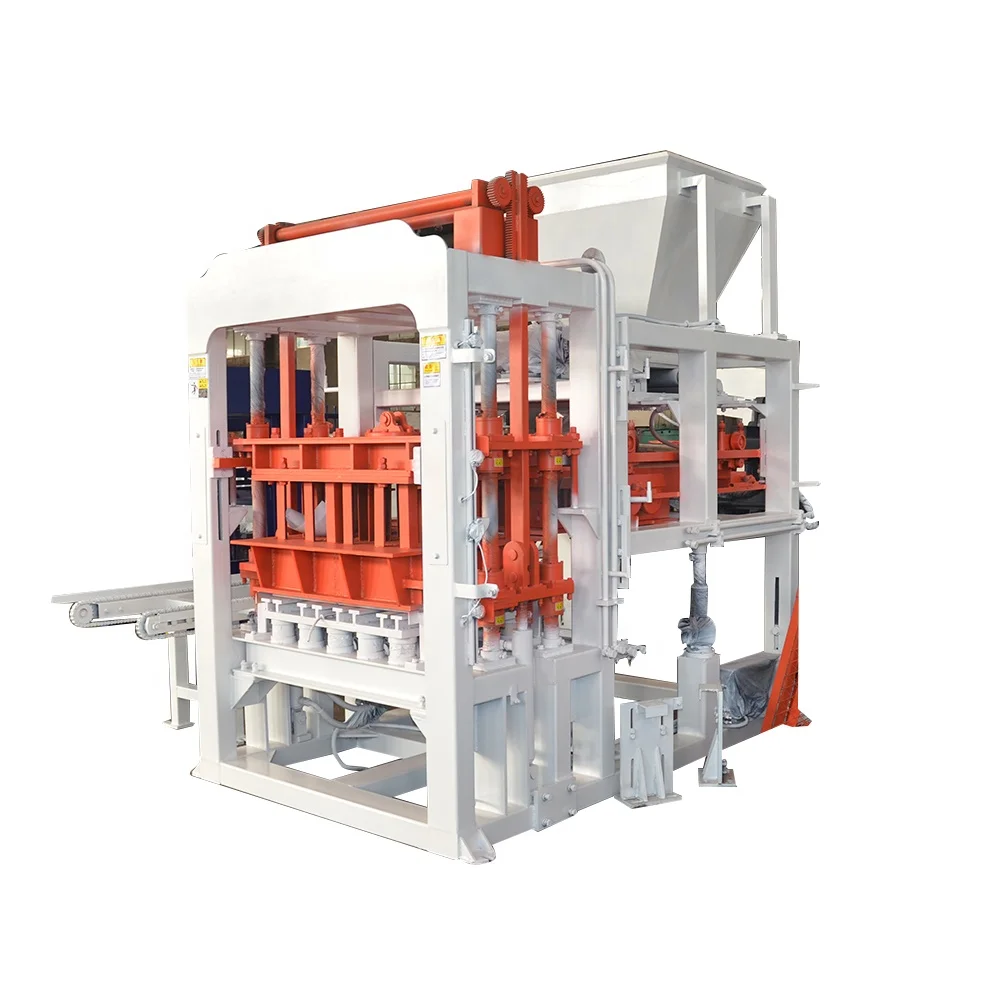
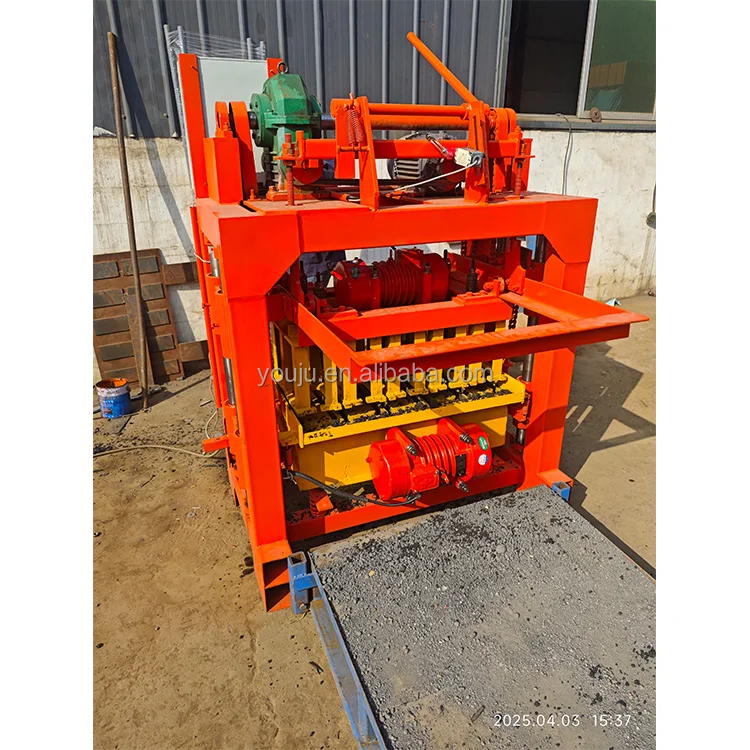
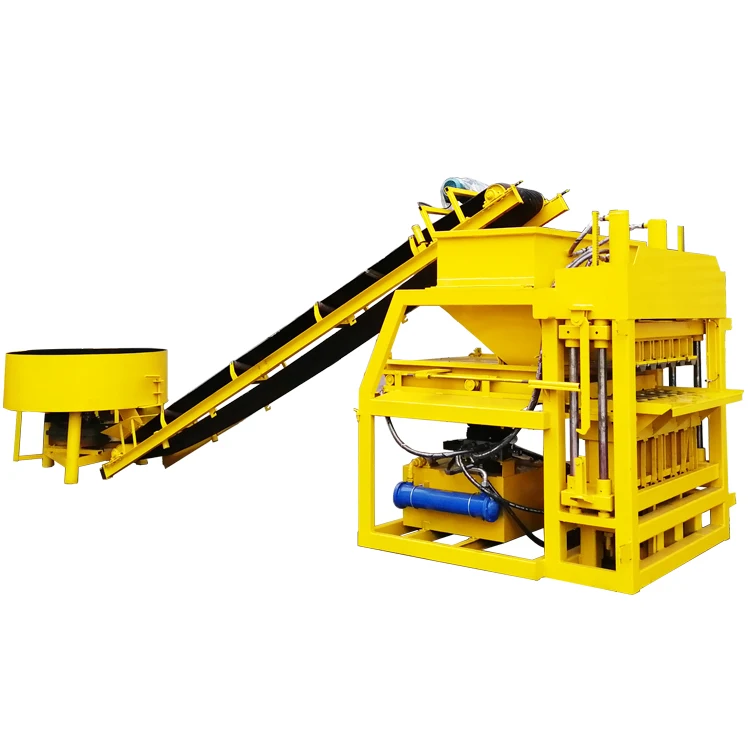
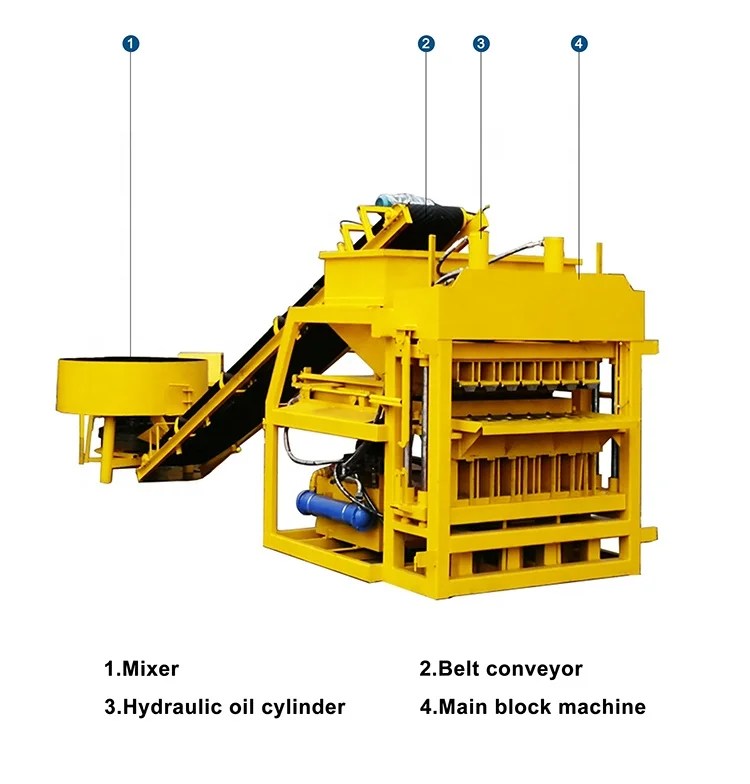
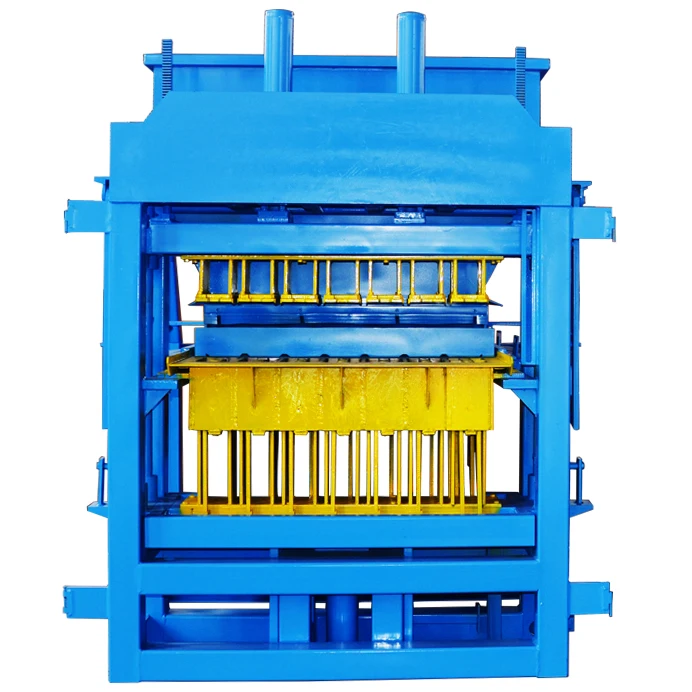
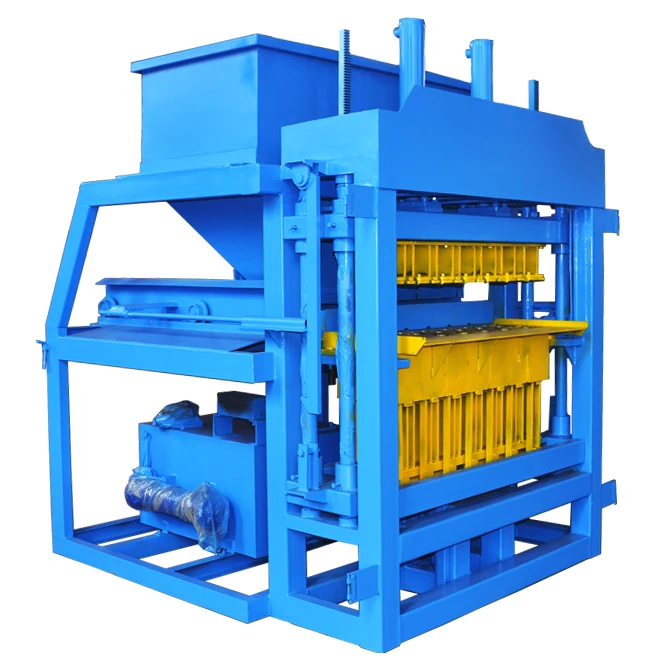
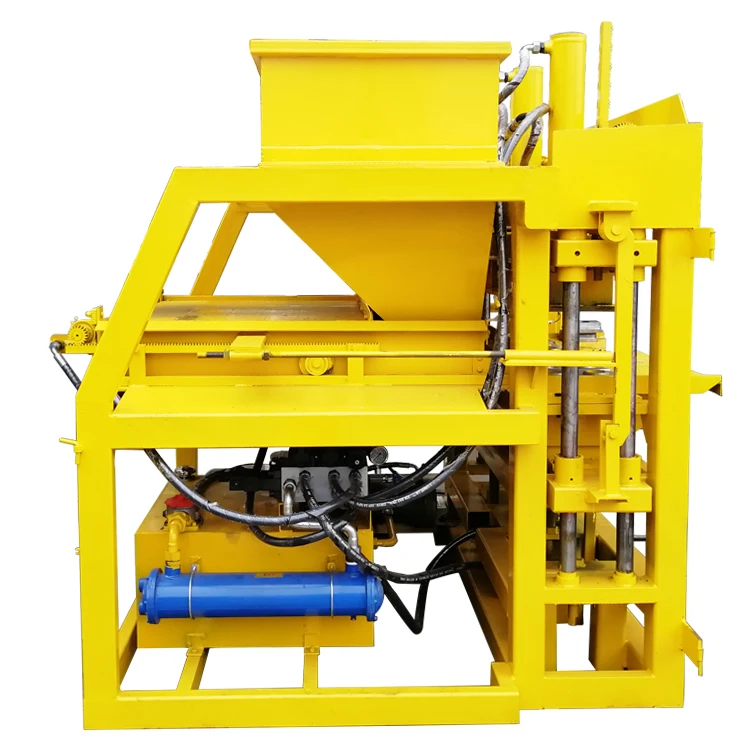
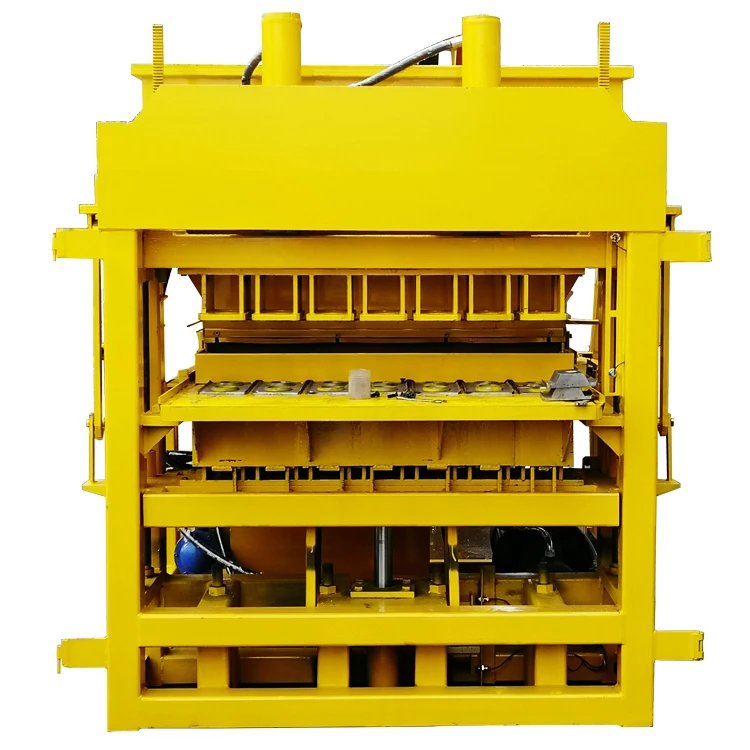
| Product Type | Automatic Clay Soil Compressed Earth Interlocking Block Making Machine |
| Machine Type | Stationary compressed earth interlocking block maker |
| Raw Material | Clay soil |
| Automation Level | Automatic |
| Block Format | Interlocking compressed earth block |
| Mould Format | Interlocking earth block |
| Hydraulic Pressure | basis not stated in source — confirm block format / material / thickness |
| Vibration Force | basis not stated in source — confirm block format / material / thickness |
| Pallet Size | basis not stated in source — confirm block format / material / thickness |
| Mould Change Time | basis not stated in source — confirm block format / material / thickness |
| Cycle Time per Format | basis not stated in source — confirm block format / material / thickness |
| Output Capacity | basis not stated in source — confirm block format / material / thickness |
| Control System | basis not stated in source — confirm block format / material / thickness |
| Voltage & Frequency | basis not stated in source — confirm block format / material / thickness |
| Overall Dimensions | basis not stated in source — confirm block format / material / thickness |
| Net Weight | basis not stated in source — confirm block format / material / thickness |
| Key Features | Automatic operation, stationary configuration, interlocking mould capability, hydraulic pressing |
Application Suitability
| Application | Material or Output |
|---|---|
| Housing and development project construction | Interlocking compressed earth blocks from locally sourced clay soil |
| On-site or plant-based block manufacturing | Clay-based interlocking bricks for residential and commercial building projects |
| Low-cost sustainable building material production | Compressed earth blocks in regions with accessible clay deposits |
| Building material manufacturers expanding product range | Interlocking earth block formats added to existing concrete or masonry lines |
| First-time block plant entrepreneurs | Clay soil interlocking blocks targeting affordable construction markets |
Why "Cycles per Hour" Fails to Tell the Full Story
Daily output means nothing unless the exact block format behind that number is stated upfront.
I once watched a buyer sign off on a compressed earth interlocking block machine specifications sheet based on a single hourly cycle count. Three months later, the actual interlocking profile he needed ran at a considerably longer cycle, and his daily throughput fell well below what he had planned his labour force around. The gap between a quoted cycle rate and the real output for your specific block format is where most plant budgets quietly break down [NEED_CITE: block format cycle time variance in compressed earth block production].
Matching the Interlocking Profile to Your Local Market
The LY7-10 is configured around the interlocking block profile that your market actually buys, not a default mould pulled from stock. Different interlocking geometries — from simple tongue-and-groove to multi-directional key profiles — demand different compression sequences and cycle times. When you evaluate compressed earth interlocking block machine specifications, the profile drawing and dimensional tolerances matter far more than a generic output claim, because the locking mechanism must align on-site without mortar adjustment.
How Clay Soil Variability Changes the Configuration
Clay soil is not a single material; its plasticity index, moisture window, and sand-to-clay ratio shift from one deposit to the next. The hydraulic pressure and compression dwell time on the LY7-10 are set only after reviewing a sample from your actual source. Running a machine calibrated for one clay composition against a different local deposit produces blocks that crumble at the interlocking joints or fail to reach adequate density [NEED_CITE: clay soil plasticity and compressed block strength correlation].
Reading the Specifications That Actually Matter
Hydraulic pressure and compression force work together to determine the final block density and interlocking edge integrity. Too little pressure on a high-clay mix leaves the block friable; excessive force on a sandy blend can crack the interlocking keys during ejection. Pallet size must match both the block footprint and the curing rack spacing already in your yard, because mismatched pallets create a bottleneck that no amount of press speed can overcome. Mould change time determines whether switching from a wall block to a corner block costs you an hour or an entire shift — a detail that only matters if you plan to run more than one format.
The Hidden Cost of Skipping Soil Testing Before Order
When a buyer skips sending a soil sample and accepts a standard configuration, the machine arrives calibrated for a mix it will never see. The result is inconsistent block density, interlocking joints that do not seat properly, and a rejection rate that erodes the project margin. Correcting this after commissioning means new mould tooling, revised compression parameters, and weeks of lost production while the supplier recalibrates remotely [NEED_CITE: compressed earth block failure modes from incorrect soil calibration].
Why Buyers Choose This Source
The LY7-10 is supplied as a matched system — press, mould, pallet, and handling specified together rather than assembled from disconnected vendors. Each machine is configured against the buyer’s clay sample and target block format, so the capacity calculation reflects the product you will actually sell. Mould design covers the interlocking profiles your market demands, including custom drawings when standard formats do not fit. The automation level is selectable, meaning a plant can start with semi-automatic pallet handling and add automatic stacking later without replacing the press. Installation support includes operator training on your specific soil mix and block format.
Documentation & Verification
- Line layout drawing with capacity calculation tied to your exact interlocking block format
- Mould drawing pack confirming interlocking profile dimensions and joint tolerances
- Machine specification sheet listing hydraulic pressure matched to your clay soil test results
- Voltage, frequency, and PLC display language written confirmation before build sign-off
- Factory test record showing block density and dimensional output on your soil sample
- Operation and maintenance manual with wear parts list specific to the LY7-10 configuration
Installation, Commissioning & Support
- Foundation requirements sized to the LY7-10 weight and hydraulic press dynamic load
- Electrical supply verified against the confirmed voltage and frequency before wiring begins
- Machine arrives in dismantled shipping state with reassembly supervised on your site
- First production run calibrated to your clay soil mix and target interlocking block density
- Operator training covers mould change procedure, compression parameter adjustment, and daily maintenance
- Wear parts list and hydraulic seal kit specified for the LY7-10 supplied at commissioning
What We Need to Configure Your Machine
To prepare an accurate proposal, share your clay soil test results including plasticity index and natural moisture content. Specify the interlocking block profile dimensions your local construction market requires and the daily output you need per format. Confirm your site voltage, frequency, and preferred PLC display language, along with the curing rack dimensions and forklift pallet capacity already in use at your yard.
Frequently Asked Questions
Q: What interlocking block formats can the LY7-10 produce, and how does cycle time differ between them?
A: The LY7-10 runs interlocking compressed earth block profiles selected for your market, including standard tongue-and-groove and custom multi-key geometries. Cycle time varies with each profile because deeper interlocking features require longer compression dwell. A capacity calculation is provided per format, not as a single blanket figure, so you know the realistic daily output for the specific block you will produce.
Q: How is daily output calculated, and which block format is it based on?
A: Daily output is calculated from the cycle time of your chosen interlocking block format, multiplied across the planned operating hours and adjusted for mould change intervals and pallet circulation. The capacity figure in your quotation names the exact block format and dimensions it assumes, so there is no ambiguity between the quoted number and what your plant will deliver on a typical production day.
Q: What clay soil properties are needed for consistent interlocking block strength?
A: Consistent block strength depends on the clay’s plasticity index, sand-to-clay ratio, and moisture content at the time of pressing. A soil sample is tested before the machine is configured, and the hydraulic pressure is set to match that specific composition. If your local deposit varies seasonally, the configuration includes adjustable compression parameters so operators can compensate without stopping production.
Q: How long does a mould change take, and what does the procedure involve?
A: Mould change time depends on the interlocking profile complexity and the changeover system fitted to your LY7-10. The procedure involves releasing the mould clamp bolts, lifting out the current mould with the plant crane or hoist, seating the replacement mould, and recalibrating the compression stroke. Training covers the full sequence so your crew can complete format switches within a planned maintenance window.
Q: What pallet size is specified, and how does it work with existing curing racks?
A: Pallet size is selected to match your interlocking block footprint and the curing rack spacing already installed at your site. The pallet material is chosen for the block weight and local climate conditions. Your quotation confirms pallet dimensions against your existing forklift capacity and rack layout, so blocks move from press to curing area without manual rehandling.