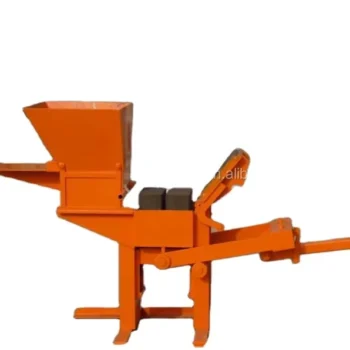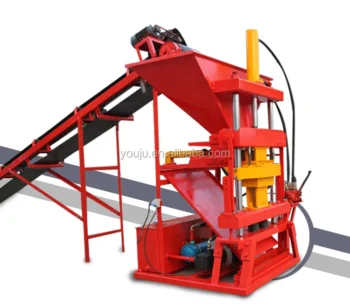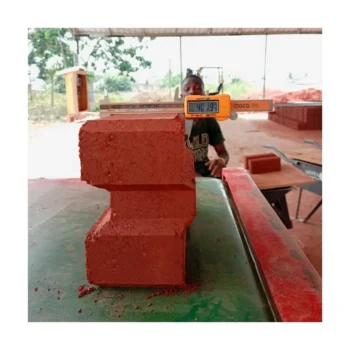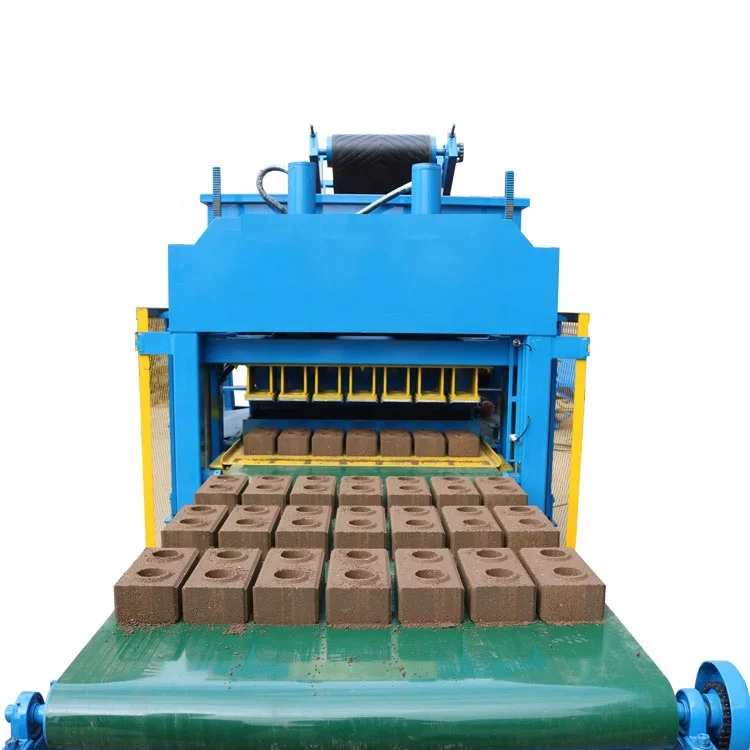
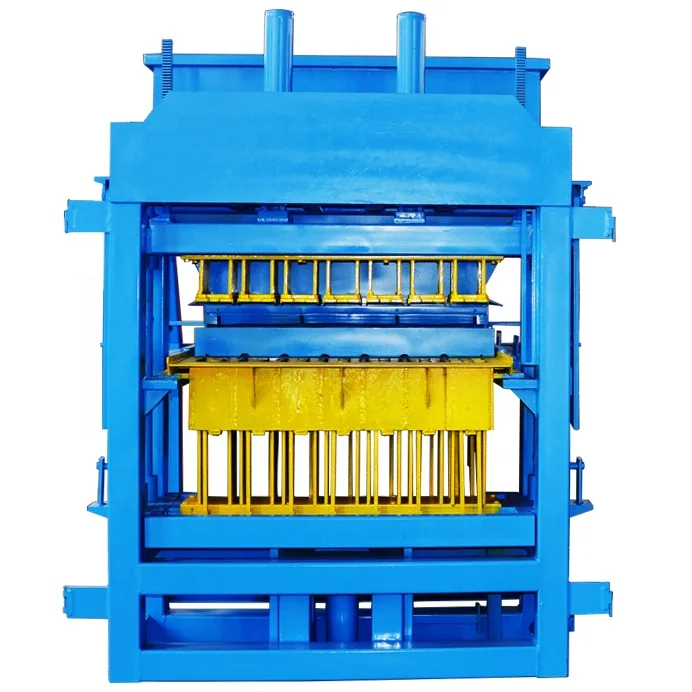
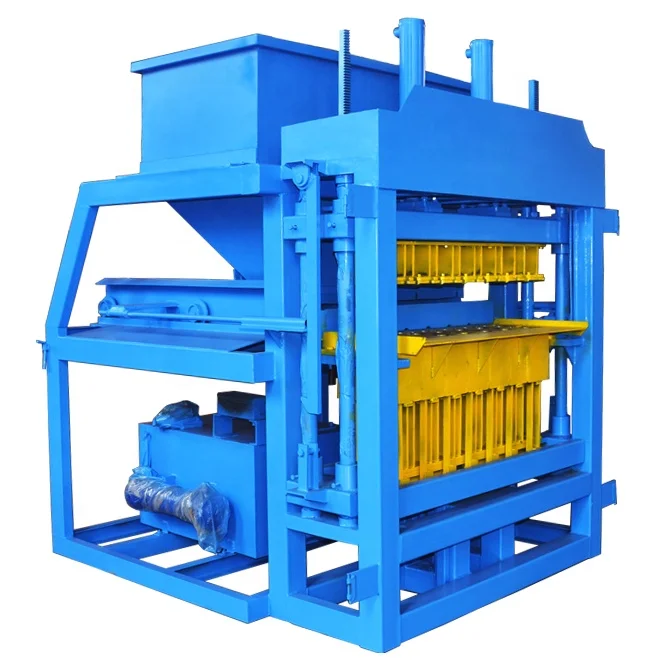
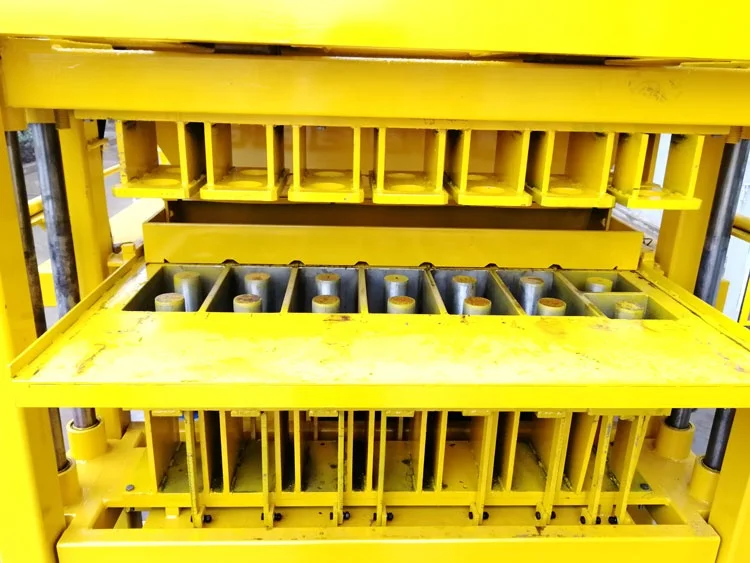
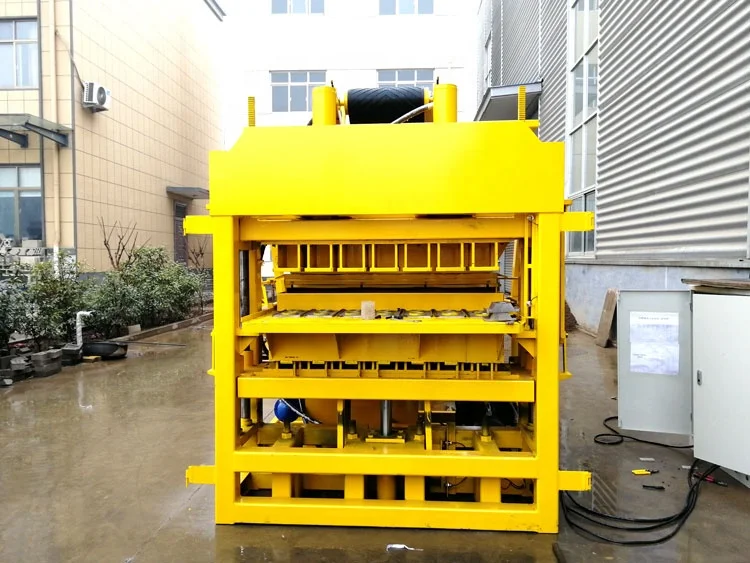
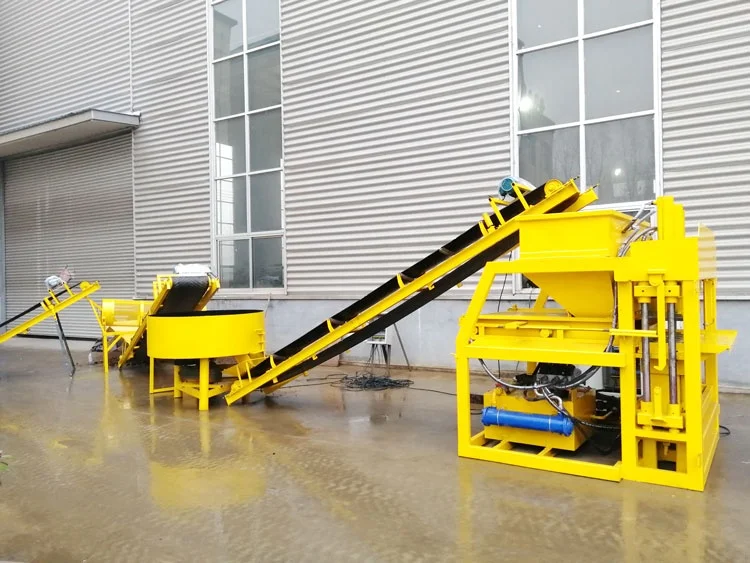
Description
Matched System Configuration — hydraulic pressure and mould geometry calibrated to the buyer’s tested clay sample before the contract is signed, so block density holds across every shift.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Clay Interlocking Brick Making Machine |
| Model | LY7-10 |
| Rated Power | 18.5 kW |
| Molding Cycle | 10-15 s |
| Output Capacity | 20,160 pcs/day (based on 300×150×100 mm interlocking brick, 7 pcs/mould) |
| Hydraulic Pressure | 25-32.5 MPa |
| Raw Material Compatibility | Laterite, yellow or red soil, sand, cement, water |
| Automation Level | Automatic feeding, pressing, and lifting |
| Labor Requirement | 1-2 workers |
| Machine Weight | 1,600 kg |
| Overall Dimensions | 2,260 × 1,500 × 2,380 mm |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site housing project brick production | Laterite or locally sourced red/yellow soil with 6-8 % cement |
| Small block plant adding clay interlocking formats | Full-clay recipe (90-95 % clay, 3 % water) or cement-clay blend |
| Construction contractor self-supply | Soil-based interlocking bricks using site-excavated material |
Why "20,000 Bricks per Day" Means Nothing Without the Format
The number only holds when the block size, mould cavity count, and cycle time are all stated together.
Most automatic clay interlocking brick making machine specifications quote a daily figure that assumes an ideal format the buyer never actually produces. I have watched contractors receive a machine rated for a small paver size, then discover their market-standard 300×150×100 mm interlocking brick cuts real output nearly in half because the mould holds fewer cavities and the pressing cycle runs longer. The gap between catalogue capacity and shift output is where project schedules fail. [NEED_CITE: common capacity misalignment in block machine procurement]
Matching the Press to the Block You Actually Sell
Capacity for the LY7-10 is stated at 2,520 pieces per hour based on a 300×150×100 mm interlocking brick with 7 cavities per mould and a 10-15 s cycle. Switch to a larger wall block and the cavity count drops, pulling hourly output down accordingly. This is why we confirm the buyer’s exact format before finalizing the mould order, not after.
Hydraulic Pressure and Mix Design Must Agree
The 25-32.5 MPa hydraulic range is wide enough to cover both a cement-clay blend (6-8 % cement, 80-90 % clay) and a full-clay recipe (90-95 % clay). Higher clay content demands greater pressure to reach target density because clay particles are finer and trap more air. Running a full-clay mix at the lower end of the pressure range produces bricks that crumble at the interlock tongue. [NEED_CITE: relationship between hydraulic pressure and clay brick compressive strength]
Reading the Numbers That Matter
A molding cycle of 10-15 s sets the rhythm for the whole line: feeder travel, press dwell, and lifting table return must all complete inside that window. The 18.5 kW rated power is sized for the hydraulic pump and feeder motor combined; undersizing would force the pump to stall at peak pressure. Machine weight of 1,600 kg provides the dead mass that absorbs vibration without requiring a separate inertia foundation, keeping installation straightforward on a compacted gravel base. Pallet dimensions must match the curing racks and forklifts already on site, or the operator spends half the shift moving bricks by hand.
The Cost of Skipping the Soil Test
Sending a soil sample before signing the order feels like a delay, but it prevents far longer delays at commissioning. I have seen projects lose weeks because the local laterite had a higher sand fraction than assumed, and the mould released bricks with chipped edges until the mix ratio and pressure were both reset. Adjusting parameters on site is always slower and more expensive than adjusting them on the factory test bench. [NEED_CITE: field failures traced to untested raw material in block production]
Why Source the Line Here
Block machinery is our single focus, so the LY7-10 press, interlocking mould, pallet specification, and material feeder are configured as one matched set rather than assembled from separate vendors. We set hydraulic pressure and cycle timing against your tested clay sample, not a default catalogue value. Custom mould designs are produced from buyer drawings, allowing interlocking formats that match local building codes. Automation level is selectable: a buyer can start with semi-automatic pallet handling and add automatic stacking later. Installation support includes operator training on mould change procedure and daily maintenance routines.
Documentation & Verification
- Line layout with capacity calculation locked to your confirmed interlocking brick format
- Mould drawing and format list showing available cavity sizes and changeover steps
- Voltage, frequency, and PLC display language confirmed before production starts
- Factory test record measuring actual cycle time on your specified block dimensions
Installation, Commissioning & Support
- Foundation pad sized to the 2,260 × 1,500 mm footprint with compacted gravel base
- Dedicated 18.5 kW circuit with voltage and frequency matched to your site supply
- Machine shipped as a single skid; lifting eyes allow forklift or crane unloading
- On-site commissioning covers pressure calibration for your tested soil sample
- Operator training on 10-15 s cycle rhythm, mould change, and daily hydraulic checks
- Wear parts list covering hydraulic seals and mould liner replacement intervals
What We Need to Configure Your Line
Tell us the exact interlocking brick dimensions your market requires, along with a 5 kg soil sample from your intended borrow pit. Share your site voltage, frequency, and preferred control language so the electrical cabinet is wired correctly before dispatch. If you already operate curing racks or forklifts, send the pallet dimensions they accept so we match the feeder and lifting table accordingly.
Frequently Asked Questions
Q: How is the daily output figure calculated for this machine?
A: The 20,160 pieces per day figure assumes a 300×150×100 mm interlocking brick, 7 cavities per mould, and a 10-15 s molding cycle running across an eight-hour shift. If your market needs a larger or smaller format, cavity count and cycle time shift, so we recalculate capacity against your confirmed brick dimensions before quoting.
Q: Can hydraulic pressure be adjusted for my local clay?
A: Yes. The system covers 25-32.5 MPa, adjustable through the relief valve on the hydraulic manifold. We set the working pressure during the factory test using your soil sample and record the value on the test certificate so your operator knows the baseline for each mix recipe.
Q: What interlocking mould formats are available?
A: Standard moulds cover common interlocking brick sizes used in housing projects, and custom moulds can be produced from buyer-supplied drawings. Mould changeover involves releasing four locating bolts and lifting the mould plate with the overhead crane; a trained operator completes the swap within a single shift break.
Q: What mix ratio works for full-clay versus cement-clay bricks?
A: For a cement-clay blend we typically start at 6-8 % cement, 80-90 % clay, and 3 % water. Full-clay recipes run 90-95 % clay with 3 % water and require higher hydraulic pressure to achieve comparable density. We validate both options with your soil sample before recommending one.
Q: Is voltage and control language confirmed before shipment?
A: Voltage, frequency, and PLC display language are confirmed in writing after order placement and verified again during the factory test. The electrical cabinet is wired to your specification, and the test record includes a photograph of the HMI screen showing the correct language before the machine is crated.