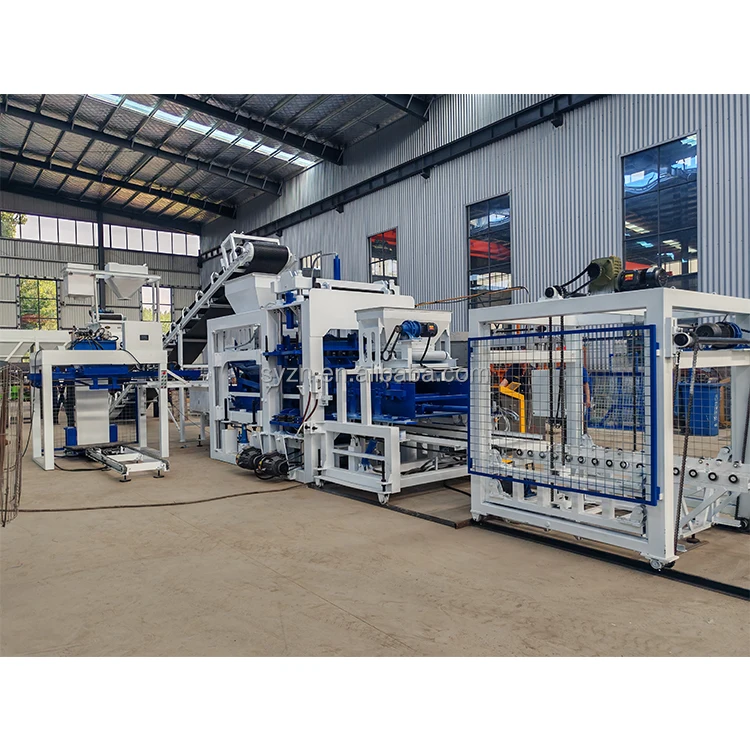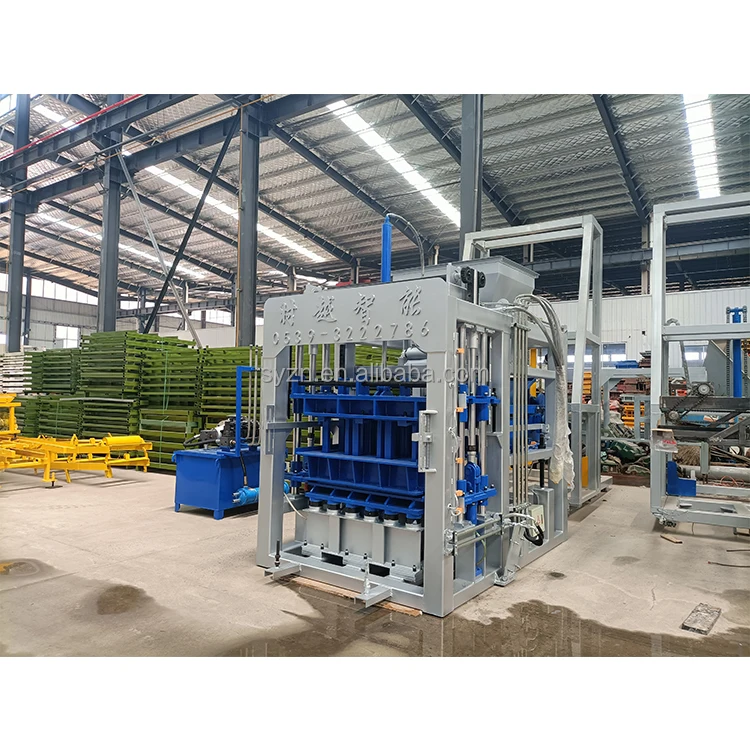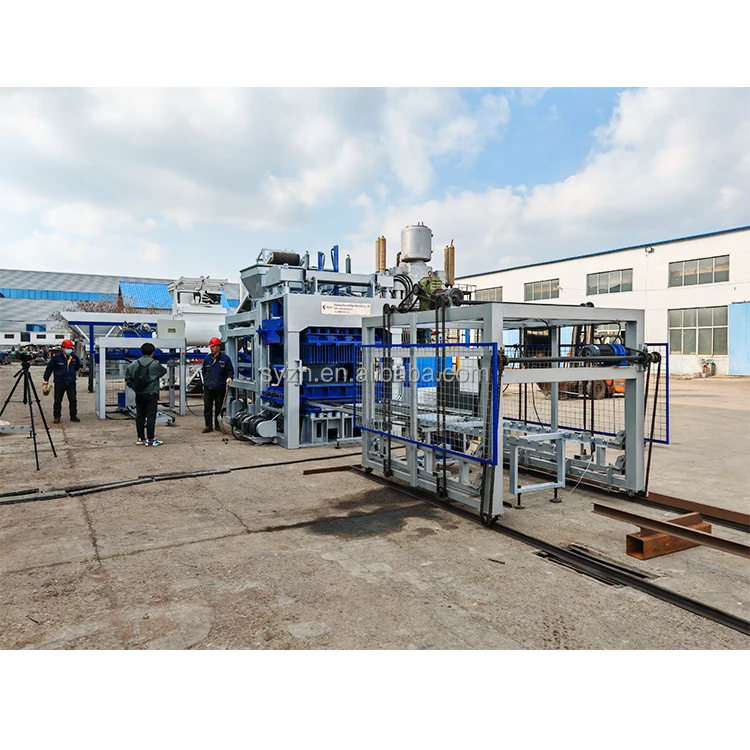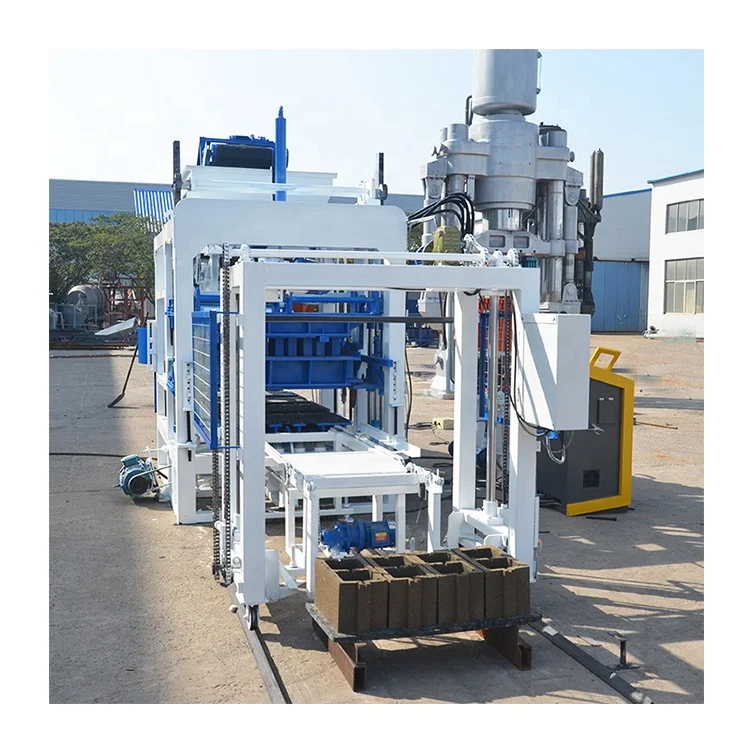


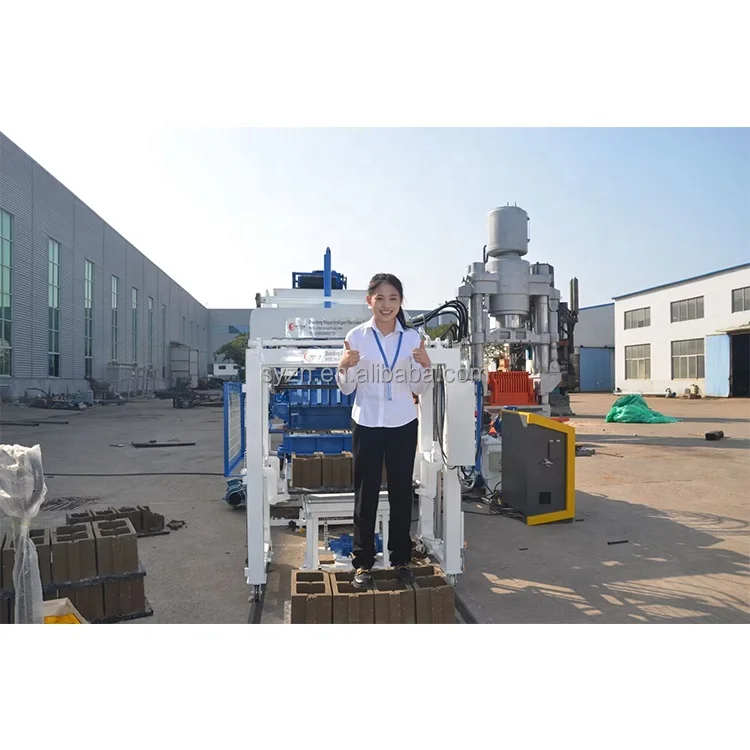
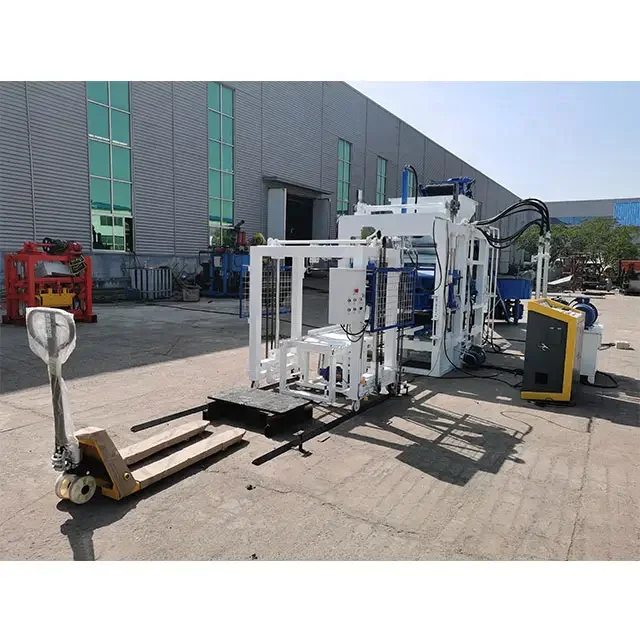
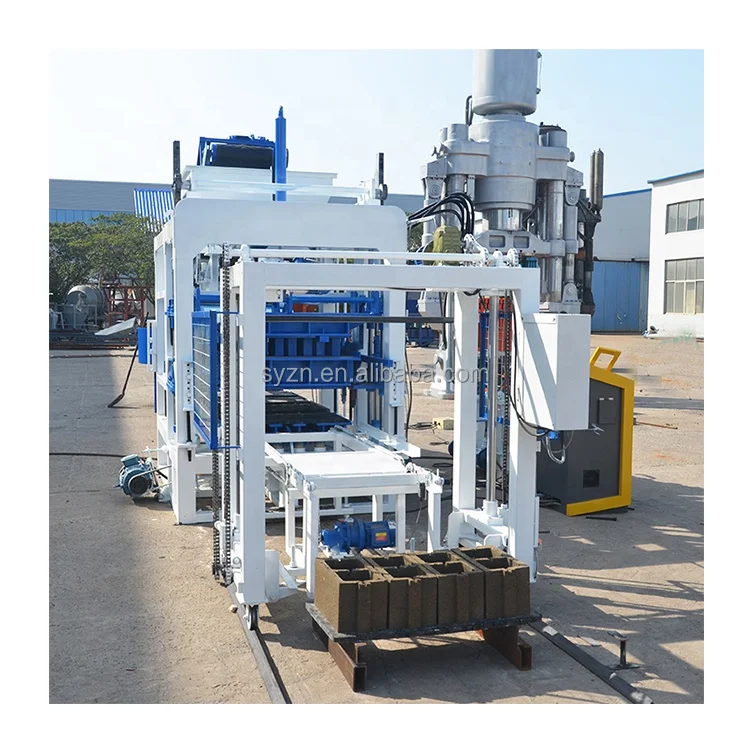
Description
Matched System Sizing — Every component from the host press to the JQ350 mixer and pallet specification is configured against your target block format and local aggregate, not pulled from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
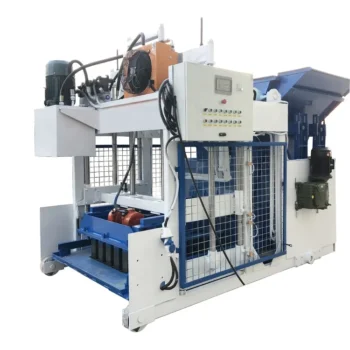
| Product Type | Hydraulic Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 3900×1600×2300 mm |
| Total Weight | 3 T |
| Rated Power | 24 kW |
| Vibration Force | 40–50 kN |
| Control System | Hydraulic station with PLC (source value — verify against manufacturer catalog) |
| Moulding Cycle | 15–25 s (basis not stated in source — confirm block format) |
| Pallet Size | 850×550×25 mm |
| Mixer Model | JQ350 |
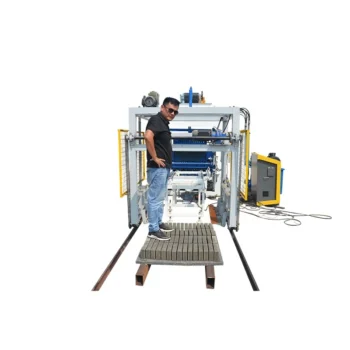
| Key Features | Semi-automatic operation, configurable mould formats (hollow, solid, paver, curbstone), separate automatic stacker station available |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for load-bearing walls | Crushed stone, sand, cement, fly ash |
| Solid brick manufacturing for masonry | Cement, dust, sand mixtures |
| Paving block production for walkways and driveways | High-density aggregate and cement blends |
| Kerbstone forming for road and pavement edges | Coarse aggregate with cement binder |
What the QT4-18 Block Making Machine Specifications Actually Mean for Your Daily Output
A quoted cycle time only becomes real capacity when tied to a specific block format and mix design.
I remember a buyer who ordered based on a single hourly figure, only to find his local sand had high clay content. The resulting hollow blocks failed strength tests, and daily output dropped sharply because rejects had to be re-pressed. The QT4-18 block making machine specifications list a moulding cycle of 15–25 seconds, but that range exists precisely because different formats and materials demand different dwell times [NEED_CITE: effect of aggregate clay content on concrete block compressive strength]. Without confirming your target format and local material properties first, any capacity number is a guess.
Mould Format Range and Changeover Reality
The QT4-18 supports hollow block, solid brick, paver, and curbstone moulds, giving a small-to-medium plant genuine format flexibility. The vibration force of 40–50 kN must be matched to whichever format you run most often, because a setting optimised for hollow blocks may not produce adequate density in solid bricks. This is where the QT4-18 block making machine specifications diverge from catalogue machines that apply a single vibration profile across all formats.
Matching the Pallet to Your Curing Area Before You Order
The 850×550×25 mm pallet size is a fixed parameter that dictates how blocks are moved from press to curing area. If your existing forklift tines or curing racks are dimensioned for a different pallet, you face either a pallet replacement cost or a curing bottleneck. I always confirm the buyer’s curing layout before locking this dimension in, because pallet mismatches have delayed commissioning on more than one project I have been involved with [NEED_CITE: pallet handling compatibility in concrete block curing operations].
Reading the Specs That Matter for Block Density
The 40–50 kN vibration force works together with hydraulic pressure to compact the mix into the mould cavity. Insufficient vibration leaves voids; excessive force can cause segregation where heavier aggregate settles and cement paste rises. The 15–25 second cycle range allows the operator to extend dwell time for denser formats like pavers while keeping hollow block cycles shorter. Rated power of 24 kW covers both the hydraulic station and the vibration motor, which is typical for a press in this output tier. The JQ350 pan mixer feeds material at a rate intended to keep the press from waiting between cycles.
When a Mismatched Line Configuration Costs More Than the Machine
If the conveyor speed does not match the press cycle, the mixer either overfeeds and material sets in the hopper, or underfeeds and the press idles. A stacker listed as a separate station means manual pallet handling is the default; without budgeting for that labour or adding the stacker, your quoted output assumes hands that may not exist on the shop floor. Buyers who focus only on the host press price often discover these gaps during commissioning [NEED_CITE: common line integration failures in small block plants].
Why Sourcing the Full Line from One Supplier Reduces Integration Risk
Block machinery as a single focus means the QT4-18 host press, JQ350 mixer, conveyor, and pallet specification are evaluated as one system. Configuration is set against your actual mix design and local aggregate rather than a default recipe. Mould design covers the formats your market demands, with custom drawings available when standard moulds do not fit. Automation level is selectable, so you can begin with semi-automatic pallet handling and add the stacker later. Installation support includes operator training on your specific block format and mix.
Documentation & Verification
- Line layout drawing showing QT4-18 station spacing and pallet flow path
- Capacity calculation sheet stating the block format assumed for each output figure
- Mould drawing and format list with confirmed cycle time per block type
- Hydraulic and electrical schematic for the 24 kW system
- Factory test record on your target block format before dispatch
- Voltage, frequency, and PLC display language confirmation document
Installation, Commissioning & Support
- Foundation pad sized for 3900×1600 mm footprint and 3 T static load
- Dedicated 24 kW power circuit with voltage and frequency confirmed before wiring
- Host machine, mixer, and conveyor arrive separately and require on-site assembly
- PLC parameter tuning for your local aggregate and target block density
- Operator training on mould changeover procedure for each purchased format
- Wear parts list covering hydraulic seals and mould liner replacements
Before Requesting a Quotation for the QT4-18
Tell us which block format sells in your market, the daily volume you need, and the local raw materials you can source. Include your site voltage, frequency, and the curing space you have available so the pallet specification and line layout can be sized correctly. If you are replacing an existing press, share the current mould dimensions and any pallet inventory you want to keep using.
Frequently Asked Questions
Q: How is output capacity verified, and which block format does each figure assume?
A: Every capacity figure must state the block format, mix design, and cycle time it assumes. For the QT4-18, hollow block 400×200×200 mm and 400×150×200 mm each produce different hourly volumes because the mould cavity count and compaction time differ. We provide a written capacity calculation tied to your chosen format before you commit.
Q: How do I match pallet size and material to my existing curing area and forklift?
A: The QT4-18 uses 850×550×25 mm pallets. Before ordering, we confirm your curing rack dimensions, forklift tine spacing, and whether you use wood, bamboo, or PVC pallets. A mismatch here causes handling delays that no amount of press speed can fix.
Q: What is the real mould change time, and does it cancel out format flexibility?
A: Mould change time depends on whether the press uses a bolt-on or slide-in mould mounting system. We state the changeover procedure and estimated time for each mould pair you purchase, so you know how many format switches per shift are practical on the QT4-18.
Q: Which raw materials and mix designs is the QT4-18 configured for?
A: The press handles crushed stone, sand, cement, dust, and fly ash. However, vibration force and hydraulic pressure must be tuned to your specific aggregate grading and cement content. If your local sand has high clay or unusual moisture, we adjust parameters before factory testing.