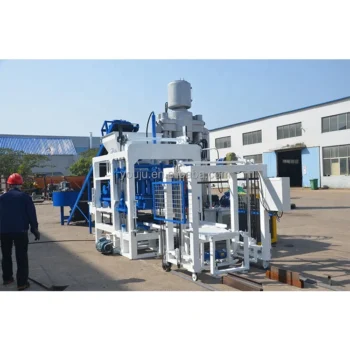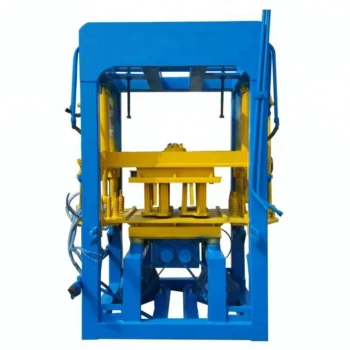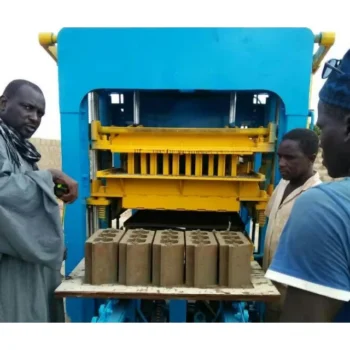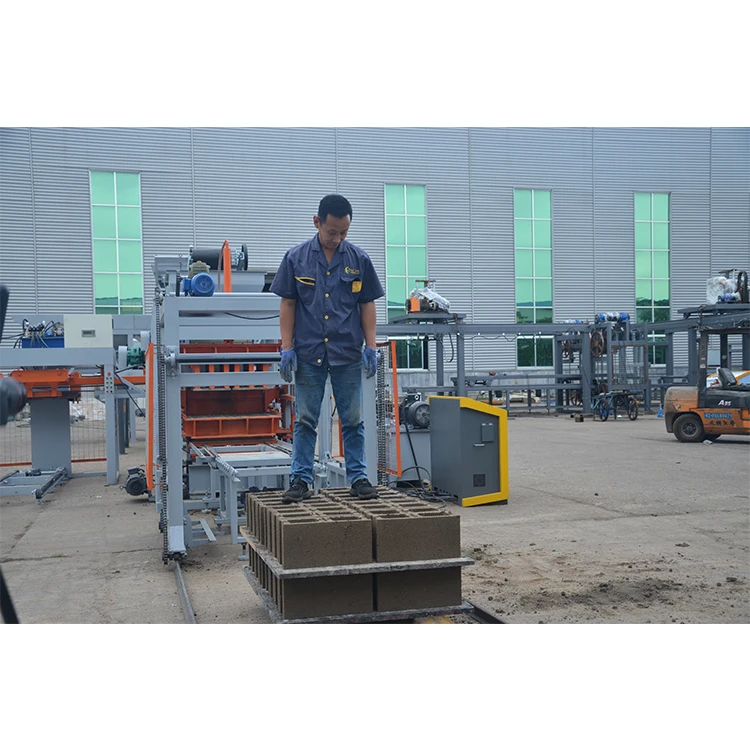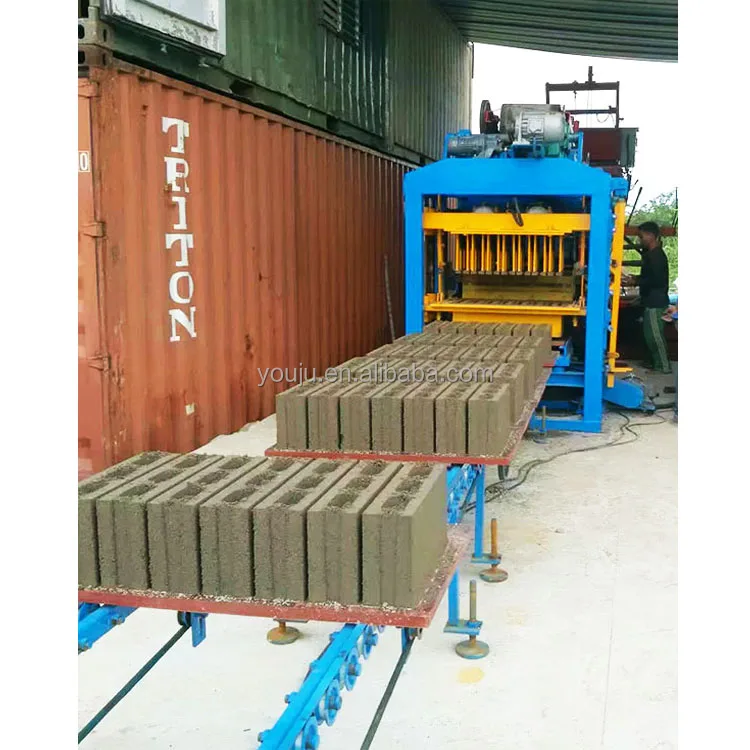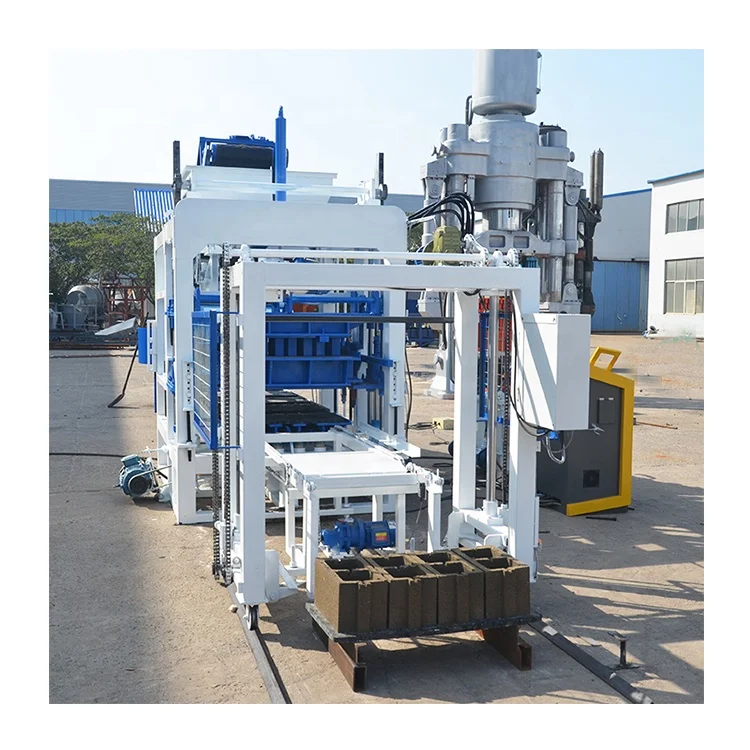
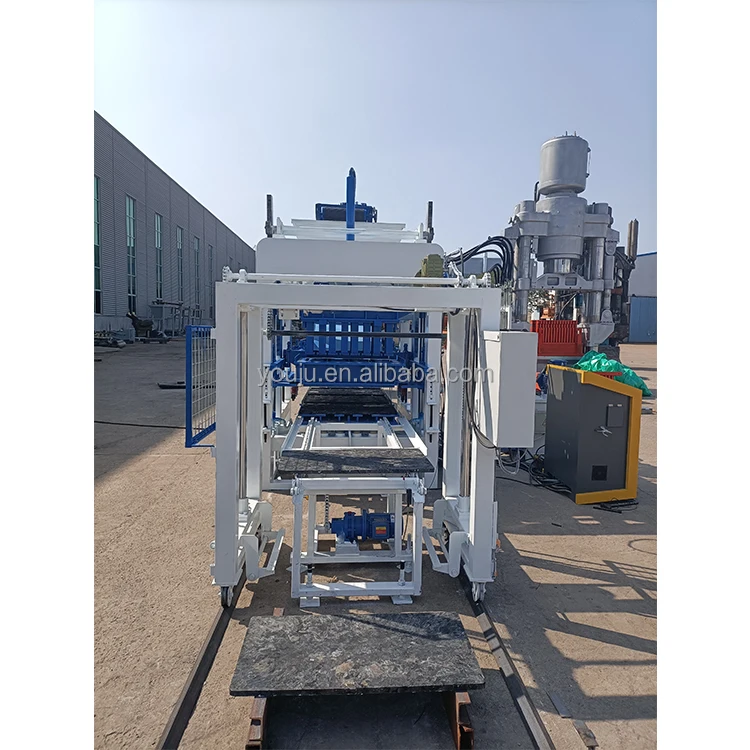

Description
Honest Capacity by Format — we calculate cycle time and daily output against the specific block format you sell, not a single catalogue figure that assumes ideal conditions.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Automatic Concrete Block Making Machine |
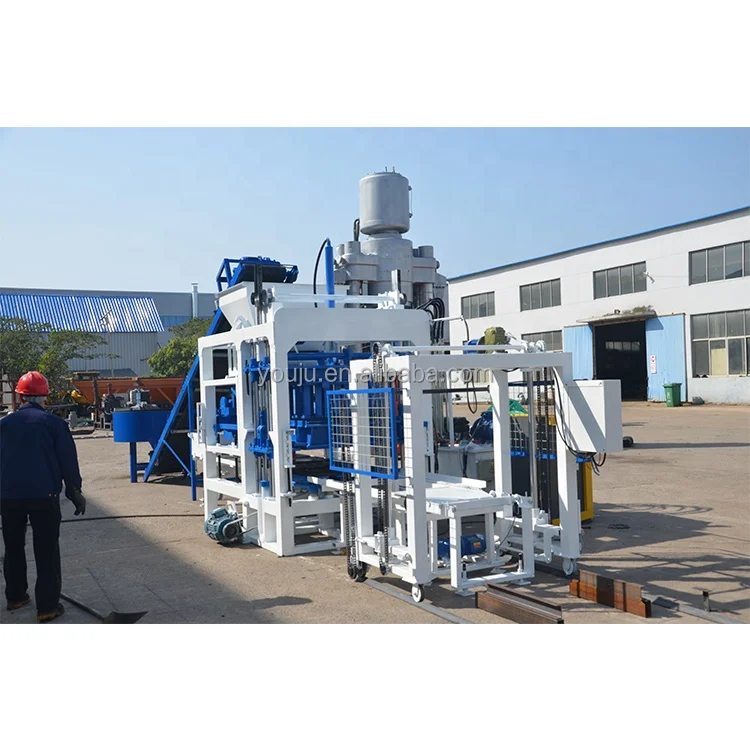
| Overall Dimensions (L×W×H) | 2500×1750×2200mm |
| Rated Pressure | 16MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550mm |
| Molding Cycle | 18-25s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 27.5kW |
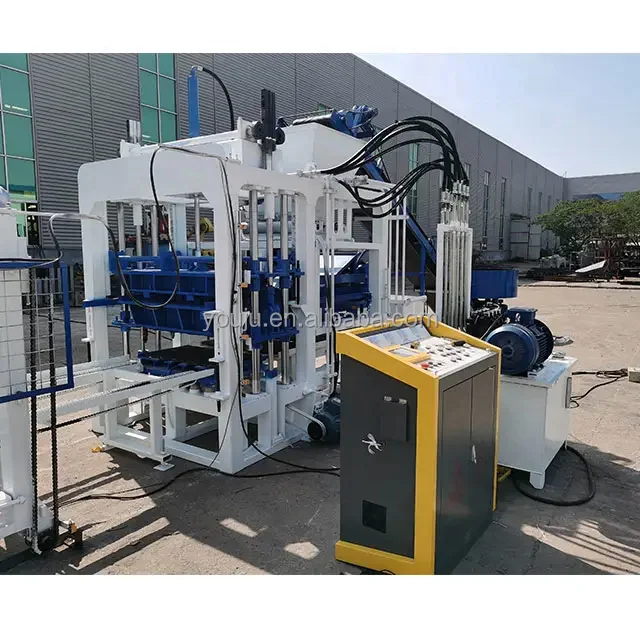
| Control System | PLC with frequency converter |
| Electrical Components | Schneider brand |
| Material Feeding System | Distribution belt hopper |
| Mold Lifting Mechanism | Double-sided sync gears |
| Automation Level | Automatic (PLC controlled, operable by one person) |
| Block Output Capacity | basis to be confirmed per block format and mix design |
| CE Declaration | Applicable per company documentation |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for load-bearing walls | Crushed stone, sand, cement, and fly ash blends |
| Solid block manufacturing for foundations | Dense aggregate with standard Portland cement |
| Paving block production for walkways and yards | Fine aggregate mix with surface pigmentation |
| On-site production for construction contractors | Locally sourced gravel and quarry dust |
| Expanding format range at existing plants | Compatible with standard concrete mix designs |
What "18-25 Seconds" Actually Means for Your Daily Tally
Cycle time only translates into daily output once you lock in the block format, wall thickness, and local aggregate grading.
I have seen buyers take a headline cycle number and multiply it by eight hours, only to find their real-world tally falling short because the figure was measured on a thin solid block while they were running 200mm hollow blocks. The QT4-18 molding cycle range exists because a lightweight garden paver fills and compresses faster than a deep-cavity hollow block that needs longer vibration to settle the mix around the core pins. When we quote capacity, we state which format the number belongs to. [NEED_CITE: ISO 13315 standards for concrete block cycle time measurement]
Matching Vibration Force to Your Local Aggregate
The platform vibration system on the QT4-18 delivers compaction energy through the pallet and into the mold cavity. If your local aggregate is angular volcanic rock rather than rounded river sand, the mix resists flow differently and needs either a longer vibration dwell or an adjusted frequency setting. This is the exact mismatch that once left a West African plant idle for a week while we recalibrated parameters remotely. Before we finalize the automatic block making machine specifications for your order, we ask for a sample of your coarse and fine aggregate so the vibration profile is set at the factory, not guessed on your first production morning.
Pallet Size and What It Decides Downstream
The 950×550mm pallet is not an arbitrary rectangle — it governs how many blocks fit per cycle, how the curing racks must be spaced, and whether your existing forklift can handle a loaded rack without a second trip. A pallet that is too large for your curing yard forces you to stack blocks higher than the bottom layer can bear while still green. A pallet that is too small wastes press capacity every cycle. We confirm your curing area dimensions and forklift rating before the pallet specification is locked. [NEED_CITE: concrete block curing and handling best practices]
Reading the Specs That Actually Move the Needle
The 16MPa rated hydraulic pressure works together with platform vibration to squeeze air voids out of the mix. Pressure alone on a stiff mix will produce a block that looks formed but crumbles at the corners; vibration alone on a wet mix yields a block that slumps before it reaches the curing rack. The QT4-18 pairs both forces so that density is consistent from the first block of the shift to the last. The distribution belt hopper feeds material across the full mold width, preventing the common problem of one side of the cavity receiving more aggregate than the other, which shows up as weight variation on the scale. Double-sided sync gears on the mold lifting mechanism keep the upper and lower mold halves aligned during the demolding stroke, reducing corner damage that would otherwise push your reject count higher. Schneider electrical components and a PLC with frequency converter mean the control cabinet can be serviced by any qualified electrician in your region without waiting for proprietary parts.
The Hidden Cost of Skipping the Format Conversation
Buyers who confirm price before they confirm block format often discover that the mold they receive produces a block their local builders do not specify. The press runs fine, but the product sits in the yard. Another frequent surprise is a pallet size that forces a complete re-layout of the curing area, adding weeks of construction before the first saleable block leaves the plant. Both issues are avoidable when the automatic block making machine specifications discussion starts with the block drawing, not the machine catalog. [NEED_CITE: common causes of block plant commissioning delays]
Why This Sourcing Path Reduces Mismatch Risk
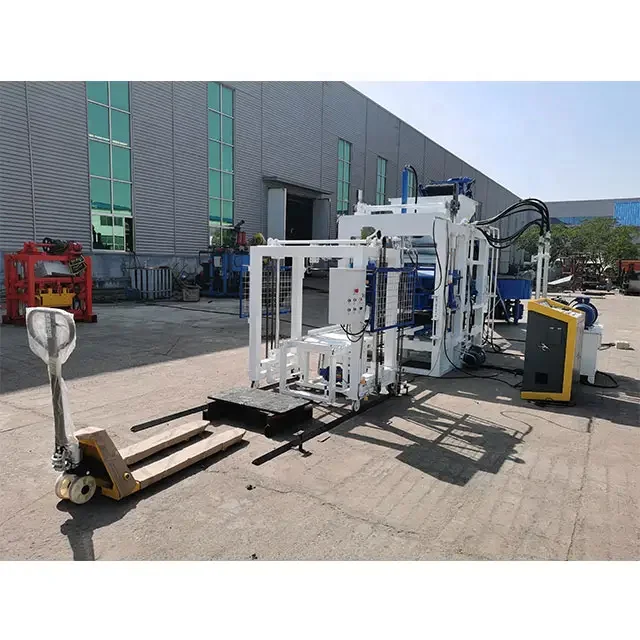
Block machinery is our single focus, so the press, mold, pallet, and handling equipment leave the factory as one matched set rather than a collection of separate purchases that must be made to cooperate on your floor. We configure the vibration and pressure settings against your actual mix sample, not a default profile. Molds are designed for the formats your market buys, and custom drawings are accepted when standard formats do not cover your specification. Automation level is selectable — the QT4-18 is PLC-controlled and can run with one operator, yet the line around it can start with manual pallet handling and add stacking later as volumes grow. Installation support and operator training are included so that your crew is not left reading a manual in a language they do not work in.
Documentation & Verification
- Line layout showing capacity calculation per block format assumed
- Mold drawing and format list confirming each block type the machine produces
- Pallet specification matched to your curing rack spacing and forklift rating
- Factory test record with actual cycle time on your target block format
- Voltage, frequency, and PLC display language confirmation before dispatch
Installation, Commissioning & Support
- Foundation pad must carry the 2500×1750mm footprint with anchor bolt inserts aligned to machine base holes
- Dedicated three-phase circuit sized for the 27.5kW total load plus starting surge
- Machine ships as a single press unit; mold and pallets packed separately for container loading
- First-run parameter tuning performed on your local aggregate sample at the factory when provided in advance
- Operator training covers PLC navigation, mold change procedure, and daily vibration plate inspection
- Wear parts list identifies mold liners, vibration springs, and hydraulic seals with reorder part numbers
What to Send Before You Request a Quote
To size the line correctly, share the block format drawings or photographs of the blocks your market currently buys, along with the target daily output you need to meet existing orders. Tell us your coarse and fine aggregate type and whether you can provide a sample. Confirm the local voltage and frequency, the language your operators read, and the dimensions of the curing area you plan to build or already have. If you have a forklift on site, send its load rating so the pallet and rack system can be matched from day one.
Frequently Asked Questions
Q: How do I verify daily output for my specific block format?
A: We run a factory test using your target block mold and, when possible, a sample of your local aggregate. The test record states the actual cycle time and the blocks produced per shift under those exact conditions, so the number you plan around is tied to your product, not a generic catalogue entry.
Q: What mold formats fit the QT4-18 and how fast can I switch?
A: The press accepts molds for hollow blocks, solid blocks, and paving blocks within the 950×550mm pallet envelope. Mold change involves releasing the sync gear clamps and lifting the mold set with an overhead hoist. We provide a format list and change procedure in the operation manual so your crew can plan changeovers around production breaks.
Q: How does pallet size affect my curing area layout?
A: The 950×550mm pallet determines rack slot width, forklift aisle spacing, and how many blocks cure per square meter. We draft a curing yard layout based on your available floor area and confirm that your existing forklift can handle a fully loaded rack before the pallet order is finalized.
Q: Which mix design works best with this vibration and pressure setup?
A: Platform vibration at the QT4-18 frequency range performs well with zero-slump mixes using angular aggregate up to 10mm grading. We ask for a sample of your coarse and fine material so we can adjust vibration duration and pressure hold time at the factory, rather than leaving the tuning to your first week of production.