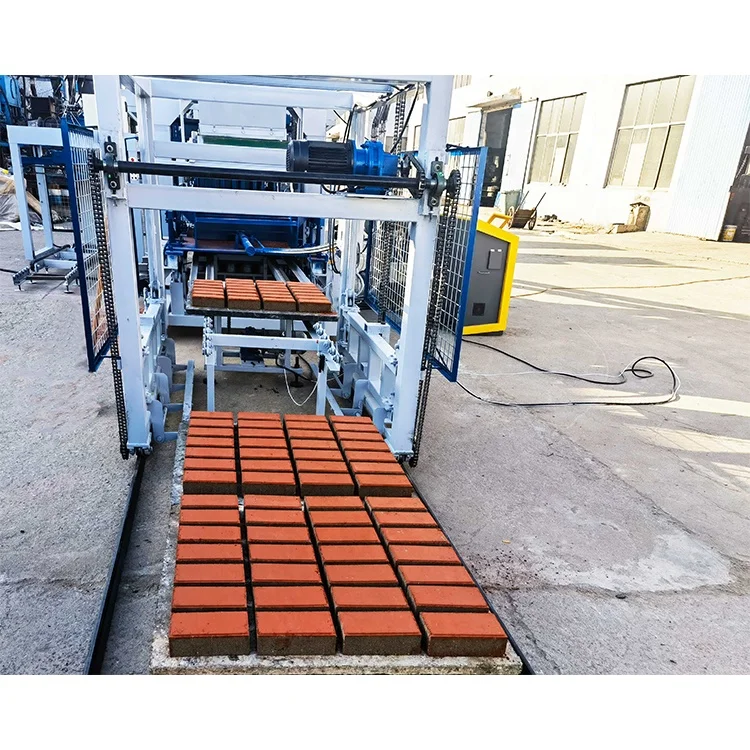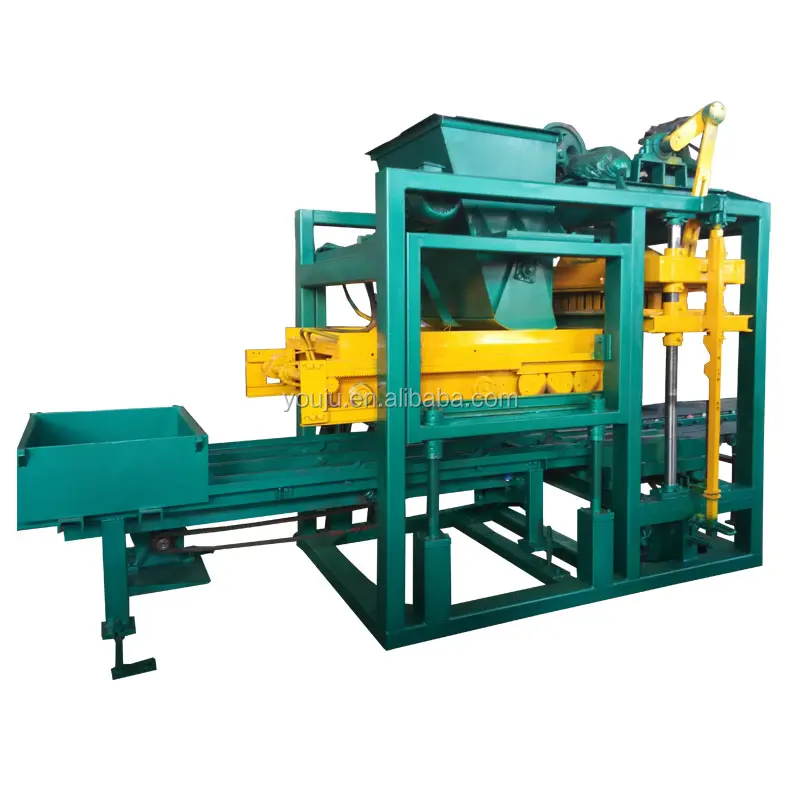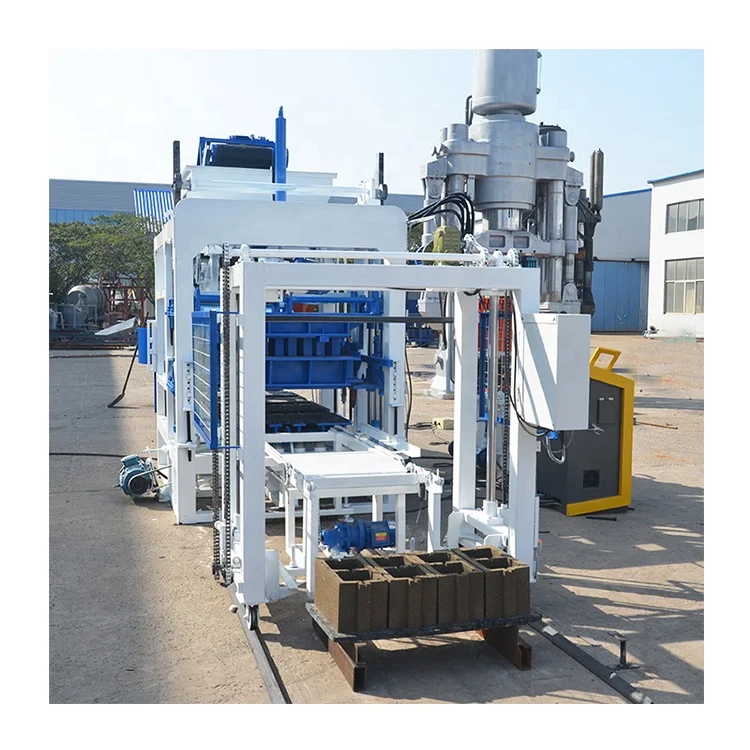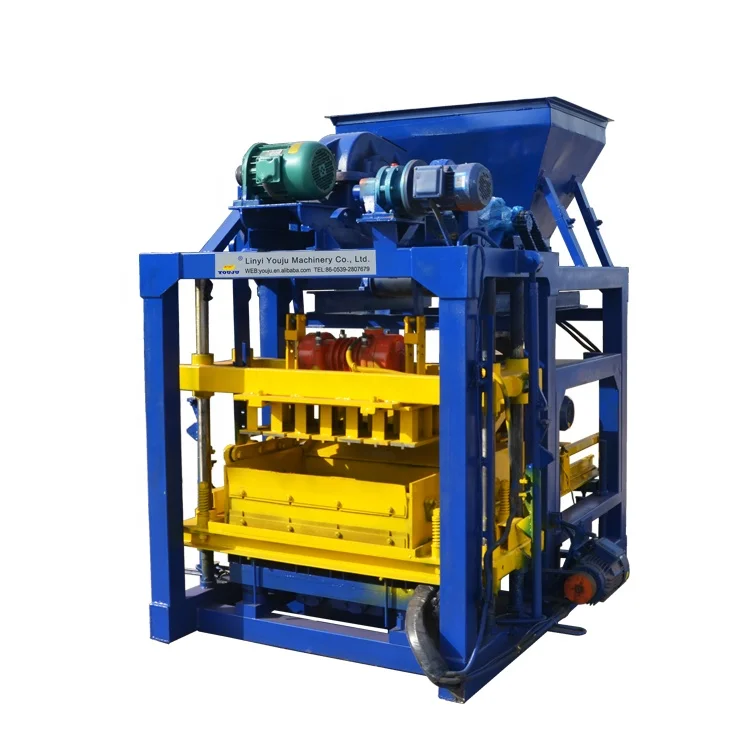
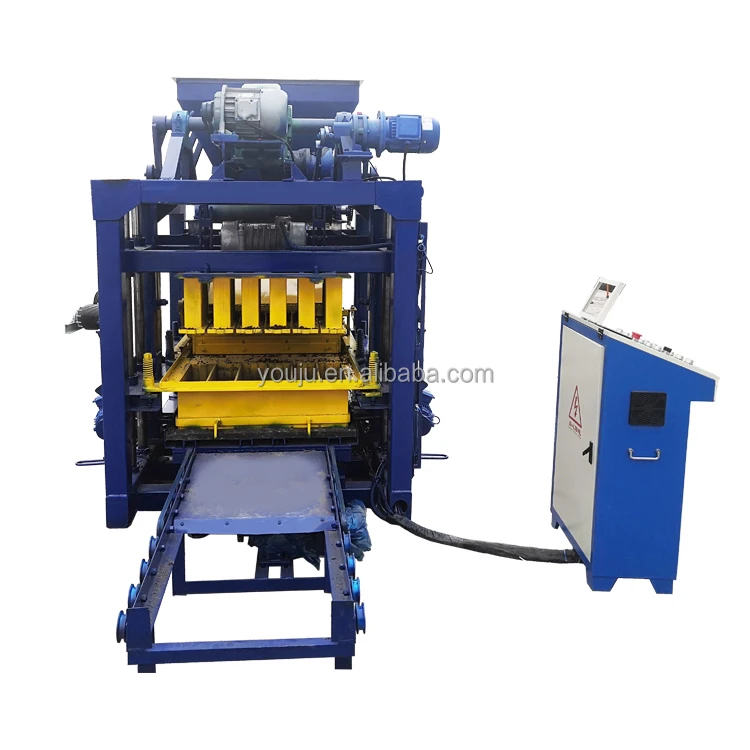
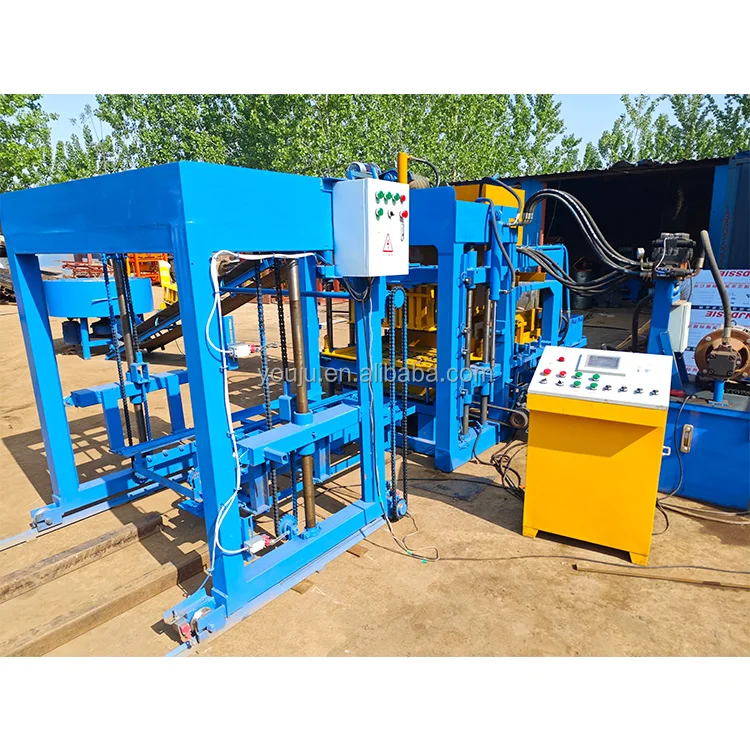
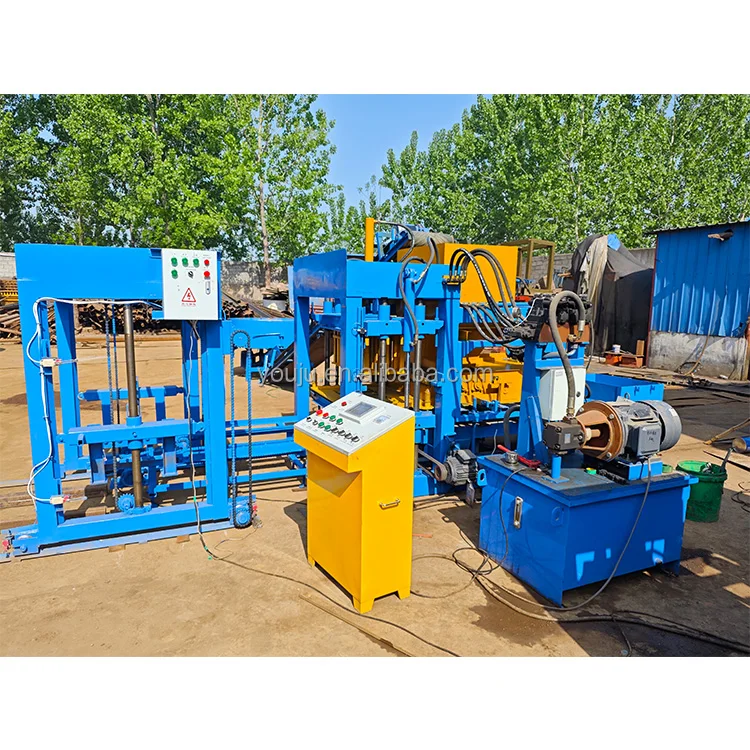
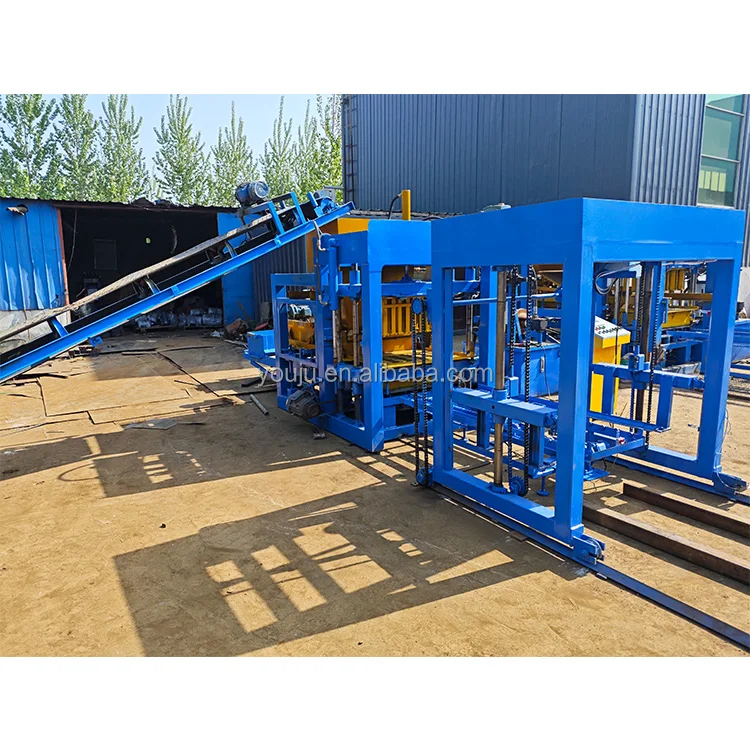
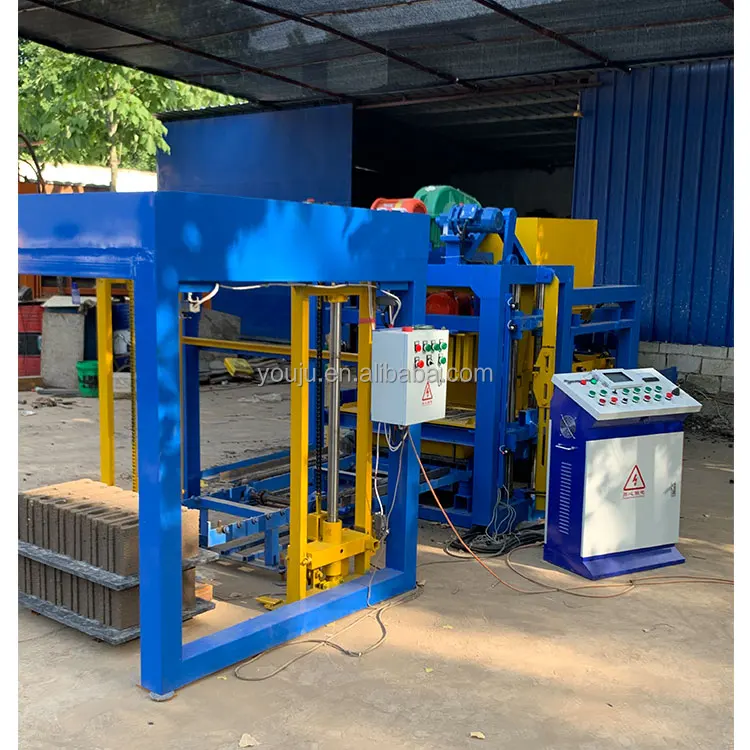
Description
Matched system configuration — machine, mould, pallet and handling are specified together against your local aggregate and target block format, not pulled from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
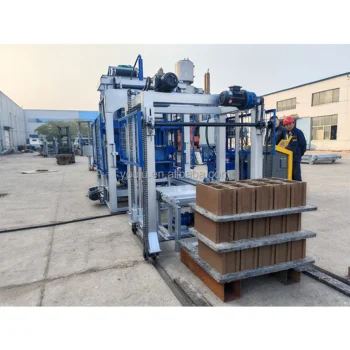
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Rated Power | 17.9 kW |
| Overall Dimensions (L×W×H) | 6400×1500×2700 mm |
| Total Mass | 2500 kg |
| Molding Cycle | 25 s |
| Vibration Frequency | 2800 r/min |
| Exciting Force | 60 kN |
| Pallet Size | 850×550×20 mm |
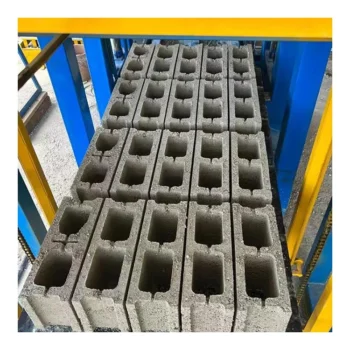
| Output Capacity | 960 pcs/h, 7680 pcs/day (based on 400×200×200 mm hollow block, 4 pcs/mould) |
| Mould Format Capability | Hollow, solid, paver, curbstone (mould change required) |
| Automation Level | Semi-automatic |
| Configuration Included | Host machine 1 set, block mould 1 set, JQ350 mixer |
| Hydraulic System | Equipped (high pressure, stable operation) |
| Voltage & Frequency | To be confirmed before shipment (basis not stated in source) |
| Control System | To be confirmed — PLC or relay logic (basis not stated in source) |
| Certification | To be confirmed (basis not stated in source) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, water mix with local aggregate |
| Solid block manufacturing for load-bearing structures | Dense aggregate blend with cement binder |
| Paving block production for walkways and yards | Fine aggregate with pigment for coloured surfaces |
| Curbstone forming for road and pathway edges | Coarse aggregate mix with high cement ratio |
| Small to medium block plant operations | Daily volumes around 7680 hollow blocks per 8-hour shift |
What "7680 Pieces per Day" Actually Means for the QTJ4-25 Block Making Machine Specifications
The figure only holds when you are running 400×200×200 mm hollow blocks at a 25-second cycle with four cavities per mould.
Capacity numbers on block machinery quotations frequently omit the format behind them. A buyer sees a large daily figure and assumes it applies to whatever block the local market demands. In practice, switching to a solid block or a smaller paver changes the cavity count, the moulding cycle, and the curing weight — and the real output shifts accordingly. I have seen plants arrive at commissioning only to discover their primary product runs at a fraction of the quoted number because the assumption was never disclosed [NEED_CITE: block machine capacity calculation standards by format].
Mould Format and Cycle Time Alignment
The QTJ4-25 block making machine specifications list hollow, solid, paver and curbstone as mould-compatible formats, but each format carries a different cavity count and compaction requirement. The 25-second cycle applies to the standard 400×200×200 mm hollow block at four pieces per mould. Smaller formats such as interlocking pavers may pack more cavities per mould yet need longer vibration to achieve the density the market expects. Confirming cycle time per format before purchase prevents planning a production schedule around a number the machine cannot sustain on your actual product.
Pallet Size and Curing Area Matching
The 850×550×20 mm pallet dimension dictates how many wet blocks travel to the curing area in one press cycle and how they stack on your existing racks. If your curing yard uses a forklift with a different fork width, or your rack spacing was built for another pallet size, the mismatch surfaces on the first day of production. This is why the QTJ4-25 block making machine specifications must be read alongside your curing layout and handling equipment, not in isolation [NEED_CITE: pallet handling compatibility in block production lines].
Vibration Force and Block Density Consistency
The 60 kN exciting force at 2800 r/min works in combination with hydraulic pressure to compact the mix into a dense, consistent block. Vertical vibration from the bed mould and compression vibration from the upper mould together determine whether the block meets the strength grade your local building code requires. When the vibration force is not matched to the buyer’s specific aggregate gradation and cement ratio, blocks can emerge with uneven density — strong on one side and friable on the other — leading to rejection at the construction site.
The Hidden Cost of Unconfirmed Voltage and Control Language
A machine built for a voltage or frequency that differs from the local grid will either underperform or fail to start, and correcting it after arrival means rewinding motors and replacing control components. The same applies to PLC display language: if the operator cannot read the interface, every parameter adjustment becomes guesswork. I once worked with a buyer whose semi-automatic line sat idle for weeks because the control panel arrived in a language none of the floor staff could read, and the PLC supplier needed a new programme chip shipped overseas [NEED_CITE: voltage and frequency standards by export market]. Confirming these details before production begins — not after the container is loaded — avoids delays that no amount of on-site effort can recover.
Why Buyers Choose This Configuration Path
Every QTJ4-25 proposal begins with the buyer’s actual block format, local aggregate sample and target daily volume, so the capacity calculation states the format assumed rather than leaving it to interpretation. Mould design covers the formats the buyer’s market actually sells, including custom drawings when a standard catalogue mould does not fit. The semi-automatic automation level allows a first-time plant owner to start with manageable complexity and add automatic pallet feeding or stacking later as volume grows. Installation support includes operator training on the specific mould set and mix design the buyer will use, not a generic demonstration. Pallet material and quantity recommendations account for the buyer’s curing area size and expected rotation cycle, preventing a shortage that would bottleneck output in the first month.
Documentation & Verification
- Line layout showing capacity per block format with mould cavity count stated
- Mould drawing and format list confirming cycle time for each product type
- Pallet specification sheet matched to curing rack dimensions and forklift capacity
- Hydraulic and electrical schematic with voltage and frequency confirmed for destination
- Factory test record run on buyer’s specified block format before dispatch
- Operation and maintenance manual in agreed control language
Installation, Commissioning & Support
- Foundation plan sized to 6400×1500 mm footprint with anchor bolt positions
- Dedicated 17.9 kW circuit with confirmed voltage and frequency for the destination grid
- Machine arrives as host unit with JQ350 mixer; on-site assembly covers pallet feeder alignment
- First-run commissioning tests 25-second cycle on buyer’s chosen hollow block format
- Operator training covers mould change procedure and vibration frequency adjustment
- Wear parts list includes vibration springs and hydraulic seals with reorder quantities
What to Share Before Requesting a Quotation
Provide the exact block dimensions and formats your market sells, along with a sample or description of the aggregate available locally. Confirm the daily volume you need and the shift pattern you plan to run. State your site voltage, frequency and preferred control panel language so the QTJ4-25 configuration is locked before production starts.
Frequently Asked Questions
Q: How is daily output calculated, and which block format is assumed?
A: The 7680 pieces per day figure is based on running 400×200×200 mm hollow blocks at four pieces per mould with a 25-second cycle across an 8-hour shift. If your primary product is a different format, the cavity count and cycle time change, and the daily output must be recalculated for that specific block before you commit to a production target.
Q: What mould formats are available, and what is the cycle time for each?
A: The QTJ4-25 supports hollow, solid, paver and curbstone moulds. The 25-second cycle applies to the standard hollow block format. Other formats require separate cycle time confirmation because cavity count, compaction pressure and vibration duration vary with block geometry and the density your local standard demands.
Q: How do I confirm voltage, frequency, and control system language for my market?
A: These parameters are not preset at quotation stage and must be confirmed before production begins. Provide your local grid specification and preferred operator language during the inquiry so the motor winding, control components and PLC display are configured correctly before the machine leaves the factory.
Q: What pallet material and quantity are recommended for my production volume?
A: Pallet material — typically bamboo, steel or PVC — is selected based on your curing environment humidity and expected rotation cycle. The 850×550×20 mm size must match your curing rack spacing and forklift fork width. Quantity is calculated from daily output and the number of days blocks remain on pallets before dispatch.