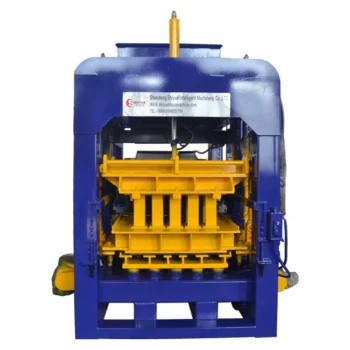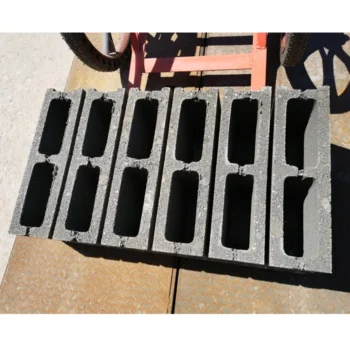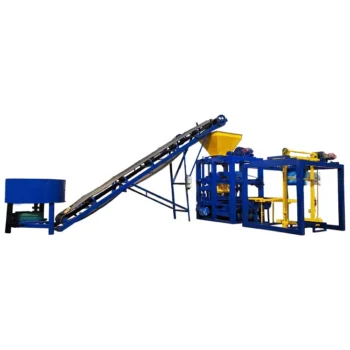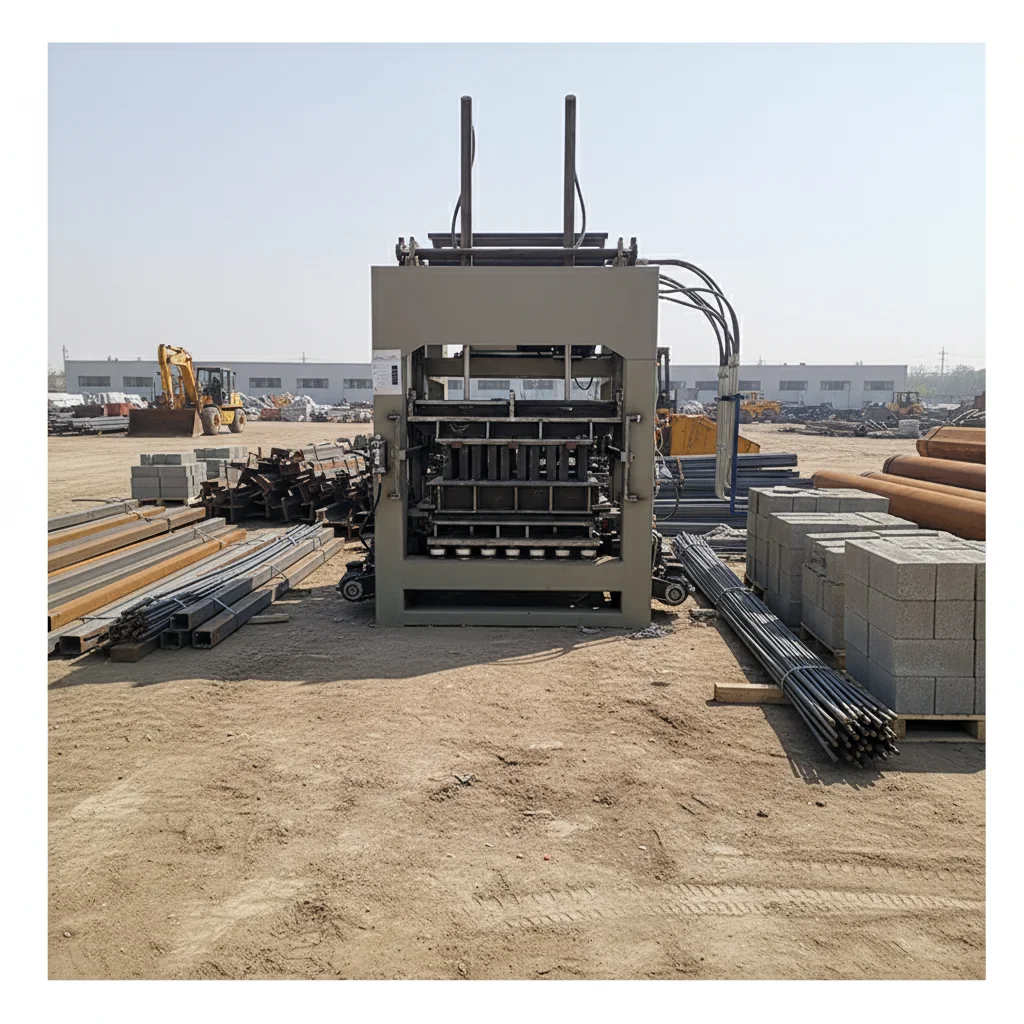
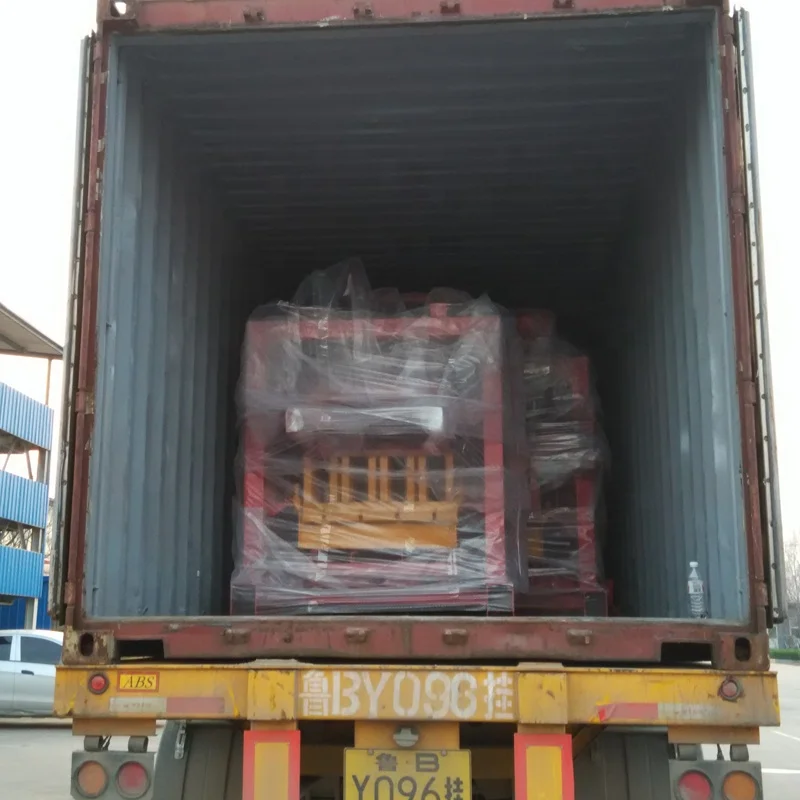
Description
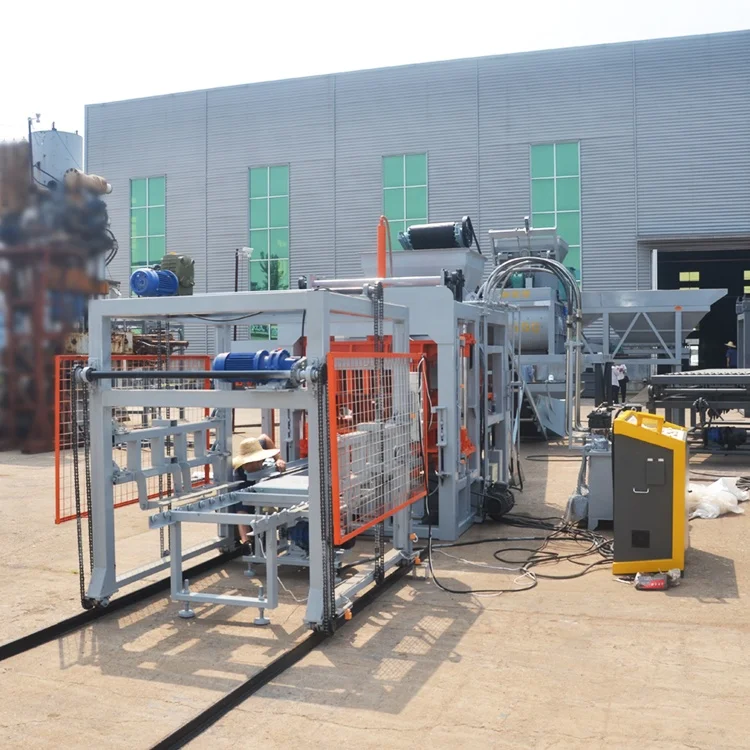
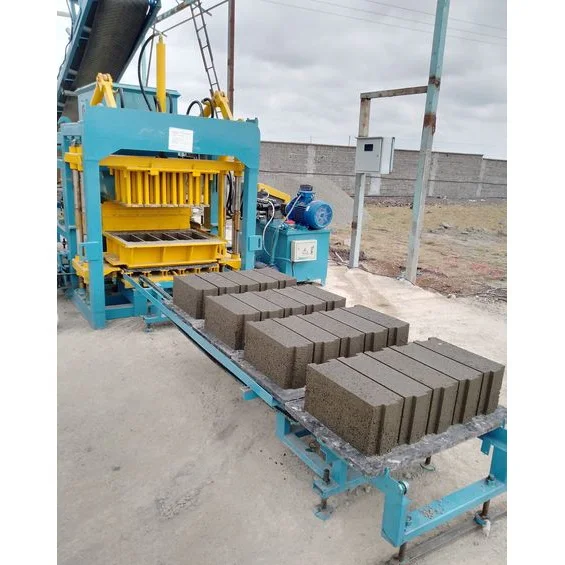
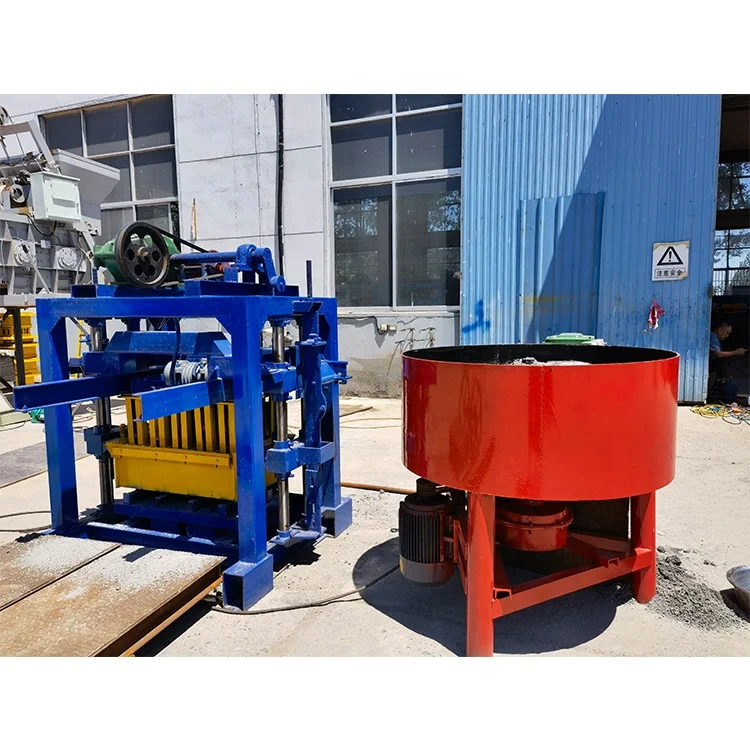
Matched system specification — the QTJ4-40 block machine, mould, pallet and cycle time are quoted as one verified set so daily output reflects the format your market actually buys.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-40 |
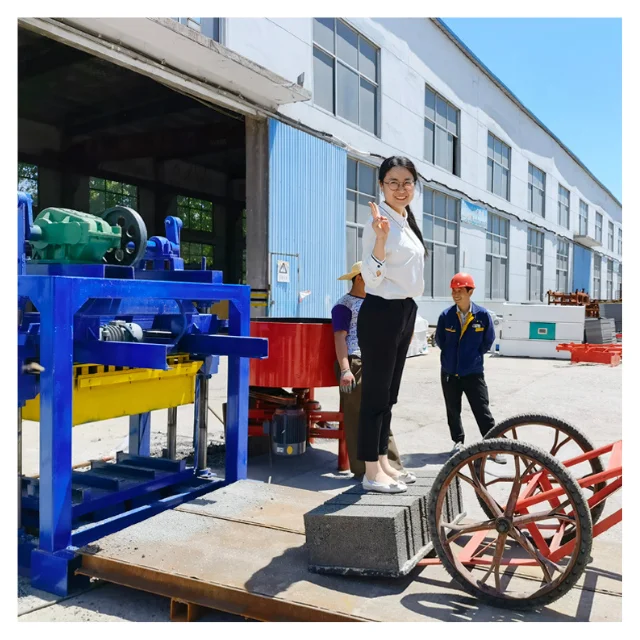
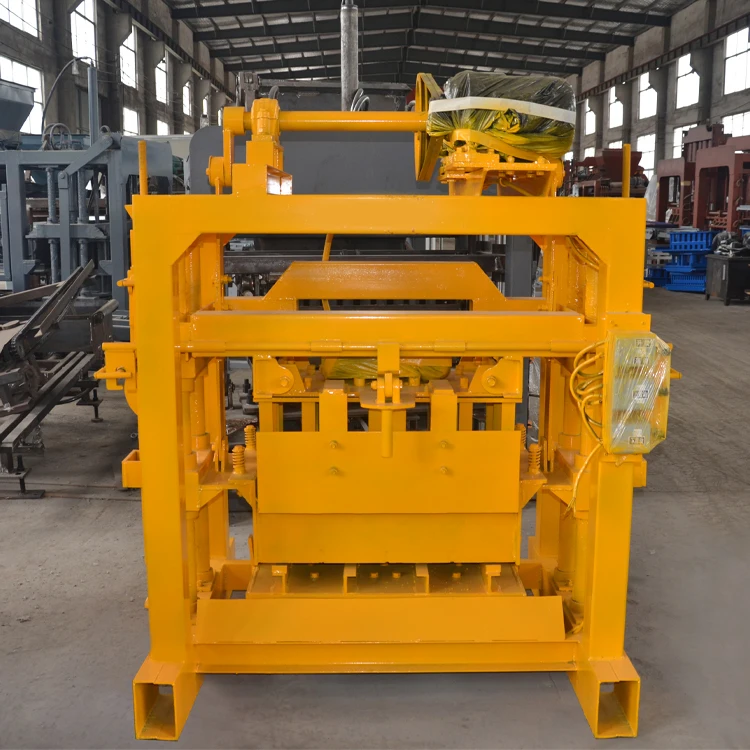
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Rated Power | 9.5 kW |
| Molding Cycle | 40 s |
| Theoretical Productivity (400×200×200 mm hollow block, 4 pcs/mould) | 360 pcs/h, 2800 pcs/day |
| Theoretical Productivity (400×150×200 mm hollow block, 5 pcs/mould) | 450 pcs/h, 3600 pcs/day |
| Theoretical Productivity (225×112.5×60 mm solid brick, 9 pcs/mould) | 800 pcs/h, 6400 pcs/day |
| Output Capacity | 2000–2500 pcs / 8 hours (basis not stated in source — confirm block format) |
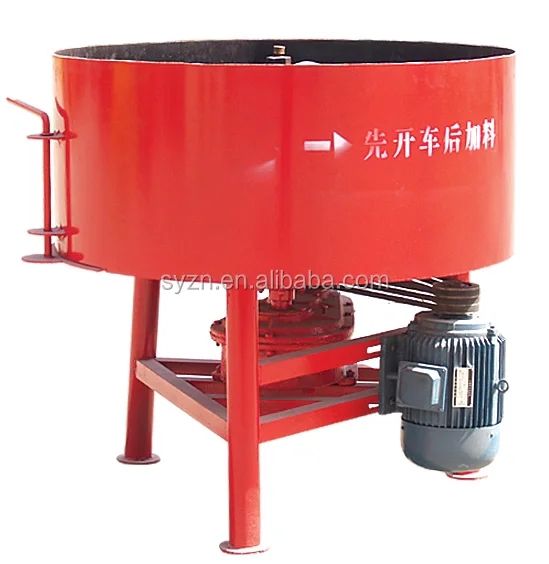
| Raw Materials | Concrete, sand, cement, fly ash, lime, gypsum |
| Vibration System | Bed mould vertical vibration + upper mould compression vibration |
| Automation Level | Semi-automatic (top die push-pull, automatic scraper, manual pallet handling) |
| Pallet Size | 850 × 450 mm |
| Net Weight | 1 T |
| Overall Dimensions (L×W×H) | 1350 × 1460 × 1800 mm |
| Voltage | Configurable to local supply (confirm exact V/Hz before order) |
| Stacking Method | Manual |
| Control System | Not stated in source |
| Certification | Not stated in source |
Application Suitability
| Application | Material or Output |
|---|---|
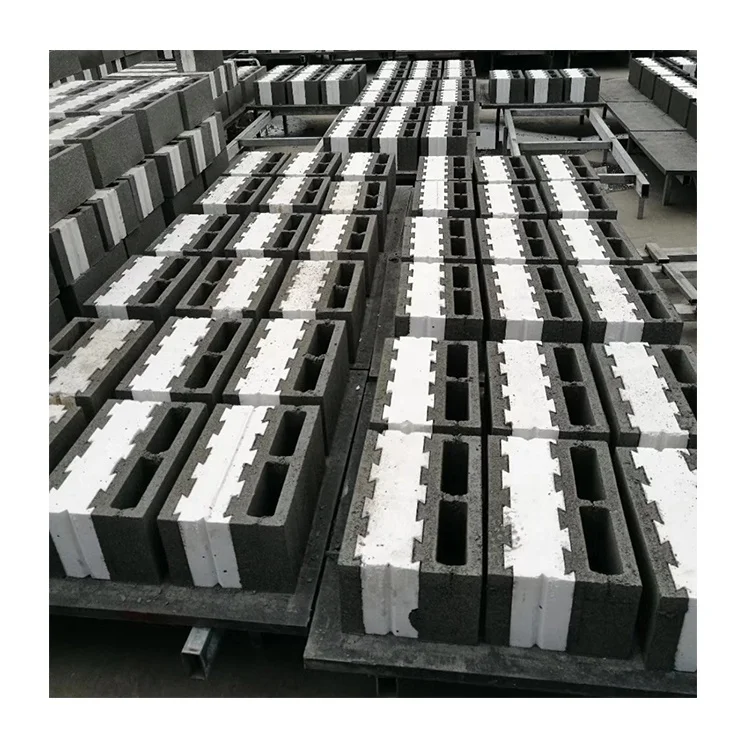
| Small-scale hollow block production | Crushed stone, sand, cement mix for 400×200×200 mm and 400×150×200 mm formats |
| Solid brick manufacturing for local supply | Sand, fly ash, cement blend for 225×112.5×60 mm bricks |
| On-site block production for housing projects | Concrete and locally sourced aggregate, semi-mobile setup |
| First block plant for entrepreneurs | Low-investment entry with room to add automation stages later |
What "2500 Blocks Per Day" Actually Means for the QTJ4-40 Block Machine Specifications
Output only holds true when the block format, mould cavity count and cycle time are stated together.
I once watched a small plant in West Africa celebrate a quoted capacity figure, then spend weeks wondering why daily production never reached it. The problem was not the QTJ4-40 block machine — it was that the quoted number assumed a solid brick format with nine cavities per mould, while the buyer’s market demanded hollow blocks with only four cavities. Once we recalculated based on the actual format and adjusted the vibration timing for the local aggregate, the numbers made sense and the operator stopped chasing an impossible target [NEED_CITE: common causes of capacity shortfalls in small block plants].
Mould Format Defines Your Real Daily Output
The QTJ4-40 block machine specifications list three distinct productivity figures because each block format uses a different mould cavity count. A 400×200×200 mm hollow block fills four positions per cycle, yielding 360 pieces per hour at a 40-second cycle. Switch to the 225×112.5×60 mm solid brick mould with nine cavities, and the same cycle produces 800 pieces per hour. The press does not change — only the mould and the math change. Any supplier quoting a single output number without naming the format is leaving the most important variable out of the conversation.
Pallet Size Must Match Your Curing Area Before the Machine Ships
The 850 × 450 mm pallet is not an arbitrary choice — it governs how many blocks fit per cycle and how your curing racks must be laid out. If your existing forklift tines are spaced for a different pallet dimension, or your curing yard was built around another supplier’s pallet standard, every loaded pallet becomes a handling problem from day one. I have seen plants where the block machine ran fine but the pallets could not stack on the curing racks, forcing workers to rebalance loads by hand [NEED_CITE: pallet and curing rack compatibility in block production]. Confirm pallet dimensions against your site before the QTJ4-40 block machine enters production.
Vibration Force and Local Aggregate Determine Block Strength
The dual vibration system — vertical vibration from the bed mould combined with compression vibration from the upper mould — is designed to compact concrete evenly across the mould cavity. But vibration settings that work for clean river sand may fail with high-clay stone dust. On one site, blocks crumbled at the edges because the local aggregate contained too much fines material, and the default vibration duration could not achieve full compaction. We adjusted the vibration timing and pressing duration to match that specific mix, and block strength stabilised. The QTJ4-40 block machine specifications must therefore be read alongside your actual raw material profile, not treated as a standalone guarantee.
The Cost of Skipping Configuration Checks Before Shipment
When voltage and frequency are not confirmed before production, the machine arrives and the motor will not start — or worse, it starts and burns out within hours. When the control display language is not specified, the operator cannot read fault codes and calls for help on every minor alarm. These are not rare events; they are the most frequent reasons commissioning stalls after delivery [NEED_CITE: electrical commissioning delays in exported machinery]. A few minutes spent confirming local power standards and operator language before the QTJ4-40 ships saves weeks of idle time on site.
Why Buyers Specify This Machine as a System
Block machinery is the single focus here, so the QTJ4-40 is not sold as a bare press — mould, pallet and handling requirements are specified together against your target format. Configuration is set against your actual mix design and local aggregate rather than a catalogue default, which means vibration and pressing parameters are adjusted before the machine leaves the factory. Mould design covers the formats your market actually sells, with custom drawings available when standard sizes do not match. The semi-automatic layout lets you start with manual pallet handling and add automatic stacking later as volume grows, so the investment scales with your plant rather than forcing a full automatic line from the start.
Documentation & Verification
- Capacity calculation sheet stating block format and cavity count for each output figure
- Pallet specification confirming 850 × 450 mm dimensions and material grade
- Voltage, frequency and control language confirmation signed before production begins
- Mould drawing and format list for every included block size
- Factory test record run on your specified block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement schedule
Installation, Commissioning & Support
- Foundation pad sized to the 1350 × 1460 mm footprint with level tolerance for vibration stability
- Dedicated electrical circuit matching confirmed voltage and the 9.5 kW rated power draw
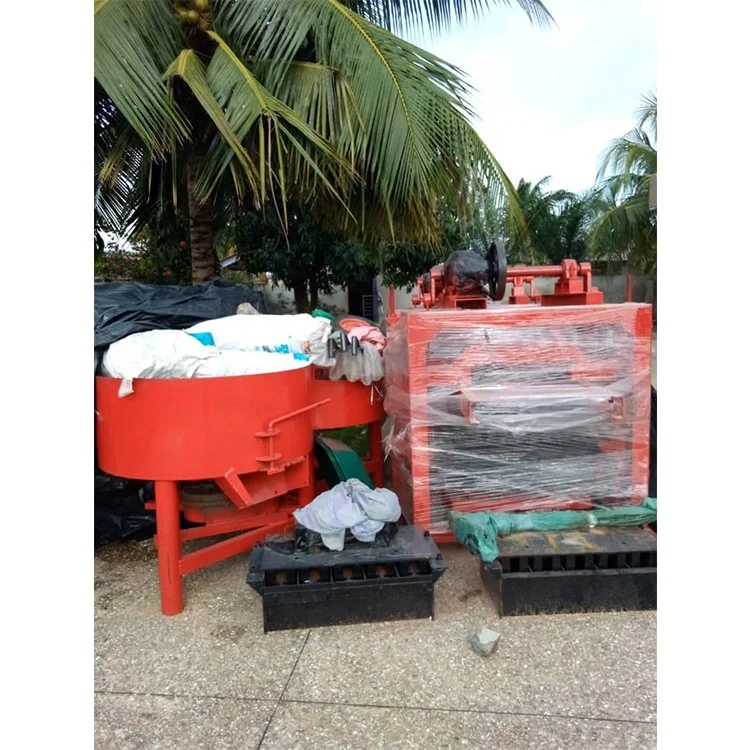
- Machine shipped as a single unit at 1 T net weight, positioned by forklift on arrival
- First-run commissioning includes vibration timing adjustment to your local aggregate mix
- Operator training covers mould change procedure, pallet loading rhythm and daily maintenance checks
- Wear parts list provided with recommended replacement intervals for vibration components and scraper
What to Include in Your Inquiry
Tell us which block format your market sells most — hollow block, solid brick or paver — along with the dimensions, so we can match the mould and calculate output honestly. Share your local aggregate type and any available sieve analysis, because vibration settings depend on the material, not just the machine. Confirm your site voltage, frequency and the language your operators read, so the QTJ4-40 block machine arrives ready to run instead of waiting for electrical modifications.
Frequently Asked Questions
Q: How is the QTJ4-40 capacity calculated and which block format does each figure assume?
A: Each output figure is tied to a specific mould cavity count and block dimension. The 360 pcs/h figure assumes the 400×200×200 mm hollow block with four cavities, while the 800 pcs/h figure assumes the 225×112.5×60 mm solid brick with nine cavities. Always ask which format a quoted capacity refers to before comparing machines.
Q: What pallet size does this machine use and how does it affect my curing area layout?
A: The QTJ4-40 uses an 850 × 450 mm pallet. Your curing racks, forklift tine spacing and yard layout must accommodate this dimension. Mismatched pallets cause handling bottlenecks that have nothing to do with the press itself, so verify compatibility before the machine ships.
Q: How do I match the vibration force and mix design to my local aggregate for consistent block strength?
A: The dual vibration system compacts concrete from both bed and upper mould, but timing must suit your specific aggregate. High-fines materials like stone dust may need longer vibration than clean sand. Provide a sample or sieve analysis so settings can be adjusted before factory testing.
Q: What voltage and frequency options are available and is the control display in my language?
A: Voltage is configured to your local supply standard — confirm exact V and Hz before production. Control display language must also be specified at order stage so operators can read settings and fault codes from the first day of commissioning.
Q: Can I upgrade the QTJ4-40 from semi-automatic to a higher automation level later?
A: Yes. The semi-automatic configuration handles pallet feeding and stacking manually, but the system supports adding automatic pallet feeding and stacking stages as your volume grows. This lets you start with lower investment and expand without replacing the press.