

Description
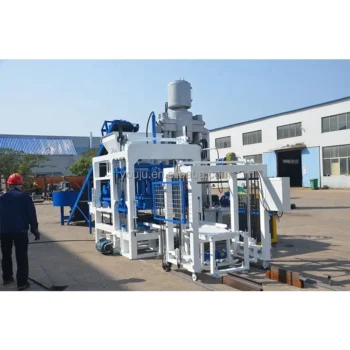
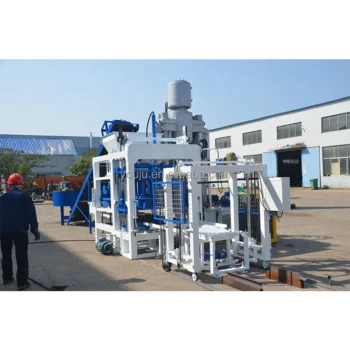
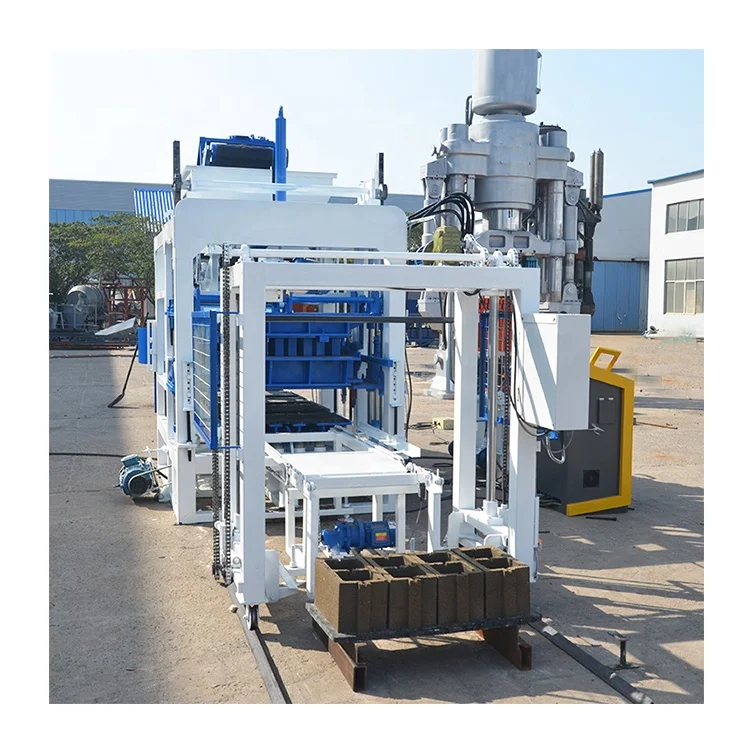
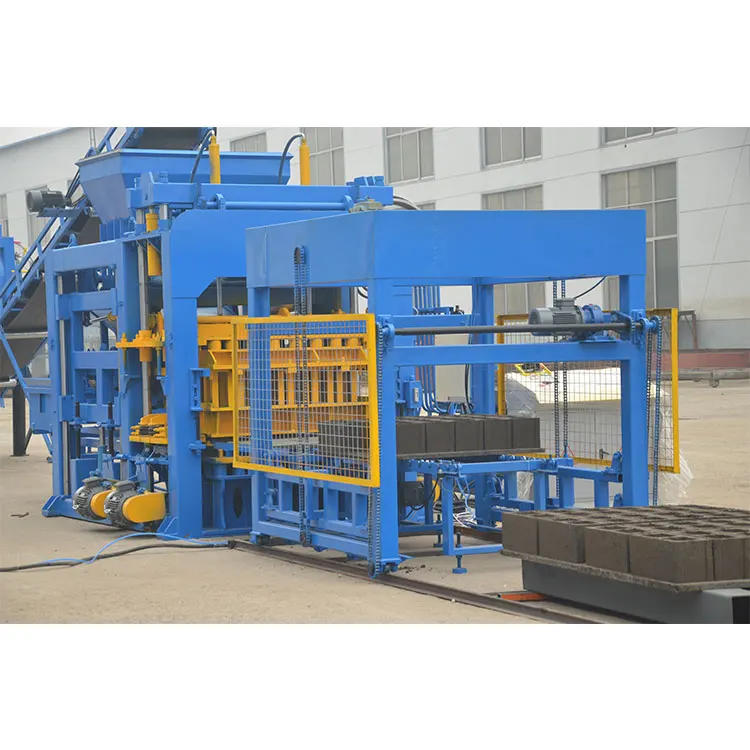
Matched System Sizing — the QT12-15 block machine, mould and pallet are specified together against your actual block format, local aggregate and curing layout, not pulled from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT12-15 |
| Product Type | Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 9350 x 2520 x 2950 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800-4500 r/min |
| Vibration Acceleration | 15-20 g |
| Exciting Force | 120 kN |
| Brick Height Range | 50-200 mm |
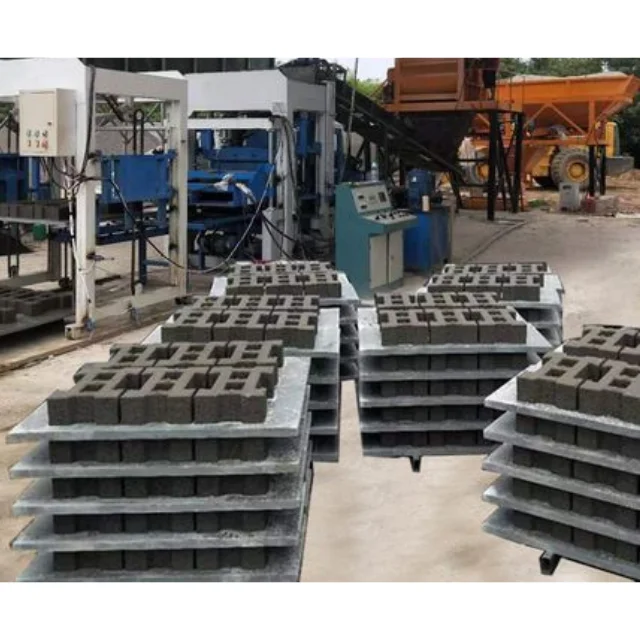
| Pallet Size | 1350 x 850 mm |
| Molding Cycle | 15-25 s |
| Storage Hopper Volume | 0.4 m³ |
| Feeding Device Volume | 0.31 m³ |
| Total Power | 50.7 kW |
| Total Weight | 12000 kg |
| Control System | PLC controlled (mechanical-hydraulic synthesis) |
| Frame Structure | Gantry frame type, super steel, shock resistant |
| Feeding System | Net wave swing type material feeding device |
| Mould Material | Manganese steel, carburizing and quenching (cartridge type welding) |
| Automation Level | Automatic |
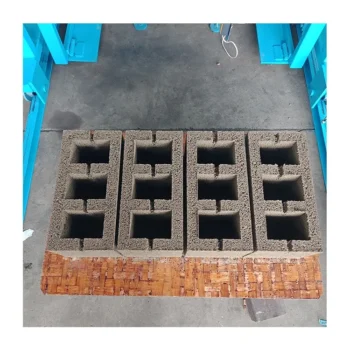
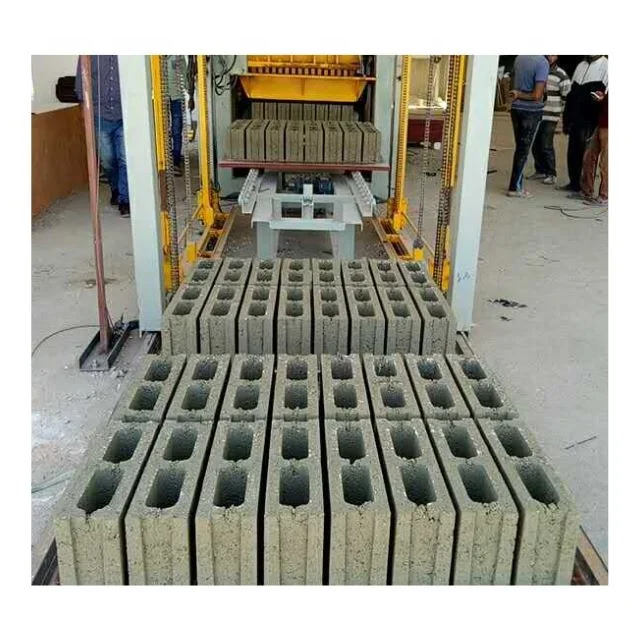
| Output — Hollow Block 390×190×190 mm | 12 pcs/mould, 1720-2160 pcs/h, 13700-17200 pcs/day (8h), based on 20-25 s molding cycle |
| Output — Porous Block 240×115×90 mm | 35 pcs/mould, 5040-6300 pcs/h, 40300-50400 pcs/day (8h), based on 20-25 s molding cycle |
| Output — Standard Block 240×115×53 mm | 62 pcs/mould, 13100-14800 pcs/h, 105000-119000 pcs/day (8h), based on 15-17 s molding cycle |
| Voltage & Frequency | To be confirmed against buyer’s site supply |
| PLC Display Language | To be confirmed before production |
| Mould Change Time | To be confirmed per mould configuration |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement and fly ash mixes on 1350×850 mm pallets |
| Porous block manufacturing for partition and insulation | Lightweight aggregate blends with controlled moisture content |
| Standard solid brick for load-bearing masonry | Dense sand-cement mixes compacted at 21 MPa rated pressure |
| Interlocking paver and paving block | High-strength surface mixes requiring platform vibration at 15-20 g acceleration |
| On-site production for housing and development projects | Local laterite, volcanic ash or river sand blends matched to vibration settings |
Why the Same Automatic Block Machine Shows Three Different Outputs
Every capacity figure is tied to a named block format and mould count, not a single blanket number.
Buyers often receive a quote stating cycles per hour without any mention of which block size that figure assumes. When the machine arrives and the first production run begins on hollow blocks instead of standard bricks, the daily output can fall to less than half of what was expected. The QT12-15 runs a 15-17 second molding cycle for standard 240×115×53 mm solid blocks but needs 20-25 seconds for hollow and porous formats, and that cycle difference reshapes the entire production schedule [NEED_CITE: block format assumptions in capacity quotations]. Honest capacity reporting means stating the block dimensions, pieces per mould, and cycle time behind every output claim so the buyer can plan labour, curing space and delivery timelines against real numbers.
Pallet Size Determines Which Formats Actually Fit Per Cycle
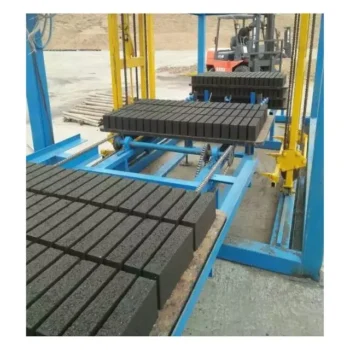
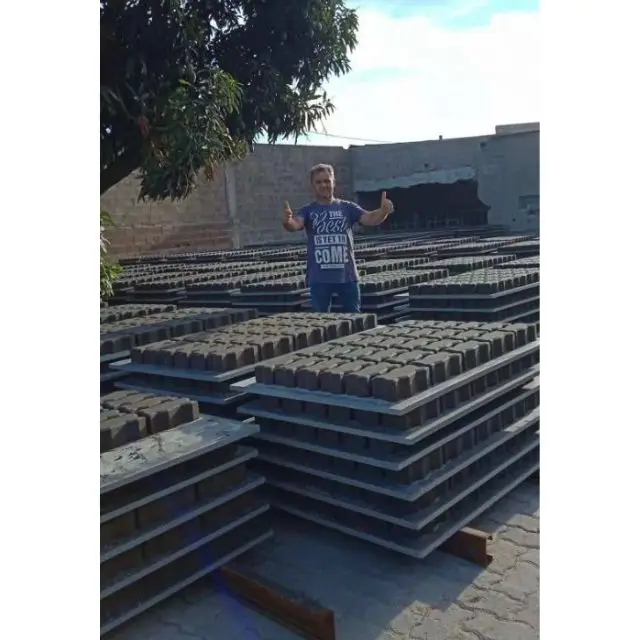
The 1350 × 850 mm pallet on the QT12-15 sets the physical limit for how many blocks of a given format can be pressed in one cycle. A standard 240×115×53 mm brick fits 62 pieces per mould on this pallet, while a 390×190×190 mm hollow block fits only 12. Before confirming the automatic block machine specifications, the buyer must verify that this pallet dimension aligns with existing curing racks, kiln cars and forklift fork widths so that freshly pressed blocks can move straight to curing without rehandling.
Mould Selection Must Follow the Formats Your Market Actually Buys
The QT12-15 accepts cartridge-welded manganese steel moulds treated by carburizing and quenching, and custom mould designs can be built from buyer drawings. A block plant adding interlocking pavers to a hollow block range needs to confirm that the mould format list includes the specific interlock pattern sold locally, and that the mould change procedure fits within a single shift. Choosing moulds based on a factory default list rather than local market demand leads to inventory that does not move and formats that sit unused on the rack [NEED_CITE: mould selection against local block market demand].
How Vibration Force and Hydraulic Pressure Shape Block Strength
The platform vibration system delivers 120 kN exciting force at 15-20 g acceleration, working together with 21 MPa rated hydraulic pressure to compact the mix into a dense, uniform block. When the buyer’s local aggregate differs from the sand-cement blend used in factory testing — for instance laterite with volcanic ash instead of river sand — the vibration frequency and pressure settings must be reworked to match that specific mix design. Without this adjustment, blocks emerge with soft edges and inconsistent compressive strength, and the entire production line sits idle while parameters are recalibrated from scratch.
What Happens When the Wrong Configuration Ships
Sending a machine configured for a mix the buyer cannot source locally forces a costly material change or a production halt on arrival. If the pallet size does not match the curing area, blocks pile up on the factory floor and cure unevenly, weakening the final product. Voltage and frequency left unconfirmed delay commissioning for weeks while transformers or motor replacements are shipped overseas, and the project timeline absorbs every day of that delay [NEED_CITE: commissioning delays from unconfirmed electrical specifications]. These are the hidden costs that never appear on the quotation sheet but show up clearly once the container is opened on site.
Why Sizing Starts With a Raw Material Sample
Block machinery is our single focus, which means the QT12-15 is configured as one matched system — press, mould, pallet and handling — rather than assembled from separate suppliers. Every configuration is set against the buyer’s actual mix design, local aggregate and target block format, not a catalogue default. Mould design and supply cover the formats the buyer’s market sells, including custom drawings for non-standard interlock or kerbstone profiles. The automation level is selectable, so a buyer can begin with semi-automatic pallet handling and add automatic stacking later. Installation support includes on-site commissioning and operator training so the crew can run every format confidently from the first week.
Documentation & Verification
- Line layout and capacity calculation stating the block format behind every output figure
- Mould drawing and format list confirming included profiles and custom design options
- Pallet specification sheet matched to buyer’s curing rack dimensions and forklift capacity
- Hydraulic and electrical schematic with confirmed voltage, frequency and PLC language
- Factory test record run on buyer’s specified block format before dispatch
Installation, Commissioning & Support
- Foundation plan accounting for the 9350×2520 mm footprint and 12000 kg operating weight
- Dedicated power circuit sized for 50.7 kW total draw with confirmed voltage and frequency
- Platform vibration calibration against buyer’s local aggregate sample during first commissioning
- PLC display language and control parameters set before the machine leaves the factory
- Mould change procedure training covering cartridge removal, alignment and cycle reset
- Wear parts list for manganese steel mould surfaces and hydraulic seals with reorder codes
What to Include With Your Inquiry
Share the specific block formats your market sells along with target daily output per format so the capacity calculation reflects your real production mix. Provide a sample or description of your local aggregate and mix design, the dimensions of your existing curing area, and your site voltage and frequency. If you already run a block line, note your current pallet size and forklift capacity so the QT12-15 pallet and handling configuration can be matched without duplication or rehandling.
Frequently Asked Questions
Q: How is capacity calculated per block format, and why does the same machine show different output?
A: The QT12-15 uses a 15-17 second cycle for standard 240×115×53 mm solid blocks with 62 pieces per mould, but needs 20-25 seconds for hollow and porous formats with fewer pieces per mould. Every capacity figure is stated with the block format, mould count and cycle time behind it so you can match output to your actual product mix.
Q: Can moulds be supplied for the specific block formats my local market sells?
A: Moulds are manufactured from manganese steel with carburizing and quenching treatment, and custom designs are built from buyer drawings. The format list is confirmed before production so the profiles your market demands — including non-standard interlock or kerbstone shapes — are included in the initial mould package.
Q: Is the 1350×850 mm pallet compatible with my existing curing racks and forklift?
A: Pallet dimensions must align with curing rack spacing and forklift fork width to avoid rehandling after pressing. The pallet specification is confirmed during the proposal stage against your site layout so freshly pressed blocks transfer directly to curing without manual restacking.
Q: How do vibration force and hydraulic pressure need to match my local aggregate?
A: The platform vibration at 120 kN and 21 MPa hydraulic pressure are calibrated against the buyer’s specific mix design and aggregate type. A raw material sample is reviewed before final parameter settings are locked so block strength remains consistent across production batches.
Q: What is the mould change time, and does it allow format switching within one shift?
A: Mould change time depends on the cartridge configuration and operator familiarity. Training covers the full procedure including removal, alignment and cycle reset, and the target changeover duration is confirmed during commissioning so format switching remains practical within your shift schedule.