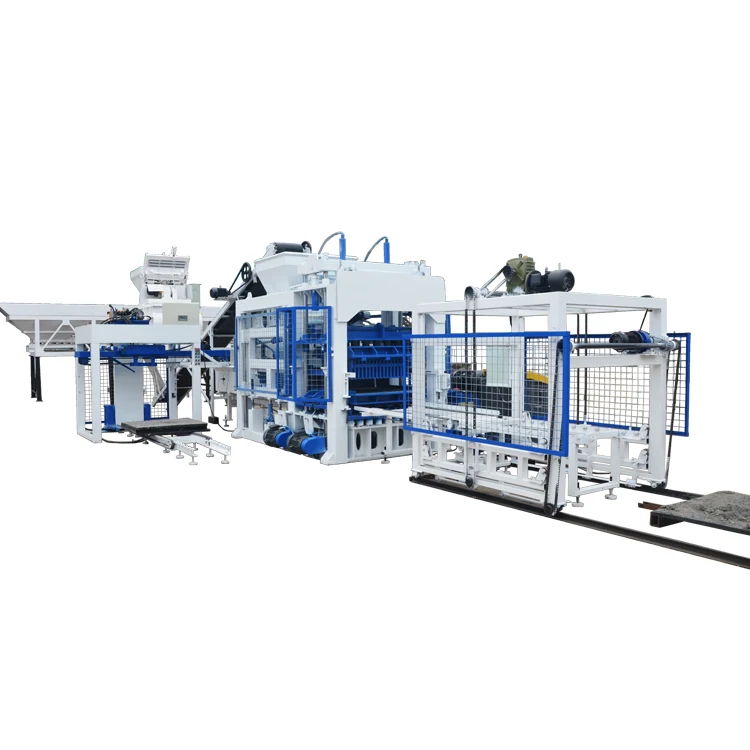
Description
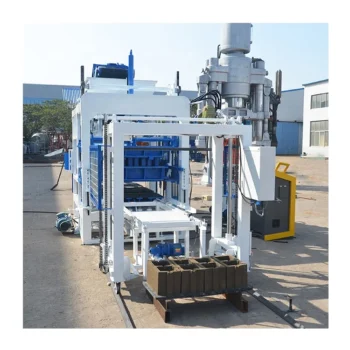
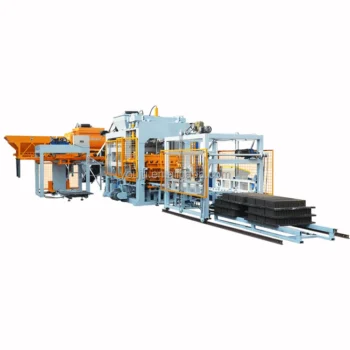
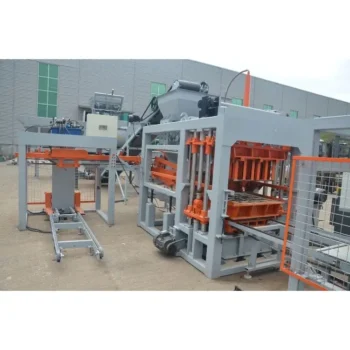
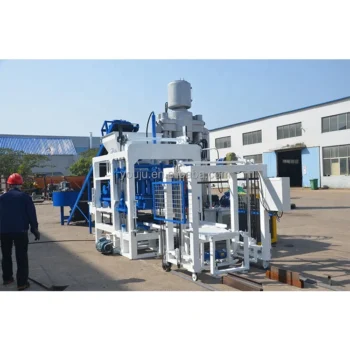
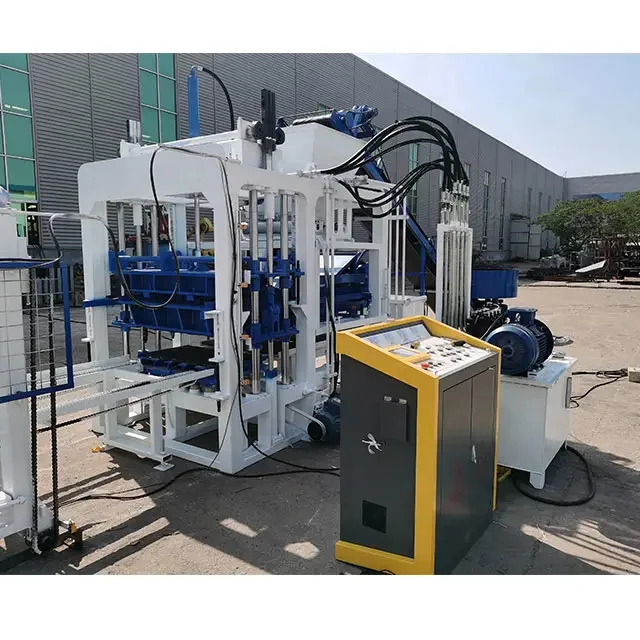
Format-matched capacity — the QT10-15 block machine is configured against your specific hollow block or paver dimensions and local aggregate, so daily output figures reflect what you will actually produce rather than a generic catalogue claim.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Concrete Block Making Machine |
| Model | QT10-15 |
| Vibration Acceleration | 20g |
| Vibration Technology | Dynamic and static table with frequency conversion, four-axis vibration |
| Feeding System | Press-in arch breaker with 360° rotation |
| Vibration Damping | Flexible reduction on pressure head; adjustable air bag in mold box |
| Mould Compatibility | Interchangeable molds for wall blocks, porous bricks, pavement bricks, slope protection bricks |
| Automation Level | Automatic |
| Output Capacity | Stated in source (basis not stated in source — confirm block format / material / thickness) |
| Hydraulic Pressure | To be confirmed based on mix design |
| Pallet Size | To be confirmed based on curing area and handling equipment |
| Control System | PLC details to be confirmed |
| Voltage & Frequency | Configurable to site requirements |
Application Suitability
| Application | Material or Output |
|---|---|
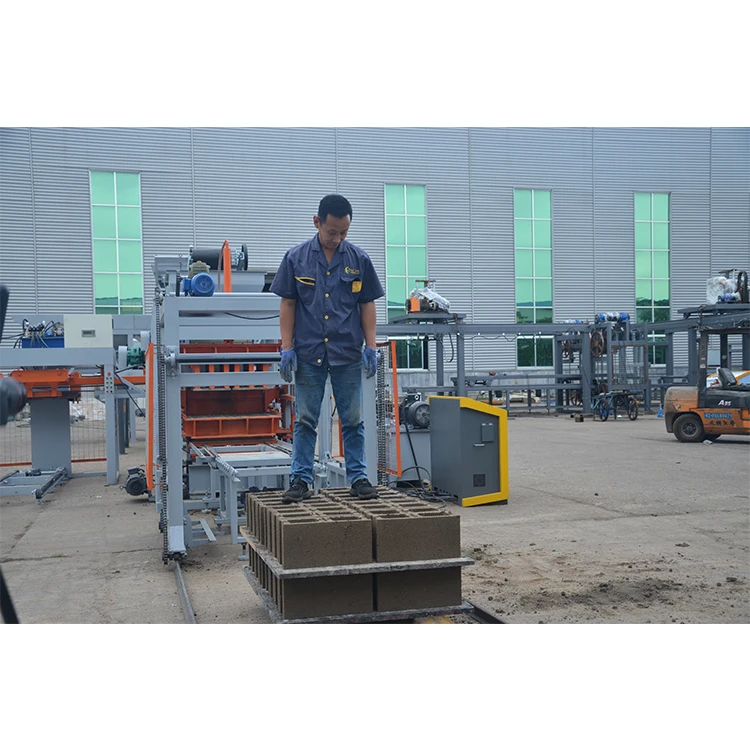
| Hollow block production for masonry walls | Crushed stone, sand, cement, water |
| Interlocking paver manufacturing | Fine aggregate, cement, pigment for color layers |
| Porous brick forming for permeable surfaces | Graded aggregate with controlled binder ratio |
| Slope protection block production | Heavy mix designs with reinforced structural requirements |
What "Cycles per Hour" Actually Means for the QT10-15 Automatic Block Making Machine
The cycle time changes with every mould you install, so one headline number cannot describe real plant output.
Many quotations list a single cycles-per-hour figure derived from a standard hollow block, then the buyer discovers that producing interlocking pavers or thinner porous bricks stretches the cycle noticeably. The QT10-15 automatic block making machine specifications must be evaluated against each format you intend to run. When high-moisture river sand replaces dry crushed sand, vibration and pressing sequences require adjustment, and daily volume drops accordingly [NEED_CITE: impact of aggregate moisture on block forming cycle time].
Vibration Control Across Different Block Geometries
The four-axis vibration system delivers 20g acceleration through both dynamic and static table elements, with frequency conversion allowing the operator to adjust forming speed per mould type. This matters because a heavy hollow block demands sustained low-frequency energy to consolidate coarse aggregate, while a thin interlocking paver requires shorter, higher-frequency bursts to achieve surface density without edge damage.
How the Feeding System Handles Difficult Mixes
The 360° press-in arch breaker forces material into every corner of the mould cavity, which becomes critical when producing interlocking bricks with narrow channels or porous bricks requiring uniform void distribution. Without this rotation, dry mixes with low cement content tend to bridge in the hopper, leaving underfilled sections that produce weak blocks rejected at the curing stage [NEED_CITE: material bridging in block mould feeding systems].
Reading the Vibration and Pressure Specifications
The 20g vibration acceleration works in conjunction with hydraulic pressure to determine final block density. Higher vibration energy liquefies the mix momentarily, allowing particles to settle tightly before hydraulic pressure locks them in place. If your local aggregate is angular crushed stone rather than rounded river gravel, the vibration must work harder to achieve the same consolidation, meaning the hydraulic pressure setting and dwell time need corresponding adjustment. The adjustable air bag vibration damping in the mould box absorbs shock between cycles, reducing structural fatigue on the mould frame and extending service life across frequent format changes. The flexible vibration reduction on the pressure head prevents transmitted energy from loosening hydraulic fittings over extended production runs.
The Cost of Skipping Format-by-Format Capacity Planning
A buyer who selects a machine based solely on a headline output figure often discovers that the format their market actually demands — perhaps a specific interlocking paver or a thin porous brick — runs at a substantially longer cycle time. The plant then cannot meet contractual delivery schedules, and penalty clauses activate. Additionally, if the pallet size was chosen without checking the buyer’s existing curing racks and forklift dimensions, the entire handling workflow breaks down from day one [NEED_CITE: block plant layout and pallet handling integration].
Why Sourcing the QT10-15 Here Reduces Specification Risk
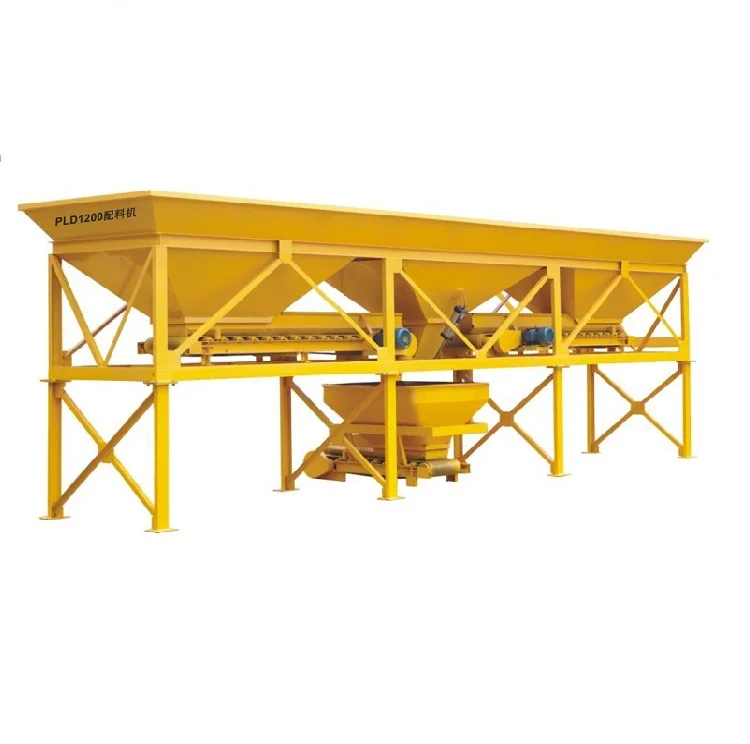
Block machinery remains the single product focus, meaning the press, mould, pallet, and handling equipment are specified as one matched system rather than sourced from separate vendors and forced to work together. Configuration begins with the buyer’s actual mix design and local aggregate sample, not a default catalogue setting. Mould design covers the specific formats the buyer’s regional market demands, including custom drawings when standard options do not match. Automation level is selectable, allowing a plant to begin with semi-automatic pallet handling and add stacking or cubing later without replacing the press. Voltage, frequency, and PLC display language are confirmed before production starts, eliminating commissioning delays when the machine arrives on site.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Mould drawing and format list confirming compatibility with target products
- Hydraulic and electrical schematic for local maintenance team review
- Voltage, frequency, and control language confirmation record before dispatch
- Factory test record on buyer’s specified block format and mix
Installation, Commissioning & Support
- Foundation plan showing load points for the QT10-15 vibration table and hydraulic power unit
- Electrical supply specification covering voltage, frequency, and dedicated circuit requirements for the rated power draw
- On-site assembly with vibration alignment verification after transit
- Parameter setting for each mould format installed, including vibration frequency and hydraulic dwell time
- Operator training covering mould change procedure, feeding system adjustment, and daily inspection points
- Wear parts list identifying hydraulic seals, vibration springs, and mould liner replacement intervals
What to Include in Your Inquiry
Provide the exact block formats your market sells, including dimensions and target compressive strength, along with a sample or description of your local aggregate and cement type. Specify your available curing area dimensions and any existing forklift or handling equipment the pallets must work with. Confirm your site voltage, frequency, and preferred PLC display language so the QT10-15 automatic block making machine arrives ready to commission.
Frequently Asked Questions
Q: How is the QT10-15 output capacity calculated per block format?
A: Each capacity figure is tied to a specific block format, mould type, and mix design. The calculation accounts for the cycle time required to fill, vibrate, press, and eject that particular geometry. Without knowing which format you will produce most, a single output number is misleading — request a format-by-format breakdown based on your actual product range.
Q: Which mould formats are available and what is the cycle time for each?
A: Standard moulds cover hollow wall blocks, interlocking pavers, porous bricks, and slope protection blocks. Cycle time varies by format thickness, aggregate particle size, and required density. A thin porous brick typically completes faster than a large hollow block, but exact figures depend on your confirmed mix design and strength target.
Q: How long does a mould change take on the QT10-15?
A: Mould change duration depends on whether the machine has quick-release clamps or bolt-fixed mounting, and whether hydraulic connections must be re-routed for the new mould height. Specify your planned format change frequency so the appropriate mould change system is included in the configuration.
Q: How is vibration force matched to the buyer’s local aggregate and mix design?
A: Angular crushed stone requires different vibration frequency and duration compared to rounded river gravel to achieve the same particle consolidation. The four-axis system with frequency conversion allows on-site tuning. An aggregate sample and trial mix test before final parameter lock-in ensures the vibration profile matches your material.