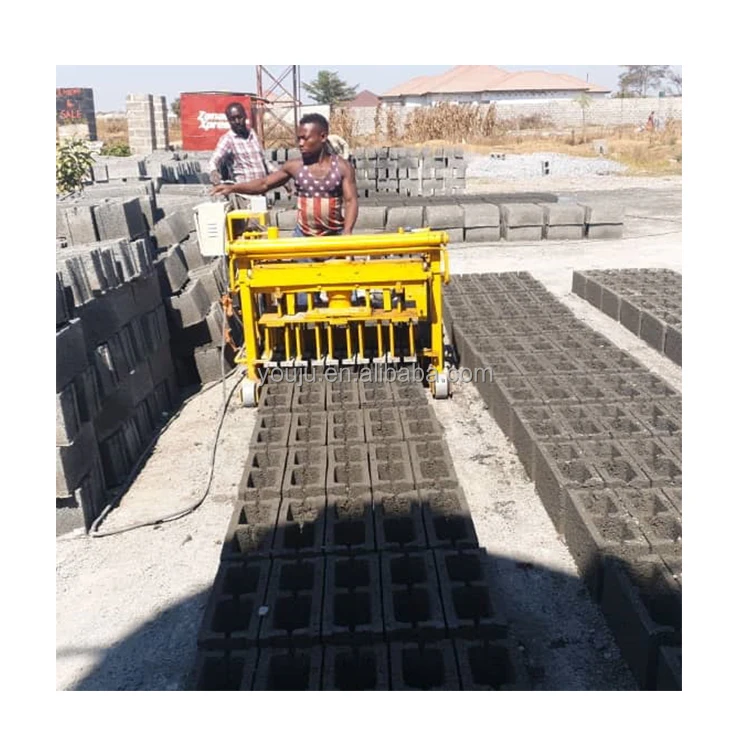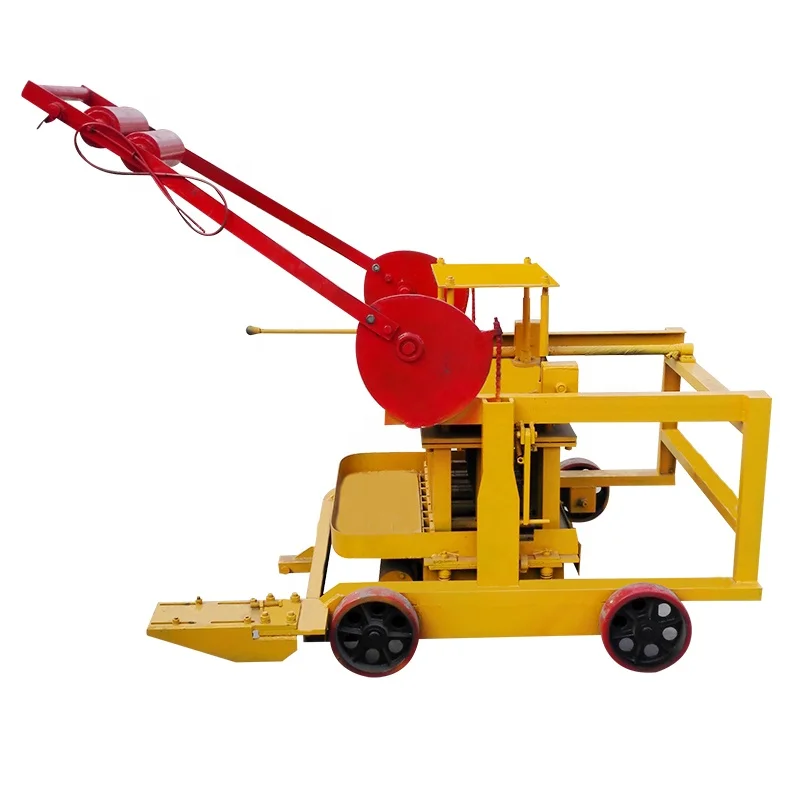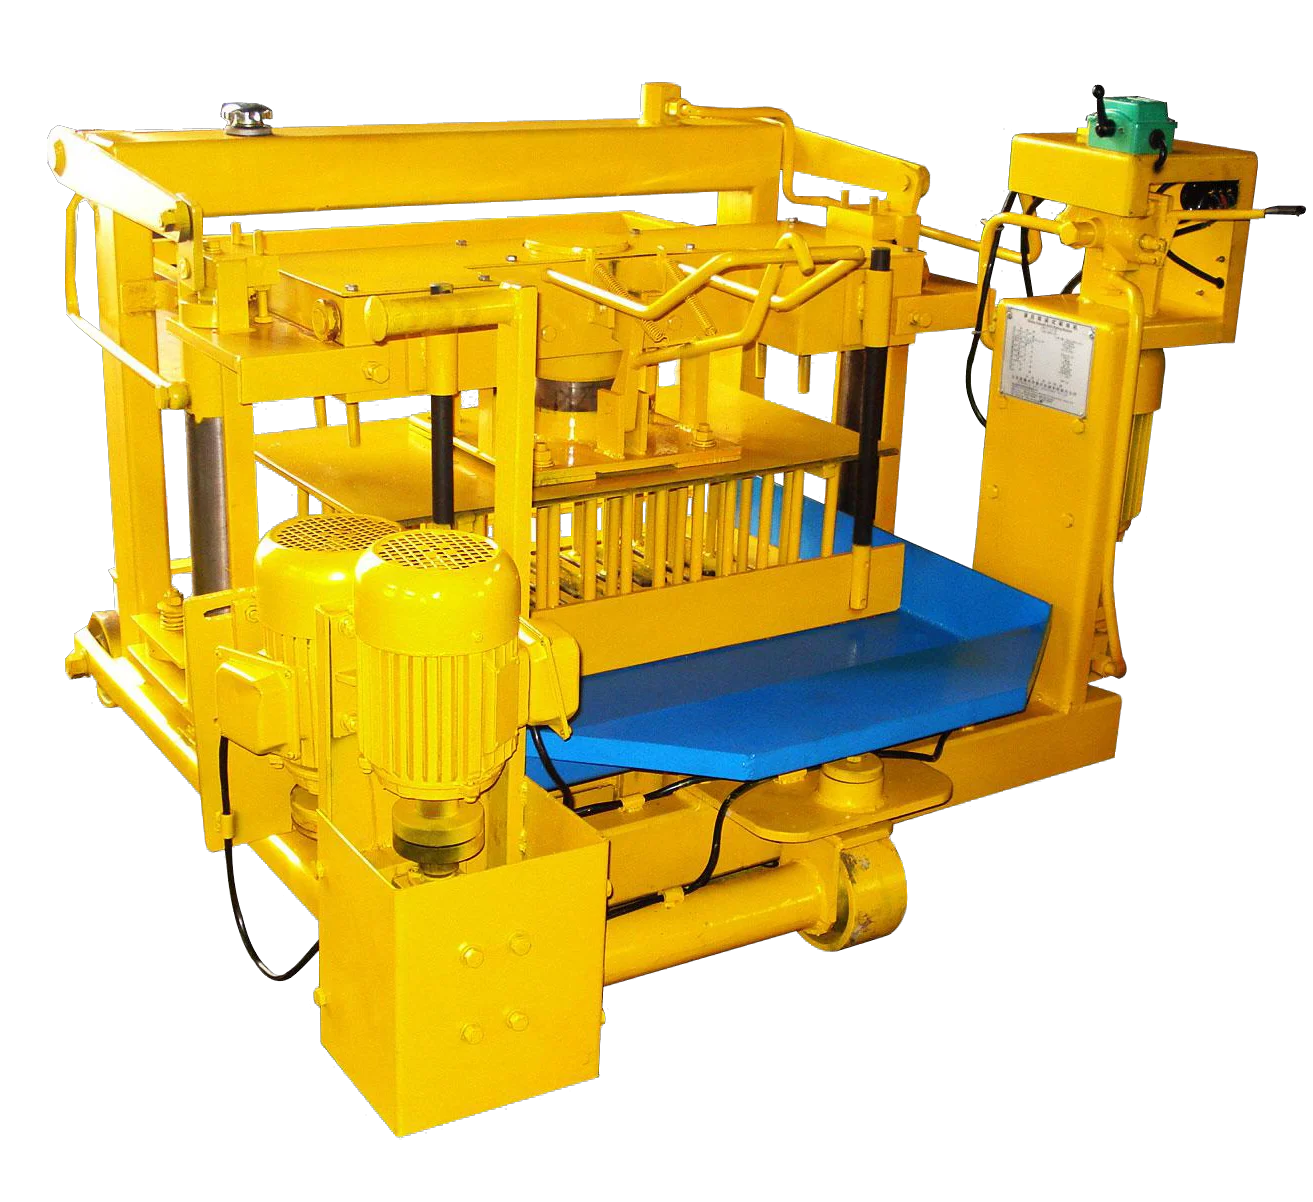
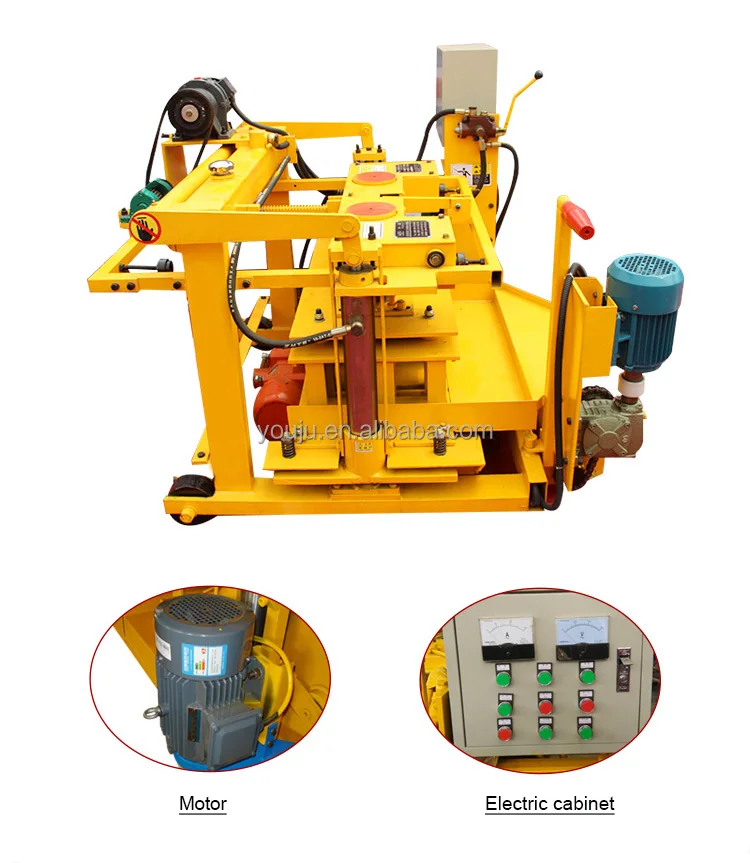


Description
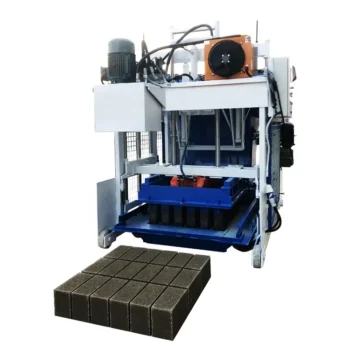
Honest Capacity by Format — the QMY4-30 mobile egg-laying block machine is specified with cycle time and daily output tied to each block size your market actually sells, not a single headline figure.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMY4-30 |
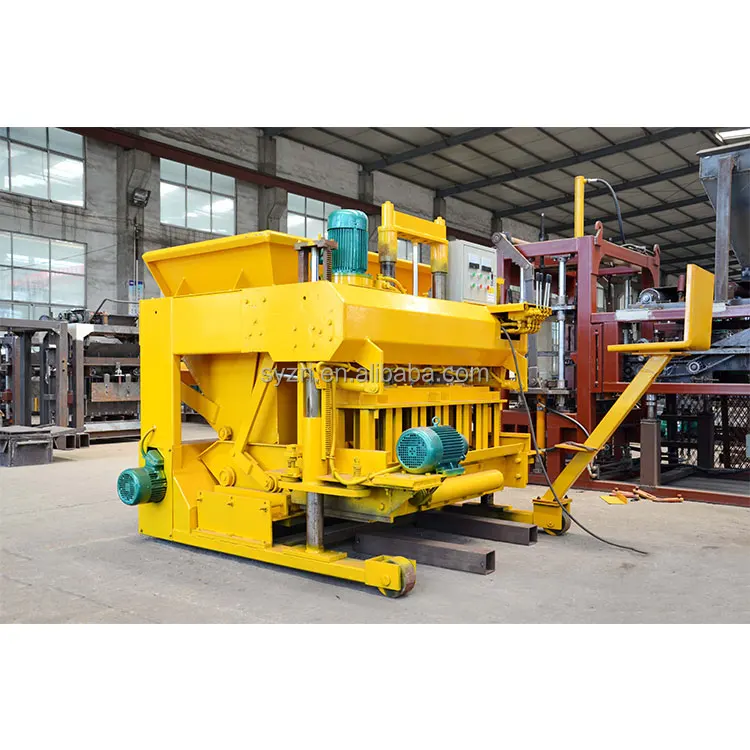
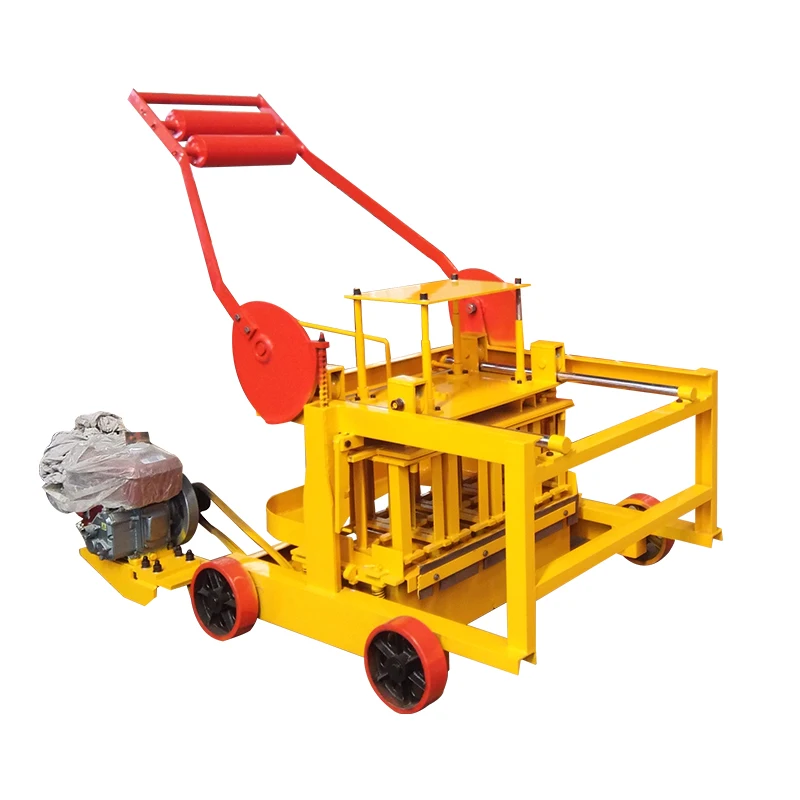
| Product Type | Mobile Egg-Laying Concrete Block Machine |
| Rated Power | 5 kW |
| Voltage & Frequency | Configurable to buyer’s local supply (basis to be confirmed) |
| Control System | Manual operation |
| Overall Dimensions (L×W×H) | 1200×1200×1100 mm |
| Net Weight | 950 kg |
| Mould Format Options | 400×200×200 mm (4 pcs/mould), 400×150×200 mm (5 pcs/mould), 400×100×200 mm (7 pcs/mould) |
| Cycle Time | 30 seconds |
| Output Capacity | 480 pcs/h based on 400×200×200 mm hollow block; 600 pcs/h based on 400×150×200 mm block; 840 pcs/h based on 400×100×200 mm block |
| Daily Output (8 h shift) | 3,840 pcs (400×200×200 mm) / 4,800 pcs (400×150×200 mm) / 6,720 pcs (400×100×200 mm) |
| Pallet Size | Not applicable — egg-laying type, blocks laid directly on ground |
| Mould Change System | Manual change between hollow block and solid brick formats |
| Raw Materials | Cement, sand, crushed stones, slag |
| Assembly State | Single mobile unit |
Application Suitability
| Application | Material or Output |
|---|---|
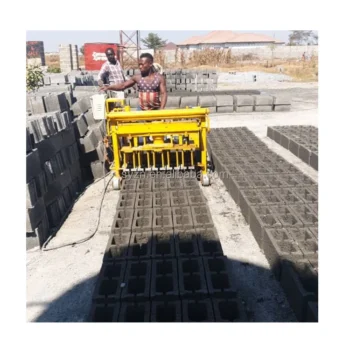
| On-site hollow block production | Crushed stone, sand, cement laid directly on project ground |
| Solid brick manufacturing for small plants | Local aggregate blended with cement, cured in place |
| Remote or temporary construction projects | Low-investment mobile production without fixed plant infrastructure |
| First plant for entrepreneurs | Entry-level output using locally sourced sand and slag |
What "840 Pieces per Hour" Leaves Out About Mobile Egg-Laying Block Machine Specifications
Every capacity number on this page is tied to a specific block format and mould — because a cycle count without a block size tells you almost nothing.
I once watched a contractor in the Middle East receive a mobile block machine quoted at a headline capacity. The local aggregate had high clay content, which meant vibration time had to be extended per cycle. Actual daily output dropped to less than half of the brochure figure. The machine was not faulty; the capacity quote simply did not state which block format it assumed. When you evaluate mobile egg-laying block machine specifications, the question is never just "how many per hour" but "how many of what, using which mix" [NEED_CITE: capacity verification methods for mobile block forming equipment].
The QMY4-30 runs a 30-second cycle, but the real output depends entirely on whether you are pressing 400×200×200 mm hollow blocks at 4 pieces per mould or 400×100×200 mm solid blocks at 7 pieces per mould. That difference alone changes your daily count from 3,840 to 6,720 over an eight-hour shift.
Mould Format Determines Your Real Daily Output
A mobile egg-laying block machine lives or dies by its mould selection. The QMY4-30 accepts three standard mould formats, each producing a different piece count per cycle. Buyers often focus on the largest number without checking which format it assumes. When sizing a machine to your market, start with the block your customers actually buy, then work backward to the mould and cycle count.
Matching Local Aggregate to Vibration Settings
Not every crushed stone source behaves the same under vibration. High-clay or high-moisture aggregates require longer consolidation time, which stretches the cycle beyond the baseline 30 seconds. Before the machine ships, the mix design and local aggregate characteristics should be documented so vibration duration and pressure can be set accordingly. Skipping this step is one of the most common reasons mobile block machines underperform on arrival [NEED_CITE: effect of aggregate clay content on block consolidation time].
Reading the Power and Footprint Together
The 5 kW rated power keeps electrical demand low, which matters when the machine is running on a generator at a remote project site. Combined with the 1200×1200×1100 mm footprint and 950 kg weight, the QMY4-30 can be moved between pouring locations without a crane. This compact envelope means the machine fits inside a standard site compound and can operate where fixed plant infrastructure does not exist.
Cycle Time, Mould Change, and Format Flexibility
The 30-second cycle is measured with the mould in position and the mix ready. Manual mould change between hollow and solid formats allows a single machine to serve multiple product lines, but the changeover itself takes operator time away from production. On a small site with two or three block formats in demand, planning which formats to run in sequence reduces the number of changeovers per shift and protects your actual daily output [NEED_CITE: operational planning for mobile block machines with manual mould change].
The Cost of Skipping Mix Verification
When a buyer orders without confirming local aggregate properties, the machine arrives configured for a standard sand-cement mix that does not match what is available on site. Blocks come out under-consolidated or cracked. The operator adjusts settings by trial and error, burning days of production. In some cases the buyer is forced to source alternative raw material at higher cost just to meet block strength requirements — a problem that could have been caught with a sample test before shipment.
Why Procurement Decisions Should Start with Format and Material
The QMY4-30 is configured against the block format your market actually trades, not a catalogue default. Mould drawings are confirmed before production, so the machine arrives with the cavities your customers need. Voltage and frequency are locked to your local grid before the unit enters assembly, avoiding the weeks-long delay that happens when a 380V machine arrives at a 415V site. Factory testing uses your stated mix design so cycle time and block density are verified under realistic conditions, not ideal laboratory parameters. Documentation travels with the machine, including the capacity calculation that states which format each output figure assumes.
Documentation & Verification
- Line layout showing block format assumed for each capacity figure
- Mould drawing and format list confirming included cavity sizes
- Factory test record run on buyer’s stated mix design before dispatch
- Voltage and frequency confirmation matched to local supply
- Operation and maintenance manual with mould change procedure
Installation, Commissioning & Support
- Level ground preparation required across the machine’s 1200×1200 mm footprint
- Dedicated electrical circuit matching confirmed voltage and frequency rating
- Machine arrives as single mobile unit — no on-site assembly of frame components
- First-run block test with operator adjusting vibration duration to local aggregate
- Manual mould change training covering hollow-to-solid format changeover
- Wear parts list provided with recommended replacement intervals for mould liners
What to Include in Your Inquiry
Tell us the block format your market buys most — dimensions, hollow or solid, and target daily volume. Share the local aggregate type and any test data you have on clay content or moisture. Confirm your site voltage, frequency, and whether the machine will run on grid power or a generator. With these details, a configuration proposal can state realistic output per format rather than a single optimistic number.
Frequently Asked Questions
Q: How is daily output verified for each block format?
A: Every capacity figure for the QMY4-30 is stated per specific mould format. The 480 pcs/h rate assumes 400×200×200 mm hollow blocks at 4 pieces per mould over a 30-second cycle. Daily output is calculated on an eight-hour shift. A capacity calculation document accompanies the quotation stating the block size behind each number.
Q: Which mould formats come with the machine, and can I order custom sizes?
A: The standard package covers 400×200×200 mm, 400×150×200 mm, and 400×100×200 mm formats. Custom moulds can be designed to buyer drawings for formats outside this range. Mould drawings are confirmed before production so the cavities match your local market requirements exactly.
Q: How should local aggregate and mix design affect machine settings?
A: High-clay or high-moisture aggregates require extended vibration time to achieve proper consolidation. The buyer’s mix design and aggregate sample data should be shared before shipment so cycle parameters can be adjusted. This prevents the common problem where standard settings produce weak blocks on unfamiliar raw material.
Q: What electrical details must be confirmed before the machine ships?
A: Voltage, frequency, and plug configuration must match the buyer’s local supply. The QMY4-30 ships with configurable electrical settings, but these must be locked before assembly begins. Confirming these details early avoids commissioning delays caused by mismatched power supply at the project site.
Q: How long does mould changeover take on site?
A: Mould change on the QMY4-30 is manual and typically completed within a single shift break when the operator is trained. Planning production runs by format reduces the number of changeovers per day. The operation manual includes a step-by-step procedure for switching between hollow block and solid brick moulds.