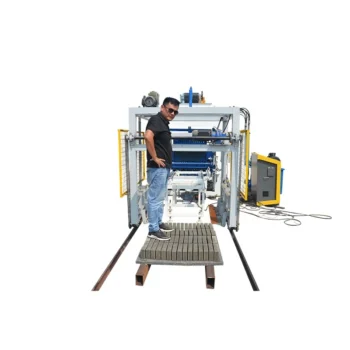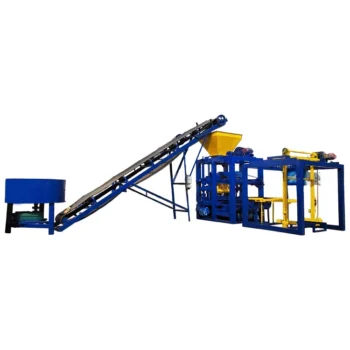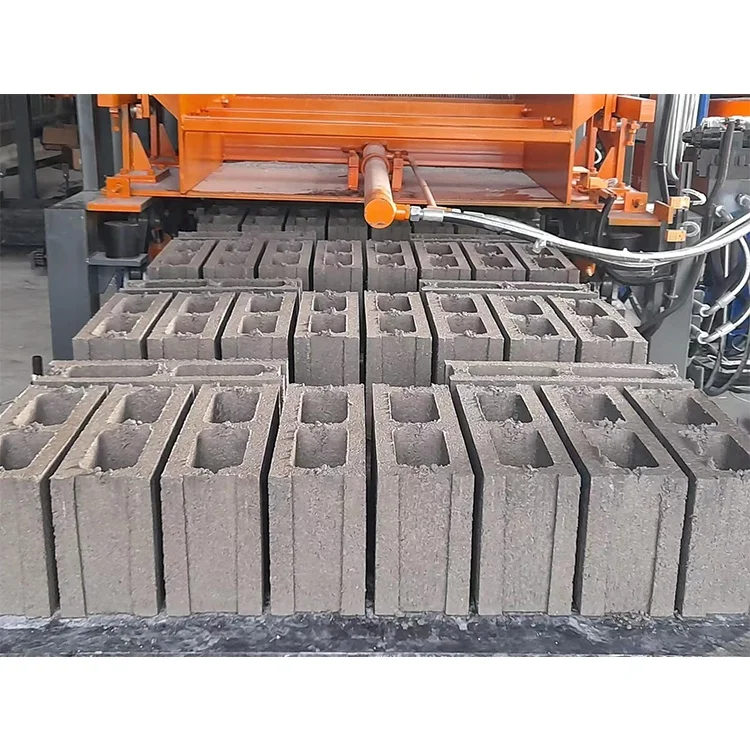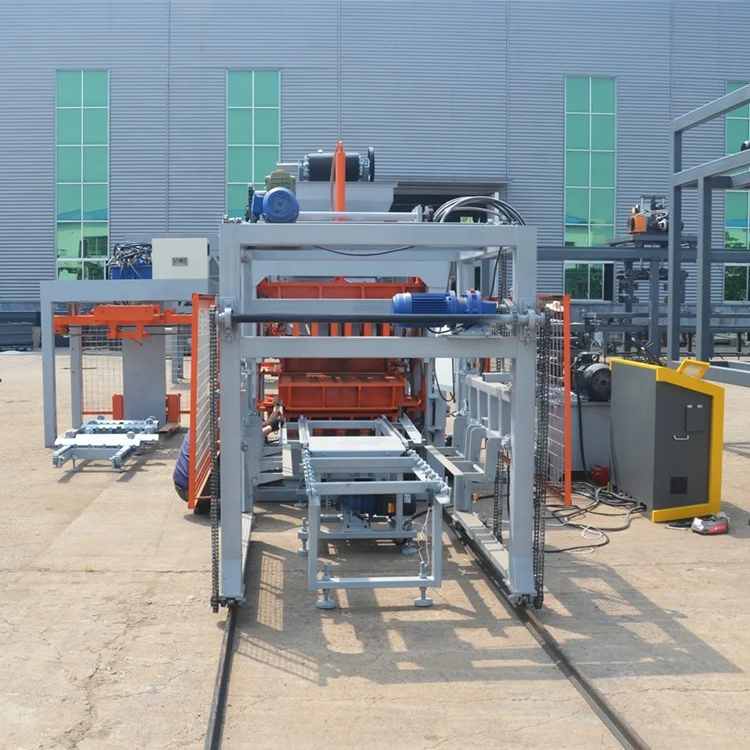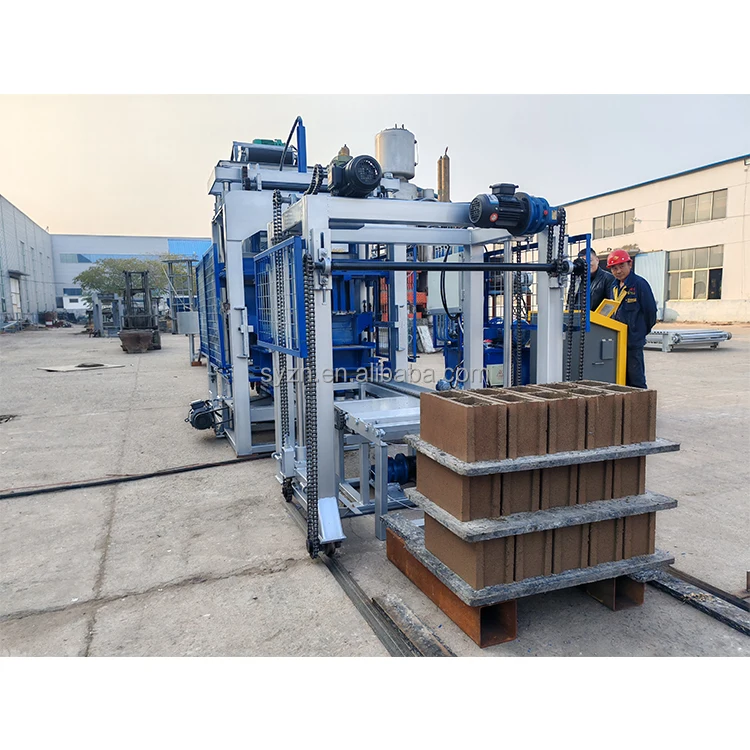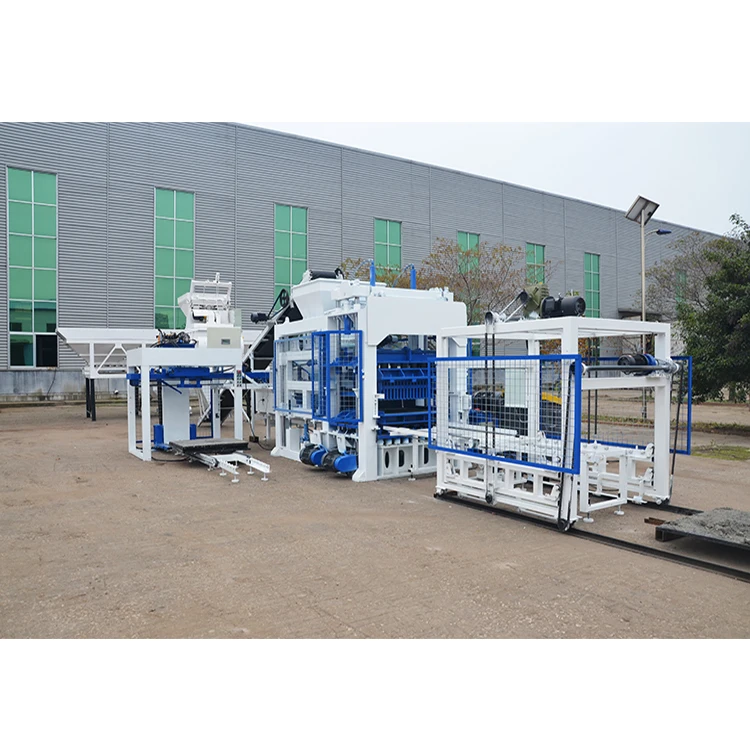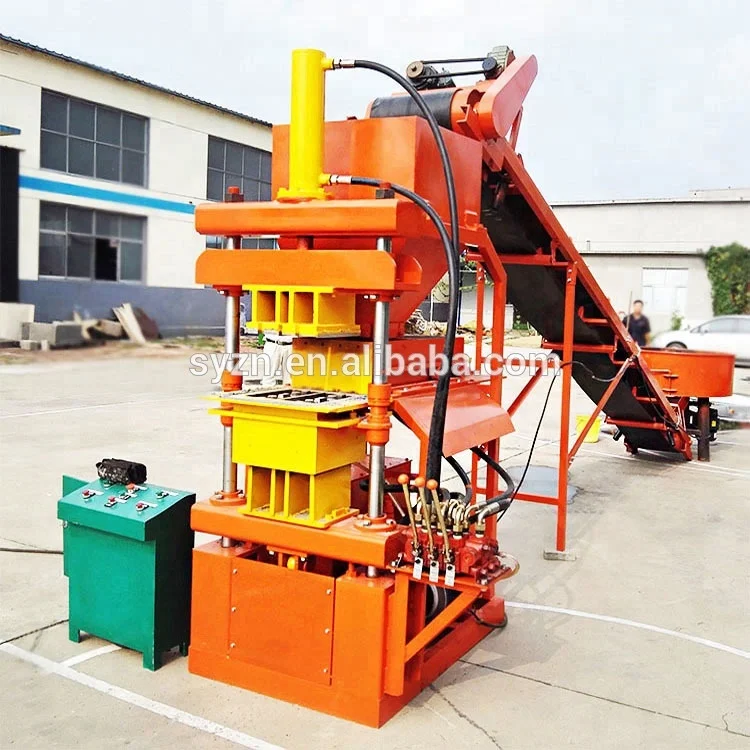


Description
Matched System Configuration — the LY2-10 is specified with mould, pallet and cycle time aligned to your actual clay or cement brick format, not assembled from catalogue defaults.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY2-10 |
| Product Type | Clay Block Making Machine |
| Machine Power | 7.5 kW |
| Molding Cycle | 10 s |
| Automation Level | Semi-automatic |
| Machine Type | Interlocking clay and cement brick machine |
| Assembly State | Stationary |
| Overall Dimensions (L×W×H) | 1300 × 1800 × 2400 mm |
| Raw Materials | Clay, soil, earth, mud, concrete, cement, fly ash |
| Standard Mould Formats | 300×150×100 mm / 250×125×75 mm / 230×220×115 mm |
| Bricks per Mould | 1 pc (per listed format) |
| Output per Format | 750 pcs/h based on 1 pc/mould and 10-second cycle (basis to be confirmed for specific block format and material) |
| Capacity Claim | 6000 pcs/8 hours (basis not stated in source — confirm block format / material / thickness) |
| Standards | CE (where applicable) |
Application Suitability
| Application | Material or Output |
|---|---|
| Clay and cement interlocking brick production | Local soil, earth, or clay mixed with cement binder |
| Small to medium block plants | Earth-based or cement-based bricks for regional construction markets |
| On-site brick manufacturing | Site-available soil and cement for housing project contractors |
| Building material distributors | Interlocking brick formats added to an existing block product range |
What "6,000 Pieces per 8 Hours" Actually Means for Your Brick Format
A capacity number without a block format attached is a guess, not a production plan.
When a clay block making machine specifications sheet quotes a single daily output figure, it usually assumes the smallest, lightest brick in the mould range. Switch to a larger interlocking format and the cycle time stays similar, but each press stroke produces fewer pieces. I have seen buyers receive a machine expecting a headline number, only to find their actual market brick yields considerably less per shift because the capacity was calculated on a format they never intended to sell. The LY2-10 output must be stated per specific mould size and confirmed against your local clay or cement mix before the machine is configured [NEED_CITE: capacity calculation methods for block making machinery].
Per-Format Output and Mould Selection
The LY2-10 ships with mould options covering three standard interlocking brick dimensions: 300×150×100 mm, 250×125×75 mm, and 230×220×115 mm. Each format produces one brick per mould cycle, and the 10-second moulding cycle applies across formats. The meaningful clay block making machine specifications for your purchase decision are the output tied to the exact brick your market demands, not a blanket figure. Mould drawings are confirmed against your required dimensions before production begins.
Semi-Automatic Operation for First-Time Plant Owners
This semi-automatic clay block making machine balances labour investment with production control. The operator manages pallet feeding and brick removal while the press cycle runs on a fixed timer. For entrepreneurs setting up a first brick plant or contractors producing interlocking bricks locally from site-available soil, this configuration keeps initial capital outlay measured while maintaining consistent pressing parameters across every cycle [NEED_CITE: semi-automatic block machine operational requirements].
Reading the Core Specifications
The 7.5 kW motor drives the vibration and pressing mechanism; this power rating suits small to medium brick formats in clay and cement mixes without excessive energy draw. The 1300 × 1800 × 2400 mm footprint means the machine fits inside a standard workshop bay without special foundation work beyond a level concrete pad. The 10-second moulding cycle is a fixed parameter that determines your theoretical hourly output once the brick format is locked in. Raw material flexibility across clay, soil, earth, mud, concrete, cement, and fly ash means the machine can be configured to whatever aggregate your site or region provides, but the mix design must be tested before the vibration force and pressure settings are finalised. Pallet size must match both the mould footprint and the curing racks or forklift you already have on site [NEED_CITE: pallet sizing for block curing and handling].
The Cost of Skipping Mix Design Testing
I once configured a clay brick machine for a Southeast Asian buyer using standard capacity figures from our sample book. The customer’s local red soil had high clay content and stickiness that standard settings could not handle — daily output fell to roughly half the quoted figure, and the buyer nearly cancelled the order. Since then, every machine I specify goes through a raw material trial with the buyer’s actual soil or clay sample before parameters are locked. Skipping this step means you risk receiving a machine tuned to a mix you cannot source locally, forcing a costly material substitution or enduring chronic underperformance [NEED_CITE: effects of local aggregate properties on block machine output].
Why Source the LY2-10 Here
Block machinery is our single focus, so the LY2-10 machine, mould, pallet, and handling requirements are specified as one matched system rather than assembled from separate suppliers. We configure the press settings against your actual mix design and local aggregate, not a catalogue default. Mould design covers the interlocking brick formats your market actually sells, with custom drawings available for non-standard dimensions. The semi-automatic configuration allows you to start with controlled investment and add automation later as production volume grows. Installation support includes operator training so your team understands mould change procedure, daily maintenance, and how to adjust parameters if your raw material source shifts.
Documentation & Verification
- Machine specification sheet confirming voltage, frequency, and control display language before production
- Mould drawing and format list matching the exact interlocking brick dimensions your market requires
- Capacity calculation document stating the block format assumed for each output figure
- Factory test record demonstrating cycle time and brick integrity against your confirmed mix design
- Operation and maintenance manual covering mould change, daily lubrication, and vibration base inspection
Installation, Commissioning & Support
- Level concrete pad required within the 1300 × 1800 mm machine footprint with anchor bolt provision
- 7.5 kW power supply on a dedicated circuit with voltage and frequency confirmed to your local grid standard
- Machine ships as a stationary unit; on-site assembly covers mould mounting and vibration base alignment
- First-run commissioning includes parameter adjustment using your local clay or cement mix sample
- Operator training covers the 10-second cycle timing, pallet handling sequence, and semi-automatic control operation
- Wear parts list identifies mould liners and vibration components with recommended replacement intervals
Before You Request a Quote
Tell us the exact interlocking brick dimensions your market sells, the type of clay or soil available at your site, and your target daily production volume. We also need your local voltage and frequency so the electrical system is wound correctly before the machine leaves the factory.
Frequently Asked Questions
Q: How is the 6,000 pcs/8 h capacity verified, and which block format is it based on?
A: That figure appears in source material without a stated block format or material assumption. We do not use it as a quoting basis. Instead, we calculate realistic output per specific mould size from the standard format list, confirmed against your mix design and the 10-second cycle time, so the number you receive reflects the brick you actually produce.
Q: Can the mould be customized to a brick size not in the standard format list?
A: Yes. We produce moulds from buyer-supplied drawings or develop custom interlocking profiles based on your market requirements. The mould drawing and dimensions are confirmed and approved before manufacturing begins, ensuring the cavity matches your target brick exactly.
Q: What mix design and local aggregate testing is done before the machine is configured?
A: We ask you to send a sample of your local clay, soil, or aggregate. We run trial pressings to determine the right moisture content, cement ratio, vibration force, and cycle behaviour for your material. Parameters are then set before the machine ships rather than adjusted blindly on arrival.
Q: How long does a mould change take, and does it cancel out format flexibility?
A: The LY2-10 mould change is a manual procedure typical of semi-automatic machines in this class. It takes a meaningful portion of a shift if done infrequently, so we recommend ordering all the mould formats you plan to run regularly and scheduling format changes at shift start or planned breaks rather than mid-run.
Q: Which voltage, frequency, and control language options are confirmed before shipment?
A: We confirm your site voltage, frequency, and preferred control display language during the quotation stage. These are written into the machine specification sheet and verified before production so the electrical system and operator interface match your local grid and workforce when the machine arrives.