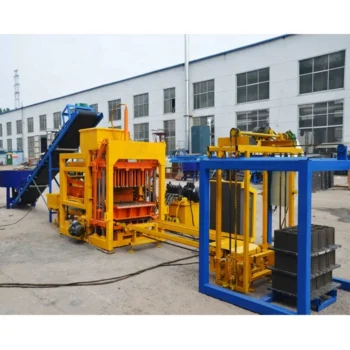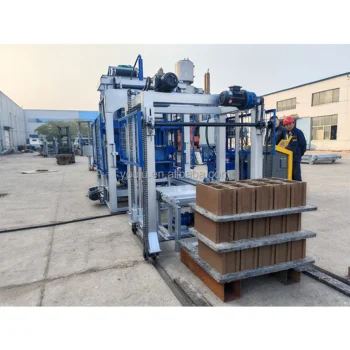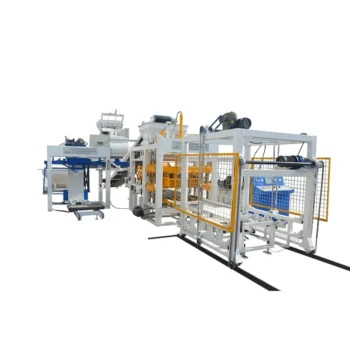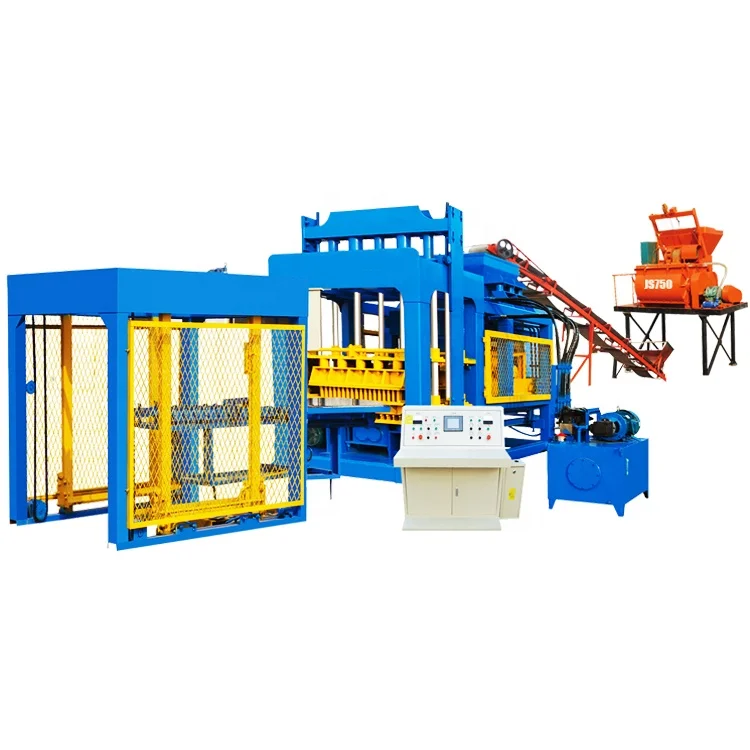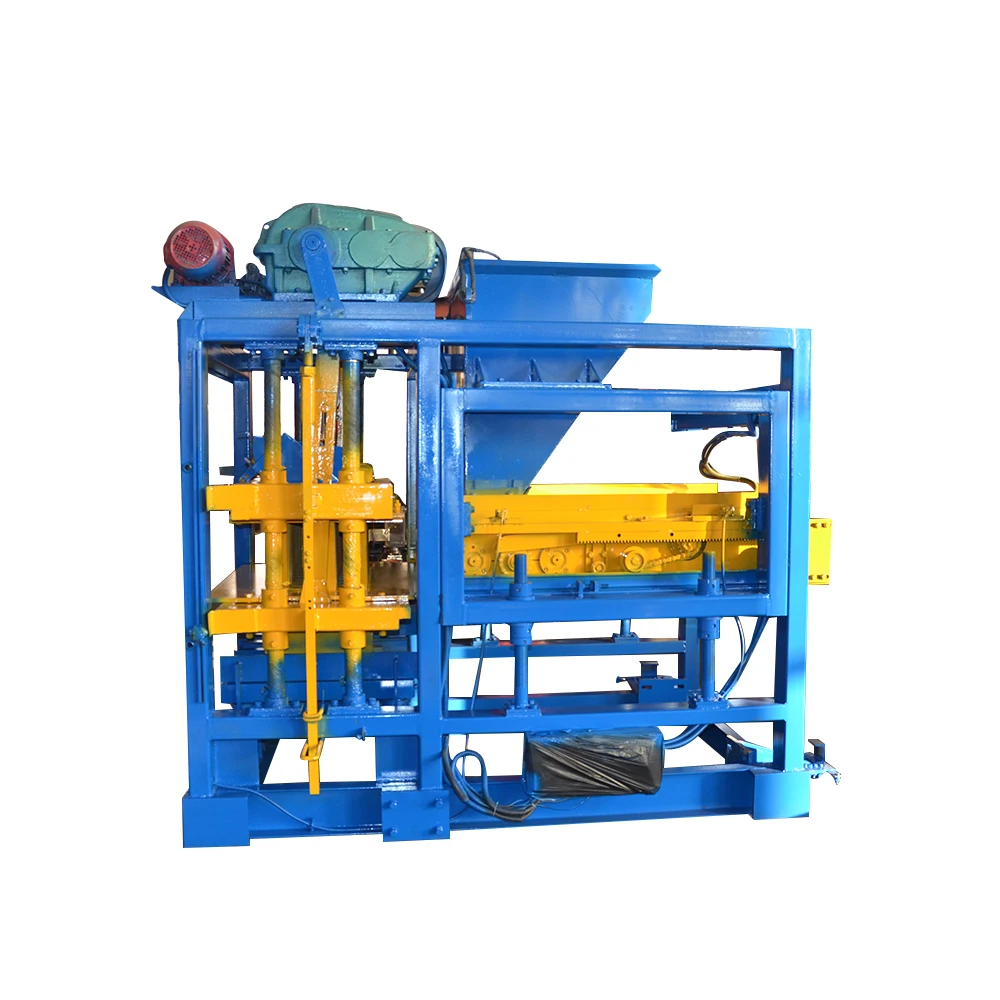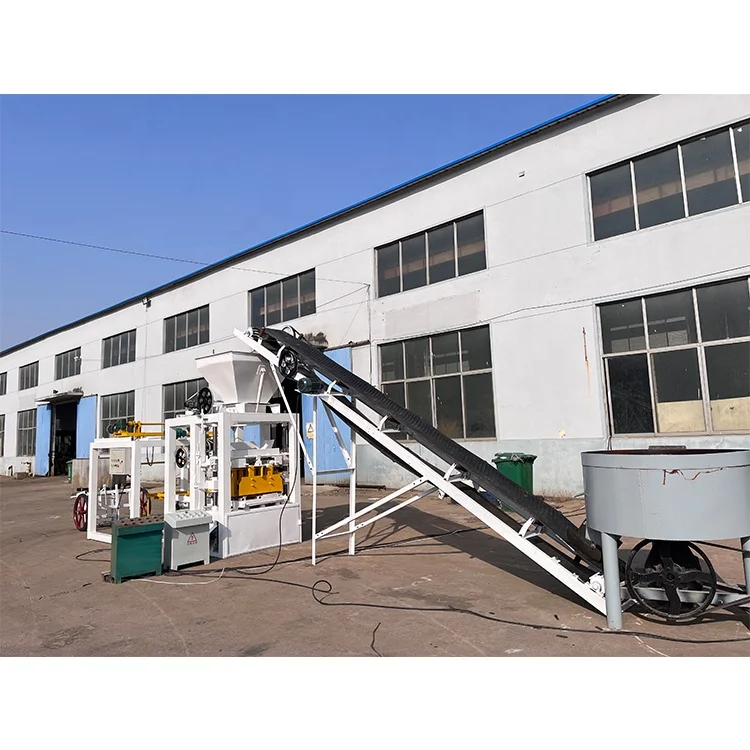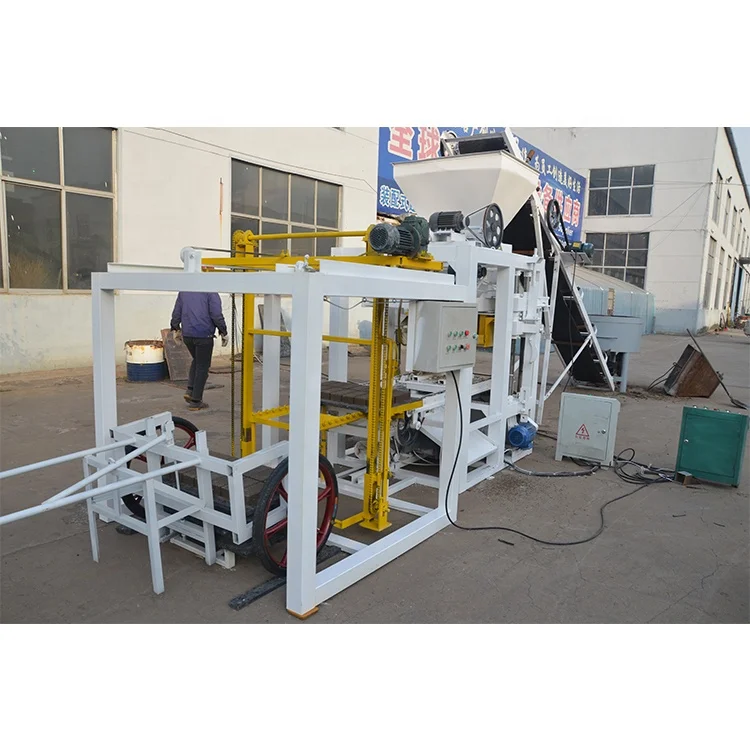
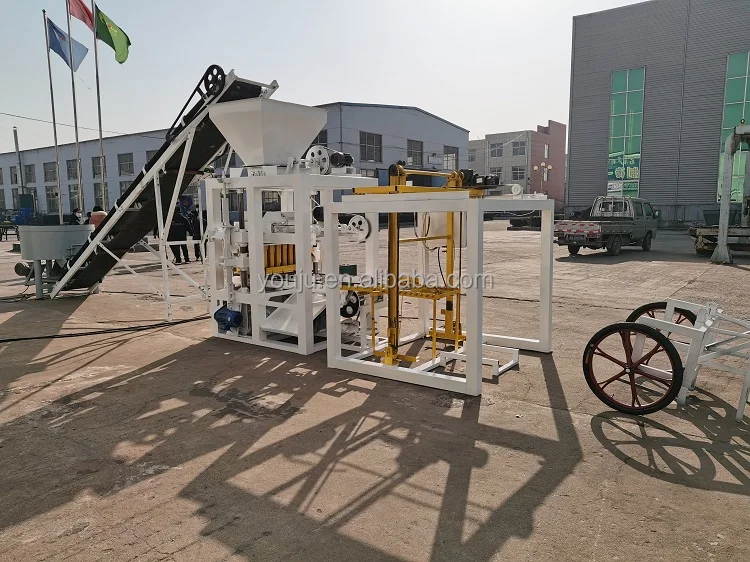
Description
Matched System Sizing — Vibration force, pallet dimension and mould format are selected together against your local aggregate and target block type, not picked from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Molding Type | Platform Vibration |
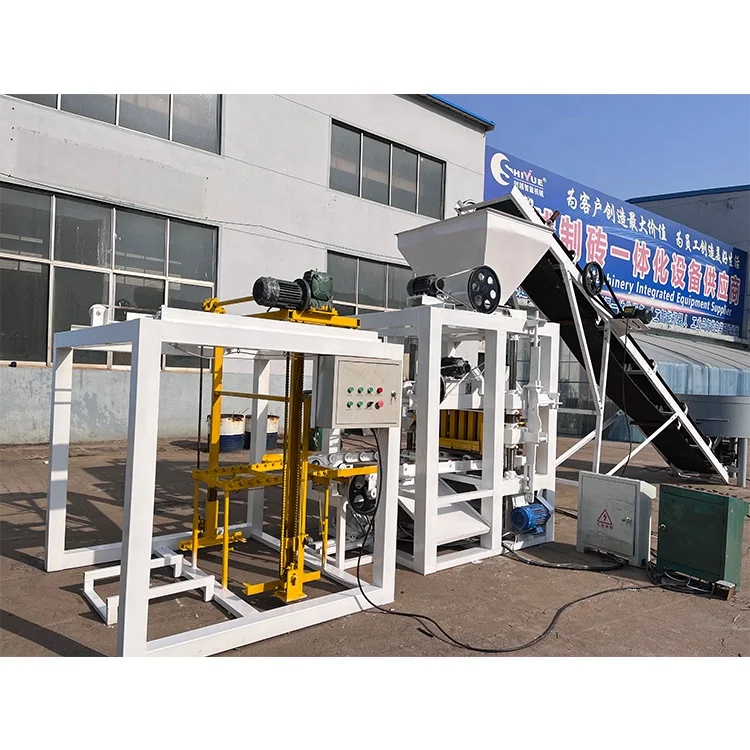
| Overall Dimensions (L×W×H) | 3600mm × 1700mm × 2560mm (working state) |
| Total Mass | 1750 kgs |
| Overall Power | 14.25 kW |
| Pallet Size | 850mm × 450mm |
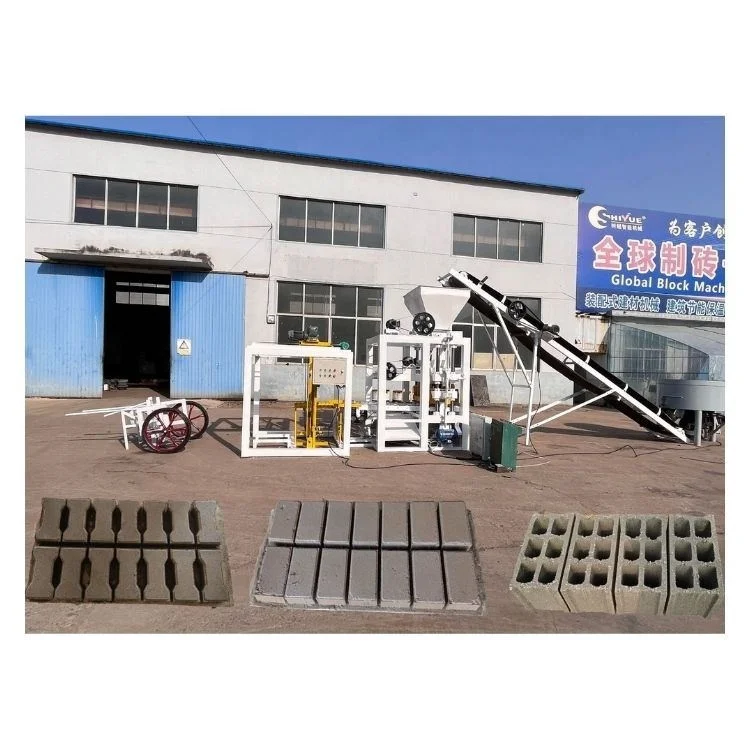
| Mould Format (Hollow Block) | 390mm × 190mm × 190mm (4 pcs/mould) |
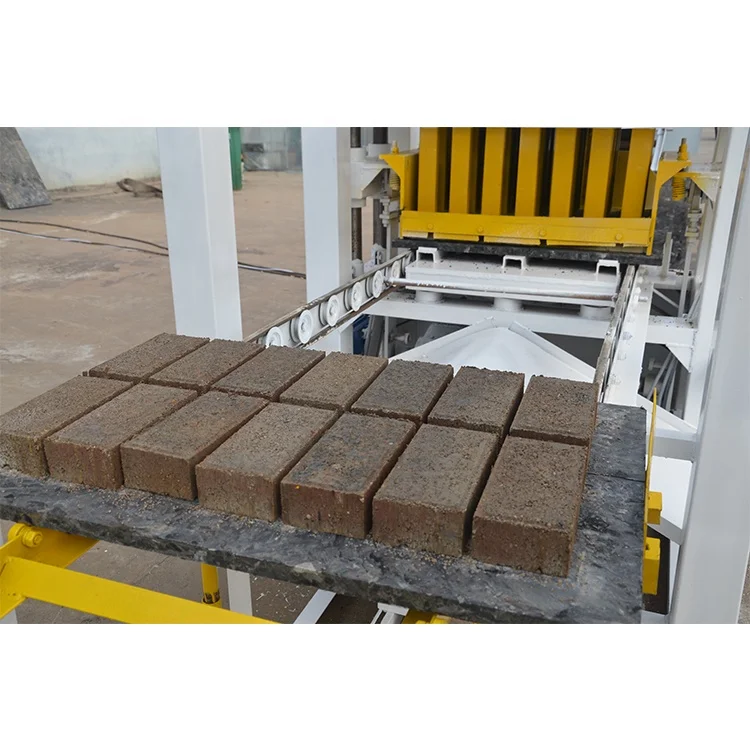
| Mould Format (Solid Brick) | 240mm × 115mm × 53mm (21 pcs/mould) |
| Vibration System | Lower platform vibration (2×3 kW motors) + Upper attached vibration (1.5 kW) |
| Elevating System | Cone-shape motor with JZQ250 speed reducer, V-belt drive |
| Delivery Device | Cycloidal pin wheel speed reducer, chains, V-belt drive |
| Material Storing Device | Material releasing hopper + material storing hopper |
| Machine Frame | Dragon gate style, super steel construction, four vertical wear-resisting shafts |
| Automation Level | Semi-automatic (mechanical and electronic combination) |
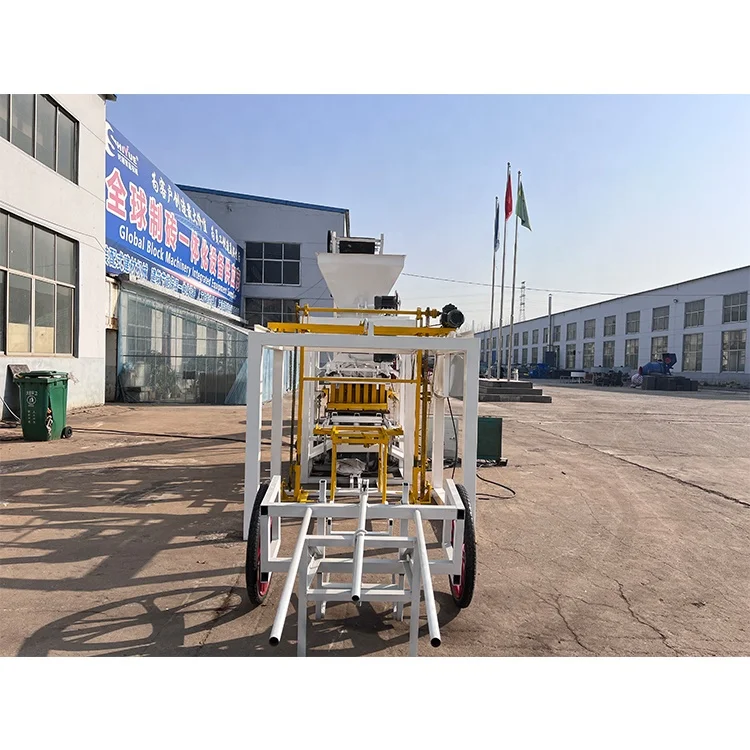
| Supporting Equipment | JQ350 pan mixer, 6m belt conveyor, optional auto stacker, trolley |
| Assembly State | Stationary, requires fixed installation |
| Voltage & Frequency | (basis to be confirmed before production) |
| Cycle Time | (basis to be confirmed per block format) |
| Output Capacity | (basis to be confirmed per block format and cycle time) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block production | Concrete mixes using local crushed stone, river sand and cement for 390×190×190mm masonry units |
| Solid brick manufacturing | Standard concrete or sand-cement mixes for 240×115×53mm bricks used in load-bearing and partition walls |
| On-site construction block making | Aggregate and cement available at project sites for housing and development contractors producing blocks locally |
| First-time block plant entrepreneurs | Semi-automatic operation with a manageable learning curve, producing hollow blocks and solid bricks for regional building material markets |
What "Output Per Hour" Leaves Out When Sizing a QTJ4-24 Block Machine
Real daily output depends on the block format you actually sell, not the fastest cycle the press can run.
Capacity figures quoted for the QTJ4-24 block machine specifications often assume a single mould format and ideal material flow, yet most plants run two or three formats across a shift. When the sand contains high clay content, the vibration force required to achieve target block density increases, cycle time lengthens, and mould wear accelerates. I have seen operators lose an entire shift to a format changeover that was never timed at the factory, turning what was sold as a flexible machine into a single-format press. [NEED_CITE: block machine capacity calculation standards by format]
Mould Format and Honest Capacity Planning
The QTJ4-24 semi-automatic block machine how to choose discussion starts with the block your market actually buys. The standard hollow block mould produces 4 pieces of 390×190×190mm per cycle, while the solid brick mould yields 21 pieces of 240×115×53mm per cycle. These are fixed numbers determined by pallet size and mould geometry, so daily output is a function of cycle time per format and the number of productive hours you can sustain — not a single headline figure.
Pallet Size as a Line Constraint
The 850×450mm pallet is the dimension that connects the press to your curing yard and forklift. If your existing curing racks are spaced for a different pallet width, every board will need manual repositioning after demoulding. Confirming pallet size against your curing area dimensions and forklift fork width before the order is placed prevents a bottleneck that no amount of press speed can fix. [NEED_CITE: pallet handling and curing yard layout for block plants]
Reading the Vibration and Frame Specs
The lower platform uses two 3 kW vibration motors while a 1.5 kW attached device provides upper vibration. This dual-vibration arrangement compacts the mix from both directions, which is critical when local aggregate varies in particle shape and moisture content. The dragon gate frame with four vertical wear-resisting shafts maintains mould alignment across thousands of cycles, preventing the uneven wall thickness that causes blocks to fail compression tests. The 14.25 kW total power draw tells you the electrical supply requirement — confirm your site transformer capacity and dedicated circuit sizing before the machine arrives.
The Cost of Skipping Mix-Vibration Matching
When vibration force is not calibrated to the buyer’s actual mix design, blocks leave the press looking acceptable but crumble under handling or fail strength tests after curing. I once supported a plant where high-clay river sand was fed into a machine configured for clean crushed sand — the vibration compacted the clay into weak layers, and mould liners wore through in weeks instead of months. The downtime waiting for replacement moulds cost far more than a material test would have. [NEED_CITE: aggregate quality effects on concrete block durability]
Why Buyers Source This Machine Here
Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default — the QTJ4-24 you receive is specified for your sand, your cement ratio and your block dimensions. Mould design covers the formats your market sells, with custom drawings available when standard sizes do not match local building codes. The machine, pallet and handling equipment are quoted as one matched system, so pallet size, mixer capacity and conveyor length are calculated together. Automation level is selectable: start with semi-automatic manual pallet handling and add an auto stacker when volume justifies it. Factory testing runs your specific mould format before dispatch, not a generic no-load run.
Documentation & Verification
- Line layout with capacity calculation stating hollow block and solid brick format assumptions
- Mould drawing confirming pieces-per-mould and dimensional tolerances for 850×450mm pallet
- Pallet specification sheet covering size, material and thickness matched to your curing setup
- Voltage, frequency and control language confirmation recorded before production begins
- Factory test record run on your specified mould format with output data documented
Installation, Commissioning & Support
- Fixed foundation required for the 3600×1700mm working footprint to absorb vibration loads
- Dedicated circuit sized for 14.25 kW total draw with voltage and frequency confirmed pre-shipment
- Machine arrives as a stationary unit requiring on-site assembly and shaft alignment verification
- First commissioning includes vibration force adjustment to your local aggregate and mix design
- Operator training covers mould changeover procedure and cycle time expectations per block format
- Wear parts list provided for vertical shafts, vibration motor bearings and mould liner replacements
Before You Send an Inquiry
Provide the block format your market sells, the local sand or aggregate type you will use, and the daily output you need to sustain. Share your site voltage and frequency, the curing yard dimensions you have available, and whether you already own a forklift sized for 850×450mm pallets. This information allows the QTJ4-24 semi-automatic block machine how to choose process to start from your actual conditions instead of generic assumptions.
Frequently Asked Questions
Q: What is the realistic daily output of the QTJ4-24 for hollow blocks versus solid bricks?
A: The hollow block mould produces 4 pieces of 390×190×190mm per cycle, and the solid brick mould produces 21 pieces of 240×115×53mm per cycle. Daily output depends on the cycle time achieved with your specific mix, the number of productive hours per shift, and how many format changes you run. We provide a capacity calculation per format once your mix and shift pattern are confirmed.
Q: How do I match the 850×450mm pallet to my existing curing yard and forklift?
A: Measure your curing rack spacing and forklift fork width before ordering. The 850×450mm pallet must slide into your existing racks without manual repositioning, and your forklift must handle the loaded pallet width. If your current setup uses a different pallet size, we discuss whether adjusting the curing area or selecting a different machine tier is more practical.
Q: Can the mould be changed on-site, and how long does a changeover take?
A: Mould changeover is performed on-site by your operators using standard tools. The time required depends on whether the new mould is pre-assembled and whether operators have been trained on the procedure. We include mould change training during commissioning so your team can switch between hollow block and solid brick formats without external support.
Q: What voltage and control language options are confirmed before shipment?
A: Voltage, frequency and control display language are confirmed and documented before production begins. This prevents commissioning delays caused by a mismatch between the machine’s electrical system and your site supply. We record these specifications in the order documentation so the machine arrives ready to connect.
Q: How is the vibration force calibrated to my local aggregate and mix design?
A: During factory testing, we run your specified mould format with a mix design that matches your local aggregate characteristics. The dual vibration system — lower platform and upper attached — is adjusted to achieve consistent block density. If your sand has high clay or moisture content, the vibration parameters are set to compensate before the machine ships.