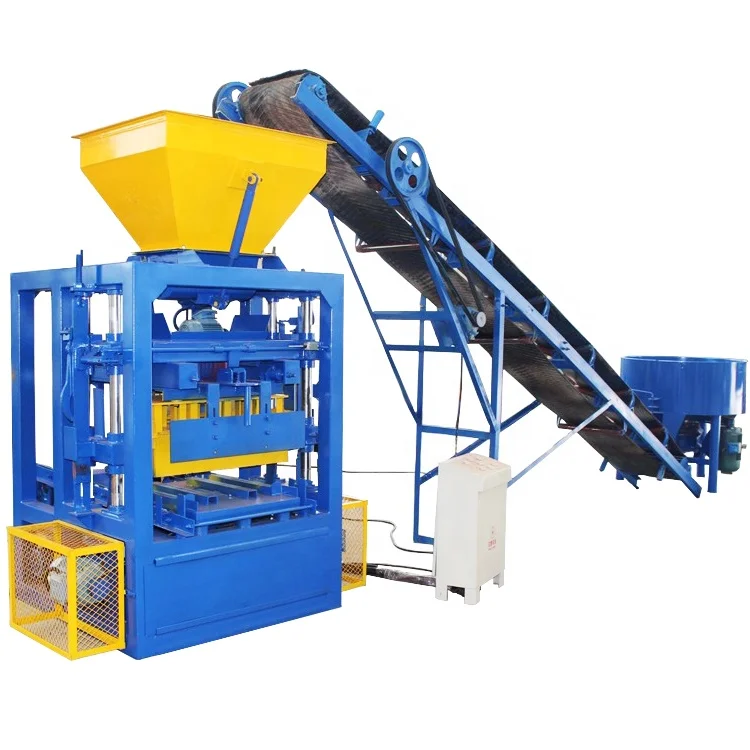
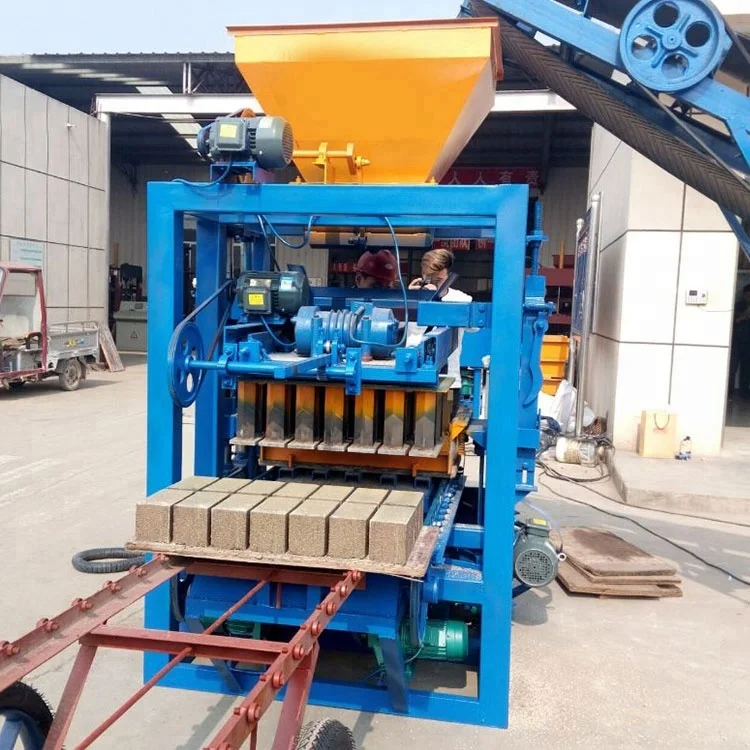
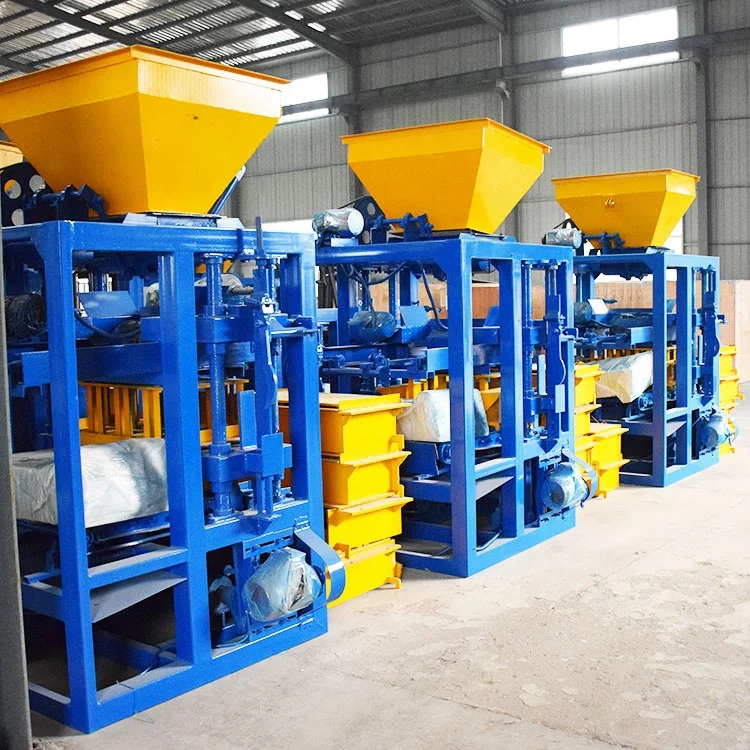
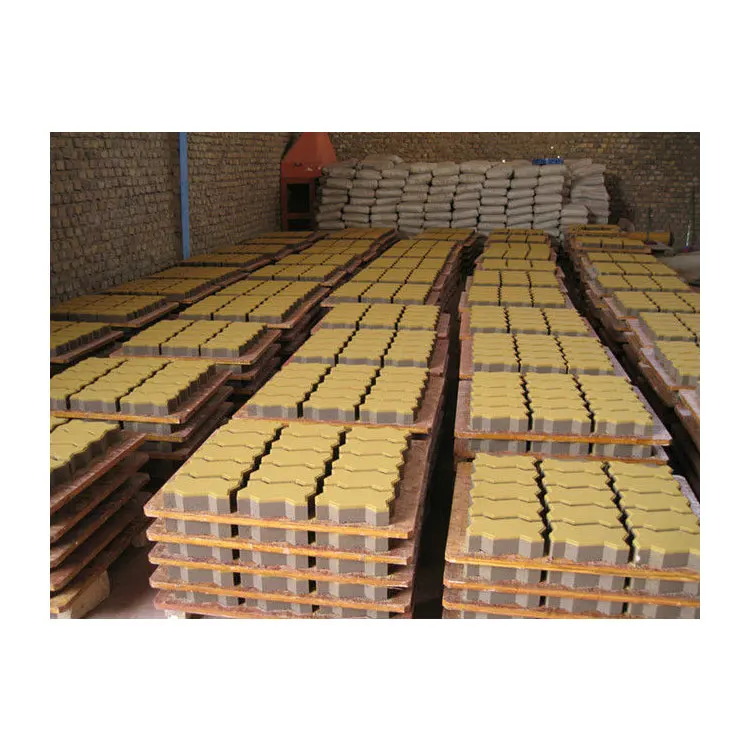

Description
Mould-Matched Output — every cycle time and capacity figure we quote for the QTJ4-24 is tied to a specific block format, pallet size, and your local aggregate, not a single brochure number.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
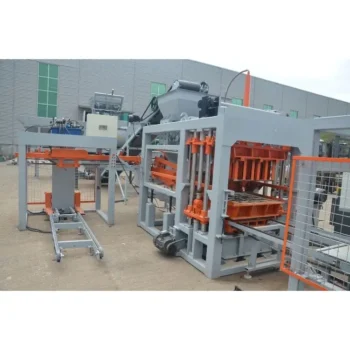
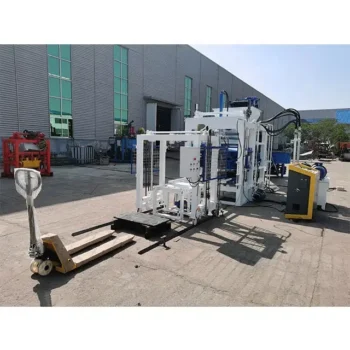
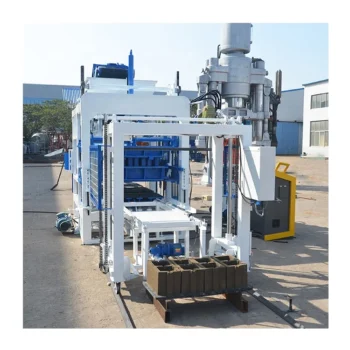
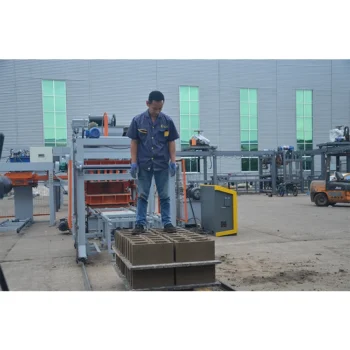
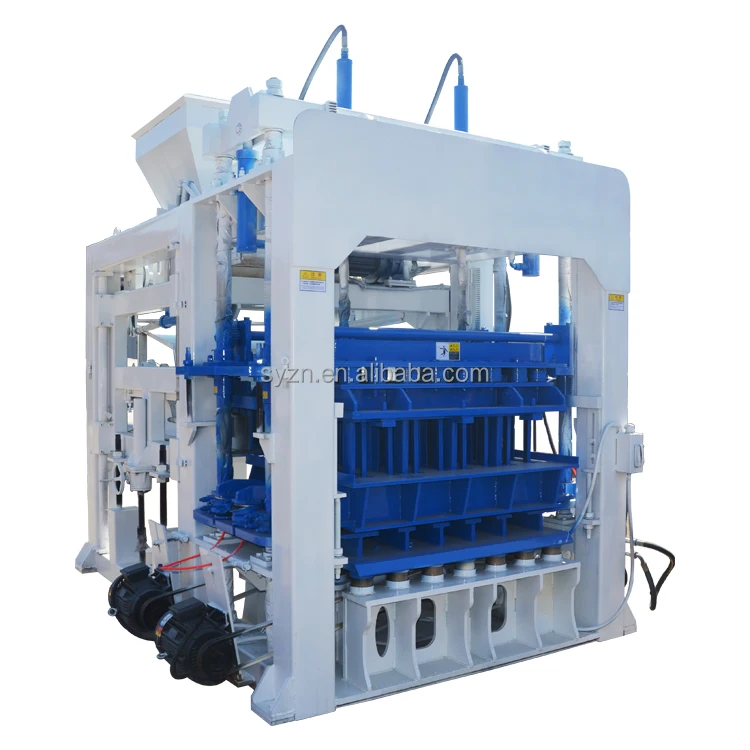
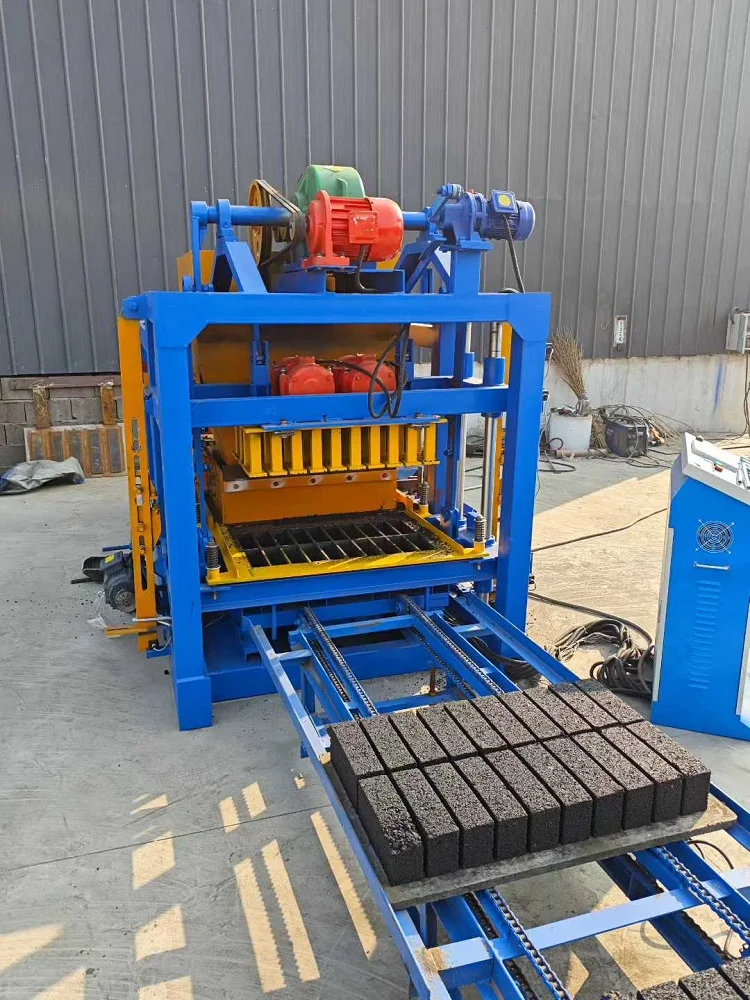
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 2060×1730×2580 mm |
| Main Vibration Form | Platform vibration |
| Vibration Frequency | 4200 r/min |
| Exciting Force | 35.5 kN |
| Rated Pressure | 15 MPa |
| Pallet Size | 880×480×38 mm |
| Molding Cycle | 26 s (basis not stated in source — confirm block format / material / thickness) |
| Total Power | 14.25 kW |
| Voltage & Frequency | 380V, 3-phase, 50Hz (customizable to local voltage) |
| Control System | Electro-mechanical integration (PLC availability to be confirmed) |
| Automation Level | Semi-automatic |
| Mould System | Exchangeable moulds |
| Motor Control | Frequency converting technology on all motors (verify against manufacturer catalog) |
| Warranty | 1 year (excluding wearing parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, water — standard lightweight and heavyweight mixes |
| Interlocking paver production | Fine aggregate and cement with pigment additives for coloured pavers |
| Solid block production | Dense aggregate blends for load-bearing masonry units |
| Small-scale and workshop manufacturing | Low-volume runs for local hardware distributors and on-site contractors |
| Home-business block manufacturing | Startup plants with manual pallet handling and open-air curing yards |
What "26-Second Cycle" Actually Means for Your Daily Output
A cycle number without a block format attached is a guess, not a quotation.
I have watched buyers in Latin America receive a QTJ4-24 block machine specifications sheet that promised a 26-second cycle, only to find that figure assumed a thin solid block while their market needed 150 mm hollow blocks requiring nearly double that time. The daily output they planned around never materialised, and the curing yard sat half-empty for the first month. When you evaluate how to choose the right configuration, start by asking which exact block format and thickness the stated cycle time was measured on — then recalculate your shift output from there [NEED_CITE: block format assumptions in manufacturer cycle time declarations].
Pallet Size Determines Your Curing Layout
The 880×480×38 mm pallet is the physical link between the press and your curing yard. Before you commit to a QTJ4-24 block machine specifications package, measure your existing curing racks and forklift tine spacing. If your racks were built for a different pallet footprint, every wet block will need re-stacking by hand before it enters the curing area — adding labour and breakage risk that no amount of press-side automation can fix.
Mould Change Time vs. Format Rotation Reality
Exchangeable moulds give the QTJ4-24 the flexibility to run hollow blocks in the morning and interlocking pavers in the afternoon, but only if the changeover fits inside your shift schedule. On semi-automatic machines of this class, mould swaps involve loosening clamp bolts, lifting the old mould with an overhead hoist, aligning the new one on the vibration platform, and re-seating the feed shoe. If your production plan calls for three format changes per day, the lost pressing minutes add up quickly and must be subtracted from your capacity calculation [NEED_CITE: typical mould change durations on semi-automatic block presses].
Vibration, Pressure, and Mix Design — The Three-Way Match
Platform vibration at 4200 r/min with 35.5 kN of exciting force works well for standard sand-and-cement mixes, but the story changes when your local aggregate carries high clay content or uses manufactured sand with irregular particle shape. The rated pressure of 15 MPa must be evaluated together with vibration amplitude to achieve target block density. In Colombia, I saw a QTJ4-24 block machine specifications run that arrived on site with factory-set vibration and pressure calibrated for clean river sand; the local crushed stone had a clay fraction that absorbed vibration energy differently, and it took a full week of adjustment before block strength and surface finish came within tolerance. Requesting a sample of your aggregate before the machine is assembled lets the factory tune the frequency converter settings and hydraulic relief valves to your actual material [NEED_CITE: effect of aggregate clay content on vibration compaction in concrete block production].
The Cost of Skipping the Voltage Conversation
One of the most common delays I see on semi-automatic block machine installations is the control panel arriving wired for a voltage or frequency that does not match the buyer’s transformer. The QTJ4-24 is configurable across common industrial voltages, but the confirmation has to happen before the electrical cabinet is closed. When it does not, you face weeks of waiting for replacement contactors and motor overload relays while the machine sits on a concrete pad that has already cured around its anchor bolts.
Why Source the Complete Line From One Supplier
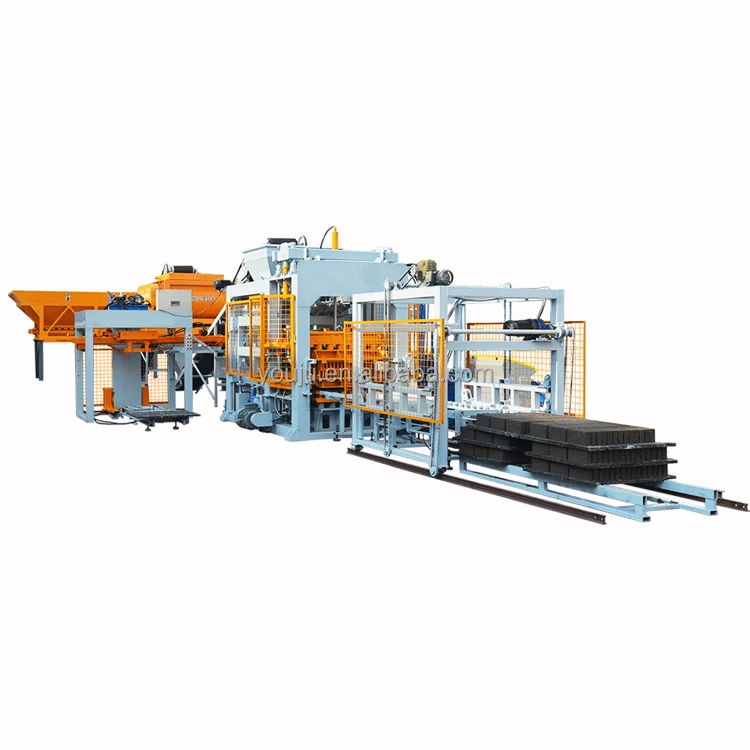
- Machine, mould, pallet, and handling equipment specified as a single matched system, so the 880×480 mm pallet feeds, stacks, and cures without dimensional conflicts.
- Configuration set against your actual mix design and target block format rather than a catalogue default, reducing on-site commissioning rework.
- Mould design covers the formats your local market actually buys, with custom drawings available when standard patterns do not match buyer demand.
- Automation level can start at semi-automatic with manual pallet handling and be upgraded later as volume justifies investment.
- Operator training delivered in your language during commissioning, so the crew understands mould change procedure and daily maintenance from day one.
Documentation & Verification
- Capacity calculation sheet stating output per block format, not a single cycles-per-hour figure
- Mould drawing and format list showing cavity count and product dimensions for each mould
- Pallet specification confirming material grade, weight rating, and dimensional tolerances
- Voltage and control language confirmation signed off before the electrical cabinet is sealed
- Factory test record run on your target block format and mix proportion before dispatch
Installation, Commissioning & Support
- Foundation slab must be level within tolerance to support 2060×1730 mm footprint and vibration loads
- Dedicated 3-phase circuit sized for 14.25 kW total draw with voltage confirmed before cable pull
- Machine ships partially dismantled; re-assembly on site includes platform alignment and mould seating
- First production run includes vibration frequency and pressure adjustment to your local aggregate sample
- Operators trained on mould change sequence, daily greasing points, and pallet feed timing
- Wear parts list with reorder codes provided so hydraulic seals and vibration springs are on hand before first replacement is due
What to Send With Your Enquiry
Tell us the exact block or paver format you intend to produce, including dimensions and target compressive strength. Share a sample or lab report of your local aggregate so we can adjust vibration and pressure settings before the QTJ4-24 leaves the factory. Confirm your site voltage, frequency, and preferred control language, along with the curing yard dimensions you have available for the 880×480 mm pallets.
Frequently Asked Questions
Q: How is the 26-second cycle time measured, and which block format does it assume?
A: The 26-second figure appears in the QTJ4-24 block machine specifications without a stated block format, thickness, or mix type. Cycle time varies depending on whether you are pressing thin solid pavers or deep-cavity hollow blocks. We provide a format-by-format capacity sheet so you can calculate realistic daily output for the specific product you plan to sell.
Q: What mould formats are available for this machine, and what is the output per format?
A: The QTJ4-24 accepts exchangeable moulds for hollow blocks, solid blocks, and interlocking pavers. Output per format depends on cavity count, block height, and compaction requirements. We supply a mould drawing and format list with your quotation so you can see daily output projections for each format before committing to an order.
Q: How does the 880×480 mm pallet affect my curing area layout?
A: Pallet dimensions govern curing rack spacing, forklift tine width, and stacking height. If your existing racks or handling equipment were sized for a different pallet, you will face re-stacking or rack modification costs. Confirm your curing infrastructure dimensions early so pallet size can be validated before production begins.
Q: Can voltage and control language be configured before shipment?
A: Yes. The QTJ4-24 supports voltage and frequency customisation for different export markets. Control panel labels and display language are confirmed during the quotation stage so the electrical cabinet arrives ready for immediate connection without component swaps on site.
Q: How long does a mould change take on the QTJ4-24?
A: Mould change duration on a semi-automatic machine of this class involves unclamping, lifting, alignment, and feed shoe re-seating. Exact time depends on operator experience and hoist availability. We include a step-by-step mould change procedure in the operation manual and cover it during on-site operator training.