
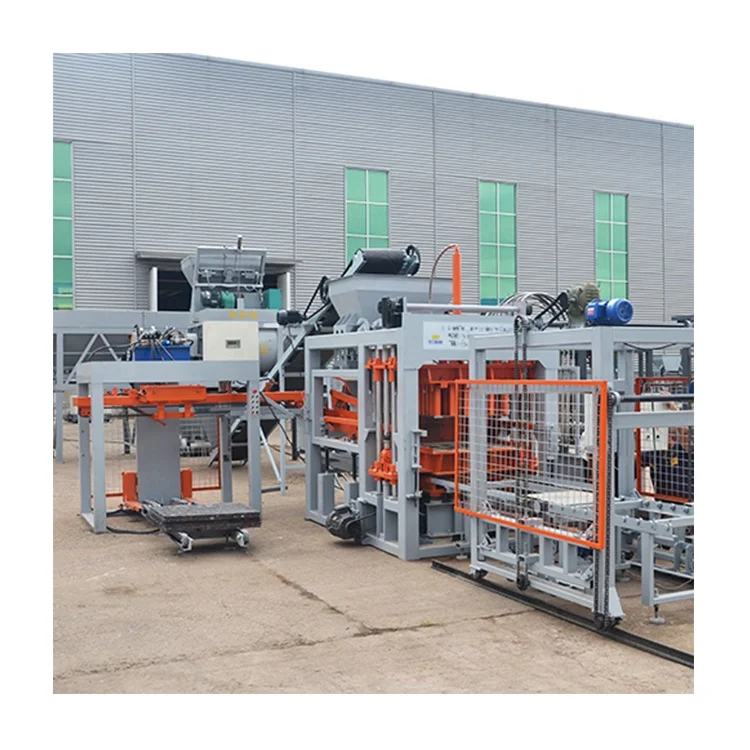
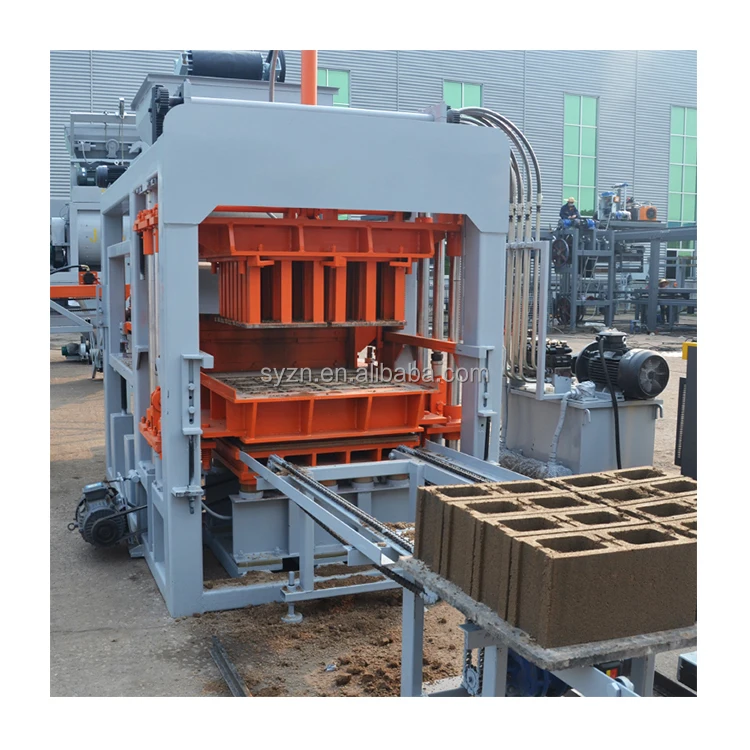

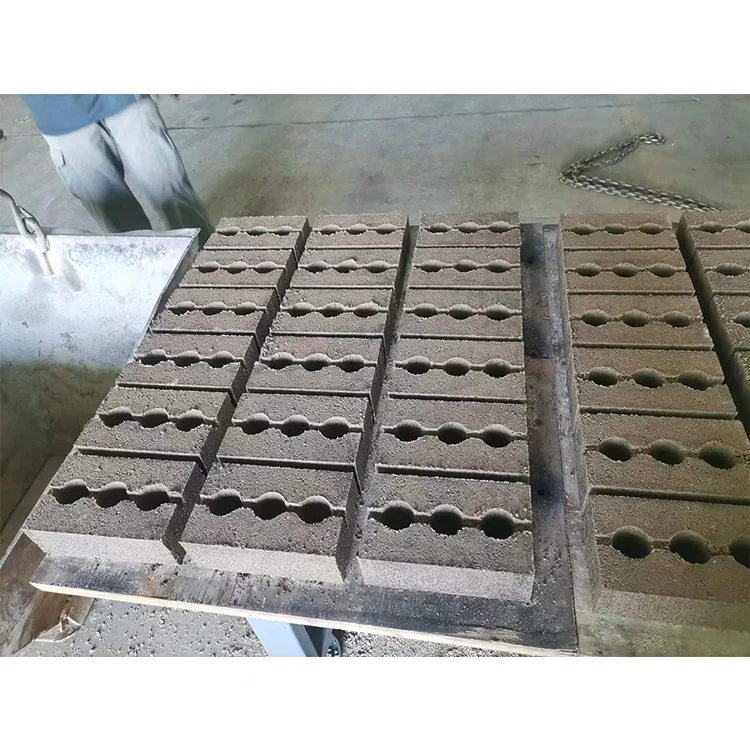
Description
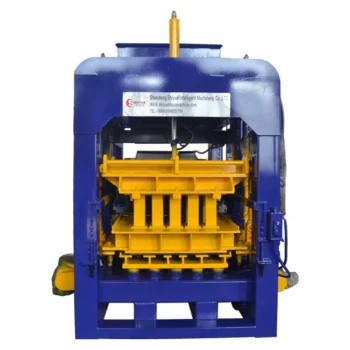
Per-format capacity verified — the QT6-15 is configured against your local aggregate, target block size, and actual mould layout rather than a catalogue default, so the output you plan against matches what the press delivers on the shop floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400 × 1900 × 2660 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Exciting Power (Vibration Force) | 40–50 kN |
| Rated Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 550 × 25 mm |
| Net Weight | 7 T |
| Control System | PLC control system |
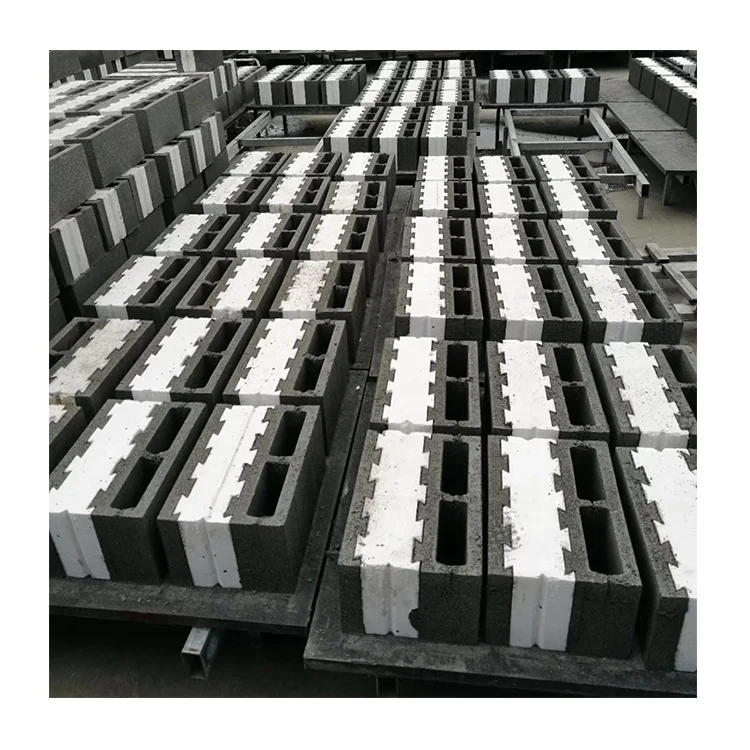
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Hydraulic Station | Included |
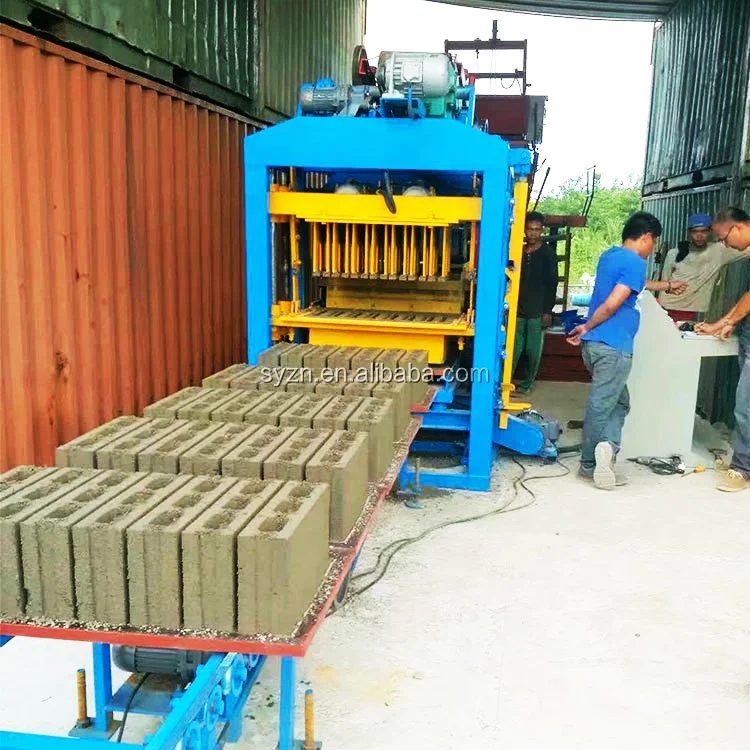
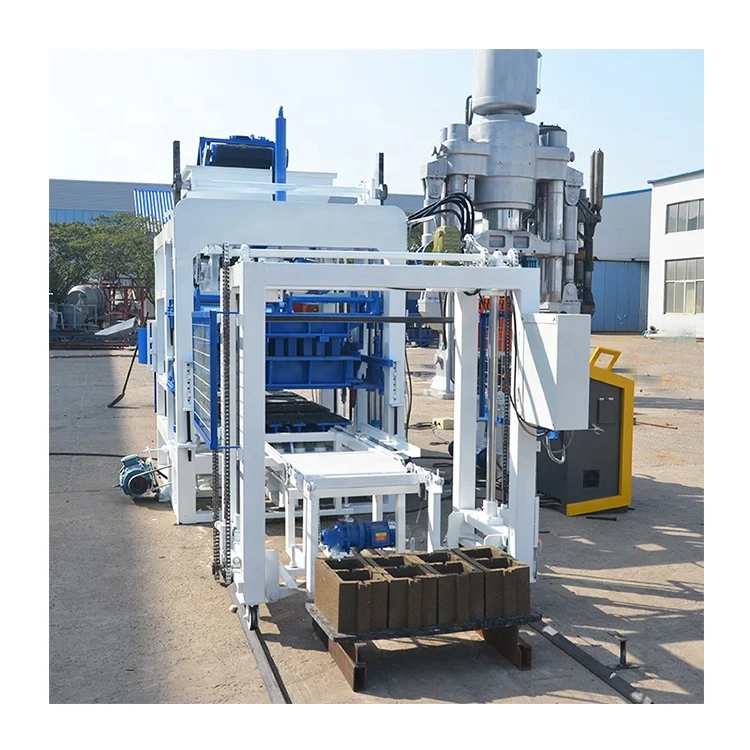
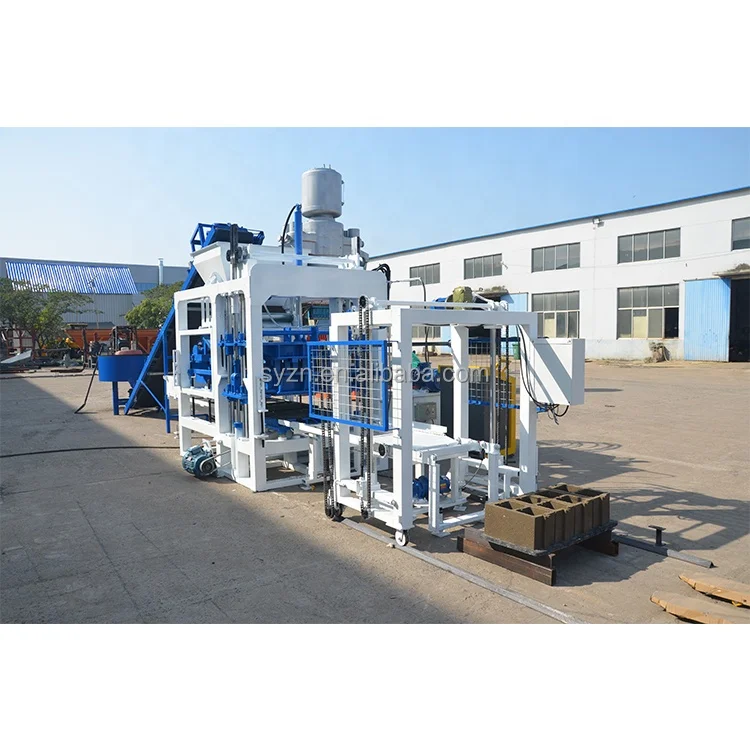
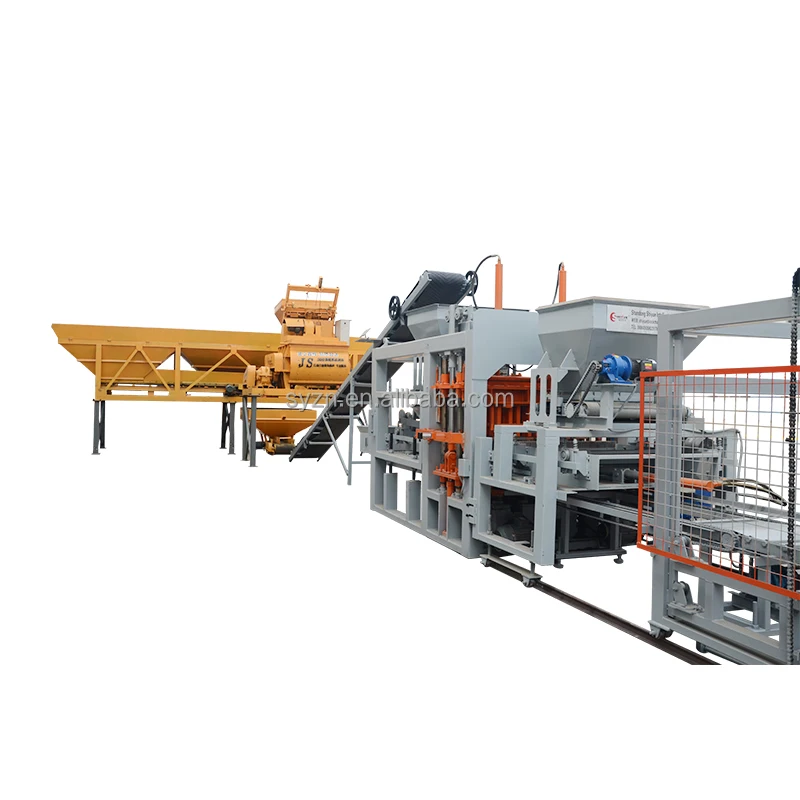
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Free Parts | Manual hydraulic trolley, spare parts and tools |
| Output Capacity (400×200×200 mm hollow block, 15–20 s cycle) | 1200–1680 pcs/h |
| Output Capacity (400×150×200 mm hollow block, 15–20 s cycle) | 1800–2400 pcs/h |
| Output Capacity (240×115×53 mm solid brick, 15–20 s cycle) | 3240 pcs/h |
| Automation Level | Automatic (PLC controlled, with pallet feeder) |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, fly ash mixes forming 400×200×200 mm and 400×150×200 mm formats |
| Solid brick manufacturing for load-bearing and partition walls | Dense aggregate and cement blends producing 240×115×53 mm bricks |
| Paver and interlocking block production for roads and yards | High-strength mixes with fine aggregate and pigment additives |
| Curbstone and kerb formation for municipal infrastructure | Coarse aggregate with high cement content in heavy-section moulds |
What "1200 Pieces per Hour" Leaves Out About Block Machine Capacity
The cycle time and block format behind every capacity number must be stated before the figure has any planning value.
I have watched buyers sign off on a concrete block making machine specifications sheet quoting a single headline output, then discover on commissioning that the figure assumed a small solid brick while their market actually buys 200 mm hollow blocks. The real daily throughput drops because each format demands a different mould cavity count and a different cycle length. Without a per-format breakdown, the gap between quoted and actual production becomes a dispute rather than a calculation [NEED_CITE: block format cycle time variation across hollow and solid products].
The QT6-15 addresses this by listing three separate output bands, each tied to a specific block dimension and cycle range. This is how the how to choose block machine question should be answered — format first, then capacity.
Matching Mould Cavity Count to Your Market Format
Every block size requires its own mould, and the number of cavities in that mould determines how many units the press produces per cycle. A 400×200×200 mm hollow block mould fits fewer cavities on the 850×550 mm pallet than a 240×115×53 mm solid brick mould. The concrete block making machine specifications for the QT6-15 reflect this reality: the same press yields 1200–1680 pcs/h on the larger hollow block and 3240 pcs/h on the smaller solid brick, both at a 15–20 s cycle. Knowing which format your market actually buys is the first step in sizing the line.
Pallet Size and Its Effect on Curing Area Layout
The 850×550×25 mm pallet is the carrier that moves every wet block from the press to the curing rack. If your existing curing racks are spaced for a different pallet dimension, the mismatch forces you to rebuild the rack system or handle blocks manually off non-standard boards. Before confirming the QT6-15, cross-check the pallet specification against your forklift fork width and rack spacing so the handling chain remains unbroken from press to dispatch [NEED_CITE: pallet and curing rack compatibility in block plants].
How Vibration Force and Hydraulic Pressure Work Together
Block density depends on two forces acting at the same moment. The 40–50 kN vibration at 4600 r/min consolidates the mix from below, while the hydraulic station applies downward pressure to close the mould and compress the top surface. If vibration is strong but hydraulic pressure is weak, the block face stays porous; if pressure is high but vibration insufficient, the core remains loose. The QT6-15 pairs both systems so the configuration can be tuned to your specific mix design and local aggregate gradation, producing consistent strength across the batch.
Cycle Time Variation Across Block Formats
A 15–20 s cycle applies to standard hollow blocks and solid bricks where the mix flows freely into the mould cavity. Pavers and curbstones often require longer vibration because their high cement content and denser aggregate resist compaction. The PLC control system on the QT6-15 allows cycle parameters to be stored per mould, so switching from hollow block to paver production does not mean running the new format on the old cycle settings and accepting lower strength.
The Hidden Cost of Specifying Without Local Aggregate in Mind
When a press is configured for a standard river sand mix but the buyer’s region only has weathered sand or crushed stone dust, the vibration force that works on the catalogue material leaves the local mix under-compacted. Blocks leave the press looking acceptable but fail the strength test after curing. I have seen entire production runs scrapped because the exciting power and cycle time were never re-matched to the aggregate the buyer could actually source [NEED_CITE: aggregate gradation effect on block compressive strength].
Why Specify the QT6-15 Through This Supplier
Block machinery is the single focus here, so the QT6-15 press, mould, pallet and handling equipment are specified as one matched system rather than assembled from unrelated sources. The configuration is set against your actual mix design and target block format, not a catalogue default. Mould design covers the formats your market sells, with custom drawings available when standard cavity layouts do not match. Automation level is selectable, allowing a buyer to begin with pallet feeder and conveyor basics and add stacking functions later. Installation support includes operator training on the PLC interface and mould change procedure.
Documentation & Verification
- Line layout showing pallet flow from feeder through press to curing rack
- Per-format capacity sheet stating mould cavity count and cycle for each block size
- Pallet specification cross-referenced to your curing rack spacing and forklift
- Voltage and PLC display language confirmation before production release
- Factory test record on your target block format before dispatch
- Mould drawing and format list for every block type in your quotation
Installation, Commissioning & Support
- Foundation plan sized for the 7400 × 1900 mm footprint and 7 T operating weight
- Dedicated power circuit for the 31.25 kW rated load at your confirmed voltage and frequency
- Machine arrives as press, hydraulic station, pallet feeder and conveyor for on-site assembly
- PLC parameters set to your confirmed block format and cycle time during commissioning
- Operator training on mould change procedure and daily vibration system inspection
- Wear parts list covering hydraulic seals, vibration springs and pallet guide rollers
What to Share Before Requesting a Quotation
To size the QT6-15 accurately, provide the block formats your market currently buys, the target daily output for each format, and a sample or description of your local aggregate and sand source. Confirm the voltage, frequency and PLC display language required at your site, along with the curing rack dimensions and forklift capacity you already have in place.
Frequently Asked Questions
Q: How is the 1200–1680 pcs/h figure calculated for the QT6-15?
A: That output range assumes a 400×200×200 mm hollow block produced at a 15–20 s molding cycle. The press completes one cycle every 15–20 seconds, and the mould cavity count for that block size determines how many units each cycle yields. Different block formats produce different hourly totals on the same machine.
Q: What mould formats can the QT6-15 run, and are custom moulds available?
A: The press accepts moulds for hollow block, solid brick, paver and curbstone on the 850×550 mm pallet. Custom mould designs are produced to buyer drawings when standard cavity layouts do not match the dimensions your local market requires.
Q: How does cycle time change between hollow block and paver production?
A: Standard hollow blocks and solid bricks typically run at 15–20 s per cycle. Pavers and curbstones with denser aggregate and higher cement content may need extended vibration within the 15–25 s range to reach full compaction and strength.
Q: How is the machine configured for my local raw material?
A: The vibration force and hydraulic pressure are matched to your actual aggregate type and mix design rather than a default setting. Providing a sample of your local sand and crushed stone allows the exciting power and cycle time to be adjusted before the press ships.
Q: What pallet size does the QT6-15 use, and why does it matter?
A: The machine uses an 850×550×25 mm pallet. This dimension must align with your existing curing rack spacing and forklift fork width so that wet blocks move from press to curing area without manual re-handling or rack modification.