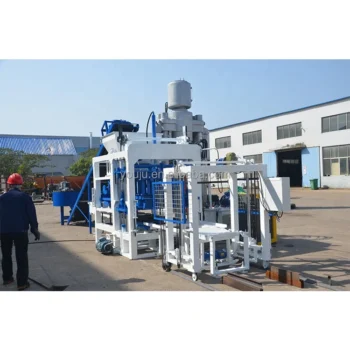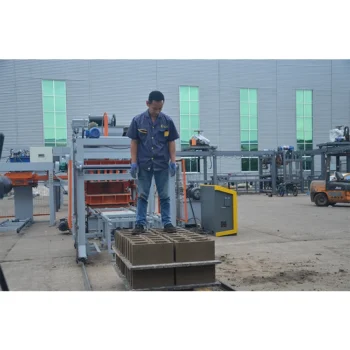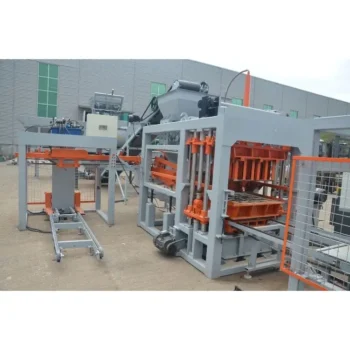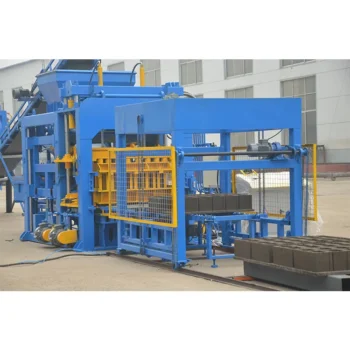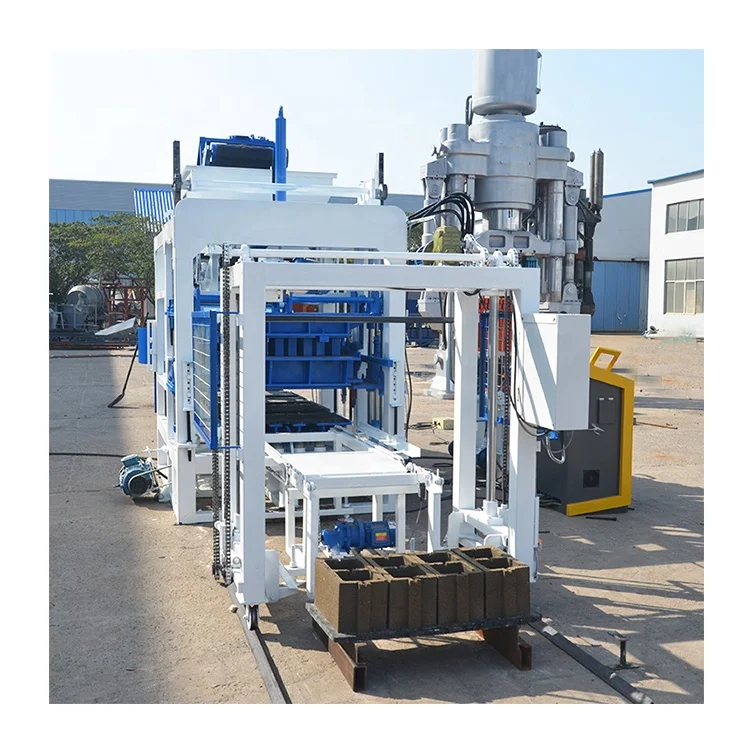
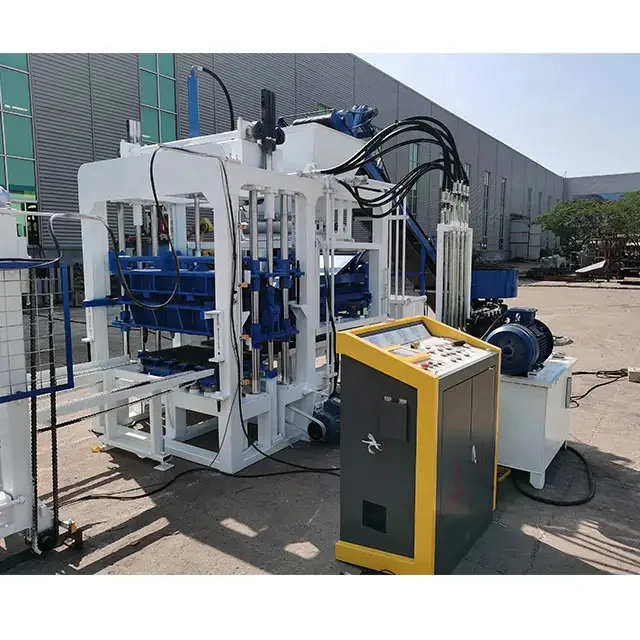
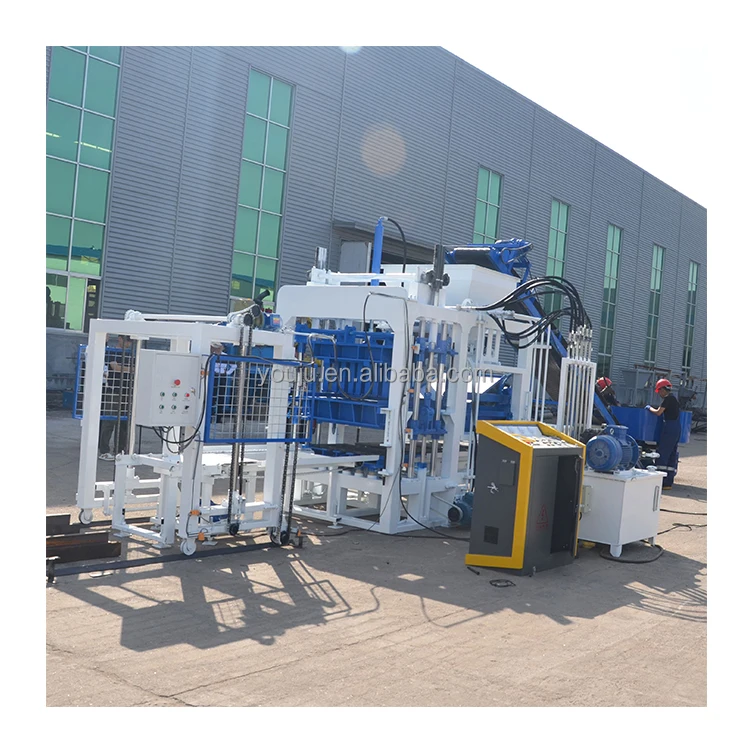
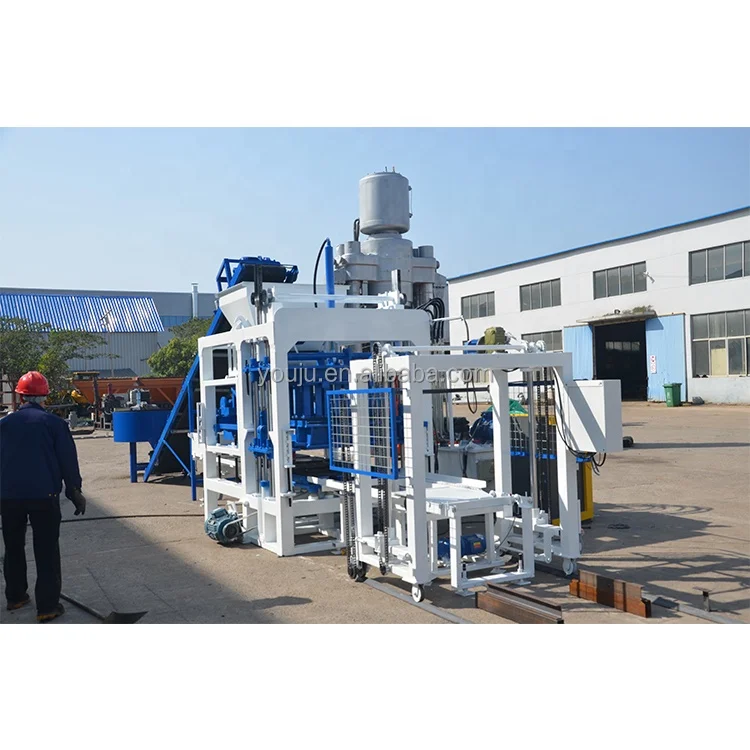
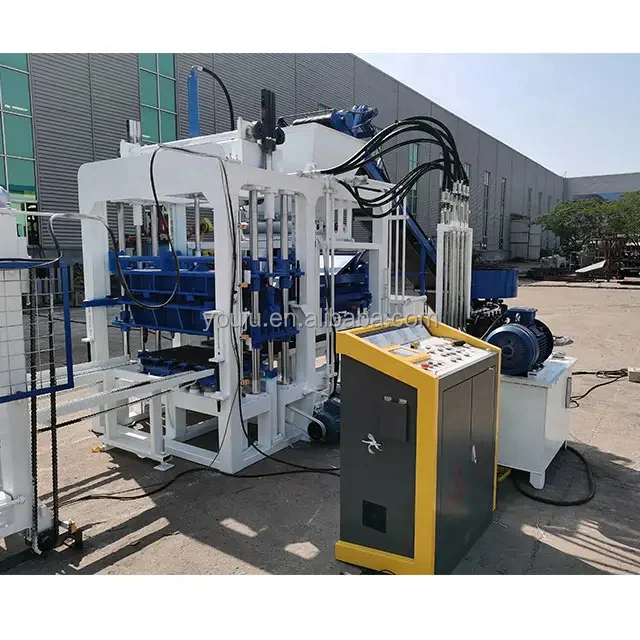
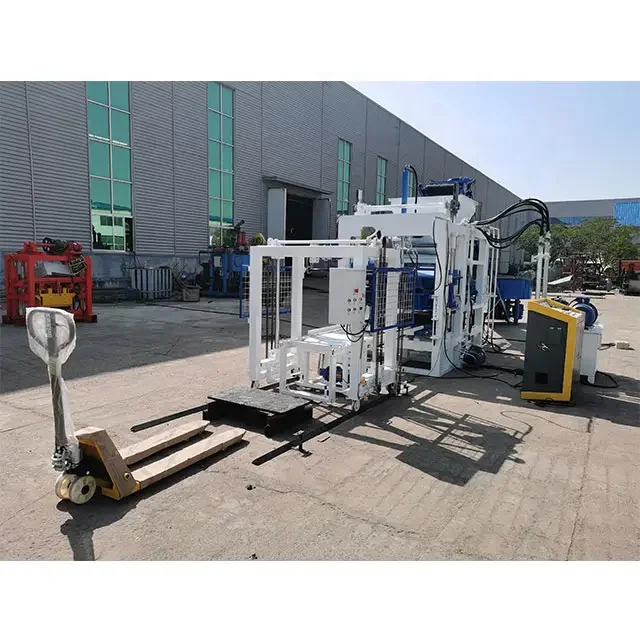
Description
Matched System Configuration — Every component from the 950×550mm pallet to the JQ500 pan mixer is selected against your local aggregate and block format, not pulled from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimension | 2500×1750×2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550 mm |
| Molding Cycle | 18–25 s (basis to be confirmed per block format) |
| Overall Power | 27.5 kW |
| Control System | PLC with frequency converter |
| Mould Lifting Mechanism | Double-sided synchronous gears |
| Electrical Components | Schneider |
| Supporting Mixer | JQ500 concrete pan mixer |
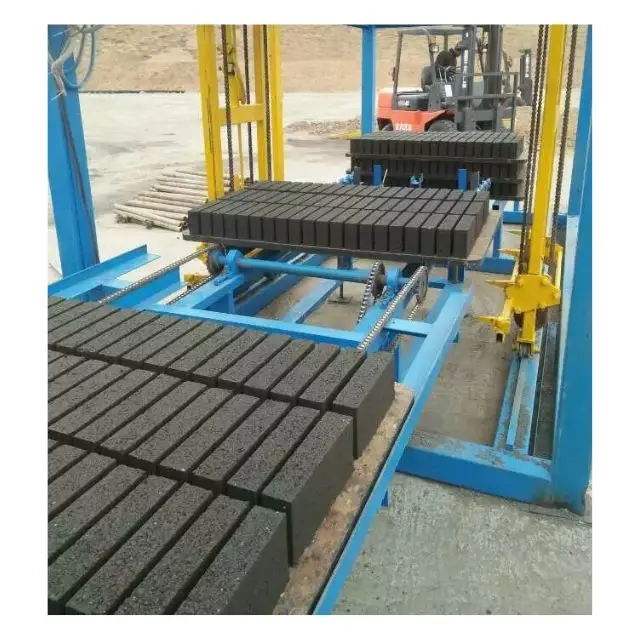
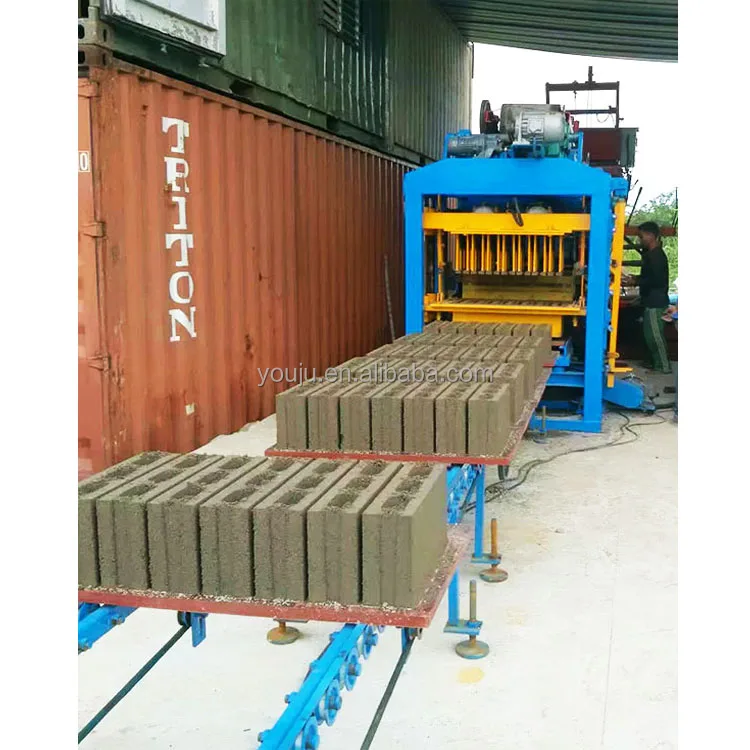
| Belt Conveyor | 8 m standard (6 m optional) |
| Automation Level | Semi-automatic, manual pallet handling to curing yard or stacker option |
| Voltage & Frequency | Configurable to buyer site requirement (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Concrete hollow block production | Cement, crushed stone, sand and fly ash mixes |
| Solid block and paving block formats | Interlocking and kerbstone profiles via mould change |
| On-site contractor block production | Local aggregate with variable grading |
| First block plant setup | Small-to-medium output with room for automation expansion |
What the 18–25 Second Cycle Actually Means for Your Output
Cycle time is only useful when tied to the exact block format and thickness you intend to sell.
I spent years on the factory floor running test cycles before moving into sales, and one lesson stuck hard: quoting a cycle range without naming the block format behind it leaves buyers guessing. The QT4-18 concrete block machine specifications list an 18–25 second molding window, but a thin paving block and a 200 mm hollow block do not share the same compaction demand. A buyer who plans production around the shorter end of that range may find daily output falling well short once the press meets a denser mix. [NEED_CITE: relationship between cycle time and block density in vibration compaction]
This is why the first document I prepare for any enquiry is a capacity table that names each block format, the pallets per cycle for that format, and the realistic daily total. Without that, you are comparing machines on a number that does not belong to your product.
Pallet, Curing Area and Forklift Must Align Before the Press Arrives
The 950×550 mm pallet on the QT4-18 concrete block machine specifications is not an arbitrary choice; it determines how many blocks sit in one layer and how those layers stack on your curing racks. If your existing racks were built for a different pallet footprint, you face a costly rack replacement or live with wasted curing space. The same logic applies to your forklift tine spacing and load rating. I always ask buyers to send a sketch of the curing yard and the forklift data plate before finalising pallet orders, because a mismatch discovered after the container arrives is one you pay for twice. [NEED_CITE: pallet-to-curing-rack compatibility standards in block production]
Mould Change Flexibility and the Time It Actually Costs
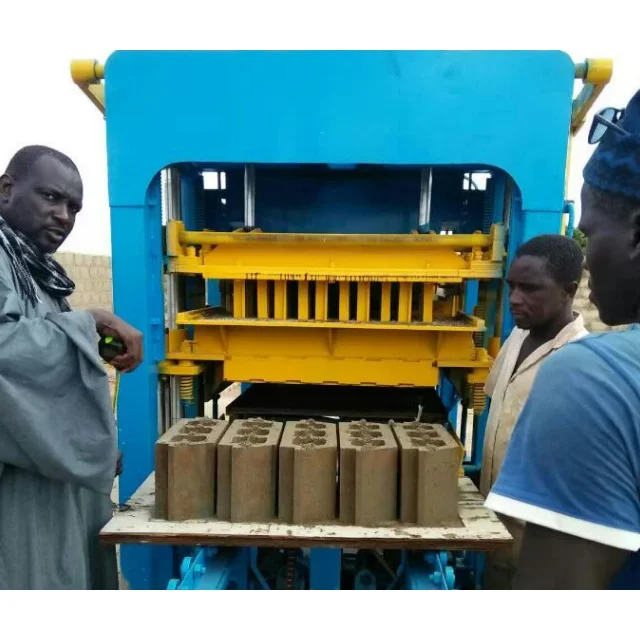
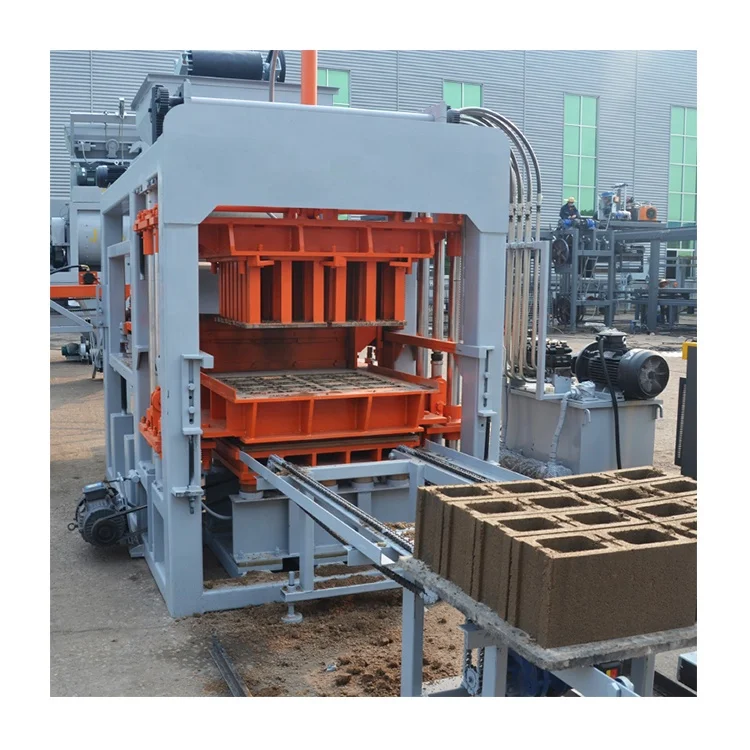
The manual bolt-release mould system on this press is straightforward, but "straightforward" still means the operator must unfasten, extract the old mould using the block conveyor as a pallet-assisted slide, and seat the new one. If your market demands three block formats in a single shift, that changeover window eats into production. Buyers who know their format rotation frequency can decide whether the manual system fits or whether they should look at a faster clamping arrangement. The QT4-18 concrete block machine specifications list a free hollow block mould with the base order, and additional format moulds are available to custom drawings.
Reading the Pressure and Vibration Figures Together
The rated pressure of 16 MPa and the platform vibration form work as a pair, not independently. Hydraulic pressure forces the mould head down while vibration consolidates the mix from below; if either value is mismatched to your aggregate hardness, the resulting blocks show density variation across the pallet. Volcanic scoria, for example, absorbs vibration energy differently from river gravel, and the frequency converter on the PLC allows on-site tuning once the line is running. The double-sided synchronous gear lifting mechanism keeps the mould head level during withdrawal, which matters most when block height tolerance is tight. Overall power draw of 27.5 kW includes the JQ500 pan mixer and 8 m belt conveyor, so the electrical supply must cover the full line, not just the press. [NEED_CITE: hydraulic pressure and vibration force matching for different aggregate types]
When a Specification Sheet Hides the Real Cost
I have watched buyers sign off on a machine based on a cycle figure, only to discover that their local mix requires longer compaction to reach the target block strength. The press still runs, but output drops and the operator adds cement to compensate, raising unit cost silently. Voltage and PLC language are another quiet trap: if the 50 Hz or 60 Hz requirement is not written on the purchase order, the motor and frequency converter arrive mismatched and commissioning stalls. [NEED_CITE: voltage and frequency standards by export market]
Why Configuration Here Is Tied to Your Site
- Machine, mould, pallet and handling equipment are specified as one system rather than sourced from separate vendors and bolted together on site.
- The mix design you actually use — with your local aggregate sample — sets the vibration and pressure parameters, not a factory default tested on standard sand.
- Mould design covers the block formats your market sells, and custom drawings are accepted for profiles outside the standard catalogue.
- Automation level is selectable; the semi-automatic pallet handling on the QT4-18 can be supplemented with a stacker now or a full stacking and cubing line later.
- Installation and operator training are included so the first week of production is not spent troubleshooting parameter settings.
Documentation & Verification
- Line layout showing pallet flow from press to curing area with cycle times stated per block format
- Mould drawing package covering every format on your order, with dimensional tolerance callouts
- Pallet specification sheet matched to your curing rack spacing and forklift load rating
- Voltage, frequency and PLC display language confirmed in writing before production release
- Factory test record run on your submitted aggregate sample before the machine is crated
Installation, Commissioning & Support
- Foundation slab must carry the 2500×1750 mm footprint and the dynamic load of platform vibration
- Dedicated 27.5 kW circuit with correct voltage and frequency confirmed before energising the PLC
- Belt conveyor ships as one 8 m section; alignment with the press feed hopper checked on site
- First production run supervised to tune frequency converter settings against your mix design
- Wear parts list with part numbers provided so reorder lead times stay short
- Operator training covers mould change procedure and double-sided gear lifting safety
What Your Enquiry Should Include
Send the block formats you intend to produce, including target dimensions and minimum compressive strength. Include your local aggregate type and any sample you can ship, along with the available voltage and frequency at the installation site. If your curing yard and forklift are already in place, share the rack dimensions and forklift data plate so the 950×550 mm pallet can be verified against them before the order is written.
Frequently Asked Questions
Q: What block format is the 18–25 second cycle based on, and what is the realistic daily output?
A: The QT4-18 concrete block machine specifications list 18–25 seconds as a range that shifts with block height, mix density and target strength. Realistic daily output is calculated per format after we test your aggregate sample on the press, so the capacity table you receive names each block and its pallets-per-cycle figure.
Q: How long does a mould change take on the QT4-18 and what tools are required?
A: The manual bolt-release system uses standard spanners and the block conveyor assists extraction. Changeover time depends on operator familiarity and mould weight, so we recommend timing the first change during training and recording it for production planning.
Q: Is the 950×550 mm pallet compatible with my existing curing racks and forklift?
A: Pallet dimensions must be checked against your rack bay width and forklift tine spacing before the order is placed. Send us the rack layout and forklift data plate, and we confirm fit or adjust pallet size within the press platform limits.
Q: Which voltage, frequency and PLC language will the machine ship with?
A: These values are confirmed in writing during the order stage. The PLC with frequency converter is configured to your site supply and the display language you specify, so commissioning is not delayed by mismatched electrical parameters.
Q: Can I start semi-automatic and upgrade stacking or automation later?
A: Yes. The semi-automatic layout handles pallets manually to the curing yard, and a stacker or full cubing line can be added when volume justifies the investment. The press control and pallet size remain unchanged, protecting your initial setup.