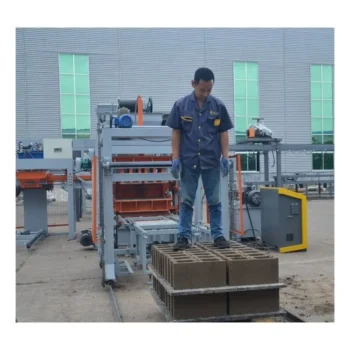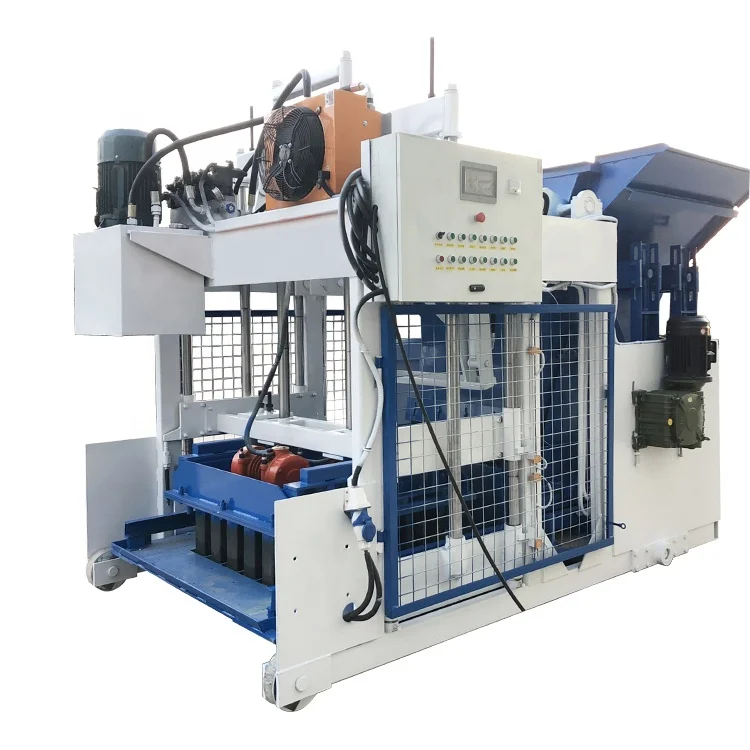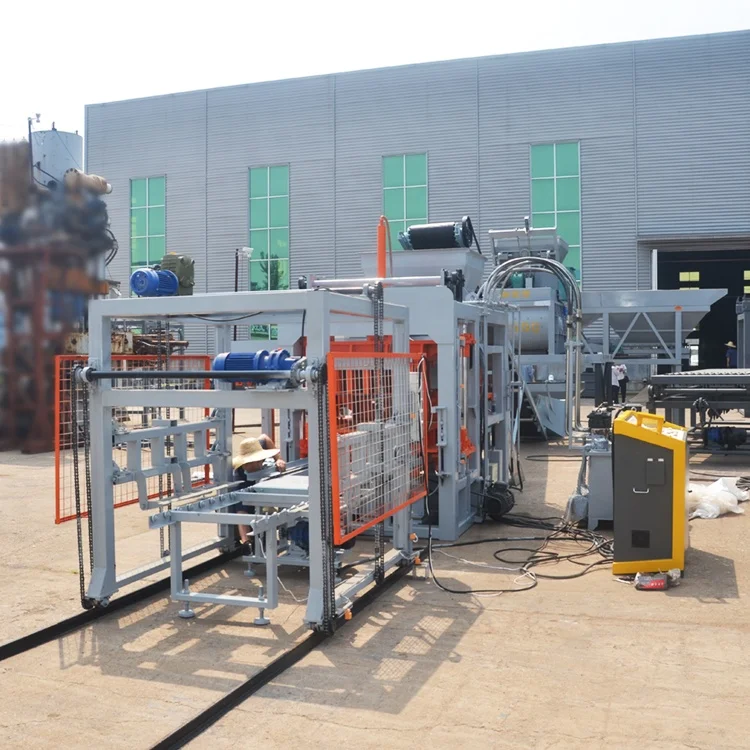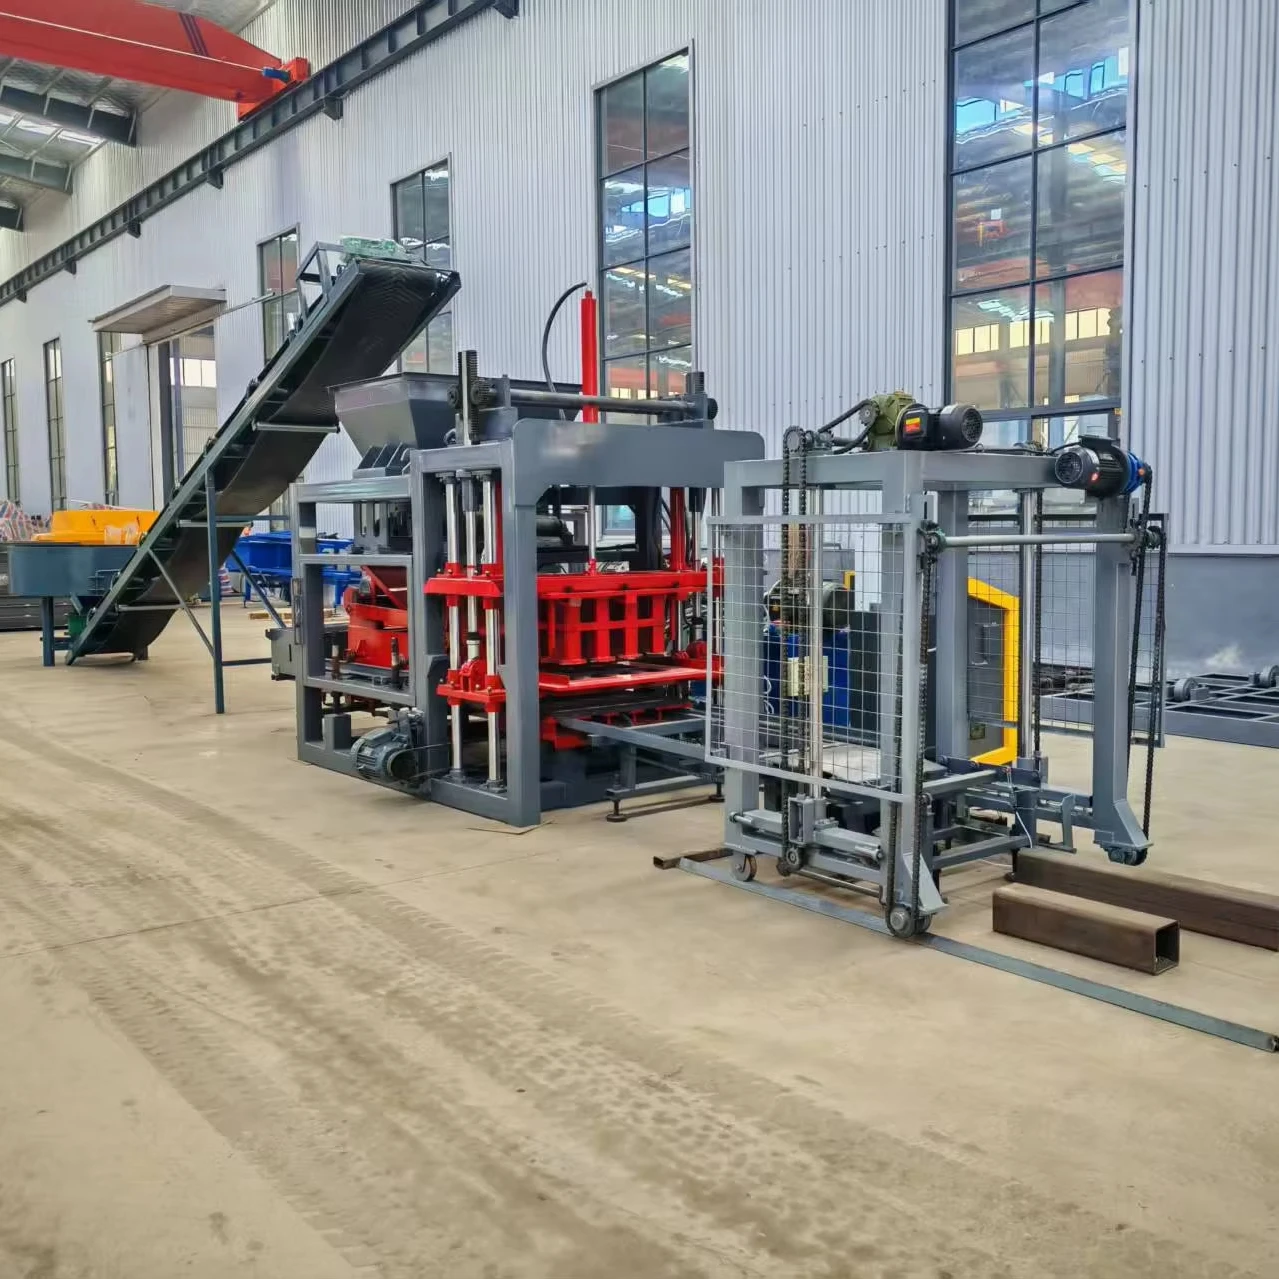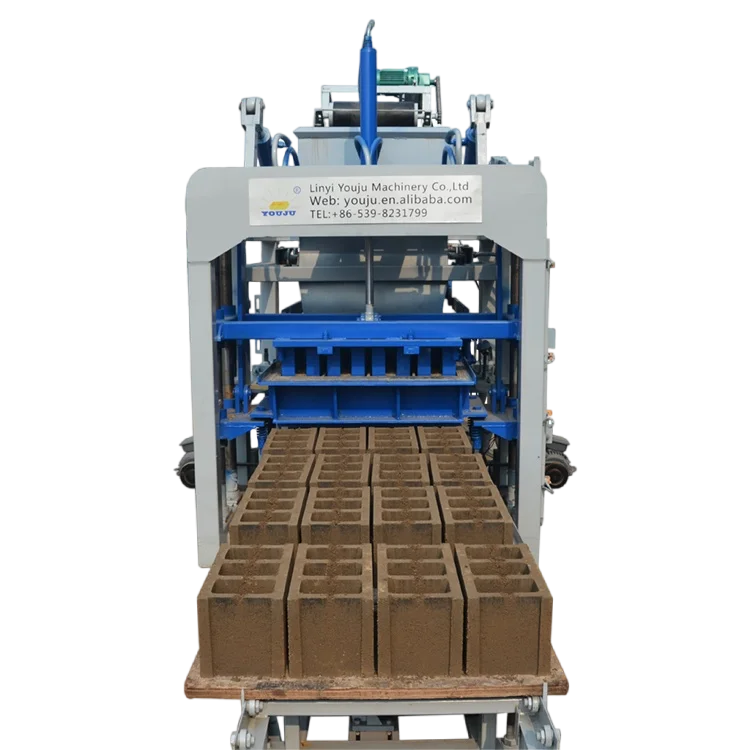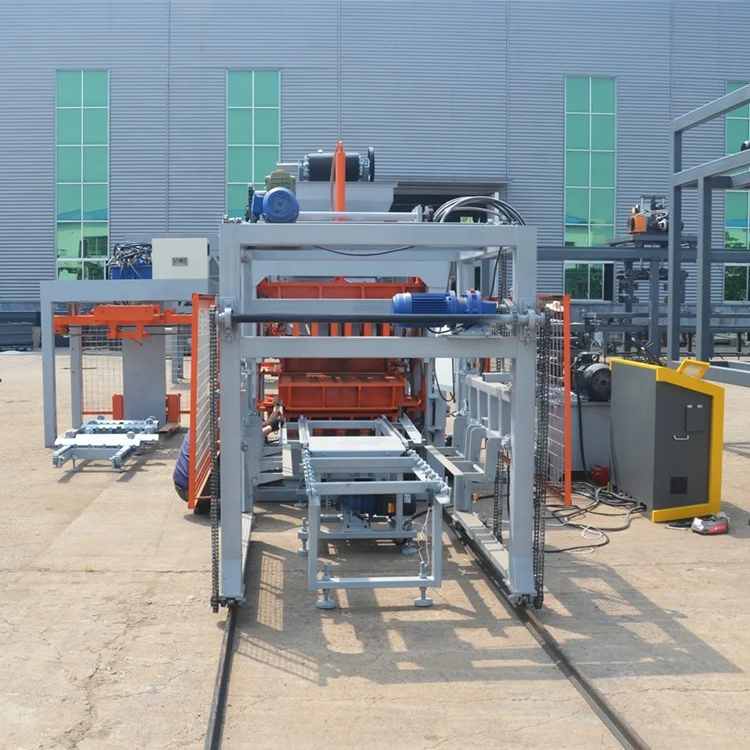
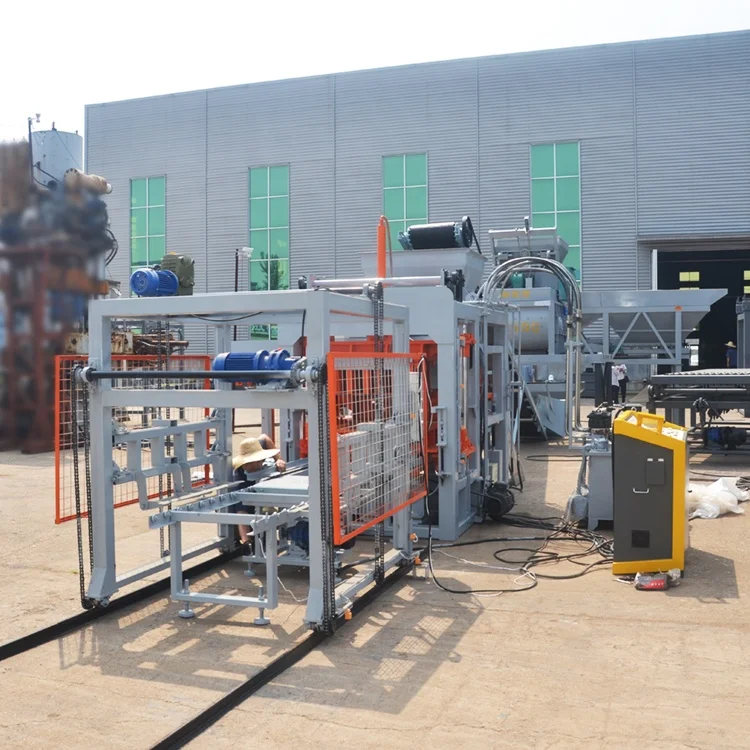
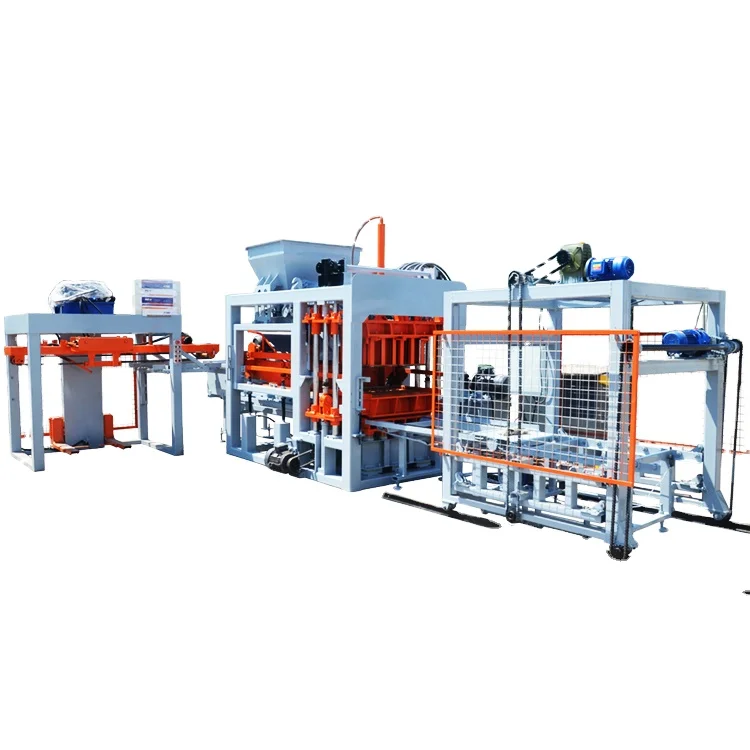
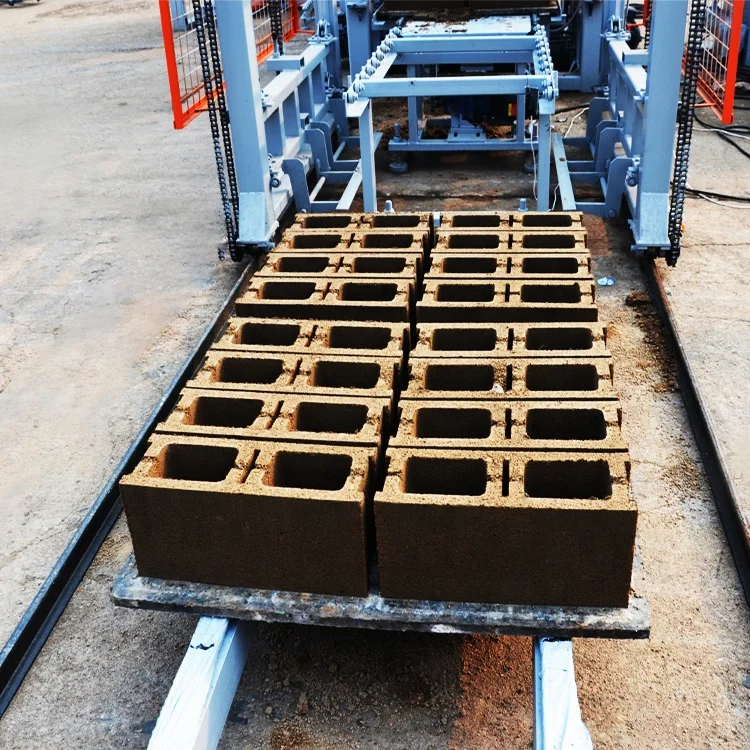


Description
Matched System Approach — Every QT6-15 configuration starts with the buyer’s block format and local aggregate, not a catalogue default that leaves mould, pallet and handling misaligned.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Hydraulic Automatic Block Making Machine |
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Vibration Frequency | 0-60 Hz (adjustable) |
| Vibration Form | Platform Vibration |
| Moulding Mode | Automatic loading with vibration moulding |
| Pallet Size | 880×850 mm |
| Molding Cycle | 15-20 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 37 kW |
| Vibration Force | 45 kN |
| Total Mass | 7 T |
| Demolding Method | Hydraulic |
| Recommended Factory Area | 1200 m² |
| Control System | PLC (Programmable Controller) with touch screen interface |
| Output Capacity (Hollow block 400×200×200 mm) | 1080-1440 pcs/h, 8640-11520 pcs/8hr |
| Output Capacity (Hollow block 400×150×200 mm) | 1440-1920 pcs/h, 11520-15360 pcs/8hr |
| Output Capacity (Solid brick 240×115×53 mm) | 5760-7680 pcs/h, 46080-61440 pcs/8hr |
| Output Capacity (Rectangular brick 200×100×60 mm) | 2160-2880 pcs/h, 17280-23040 pcs/8hr (cycle 20-25 s) |
| Output Capacity (Zigzag brick 225×112.5×60 mm) | 2160-2880 pcs/h, 17280-23040 pcs/8hr (cycle 20-25 s) |
| Block Compressive Strength | More than 15 MPa |
| Hydraulic System | Independent integrated hydraulic station |
| Fault Diagnosis | Built-in fault diagnosis system with action interlock logic |
| Voltage & Frequency | Configurable — confirm before order |
| PLC Display Language | Configurable — confirm before order |
| Automation Level | Automatic (mechanical-hydraulic-PLC synthesis) |
| Raw Material Adaptability | Waste ash, slag, and various aggregates; reduces cement dosage |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid brick production for structural and infill masonry | Local aggregates with standard cement ratios |
| Rectangular and zigzag paving brick production | Fine aggregates with reduced cement content |
| Production using industrial waste materials | Waste ash, slag, and recycled aggregates |
| Block plants with established curing areas | Minimum 1200 m² factory footprint required |
Why "Pieces per Hour" Means Nothing Without the Block Format
Capacity figures detached from a specific block size and cycle time are the single biggest reason daily output disappoints after commissioning.
A buyer sees a headline number, places the order, and then discovers the machine was rated on a format their market does not buy. The QT6-15 hydraulic block machine specifications list five distinct formats, each with its own cavity count, cycle time and eight-hour output. Hollow blocks at 400×200×200 mm run at a different cadence than 60 mm paving bricks, and pretending otherwise leaves a plant owner chasing numbers that never materialize on the shop floor [NEED_CITE: block machine capacity calculation standards by format].
Format-Specific Output That Survives the First Shift
The QT6-15 hydraulic block machine specifications break output into five block formats because each one demands a different mould cavity layout and pressing cycle. A 400×200×200 mm hollow block yields 8640-11520 pieces per eight-hour shift, while the same machine running 240×115×53 mm solid bricks reaches 46080-61440 pieces over the same period. This spread exists because cavity count and cycle duration change with format — not because the machine suddenly works harder.
Pallet Size as the Hidden Constraint on Curing Logistics
The 880×850 mm pallet is the physical link between the press and the curing area. If the buyer’s existing racks, stacking height or forklift fork width were sized around a different pallet dimension, every loaded board becomes a handling problem before the blocks even cure. Confirming pallet compatibility is not a paperwork exercise; it determines whether output moves smoothly to the yard or piles up at the machine exit [NEED_CITE: pallet handling standards in concrete block production].
How Vibration Force and Hydraulic Pressure Shape Block Density
The 45 kN vibration force operates across a 0-60 Hz adjustable range on a platform vibration system, while the independent hydraulic station delivers demolding pressure isolated from frame vibration. These two forces must be matched to the buyer’s specific mix design and local aggregate. A mix high in fine ash responds differently to vibration frequency than one built on coarse crushed stone, and the QT6-15 hydraulic block machine specifications allow tuning within that range rather than locking the operator into a single preset. Compressive strength above 15 MPa is achievable when vibration, pressure and material are correctly aligned.
The Cost of Skipping the Mould Change Conversation
A machine that offers format flexibility on paper can still lose an entire shift to mould changeover if the bolt pattern, alignment method and hydraulic clamp sequence were never discussed before delivery. Buyers who assume all moulds swap in minutes often discover that the change process requires tools, adjustments and trial cycles that consume most of a working day. The QT6-15 supports multiple formats, but the time cost of switching between them must be established during configuration so that daily scheduling reflects reality [NEED_CITE: mould changeover time impact on block plant scheduling].
Why Configuration Starts with the Mix, Not the Machine
A buyer sourcing fly ash or slag locally needs the QT6-15 configured around those materials from the start. The raw material adaptability listed in the QT6-15 hydraulic block machine specifications covers waste ash, slag and various aggregates with reduced cement dosage, but this only holds if vibration frequency, hydraulic pressure and cycle time are set against a sample of the actual mix. A machine tuned for clean river sand will underperform on high-clay local aggregate, and no amount of on-site adjustment fully corrects a configuration that ignored the feed material.
Documentation That Prevents Commissioning Delays
- Factory test record run on buyer’s specified block format and cycle time before dispatch
- Mould drawing and format list showing cavity count for each included block type
- Voltage, frequency and PLC display language confirmation sheet signed before production
- Pallet specification matched to buyer’s curing rack dimensions and forklift capacity
- Line layout with capacity calculation stating the exact block format assumed
- Hydraulic and electrical schematic for on-site maintenance reference
Installation, Commissioning & Support
- Foundation must support 7 T machine mass across the 8200×1700 mm footprint with level tolerance
- Dedicated 37 kW power circuit with confirmed voltage and frequency matching the PLC and hydraulic station
- Machine arrives dismantled for container loading; on-site reassembly includes frame alignment and hydraulic line connection
- First production run verifies cycle time and block compressive strength against the agreed format specification
- Operator training covers PLC touch screen navigation, fault diagnosis system and action interlock logic
- Wear parts list identifies hydraulic seals and vibration platform components requiring scheduled replacement
What to Prepare Before Requesting a Quote
A meaningful QT6-15 proposal requires the exact block dimensions and format the plant will produce, the local aggregate type and source, and the daily output target tied to that specific format. Voltage, frequency and preferred PLC display language should be confirmed early to avoid commissioning hold-ups. If the buyer already operates curing racks and forklifts, their dimensions help verify that the 880×850 mm pallet fits the existing handling setup without modification.
Frequently Asked Questions
Q: How is the QT6-15 output capacity calculated per block format?
A: Each format listed in the QT6-15 hydraulic block machine specifications carries its own mould cavity count, cycle time and eight-hour output figure. A 400×200×200 mm hollow block runs a different cycle than a 60 mm paver, so capacity is stated per format rather than as a single number. Buyers should match their target format to the corresponding row before comparing machines.
Q: Which block formats can one QT6-15 produce and how long does a mould change take?
A: The machine supports hollow blocks, solid bricks, rectangular and zigzag paving bricks through mould swaps. Mould change time depends on the bolt pattern and alignment system specified at order. Confirming this duration during configuration ensures that format switching does not consume a significant portion of the production shift.
Q: How is the machine configured to match my local aggregate and mix design?
A: Vibration frequency adjusts between 0-60 Hz and hydraulic pressure is set against a sample of the buyer’s actual mix. Waste ash, slag and local aggregates are accommodated, but the configuration must reflect what the buyer can source. A machine tuned for unavailable materials creates ongoing production problems.
Q: What voltage, frequency and PLC language will the QT6-15 ship with?
A: These three parameters are configurable and must be confirmed in writing before production begins. The PLC display language affects daily operation, while incorrect voltage or frequency delays commissioning. Locking these details early prevents avoidable on-site issues after delivery.
Q: What pallet size does the QT6-15 use and how does it affect my curing setup?
A: The machine uses an 880×850 mm pallet. This dimension must align with the buyer’s existing curing rack spacing, stacking height and forklift fork width. A mismatch means every loaded pallet requires manual repositioning, slowing the line between the press and the curing yard.